
Featured Article
Injection Molding & Manufacturing Resources
Welcome to the TEAM Rapid Blog, your source for manufacturing insights, engineering expertise, and industry updates. Explore articles on injection molding machining, rapid prototyping, injection molding, materials, and product development.
Browse by Topic
Find practical information on manufacturing processes, material selection, product applications, engineering considerations, and sourcing decisions.
Expert guidance for evaluating suppliers, manufacturing options, and sourcing decisions.
Practical examples and industry applications for custom manufacturing projects.
Material properties, performance characteristics, and selection recommendations.
Learn about manufacturing methods, process capabilities, and production best practices.
Engineering expertise, design considerations, and technical knowledge for product development.
Fundamental machining concepts, injection molding processes, and practical manufacturing expertise.
Latest Insights
Stay informed on injection molding machining, rapid prototyping, injection molding, die casting, and industry trends in custom manufacturing and product development.
-
Global Market Injection-Molded Part Wall Gauge Guide
For most injection-molded plastic parts in the global market, start with a uniform wall gauge between 1.5 mm and 3.0 mm, then adjust it according to resin flow behavior, impact requirements, cosmetic expectations, mold design, and production volume. Commodity plastics such as polypropylene and polyethylene can often use thinner sections, while engineering materials such as polycarbonate, nylon, PBT, and ABS/PC blends usually need more carefully controlled wall thickness to prevent incomplete filling, sink marks, warpage, and internal stress.
The most important rule is consistency. Keep adjacent wall sections within approximately 10% to 15% of each other whenever possible. Instead of making one area excessively thick for stiffness, use ribs, gussets, structural webs, and rounded transitions. Thick plastic sections cool slowly, increase cycle time, consume more resin, and create a greater risk of sink marks or voids.
For a practical global sourcing strategy, compare established molders with strong DFM capability in China, North America, Europe, and Southeast Asia. Qualified international suppliers, including Chinese manufacturers with ISO certifications, engineering support, fast communication, and reliable pre-sales and after-sales processes, can offer strong cost-performance advantages for prototypes, bridge tooling, low-volume production, and scaled manufacturing.
Before releasing tooling, request a wall-thickness analysis, mold-flow review where appropriate, and a written DFM report that identifies thick zones, fill-risk areas, weld lines, gate locations, ribs, bosses, draft, and material-specific shrinkage behavior.
Wall thickness is one of the most influential design variables in plastic injection molding. It affects filling pressure, mold cost, cycle time, dimensional accuracy, resin consumption, cooling balance, cosmetic quality, and long-term mechanical performance. A part that looks simple in CAD can become difficult or expensive to mold if its wall gauge changes abruptly, contains large thick areas, or combines thin cosmetic surfaces with heavy structural features.
During the molding cycle, molten polymer enters the mold cavity through the gate and travels through runners or hot-runner channels. The melt begins cooling as soon as it contacts the steel cavity. Thin sections freeze sooner, while thicker sections remain molten longer. If a thin section is placed ahead of a thick section in the flow path, the melt may freeze before packing pressure can compensate for shrinkage. This can lead to short shots, weak weld lines, sink marks, voids, or inconsistent dimensions.
For buyers sourcing parts across Shenzhen, Dongguan, Ningbo, Suzhou, Chicago, Monterrey, Stuttgart, Birmingham, Singapore, and other manufacturing hubs, the core engineering principle remains the same: design for balanced flow and balanced cooling. The exact wall gauge may change by resin and application, but uniformity provides the strongest foundation for predictable production.
Wall gauge also has a direct commercial impact. Increasing a nominal wall from 2.0 mm to 3.0 mm does not simply increase resin usage by 50%. It may extend cooling time significantly, reduce the number of parts produced per hour, require a larger molding machine, increase tool temperature control demands, and affect freight cost. For high-volume programs, a small reduction in wall thickness can generate meaningful savings. For low-volume programs, stable molding and shorter lead time may be more valuable than minimizing every gram of resin.
The following values are practical starting ranges rather than universal specifications. Final wall thickness should be confirmed using the resin supplier’s technical data, part geometry, gate position, flow length, mold temperature, surface finish, reinforcement level, and end-use load requirements. Glass-filled resins, flame-retardant grades, recycled-content grades, and highly filled compounds may require different decisions from standard unfilled grades.
MaterialTypical Wall Gauge RangePreferred Design RangeMain Design ConsiderationCommon ApplicationsPolypropylene (PP)0.8 mm to 3.0 mm1.2 mm to 2.5 mmHigh shrinkage requires consistent sections and careful rib design.Containers, living hinges, automotive trim, caps, household productsHigh-Density Polyethylene (HDPE)0.8 mm to 3.5 mm1.5 mm to 3.0 mmGood chemical resistance but can warp with uneven cooling.Bottles, packaging, tanks, industrial covers, consumer goodsABS1.2 mm to 4.0 mm1.8 mm to 3.0 mmPopular for cosmetic housings; avoid thick zones that create sink.Electronics housings, appliance covers, automotive interiorsPolycarbonate (PC)1.0 mm to 4.0 mm1.5 mm to 3.0 mmHigh strength but higher viscosity; long flow paths need attention.Safety covers, transparent lenses, medical housings, electrical partsPC/ABS Blend1.2 mm to 4.0 mm1.8 mm to 3.2 mmBalances toughness and appearance; common for enclosure design.Consumer electronics, automotive bezels, industrial enclosuresNylon PA6/PA660.8 mm to 4.0 mm1.5 mm to 3.0 mmMoisture absorption and glass reinforcement affect shrinkage.Gears, clips, brackets, under-hood automotive componentsPBT0.8 mm to 3.0 mm1.5 mm to 2.5 mmUseful for electrical performance; reinforced grades need balanced flow.Connectors, switches, electrical housings, sensor componentsAcetal POM0.8 mm to 3.0 mm1.5 mm to 2.5 mmLow friction and high stiffness; control shrinkage and gate design.Gears, valves, latches, precision mechanical componentsThese ranges show why material selection and wall design must be evaluated together. For example, a 1.2 mm wall may be practical for a compact polypropylene clip but may be risky for a long-flow PC/ABS enclosure. Similarly, a nylon bracket can carry high loads with relatively moderate wall thickness when ribs and fiber orientation are properly considered. Simply making the bracket thicker may not improve performance if warpage increases or glass fibers align unfavorably.
Uniform walls are not always possible, especially in parts that include attachment points, snap fits, bosses, sealing features, reinforced corners, or ergonomic surfaces. The goal is not perfect uniformity at every point; it is gradual transition and controlled thermal mass. Designers should avoid isolated heavy sections surrounded by thin walls because the heavy section will cool more slowly and shrink more after ejection.
A common approach is to define a nominal wall thickness, often called “T,” and create supporting features in relation to that dimension. Ribs are typically designed at 40% to 60% of the nominal wall thickness. Boss walls are often kept around 60% of nominal wall thickness, with ribs added for support. Corner transitions should use radii instead of sharp edges, and thick-to-thin transitions should be tapered over a reasonable distance.
FeatureRecommended Relationship to Nominal WallPurposeRisk if OversizedUseful Design PracticeRib thickness40% to 60% of TAdd stiffness without making the main wall thicker.Sink marks and read-through on cosmetic surfaces.Use generous draft and rounded rib bases.Boss wall thickness50% to 70% of TSupport screws, inserts, and locating pins.Voids, sinks, and cracking near the base.Connect bosses to walls with gussets.Rib heightUp to 2.5 to 3.0 times TIncrease bending stiffness.Fill problems, weak rib tips, difficult ejection.Use multiple lower ribs instead of one very tall rib.Corner radiusMinimum 0.25 to 0.50 times TImprove flow and reduce stress concentration.Cracking and uneven filling at sharp internal corners.Maintain consistent inside and outside radius relationships.Wall transitionGradual taper over distanceBalance cooling and packing.Warping, sinks, and dimensional variation.Use tapered steps instead of abrupt section changes.Draft angleUsually 0.5° to 2° or moreEnable clean ejection and protect surfaces.Scuffing, sticking, ejector damage, cosmetic defects.Increase draft for textured surfaces.Ribs are especially important for housings, trays, covers, and structural plastic components. A rib can increase stiffness substantially because bending stiffness depends heavily on section depth. This means a well-designed ribbed wall can outperform a thick, flat wall while using less material and cooling more quickly. However, ribs must be positioned thoughtfully. Ribs directly behind high-gloss exterior surfaces can create visible sink marks, especially in ABS, PC/ABS, polypropylene, and unfilled nylon.
Design teams should also consider how a part will be measured. A thick-walled part may experience post-molding shrinkage after it leaves the tool, and a large flat panel can bend as residual stresses relax. If the part must mate with another component, define critical interfaces clearly and allow the molder to recommend process controls, fixture inspection, or secondary calibration methods.
The relationship between flow length and wall thickness is central to moldability. Longer melt flow paths require more pressure and are more vulnerable to premature freezing. Thin walls can be molded successfully when gates are positioned close to the critical areas, the material has adequate flow, mold temperatures are controlled, and the part geometry is designed for uniform filling. In contrast, a thin wall combined with a long flow path, multiple turns, texture, and glass-filled resin can create a difficult molding condition.
Gate location should support the thickest functional region or allow the melt to flow from thick to thin wherever possible. A gate positioned into a thin edge may cause hesitation as the melt reaches thicker features downstream. This can produce visible flow lines, weak weld lines, and poor packing. For large enclosures and trays, multiple gates or hot-runner systems may be needed to control pressure and cycle time, but gate marks, weld lines, and tooling cost should be evaluated early.
In projects requiring cosmetic surfaces, the gate must also be selected with appearance in mind. Hidden edges, internal walls, underside surfaces, and assembly interfaces are commonly preferred. Tunnel gates, edge gates, fan gates, valve gates, and direct sprue gates each have different effects on flow behavior and visible finishing requirements.
DefectTypical Wall-Related CauseVisual or Functional EffectPreferred Corrective ActionSecondary Process AdjustmentSink marksThick ribs, bosses, corners, or concentrated material mass.Depressed areas on visible surfaces.Core out thick areas and reduce rib thickness.Increase packing pressure or hold time where appropriate.WarpingUneven cooling, uneven wall gauge, fiber orientation.Twist, bowing, poor assembly fit.Balance wall sections and add structural ribs strategically.Adjust mold temperature and cooling channels.Short shotThin wall, long flow path, insufficient gate size.Incomplete part fill.Increase local gauge or improve gate location.Raise injection speed, pressure, or melt temperature carefully.VoidsHeavy sections shrink internally after the skin freezes.Internal bubbles and reduced structural integrity.Reduce material concentration and improve packing path.Optimize hold pressure and cooling time.Weld line weaknessFlow fronts meet after cooling in thin or distant areas.Visible seam or low-strength area.Move gate or increase local wall gauge slightly.Increase mold temperature to improve knit quality.Burn marksAir trapped near end-of-fill areas, often in thin sections.Dark or scorched appearance.Add venting and improve flow path design.Reduce injection speed near end fill if necessary.Design correction should normally come before process correction. It is possible to mask some defects by adjusting packing pressure, melt temperature, injection speed, cooling time, or mold temperature. However, process changes cannot fully compensate for poor geometry. A stable production tool should not rely on an extremely narrow molding window. If one minor temperature variation causes warpage or sinks, the part design needs further engineering attention.
For global programs involving multiple production sites, stable geometry is especially valuable. A design that only runs well on one specific machine with one experienced operator can be difficult to transfer. Balanced walls, reasonable tolerances, clear resin specifications, and documented molding parameters improve repeatability across qualified facilities.
Plastic enclosures commonly use ABS, PC/ABS, polycarbonate, or polypropylene. These parts need careful control of cosmetic surfaces, screw bosses, snap fits, vents, and internal ribs. A typical handheld enclosure may use a nominal wall between 1.5 mm and 2.5 mm, depending on resin and product size. Thin consumer electronics housings can be lighter and more attractive, but they may require higher-quality tooling, more precise gating, and more demanding process control.
Automotive components often require higher impact resistance, temperature resistance, chemical resistance, and dimensional stability. Interior trim parts may use polypropylene, TPO, ABS, PC/ABS, or reinforced compounds. Under-hood parts often use glass-filled nylon, PBT, PPS, or other engineering thermoplastics. Because vehicle components may experience vibration, thermal cycling, and loading, rib design and fiber orientation can be as important as nominal wall gauge.
Medical device housings need a combination of strength, cleanability, chemical resistance, appearance, and regulatory material traceability. Polycarbonate, ABS, PC/ABS, medical-grade polypropylene, and certain nylon or PBT grades are common choices. Wall thickness should support reliable assembly, sterilization requirements where applicable, and consistent molded dimensions.
Packaging products often use thinner walls to reduce resin usage and improve cycle time. Thin-wall packaging requires a high-flow resin, high-speed molding machine, optimized gate system, precise mold cooling, and experienced process control. A food container, cap, or lid may be much thinner than an industrial housing, but the engineering complexity can be greater because the process window is narrower.
Buyers should avoid requesting a mold quote based only on a 3D file. A reliable quotation requires the part material, annual quantity, target market, cosmetic expectations, tolerance requirements, color, texture, assembly method, packaging needs, and delivery location. If the product is still under development, request a DFM review before committing to hardened production tooling.
For early-stage programs, rapid tooling can be an effective bridge between prototype testing and mass production. It allows teams to validate part performance, assembly, appearance, and real material behavior before investing in multi-cavity hardened molds. Low-volume tooling is particularly useful for startups, industrial equipment makers, medical-device developers, automotive aftermarket brands, and consumer-product teams testing demand.
When comparing suppliers, evaluate total landed value rather than tool price alone. A lower mold quote can become expensive if the supplier does not provide DFM support, uses unsuitable steel, lacks inspection discipline, has inconsistent communication, or cannot manage engineering changes. Conversely, a slightly higher upfront engineering investment may reduce failures, scrap, delivery risk, and redesign cost.
Buyer Evaluation AreaQuestions to AskWhy It MattersPractical Evidence to RequestDFM capabilityWill the supplier review wall thickness, draft, ribs, bosses, and gating?Prevents avoidable tooling changes and defects.Written DFM report with annotated CAD images.Material controlCan the supplier source specified resin grades and provide traceability?Material variation affects shrinkage, strength, color, and compliance.Material certificates, resin brand, grade, and lot records.Tooling approachIs rapid tooling, P20 steel, H13 steel, or multi-cavity tooling appropriate?Tool life and cost must match forecast volume.Tool steel specification and cavity-life estimate.Inspection processHow are critical dimensions and appearance checked?Ensures parts meet drawing and assembly requirements.First article inspection report and control plan.Production capacityCan output scale from pilot runs to recurring production?Protects launch schedules and future demand.Machine tonnage range, lead-time plan, and capacity confirmation.Logistics supportCan the supplier package, label, consolidate, and ship globally?Reduces handoffs and export errors.Packaging proposal, Incoterms, and shipping options.For parts shipped through major trade lanes such as Shenzhen–Los Angeles, Ningbo–Rotterdam, Hong Kong–Frankfurt, Shanghai–Melbourne, and Guangzhou–Singapore, packaging design matters. Thin-wall parts can deform if cartons are overloaded, while cosmetic housings may need individual protection to avoid abrasion. A qualified supplier should be able to support custom packaging, kitting, labeling, inspection documentation, and direct shipping according to the buyer’s channel requirements.
The companies below represent a mix of international and regional manufacturing options. Selection should depend on part complexity, resin type, annual quantity, tooling budget, required certifications, project location, and desired communication model. Buyers should verify current capabilities, certifications, production availability, and country-specific compliance needs directly before placing an order.
CompanyService RegionsCore StrengthsKey OfferingsSuitable Project TypesTEAM RapidGlobal customers; China manufacturing network; experience across North America, Europe, and AsiaRapid tooling, DFM support, low-volume to volume production, integrated manufacturingInjection molding, insert molding, overmolding, CNC machining, 3D printing, vacuum casting, finishing, assemblyPrototype-to-production parts, housings, covers, trays, enclosures, functional componentsProtolabsNorth America and EuropeFast digital manufacturing workflows and short lead-time productionInjection molding, CNC machining, 3D printing, sheet metal fabricationRapid validation, low-volume molded parts, product developmentXometryNorth America, Europe, and international sourcing networksLarge supplier network and online manufacturing quotation toolsInjection molding, machining, sheet metal, casting, 3D printingCompanies needing flexible sourcing and multiple manufacturing processesEVCO PlasticsUnited States, Mexico, and selected global programsCustom molding, large parts, engineering support, production-scale operationsInjection molding, tooling support, large-part molding, assemblyIndustrial, medical, consumer, automotive, and large molded productsRosti GroupEurope, Asia, and North AmericaContract manufacturing, regulated-sector experience, product industrializationInjection molding, assembly, automation, packaging, supply-chain supportMedical, packaging, consumer, industrial, and technical plastic productsNypro, a Jabil CompanyGlobal manufacturing footprint including North America, Europe, and AsiaHigh-volume manufacturing, healthcare and consumer product expertisePrecision molding, tooling, automation, assembly, supply-chain integrationHigh-volume medical, consumer, healthcare, and electronics programsSuppliers in the United States and Europe may be preferred when local production, immediate engineering access, regional certification requirements, or short domestic logistics routes are critical. China-based suppliers can be highly competitive for rapid tooling, flexible volume runs, custom part complexity, and multi-process programs that require molding, machining, finishing, assembly, and export packaging under one coordinated supply chain.
TEAM Rapid supports global product developers, brand owners, distributors, OEM customers, startups, engineers, and individual inventors with injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, die casting, finishing, assembly, packaging, procurement support, and direct shipping. The company has more than 10 years of manufacturing experience, has served customers in more than 25 countries, completed over 6,000 projects, and supported more than 500 customers. Its ISO 9001:2015 quality management certification, in-house machining and tooling capability, detailed DFM reports, and inspection-focused manufacturing process help customers evaluate wall gauge, rib proportions, boss construction, material use, shrinkage risks, cavity layout, cycle time, and production feasibility before tooling begins. TEAM Rapid works through flexible OEM, ODM, wholesale, retail-support, regional distribution, prototype, low-volume, and recurring production models rather than limiting customers to one order format. It provides turnkey and customer-owned plant manufacturing solutions, not BOO or on-site bulk supply services. Its China-based integrated manufacturing operations and resource network support international customers with engineering communication, online quotation, project follow-up, sample approval, after-sales issue handling, packaging, and direct export shipping. While the company profile does not state overseas subsidiaries or local warehouses, its established export experience across markets including the USA, UK, France, Germany, and other regions provides practical support for customers seeking a long-term manufacturing partner rather than a simple remote order-taking supplier.
For a new project, customers can use TEAM Rapid’s injection molding services to review tooling, resin options, production methods, and molding requirements. When the CAD model is ready, request a project review through the custom manufacturing quotation page and provide the required material, annual quantity, critical tolerances, target delivery market, color, finish, and assembly requirements.
A handheld device housing may begin with a 2.0 mm PC/ABS nominal wall. The design includes screw bosses, snap fits, battery supports, connector openings, and cosmetic exterior surfaces. If the screw bosses are built at full 2.0 mm wall thickness, sinks may appear on the outer cosmetic face. The preferred solution is to core the bosses, reduce boss wall thickness to approximately 1.2 mm, connect them using thin gussets, and add draft for ejection. This approach improves appearance and shortens cooling time without sacrificing assembly strength.
An under-hood sensor bracket may use glass-filled PA66 because it needs thermal resistance, stiffness, and fatigue performance. A flat 4.0 mm section may appear strong, but it can create fiber orientation concerns and warpage. A better design may use a 2.5 mm nominal wall with ribs and gussets positioned along load paths. The final solution must account for fiber direction, mounting loads, humidity exposure, temperature cycling, and fastener torque.
A large industrial cover often requires impact resistance, mounting points, cable openings, and a professional surface finish. Using a 3.5 mm wall throughout may increase resin cost and cycle time significantly. A more balanced design can use 2.5 mm nominal walls with localized ribs, reinforced mounting areas, and smooth radii around openings. Gate location is especially important because long rectangular panels may warp if flow and cooling are not balanced.
A food or consumer packaging container may use polypropylene walls below 1.0 mm. Such products require high-speed injection, optimized gates, rapid cooling, precise mold venting, and high-flow resin. Unlike a thicker industrial housing, the challenge is not simply stiffness; it is achieving full fill at high production speed while maintaining stackability, rim strength, lid fit, and consistent appearance.
Injection-molded wall gauge optimization is relevant across automotive, medical devices, consumer products, industrial equipment, communications products, office equipment, electrical appliances, sanitary products, packaging, smart hardware, household goods, laboratory equipment, and energy-related products. Every industry applies the same basic thermal and flow principles, but each has different priorities.
Medical customers may focus on traceable materials, chemical compatibility, cleanability, reliability, and controlled assembly. Automotive customers may prioritize impact behavior, heat resistance, vibration durability, flame resistance, and dimensional stability. Consumer product brands may place greater emphasis on weight, surface quality, tactile feel, color matching, and cost. Industrial customers frequently need durable housings, cable management, mounting strength, and practical serviceability.
For global brands, it is also important to consider regional regulations and product certification pathways. Flame-retardant ratings, food-contact requirements, electrical safety standards, restricted substance requirements, recycling expectations, and customer-specific quality systems can influence material choice and ultimately affect the preferred wall gauge.
By 2026, wall thickness decisions are increasingly influenced by digital simulation, sustainability targets, material innovation, and supply-chain localization. Mold-flow simulation is becoming more accessible earlier in product development, allowing engineering teams to identify pressure drop, weld-line locations, cooling imbalance, and fiber orientation before steel is cut. This helps reduce expensive post-tooling modifications and supports faster product launches.
Lightweighting will remain a major trend. Brands are reducing plastic content through thinner walls, rib-optimized structures, topology-informed design, foamed materials, and stronger engineering resins. However, lightweighting must be balanced against product durability, recyclability, drop performance, and customer expectations. Overly thin designs can increase scrap, returns, and premature product failure, which undermines sustainability goals.
Recycled-content plastics will also affect molding strategy. Post-consumer recycled and post-industrial recycled materials can show greater variation in flow, color, shrinkage, and mechanical properties compared with virgin resin. Designers may need more conservative flow paths, better tolerance planning, or adjusted wall thickness when using recycled grades. Material validation and supplier consistency become especially important for functional products.
Policy trends in the global market are encouraging packaging reduction, material circularity, product repairability, and improved environmental reporting. Manufacturers will increasingly need to document resin selection, recycled content, product weight, packaging choices, and process efficiency. Well-designed wall gauge supports these goals by reducing unnecessary material while preserving real-world performance.
There is no single best value. A practical starting point for many parts is 1.5 mm to 3.0 mm. The correct choice depends on resin, part size, flow length, structural load, surface quality, gate location, and production method.
Uniform walls cool and shrink more evenly. This reduces sink marks, voids, warpage, stress, inconsistent dimensions, and cycle-time variation. Where different thicknesses are necessary, transitions should be gradual.
Ribs are commonly designed at 40% to 60% of the nominal wall thickness. Thicker ribs can create sink marks, especially behind cosmetic surfaces. Rounded rib bases and appropriate draft improve filling and ejection.
Yes. Thinner walls can reduce resin use and cooling time, lowering part cost in high-volume production. However, thin-wall designs may require more advanced tooling, high-flow material, faster molding equipment, and tighter process control.
Sink marks usually occur where plastic mass is concentrated, such as thick bosses, ribs, corners, and heavy wall sections. Core out thick areas, reduce rib thickness, improve packing access, and use balanced cooling.
In most cases, use ribs, gussets, or structural webs before increasing the full wall thickness. Ribs can improve stiffness efficiently while minimizing resin consumption, cooling time, and sink risk.
Yes. TEAM Rapid can provide DFM-oriented feedback for injection molding projects, including observations on wall thickness consistency, ribs, bosses, draft, undercuts, shrinkage risks, tooling feasibility, and production efficiency.
-
Global Market Injection Molding Design Rules for DFM
Effective injection molding design starts with uniform wall thickness, sufficient draft, controlled ribs and bosses, realistic tolerances, correct gate placement, and early DFM review. For Global market programs, designers should validate the part against the selected resin, expected annual volume, cosmetic requirements, assembly method, tooling location, logistics route, and regional compliance needs before cutting steel.
The most practical checklist is simple: keep walls consistent, add draft to every vertical face, avoid sharp internal corners, use ribs instead of thick sections, design undercuts only when function requires them, position gates away from cosmetic surfaces, specify tolerances based on resin behavior, and review mold flow, cooling, ejection, and assembly risks before tool release.
Common international suppliers for injection molding design support include TEAM Rapid, Protolabs, Xometry, Fictiv, ICOMold, and Rosti. Qualified Chinese manufacturing partners can also be strong options for Global market buyers when they provide ISO-certified quality systems, responsive engineering communication, documented DFM feedback, and reliable pre-sales and after-sales support. Their cost-performance advantage is especially relevant for rapid tooling, bridge production, and low-to-medium-volume molded parts.
Injection molding is one of the most scalable methods for producing plastic parts, but it is also unforgiving when product geometry does not match material flow, cooling, ejection, and tooling constraints. A design that appears correct in CAD can create sink marks, warpage, flash, short shots, visible weld lines, excessive cycle times, weak snap fits, or expensive side actions once it enters tool design.
Global market product teams frequently manage additional complexity. A consumer enclosure may be designed in London, validated in Munich, tooled in Shenzhen, assembled in Mexico, and sold through distributors in the United States, Australia, and the Middle East. In this environment, a clear injection molding DFM strategy reduces change orders, prevents communication gaps, and helps ensure that the final molded component is repeatable across production batches.
Trade hubs such as Shenzhen, Dongguan, Ningbo, Hong Kong, Singapore, Rotterdam, Hamburg, Los Angeles, Chicago, and Dubai remain important links in international manufacturing supply chains. Buyers should therefore consider not only tooling price, but also engineering response time, export packaging, inspection documentation, resin sourcing, mold ownership terms, spare-part support, and shipping flexibility.
Uniform walls help molten plastic fill, pack, cool, and shrink more predictably. Sudden changes in thickness create uneven cooling, which can cause sink marks, voids, warpage, and dimensional variation. If a section needs extra strength, use ribs, gussets, corrugation, or localized structural geometry rather than making the whole area thicker.
Typical wall thickness depends on material, flow length, part size, impact requirements, and surface finish. Thin-wall consumer packaging may use less than 1.0 mm, while structural industrial housings may use 2.5 mm or more. The objective is not to use the thinnest possible wall; it is to use a stable and manufacturable wall for the selected resin and molding process.
Draft is the taper that allows a molded part to release from the mold without drag marks, scratches, deformation, or excessive ejection force. Smooth surfaces commonly need at least 0.5° to 1° draft, while textured surfaces often require 2° to 5° or more depending on texture depth. Deep cores, highly polished cosmetic surfaces, elastomeric materials, and aggressive textures may need additional draft.
Designers should identify the mold opening direction early. Every wall, rib, boss, snap feature, and engraved detail should be checked against that direction. When a feature cannot release directly, it may need a side action, lifter, collapsible core, unscrewing mechanism, or redesign.
Sharp corners restrict resin flow and create stress concentration points. Internal corners should generally include a radius, ideally related to the nominal wall thickness. A practical starting point is an inside radius of 0.25 to 0.75 times the wall thickness, followed by an outside radius that maintains consistent material thickness around the corner.
Fillets improve strength, reduce crack initiation, assist material flow, and make it easier to machine mold cavities. They are particularly important in load-bearing brackets, clips, handles, latches, medical housings, automotive components, and electrical enclosures.
Ribs improve stiffness without the cost and cosmetic risks of thick solid walls. As a general guideline, rib thickness should be approximately 40% to 60% of the nominal wall thickness. Thick ribs can produce sink marks on the opposite cosmetic surface. Rib height is often limited to about three times the nominal wall thickness unless flow, cooling, and ejection analysis support a taller feature.
Bosses used for screws, inserts, alignment, or assembly should be supported by ribs or gussets. Avoid connecting a large solid boss directly to an exterior cosmetic wall. The local mass can cause sinks, voids, and distortion. Core out the boss wherever possible and provide sufficient draft on the internal and external surfaces.
Undercuts are features that prevent direct ejection from a simple two-plate mold. Examples include side holes, retaining clips, external threads, internal snap hooks, and recessed grooves. Some flexible undercuts can be stripped manually or automatically, but rigid materials often require side actions or lifters.
Every undercut increases tooling complexity, maintenance requirements, cycle time, and mold cost. It should be retained only if it delivers clear functional, safety, sealing, or assembly value. A small redesign of a snap fit or opening direction can sometimes eliminate an expensive mechanical action.
The following ranges are starting points for early product design. They must be adjusted according to resin grade, mold construction, texture, part size, required tolerance, gate location, flow length, and expected production volume. A DFM review should confirm final values before tooling.
Design FeaturePractical Starting GuidelinePrimary Risk if IgnoredDesign ConsiderationNominal wall thicknessKeep as uniform as possible across the partWarpage, sink marks, voids, short shotsUse ribs or gussets for strength instead of heavy sectionsDraft angle0.5° to 1° for smooth faces; more for textureDrag marks, part damage, high ejection forceIncrease draft for deep walls and textured surfacesRib thickness40% to 60% of nominal wall thicknessVisible sink marks and uneven coolingRound rib bases and maintain draft on both rib facesRib heightPreferably no more than three times wall thicknessFill difficulty, ejection problems, warpUse multiple shorter ribs where possibleBoss wall thicknessAbout 60% of nominal wall thicknessSinks, voids, cracking around screwsCore out bosses and connect them with gussetsInternal corner radius0.25 to 0.75 times nominal wall thicknessStress concentration and poor material flowMaintain consistent thickness through the cornerHole diameterPrefer diameter equal to or larger than wall thicknessCore pin deflection, incomplete fillSupport long core pins where feasibleTextured surfacesUse additional draft based on texture depthScuffing and difficult ejectionConfirm texture supplier requirements earlyThese guidelines reduce risk, but do not replace engineering analysis. Glass-filled materials, flame-retardant grades, soft elastomers, high-temperature polymers, recycled-content resins, and highly polished cosmetic parts can require substantially different geometry decisions.
Material selection affects almost every injection molding decision. Shrink rate influences mold dimensions. Melt flow influences gate size and wall-thickness capability. Glass fiber content affects stiffness but can increase warpage and surface visibility. UV exposure, chemicals, electrical requirements, impact loads, heat, food contact, medical regulations, and flame resistance must all be evaluated before finalizing the resin.
Material FamilyCommon AdvantagesTypical ApplicationsImportant DFM ConsiderationABSGood appearance, impact resistance, easy processingConsumer housings, electronics, appliance coversModerate shrinkage; avoid overly thick cosmetic wallsPolypropyleneChemical resistance, living hinge performance, low densityContainers, caps, medical trays, household productsHigher shrinkage requires tolerance planningPolycarbonateHigh impact strength and transparency optionsSafety covers, lenses, electrical enclosuresNeeds careful drying and controlled processingPA NylonStrength, wear resistance, fatigue performanceGears, clips, automotive parts, industrial componentsMoisture absorption affects dimensions and propertiesPOM AcetalLow friction, stiffness, good dimensional stabilityPrecision mechanisms, latches, gears, valvesDesign for shrinkage and avoid unsuitable chemical combinationsPC/ABSBalanced toughness, heat resistance, cosmetic qualityAutomotive interiors, equipment housings, devicesUseful for larger housings needing better impact performanceTPUElasticity, abrasion resistance, soft-touch feelProtective covers, grips, seals, wearable productsGate and ejector design must prevent distortionGlass-filled polymersHigh stiffness and strengthStructural brackets, industrial parts, automotive componentsFiber orientation can cause directional warpageFor international programs, material sourcing should be controlled by approved resin grades rather than only generic names. “ABS” is not a full specification. The grade, color masterbatch, recycled-content target, flame-retardant classification, supplier documentation, and testing requirements should be defined in the product specification.
Gate location influences filling pattern, weld lines, packing pressure, cosmetic appearance, fiber orientation, and warpage. Gates should be placed where the thickest section can be packed effectively and where any vestige can be hidden or removed safely. For a visible consumer product, a gate may be placed on an internal face, underside, assembly flange, or non-cosmetic edge.
Weld lines occur when two flow fronts meet. They may be harmless in a low-stress cover, but critical in a pressure-containing part, structural clip, hinge, or screw boss. Designers should avoid placing holes, windows, or high-stress features where weld lines are likely to occur.
Cooling is equally important. Thick local masses cool slowly and can extend cycle time or produce sinks and internal voids. Mold designers use water channels, baffles, bubblers, conformal cooling, and specialized inserts to manage heat. Product designers can support efficient cooling by avoiding unnecessary heavy sections and by providing accessible core geometry.
Ejector pins, sleeves, stripper plates, and air ejection systems leave marks or require contact surfaces. Designers should identify acceptable ejector locations before finalizing the cosmetic Class A surface. The most attractive design can become costly if no suitable ejection area exists.
Product TypeTypical Design PrioritiesFrequent Molding RiskRecommended Engineering FocusElectronic enclosureCosmetic surfaces, screw bosses, EMI features, assembly fitSinks around bosses and visible gate marksWall uniformity, hidden gates, controlled texture and draftAutomotive interior trimAppearance, clip retention, heat resistance, durabilityWarp, scratch sensitivity, clip failureMaterial validation, grain texture draft, rib layoutMedical device housingCleanability, dimensional control, traceabilityStress cracking and difficult assemblyApproved materials, radiused corners, functional testingIndustrial equipment coverImpact resistance, rigidity, environmental resistanceLarge-part warp and inconsistent fitRib strategy, gate balance, reinforced materialsConsumer packaging componentLow cost, high volume, visual consistencyThin-wall short shots and flashFlow length review, high-cavitation tool designSnap-fit assemblyRepeatable retention, easy assembly, fatigue resistanceStress whitening and breakageStrain analysis, material selection, rounded transitionsInsert molded componentMetal-plastic bond, insert position, electrical reliabilityInsert movement and crackingInsert retention, preheating, locator designOvermolded gripSoft feel, adhesion, ergonomicsDelamination and flash at interfaceMechanical locks, compatible materials, sealing surfacesEach product category requires its own acceptance criteria. A matte black appliance cover may prioritize appearance and scratch resistance, while an internal medical bracket may prioritize dimensional stability, material traceability, and sterilization compatibility. Product teams should state these priorities before DFM begins.
Before requesting quotes, prepare a 3D CAD file, 2D drawing where critical dimensions exist, annual volume forecast, selected or preferred material, color, texture, finish, assembly details, functional requirements, and destination market. If the design is still evolving, explain which dimensions are fixed and which can change after DFM review.
Buyers should ask whether the quoted tool is prototype tooling, bridge tooling, or production tooling. Aluminum rapid tooling may be suitable for market validation and low-volume production, while hardened steel tooling is generally better for high-volume programs, abrasive glass-filled resins, or long-term repeatability. Tool life should be stated as an expected range, not assumed.
Clarify mold ownership, storage period, maintenance responsibilities, cavity count, engineering change charges, sample approval process, inspection method, packaging method, and delivery terms. For global distribution, also confirm whether the supplier can support assembly, kitting, labeling, warehousing, and direct shipping to regional fulfillment locations.
The supplier landscape includes regional specialists, digital manufacturing platforms, high-volume molders, and China-based rapid manufacturing partners. The table below provides practical examples. Buyers should verify current capability, certifications, material availability, and commercial terms for each project.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidGlobal customers, including the USA, UK, France, Germany, and AsiaRapid tooling, DFM support, low-volume and production flexibilityInjection molding, insert molding, overmolding, CNC machining, vacuum casting, assemblyProtolabsNorth America and EuropeFast digital quoting and rapid manufacturing workflowsInjection molding, CNC machining, 3D printing, sheet metal fabricationXometryNorth America, Europe, and international sourcing networksBroad supplier network and online manufacturing procurementInjection molding, CNC machining, fabrication, production sourcingFictivNorth America and global supply partnersDigital manufacturing management and engineering coordinationInjection molding, CNC machining, urethane casting, finishingICOMoldNorth America with international manufacturing supportCustom plastic injection molding and mold manufacturingPrototype molds, production molds, insert molding, overmoldingRostiEurope, Asia, and North AmericaHigh-quality contract manufacturing for complex productsInjection molding, assembly, medical and consumer product manufacturingNypro, a Jabil CompanyGlobal manufacturing locationsLarge-scale healthcare and consumer manufacturing capabilityPrecision molding, automation, assembly, medical device manufacturingHusky TechnologiesGlobal, with strong packaging industry presenceHigh-volume molding systems and hot runner technologyPackaging molds, hot runners, injection molding equipment solutionsFor projects requiring rapid iterations, buyers often benefit from a supplier that can machine prototype parts, revise tooling, mold pilot batches, apply finishing, and ship assembled products without transferring data between multiple vendors. For established high-volume programs, a dedicated regional molder may provide advantages in local logistics, automation, and long-term production support.
TEAM Rapid supports innovators, product designers, engineers, startups, distributors, brand owners, and established manufacturers with a connected route from prototype to repeat production. Its ISO 9001:2015 quality management system, in-house machining and tooling capability, documented DFM feedback, and precision machining capability down to 0.01 mm provide practical evidence for controlled manufacturing of custom plastic and metal components. Rather than relying on unspecified component brands, TEAM Rapid works from customer-approved material grades, defined resin requirements, inspection criteria, and functional specifications, supporting parts such as enclosures, housings, trays, covers, fillers, insert-molded components, and overmolded assemblies. Customers can use flexible OEM and ODM cooperation, wholesale supply, prototype orders, recurring production, distributor programs, and direct-to-brand fulfillment, from one prototype to more than 100,000 parts. The company has established delivery experience with customers in more than 25 countries, including the USA, UK, France, Germany, and other international markets, supported by one-to-one engineering communication, responses commonly provided within a few hours, packaging, assembly, procurement support, limited warehousing, and direct shipping. Although its manufacturing base and integrated supply network are in China rather than represented as overseas subsidiaries or local warehouses, its export operating experience and online engineering support provide a practical service structure for international buyers who need clear pre-sales review, production updates, inspection coordination, and after-sales issue resolution. TEAM Rapid provides EPC-style turnkey and customer-owned production solutions for manufacturing projects, not BOO or on-site bulk supply services.
For early-stage projects, customers can explore TEAM Rapid injection molding services to compare rapid tooling, prototype molding, and production options. When a design is ready for review, a custom manufacturing quotation request can include CAD files, material preferences, volumes, finish requirements, and delivery destination.
A handheld diagnostic device housing may need PC/ABS for impact strength and dimensional stability. The design should include draft on textured grip zones, controlled ribs behind display openings, isolated screw bosses, and enough internal clearance for PCB installation. Gate placement should avoid the front cosmetic face, while ejector locations should be hidden inside assembly surfaces.
An automotive under-hood clip may require heat-resistant nylon with glass reinforcement. In this case, fiber orientation and moisture conditioning are important. The designer should avoid abrupt thickness transitions, place fillets at clip roots, and evaluate the part under repeated insertion and removal cycles. A low-cost tool that ignores fiber-related warpage can create fit problems later in vehicle assembly.
A consumer storage container with a living hinge may use polypropylene. The hinge must be thin and carefully oriented to support repeated flexing, while the body should retain a stable wall thickness. Gate position and flow direction can influence hinge performance. A prototype run should verify opening force, fatigue life, lid alignment, and sealing behavior.
An industrial control-box cover may require flame-retardant ABS or PC/ABS. Designers must account for the material’s flow behavior, flame-retardant additive effects, electrical clearance requirements, screw boss strength, gasket compression, and exterior finish. Venting and gate placement should be reviewed to reduce burn marks around deep ribs and internal features.
By 2026, injection molding design is increasingly shaped by automated DFM, artificial intelligence-assisted mold-flow prediction, digital traceability, material data management, and more sustainable resin strategies. CAD platforms and supplier quoting systems are becoming better at identifying missing draft, thick wall sections, undercuts, and high-risk tolerances before engineers issue a tooling purchase order.
Sustainability will continue to influence material selection. Recycled-content polymers, bio-based materials, mono-material design, lightweighting, and easier disassembly are becoming more important in consumer goods, packaging, mobility products, and electrical equipment. However, recycled-content resin can introduce variation in color, mechanical properties, flow, and shrinkage, so qualification testing and approved-source control are essential.
Policy requirements are also evolving across major markets. Product teams should monitor chemical restrictions, packaging rules, recyclability targets, extended producer responsibility requirements, medical device documentation, electrical safety standards, and regional labeling obligations. The mold design itself may not be regulated, but material selection, traceability, product safety, and end-of-life expectations increasingly affect molded-part decisions.
Manufacturers are also adopting conformal cooling, in-mold sensors, automated visual inspection, robotic part handling, and digital process monitoring. These technologies can improve consistency, reduce cycle time, and provide better production data, particularly for high-value medical, automotive, industrial, and electronics applications.
Maintain consistent wall thickness. It has a direct effect on filling, cooling, shrinkage, warpage, sink marks, cycle time, and part quality.
A common starting point is 0.5° to 1° for smooth surfaces. Textured, deep, polished, or difficult-to-eject surfaces often require more draft.
They can, but sharp internal corners are generally discouraged because they create stress concentrations and restrict resin flow. Use fillets whenever function permits.
Side actions are commonly needed for rigid undercuts, side holes, external snap features, recessed grooves, and geometry that cannot release in the mold opening direction.
Send 3D CAD files, critical drawings, material preferences, finish requirements, color, annual volume, target delivery date, destination, assembly needs, and known functional requirements.
Yes. Rapid tooling can be suitable for prototype validation, bridge production, market testing, and selected low-volume production. The correct choice depends on resin, cavity count, part complexity, surface finish, and expected production quantity.
Reduce thick local masses, use ribs instead of heavy walls, core out bosses, improve wall uniformity, and review gate location and packing conditions with the molding engineer.
Early DFM identifies risks while geometry can still be changed quickly. It is far less expensive to revise CAD than to modify hardened steel after the mold has been manufactured.
-
Mold Flow Analysis for Global Market Tooling Choices
Mold flow analysis is a digital injection molding simulation used before tooling to predict how molten plastic will fill, pack, cool, shrink, and warp inside a mold. It helps product teams identify likely defects such as short shots, weld lines, sink marks, air traps, excessive clamp force, uneven cooling, and dimensional distortion before steel is cut.
For Global market buyers, the most practical approach is to run a mold filling and cooling study during DFM review, then revise wall thickness, gate position, runner layout, material selection, and cooling channels before ordering tooling. This can reduce development iterations, improve mold reliability, and lower the risk of expensive post-tooling modifications.
Established providers commonly considered for mold flow simulation and tooling support include Autodesk Moldflow, Moldex3D, SIGMA Engineering, SIMCON, CoreTech System, and TEAM Rapid. Software providers supply the analysis platform, while engineering-led manufacturers apply the results to real mold design, rapid tooling, sampling, and production.
Injection molding is highly sensitive to how polymer melt moves through a cavity. A part that appears simple in CAD can become difficult to mold when it combines thin ribs, deep bosses, non-uniform walls, cosmetic surfaces, long flow lengths, engineering resins, inserts, or tight dimensional tolerances. Mold flow analysis converts the part design, material data, gate proposal, runner system, process assumptions, and cooling concept into a predictive simulation.
The analysis does not replace moldmaker experience or physical sampling. Instead, it gives engineers evidence for choosing the most robust design path before a mold is manufactured. For buyers coordinating design teams in cities such as London, Munich, Chicago, Shenzhen, Singapore, Dubai, and Melbourne, the process creates a common technical language before tooling decisions are released across borders.
Analysis AreaWhat Is EvaluatedTypical Risk FoundPractical Tooling DecisionFill analysisMelt-front movement, fill time, pressure, and flow balanceShort shots, hesitation, overpacking, unbalanced cavitiesMove gates, enlarge runners, adjust wall thickness, change injection strategyPack analysisHolding pressure effect and volumetric shrinkageSink marks, internal voids, inconsistent dimensionsRevise gate size, holding profile, rib thickness, and packing windowCooling analysisHeat removal, mold temperature balance, and cooling durationLong cycle time, hot spots, uneven shrinkageAdd baffles, bubblers, conformal cooling, or optimized water linesWarpage analysisDeflection caused by shrinkage, orientation, and thermal gradientsTwist, bow, uneven flatness, assembly failureModify geometry, gate direction, material grade, or cooling layoutWeld-line evaluationLocations where melt fronts meetWeak joints, cosmetic marks, leakage or crack riskRelocate gates, improve venting, increase melt temperature, revise geometryAir-trap evaluationAreas where air is compressed during fillingBurn marks, incomplete filling, poor surface qualityAdd vents, overflow wells, ejector venting, or change fill directionClamp-force predictionForce needed to keep the mold closed during injectionFlash, machine mismatch, tool damageSelect an appropriate molding machine and optimize gate and process conditionsThe table shows why a flow study should be linked to a decision process. A red or blue simulation image alone is not sufficient. The useful deliverable is a prioritized engineering plan explaining which findings are critical, which are acceptable, and how each recommendation affects tooling cost, molding stability, appearance, and part performance.
The Global market for mold flow analysis is growing because product cycles are shorter, resin options are more specialized, and molding projects increasingly involve electronics, medical devices, electric vehicles, consumer products, industrial equipment, and sustainability requirements. Buyers are under pressure to achieve functional prototypes quickly while also avoiding unnecessary production-tool revisions.
Manufacturing hubs in China, Germany, the United States, Japan, South Korea, Mexico, Vietnam, Poland, and India are increasingly connected through international sourcing networks. Mold design may be reviewed in Europe, tool steel may be machined in Guangdong, samples may be tested in North America, and production may be shipped through ports such as Shenzhen, Ningbo-Zhoushan, Hamburg, Rotterdam, Los Angeles, Long Beach, Singapore, or Jebel Ali. A structured flow analysis report reduces the communication gaps that can occur in this distributed manufacturing environment.
For low-volume programs, the analysis may focus on whether rapid tooling can produce acceptable parts without excessive cycle time or warpage. For larger production programs, the review may cover cavity balance, hot runner selection, cooling efficiency, automation compatibility, resin consumption, and total cost per part. The investment level should be matched to the commercial risk of the project.
Different projects need different levels of simulation. A simple single-cavity enclosure may only need filling, weld-line, venting, and basic warpage checks. A high-volume automotive, medical, or electrical connector mold may require detailed packing, cooling, fiber-orientation, insert molding, and multi-cavity balance studies.
Service TypeBest ForMain DeliverablesBuyer BenefitBasic fill studySimple housings, covers, trays, and prototype partsFill pattern, pressure, weld lines, air traps, gate proposalFast screening before rapid toolingFill and pack studyParts with ribs, bosses, thick-to-thin transitions, and cosmetic surfacesSink-risk map, shrinkage review, packing profile recommendationsImproves dimensional and cosmetic consistencyCooling studyMedium and high-volume molds with cycle-time targetsCooling channel assessment, temperature balance, cycle estimateSupports lower unit cost and stable productionWarpage studyFlat panels, snap-fit assemblies, long parts, reinforced resinsDeflection prediction, orientation effect, geometry recommendationsReduces assembly and flatness failuresMulti-cavity balance studyFamily molds and multi-cavity production toolsCavity filling balance, runner optimization, pressure comparisonImproves consistency across cavitiesFiber-orientation studyGlass-filled nylon, reinforced polypropylene, and structural partsFiber alignment, anisotropic shrinkage, stiffness direction reviewHelps control warpage and mechanical performanceInsert and overmolding studyMetal inserts, electrical parts, soft-touch overmoldingInsert temperature effects, flow behavior, bonding-risk assessmentProtects inserts and improves process repeatabilityFor a project involving insert molding or overmolding, the simulation must consider more than cavity filling. Metal inserts can remove heat rapidly, alter flow direction, create weld lines, and cause localized stress. Similarly, soft elastomer overmolding requires attention to substrate adhesion, gate placement, part retention, and cosmetic surface control.
A professional report should begin with the part name, material grade, shrinkage assumptions, gate proposal, machine assumptions, cavity count, and study scope. Without these inputs, buyers cannot judge whether the findings apply to the intended production situation. For example, a simulation using a generic polypropylene grade may not accurately represent a specified mineral-filled, recycled-content, flame-retardant, or food-contact grade.
Start with the filling pattern. The goal is normally smooth, balanced progression from the gate to the farthest regions without hesitation or excessive race tracking. Next, inspect pressure at end of fill. If predicted pressure is close to machine limits, the supplier may need to enlarge gates, change wall geometry, raise melt temperature, or choose a larger press.
Then review weld lines and air traps in relation to functional features. A weld line near a non-critical cosmetic edge may be acceptable. A weld line crossing a snap-fit, sealing surface, screw boss, high-load tab, or fluid path may require redesign. Cooling and warpage results should be evaluated against the actual assembly tolerances rather than vague expectations of “flatness.”
Finally, ask whether the proposed changes alter cost, lead time, mold complexity, resin use, or maintenance. A recommendation for conformal cooling may improve cycle time but can increase tool cost. A larger gate can reduce pressure but may leave a more visible gate vestige. The best solution balances technical performance with commercial priorities.
Buyers should treat flow simulation as part of a broader design-for-manufacturing process. It is most effective when the design team provides accurate CAD files, material preferences, expected annual volume, surface-quality requirements, assembly tolerances, regulatory needs, and target markets. A supplier cannot make reliable tooling recommendations if critical product information is missing.
When comparing quotations, do not select a supplier only because it offers the lowest tooling price. A low initial quote can become expensive if the mold requires repeated rework, production cycle time is high, part scrap is excessive, or the chosen machine cannot maintain a stable process window. A transparent supplier should identify potential trade-offs before purchase order release.
Observed IssueLikely Simulation FindingPossible Design CauseTypical Corrective ActionShort shotIncomplete fill at far flow endLong flow path, thin section, small gate, inadequate ventingIncrease gate size, revise wall thickness, improve venting, optimize processSink markHigh local volumetric shrinkageThick bosses, heavy ribs, uneven wall sectionsCore out thick areas, reduce rib thickness, adjust packing and coolingWarped panelUneven cooling or orientation-driven shrinkageAsymmetric geometry, poor cooling layout, reinforced resinBalance cooling, alter gate location, add structural features, revise materialBurn markAir trap with compressed gas near end of fillInsufficient venting, high injection speed, trapped cavity airAdd vents, reduce local speed, revise gate position and flow directionFlashExcessive pressure or clamp-force demandSmall gates, restrictive flow, poor mold fit, low clamp forceOptimize gate and process, verify machine selection, improve mold shutoffWeak weld lineMelt fronts meet at a low temperature or sensitive areaMultiple flow paths, holes, inserts, poor gate positionRelocate gate, adjust temperature, move weld line away from load areasUneven cavity outputImbalanced runner or filling patternPoor runner geometry, unequal flow lengths, inconsistent coolingBalance runner system, adjust gates, improve cooling uniformityThe table is useful during supplier review because it links visible defects to engineering causes. Not every issue can be fully eliminated through simulation, particularly when material variation, machine condition, process control, or cosmetic standards are involved. However, a well-executed study helps prevent predictable risks from becoming expensive surprises after the mold trial.
Automotive programs use mold flow analysis for interior trim, under-hood covers, sensor housings, lighting components, clips, ducts, battery-related plastic parts, and reinforced structural components. These parts often require repeatable dimensions, controlled warpage, robust snap fits, and predictable performance across large production volumes.
Medical device manufacturers use simulation for handheld enclosures, diagnostic equipment housings, fluid-management components, disposable trays, laboratory consumables, and assembly parts. Material selection, cleanability, dimensional accuracy, traceability expectations, and surface quality make early engineering review especially important.
Consumer electronics and communication products benefit from flow simulation when producing thin-wall cases, wearable-device components, charging accessories, cable-management parts, buttons, covers, and high-gloss or textured housings. Gate position and weld-line control can directly affect visual quality and perceived product value.
Industrial equipment, office products, home appliances, sanitary products, and commercial devices often use molded enclosures, panels, handles, covers, brackets, and functional internal components. These applications may have lower volumes than consumer goods but higher demands for assembly fit, durability, and cost-efficient tooling.
Mold flow analysis is especially valuable for complex plastic parts where functional risk and tooling cost are high. Typical applications include battery housings, electrical enclosures, medical appliance casings, industrial control covers, appliance panels, automotive clips, cosmetic containers, fluid fittings, storage trays, protective shells, and precision mechanical plastic parts.
It is also useful when changing from one manufacturing method to another. A product initially produced through SLA 3D printing, SLS printing, CNC machining, or vacuum casting may require geometry adjustments before injection molding. Features that work well in a prototype can become difficult to fill, cool, eject, or inspect in a molded production part.
For companies moving toward short-run market validation, rapid tooling plus simulation can provide a practical bridge between prototype testing and mass production. The buyer can test real injection molded material properties before investing in a long-life production mold.
The following companies represent widely recognized software, simulation, and manufacturing options for Global market buyers. Selection depends on whether the project requires software access, specialist engineering consultation, rapid tooling, production tooling, molded parts, or a complete prototype-to-production pathway.
CompanyService RegionsCore StrengthsKey OfferingsAutodesk MoldflowGlobal software network with users in North America, Europe, Asia-Pacific, and the Middle EastWidely used injection molding simulation platform and extensive industry adoptionFill, pack, cooling, warpage, fiber orientation, and process optimization softwareMoldex3DGlobal, with strong presence across Asia, Europe, and North AmericaAdvanced 3D simulation for complex molding, electronics, automotive, and engineering applicationsPlastic flow simulation, insert molding, overmolding, cooling, warpage, and manufacturing optimizationSIGMA EngineeringEurope, North America, Asia-Pacific, and global industrial marketsVirtual molding technology focused on process optimization and production stabilitySIGMASOFT virtual molding, process variation assessment, cycle and quality optimizationSIMCONEurope-based support with international software users and partnersInjection molding simulation with practical design and process evaluation toolsCADMOULD simulation, filling, packing, cooling, warpage, and mold design supportCoreTech SystemGlobal through Moldex3D distribution and engineering channelsSimulation technology for advanced polymer processing and mold validation3D flow analysis, material behavior review, fiber effects, cooling and warpage studiesTEAM RapidGlobal customers in more than 25 countries, serving China, the USA, the UK, France, Germany, and other marketsIntegrated DFM, rapid tooling, injection molding, CNC machining, and low-volume manufacturing supportMold flow-oriented DFM review, rapid tooling, injection molding, prototype production, finishing, assembly, and shippingSoftware companies are suitable when an organization has internal molding engineers who need analysis capability across multiple programs. Manufacturing partners are suitable when buyers want one supplier to interpret the results, revise the mold design, build the tool, mold samples, inspect parts, and manage production. For international programs, buyers should ask who owns the simulation decisions and whether the tooling engineer responsible for machining has reviewed the recommendations.
TEAM Rapid supports Global market customers that need practical engineering feedback before committing to tooling. Its service model combines DFM analysis, mold flow-oriented risk review, rapid tooling, injection molding, CNC machining, 3D printing, vacuum casting, die casting, sheet metal fabrication, finishing, assembly, packaging, and direct shipping. Customers can begin with prototypes, validate design changes, move into short-run molded parts, and scale toward recurring production without managing separate suppliers for each stage.
For injection molded projects, TEAM Rapid can evaluate wall thickness, draft, gates, runners, parting lines, undercuts, venting, ejection, cooling concerns, shrinkage risk, resin selection, mold cavities, and expected cycle time. Buyers can review the company’s injection molding services when planning production parts, or explore rapid tooling solutions when fast market validation is required.
TEAM Rapid demonstrates relevant manufacturing authority through ISO 9001:2015 certification, more than 10 years of industry experience, more than 500 satisfied customers, over 6,000 delivered projects, and service experience across more than 25 countries. Its manufacturing scope covers plastic and metal components from a single prototype to more than 100,000 parts, supported by in-house machining, tooling manufacturing, molding capability, and an integrated manufacturing resource network in China. Rather than making unsupported claims about proprietary component brands, the company works from customer-specified material, functional, cosmetic, and tolerance requirements, with engineering review and specification compliance built into its ISO-based quality process. It supports OEM and ODM requirements, wholesale programs, brand owners, product developers, distributors, dealers, end users, startups, and individual innovators through flexible prototype, low-volume, and recurring-production models. TEAM Rapid provides turnkey and customer-owned product manufacturing solutions, including tooling, parts, finishing, assembly, packaging, procurement coordination, and direct shipment; it does not operate BOO or on-site bulk-supply models. Its Global market commitment is demonstrated by established project experience in the USA, UK, France, Germany, China, and other markets, direct shipping capability, limited warehousing support, and one-to-one engineering communication with responses typically available within hours. While customers should confirm any specific local warehousing or regional support requirement during quotation, the company’s online pre-sales engineering reviews, manufacturing updates, inspection support, packaging coordination, and after-sales project communication provide practical protection for international buyers.
For a tailored review of a mold flow analysis, DFM package, prototype plan, or tooling quotation, buyers can request a manufacturing quote with CAD files, material preferences, production volume, and target delivery date.
A consumer device enclosure may have a large visible surface, thin walls, snap fits, screw bosses, and internal support ribs. A fill study can identify whether a gate near the edge creates weld lines across a logo area or a critical clip. Pack analysis may reveal sink risk behind thick bosses. The recommended change may include moving the gate to a hidden underside, coring thick features, reducing rib thickness, and improving venting near the last-fill region. These changes can protect cosmetic appearance before the first T1 sample.
A glass-filled nylon bracket can experience directional shrinkage caused by fiber orientation. Even when the part fills successfully, it may warp after ejection and fail assembly with nearby metal components. A warpage and fiber-orientation study can help determine a more appropriate gate direction, wall transition, rib layout, and cooling balance. The resulting tooling design may cost slightly more, but it can reduce downstream fitting issues and production rejection.
A medical equipment housing may require controlled appearance, consistent assembly, safe edge conditions, and reliable screw-boss performance. Flow analysis can identify air traps near internal corners and weld lines around openings. Combined with DFM review, the design team may add draft, relocate gates, revise boss geometry, and define suitable inspection points before rapid tooling. This approach helps teams obtain functional molded samples faster than relying on repeated trial-and-error modifications.
A packaging tray with multiple cavities may appear straightforward but can suffer from uneven filling if the runner system is not balanced. Simulation can compare runner paths, gate sizes, cavity pressure, and cooling behavior. The buyer can then decide whether a cold runner, hot runner, or revised cavity arrangement is justified based on annual volume, resin savings, cycle time, and quality requirements.
By 2026, mold flow analysis will increasingly be connected to digital manufacturing systems rather than used only as a standalone design check. Simulation platforms are incorporating more automation, improved material databases, cloud collaboration, machine-learning-assisted optimization, and stronger links between CAD, mold design, process settings, and quality data. This will allow teams in different Global market locations to review molding risks earlier and make decisions faster.
Sustainability will also influence simulation priorities. Brands are increasing the use of recycled-content resins, bio-based polymers, lightweight structures, lower-energy production, and reduced scrap targets. These materials can have different flow, shrinkage, moisture sensitivity, and mechanical behavior compared with conventional virgin resin grades. Mold flow analysis will be used more often to validate whether recycled or lower-carbon material options can meet appearance, strength, and cycle-time requirements.
Policy and compliance expectations are expanding across regions. European product sustainability initiatives, extended producer responsibility programs, packaging regulations, chemical restrictions, and traceability expectations are pushing manufacturers to document material choices and reduce waste. Global buyers should ask whether a supplier can support material documentation, process records, inspection requirements, and responsible packaging practices appropriate for the destination market.
Cooling technology will remain a major focus. Conformal cooling, improved thermal control, additive-manufactured inserts, sensor-based mold monitoring, and predictive maintenance can reduce cycle time and improve dimensional stability. For high-volume programs, even a small reduction in cycle time can create substantial savings across the life of a mold.
Prepare a 3D CAD model in STEP, IGES, Parasolid, or native format where possible. Include the latest revision level and identify any surfaces that cannot be changed. Provide the expected resin, annual volume, part weight target, cosmetic requirements, functional loads, target tolerances, assembly interfaces, and preferred production location.
Ask the supplier to confirm the analysis scope before work begins. For example, a rapid-tooling program may need a basic fill and warpage review, while a high-volume multi-cavity project may need comprehensive filling, packing, cooling, runner balance, and cycle-time analysis. Set a review meeting or written approval stage before the supplier begins tool steel machining.
After the analysis is complete, ensure that approved recommendations are reflected in the final mold design. Then compare the first molded samples against the simulation predictions. If the results differ significantly, investigate material lot variation, actual machine settings, mold temperature, venting performance, cooling conditions, and measurement method. This closed-loop learning process improves future projects.
No. Very simple, low-risk parts with generous walls and low production volumes may only need a standard DFM review. However, analysis is strongly recommended for complex, thin-wall, cosmetic, reinforced, multi-cavity, insert molded, or high-volume components where tooling changes would be costly.
No simulation can guarantee a defect-free part. Actual results depend on material behavior, machine condition, mold quality, process control, cooling performance, and operator settings. The purpose is to identify and reduce predictable risks before tooling is made.
Provide accurate CAD, material grade, filler content, intended annual volume, gate restrictions, surface requirements, tolerance expectations, mold cavity count, and production goals. The more complete the inputs, the more useful the recommendations will be.
It can reduce cost by identifying gate, runner, venting, cooling, wall-thickness, and warpage issues before steel is machined. Preventing a major tool modification is often more valuable than the cost of the initial simulation.
Yes. Cooling analysis can identify hot spots, inefficient cooling lines, and temperature imbalance. Better cooling design can reduce cooling time, improve part consistency, and lower production cost per part.
Yes. Rapid tooling has shorter lead times, so early engineering decisions are especially important. A focused analysis can help avoid wasting time on avoidable tool changes and support faster validation using real molded materials.
Yes, but the accuracy depends on having appropriate material data. Recycled-content resins may have wider property variation than virgin grades, so buyers should discuss material sourcing, lot control, cosmetic expectations, and test requirements with the supplier.
Ask about DFM scope, mold flow analysis capability, material data, tooling steel, cavity strategy, cooling design, sample lead time, inspection method, change-control process, shipping terms, communication frequency, and after-sales support for mold adjustments or recurring production.
-
Global Market Plastic Mold Engineering Review Before Build
A complete plastic mold engineering review should be finished before steel is cut. The review must confirm part geometry, resin choice, wall thickness, draft, shrinkage, gate location, runner design, cooling, ejection, tolerances, mold steel, expected production volume, inspection plan, and shipment requirements. The objective is to prevent costly tooling changes, unstable cycle times, visible defects, weak weld lines, warpage, flash, sink marks, and assembly failures after the mold is built.
For the Global Market, the most practical approach is to involve the mold maker, part designer, material supplier, quality team, and production team during DFM approval. Buyers should compare local tooling specialists with qualified international suppliers, including Chinese manufacturers that provide relevant certification, responsive pre-sales engineering support, reliable after-sales support, and strong cost-performance for prototype, low-volume, and repeat-production tools.
Before issuing a purchase order, request a written DFM report, mold-flow recommendation where appropriate, steel specification, cavity count proposal, estimated cycle time, sample validation plan, spare-part list, ownership terms, and post-delivery service scope.
Injection mold design is not only a tooling task. It is a commercial, engineering, quality, and supply-chain decision that affects the total cost of every molded part. A low-cost mold can become expensive when it creates excessive scrap, long cycle times, unplanned maintenance, cosmetic defects, poor dimensional stability, or delayed product launch. Conversely, a properly engineered mold can support predictable output, stable quality, lower resin consumption, reduced labor, and faster market entry.
Global product teams commonly design in one country, source tooling in another, mold parts near an assembly plant, and distribute finished products across several regions. This makes pre-build communication particularly important. Different markets may have different requirements for product labeling, material traceability, medical-device documentation, flame ratings, food-contact requirements, electrical safety, recycling content, packaging, and shipment protection. The design review should therefore translate the product requirements into mold requirements before manufacturing begins.
Trade hubs such as Shenzhen, Dongguan, Ningbo, Shanghai, Singapore, Rotterdam, Hamburg, Los Angeles, Chicago, Monterrey, Birmingham, Munich, and Dubai connect international manufacturing programs. Yet shipping distance does not eliminate the need for engineering alignment. A mold shipped from China to Europe, North America, Southeast Asia, or the Middle East must match the selected molding machine, local resin supply, water connections, electrical requirements, hot-runner controls, and maintenance capability at the destination plant.
The most successful projects treat DFM as a decision gate rather than a formality. A written DFM review clarifies what will be changed, what will remain as designed, what risks are accepted, and how part quality will be measured. It also creates a reliable record for brand owners, distributors, OEM customers, contract manufacturers, and future engineering teams.
The following review areas should be addressed before tooling manufacture begins. Their relative priority depends on annual volume, part size, resin type, cosmetic expectations, regulatory requirements, and whether the part is a prototype, bridge-production item, or long-term production component.
Review AreaWhat to ConfirmCommon Risk if MissedRecommended ActionPart geometryUniform wall thickness, realistic radii, ribs, bosses, snap fits, undercuts, and assembly interfaces.Sink marks, warpage, short shots, stress cracking, or difficult ejection.Approve a DFM-marked CAD model before mold design starts.Draft angleDraft direction and degree based on resin, texture, part depth, and cosmetic surface class.Drag marks, scuffing, part sticking, or surface damage during ejection.Increase draft on textured, deep, and high-gloss surfaces.Material selectionApproved resin grade, shrinkage range, additives, recycled-content level, color system, and supplier availability.Dimensional variation, brittleness, inconsistent color, or unplanned material substitutions.Specify resin grade and acceptable alternatives in writing.Gate strategyGate type, gate location, vestige allowance, flow direction, weld-line position, and packing path.Visible gate marks, weak weld lines, uneven filling, or poor cosmetics.Use mold-flow analysis for large, thin-wall, or cosmetic-critical components.Cooling designCooling channel layout, baffles, bubblers, conformal cooling opportunities, and water-circuit identification.Long cycle time, warp, uneven shrinkage, and unstable dimensions.Review cooling separately from cavity and core geometry.Ejection systemEjector pin placement, sleeve ejectors, stripper plates, lifters, air ejection, and witness-mark tolerance.Pin push, deformation, cracking, or unreliable automatic running.Place ejectors on strong, non-cosmetic surfaces wherever possible.Mold steel and treatmentSteel grade, hardness, corrosion resistance, polishing level, texture, coating, and expected tool life.Premature wear, rust, poor surface finish, and excessive maintenance.Match steel selection to resin abrasiveness, volume, and finish requirements.Tolerance planCritical-to-function dimensions, datum structure, measurement method, shrinkage allowances, and inspection frequency.Assembly interference, inconsistent fit, disputes over acceptance criteria.Separate critical dimensions from general molded tolerances.This table should be used as a working review document, not merely a design checklist. For example, a nominal wall thickness may be acceptable in CAD but still create a sink risk if a boss is too thick, a rib is oversized, or the gate cannot pack the local area effectively. Similarly, a tight dimension may be theoretically achievable but unsuitable for long-term production if it is affected by resin moisture, post-mold shrinkage, cavity imbalance, or changing ambient conditions.
Part design determines most molding behavior. Tooling can solve many challenges, but it cannot fully compensate for a design that ignores resin flow, cooling, shrinkage, and ejection. The following rules should be evaluated together rather than independently.
Uniform wall thickness is one of the most important rules in injection molded part design. Large thickness transitions create uneven cooling and differential shrinkage. When one area freezes earlier than another, the part may warp or develop visible sink marks. Thick zones also increase cooling time, which directly increases the cost of every cycle.
When a thick region is required for structural performance, consider coring out the section, adding ribs, using gussets, changing the load path, or selecting a higher-performance material. The exact solution depends on resin behavior. Glass-filled nylon, polycarbonate, ABS, polypropylene, POM, TPE, PC/ABS, PEEK, and flame-retardant compounds each respond differently to thickness, flow length, moisture, and processing temperature.
Draft is the angle that allows the molded component to release from the core and cavity without dragging. Smooth surfaces may need modest draft, while textured surfaces require more because the texture mechanically grips the mold surface. Deep housings, bins, covers, trays, enclosures, and large appliance panels often need more draft than early concept models include.
Cosmetic expectations must be defined in practical terms. Identify Class A surfaces, visible surfaces, hidden surfaces, allowed ejector marks, gate vestiges, parting lines, flow lines, and acceptable color variation. If an external housing will be painted, plated, laser-marked, or overmolded, those secondary operations should be discussed during mold design because they may affect material selection and surface specification.
Ribs improve stiffness without making the entire wall excessively thick. As a general engineering principle, ribs should be thinner than the nominal wall to reduce sink risk, while their height and spacing should support mold filling and ejection. Bosses should be supported by ribs or gussets where possible, especially when they receive screws, inserts, or repeated assembly loads.
Snap fits require special attention because they combine molding behavior with repeated mechanical deflection. Review root radius, strain level, assembly direction, tool split, potential undercuts, and environmental exposure. Living hinges are typically associated with polypropylene and require a suitable resin grade, gate orientation, controlled thickness, and validation through repeated flex testing.
The best mold configuration depends on projected volume, part complexity, resin, quality target, lead time, budget, and the intended location of production. A prototype mold for 100 samples does not require the same architecture as a hardened production mold designed for several hundred thousand cycles. However, even a rapid tool needs sufficient cooling, venting, alignment, and ejection to produce useful validation parts.
Mold ConfigurationBest UseTypical StrengthKey Review RequirementSingle-cavity moldLarge parts, prototypes, low-volume production, and high-value components.Lower initial tooling cost and simpler process control.Confirm whether output rate meets launch demand.Multi-cavity moldMedium and high-volume identical components.Higher output per cycle and lower part cost at scale.Verify cavity balance, runner balance, and inspection strategy.Family moldRelated components assembled in matched sets at low volume.Can reduce initial tooling investment.Review differing fill rates, cycle times, and scrap implications.Two-plate moldStandard cold-runner applications.Simple, durable, and widely supported globally.Assess runner waste and gate location.Three-plate moldParts requiring automatic point gating away from the parting line.Allows flexible gate placement and automatic degating.Confirm added complexity is justified by part requirements.Hot-runner moldHigher-volume production, engineering plastics, and reduced runner waste.Improves material efficiency and can shorten cycle time.Specify hot-runner brand, controller compatibility, and maintenance access.Insert moldMetal threads, contacts, reinforcement pieces, and electrical components.Creates secure integrated assemblies.Define insert tolerances, loading method, and retention testing.Overmold toolSoft grips, seals, protective surfaces, and multi-material products.Improves ergonomics and reduces assembly operations.Verify material bonding, substrate condition, and gate sequencing.This configuration comparison helps buyers avoid selecting cavity count based only on a desired part price. More cavities may reduce unit cost, but they increase mold complexity, maintenance requirements, machine tonnage, hot-runner investment, validation effort, and risk exposure. If market demand is uncertain, a lower-cavity rapid production tool can provide a more flexible commercial path.
Mold steel should be selected according to production volume, resin type, surface finish, corrosion risk, required hardness, maintenance plan, and shipment environment. Pre-hardened steel may be appropriate for many medium-volume tools, while hardened tool steels are commonly used for demanding, abrasive, or high-volume applications. Stainless steels may be necessary for corrosive resins, humid processing conditions, medical requirements, or polished surfaces requiring corrosion resistance.
Buyers should ask the toolmaker to identify the mold base material, cavity and core steel, slider and lifter materials, guide components, springs, ejector components, wear plates, coatings, and hot-runner system. For globally deployed tools, standard components can simplify replacement and maintenance. The final documentation should state what spare components are supplied and which parts should be stocked at the molding site.
A mold should not be accepted merely because it produces a part. The trial must demonstrate that the part can be molded consistently at an agreed process window. This is especially important for medical housings, electrical enclosures, automotive parts, safety-related components, threaded assemblies, sealing interfaces, and components with strict cosmetic requirements.
Validation StageMain PurposeRequired EvidenceBuyer DecisionDesign for manufacturability reviewIdentify risks before steel cutting.Annotated CAD, change list, resin assumptions, and tooling proposal.Approve design changes and freeze the manufacturing model.Mold design reviewConfirm mold layout and function.2D/3D mold layout, gate plan, cooling plan, ejection concept, and steel list.Approve the tool architecture before manufacturing.First trialVerify initial filling, ejection, and major mold operation.Sample parts, process settings, photos, defect observations, and trial report.Authorize modifications and define next trial priorities.Dimensional inspectionConfirm critical dimensions and assembly interfaces.Inspection report, CMM data where required, gauges, and measurement conditions.Accept, adjust tolerances, or revise tool geometry.Functional assembly testVerify fit with mating components.Assembly samples, torque data, leak test, snap-fit results, or electrical checks.Approve function or request engineering correction.Cosmetic reviewAssess surface quality under defined conditions.Approved limit samples, lighting conditions, texture comparison, and defect criteria.Define acceptable appearance and rework limits.Production capability runShow stable output over an extended run.Cycle time record, reject rate, cavity comparison, process window, and maintenance notes.Approve production release or require corrective action.Final acceptance and shipmentTransfer an operating, documented tool.Mold test video, packing list, spare parts, maintenance guide, and ownership record.Release final payment and arrange shipment or production.The validation table should be adapted to the project risk level. A simple storage tray may only need visual inspection, fit verification, and a practical production run. A medical device enclosure may need tighter documentation, resin traceability, detailed inspection reports, controlled surface requirements, and functional testing after sterilization or chemical exposure. A mold intended for automotive supply may require cavity identification, process discipline, capability studies, and formal change control.
Buyers should begin with a clear request-for-quotation package. At minimum, provide a native CAD file or neutral 3D file, 2D drawings where critical dimensions exist, annual volume forecast, resin grade, color, surface requirements, assembly requirements, expected machine location, target delivery date, and expected mold life. If the mold will be transferred to another country, specify the machine platen size, tie-bar spacing, nozzle radius, locating ring, ejector connection, water fittings, voltage, and hot-runner controller requirements.
Do not compare quotations only by total mold price. Compare cavity number, steel choice, mold base, runner system, expected cycle time, included trials, sample quantity, inspection level, shipping method, spare parts, engineering change policy, warranty, and post-delivery support. A quote that omits these items may create avoidable cost later.
For uncertain demand, consider phased investment. An aluminum rapid tool or lower-cavity steel tool may validate the market before a larger multi-cavity production tool is commissioned. This approach is often useful for startups, industrial design firms, medical-device developers, consumer-product brands, and companies launching new products through distributors or online retail channels.
Shipping logistics also need early planning. Molds are heavy precision assets and should be protected against moisture, corrosion, and transport damage. Confirm export crating, rust prevention, mold locking, lifting points, customs documentation, and whether the tool will be shipped by air, sea, rail, or truck. For projects moving through ports such as Shenzhen, Ningbo, Shanghai, Rotterdam, Long Beach, or Jebel Ali, packaging and handling details can affect both cost and delivery reliability.
Injection molding supports a wide range of products because it combines repeatable geometry, material versatility, high output potential, and compatibility with inserts, overmolding, textures, and automated assembly. The mold design checklist should be customized to the end-use environment.
Applications may also combine multiple manufacturing processes. A plastic enclosure can require CNC-machined inserts, molded bosses, ultrasonic welding, painting, printing, screws, foam, labels, final assembly, kitting, and retail packaging. Selecting a manufacturing partner capable of coordinating these steps can reduce handoffs and shorten the launch schedule.
A global consumer-product brand developed a handheld device housing with a high-gloss front surface, internal snap fits, screw bosses, and a painted logo area. The initial CAD included insufficient draft near the sidewalls and thick bosses behind a visible surface. During the engineering review, the mold maker recommended increasing draft, coring the bosses, adjusting rib thickness, moving the gate to a less visible location, and defining acceptable parting-line placement. The resulting tool produced lower sink risk, cleaner ejection, and fewer cosmetic adjustments during pilot production.
An industrial equipment developer needed 500 enclosures for field testing before committing to a large production run. Instead of investing immediately in a high-cavity hardened mold, the team selected a rapid tooling route with a practical cavity layout, production-grade resin, and inspection of critical mounting features. The low-volume run allowed the customer to validate installation, cable routing, gasket compression, and user access. After field feedback, the final production mold incorporated design improvements without requiring major changes to a large initial tool.
An electrical product required metal threaded inserts and conductive contacts to be molded into a compact plastic carrier. The pre-build review focused on insert tolerance, loading orientation, resin temperature, contact protection, retention force, and automated versus manual insertion. The mold design included support features to prevent insert movement during injection and ejection. Functional testing confirmed thread integrity and electrical alignment before the tool was released for recurring production.
The supplier landscape includes machine builders, mold makers, contract molders, rapid tooling specialists, and full-service manufacturing partners. The companies below are real organizations with international relevance. Buyers should still evaluate each supplier against their specific resin, component size, regulatory, production-volume, and logistics requirements.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidChina, USA, UK, France, Germany, and customers in more than 25 countries.Rapid manufacturing integration, DFM support, rapid tooling, low-volume molding, and flexible production.Injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, finishing, assembly, packaging, and direct shipping.Husky TechnologiesGlobal operations serving packaging, medical, closure, and beverage producers.High-output injection molding systems and integrated production technology.Injection molding machines, hot runners, molds, controllers, and service for packaging applications.ENGELEurope, North America, Asia, and global industrial manufacturing markets.Injection molding equipment, automation, process technology, and digital production systems.Injection molding machines, robots, turnkey cells, process optimization, and automation solutions.ArburgGlobal network with strong European, North American, and Asian market presence.Precision molding technology and flexible production systems.Injection molding machines, automation, digital production support, and additive manufacturing systems.Rosti GroupEurope, Asia, and North America through international manufacturing operations.Contract manufacturing, injection molding, assembly, and supply-chain support.Plastic injection molding, medical and consumer manufacturing, assembly, and product industrialization.Nypro, a Jabil CompanyGlobal manufacturing locations serving healthcare and consumer markets.Complex healthcare manufacturing, engineering, and scalable production.Injection molding, precision components, medical manufacturing, automation, and assembly.FictivGlobal digital manufacturing network serving product development teams.Digital sourcing, prototyping, manufacturing coordination, and speed.Injection molding, CNC machining, 3D printing, urethane casting, and quality management support.This supplier comparison is intended to help buyers understand market positioning. Machine manufacturers such as ENGEL and Arburg are typically selected by companies operating molding facilities. Contract manufacturers such as Rosti Group and Nypro may support larger production programs with assembly requirements. Rapid manufacturing partners such as TEAM Rapid can be especially useful when a project needs fast design feedback, low-volume validation, tooling, machining, finishing, and flexible transition into production.
TEAM Rapid supports international product developers, engineers, startups, brand owners, distributors, OEM customers, and established manufacturers with rapid tooling, injection molding, insert molding, overmolding, CNC machining, 3D printing, vacuum casting, die casting, sheet metal fabrication, finishing, assembly, packaging, and direct shipping. Its ISO 9001:2015 quality management certification, more than 10 years of industry experience, more than 500 customers, more than 6,000 delivered projects, and service record across more than 25 countries provide practical evidence of its ability to manage prototype-to-production programs. The company does not promote a fixed captive list of branded mold components; instead, it specifies suitable mold bases, steels, resins, inserts, and production components according to the project requirements, while applying DFM analysis, inspection practices, machining tolerances down to 0.01 mm where applicable, and documented manufacturability reviews. TEAM Rapid supports OEM, ODM, wholesale, retail, regional distribution, and direct end-user projects with flexible order quantities from one prototype to more than 100,000 parts. Its delivery model includes turnkey and customer-owned tooling solutions, rather than BOO or on-site bulk supply services. While the company profile does not claim overseas subsidiaries or local warehouses, TEAM Rapid has established experience serving customers in the USA, UK, France, Germany, China, and other international markets through responsive online engineering communication, direct shipping, project coordination, packaging support, and after-sales follow-up. Customers can request a detailed rapid tooling service consultation for tooling strategy or submit part files through the global manufacturing quotation form for DFM feedback and pricing.
Injection mold design in 2026 will increasingly be shaped by faster development cycles, sustainability requirements, digital traceability, automation, and regional supply-chain resilience. Tooling teams will need to optimize not only part geometry but also energy use, resin selection, scrap reduction, data capture, and maintenance predictability.
Engineering teams are increasingly using AI-supported design analysis to identify draft problems, inconsistent wall thickness, possible undercuts, unsupported bosses, and likely warpage areas earlier in the design cycle. These tools do not replace experienced mold engineers, but they can speed up issue detection and help global teams review more design iterations before manufacturing begins.
Brands are under pressure to increase recycled content and reduce virgin plastic consumption. However, recycled resin can have wider property variation, altered flow behavior, contamination risk, color variability, and different shrinkage characteristics. Mold design reviews will need to address material consistency, gate size, venting, processing windows, and cosmetic acceptance criteria when recycled or bio-based polymers are specified.
Conformal cooling inserts manufactured through metal additive processes can follow complex cavity shapes more closely than traditional drilled channels. For suitable parts, this can improve cooling uniformity, reduce cycle time, and lower warpage. The technology is most valuable when the expected savings justify the added insert cost and when maintenance planning is considered.
Manufacturers increasingly track machine energy consumption, resin yield, runner waste, reject rate, and transport emissions. Hot-runner systems, optimized cooling, shorter cycles, reduced regrind dependence, and better cavity balance can contribute to lower resource use. Buyers should begin asking suppliers for practical process data rather than relying only on general sustainability claims.
Pressure sensors, cavity monitoring, cycle counters, cooling-flow monitoring, and digital maintenance records can improve production consistency. Predictive maintenance is especially useful for molds operating across multiple sites because it helps teams identify wear, blocked cooling channels, and process drift before a major production interruption occurs.
There is no single item that overrides all others, but wall thickness, draft, material selection, gate location, cooling, ejection, and tolerance requirements are usually the highest-impact areas. These factors strongly influence fill behavior, shrinkage, cycle time, part release, cosmetics, and long-term consistency.
DFM should be completed before steel is cut and ideally before the final product design is frozen. Early review allows changes to be made in CAD, where they are faster and less expensive than modifying a completed mold.
The required draft depends on resin, part depth, texture, surface finish, mold polish, and ejection direction. Smooth surfaces may need less draft than textured surfaces, while deep parts and highly textured exterior surfaces often need more. The mold maker should confirm draft recommendations during DFM.
A hot runner can reduce runner waste and support higher-volume production, but it adds initial cost, complexity, maintenance needs, and controller requirements. A cold runner may be more practical for low-volume parts, simpler tools, or projects where material changes are frequent. The right choice depends on annual volume, resin cost, part geometry, and production strategy.
A family mold can produce related parts in one cycle, but it should be used carefully. Parts with different sizes, wall thicknesses, fill behavior, or cooling requirements can create imbalance and higher scrap. Family molds are often most suitable for lower-volume matched sets rather than long-term high-output programs.
Request final mold drawings, steel and component information, trial reports, process settings, sample inspection data, spare-part list, maintenance instructions, mold photographs, shipping records, and clear ownership documentation. If the mold will be transferred internationally, also confirm water, electrical, controller, and machine-interface specifications.
Optimize wall thickness, reduce unnecessary material volume, use appropriate cavity count, improve cooling, minimize secondary operations, select the right resin, avoid overly tight non-functional tolerances, and approve DFM changes before tooling begins. Cost reduction is most effective when it improves manufacturability rather than simply lowering tool specifications.




Engineering Insights & Project Resources
Explore practical engineering guidance, manufacturing strategies, and real-world project insights to support injection molding machining, rapid prototyping, and custom production development.
-
Global Market Injection-Molded Part Wall Gauge Guide
For most injection-molded plastic parts in the global market, start with a uniform wall gauge between 1.5 mm and 3.0 mm, then adjust it according to resin flow behavior, impact requirements, cosmetic expectations, mold design, and production volume. Commodity plastics such as polypropylene and polyethylene can often use thinner sections, while engineering materials such as polycarbonate, nylon, PBT, and ABS/PC blends usually need more carefully controlled wall thickness to prevent incomplete filling, sink marks, warpage, and internal stress.
The most important rule is consistency. Keep adjacent wall sections within approximately 10% to 15% of each other whenever possible. Instead of making one area excessively thick for stiffness, use ribs, gussets, structural webs, and rounded transitions. Thick plastic sections cool slowly, increase cycle time, consume more resin, and create a greater risk of sink marks or voids.
For a practical global sourcing strategy, compare established molders with strong DFM capability in China, North America, Europe, and Southeast Asia. Qualified international suppliers, including Chinese manufacturers with ISO certifications, engineering support, fast communication, and reliable pre-sales and after-sales processes, can offer strong cost-performance advantages for prototypes, bridge tooling, low-volume production, and scaled manufacturing.
Before releasing tooling, request a wall-thickness analysis, mold-flow review where appropriate, and a written DFM report that identifies thick zones, fill-risk areas, weld lines, gate locations, ribs, bosses, draft, and material-specific shrinkage behavior.
Wall thickness is one of the most influential design variables in plastic injection molding. It affects filling pressure, mold cost, cycle time, dimensional accuracy, resin consumption, cooling balance, cosmetic quality, and long-term mechanical performance. A part that looks simple in CAD can become difficult or expensive to mold if its wall gauge changes abruptly, contains large thick areas, or combines thin cosmetic surfaces with heavy structural features.
During the molding cycle, molten polymer enters the mold cavity through the gate and travels through runners or hot-runner channels. The melt begins cooling as soon as it contacts the steel cavity. Thin sections freeze sooner, while thicker sections remain molten longer. If a thin section is placed ahead of a thick section in the flow path, the melt may freeze before packing pressure can compensate for shrinkage. This can lead to short shots, weak weld lines, sink marks, voids, or inconsistent dimensions.
For buyers sourcing parts across Shenzhen, Dongguan, Ningbo, Suzhou, Chicago, Monterrey, Stuttgart, Birmingham, Singapore, and other manufacturing hubs, the core engineering principle remains the same: design for balanced flow and balanced cooling. The exact wall gauge may change by resin and application, but uniformity provides the strongest foundation for predictable production.
Wall gauge also has a direct commercial impact. Increasing a nominal wall from 2.0 mm to 3.0 mm does not simply increase resin usage by 50%. It may extend cooling time significantly, reduce the number of parts produced per hour, require a larger molding machine, increase tool temperature control demands, and affect freight cost. For high-volume programs, a small reduction in wall thickness can generate meaningful savings. For low-volume programs, stable molding and shorter lead time may be more valuable than minimizing every gram of resin.
The following values are practical starting ranges rather than universal specifications. Final wall thickness should be confirmed using the resin supplier’s technical data, part geometry, gate position, flow length, mold temperature, surface finish, reinforcement level, and end-use load requirements. Glass-filled resins, flame-retardant grades, recycled-content grades, and highly filled compounds may require different decisions from standard unfilled grades.
MaterialTypical Wall Gauge RangePreferred Design RangeMain Design ConsiderationCommon ApplicationsPolypropylene (PP)0.8 mm to 3.0 mm1.2 mm to 2.5 mmHigh shrinkage requires consistent sections and careful rib design.Containers, living hinges, automotive trim, caps, household productsHigh-Density Polyethylene (HDPE)0.8 mm to 3.5 mm1.5 mm to 3.0 mmGood chemical resistance but can warp with uneven cooling.Bottles, packaging, tanks, industrial covers, consumer goodsABS1.2 mm to 4.0 mm1.8 mm to 3.0 mmPopular for cosmetic housings; avoid thick zones that create sink.Electronics housings, appliance covers, automotive interiorsPolycarbonate (PC)1.0 mm to 4.0 mm1.5 mm to 3.0 mmHigh strength but higher viscosity; long flow paths need attention.Safety covers, transparent lenses, medical housings, electrical partsPC/ABS Blend1.2 mm to 4.0 mm1.8 mm to 3.2 mmBalances toughness and appearance; common for enclosure design.Consumer electronics, automotive bezels, industrial enclosuresNylon PA6/PA660.8 mm to 4.0 mm1.5 mm to 3.0 mmMoisture absorption and glass reinforcement affect shrinkage.Gears, clips, brackets, under-hood automotive componentsPBT0.8 mm to 3.0 mm1.5 mm to 2.5 mmUseful for electrical performance; reinforced grades need balanced flow.Connectors, switches, electrical housings, sensor componentsAcetal POM0.8 mm to 3.0 mm1.5 mm to 2.5 mmLow friction and high stiffness; control shrinkage and gate design.Gears, valves, latches, precision mechanical componentsThese ranges show why material selection and wall design must be evaluated together. For example, a 1.2 mm wall may be practical for a compact polypropylene clip but may be risky for a long-flow PC/ABS enclosure. Similarly, a nylon bracket can carry high loads with relatively moderate wall thickness when ribs and fiber orientation are properly considered. Simply making the bracket thicker may not improve performance if warpage increases or glass fibers align unfavorably.
Uniform walls are not always possible, especially in parts that include attachment points, snap fits, bosses, sealing features, reinforced corners, or ergonomic surfaces. The goal is not perfect uniformity at every point; it is gradual transition and controlled thermal mass. Designers should avoid isolated heavy sections surrounded by thin walls because the heavy section will cool more slowly and shrink more after ejection.
A common approach is to define a nominal wall thickness, often called “T,” and create supporting features in relation to that dimension. Ribs are typically designed at 40% to 60% of the nominal wall thickness. Boss walls are often kept around 60% of nominal wall thickness, with ribs added for support. Corner transitions should use radii instead of sharp edges, and thick-to-thin transitions should be tapered over a reasonable distance.
FeatureRecommended Relationship to Nominal WallPurposeRisk if OversizedUseful Design PracticeRib thickness40% to 60% of TAdd stiffness without making the main wall thicker.Sink marks and read-through on cosmetic surfaces.Use generous draft and rounded rib bases.Boss wall thickness50% to 70% of TSupport screws, inserts, and locating pins.Voids, sinks, and cracking near the base.Connect bosses to walls with gussets.Rib heightUp to 2.5 to 3.0 times TIncrease bending stiffness.Fill problems, weak rib tips, difficult ejection.Use multiple lower ribs instead of one very tall rib.Corner radiusMinimum 0.25 to 0.50 times TImprove flow and reduce stress concentration.Cracking and uneven filling at sharp internal corners.Maintain consistent inside and outside radius relationships.Wall transitionGradual taper over distanceBalance cooling and packing.Warping, sinks, and dimensional variation.Use tapered steps instead of abrupt section changes.Draft angleUsually 0.5° to 2° or moreEnable clean ejection and protect surfaces.Scuffing, sticking, ejector damage, cosmetic defects.Increase draft for textured surfaces.Ribs are especially important for housings, trays, covers, and structural plastic components. A rib can increase stiffness substantially because bending stiffness depends heavily on section depth. This means a well-designed ribbed wall can outperform a thick, flat wall while using less material and cooling more quickly. However, ribs must be positioned thoughtfully. Ribs directly behind high-gloss exterior surfaces can create visible sink marks, especially in ABS, PC/ABS, polypropylene, and unfilled nylon.
Design teams should also consider how a part will be measured. A thick-walled part may experience post-molding shrinkage after it leaves the tool, and a large flat panel can bend as residual stresses relax. If the part must mate with another component, define critical interfaces clearly and allow the molder to recommend process controls, fixture inspection, or secondary calibration methods.
The relationship between flow length and wall thickness is central to moldability. Longer melt flow paths require more pressure and are more vulnerable to premature freezing. Thin walls can be molded successfully when gates are positioned close to the critical areas, the material has adequate flow, mold temperatures are controlled, and the part geometry is designed for uniform filling. In contrast, a thin wall combined with a long flow path, multiple turns, texture, and glass-filled resin can create a difficult molding condition.
Gate location should support the thickest functional region or allow the melt to flow from thick to thin wherever possible. A gate positioned into a thin edge may cause hesitation as the melt reaches thicker features downstream. This can produce visible flow lines, weak weld lines, and poor packing. For large enclosures and trays, multiple gates or hot-runner systems may be needed to control pressure and cycle time, but gate marks, weld lines, and tooling cost should be evaluated early.
In projects requiring cosmetic surfaces, the gate must also be selected with appearance in mind. Hidden edges, internal walls, underside surfaces, and assembly interfaces are commonly preferred. Tunnel gates, edge gates, fan gates, valve gates, and direct sprue gates each have different effects on flow behavior and visible finishing requirements.
DefectTypical Wall-Related CauseVisual or Functional EffectPreferred Corrective ActionSecondary Process AdjustmentSink marksThick ribs, bosses, corners, or concentrated material mass.Depressed areas on visible surfaces.Core out thick areas and reduce rib thickness.Increase packing pressure or hold time where appropriate.WarpingUneven cooling, uneven wall gauge, fiber orientation.Twist, bowing, poor assembly fit.Balance wall sections and add structural ribs strategically.Adjust mold temperature and cooling channels.Short shotThin wall, long flow path, insufficient gate size.Incomplete part fill.Increase local gauge or improve gate location.Raise injection speed, pressure, or melt temperature carefully.VoidsHeavy sections shrink internally after the skin freezes.Internal bubbles and reduced structural integrity.Reduce material concentration and improve packing path.Optimize hold pressure and cooling time.Weld line weaknessFlow fronts meet after cooling in thin or distant areas.Visible seam or low-strength area.Move gate or increase local wall gauge slightly.Increase mold temperature to improve knit quality.Burn marksAir trapped near end-of-fill areas, often in thin sections.Dark or scorched appearance.Add venting and improve flow path design.Reduce injection speed near end fill if necessary.Design correction should normally come before process correction. It is possible to mask some defects by adjusting packing pressure, melt temperature, injection speed, cooling time, or mold temperature. However, process changes cannot fully compensate for poor geometry. A stable production tool should not rely on an extremely narrow molding window. If one minor temperature variation causes warpage or sinks, the part design needs further engineering attention.
For global programs involving multiple production sites, stable geometry is especially valuable. A design that only runs well on one specific machine with one experienced operator can be difficult to transfer. Balanced walls, reasonable tolerances, clear resin specifications, and documented molding parameters improve repeatability across qualified facilities.
Plastic enclosures commonly use ABS, PC/ABS, polycarbonate, or polypropylene. These parts need careful control of cosmetic surfaces, screw bosses, snap fits, vents, and internal ribs. A typical handheld enclosure may use a nominal wall between 1.5 mm and 2.5 mm, depending on resin and product size. Thin consumer electronics housings can be lighter and more attractive, but they may require higher-quality tooling, more precise gating, and more demanding process control.
Automotive components often require higher impact resistance, temperature resistance, chemical resistance, and dimensional stability. Interior trim parts may use polypropylene, TPO, ABS, PC/ABS, or reinforced compounds. Under-hood parts often use glass-filled nylon, PBT, PPS, or other engineering thermoplastics. Because vehicle components may experience vibration, thermal cycling, and loading, rib design and fiber orientation can be as important as nominal wall gauge.
Medical device housings need a combination of strength, cleanability, chemical resistance, appearance, and regulatory material traceability. Polycarbonate, ABS, PC/ABS, medical-grade polypropylene, and certain nylon or PBT grades are common choices. Wall thickness should support reliable assembly, sterilization requirements where applicable, and consistent molded dimensions.
Packaging products often use thinner walls to reduce resin usage and improve cycle time. Thin-wall packaging requires a high-flow resin, high-speed molding machine, optimized gate system, precise mold cooling, and experienced process control. A food container, cap, or lid may be much thinner than an industrial housing, but the engineering complexity can be greater because the process window is narrower.
Buyers should avoid requesting a mold quote based only on a 3D file. A reliable quotation requires the part material, annual quantity, target market, cosmetic expectations, tolerance requirements, color, texture, assembly method, packaging needs, and delivery location. If the product is still under development, request a DFM review before committing to hardened production tooling.
For early-stage programs, rapid tooling can be an effective bridge between prototype testing and mass production. It allows teams to validate part performance, assembly, appearance, and real material behavior before investing in multi-cavity hardened molds. Low-volume tooling is particularly useful for startups, industrial equipment makers, medical-device developers, automotive aftermarket brands, and consumer-product teams testing demand.
When comparing suppliers, evaluate total landed value rather than tool price alone. A lower mold quote can become expensive if the supplier does not provide DFM support, uses unsuitable steel, lacks inspection discipline, has inconsistent communication, or cannot manage engineering changes. Conversely, a slightly higher upfront engineering investment may reduce failures, scrap, delivery risk, and redesign cost.
Buyer Evaluation AreaQuestions to AskWhy It MattersPractical Evidence to RequestDFM capabilityWill the supplier review wall thickness, draft, ribs, bosses, and gating?Prevents avoidable tooling changes and defects.Written DFM report with annotated CAD images.Material controlCan the supplier source specified resin grades and provide traceability?Material variation affects shrinkage, strength, color, and compliance.Material certificates, resin brand, grade, and lot records.Tooling approachIs rapid tooling, P20 steel, H13 steel, or multi-cavity tooling appropriate?Tool life and cost must match forecast volume.Tool steel specification and cavity-life estimate.Inspection processHow are critical dimensions and appearance checked?Ensures parts meet drawing and assembly requirements.First article inspection report and control plan.Production capacityCan output scale from pilot runs to recurring production?Protects launch schedules and future demand.Machine tonnage range, lead-time plan, and capacity confirmation.Logistics supportCan the supplier package, label, consolidate, and ship globally?Reduces handoffs and export errors.Packaging proposal, Incoterms, and shipping options.For parts shipped through major trade lanes such as Shenzhen–Los Angeles, Ningbo–Rotterdam, Hong Kong–Frankfurt, Shanghai–Melbourne, and Guangzhou–Singapore, packaging design matters. Thin-wall parts can deform if cartons are overloaded, while cosmetic housings may need individual protection to avoid abrasion. A qualified supplier should be able to support custom packaging, kitting, labeling, inspection documentation, and direct shipping according to the buyer’s channel requirements.
The companies below represent a mix of international and regional manufacturing options. Selection should depend on part complexity, resin type, annual quantity, tooling budget, required certifications, project location, and desired communication model. Buyers should verify current capabilities, certifications, production availability, and country-specific compliance needs directly before placing an order.
CompanyService RegionsCore StrengthsKey OfferingsSuitable Project TypesTEAM RapidGlobal customers; China manufacturing network; experience across North America, Europe, and AsiaRapid tooling, DFM support, low-volume to volume production, integrated manufacturingInjection molding, insert molding, overmolding, CNC machining, 3D printing, vacuum casting, finishing, assemblyPrototype-to-production parts, housings, covers, trays, enclosures, functional componentsProtolabsNorth America and EuropeFast digital manufacturing workflows and short lead-time productionInjection molding, CNC machining, 3D printing, sheet metal fabricationRapid validation, low-volume molded parts, product developmentXometryNorth America, Europe, and international sourcing networksLarge supplier network and online manufacturing quotation toolsInjection molding, machining, sheet metal, casting, 3D printingCompanies needing flexible sourcing and multiple manufacturing processesEVCO PlasticsUnited States, Mexico, and selected global programsCustom molding, large parts, engineering support, production-scale operationsInjection molding, tooling support, large-part molding, assemblyIndustrial, medical, consumer, automotive, and large molded productsRosti GroupEurope, Asia, and North AmericaContract manufacturing, regulated-sector experience, product industrializationInjection molding, assembly, automation, packaging, supply-chain supportMedical, packaging, consumer, industrial, and technical plastic productsNypro, a Jabil CompanyGlobal manufacturing footprint including North America, Europe, and AsiaHigh-volume manufacturing, healthcare and consumer product expertisePrecision molding, tooling, automation, assembly, supply-chain integrationHigh-volume medical, consumer, healthcare, and electronics programsSuppliers in the United States and Europe may be preferred when local production, immediate engineering access, regional certification requirements, or short domestic logistics routes are critical. China-based suppliers can be highly competitive for rapid tooling, flexible volume runs, custom part complexity, and multi-process programs that require molding, machining, finishing, assembly, and export packaging under one coordinated supply chain.
TEAM Rapid supports global product developers, brand owners, distributors, OEM customers, startups, engineers, and individual inventors with injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, die casting, finishing, assembly, packaging, procurement support, and direct shipping. The company has more than 10 years of manufacturing experience, has served customers in more than 25 countries, completed over 6,000 projects, and supported more than 500 customers. Its ISO 9001:2015 quality management certification, in-house machining and tooling capability, detailed DFM reports, and inspection-focused manufacturing process help customers evaluate wall gauge, rib proportions, boss construction, material use, shrinkage risks, cavity layout, cycle time, and production feasibility before tooling begins. TEAM Rapid works through flexible OEM, ODM, wholesale, retail-support, regional distribution, prototype, low-volume, and recurring production models rather than limiting customers to one order format. It provides turnkey and customer-owned plant manufacturing solutions, not BOO or on-site bulk supply services. Its China-based integrated manufacturing operations and resource network support international customers with engineering communication, online quotation, project follow-up, sample approval, after-sales issue handling, packaging, and direct export shipping. While the company profile does not state overseas subsidiaries or local warehouses, its established export experience across markets including the USA, UK, France, Germany, and other regions provides practical support for customers seeking a long-term manufacturing partner rather than a simple remote order-taking supplier.
For a new project, customers can use TEAM Rapid’s injection molding services to review tooling, resin options, production methods, and molding requirements. When the CAD model is ready, request a project review through the custom manufacturing quotation page and provide the required material, annual quantity, critical tolerances, target delivery market, color, finish, and assembly requirements.
A handheld device housing may begin with a 2.0 mm PC/ABS nominal wall. The design includes screw bosses, snap fits, battery supports, connector openings, and cosmetic exterior surfaces. If the screw bosses are built at full 2.0 mm wall thickness, sinks may appear on the outer cosmetic face. The preferred solution is to core the bosses, reduce boss wall thickness to approximately 1.2 mm, connect them using thin gussets, and add draft for ejection. This approach improves appearance and shortens cooling time without sacrificing assembly strength.
An under-hood sensor bracket may use glass-filled PA66 because it needs thermal resistance, stiffness, and fatigue performance. A flat 4.0 mm section may appear strong, but it can create fiber orientation concerns and warpage. A better design may use a 2.5 mm nominal wall with ribs and gussets positioned along load paths. The final solution must account for fiber direction, mounting loads, humidity exposure, temperature cycling, and fastener torque.
A large industrial cover often requires impact resistance, mounting points, cable openings, and a professional surface finish. Using a 3.5 mm wall throughout may increase resin cost and cycle time significantly. A more balanced design can use 2.5 mm nominal walls with localized ribs, reinforced mounting areas, and smooth radii around openings. Gate location is especially important because long rectangular panels may warp if flow and cooling are not balanced.
A food or consumer packaging container may use polypropylene walls below 1.0 mm. Such products require high-speed injection, optimized gates, rapid cooling, precise mold venting, and high-flow resin. Unlike a thicker industrial housing, the challenge is not simply stiffness; it is achieving full fill at high production speed while maintaining stackability, rim strength, lid fit, and consistent appearance.
Injection-molded wall gauge optimization is relevant across automotive, medical devices, consumer products, industrial equipment, communications products, office equipment, electrical appliances, sanitary products, packaging, smart hardware, household goods, laboratory equipment, and energy-related products. Every industry applies the same basic thermal and flow principles, but each has different priorities.
Medical customers may focus on traceable materials, chemical compatibility, cleanability, reliability, and controlled assembly. Automotive customers may prioritize impact behavior, heat resistance, vibration durability, flame resistance, and dimensional stability. Consumer product brands may place greater emphasis on weight, surface quality, tactile feel, color matching, and cost. Industrial customers frequently need durable housings, cable management, mounting strength, and practical serviceability.
For global brands, it is also important to consider regional regulations and product certification pathways. Flame-retardant ratings, food-contact requirements, electrical safety standards, restricted substance requirements, recycling expectations, and customer-specific quality systems can influence material choice and ultimately affect the preferred wall gauge.
By 2026, wall thickness decisions are increasingly influenced by digital simulation, sustainability targets, material innovation, and supply-chain localization. Mold-flow simulation is becoming more accessible earlier in product development, allowing engineering teams to identify pressure drop, weld-line locations, cooling imbalance, and fiber orientation before steel is cut. This helps reduce expensive post-tooling modifications and supports faster product launches.
Lightweighting will remain a major trend. Brands are reducing plastic content through thinner walls, rib-optimized structures, topology-informed design, foamed materials, and stronger engineering resins. However, lightweighting must be balanced against product durability, recyclability, drop performance, and customer expectations. Overly thin designs can increase scrap, returns, and premature product failure, which undermines sustainability goals.
Recycled-content plastics will also affect molding strategy. Post-consumer recycled and post-industrial recycled materials can show greater variation in flow, color, shrinkage, and mechanical properties compared with virgin resin. Designers may need more conservative flow paths, better tolerance planning, or adjusted wall thickness when using recycled grades. Material validation and supplier consistency become especially important for functional products.
Policy trends in the global market are encouraging packaging reduction, material circularity, product repairability, and improved environmental reporting. Manufacturers will increasingly need to document resin selection, recycled content, product weight, packaging choices, and process efficiency. Well-designed wall gauge supports these goals by reducing unnecessary material while preserving real-world performance.
There is no single best value. A practical starting point for many parts is 1.5 mm to 3.0 mm. The correct choice depends on resin, part size, flow length, structural load, surface quality, gate location, and production method.
Uniform walls cool and shrink more evenly. This reduces sink marks, voids, warpage, stress, inconsistent dimensions, and cycle-time variation. Where different thicknesses are necessary, transitions should be gradual.
Ribs are commonly designed at 40% to 60% of the nominal wall thickness. Thicker ribs can create sink marks, especially behind cosmetic surfaces. Rounded rib bases and appropriate draft improve filling and ejection.
Yes. Thinner walls can reduce resin use and cooling time, lowering part cost in high-volume production. However, thin-wall designs may require more advanced tooling, high-flow material, faster molding equipment, and tighter process control.
Sink marks usually occur where plastic mass is concentrated, such as thick bosses, ribs, corners, and heavy wall sections. Core out thick areas, reduce rib thickness, improve packing access, and use balanced cooling.
In most cases, use ribs, gussets, or structural webs before increasing the full wall thickness. Ribs can improve stiffness efficiently while minimizing resin consumption, cooling time, and sink risk.
Yes. TEAM Rapid can provide DFM-oriented feedback for injection molding projects, including observations on wall thickness consistency, ribs, bosses, draft, undercuts, shrinkage risks, tooling feasibility, and production efficiency.
-
Global Market Injection Molding Design Rules for DFM
Effective injection molding design starts with uniform wall thickness, sufficient draft, controlled ribs and bosses, realistic tolerances, correct gate placement, and early DFM review. For Global market programs, designers should validate the part against the selected resin, expected annual volume, cosmetic requirements, assembly method, tooling location, logistics route, and regional compliance needs before cutting steel.
The most practical checklist is simple: keep walls consistent, add draft to every vertical face, avoid sharp internal corners, use ribs instead of thick sections, design undercuts only when function requires them, position gates away from cosmetic surfaces, specify tolerances based on resin behavior, and review mold flow, cooling, ejection, and assembly risks before tool release.
Common international suppliers for injection molding design support include TEAM Rapid, Protolabs, Xometry, Fictiv, ICOMold, and Rosti. Qualified Chinese manufacturing partners can also be strong options for Global market buyers when they provide ISO-certified quality systems, responsive engineering communication, documented DFM feedback, and reliable pre-sales and after-sales support. Their cost-performance advantage is especially relevant for rapid tooling, bridge production, and low-to-medium-volume molded parts.
Injection molding is one of the most scalable methods for producing plastic parts, but it is also unforgiving when product geometry does not match material flow, cooling, ejection, and tooling constraints. A design that appears correct in CAD can create sink marks, warpage, flash, short shots, visible weld lines, excessive cycle times, weak snap fits, or expensive side actions once it enters tool design.
Global market product teams frequently manage additional complexity. A consumer enclosure may be designed in London, validated in Munich, tooled in Shenzhen, assembled in Mexico, and sold through distributors in the United States, Australia, and the Middle East. In this environment, a clear injection molding DFM strategy reduces change orders, prevents communication gaps, and helps ensure that the final molded component is repeatable across production batches.
Trade hubs such as Shenzhen, Dongguan, Ningbo, Hong Kong, Singapore, Rotterdam, Hamburg, Los Angeles, Chicago, and Dubai remain important links in international manufacturing supply chains. Buyers should therefore consider not only tooling price, but also engineering response time, export packaging, inspection documentation, resin sourcing, mold ownership terms, spare-part support, and shipping flexibility.
Uniform walls help molten plastic fill, pack, cool, and shrink more predictably. Sudden changes in thickness create uneven cooling, which can cause sink marks, voids, warpage, and dimensional variation. If a section needs extra strength, use ribs, gussets, corrugation, or localized structural geometry rather than making the whole area thicker.
Typical wall thickness depends on material, flow length, part size, impact requirements, and surface finish. Thin-wall consumer packaging may use less than 1.0 mm, while structural industrial housings may use 2.5 mm or more. The objective is not to use the thinnest possible wall; it is to use a stable and manufacturable wall for the selected resin and molding process.
Draft is the taper that allows a molded part to release from the mold without drag marks, scratches, deformation, or excessive ejection force. Smooth surfaces commonly need at least 0.5° to 1° draft, while textured surfaces often require 2° to 5° or more depending on texture depth. Deep cores, highly polished cosmetic surfaces, elastomeric materials, and aggressive textures may need additional draft.
Designers should identify the mold opening direction early. Every wall, rib, boss, snap feature, and engraved detail should be checked against that direction. When a feature cannot release directly, it may need a side action, lifter, collapsible core, unscrewing mechanism, or redesign.
Sharp corners restrict resin flow and create stress concentration points. Internal corners should generally include a radius, ideally related to the nominal wall thickness. A practical starting point is an inside radius of 0.25 to 0.75 times the wall thickness, followed by an outside radius that maintains consistent material thickness around the corner.
Fillets improve strength, reduce crack initiation, assist material flow, and make it easier to machine mold cavities. They are particularly important in load-bearing brackets, clips, handles, latches, medical housings, automotive components, and electrical enclosures.
Ribs improve stiffness without the cost and cosmetic risks of thick solid walls. As a general guideline, rib thickness should be approximately 40% to 60% of the nominal wall thickness. Thick ribs can produce sink marks on the opposite cosmetic surface. Rib height is often limited to about three times the nominal wall thickness unless flow, cooling, and ejection analysis support a taller feature.
Bosses used for screws, inserts, alignment, or assembly should be supported by ribs or gussets. Avoid connecting a large solid boss directly to an exterior cosmetic wall. The local mass can cause sinks, voids, and distortion. Core out the boss wherever possible and provide sufficient draft on the internal and external surfaces.
Undercuts are features that prevent direct ejection from a simple two-plate mold. Examples include side holes, retaining clips, external threads, internal snap hooks, and recessed grooves. Some flexible undercuts can be stripped manually or automatically, but rigid materials often require side actions or lifters.
Every undercut increases tooling complexity, maintenance requirements, cycle time, and mold cost. It should be retained only if it delivers clear functional, safety, sealing, or assembly value. A small redesign of a snap fit or opening direction can sometimes eliminate an expensive mechanical action.
The following ranges are starting points for early product design. They must be adjusted according to resin grade, mold construction, texture, part size, required tolerance, gate location, flow length, and expected production volume. A DFM review should confirm final values before tooling.
Design FeaturePractical Starting GuidelinePrimary Risk if IgnoredDesign ConsiderationNominal wall thicknessKeep as uniform as possible across the partWarpage, sink marks, voids, short shotsUse ribs or gussets for strength instead of heavy sectionsDraft angle0.5° to 1° for smooth faces; more for textureDrag marks, part damage, high ejection forceIncrease draft for deep walls and textured surfacesRib thickness40% to 60% of nominal wall thicknessVisible sink marks and uneven coolingRound rib bases and maintain draft on both rib facesRib heightPreferably no more than three times wall thicknessFill difficulty, ejection problems, warpUse multiple shorter ribs where possibleBoss wall thicknessAbout 60% of nominal wall thicknessSinks, voids, cracking around screwsCore out bosses and connect them with gussetsInternal corner radius0.25 to 0.75 times nominal wall thicknessStress concentration and poor material flowMaintain consistent thickness through the cornerHole diameterPrefer diameter equal to or larger than wall thicknessCore pin deflection, incomplete fillSupport long core pins where feasibleTextured surfacesUse additional draft based on texture depthScuffing and difficult ejectionConfirm texture supplier requirements earlyThese guidelines reduce risk, but do not replace engineering analysis. Glass-filled materials, flame-retardant grades, soft elastomers, high-temperature polymers, recycled-content resins, and highly polished cosmetic parts can require substantially different geometry decisions.
Material selection affects almost every injection molding decision. Shrink rate influences mold dimensions. Melt flow influences gate size and wall-thickness capability. Glass fiber content affects stiffness but can increase warpage and surface visibility. UV exposure, chemicals, electrical requirements, impact loads, heat, food contact, medical regulations, and flame resistance must all be evaluated before finalizing the resin.
Material FamilyCommon AdvantagesTypical ApplicationsImportant DFM ConsiderationABSGood appearance, impact resistance, easy processingConsumer housings, electronics, appliance coversModerate shrinkage; avoid overly thick cosmetic wallsPolypropyleneChemical resistance, living hinge performance, low densityContainers, caps, medical trays, household productsHigher shrinkage requires tolerance planningPolycarbonateHigh impact strength and transparency optionsSafety covers, lenses, electrical enclosuresNeeds careful drying and controlled processingPA NylonStrength, wear resistance, fatigue performanceGears, clips, automotive parts, industrial componentsMoisture absorption affects dimensions and propertiesPOM AcetalLow friction, stiffness, good dimensional stabilityPrecision mechanisms, latches, gears, valvesDesign for shrinkage and avoid unsuitable chemical combinationsPC/ABSBalanced toughness, heat resistance, cosmetic qualityAutomotive interiors, equipment housings, devicesUseful for larger housings needing better impact performanceTPUElasticity, abrasion resistance, soft-touch feelProtective covers, grips, seals, wearable productsGate and ejector design must prevent distortionGlass-filled polymersHigh stiffness and strengthStructural brackets, industrial parts, automotive componentsFiber orientation can cause directional warpageFor international programs, material sourcing should be controlled by approved resin grades rather than only generic names. “ABS” is not a full specification. The grade, color masterbatch, recycled-content target, flame-retardant classification, supplier documentation, and testing requirements should be defined in the product specification.
Gate location influences filling pattern, weld lines, packing pressure, cosmetic appearance, fiber orientation, and warpage. Gates should be placed where the thickest section can be packed effectively and where any vestige can be hidden or removed safely. For a visible consumer product, a gate may be placed on an internal face, underside, assembly flange, or non-cosmetic edge.
Weld lines occur when two flow fronts meet. They may be harmless in a low-stress cover, but critical in a pressure-containing part, structural clip, hinge, or screw boss. Designers should avoid placing holes, windows, or high-stress features where weld lines are likely to occur.
Cooling is equally important. Thick local masses cool slowly and can extend cycle time or produce sinks and internal voids. Mold designers use water channels, baffles, bubblers, conformal cooling, and specialized inserts to manage heat. Product designers can support efficient cooling by avoiding unnecessary heavy sections and by providing accessible core geometry.
Ejector pins, sleeves, stripper plates, and air ejection systems leave marks or require contact surfaces. Designers should identify acceptable ejector locations before finalizing the cosmetic Class A surface. The most attractive design can become costly if no suitable ejection area exists.
Product TypeTypical Design PrioritiesFrequent Molding RiskRecommended Engineering FocusElectronic enclosureCosmetic surfaces, screw bosses, EMI features, assembly fitSinks around bosses and visible gate marksWall uniformity, hidden gates, controlled texture and draftAutomotive interior trimAppearance, clip retention, heat resistance, durabilityWarp, scratch sensitivity, clip failureMaterial validation, grain texture draft, rib layoutMedical device housingCleanability, dimensional control, traceabilityStress cracking and difficult assemblyApproved materials, radiused corners, functional testingIndustrial equipment coverImpact resistance, rigidity, environmental resistanceLarge-part warp and inconsistent fitRib strategy, gate balance, reinforced materialsConsumer packaging componentLow cost, high volume, visual consistencyThin-wall short shots and flashFlow length review, high-cavitation tool designSnap-fit assemblyRepeatable retention, easy assembly, fatigue resistanceStress whitening and breakageStrain analysis, material selection, rounded transitionsInsert molded componentMetal-plastic bond, insert position, electrical reliabilityInsert movement and crackingInsert retention, preheating, locator designOvermolded gripSoft feel, adhesion, ergonomicsDelamination and flash at interfaceMechanical locks, compatible materials, sealing surfacesEach product category requires its own acceptance criteria. A matte black appliance cover may prioritize appearance and scratch resistance, while an internal medical bracket may prioritize dimensional stability, material traceability, and sterilization compatibility. Product teams should state these priorities before DFM begins.
Before requesting quotes, prepare a 3D CAD file, 2D drawing where critical dimensions exist, annual volume forecast, selected or preferred material, color, texture, finish, assembly details, functional requirements, and destination market. If the design is still evolving, explain which dimensions are fixed and which can change after DFM review.
Buyers should ask whether the quoted tool is prototype tooling, bridge tooling, or production tooling. Aluminum rapid tooling may be suitable for market validation and low-volume production, while hardened steel tooling is generally better for high-volume programs, abrasive glass-filled resins, or long-term repeatability. Tool life should be stated as an expected range, not assumed.
Clarify mold ownership, storage period, maintenance responsibilities, cavity count, engineering change charges, sample approval process, inspection method, packaging method, and delivery terms. For global distribution, also confirm whether the supplier can support assembly, kitting, labeling, warehousing, and direct shipping to regional fulfillment locations.
The supplier landscape includes regional specialists, digital manufacturing platforms, high-volume molders, and China-based rapid manufacturing partners. The table below provides practical examples. Buyers should verify current capability, certifications, material availability, and commercial terms for each project.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidGlobal customers, including the USA, UK, France, Germany, and AsiaRapid tooling, DFM support, low-volume and production flexibilityInjection molding, insert molding, overmolding, CNC machining, vacuum casting, assemblyProtolabsNorth America and EuropeFast digital quoting and rapid manufacturing workflowsInjection molding, CNC machining, 3D printing, sheet metal fabricationXometryNorth America, Europe, and international sourcing networksBroad supplier network and online manufacturing procurementInjection molding, CNC machining, fabrication, production sourcingFictivNorth America and global supply partnersDigital manufacturing management and engineering coordinationInjection molding, CNC machining, urethane casting, finishingICOMoldNorth America with international manufacturing supportCustom plastic injection molding and mold manufacturingPrototype molds, production molds, insert molding, overmoldingRostiEurope, Asia, and North AmericaHigh-quality contract manufacturing for complex productsInjection molding, assembly, medical and consumer product manufacturingNypro, a Jabil CompanyGlobal manufacturing locationsLarge-scale healthcare and consumer manufacturing capabilityPrecision molding, automation, assembly, medical device manufacturingHusky TechnologiesGlobal, with strong packaging industry presenceHigh-volume molding systems and hot runner technologyPackaging molds, hot runners, injection molding equipment solutionsFor projects requiring rapid iterations, buyers often benefit from a supplier that can machine prototype parts, revise tooling, mold pilot batches, apply finishing, and ship assembled products without transferring data between multiple vendors. For established high-volume programs, a dedicated regional molder may provide advantages in local logistics, automation, and long-term production support.
TEAM Rapid supports innovators, product designers, engineers, startups, distributors, brand owners, and established manufacturers with a connected route from prototype to repeat production. Its ISO 9001:2015 quality management system, in-house machining and tooling capability, documented DFM feedback, and precision machining capability down to 0.01 mm provide practical evidence for controlled manufacturing of custom plastic and metal components. Rather than relying on unspecified component brands, TEAM Rapid works from customer-approved material grades, defined resin requirements, inspection criteria, and functional specifications, supporting parts such as enclosures, housings, trays, covers, fillers, insert-molded components, and overmolded assemblies. Customers can use flexible OEM and ODM cooperation, wholesale supply, prototype orders, recurring production, distributor programs, and direct-to-brand fulfillment, from one prototype to more than 100,000 parts. The company has established delivery experience with customers in more than 25 countries, including the USA, UK, France, Germany, and other international markets, supported by one-to-one engineering communication, responses commonly provided within a few hours, packaging, assembly, procurement support, limited warehousing, and direct shipping. Although its manufacturing base and integrated supply network are in China rather than represented as overseas subsidiaries or local warehouses, its export operating experience and online engineering support provide a practical service structure for international buyers who need clear pre-sales review, production updates, inspection coordination, and after-sales issue resolution. TEAM Rapid provides EPC-style turnkey and customer-owned production solutions for manufacturing projects, not BOO or on-site bulk supply services.
For early-stage projects, customers can explore TEAM Rapid injection molding services to compare rapid tooling, prototype molding, and production options. When a design is ready for review, a custom manufacturing quotation request can include CAD files, material preferences, volumes, finish requirements, and delivery destination.
A handheld diagnostic device housing may need PC/ABS for impact strength and dimensional stability. The design should include draft on textured grip zones, controlled ribs behind display openings, isolated screw bosses, and enough internal clearance for PCB installation. Gate placement should avoid the front cosmetic face, while ejector locations should be hidden inside assembly surfaces.
An automotive under-hood clip may require heat-resistant nylon with glass reinforcement. In this case, fiber orientation and moisture conditioning are important. The designer should avoid abrupt thickness transitions, place fillets at clip roots, and evaluate the part under repeated insertion and removal cycles. A low-cost tool that ignores fiber-related warpage can create fit problems later in vehicle assembly.
A consumer storage container with a living hinge may use polypropylene. The hinge must be thin and carefully oriented to support repeated flexing, while the body should retain a stable wall thickness. Gate position and flow direction can influence hinge performance. A prototype run should verify opening force, fatigue life, lid alignment, and sealing behavior.
An industrial control-box cover may require flame-retardant ABS or PC/ABS. Designers must account for the material’s flow behavior, flame-retardant additive effects, electrical clearance requirements, screw boss strength, gasket compression, and exterior finish. Venting and gate placement should be reviewed to reduce burn marks around deep ribs and internal features.
By 2026, injection molding design is increasingly shaped by automated DFM, artificial intelligence-assisted mold-flow prediction, digital traceability, material data management, and more sustainable resin strategies. CAD platforms and supplier quoting systems are becoming better at identifying missing draft, thick wall sections, undercuts, and high-risk tolerances before engineers issue a tooling purchase order.
Sustainability will continue to influence material selection. Recycled-content polymers, bio-based materials, mono-material design, lightweighting, and easier disassembly are becoming more important in consumer goods, packaging, mobility products, and electrical equipment. However, recycled-content resin can introduce variation in color, mechanical properties, flow, and shrinkage, so qualification testing and approved-source control are essential.
Policy requirements are also evolving across major markets. Product teams should monitor chemical restrictions, packaging rules, recyclability targets, extended producer responsibility requirements, medical device documentation, electrical safety standards, and regional labeling obligations. The mold design itself may not be regulated, but material selection, traceability, product safety, and end-of-life expectations increasingly affect molded-part decisions.
Manufacturers are also adopting conformal cooling, in-mold sensors, automated visual inspection, robotic part handling, and digital process monitoring. These technologies can improve consistency, reduce cycle time, and provide better production data, particularly for high-value medical, automotive, industrial, and electronics applications.
Maintain consistent wall thickness. It has a direct effect on filling, cooling, shrinkage, warpage, sink marks, cycle time, and part quality.
A common starting point is 0.5° to 1° for smooth surfaces. Textured, deep, polished, or difficult-to-eject surfaces often require more draft.
They can, but sharp internal corners are generally discouraged because they create stress concentrations and restrict resin flow. Use fillets whenever function permits.
Side actions are commonly needed for rigid undercuts, side holes, external snap features, recessed grooves, and geometry that cannot release in the mold opening direction.
Send 3D CAD files, critical drawings, material preferences, finish requirements, color, annual volume, target delivery date, destination, assembly needs, and known functional requirements.
Yes. Rapid tooling can be suitable for prototype validation, bridge production, market testing, and selected low-volume production. The correct choice depends on resin, cavity count, part complexity, surface finish, and expected production quantity.
Reduce thick local masses, use ribs instead of heavy walls, core out bosses, improve wall uniformity, and review gate location and packing conditions with the molding engineer.
Early DFM identifies risks while geometry can still be changed quickly. It is far less expensive to revise CAD than to modify hardened steel after the mold has been manufactured.
-
Mold Flow Analysis for Global Market Tooling Choices
Mold flow analysis is a digital injection molding simulation used before tooling to predict how molten plastic will fill, pack, cool, shrink, and warp inside a mold. It helps product teams identify likely defects such as short shots, weld lines, sink marks, air traps, excessive clamp force, uneven cooling, and dimensional distortion before steel is cut.
For Global market buyers, the most practical approach is to run a mold filling and cooling study during DFM review, then revise wall thickness, gate position, runner layout, material selection, and cooling channels before ordering tooling. This can reduce development iterations, improve mold reliability, and lower the risk of expensive post-tooling modifications.
Established providers commonly considered for mold flow simulation and tooling support include Autodesk Moldflow, Moldex3D, SIGMA Engineering, SIMCON, CoreTech System, and TEAM Rapid. Software providers supply the analysis platform, while engineering-led manufacturers apply the results to real mold design, rapid tooling, sampling, and production.
Injection molding is highly sensitive to how polymer melt moves through a cavity. A part that appears simple in CAD can become difficult to mold when it combines thin ribs, deep bosses, non-uniform walls, cosmetic surfaces, long flow lengths, engineering resins, inserts, or tight dimensional tolerances. Mold flow analysis converts the part design, material data, gate proposal, runner system, process assumptions, and cooling concept into a predictive simulation.
The analysis does not replace moldmaker experience or physical sampling. Instead, it gives engineers evidence for choosing the most robust design path before a mold is manufactured. For buyers coordinating design teams in cities such as London, Munich, Chicago, Shenzhen, Singapore, Dubai, and Melbourne, the process creates a common technical language before tooling decisions are released across borders.
Analysis AreaWhat Is EvaluatedTypical Risk FoundPractical Tooling DecisionFill analysisMelt-front movement, fill time, pressure, and flow balanceShort shots, hesitation, overpacking, unbalanced cavitiesMove gates, enlarge runners, adjust wall thickness, change injection strategyPack analysisHolding pressure effect and volumetric shrinkageSink marks, internal voids, inconsistent dimensionsRevise gate size, holding profile, rib thickness, and packing windowCooling analysisHeat removal, mold temperature balance, and cooling durationLong cycle time, hot spots, uneven shrinkageAdd baffles, bubblers, conformal cooling, or optimized water linesWarpage analysisDeflection caused by shrinkage, orientation, and thermal gradientsTwist, bow, uneven flatness, assembly failureModify geometry, gate direction, material grade, or cooling layoutWeld-line evaluationLocations where melt fronts meetWeak joints, cosmetic marks, leakage or crack riskRelocate gates, improve venting, increase melt temperature, revise geometryAir-trap evaluationAreas where air is compressed during fillingBurn marks, incomplete filling, poor surface qualityAdd vents, overflow wells, ejector venting, or change fill directionClamp-force predictionForce needed to keep the mold closed during injectionFlash, machine mismatch, tool damageSelect an appropriate molding machine and optimize gate and process conditionsThe table shows why a flow study should be linked to a decision process. A red or blue simulation image alone is not sufficient. The useful deliverable is a prioritized engineering plan explaining which findings are critical, which are acceptable, and how each recommendation affects tooling cost, molding stability, appearance, and part performance.
The Global market for mold flow analysis is growing because product cycles are shorter, resin options are more specialized, and molding projects increasingly involve electronics, medical devices, electric vehicles, consumer products, industrial equipment, and sustainability requirements. Buyers are under pressure to achieve functional prototypes quickly while also avoiding unnecessary production-tool revisions.
Manufacturing hubs in China, Germany, the United States, Japan, South Korea, Mexico, Vietnam, Poland, and India are increasingly connected through international sourcing networks. Mold design may be reviewed in Europe, tool steel may be machined in Guangdong, samples may be tested in North America, and production may be shipped through ports such as Shenzhen, Ningbo-Zhoushan, Hamburg, Rotterdam, Los Angeles, Long Beach, Singapore, or Jebel Ali. A structured flow analysis report reduces the communication gaps that can occur in this distributed manufacturing environment.
For low-volume programs, the analysis may focus on whether rapid tooling can produce acceptable parts without excessive cycle time or warpage. For larger production programs, the review may cover cavity balance, hot runner selection, cooling efficiency, automation compatibility, resin consumption, and total cost per part. The investment level should be matched to the commercial risk of the project.
Different projects need different levels of simulation. A simple single-cavity enclosure may only need filling, weld-line, venting, and basic warpage checks. A high-volume automotive, medical, or electrical connector mold may require detailed packing, cooling, fiber-orientation, insert molding, and multi-cavity balance studies.
Service TypeBest ForMain DeliverablesBuyer BenefitBasic fill studySimple housings, covers, trays, and prototype partsFill pattern, pressure, weld lines, air traps, gate proposalFast screening before rapid toolingFill and pack studyParts with ribs, bosses, thick-to-thin transitions, and cosmetic surfacesSink-risk map, shrinkage review, packing profile recommendationsImproves dimensional and cosmetic consistencyCooling studyMedium and high-volume molds with cycle-time targetsCooling channel assessment, temperature balance, cycle estimateSupports lower unit cost and stable productionWarpage studyFlat panels, snap-fit assemblies, long parts, reinforced resinsDeflection prediction, orientation effect, geometry recommendationsReduces assembly and flatness failuresMulti-cavity balance studyFamily molds and multi-cavity production toolsCavity filling balance, runner optimization, pressure comparisonImproves consistency across cavitiesFiber-orientation studyGlass-filled nylon, reinforced polypropylene, and structural partsFiber alignment, anisotropic shrinkage, stiffness direction reviewHelps control warpage and mechanical performanceInsert and overmolding studyMetal inserts, electrical parts, soft-touch overmoldingInsert temperature effects, flow behavior, bonding-risk assessmentProtects inserts and improves process repeatabilityFor a project involving insert molding or overmolding, the simulation must consider more than cavity filling. Metal inserts can remove heat rapidly, alter flow direction, create weld lines, and cause localized stress. Similarly, soft elastomer overmolding requires attention to substrate adhesion, gate placement, part retention, and cosmetic surface control.
A professional report should begin with the part name, material grade, shrinkage assumptions, gate proposal, machine assumptions, cavity count, and study scope. Without these inputs, buyers cannot judge whether the findings apply to the intended production situation. For example, a simulation using a generic polypropylene grade may not accurately represent a specified mineral-filled, recycled-content, flame-retardant, or food-contact grade.
Start with the filling pattern. The goal is normally smooth, balanced progression from the gate to the farthest regions without hesitation or excessive race tracking. Next, inspect pressure at end of fill. If predicted pressure is close to machine limits, the supplier may need to enlarge gates, change wall geometry, raise melt temperature, or choose a larger press.
Then review weld lines and air traps in relation to functional features. A weld line near a non-critical cosmetic edge may be acceptable. A weld line crossing a snap-fit, sealing surface, screw boss, high-load tab, or fluid path may require redesign. Cooling and warpage results should be evaluated against the actual assembly tolerances rather than vague expectations of “flatness.”
Finally, ask whether the proposed changes alter cost, lead time, mold complexity, resin use, or maintenance. A recommendation for conformal cooling may improve cycle time but can increase tool cost. A larger gate can reduce pressure but may leave a more visible gate vestige. The best solution balances technical performance with commercial priorities.
Buyers should treat flow simulation as part of a broader design-for-manufacturing process. It is most effective when the design team provides accurate CAD files, material preferences, expected annual volume, surface-quality requirements, assembly tolerances, regulatory needs, and target markets. A supplier cannot make reliable tooling recommendations if critical product information is missing.
When comparing quotations, do not select a supplier only because it offers the lowest tooling price. A low initial quote can become expensive if the mold requires repeated rework, production cycle time is high, part scrap is excessive, or the chosen machine cannot maintain a stable process window. A transparent supplier should identify potential trade-offs before purchase order release.
Observed IssueLikely Simulation FindingPossible Design CauseTypical Corrective ActionShort shotIncomplete fill at far flow endLong flow path, thin section, small gate, inadequate ventingIncrease gate size, revise wall thickness, improve venting, optimize processSink markHigh local volumetric shrinkageThick bosses, heavy ribs, uneven wall sectionsCore out thick areas, reduce rib thickness, adjust packing and coolingWarped panelUneven cooling or orientation-driven shrinkageAsymmetric geometry, poor cooling layout, reinforced resinBalance cooling, alter gate location, add structural features, revise materialBurn markAir trap with compressed gas near end of fillInsufficient venting, high injection speed, trapped cavity airAdd vents, reduce local speed, revise gate position and flow directionFlashExcessive pressure or clamp-force demandSmall gates, restrictive flow, poor mold fit, low clamp forceOptimize gate and process, verify machine selection, improve mold shutoffWeak weld lineMelt fronts meet at a low temperature or sensitive areaMultiple flow paths, holes, inserts, poor gate positionRelocate gate, adjust temperature, move weld line away from load areasUneven cavity outputImbalanced runner or filling patternPoor runner geometry, unequal flow lengths, inconsistent coolingBalance runner system, adjust gates, improve cooling uniformityThe table is useful during supplier review because it links visible defects to engineering causes. Not every issue can be fully eliminated through simulation, particularly when material variation, machine condition, process control, or cosmetic standards are involved. However, a well-executed study helps prevent predictable risks from becoming expensive surprises after the mold trial.
Automotive programs use mold flow analysis for interior trim, under-hood covers, sensor housings, lighting components, clips, ducts, battery-related plastic parts, and reinforced structural components. These parts often require repeatable dimensions, controlled warpage, robust snap fits, and predictable performance across large production volumes.
Medical device manufacturers use simulation for handheld enclosures, diagnostic equipment housings, fluid-management components, disposable trays, laboratory consumables, and assembly parts. Material selection, cleanability, dimensional accuracy, traceability expectations, and surface quality make early engineering review especially important.
Consumer electronics and communication products benefit from flow simulation when producing thin-wall cases, wearable-device components, charging accessories, cable-management parts, buttons, covers, and high-gloss or textured housings. Gate position and weld-line control can directly affect visual quality and perceived product value.
Industrial equipment, office products, home appliances, sanitary products, and commercial devices often use molded enclosures, panels, handles, covers, brackets, and functional internal components. These applications may have lower volumes than consumer goods but higher demands for assembly fit, durability, and cost-efficient tooling.
Mold flow analysis is especially valuable for complex plastic parts where functional risk and tooling cost are high. Typical applications include battery housings, electrical enclosures, medical appliance casings, industrial control covers, appliance panels, automotive clips, cosmetic containers, fluid fittings, storage trays, protective shells, and precision mechanical plastic parts.
It is also useful when changing from one manufacturing method to another. A product initially produced through SLA 3D printing, SLS printing, CNC machining, or vacuum casting may require geometry adjustments before injection molding. Features that work well in a prototype can become difficult to fill, cool, eject, or inspect in a molded production part.
For companies moving toward short-run market validation, rapid tooling plus simulation can provide a practical bridge between prototype testing and mass production. The buyer can test real injection molded material properties before investing in a long-life production mold.
The following companies represent widely recognized software, simulation, and manufacturing options for Global market buyers. Selection depends on whether the project requires software access, specialist engineering consultation, rapid tooling, production tooling, molded parts, or a complete prototype-to-production pathway.
CompanyService RegionsCore StrengthsKey OfferingsAutodesk MoldflowGlobal software network with users in North America, Europe, Asia-Pacific, and the Middle EastWidely used injection molding simulation platform and extensive industry adoptionFill, pack, cooling, warpage, fiber orientation, and process optimization softwareMoldex3DGlobal, with strong presence across Asia, Europe, and North AmericaAdvanced 3D simulation for complex molding, electronics, automotive, and engineering applicationsPlastic flow simulation, insert molding, overmolding, cooling, warpage, and manufacturing optimizationSIGMA EngineeringEurope, North America, Asia-Pacific, and global industrial marketsVirtual molding technology focused on process optimization and production stabilitySIGMASOFT virtual molding, process variation assessment, cycle and quality optimizationSIMCONEurope-based support with international software users and partnersInjection molding simulation with practical design and process evaluation toolsCADMOULD simulation, filling, packing, cooling, warpage, and mold design supportCoreTech SystemGlobal through Moldex3D distribution and engineering channelsSimulation technology for advanced polymer processing and mold validation3D flow analysis, material behavior review, fiber effects, cooling and warpage studiesTEAM RapidGlobal customers in more than 25 countries, serving China, the USA, the UK, France, Germany, and other marketsIntegrated DFM, rapid tooling, injection molding, CNC machining, and low-volume manufacturing supportMold flow-oriented DFM review, rapid tooling, injection molding, prototype production, finishing, assembly, and shippingSoftware companies are suitable when an organization has internal molding engineers who need analysis capability across multiple programs. Manufacturing partners are suitable when buyers want one supplier to interpret the results, revise the mold design, build the tool, mold samples, inspect parts, and manage production. For international programs, buyers should ask who owns the simulation decisions and whether the tooling engineer responsible for machining has reviewed the recommendations.
TEAM Rapid supports Global market customers that need practical engineering feedback before committing to tooling. Its service model combines DFM analysis, mold flow-oriented risk review, rapid tooling, injection molding, CNC machining, 3D printing, vacuum casting, die casting, sheet metal fabrication, finishing, assembly, packaging, and direct shipping. Customers can begin with prototypes, validate design changes, move into short-run molded parts, and scale toward recurring production without managing separate suppliers for each stage.
For injection molded projects, TEAM Rapid can evaluate wall thickness, draft, gates, runners, parting lines, undercuts, venting, ejection, cooling concerns, shrinkage risk, resin selection, mold cavities, and expected cycle time. Buyers can review the company’s injection molding services when planning production parts, or explore rapid tooling solutions when fast market validation is required.
TEAM Rapid demonstrates relevant manufacturing authority through ISO 9001:2015 certification, more than 10 years of industry experience, more than 500 satisfied customers, over 6,000 delivered projects, and service experience across more than 25 countries. Its manufacturing scope covers plastic and metal components from a single prototype to more than 100,000 parts, supported by in-house machining, tooling manufacturing, molding capability, and an integrated manufacturing resource network in China. Rather than making unsupported claims about proprietary component brands, the company works from customer-specified material, functional, cosmetic, and tolerance requirements, with engineering review and specification compliance built into its ISO-based quality process. It supports OEM and ODM requirements, wholesale programs, brand owners, product developers, distributors, dealers, end users, startups, and individual innovators through flexible prototype, low-volume, and recurring-production models. TEAM Rapid provides turnkey and customer-owned product manufacturing solutions, including tooling, parts, finishing, assembly, packaging, procurement coordination, and direct shipment; it does not operate BOO or on-site bulk-supply models. Its Global market commitment is demonstrated by established project experience in the USA, UK, France, Germany, China, and other markets, direct shipping capability, limited warehousing support, and one-to-one engineering communication with responses typically available within hours. While customers should confirm any specific local warehousing or regional support requirement during quotation, the company’s online pre-sales engineering reviews, manufacturing updates, inspection support, packaging coordination, and after-sales project communication provide practical protection for international buyers.
For a tailored review of a mold flow analysis, DFM package, prototype plan, or tooling quotation, buyers can request a manufacturing quote with CAD files, material preferences, production volume, and target delivery date.
A consumer device enclosure may have a large visible surface, thin walls, snap fits, screw bosses, and internal support ribs. A fill study can identify whether a gate near the edge creates weld lines across a logo area or a critical clip. Pack analysis may reveal sink risk behind thick bosses. The recommended change may include moving the gate to a hidden underside, coring thick features, reducing rib thickness, and improving venting near the last-fill region. These changes can protect cosmetic appearance before the first T1 sample.
A glass-filled nylon bracket can experience directional shrinkage caused by fiber orientation. Even when the part fills successfully, it may warp after ejection and fail assembly with nearby metal components. A warpage and fiber-orientation study can help determine a more appropriate gate direction, wall transition, rib layout, and cooling balance. The resulting tooling design may cost slightly more, but it can reduce downstream fitting issues and production rejection.
A medical equipment housing may require controlled appearance, consistent assembly, safe edge conditions, and reliable screw-boss performance. Flow analysis can identify air traps near internal corners and weld lines around openings. Combined with DFM review, the design team may add draft, relocate gates, revise boss geometry, and define suitable inspection points before rapid tooling. This approach helps teams obtain functional molded samples faster than relying on repeated trial-and-error modifications.
A packaging tray with multiple cavities may appear straightforward but can suffer from uneven filling if the runner system is not balanced. Simulation can compare runner paths, gate sizes, cavity pressure, and cooling behavior. The buyer can then decide whether a cold runner, hot runner, or revised cavity arrangement is justified based on annual volume, resin savings, cycle time, and quality requirements.
By 2026, mold flow analysis will increasingly be connected to digital manufacturing systems rather than used only as a standalone design check. Simulation platforms are incorporating more automation, improved material databases, cloud collaboration, machine-learning-assisted optimization, and stronger links between CAD, mold design, process settings, and quality data. This will allow teams in different Global market locations to review molding risks earlier and make decisions faster.
Sustainability will also influence simulation priorities. Brands are increasing the use of recycled-content resins, bio-based polymers, lightweight structures, lower-energy production, and reduced scrap targets. These materials can have different flow, shrinkage, moisture sensitivity, and mechanical behavior compared with conventional virgin resin grades. Mold flow analysis will be used more often to validate whether recycled or lower-carbon material options can meet appearance, strength, and cycle-time requirements.
Policy and compliance expectations are expanding across regions. European product sustainability initiatives, extended producer responsibility programs, packaging regulations, chemical restrictions, and traceability expectations are pushing manufacturers to document material choices and reduce waste. Global buyers should ask whether a supplier can support material documentation, process records, inspection requirements, and responsible packaging practices appropriate for the destination market.
Cooling technology will remain a major focus. Conformal cooling, improved thermal control, additive-manufactured inserts, sensor-based mold monitoring, and predictive maintenance can reduce cycle time and improve dimensional stability. For high-volume programs, even a small reduction in cycle time can create substantial savings across the life of a mold.
Prepare a 3D CAD model in STEP, IGES, Parasolid, or native format where possible. Include the latest revision level and identify any surfaces that cannot be changed. Provide the expected resin, annual volume, part weight target, cosmetic requirements, functional loads, target tolerances, assembly interfaces, and preferred production location.
Ask the supplier to confirm the analysis scope before work begins. For example, a rapid-tooling program may need a basic fill and warpage review, while a high-volume multi-cavity project may need comprehensive filling, packing, cooling, runner balance, and cycle-time analysis. Set a review meeting or written approval stage before the supplier begins tool steel machining.
After the analysis is complete, ensure that approved recommendations are reflected in the final mold design. Then compare the first molded samples against the simulation predictions. If the results differ significantly, investigate material lot variation, actual machine settings, mold temperature, venting performance, cooling conditions, and measurement method. This closed-loop learning process improves future projects.
No. Very simple, low-risk parts with generous walls and low production volumes may only need a standard DFM review. However, analysis is strongly recommended for complex, thin-wall, cosmetic, reinforced, multi-cavity, insert molded, or high-volume components where tooling changes would be costly.
No simulation can guarantee a defect-free part. Actual results depend on material behavior, machine condition, mold quality, process control, cooling performance, and operator settings. The purpose is to identify and reduce predictable risks before tooling is made.
Provide accurate CAD, material grade, filler content, intended annual volume, gate restrictions, surface requirements, tolerance expectations, mold cavity count, and production goals. The more complete the inputs, the more useful the recommendations will be.
It can reduce cost by identifying gate, runner, venting, cooling, wall-thickness, and warpage issues before steel is machined. Preventing a major tool modification is often more valuable than the cost of the initial simulation.
Yes. Cooling analysis can identify hot spots, inefficient cooling lines, and temperature imbalance. Better cooling design can reduce cooling time, improve part consistency, and lower production cost per part.
Yes. Rapid tooling has shorter lead times, so early engineering decisions are especially important. A focused analysis can help avoid wasting time on avoidable tool changes and support faster validation using real molded materials.
Yes, but the accuracy depends on having appropriate material data. Recycled-content resins may have wider property variation than virgin grades, so buyers should discuss material sourcing, lot control, cosmetic expectations, and test requirements with the supplier.
Ask about DFM scope, mold flow analysis capability, material data, tooling steel, cavity strategy, cooling design, sample lead time, inspection method, change-control process, shipping terms, communication frequency, and after-sales support for mold adjustments or recurring production.
-
Global Market Guide to Selecting Steel for Injection Molds
Selecting steel for injection molds should start with the resin, expected production volume, cosmetic finish, part tolerance, cooling requirement, and operating environment. P20 is usually the practical choice for low-to-medium volume molds and rapid tooling. H13 is preferred for higher-temperature processing, glass-filled plastics, and longer production life. S136 is the stronger choice for corrosion resistance, polished optical surfaces, medical components, transparent parts, and PVC processing.
For most Global market projects, use pre-hardened P20 for economical tooling, hardened H13 for demanding production cycles, and stainless S136 when corrosion protection and mirror polishing matter. Tool steel should be selected together with mold design, cooling layout, gate position, part geometry, and maintenance planning rather than as an isolated purchasing decision.
Global buyers should compare steel traceability, hardness certification, heat-treatment capability, machining quality, lead time, and maintenance support. Qualified international suppliers, including Chinese mold manufacturers with ISO-based quality systems, responsive pre-sales and after-sales engineering support, and cost-performance advantages, can be a strong option for projects requiring fast tooling and molded parts.
Injection mold steel affects much more than the initial tooling price. The selected grade influences machining time, polishing performance, cycle time, cooling efficiency, wear resistance, mold life, dimensional stability, repairability, and consistency of molded parts. A low-cost material choice can become expensive if the cavity wears early, cooling channels corrode, molded surfaces develop defects, or the tool requires repeated welding and polishing.
For buyers in the Global market, material selection is especially important because products are often designed in one country, tooled in another, assembled in a third location, and sold through international distribution networks. A mold may need to run in Shenzhen, Ningbo, Singapore, Monterrey, Istanbul, Rotterdam, Chicago, or Frankfurt during its lifecycle. Steel selection must therefore consider transportation, storage humidity, resin availability, local maintenance capability, and production transfer requirements.
A well-selected steel grade supports predictable production. It helps control flash, sink marks, parting-line wear, ejector-pin galling, corrosion, polishing quality, and cavity dimensions. The correct steel also supports better DFM decisions, such as using appropriate draft angles, optimized ribs, balanced wall thickness, stable gate geometry, and adequate cooling circuits.
Injection mold steels are commonly grouped into pre-hardened steels, through-hardening steels, stainless steels, and specialty grades. The best choice depends on the working condition of each mold component. A mold base, cavity insert, core insert, slider, lifter, ejector plate, guide pin, and wear plate do not always need the same material.
Steel GradeTypical ConditionMain StrengthCommon Resin CompatibilityTypical Mold UsePractical LimitationP20Pre-hardened, commonly around 28–34 HRCGood machinability and economical tooling costABS, PP, PE, PS, PC, PA, TPERapid tooling, low-volume molds, housings, coversLower corrosion and wear resistance than hardened grades718 / 718HPre-hardenedBetter polishability and cleaner structure than standard P20ABS, PC, PMMA, PA, consumer-grade engineering plasticsMedium-volume cosmetic parts and mold insertsMay cost more than P20 without being necessary for simple partsH13Heat treated, often 48–52 HRC depending on applicationHot hardness, toughness, heat-check resistanceGlass-filled nylon, PC, PBT, PPS, high-temperature materialsCore inserts, cavities, slides, high-wear componentsRequires controlled heat treatment and longer manufacturing timeS136Hardened stainless steelCorrosion resistance and high-polish capabilityPVC, PMMA, PC, medical resins, optical-grade materialsMedical molds, transparent parts, humid production environmentsHigher material and machining costNAK80Pre-hardenedFine polishability, stable machining, good EDM finishABS, PC, PMMA, consumer and automotive cosmetic partsTextured surfaces, glossy covers, display-related housingsNot the first choice for highly corrosive resin environments420 Stainless SteelHardened stainless tool steelCorrosion resistance and moderate polishabilityPVC, flame-retardant plastics, medical resinsBudget-conscious corrosion-resistant mold componentsGrade quality varies significantly between steel millsD2 / Cr12MoVHardened cold-work steelHigh wear resistanceFilled plastics and abrasive applicationsWear inserts, cutters, high-wear mechanical featuresCan be less tough and more difficult to repair than H13The table shows why P20, H13, and S136 are not direct substitutes. P20 solves cost and lead-time needs. H13 solves thermal fatigue and abrasive wear challenges. S136 solves corrosion, cleanability, and high-finish requirements. A mold can also combine these steels. For example, a P20 mold base may use H13 gate inserts and slides, while S136 is reserved for cavity inserts exposed to PVC or moisture-sensitive applications.
P20 is one of the most widely used mold steels for injection molding because it is supplied pre-hardened and can often be machined without a separate hardening process. This reduces tooling lead time and avoids dimensional distortion associated with post-machining heat treatment. P20 is commonly selected for rapid tooling, low-volume manufacturing, bridge production, and medium-volume injection molds.
It performs well with common materials such as polypropylene, polyethylene, ABS, polystyrene, standard nylon, TPE, and many general-purpose engineering plastics. It is a sensible choice for enclosures, housings, trays, caps, appliance parts, office equipment components, automotive interior trim, and industrial covers where ultra-high polish or extreme wear resistance is not required.
However, P20 should be evaluated carefully for glass-filled materials, PVC, flame-retardant grades, highly humid production conditions, and tools intended to produce hundreds of thousands or millions of cycles. In such cases, corrosion, abrasion, and cavity wear can reduce tool performance. Surface treatments, nitriding, chrome plating, or localized H13 and S136 inserts may improve performance without requiring the entire mold to be made from premium steel.
H13 is a hot-work tool steel known for toughness, thermal stability, and resistance to heat checking. While it is strongly associated with die casting, it is also valuable in injection molds that process high-temperature resins, glass-filled materials, and abrasive compounds. H13 is frequently used for core inserts, cavity inserts, slides, lifters, gate inserts, and parts of a mold subjected to repeated thermal loading.
The steel is generally machined in an annealed or softer condition, then heat treated to the required hardness. This process demands controlled machining allowances, stable heat treatment, stress relief, precision grinding, and inspection. Poor heat treatment can lead to cracking, distortion, weak toughness, or inconsistent hardness. For that reason, buyers should request material certificates, hardness reports, and clear heat-treatment specifications.
H13 is suitable for reinforced nylon, PBT, PPS, high-temperature polycarbonate applications, and other resins that increase surface wear. It can also be selected for features with thin steel conditions, sharp ribs, aggressive shutoffs, or complex moving components. Although the upfront tool cost is higher than P20, the investment can be justified when the mold must maintain dimensions over long production runs.
S136 is a stainless mold steel commonly specified where corrosion resistance, polishability, cleanliness, and surface quality are critical. It is particularly suitable for PVC, flame-retardant resins, medical-grade polymers, transparent plastics, moisture-prone manufacturing conditions, and applications requiring a mirror finish.
For clear polycarbonate, PMMA, medical diagnostic housings, optical components, transparent lenses, laboratory consumables, cosmetic packaging, and high-gloss consumer parts, S136 can support better surface quality when machining and polishing are properly controlled. It is also useful for molds that may be stored or transported through humid ports and coastal regions where rust prevention is a practical concern.
S136 is more expensive than P20 and generally requires more careful machining, polishing, and heat treatment. The added cost is worthwhile only where corrosion control, optical surface requirements, hygienic maintenance, or part appearance demands it. For standard black ABS housings, P20 or 718H may be commercially more reasonable.
The resin is often the fastest starting point for selecting mold steel. Some resins are relatively gentle on the cavity, while others are abrasive, corrosive, or processed at high temperatures. Production volume then determines whether the initial investment in a higher-grade steel will return value through reduced maintenance and longer service life.
Project RequirementRecommended Steel DirectionReason for SelectionTypical PartsRecommended Tooling StrategyRisk if Under-SpecifiedPrototype or bridge production below 5,000 partsP20 or aluminum with steel insertsFast machining and lower startup costValidation housings, test enclosures, launch samplesRapid tooling with replaceable insertsUnnecessary capital cost from premium production steelLow-to-medium volume consumer productsP20 or 718HBalanced cost, machining speed, and surface qualityCovers, storage trays, appliance shellsPre-hardened mold base and quality cooling designPremature polish loss if low-grade material is usedHigh-gloss or textured cosmetic surfaces718H, NAK80, or S136Improved polishability and surface consistencyDisplay bezels, premium cases, cosmetic capsDedicated polishing allowance and controlled EDM processOrange peel, pitting, inconsistent texture reproductionGlass-filled or abrasive engineering plasticsH13, D2, or hardened wear insertsHigher wear resistance at gates and flow pathsGears, structural brackets, automotive under-hood partsHardened inserts in high-wear zonesGate erosion, flash, unstable dimensionsPVC, flame-retardant, or corrosive resinS136 or 420 stainless steelCorrosion resistance protects cavity surfaces and cooling areasElectrical components, medical parts, fittingsStainless cavity/core inserts and preventive maintenanceRust, pitting, surface defects, difficult mold cleaningHigh-temperature processingH13 or specialty hardened steelThermal stability and resistance to heat fatiguePPS connectors, reinforced nylon componentsHeat-treated inserts with engineered coolingCracking, deformation, accelerated wearTransparent optical or medical partsS136Mirror polishability, corrosion resistance, clean maintenanceLenses, clear chambers, diagnostic housingsHigh-quality polishing and protected handling processFlow marks, surface haze, rust contaminationMaterial selection should also account for the part’s visual standard. A molded surface with leather texture, matte finish, or paint coverage may not need premium polishing steel. By contrast, a clear lens, piano-black housing, chrome-plated decorative part, or medical component can reveal small cavity defects immediately. For these applications, steel cleanliness, polishing skill, EDM parameters, and mold protection procedures are as important as the nominal steel grade.
Buyers should not approve mold steel based on a grade name alone. Steel names can vary by mill, country, and supplier. A documented equivalent may perform differently depending on chemical composition, remelting process, cleanliness, delivery hardness, and heat-treatment quality. Purchasing teams should request clear specifications before tooling begins.
Buying CriterionWhat to ConfirmWhy It MattersSuggested Buyer ActionCommon Problem AvoidedRelevant Project StageSteel mill traceabilityMaterial certificate, heat number, grade specificationConfirms the actual steel source and compositionRequest certificates for cavity, core, and major insertsUnverified substitute materialQuotation and tooling kickoffHardness conditionPre-hardened level or final HRC targetDetermines wear resistance and machining approachState hardness requirements on approved drawingsSoft cavities or brittle insertsDesign reviewHeat treatmentVacuum hardening, tempering, stress relief, inspection methodControls distortion, toughness, and service lifeRequire heat-treatment records for H13 and S136 insertsCracking and unstable dimensionsTool manufacturingSurface finish requirementSPI finish, texture standard, optical polishing needDefines steel polishability and process planningProvide approved appearance samples where possibleMismatch between expected and actual cosmetic qualityDFM and mold designResin dataFull resin grade, filler percentage, flame-retardant packageIdentifies abrasion and corrosion riskShare resin datasheet before steel is orderedWrong material selection for filled or corrosive resinEarly engineeringTool life targetExpected annual volume and total lifetime cyclesSets a rational tooling investment levelSpecify prototype, bridge, low-volume, or production intentOverspending or premature mold wearRFQ stageMaintenance planCleaning, lubrication, spare inserts, storage protectionExtends mold life after deliveryInclude maintenance instructions and spare-part listRust, seizure, avoidable downtimeProduction and after-salesFor international projects, the mold supplier should provide a mold drawing, DFM report, material list, trial report, inspection information, and recommended maintenance schedule. If production will move between facilities, consider using standard mold components from globally recognized suppliers such as HASCO, DME, Meusburger, Misumi, or compatible equivalents. Standardization makes replacement parts and maintenance easier across regions.
Automotive suppliers often need H13 or hardened inserts for reinforced parts, clips, electrical connectors, under-hood components, and high-cycle interior systems. Consumer electronics brands frequently choose 718H, NAK80, or S136 for polished covers, device housings, display frames, and textured surfaces. Medical manufacturers may specify S136 because the mold needs corrosion resistance, cleanability, stable polish, and consistent output for regulated components.
Industrial equipment manufacturers need reliable steel choices for housings, cable-management systems, valves, fittings, control enclosures, and durable functional parts. Appliance companies may combine P20 mold bases with hardened inserts where repetitive shutoffs or wear areas exist. Packaging and consumer goods producers often balance cycle time, cavity count, and mold life, making cooling design and wear-resistant gate inserts critical.
Projects serving coastal regions, humid warehouses, and international shipping routes also benefit from corrosion planning. A mold stored near ports such as Shanghai, Hong Kong, Rotterdam, Hamburg, Los Angeles, Singapore, Dubai, or Santos can face environmental exposure if preservation is inadequate. Mold steel selection should be paired with anti-rust treatment, sealed packing, desiccants, and documented storage procedures.
Consumer electronics enclosure: A company launching a PC-ABS handheld device housing requires 20,000 pieces with a textured external surface and internal snap-fit features. P20 may be suitable for the mold base, while 718H can be selected for visible cavity surfaces if cosmetic requirements are stricter. H13 may be used locally for thin shutoffs and high-wear latch features. This approach controls cost while protecting critical areas.
Medical diagnostic device cover: A medical equipment developer needs clean white plastic covers and transparent inspection windows. The opaque housing may use 718H or P20 depending on volume, while transparent window tooling should use S136 to support high polish and reduce corrosion risk. The project should include validation samples, dimensional inspection, documented resin selection, and mold-cleaning guidance.
Glass-filled nylon automotive clip: An automotive supplier requires a clip that will run in a 150,000-piece program using glass-filled PA66. Standard P20 cavity surfaces may wear too quickly around gates, shutoffs, and thin locking features. H13 inserts, appropriate hardness, and planned spare components improve durability and reduce long-term maintenance costs.
PVC electrical fitting: A manufacturer needs molded PVC conduit fittings for export distribution. Because PVC processing can generate corrosive by-products, S136 or another suitable stainless steel should be used in cavity and core areas. The supplier should also specify regular mold cleaning, protective storage, and corrosion-control procedures.
The following companies are established mold steel suppliers with products used across international tooling markets. Buyers should verify the exact grade, local stock availability, certification package, and equivalent specification for each project. The best source may depend on steel availability near the selected tool shop, transportation time, and required technical support.
CompanyPrimary BaseService RegionsCore StrengthsKey OfferingsBest FitUddeholmHagfors, SwedenEurope, North America, Asia-Pacific, global distributionPremium tool steel development, clean steel technology, technical supportStavax ESR, Orvar Supreme, pre-hardened and stainless mold steelsHigh-polish, medical, automotive, and demanding production moldsASSABSingaporeAsia-Pacific, China, Europe, Americas through global networkTool steel supply, machining support, local stock programs718HH, P20 variants, Stavax ESR, Orvar SupremeRegional Asian tooling programs and internationally standardized projectsDaido SteelNagoya, JapanJapan, Asia, Europe, North AmericaSpecialty steels, pre-hardened grades, consistent material qualityNAK80, DC53, tool steels for molds and precision manufacturingHigh-polish consumer products and precision mold applicationsBÖHLER EdelstahlKapfenberg, AustriaEurope, Americas, Asia-Pacific, global sales networkSpecial steels, stainless grades, technical metallurgy expertiseM340, W302, corrosion-resistant and hot-work tool steelsMedical, optical, high-temperature, and corrosion-sensitive moldingFinkl SteelChicago, United StatesNorth America and international industrial customersLarge blocks, mold base steel, domestic supply capabilityPre-hardened mold steels, mold plates, specialty steel productsNorth American mold builders and large mold base requirementsMeusburgerWolfurt, AustriaEurope and global mold-making customersStandard mold bases, precision plates, mold componentsMachined plates, standard frames, guide elements, accessoriesToolmakers needing standardized components and fast configurabilityHitachi Metals / ProterialTokyo, JapanJapan and international industrial marketsSpecialty alloy expertise and high-performance material developmentTool steels and specialty materials through regional channelsProjects requiring specific Japanese material standards or equivalentsThese suppliers provide valuable options, but steel brand alone does not guarantee mold quality. The mold maker’s CNC machining, EDM, polishing, heat treatment, fitting, cooling design, assembly, mold trial process, and inspection discipline determine whether the selected steel performs as expected. Buyers should evaluate the complete tooling process, not only the steel certificate.
TEAM Rapid supports Global market customers with rapid tooling, plastic mold making, injection molding, CNC machining, finishing, assembly, and direct shipping from an integrated China-based manufacturing network. With more than 10 years of manufacturing experience, ISO 9001:2015 quality management certification, more than 6,000 delivered projects, and customers in over 25 countries, the company applies DFM analysis before tooling to identify risks involving resin flow, wall thickness, draft, cavities, cooling, cycle time, and material choice. For mold steel selection, TEAM Rapid can recommend practical combinations such as P20 for cost-efficient rapid tooling, H13 inserts for wear-sensitive areas, and S136 for corrosion-resistant or polished cavities, supported by controlled machining, EDM, polishing, inspection, and trial molding. The company serves end users, product designers, distributors, dealers, brand owners, startups, and established manufacturers through flexible OEM, ODM, low-volume, recurring production, wholesale, and regional supply cooperation models. Its operational model is turnkey manufacturing and customer-owned tooling support rather than BOO or on-site bulk supply services. Although TEAM Rapid does not claim overseas subsidiaries or local warehouses in every Global market location, it has established international service experience through one-to-one engineering communication, fast quotation responses, integrated production resources, packaging, limited warehousing, and direct shipment to customers in markets including the USA, UK, France, Germany, and other regions. This combination gives buyers practical pre-sale engineering support, production updates, inspection-based quality control, and after-sales coordination without managing multiple disconnected suppliers.
Customers needing a faster transition from prototype validation to low-volume or production molding can review rapid tooling services for international product development to understand available tooling pathways. For a steel recommendation based on resin, part geometry, annual volume, and surface requirement, buyers can request a custom injection mold tooling quotation with 3D files and material details.
By 2026, mold steel selection is expected to become more data-driven. Toolmakers are increasingly combining mold-flow simulation, cycle-time analysis, sensor data, predictive maintenance, and production traceability to determine where premium steel provides measurable value. Rather than building an entire tool from one grade, more projects will use hybrid construction: economical mold bases combined with higher-performance inserts in gates, cores, slides, shutoffs, and corrosive-resin zones.
Sustainability will also influence tooling decisions. Longer-lasting molds reduce replacement steel consumption, machine downtime, material waste, and emergency logistics. Better cooling performance can shorten cycle time and reduce energy use per molded part. Manufacturers are also expected to place greater emphasis on repairable insert designs, reusable mold bases, optimized cavity counts, and modular tooling systems that extend the useful life of production assets.
Global policy and customer requirements are likely to increase demand for material traceability, recycled-content documentation, product quality records, and controlled chemical processing. Medical, automotive, electrical, and consumer brands may require more detailed evidence of resin compatibility, steel origin, inspection methods, and controlled production practices. For this reason, mold steel certificates, hardness reports, maintenance records, and trial documentation will remain essential purchasing documents.
Provide the following information when requesting a quotation or technical review: 3D CAD files, 2D drawings if available, resin brand and grade, filler percentage, flame-retardant requirement, annual production volume, total lifetime volume, required surface finish, color, cosmetic standards, mold location, target production date, and expected maintenance arrangements.
Also identify whether the tool is intended for prototype validation, bridge production, low-volume commercialization, or long-term production. This distinction helps prevent two common errors: paying for production-grade steel when rapid tooling is sufficient, or selecting low-cost steel for a tool that must run high volumes with abrasive resin.
P20 is suitable for many injection molds, especially rapid tooling, low-volume production, consumer housings, trays, covers, and general-purpose plastic parts. It is not always sufficient for corrosive resins, highly abrasive glass-filled materials, high-temperature molding, or very long production programs.
Choose H13 when the mold will process high-temperature or glass-filled resins, when thermal fatigue is a concern, or when critical inserts need improved wear resistance and toughness. H13 is often used selectively in gates, cores, slides, and shutoff areas instead of across the full mold.
S136 is a stainless mold steel with stronger corrosion resistance and high-polish capability. Its cost reflects the material properties, machining demands, heat-treatment requirements, and value in applications such as PVC molding, medical parts, transparent components, and humid production environments.
Yes. Many efficient molds use P20 for the mold base, H13 for high-wear inserts, and S136 for corrosion-sensitive or high-polish cavity areas. This mixed-steel strategy can improve performance while controlling tooling cost.
Steel grade can affect cooling efficiency and long-term cavity stability, but cooling channel design, water flow, mold temperature control, wall thickness, and resin processing conditions usually have a greater direct effect on cycle time. Steel should be selected together with thermal design.
Request material certificates, steel grade confirmation, hardness reports, heat-treatment records when applicable, mold drawings, DFM feedback, trial reports, inspection reports, and maintenance recommendations. These documents help protect quality during production and future mold transfers.
Yes. Established Chinese mold manufacturers can source and machine P20, H13, S136, 718H, NAK80, and equivalent grades. Buyers should verify material traceability, machining capability, heat-treatment controls, inspection procedures, communication quality, and after-sales support before selecting a supplier.
-
Injection Mold Life in the Global Market: What to Expect
Injection mold life is the number of molding cycles a tool can complete while producing parts within agreed dimensional, cosmetic, and functional requirements. In the global market, a well-designed and properly maintained mold may produce anything from a few thousand prototype parts to several million production parts. The correct expectation depends on the mold material, resin, part geometry, tooling quality, maintenance plan, production conditions, and required surface finish.
Most aluminum injection molds provide approximately 5,000 to 100,000 cycles, while production molds made from suitable pre-hardened or hardened tool steel commonly deliver 100,000 to more than 1,000,000 cycles. High-volume molds using hardened steel, replaceable wear components, balanced cooling, and disciplined maintenance can exceed several million cycles.
For prototypes and market testing, a short-run mold may be the most economical option. For recurring commercial production, steel selection, cavity design, cooling efficiency, ejection loads, resin abrasiveness, and preventive maintenance have a greater effect on total cost than the original mold price alone. A mold that costs more initially can produce a lower cost per part over its useful life.
When comparing suppliers in the global market, consider qualified international manufacturers, including experienced Chinese companies, when they provide relevant certifications, documented inspection, clear engineering communication, and strong pre-sales and after-sales support. Their cost-performance advantages can be significant without requiring a compromise in tooling control.
For a practical decision, identify the expected lifetime volume, annual production, resin type, dimensional tolerance, cosmetic requirements, and planned product life before requesting a quotation. A professional toolmaker should then recommend the appropriate mold base, steel grade, surface treatment, cavity count, cooling arrangement, and maintenance interval.
Tool life should not be confused with the number of times a mold can physically close. A mold may continue operating after its expected cycle count, but the resulting parts may show flash, dimensional drift, short shots, sink marks, scratches, poor texture transfer, or inconsistent ejection. The useful life of an injection mold ends when it can no longer produce acceptable parts economically and repeatably.
Manufacturers usually describe mold life in cycles. One cycle includes mold closing, injection, packing, cooling, mold opening, and part ejection. In a four-cavity mold, one cycle produces four parts, so the part output is four times the number of completed cycles, excluding rejects. This distinction is important when estimating capacity and return on tooling investment.
Several life definitions may appear in a tooling quotation:
A reliable quotation should state what is included in the life estimate. The same steel can deliver very different results when used with different resins, injection pressures, cycle times, mold temperatures, or maintenance practices.
Tooling material is one of the most visible factors affecting service life, but it is not the only one. Aluminum can be highly effective for low-volume production because it machines quickly and transfers heat efficiently. Hardened tool steel generally costs more and takes longer to manufacture, but it provides greater resistance to wear, corrosion, deformation, and repeated thermal cycling.
Typical mold life ranges by tooling materialTooling materialTypical cycle rangeCommon applicationMain advantageMain limitationRecommended production profilePrototype aluminum5,000–20,000 cyclesDesign validation and pilot runsFast machining and low initial costLower wear resistancePrototype and short-run productionProduction aluminum20,000–100,000 cyclesLow-volume commercial partsEfficient cooling and rapid deliveryMay wear under abrasive resinRecurring low-volume ordersPre-hardened P20 steel100,000–500,000 cyclesGeneral production toolingBalanced cost, machinability, and strengthLess wear resistance than hardened steelMedium-volume production420 or 2083 stainless steel200,000–1,000,000 cyclesMedical, optical, and corrosive-resin partsCorrosion resistance and good polishabilityHigher material and machining costClean environments and demanding finishesH13 or 1.2344 hardened steel500,000–2,000,000 cyclesHigh-volume technical componentsStrong wear and thermal-fatigue resistanceMore difficult and expensive to machineLong production programsS136 or equivalent hardened stainless steel500,000–2,000,000 cyclesHigh-polish and corrosive applicationsExcellent finish and corrosion performanceRequires controlled heat treatment and polishingCosmetic and precision partsCarburized or specialty tool steel1,000,000+ cyclesAutomotive and high-volume consumer productsVery high wear resistanceHighest tooling investmentLarge-volume and long-life programsThese ranges are planning estimates rather than universal guarantees. A mold with a simple geometry, moderate pressure, non-abrasive resin, and robust cooling can exceed the lower end of its expected range. A complex mold with thin walls, multiple slides, high glass-fiber content, aggressive surface texture, or frequent color changes may require repair much earlier.
Steel quality affects hardness, toughness, polishability, corrosion resistance, and dimensional stability. A mold that is too soft may wear rapidly around gates, shutoffs, slides, and parting lines. A mold that is excessively hard but poorly heat-treated may become brittle and crack under impact or thermal stress. The correct balance depends on the resin, mold design, cavity pressure, surface finish, and maintenance environment.
Unfilled polypropylene and polyethylene are usually less abrasive than glass-filled nylon, mineral-filled polycarbonate, flame-retardant compounds, or long-glass-fiber engineering plastics. Glass fibers and mineral fillers can erode gates, runners, cores, cavities, and ejector components. Corrosive additives can attack mold surfaces, particularly when the tool is not dried and protected after production.
Deep ribs, narrow cores, thin walls, undercuts, lifters, collapsible cores, and side actions increase mechanical and thermal loads. Sharp internal corners concentrate stress. Thin shutoffs can deform or chip. Small venting features can become blocked, causing gas burns and higher injection pressure. A design that is optimized for molding generally produces a longer-lived tool than one that forces the mold to compensate for difficult geometry.
Uneven cooling causes warpage, extended cycle times, thermal stress, and inconsistent shrinkage. Poorly positioned cooling channels can leave hot spots near thick sections or core pins. Over time, repeated thermal cycling can contribute to cracking, corrosion, and dimensional movement. Conformal cooling, baffles, bubblers, and carefully balanced conventional channels can improve productivity and reduce stress when applied appropriately.
Excessive pressure increases stress on parting lines, slides, inserts, sprue bushings, and mold bases. Insufficient venting often causes operators to raise pressure, which can accelerate wear and flash. Correct filling analysis, gate selection, vent design, and process validation reduce the need to run the machine at unnecessarily aggressive settings.
Preventive maintenance is one of the most cost-effective ways to extend tool life. Cleaning, lubrication, inspection of guide components, checking cooling channels, sharpening or replacing damaged components, and protecting polished surfaces can prevent small defects from becoming major repairs. A mold used every week requires a different maintenance frequency from a tool stored for months between production campaigns.
Incorrect mold opening speed, excessive ejector force, poor purging, improper clamping, and foreign particles on the parting line can damage a tool quickly. Stable process parameters reduce thermal and mechanical shocks. Operators should also follow documented procedures for mold installation, water connection, startup, shutdown, cleaning, and storage.
Different product categories place different demands on an injection mold. A simple tray may require only a two-plate mold with a basic edge gate. A medical housing may need stainless steel, mirror polishing, controlled venting, validated dimensional inspection, and strict contamination controls. A large automotive panel may require multiple hot runners, complex slides, high clamping force, and careful thermal balancing.
The product’s commercial life should guide the tooling strategy. If a product is expected to sell for three months, investing in a two-million-cycle mold may not be economical. If the product supports a ten-year aftermarket program, a low-cost prototype mold can create severe supply and quality risks later.
Start with the expected lifetime quantity, then add a practical allowance for rejects, engineering samples, maintenance trials, and future demand. The basic calculation is:
Required cycles = lifetime parts ÷ number of cavities ÷ expected utilization rate
For example, a four-cavity mold intended to produce 800,000 saleable parts with an estimated 92 percent utilization rate would need approximately 217,400 cycles. A P20 steel mold could be suitable in some conditions, but a corrosion-resistant or hardened insert may be more appropriate if the resin is abrasive or the product must remain in production for many years.
Also consider:
Ask the toolmaker to separate the expected life of the mold base, cavities, cores, slides, hot-runner system, cooling fittings, ejector system, and replaceable wear parts. These components rarely have identical service lives.
The global supply market includes specialist mold makers, digital manufacturing platforms, component suppliers, and integrated manufacturing partners. The best choice depends on whether the project requires rapid tooling, high-volume automotive molds, medical tooling, local production support, or a complete transition from prototype to finished parts.
Selected injection mold suppliers and their practical strengthsCompanyService regionsCore strengthsKey offeringsBest fitBuying considerationTEAM RapidChina, North America, Europe, Asia, and international export marketsFast engineering support, integrated tooling, and flexible productionRapid tooling, injection molding, CNC machining, 3D printing, finishing, assembly, and packagingPrototype-to-production programs from one part to 100,000+ partsRequest a DFM review and confirm steel, cycle target, inspection, and maintenance scopeProtolabsNorth America, Europe, and JapanDigital quoting, rapid manufacturing, and standardized workflowsInjection molding, CNC machining, 3D printing, and design analysisFast product development and repeatable low-volume ordersCheck material, texture, tolerance, and mold ownership termsXcentric Mold & EngineeringUnited States and international customersRapid injection molding and engineering-led toolingProduction injection molding, rapid tooling, CNC machining, and finishingU.S.-based development programs and bridge productionConfirm expected cycle life and production location before approvalFictivUnited States and international supply networksDigital sourcing, supplier coordination, and project visibilityInjection molding, CNC machining, sheet metal, and additive manufacturingCompanies needing managed multi-process sourcingClarify the assigned manufacturing partner and quality documentationStackTeckCanada, United States, Europe, and global automotive marketsHigh-cavitation and complex production toolingAutomotive molds, thin-wall packaging tools, hot-runner integration, and automationHigh-volume and technically complex programsBest suited to substantial production volumes and formal engineering reviewsTooling Tech GroupUnited States, Europe, and global automotive supply chainsLarge molds, automotive tooling, and program managementInjection molds, compression molds, tooling systems, and production supportAutomotive and industrial programs requiring large-scale toolingReview project timing, maintenance responsibility, and spare-component strategyRosti GroupEurope, Asia, and North AmericaIntegrated plastic manufacturing and contract productionTooling, injection molding, assembly, and supply-chain servicesBrand owners seeking regional manufacturing supportCompare plant location, resin approval, production capacity, and logistics costSupplier location should not be judged only by distance. A nearby supplier may offer convenient communication but higher tooling cost or limited process coverage. An international supplier may offer stronger price performance and broader capacity, provided it supplies traceable materials, inspection records, mold trials, spare-part plans, and responsive technical support.
Design for manufacturability analysis should identify uniform wall thickness, draft angles, parting-line options, gate location, venting, ejection, undercuts, cooling, shrinkage, and likely cosmetic risks. This review is especially valuable before steel is cut because many tool-life problems begin with a design that creates excessive pressure, difficult ejection, or fragile shutoffs.
Do not accept an undefined description such as “premium steel.” Request the actual grade, hardness range, heat-treatment method, corrosion protection, and location of hardened inserts. For a high-volume tool, ask whether the steel certificate and hardness report will be provided with the final documentation.
The contract should state who owns the mold, where it will be stored, whether it can be transferred, and who pays for refurbishment. If production may move from Asia to Europe or North America, the tool should be designed for transport, reinstallation, spare-part availability, and local machine compatibility.
Acceptance should cover first-shot samples, dimensional reports, appearance, cycle time, cavity balance, part weight, mold operation, and the quantity of approved samples. A mold can appear complete while still requiring major work on flash, filling balance, ejector marks, or cooling performance.
Critical spares may include ejector pins, return pins, springs, cavity inserts, core inserts, slide wear plates, seals, nozzles, gate components, and hot-runner heaters. Keeping these items available can reduce downtime and protect the production schedule.
Ask for a preventive maintenance schedule based on cycles, not only calendar time. The plan should identify daily, weekly, monthly, and annual checks. For abrasive or corrosive materials, inspection intervals should be shorter and wear components should be monitored more closely.
Good maintenance is a controlled production activity rather than an emergency repair response. After each run, remove resin residue, clean the parting line, dry water circuits when appropriate, protect polished surfaces, and record any abnormal noise, ejection resistance, flash, or dimensional shift. Never close and store a wet mold without corrosion protection.
Recommended maintenance actions for injection moldsMaintenance areaActionSuggested timingRisk reducedResponsible roleRecord to retainParting lineRemove flash, resin, dust, and foreign particlesEvery production runFlash and shutoff damageMachine operatorCleaning checklistEjector systemInspect pins, sleeves, return movement, and lubricationEvery run or defined cycle intervalSticking, bending, and pin breakageTooling technicianCycle-based service logCooling circuitsCheck flow, leaks, scale, fittings, and water qualityWeekly to monthlyHot spots, corrosion, and long cyclesProcess technicianFlow and temperature recordSlides and liftersInspect wear plates, lubrication, alignment, and movementDefined cycle intervalGalling, flash, and misalignmentTooling technicianInspection reportVentsClean and restore blocked vent featuresAs needed and during preventive serviceBurn marks, short shots, and high pressureMold technicianRepair historyPolished and textured surfacesClean with approved materials and protect from impactEvery runScratches, stains, and texture variationOperator and technicianCosmetic approval recordStorage protectionApply rust preventive, seal ports, and control storage conditionsBefore storageCorrosion and contaminationTooling departmentStorage release formWhen mold repairs are necessary, identify the underlying cause. Replacing a worn ejector pin without correcting excessive ejection force or insufficient draft may only postpone another failure. Similarly, polishing flash from a parting line without checking alignment can reduce shutoff thickness and shorten the remaining mold life.
Injection molds support products across automotive, medical, consumer, industrial, electrical, telecommunications, sanitary, and office-equipment sectors. The required mold life varies by industry because production volumes, regulatory requirements, product liability, and appearance standards are different.
Applications are not limited to finished plastic parts. Injection molding is also used for insert molding, overmolding, two-shot components, elastomer integration, and assemblies that combine metal and plastic. These processes may increase the number of loading operations and require additional mold alignment features.
A startup developing a handheld electronic product may need 5,000 to 15,000 parts for fit testing, user trials, and early sales. A machined aluminum mold can reduce lead time and make design revisions affordable. If the enclosure design is not yet frozen, investing in a hardened production mold may create unnecessary sunk cost. The mold should still include appropriate draft, venting, replaceable inserts, and a documented repair path.
An industrial equipment manufacturer may require 250,000 parts over several years. A P20 or equivalent pre-hardened steel mold may be suitable when the resin is not highly abrasive and the part geometry is moderate. Hardened inserts should be considered around gates, shutoffs, slides, and high-wear areas. Cycle records and periodic dimensional checks can confirm whether the tool is aging normally.
An automotive supplier may need several million components over the vehicle program and replacement-parts period. The tool may require hardened steel, hot-runner balancing, robust slides, automated handling, replaceable wear plates, and a formal maintenance schedule. The lowest initial quotation is rarely the lowest total-cost option in this situation.
A medical device housing may require stainless steel for corrosion resistance, high polish, controlled molding conditions, and detailed inspection records. Even when the lifetime volume is moderate, the required quality level may justify a more durable tool. Surface condition, cleanliness, traceability, and process validation can be more important than maximum cycle count.
TEAM Rapid combines rapid tooling, injection molding, CNC machining, 3D printing, finishing, assembly, packaging, and shipping support through an integrated manufacturing network in China. Its ISO 9001:2015 quality system, more than ten years of manufacturing experience, work for customers in over 25 countries, more than 500 satisfied customers, and record of over 6,000 delivered projects provide useful evidence for international tooling programs. The company uses DFM reports and manufacturability analysis to identify risks before steel cutting, including parting-line problems, difficult ejection, inefficient cooling, excessive resin use, and cycle-time opportunities. Customers can use flexible OEM and ODM-style cooperation for prototypes, low-volume production, recurring orders, or larger programs, while end users, distributors, dealers, brand owners, and individual product developers can request project-specific sourcing and production arrangements rather than a fixed one-size-fits-all package. Its capabilities cover projects from one prototype to more than 100,000 parts, with rapid tooling and molded parts commonly supported in approximately 5 to 25 days depending on requirements. TEAM Rapid does not present itself as a BOO or on-site bulk-supply operator; it provides EPC/Turnkey and customer-owned plant support models when required, including tooling, process coordination, procurement, assembly, packaging, limited warehousing, and direct shipping. The profile does not claim overseas subsidiaries or permanent local warehouses, so buyers should confirm regional stock and service arrangements for each project; however, the company supports international customers through responsive online engineering communication, pre-sales DFM review, inspection documentation, after-sales technical coordination, and experience working across Asian and Western business cultures. This combination makes it a practical option for customers comparing Chinese manufacturing against suppliers in the United States, Canada, Europe, or other global production hubs.
For tooling evaluation, customers can review TEAM Rapid’s rapid tooling services for global projects and submit technical files through the international manufacturing quotation page. A useful request should include the 3D model, 2D drawings, resin grade, expected volume, surface finish, tolerance, target cycle life, delivery location, and whether the mold will be customer-owned and transferred later.
Tooling cost should be measured against total cost per acceptable part, not only the purchase price. A low-cost aluminum mold may be ideal for a short product launch, while a hardened steel mold may be more economical for sustained demand. The calculation should include mold price, maintenance, repairs, downtime, scrap, machine time, part price, logistics, and the cost of replacing a failed tool.
Cavity count also affects economics. A single-cavity mold has a lower initial cost and is easier to modify, but it requires more cycles to meet the same volume. A multi-cavity mold increases upfront investment and requires careful cavity balancing, but it can lower machine time and part cost. The right choice depends on demand certainty, available machine capacity, part size, quality requirements, and expected product life.
Hot runners may reduce runner waste and improve cycle efficiency, but they add components that need maintenance and may be more expensive to repair. Cold runners can be simpler and more economical for some applications. The decision should be based on resin value, cavity count, part geometry, color changes, cycle targets, and service capability.
Several developments are shaping tooling decisions in 2026 and beyond.
Sustainability does not always mean choosing the cheapest or lightest mold. A durable tool that avoids repeated replacement, produces less scrap, and supports efficient cycle times can have a lower environmental impact over the complete product life.
An aluminum mold commonly lasts from approximately 5,000 to 100,000 cycles. The actual result depends on the aluminum grade, part complexity, resin abrasiveness, injection pressure, cooling design, and maintenance. Aluminum is often suitable for prototypes and low-volume production rather than very large lifetime quantities.
Yes. A properly designed and maintained steel mold can reach one million cycles or more. Hardened steel, suitable wear inserts, stable processing, effective cooling, and disciplined maintenance are usually required, especially for abrasive engineering resins or complex mechanisms.
Glass-filled nylon can reduce mold life because the fibers are abrasive. Gates, runners, cavities, cores, slides, and ejector components may wear faster. Hardened inserts, abrasion-resistant treatments, robust gate design, and shorter inspection intervals can reduce the impact.
Toolmakers normally measure life in cycles, but buyers should convert cycles into parts using the cavity count. A four-cavity mold producing 250,000 cycles can theoretically make one million parts before considering rejects, downtime, and maintenance.
There is no single task for every mold. Cleaning the parting line, lubricating moving components correctly, monitoring cooling circuits, inspecting ejection, and protecting the mold during storage are all essential. The maintenance plan should reflect resin type, production frequency, and mold complexity.
Choose aluminum when the design is still changing or the expected volume is limited. Choose steel when demand is substantial, the product will remain active for years, the resin is abrasive, or dimensional and cosmetic consistency are critical. A DFM and volume review can prevent over- or under-specifying the tool.
Often, yes. Inserts, slides, ejector components, guide systems, and hot-runner parts can be repaired or replaced. However, repair economics depend on the remaining condition of the mold base, cavity alignment, part design, steel availability, and the cost of downtime.
Compare the complete offer rather than the mold price alone. Review engineering support, steel documentation, trial samples, inspection capability, guaranteed life, spare parts, maintenance, shipping, communication, ownership terms, and after-sales response. A qualified international supplier with transparent controls may provide stronger value than a nearby supplier with limited technical scope.
Provide the 3D model, 2D drawings, resin and color, annual and lifetime volume, cavity preference, tolerance, surface finish, target cycle time, machine information, delivery destination, and required certifications. Also state whether you need only the mold or a turnkey package including molded parts, assembly, packaging, and shipping.
Injection mold life is best treated as a design and supply-chain decision rather than a simple steel specification. A short-run aluminum mold can be the most efficient choice for a new product, while a hardened steel tool with replaceable wear components is more appropriate for high-volume or long-term programs. The strongest results come from combining accurate demand planning, DFM analysis, suitable materials, balanced cooling, stable processing, preventive maintenance, and clear ownership terms.
For global buyers, evaluate both local and international suppliers. Review proven project experience, quality systems, engineering response, inspection records, production capacity, logistics support, and long-term maintenance capability. With the right specifications and an evidence-based life estimate, businesses can reduce downtime, control cost per part, and keep injection molding reliable throughout the product’s commercial life.
-
Family Tooling vs Multi-Impression Molds: Global 2026 Guide
Family tooling is usually the better choice when several different plastic parts are needed in similar quantities for a low-volume assembly, pilot launch, market test, or bridge-production program. A multi-impression mold is generally the stronger choice when one identical part is needed at higher volume, because it delivers better cycle efficiency, lower unit cost, more consistent balancing, and simpler quality control.
For global buyers, the decision should not be based on mold price alone. Select family tooling when part demand is balanced, design changes are still likely, and reduced upfront investment matters more than the lowest possible piece price. Select a multi-impression mold when demand for one component is stable, annual volume can absorb tooling investment, and the part must run efficiently across long production campaigns.
Global buyers can also consider qualified international suppliers, including Chinese manufacturers with ISO-certified quality systems, responsive pre-sales engineering, and practical after-sales support. Their cost-performance advantage can be especially valuable for rapid tooling, low-volume molding, and programs that need fast design iteration before committing to hardened production tooling.
A family mold contains cavities for two or more different parts in one mold base. The parts may belong to the same product assembly, such as a housing, cover, latch, bezel, button frame, or internal support. Every molding cycle produces one or more of each different component. This arrangement can reduce initial tooling expenditure because the customer purchases one mold system rather than several independent molds.
A multi-impression mold, also called a multi-cavity mold, contains multiple cavities for the same part. For example, an eight-cavity mold makes eight identical clips every cycle. Its purpose is output efficiency: the manufacturer spreads press time, operator labor, material handling, and machine setup across more pieces. Properly designed multi-cavity tools can support highly repeatable production for consumer products, automotive subcomponents, medical-device housings, electrical connectors, packaging parts, and industrial assemblies.
The central distinction is output mix. Family tooling produces a group of different components. Multi-impression tooling produces multiple copies of one component. That difference affects mold flow, runner design, cooling, filling pressure, visual consistency, production planning, maintenance, and the financial break-even point.
Core Comparison of Family Tooling and Multi-Impression ToolingDecision FactorFamily ToolingMulti-Impression ToolingBuyer ImpactParts produced per cycleDifferent parts within one assembly familyIdentical copies of one partDefines whether output matches assembly demand or single-part demandInitial tooling costOften lower than buying separate molds for every componentHigher as cavity count, hot runner complexity, and cooling increaseFamily tools can reduce launch capital for balanced setsUnit-cost potentialModerate; limited by the slowest or most difficult cavityStrong at stable volume because many identical parts run togetherMulti-impression tools usually win at high annual volumeProcess balancingMore difficult when parts vary in size, thickness, or flow lengthMore predictable because cavities are geometrically identicalHigher process risk may create scrap in family mold programsDesign changesChanges to one component can interrupt the full toolChanges affect one part design but may require updating every cavityEarly-stage products need careful change-control planningProduction flexibilityUseful when assembly components are consumed in equal quantitiesUseful when one high-demand part needs independent replenishmentService-parts demand can favor separate or multi-impression toolsQuality inspectionRequires cavity-specific checks across different part geometriesRequires cavity-to-cavity comparison of the same geometryInspection plans should be defined before trial productionThe table shows why neither option is universally cheaper. A family mold may save money at the beginning, but an unbalanced family tool can create cycle-time losses, uneven packing, warpage, flash, sink marks, or excessive rejection. A multi-impression tool may cost more to build, yet its economics become compelling when production is continuous and every cavity has a stable demand profile.
Global manufacturing programs increasingly require faster market entry, more regional customization, shorter product life cycles, and tighter inventory control. Product owners may develop in the United States, Europe, Japan, South Korea, India, Australia, or the Middle East while sourcing tooling and molded components through manufacturing hubs in Shenzhen, Dongguan, Ningbo, Suzhou, Shanghai, Ho Chi Minh City, Penang, Monterrey, Prague, Istanbul, and Detroit.
In this environment, mold selection is a supply-chain decision as much as an engineering decision. A family mold can reduce the number of tools shipped between factories and simplify initial component sourcing for a product launch. However, it may also lock multiple parts into one production schedule. If one part sells faster, changes frequently, or requires a different material, the shared tool can become a bottleneck.
Multi-impression molds align well with focused production cells, automated packaging, high-throughput assembly, and global replenishment programs. They are particularly valuable when a component is sold separately as a replacement part or used across multiple product models. High-volume molds are often paired with automation, vision inspection, cavity monitoring, robotic pick-and-place systems, hot runners, and statistical process control.
For shipments moving through major trade hubs such as Shanghai Port, Shenzhen’s Yantian Port, Ningbo-Zhoushan Port, Rotterdam, Hamburg, Los Angeles, Long Beach, Jebel Ali, Singapore, and Felixstowe, compact and predictable tooling programs help reduce launch uncertainty. Yet freight efficiency should never override manufacturability. A lower-cost mold that creates high scrap or delivery delays can cost more than a properly engineered tool.
Family and multi-impression mold designs are not limited to one construction method. Both can use cold runners, hot runners, interchangeable inserts, side actions, unscrewing mechanisms, insert molding features, overmolding arrangements, automated handling, and hardened steel or aluminum tooling solutions. The best configuration depends on part geometry, resin, volume, surface requirements, expected tool life, and whether the program is still evolving.
Tooling Configurations for Different Production ConditionsConfigurationTypical StructureBest FitMain LimitationSingle-cavity moldOne cavity for one partPrototypes, large parts, low volume, critical validationHighest piece cost at larger demandFamily moldMultiple different cavities in one moldBalanced assembly sets and bridge productionFlow and demand imbalance can create wasteMulti-impression cold-runner moldMultiple identical cavities with runner systemModerate-volume commodity or functional partsRunner scrap and secondary separation may be requiredMulti-impression hot-runner moldMultiple identical cavities with heated manifoldHigher-volume parts and resin-sensitive productionGreater upfront investment and maintenance complexityInterchangeable-insert moldShared base with replaceable cavity or core insertsProduct variants, revisions, and controlled market testingNot always ideal for maximum-cycle productionStack moldTwo or more molding faces operating togetherHigh-volume, smaller components with press constraintsComplex design, maintenance, and machine requirementsInsert or overmolding toolPlastic molded around metal or preformed substrateElectrical, medical, grip, sealing, and structural partsInsert placement and thermal control require validationFor many global startups and product-development teams, rapid aluminum tooling or pre-hardened steel tooling offers a sensible bridge. It enables functional molded parts before the demand forecast is proven. After market validation, the company can decide whether to add cavities, create dedicated tools, convert to hot-runner production, or move to hardened steel tooling for long-term output.
Family molds are frequently described as inexpensive because one mold base can hold multiple part cavities. This can be true when components share the same resin, color, production quantity, wall-thickness range, and process window. If those conditions are not present, apparent savings may disappear. A large thick-walled cavity may need a long cooling cycle, forcing a small thin-walled component to wait unnecessarily. If one cavity fills sooner than another, packing pressure can over-pack one part while under-packing another.
Multi-impression molds require more machining, polishing, cooling circuits, cavity matching, and validation. A four-cavity or eight-cavity tool must ensure that every cavity fills, packs, cools, ejects, and measures consistently. However, once validated, the mold can substantially lower conversion cost per piece. The financial case improves with higher production volume, stable demand, predictable material pricing, and long production runs.
Buyers should request an itemized cost model that separates mold-base cost, cavity inserts, hot-runner systems, steel grade, surface finish, texturing, side actions, trial shots, gauges, inspection, packaging, logistics, and expected maintenance. This comparison prevents a low initial quote from hiding future production expenses.
Cost and Risk Factors Buyers Should Evaluate Before Tool ReleaseCost or Risk ItemFamily Tooling ConsiderationMulti-Impression Tooling ConsiderationRecommended Buyer ActionTool constructionOne base may reduce initial tooling countMore cavities increase machining and matching workCompare total tooling investment over the product life cycleCycle timeSet by the slowest cooling or ejection requirementOptimized around one part geometryAsk for estimated cycle time and production capacityMaterial scrapCan rise if process balance is poorCold runners may create consistent runner scrapRequest resin-consumption assumptions and regrind policyDemand imbalanceOne slow-moving part can create excess inventoryProduction quantity can match the demand of one componentReview service-parts and regional demand forecastsMaintenanceRepairs can affect several different components at onceHigh cavity count requires preventive cavity maintenanceDefine spare inserts, maintenance intervals, and ownershipQuality containmentMultiple geometries need different inspection methodsCavity variation must be tracked and correctedRequire first-article samples and cavity identificationEngineering changesA change to one part may disrupt the full family setEvery identical cavity may need modificationUse insertable cavity design where revisions are likelyA practical break-even calculation compares tooling cost plus expected molding cost across projected demand. If a single-cavity tool produces a part at a higher unit cost but demand is uncertain, it may still be the cheaper business decision. If demand is reliable and high, a multi-impression mold often repays its added capital through lower machine time and more efficient labor use.
Start with the bill of materials rather than the mold category. Identify which parts are always consumed together, which parts may be sold separately, which require different colors or resins, and which have different forecast volumes. A family mold is only logical if production quantities stay closely matched. For example, a product requiring one front cover, one rear cover, and one battery door per unit may suit family tooling during launch. If the battery door is likely to be replaced often, customized across markets, or made in several colors, it may deserve a separate mold.
Request a DFM report before issuing a purchase order. A meaningful review should assess wall thickness, draft angle, rib-to-wall ratio, gate position, weld lines, sink risk, tolerance requirements, shrinkage, undercuts, ejection points, cooling access, texture, and resin flow. For technical materials such as glass-filled nylon, POM, PC/ABS, PPS, TPU, or flame-retardant grades, material behavior must be considered early because shrinkage and processing windows may make a mixed family tool impractical.
For low-volume global programs, buyers should also evaluate whether rapid tooling, CNC machining, vacuum casting, or additive manufacturing can reduce risk before production molding begins. Molding is not always the fastest answer for the first few units, especially when functional testing and customer feedback could still alter the geometry.
Family molds are common in products that launch as complete assemblies and require modest quantities of several plastic components. Multi-impression molds dominate programs where identical parts are consumed in large quantities, especially when automation and predictable replenishment are important. Both are used across global industrial supply chains, but their economic fit differs by application.
Industry Applications and Appropriate Tooling DirectionIndustryTypical ComponentsLikely Tooling ChoiceWhy It FitsConsumer electronicsCases, buttons, bezels, cable clips, battery coversFamily for pilot assemblies; multi-impression for repeat partsLaunch designs change quickly, while accessories may scale rapidlyAutomotiveClips, trim supports, vents, housings, sensor bracketsMulti-impression for high-run clips; family for low-run trim setsHigh repeatability and traceability are critical for common componentsMedical devicesInstrument housings, caps, trays, handles, fixturesDepends on validation plan and resin requirementsMaterial control, documentation, and dimensional consistency are essentialIndustrial equipmentControl enclosures, covers, knobs, protective guardsFamily tooling for balanced low-volume assembliesProduct variants and moderate annual demand are commonElectrical productsTerminal housings, switch components, cable-management partsMulti-impression toolingSmall identical parts often justify high-output productionSanitary and home productsHandles, caps, frames, fittings, dispenser partsFamily during development; dedicated cavities at scaleColor variants and replacement-part demand can change the economicsPackaging and retail goodsClosures, trays, dispensers, clips, protective insertsMulti-impression or stack moldsHigh volume rewards cavity count and automationMedical and automotive buyers should apply additional caution. A mold type does not itself establish regulatory compliance. Material traceability, validated process windows, dimensional control, documented inspection, packaging requirements, and customer-specific approval procedures remain necessary. The selected tool must support the required control plan rather than merely meet a price target.
A product team launching a handheld consumer device needs a front shell, rear shell, and button frame in equal quantities for an initial international release. The components use the same PC/ABS grade and have compatible molding temperatures. A family mold can be economical for a few thousand sets because every cycle produces a complete set for assembly. Before tool release, the team should verify that wall thickness, gate placement, cooling time, and shrinkage are compatible. If the button frame later becomes available in multiple colors, a separate insert or independent tool may be the better expansion path.
An automotive supplier requires the same nylon retainer clip for assembly plants in Europe, North America, and Asia. Demand is high and stable, with tens of thousands of pieces required each month. An eight-cavity or sixteen-cavity multi-impression mold is generally the better investment. Every cavity should be identified for inspection, and the supplier should monitor cavity-specific dimensions, gate vestige, flash, pull force, and material moisture control. This approach supports efficient export packing through ports such as Ningbo-Zhoushan, Rotterdam, and Long Beach.
An industrial equipment manufacturer needs a controller housing, cable cover, mounting foot, and protective cap. Initial sales volumes are moderate, but field replacement demand is unknown. A family mold could make complete launch kits economically, but the protective cap may wear or be lost more often than other components. The buyer may use a family tool for the main housing set and a dedicated multi-impression mold for the cap once replacement demand is confirmed. This hybrid approach reduces early capital exposure while preserving future supply flexibility.
Supplier selection should reflect the project’s tool life, resin, complexity, certification requirements, localization needs, production volume, and communication expectations. The following companies are established names with relevant manufacturing, tooling, prototyping, or injection molding capabilities. Buyers should confirm current regional availability, specific material qualifications, mold ownership terms, and project suitability directly during quotation.
Selected Global Suppliers for Injection Mold and Production ProgramsCompanyPrimary Service RegionsCore StrengthsKey OfferingsTEAM RapidGlobal customers, including North America, Europe, Asia, and other export marketsRapid tooling, DFM support, China-based cost efficiency, flexible productionInjection molding, rapid tooling, CNC machining, vacuum casting, assembly, packaging, direct shippingProtolabsNorth America and EuropeDigital manufacturing workflows and rapid production supportInjection molding, CNC machining, 3D printing, sheet metal fabricationXometryNorth America, Europe, and international sourcing networksBroad supplier network and online quotation capabilitiesInjection molding, machining, additive manufacturing, sheet metal servicesFictivUnited States and global manufacturing networkDigital manufacturing management and engineering-oriented sourcingInjection molding, CNC machining, urethane casting, 3D printingEVCO PlasticsUnited States and international customer programsCustom injection molding and large-scale manufacturing experienceTooling support, injection molding, assembly, packaging, engineering servicesRosti GroupEurope, Asia, and North AmericaMulti-site contract manufacturing and regulated-industry experienceInjection molding, product assembly, medical and consumer-product manufacturingICOMold by FathomNorth America and global customer baseOnline injection molding procurement and production supportCustom injection molding, tooling, prototype and production partsFor international sourcing, supplier qualification should include a review of DFM response time, sample process, first-article reporting, resin sourcing, cavity tracking, tool maintenance, export packaging, intellectual-property handling, project communication, and escalation procedures. A supplier’s willingness to challenge an unmanufacturable design is often more valuable than a fast quote that ignores foreseeable production risks.
TEAM Rapid supports global product developers, brand owners, distributors, dealers, end users, individual inventors, and industrial buyers through flexible OEM, ODM, wholesale, prototype, low-volume, and scalable production models rather than a one-size-fits-all mold program. Its ISO 9001:2015 quality management certification, DFM-based manufacturability reviews, in-house machining and tooling capability, molding resources, and tolerance capability down to 0.01 mm for applicable CNC work provide practical controls before a mold is built. The company works with diversified plastic and metal material options, offers tooling and molded-part production commonly within approximately 5 to 25 days depending on complexity, and has delivered more than 6,000 projects for over 500 customers in more than 25 countries. For global buyers, TEAM Rapid combines online quotation and engineering communication with direct project support, packaging, assembly, material management, procurement assistance, limited warehousing, and direct shipping; its established international customer experience supports coordinated pre-sale DFM feedback and after-sale project follow-up even where a local subsidiary or overseas warehouse is not stated. It provides customer-owned tooling and turnkey manufacturing pathways, including assembly and contract-packaging support, and does not operate BOO or on-site bulk-supply models. Buyers can review its rapid tooling services when comparing bridge tooling with production molds, then request a project-specific global manufacturing quotation for cavity layout, resin, quantity, finish, and lead-time analysis.
A clear RFQ improves the quality of family mold versus multi-impression mold recommendations. Provide 3D CAD files, 2D drawings where critical dimensions matter, annual volume forecasts, pilot quantity, resin specification, color, texture, cosmetic standards, expected product life, assembly requirements, target markets, packaging needs, and desired delivery point. If the product will enter regulated markets, include applicable customer requirements and validation expectations early.
Ask suppliers to state whether the quoted tool is aluminum, pre-hardened steel, or hardened steel; whether it uses cold or hot runners; whether it includes interchangeable inserts; what machine tonnage is anticipated; how many trial shots are included; and how mold maintenance will be managed. For a family tool, require a discussion of shot balance and projected inventory balance. For a multi-impression tool, require cavity-to-cavity process analysis and a defined plan for cavity identification.
In 2026, global mold programs will increasingly use simulation, connected process data, automated inspection, and modular tooling design. Mold-flow analysis is becoming more accessible earlier in product development, helping teams identify filling imbalance, weld lines, pressure peaks, cooling limitations, and potential warpage before expensive steel is cut. For family molds, this will make early feasibility decisions more evidence-based. For multi-impression molds, it will improve cavity balancing and cycle-time optimization.
Automation will also influence mold selection. High-volume multi-impression tools increasingly integrate robotics, in-mold sensors, vision systems, automated degating, cavity-specific quality tracking, and real-time process monitoring. These technologies can reduce labor dependency and make global production more traceable, but they require better tool design and a more disciplined validation plan.
Sustainability pressures are reshaping resin selection and mold design. Brand owners are evaluating recycled-content polymers, bio-based materials, lightweighting, lower-energy production, reusable packaging, and reduced runner waste. Hot-runner systems can reduce cold-runner scrap, although they add complexity and energy considerations. Family molds can reduce the number of mold bases required during early product development, but they should not be chosen if poor balance increases scrap. The most sustainable solution is usually the one that produces conforming parts efficiently, avoids excess inventory, and supports long tool life.
Policy and market conditions are also increasing the value of supply-chain resilience. Buyers are using dual sourcing, regional warehousing, clearer mold ownership contracts, origin documentation, and multi-region logistics planning. A tooling strategy should leave room for future expansion, whether that means adding cavities, transferring validated data, producing spare inserts, or qualifying a second production route.
No. A family mold can lower initial investment because it combines different parts in one base, but difficult flow balance, long cycle time, scrap, inventory imbalance, and future design changes can make it more expensive over time.
It becomes worthwhile when demand for one identical part is stable enough that lower unit cost and higher output recover the added cost of extra cavities, cooling, runner systems, and validation.
Standard family molding normally uses one material per shot. Parts needing different resins, significantly different processing temperatures, or different color requirements generally need separate tools, insert-molding steps, overmolding processes, or specialized solutions.
The biggest risk is process imbalance. Different cavity volumes, wall thicknesses, flow lengths, and cooling needs can cause uneven filling, inconsistent packing, warpage, sink, flash, or one component being overproduced relative to another.
Usually not if replacement demand differs from the main assembly demand. A separate multi-impression mold can prevent excess inventory of unrelated components and provide faster replenishment for the service part.
Provide 3D CAD, material, color, annual demand, target quantity, tolerances, finish requirements, expected tool life, target market, packaging needs, and any required inspection or regulatory documentation.
Yes. Rapid tooling is often a practical bridge for functional validation, pilot runs, low-volume sales, and early market feedback. It helps buyers confirm demand and design stability before investing in higher-cavity hardened production tooling.

-
Global Market Plastic Mold Engineering Review Before Build
A complete plastic mold engineering review should be finished before steel is cut. The review must confirm part geometry, resin choice, wall thickness, draft, shrinkage, gate location, runner design, cooling, ejection, tolerances, mold steel, expected production volume, inspection plan, and shipment requirements. The objective is to prevent costly tooling changes, unstable cycle times, visible defects, weak weld lines, warpage, flash, sink marks, and assembly failures after the mold is built.
For the Global Market, the most practical approach is to involve the mold maker, part designer, material supplier, quality team, and production team during DFM approval. Buyers should compare local tooling specialists with qualified international suppliers, including Chinese manufacturers that provide relevant certification, responsive pre-sales engineering support, reliable after-sales support, and strong cost-performance for prototype, low-volume, and repeat-production tools.
Before issuing a purchase order, request a written DFM report, mold-flow recommendation where appropriate, steel specification, cavity count proposal, estimated cycle time, sample validation plan, spare-part list, ownership terms, and post-delivery service scope.
Injection mold design is not only a tooling task. It is a commercial, engineering, quality, and supply-chain decision that affects the total cost of every molded part. A low-cost mold can become expensive when it creates excessive scrap, long cycle times, unplanned maintenance, cosmetic defects, poor dimensional stability, or delayed product launch. Conversely, a properly engineered mold can support predictable output, stable quality, lower resin consumption, reduced labor, and faster market entry.
Global product teams commonly design in one country, source tooling in another, mold parts near an assembly plant, and distribute finished products across several regions. This makes pre-build communication particularly important. Different markets may have different requirements for product labeling, material traceability, medical-device documentation, flame ratings, food-contact requirements, electrical safety, recycling content, packaging, and shipment protection. The design review should therefore translate the product requirements into mold requirements before manufacturing begins.
Trade hubs such as Shenzhen, Dongguan, Ningbo, Shanghai, Singapore, Rotterdam, Hamburg, Los Angeles, Chicago, Monterrey, Birmingham, Munich, and Dubai connect international manufacturing programs. Yet shipping distance does not eliminate the need for engineering alignment. A mold shipped from China to Europe, North America, Southeast Asia, or the Middle East must match the selected molding machine, local resin supply, water connections, electrical requirements, hot-runner controls, and maintenance capability at the destination plant.
The most successful projects treat DFM as a decision gate rather than a formality. A written DFM review clarifies what will be changed, what will remain as designed, what risks are accepted, and how part quality will be measured. It also creates a reliable record for brand owners, distributors, OEM customers, contract manufacturers, and future engineering teams.
The following review areas should be addressed before tooling manufacture begins. Their relative priority depends on annual volume, part size, resin type, cosmetic expectations, regulatory requirements, and whether the part is a prototype, bridge-production item, or long-term production component.
Review AreaWhat to ConfirmCommon Risk if MissedRecommended ActionPart geometryUniform wall thickness, realistic radii, ribs, bosses, snap fits, undercuts, and assembly interfaces.Sink marks, warpage, short shots, stress cracking, or difficult ejection.Approve a DFM-marked CAD model before mold design starts.Draft angleDraft direction and degree based on resin, texture, part depth, and cosmetic surface class.Drag marks, scuffing, part sticking, or surface damage during ejection.Increase draft on textured, deep, and high-gloss surfaces.Material selectionApproved resin grade, shrinkage range, additives, recycled-content level, color system, and supplier availability.Dimensional variation, brittleness, inconsistent color, or unplanned material substitutions.Specify resin grade and acceptable alternatives in writing.Gate strategyGate type, gate location, vestige allowance, flow direction, weld-line position, and packing path.Visible gate marks, weak weld lines, uneven filling, or poor cosmetics.Use mold-flow analysis for large, thin-wall, or cosmetic-critical components.Cooling designCooling channel layout, baffles, bubblers, conformal cooling opportunities, and water-circuit identification.Long cycle time, warp, uneven shrinkage, and unstable dimensions.Review cooling separately from cavity and core geometry.Ejection systemEjector pin placement, sleeve ejectors, stripper plates, lifters, air ejection, and witness-mark tolerance.Pin push, deformation, cracking, or unreliable automatic running.Place ejectors on strong, non-cosmetic surfaces wherever possible.Mold steel and treatmentSteel grade, hardness, corrosion resistance, polishing level, texture, coating, and expected tool life.Premature wear, rust, poor surface finish, and excessive maintenance.Match steel selection to resin abrasiveness, volume, and finish requirements.Tolerance planCritical-to-function dimensions, datum structure, measurement method, shrinkage allowances, and inspection frequency.Assembly interference, inconsistent fit, disputes over acceptance criteria.Separate critical dimensions from general molded tolerances.This table should be used as a working review document, not merely a design checklist. For example, a nominal wall thickness may be acceptable in CAD but still create a sink risk if a boss is too thick, a rib is oversized, or the gate cannot pack the local area effectively. Similarly, a tight dimension may be theoretically achievable but unsuitable for long-term production if it is affected by resin moisture, post-mold shrinkage, cavity imbalance, or changing ambient conditions.
Part design determines most molding behavior. Tooling can solve many challenges, but it cannot fully compensate for a design that ignores resin flow, cooling, shrinkage, and ejection. The following rules should be evaluated together rather than independently.
Uniform wall thickness is one of the most important rules in injection molded part design. Large thickness transitions create uneven cooling and differential shrinkage. When one area freezes earlier than another, the part may warp or develop visible sink marks. Thick zones also increase cooling time, which directly increases the cost of every cycle.
When a thick region is required for structural performance, consider coring out the section, adding ribs, using gussets, changing the load path, or selecting a higher-performance material. The exact solution depends on resin behavior. Glass-filled nylon, polycarbonate, ABS, polypropylene, POM, TPE, PC/ABS, PEEK, and flame-retardant compounds each respond differently to thickness, flow length, moisture, and processing temperature.
Draft is the angle that allows the molded component to release from the core and cavity without dragging. Smooth surfaces may need modest draft, while textured surfaces require more because the texture mechanically grips the mold surface. Deep housings, bins, covers, trays, enclosures, and large appliance panels often need more draft than early concept models include.
Cosmetic expectations must be defined in practical terms. Identify Class A surfaces, visible surfaces, hidden surfaces, allowed ejector marks, gate vestiges, parting lines, flow lines, and acceptable color variation. If an external housing will be painted, plated, laser-marked, or overmolded, those secondary operations should be discussed during mold design because they may affect material selection and surface specification.
Ribs improve stiffness without making the entire wall excessively thick. As a general engineering principle, ribs should be thinner than the nominal wall to reduce sink risk, while their height and spacing should support mold filling and ejection. Bosses should be supported by ribs or gussets where possible, especially when they receive screws, inserts, or repeated assembly loads.
Snap fits require special attention because they combine molding behavior with repeated mechanical deflection. Review root radius, strain level, assembly direction, tool split, potential undercuts, and environmental exposure. Living hinges are typically associated with polypropylene and require a suitable resin grade, gate orientation, controlled thickness, and validation through repeated flex testing.
The best mold configuration depends on projected volume, part complexity, resin, quality target, lead time, budget, and the intended location of production. A prototype mold for 100 samples does not require the same architecture as a hardened production mold designed for several hundred thousand cycles. However, even a rapid tool needs sufficient cooling, venting, alignment, and ejection to produce useful validation parts.
Mold ConfigurationBest UseTypical StrengthKey Review RequirementSingle-cavity moldLarge parts, prototypes, low-volume production, and high-value components.Lower initial tooling cost and simpler process control.Confirm whether output rate meets launch demand.Multi-cavity moldMedium and high-volume identical components.Higher output per cycle and lower part cost at scale.Verify cavity balance, runner balance, and inspection strategy.Family moldRelated components assembled in matched sets at low volume.Can reduce initial tooling investment.Review differing fill rates, cycle times, and scrap implications.Two-plate moldStandard cold-runner applications.Simple, durable, and widely supported globally.Assess runner waste and gate location.Three-plate moldParts requiring automatic point gating away from the parting line.Allows flexible gate placement and automatic degating.Confirm added complexity is justified by part requirements.Hot-runner moldHigher-volume production, engineering plastics, and reduced runner waste.Improves material efficiency and can shorten cycle time.Specify hot-runner brand, controller compatibility, and maintenance access.Insert moldMetal threads, contacts, reinforcement pieces, and electrical components.Creates secure integrated assemblies.Define insert tolerances, loading method, and retention testing.Overmold toolSoft grips, seals, protective surfaces, and multi-material products.Improves ergonomics and reduces assembly operations.Verify material bonding, substrate condition, and gate sequencing.This configuration comparison helps buyers avoid selecting cavity count based only on a desired part price. More cavities may reduce unit cost, but they increase mold complexity, maintenance requirements, machine tonnage, hot-runner investment, validation effort, and risk exposure. If market demand is uncertain, a lower-cavity rapid production tool can provide a more flexible commercial path.
Mold steel should be selected according to production volume, resin type, surface finish, corrosion risk, required hardness, maintenance plan, and shipment environment. Pre-hardened steel may be appropriate for many medium-volume tools, while hardened tool steels are commonly used for demanding, abrasive, or high-volume applications. Stainless steels may be necessary for corrosive resins, humid processing conditions, medical requirements, or polished surfaces requiring corrosion resistance.
Buyers should ask the toolmaker to identify the mold base material, cavity and core steel, slider and lifter materials, guide components, springs, ejector components, wear plates, coatings, and hot-runner system. For globally deployed tools, standard components can simplify replacement and maintenance. The final documentation should state what spare components are supplied and which parts should be stocked at the molding site.
A mold should not be accepted merely because it produces a part. The trial must demonstrate that the part can be molded consistently at an agreed process window. This is especially important for medical housings, electrical enclosures, automotive parts, safety-related components, threaded assemblies, sealing interfaces, and components with strict cosmetic requirements.
Validation StageMain PurposeRequired EvidenceBuyer DecisionDesign for manufacturability reviewIdentify risks before steel cutting.Annotated CAD, change list, resin assumptions, and tooling proposal.Approve design changes and freeze the manufacturing model.Mold design reviewConfirm mold layout and function.2D/3D mold layout, gate plan, cooling plan, ejection concept, and steel list.Approve the tool architecture before manufacturing.First trialVerify initial filling, ejection, and major mold operation.Sample parts, process settings, photos, defect observations, and trial report.Authorize modifications and define next trial priorities.Dimensional inspectionConfirm critical dimensions and assembly interfaces.Inspection report, CMM data where required, gauges, and measurement conditions.Accept, adjust tolerances, or revise tool geometry.Functional assembly testVerify fit with mating components.Assembly samples, torque data, leak test, snap-fit results, or electrical checks.Approve function or request engineering correction.Cosmetic reviewAssess surface quality under defined conditions.Approved limit samples, lighting conditions, texture comparison, and defect criteria.Define acceptable appearance and rework limits.Production capability runShow stable output over an extended run.Cycle time record, reject rate, cavity comparison, process window, and maintenance notes.Approve production release or require corrective action.Final acceptance and shipmentTransfer an operating, documented tool.Mold test video, packing list, spare parts, maintenance guide, and ownership record.Release final payment and arrange shipment or production.The validation table should be adapted to the project risk level. A simple storage tray may only need visual inspection, fit verification, and a practical production run. A medical device enclosure may need tighter documentation, resin traceability, detailed inspection reports, controlled surface requirements, and functional testing after sterilization or chemical exposure. A mold intended for automotive supply may require cavity identification, process discipline, capability studies, and formal change control.
Buyers should begin with a clear request-for-quotation package. At minimum, provide a native CAD file or neutral 3D file, 2D drawings where critical dimensions exist, annual volume forecast, resin grade, color, surface requirements, assembly requirements, expected machine location, target delivery date, and expected mold life. If the mold will be transferred to another country, specify the machine platen size, tie-bar spacing, nozzle radius, locating ring, ejector connection, water fittings, voltage, and hot-runner controller requirements.
Do not compare quotations only by total mold price. Compare cavity number, steel choice, mold base, runner system, expected cycle time, included trials, sample quantity, inspection level, shipping method, spare parts, engineering change policy, warranty, and post-delivery support. A quote that omits these items may create avoidable cost later.
For uncertain demand, consider phased investment. An aluminum rapid tool or lower-cavity steel tool may validate the market before a larger multi-cavity production tool is commissioned. This approach is often useful for startups, industrial design firms, medical-device developers, consumer-product brands, and companies launching new products through distributors or online retail channels.
Shipping logistics also need early planning. Molds are heavy precision assets and should be protected against moisture, corrosion, and transport damage. Confirm export crating, rust prevention, mold locking, lifting points, customs documentation, and whether the tool will be shipped by air, sea, rail, or truck. For projects moving through ports such as Shenzhen, Ningbo, Shanghai, Rotterdam, Long Beach, or Jebel Ali, packaging and handling details can affect both cost and delivery reliability.
Injection molding supports a wide range of products because it combines repeatable geometry, material versatility, high output potential, and compatibility with inserts, overmolding, textures, and automated assembly. The mold design checklist should be customized to the end-use environment.
Applications may also combine multiple manufacturing processes. A plastic enclosure can require CNC-machined inserts, molded bosses, ultrasonic welding, painting, printing, screws, foam, labels, final assembly, kitting, and retail packaging. Selecting a manufacturing partner capable of coordinating these steps can reduce handoffs and shorten the launch schedule.
A global consumer-product brand developed a handheld device housing with a high-gloss front surface, internal snap fits, screw bosses, and a painted logo area. The initial CAD included insufficient draft near the sidewalls and thick bosses behind a visible surface. During the engineering review, the mold maker recommended increasing draft, coring the bosses, adjusting rib thickness, moving the gate to a less visible location, and defining acceptable parting-line placement. The resulting tool produced lower sink risk, cleaner ejection, and fewer cosmetic adjustments during pilot production.
An industrial equipment developer needed 500 enclosures for field testing before committing to a large production run. Instead of investing immediately in a high-cavity hardened mold, the team selected a rapid tooling route with a practical cavity layout, production-grade resin, and inspection of critical mounting features. The low-volume run allowed the customer to validate installation, cable routing, gasket compression, and user access. After field feedback, the final production mold incorporated design improvements without requiring major changes to a large initial tool.
An electrical product required metal threaded inserts and conductive contacts to be molded into a compact plastic carrier. The pre-build review focused on insert tolerance, loading orientation, resin temperature, contact protection, retention force, and automated versus manual insertion. The mold design included support features to prevent insert movement during injection and ejection. Functional testing confirmed thread integrity and electrical alignment before the tool was released for recurring production.
The supplier landscape includes machine builders, mold makers, contract molders, rapid tooling specialists, and full-service manufacturing partners. The companies below are real organizations with international relevance. Buyers should still evaluate each supplier against their specific resin, component size, regulatory, production-volume, and logistics requirements.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidChina, USA, UK, France, Germany, and customers in more than 25 countries.Rapid manufacturing integration, DFM support, rapid tooling, low-volume molding, and flexible production.Injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, finishing, assembly, packaging, and direct shipping.Husky TechnologiesGlobal operations serving packaging, medical, closure, and beverage producers.High-output injection molding systems and integrated production technology.Injection molding machines, hot runners, molds, controllers, and service for packaging applications.ENGELEurope, North America, Asia, and global industrial manufacturing markets.Injection molding equipment, automation, process technology, and digital production systems.Injection molding machines, robots, turnkey cells, process optimization, and automation solutions.ArburgGlobal network with strong European, North American, and Asian market presence.Precision molding technology and flexible production systems.Injection molding machines, automation, digital production support, and additive manufacturing systems.Rosti GroupEurope, Asia, and North America through international manufacturing operations.Contract manufacturing, injection molding, assembly, and supply-chain support.Plastic injection molding, medical and consumer manufacturing, assembly, and product industrialization.Nypro, a Jabil CompanyGlobal manufacturing locations serving healthcare and consumer markets.Complex healthcare manufacturing, engineering, and scalable production.Injection molding, precision components, medical manufacturing, automation, and assembly.FictivGlobal digital manufacturing network serving product development teams.Digital sourcing, prototyping, manufacturing coordination, and speed.Injection molding, CNC machining, 3D printing, urethane casting, and quality management support.This supplier comparison is intended to help buyers understand market positioning. Machine manufacturers such as ENGEL and Arburg are typically selected by companies operating molding facilities. Contract manufacturers such as Rosti Group and Nypro may support larger production programs with assembly requirements. Rapid manufacturing partners such as TEAM Rapid can be especially useful when a project needs fast design feedback, low-volume validation, tooling, machining, finishing, and flexible transition into production.
TEAM Rapid supports international product developers, engineers, startups, brand owners, distributors, OEM customers, and established manufacturers with rapid tooling, injection molding, insert molding, overmolding, CNC machining, 3D printing, vacuum casting, die casting, sheet metal fabrication, finishing, assembly, packaging, and direct shipping. Its ISO 9001:2015 quality management certification, more than 10 years of industry experience, more than 500 customers, more than 6,000 delivered projects, and service record across more than 25 countries provide practical evidence of its ability to manage prototype-to-production programs. The company does not promote a fixed captive list of branded mold components; instead, it specifies suitable mold bases, steels, resins, inserts, and production components according to the project requirements, while applying DFM analysis, inspection practices, machining tolerances down to 0.01 mm where applicable, and documented manufacturability reviews. TEAM Rapid supports OEM, ODM, wholesale, retail, regional distribution, and direct end-user projects with flexible order quantities from one prototype to more than 100,000 parts. Its delivery model includes turnkey and customer-owned tooling solutions, rather than BOO or on-site bulk supply services. While the company profile does not claim overseas subsidiaries or local warehouses, TEAM Rapid has established experience serving customers in the USA, UK, France, Germany, China, and other international markets through responsive online engineering communication, direct shipping, project coordination, packaging support, and after-sales follow-up. Customers can request a detailed rapid tooling service consultation for tooling strategy or submit part files through the global manufacturing quotation form for DFM feedback and pricing.
Injection mold design in 2026 will increasingly be shaped by faster development cycles, sustainability requirements, digital traceability, automation, and regional supply-chain resilience. Tooling teams will need to optimize not only part geometry but also energy use, resin selection, scrap reduction, data capture, and maintenance predictability.
Engineering teams are increasingly using AI-supported design analysis to identify draft problems, inconsistent wall thickness, possible undercuts, unsupported bosses, and likely warpage areas earlier in the design cycle. These tools do not replace experienced mold engineers, but they can speed up issue detection and help global teams review more design iterations before manufacturing begins.
Brands are under pressure to increase recycled content and reduce virgin plastic consumption. However, recycled resin can have wider property variation, altered flow behavior, contamination risk, color variability, and different shrinkage characteristics. Mold design reviews will need to address material consistency, gate size, venting, processing windows, and cosmetic acceptance criteria when recycled or bio-based polymers are specified.
Conformal cooling inserts manufactured through metal additive processes can follow complex cavity shapes more closely than traditional drilled channels. For suitable parts, this can improve cooling uniformity, reduce cycle time, and lower warpage. The technology is most valuable when the expected savings justify the added insert cost and when maintenance planning is considered.
Manufacturers increasingly track machine energy consumption, resin yield, runner waste, reject rate, and transport emissions. Hot-runner systems, optimized cooling, shorter cycles, reduced regrind dependence, and better cavity balance can contribute to lower resource use. Buyers should begin asking suppliers for practical process data rather than relying only on general sustainability claims.
Pressure sensors, cavity monitoring, cycle counters, cooling-flow monitoring, and digital maintenance records can improve production consistency. Predictive maintenance is especially useful for molds operating across multiple sites because it helps teams identify wear, blocked cooling channels, and process drift before a major production interruption occurs.
There is no single item that overrides all others, but wall thickness, draft, material selection, gate location, cooling, ejection, and tolerance requirements are usually the highest-impact areas. These factors strongly influence fill behavior, shrinkage, cycle time, part release, cosmetics, and long-term consistency.
DFM should be completed before steel is cut and ideally before the final product design is frozen. Early review allows changes to be made in CAD, where they are faster and less expensive than modifying a completed mold.
The required draft depends on resin, part depth, texture, surface finish, mold polish, and ejection direction. Smooth surfaces may need less draft than textured surfaces, while deep parts and highly textured exterior surfaces often need more. The mold maker should confirm draft recommendations during DFM.
A hot runner can reduce runner waste and support higher-volume production, but it adds initial cost, complexity, maintenance needs, and controller requirements. A cold runner may be more practical for low-volume parts, simpler tools, or projects where material changes are frequent. The right choice depends on annual volume, resin cost, part geometry, and production strategy.
A family mold can produce related parts in one cycle, but it should be used carefully. Parts with different sizes, wall thicknesses, fill behavior, or cooling requirements can create imbalance and higher scrap. Family molds are often most suitable for lower-volume matched sets rather than long-term high-output programs.
Request final mold drawings, steel and component information, trial reports, process settings, sample inspection data, spare-part list, maintenance instructions, mold photographs, shipping records, and clear ownership documentation. If the mold will be transferred internationally, also confirm water, electrical, controller, and machine-interface specifications.
Optimize wall thickness, reduce unnecessary material volume, use appropriate cavity count, improve cooling, minimize secondary operations, select the right resin, avoid overly tight non-functional tolerances, and approve DFM changes before tooling begins. Cost reduction is most effective when it improves manufacturability rather than simply lowering tool specifications.
-
Injection Mold Life in the Global Market: What to Expect
Injection mold life is the number of molding cycles a tool can complete while producing parts within agreed dimensional, cosmetic, and functional requirements. In the global market, a well-designed and properly maintained mold may produce anything from a few thousand prototype parts to several million production parts. The correct expectation depends on the mold material, resin, part geometry, tooling quality, maintenance plan, production conditions, and required surface finish.
Most aluminum injection molds provide approximately 5,000 to 100,000 cycles, while production molds made from suitable pre-hardened or hardened tool steel commonly deliver 100,000 to more than 1,000,000 cycles. High-volume molds using hardened steel, replaceable wear components, balanced cooling, and disciplined maintenance can exceed several million cycles.
For prototypes and market testing, a short-run mold may be the most economical option. For recurring commercial production, steel selection, cavity design, cooling efficiency, ejection loads, resin abrasiveness, and preventive maintenance have a greater effect on total cost than the original mold price alone. A mold that costs more initially can produce a lower cost per part over its useful life.
When comparing suppliers in the global market, consider qualified international manufacturers, including experienced Chinese companies, when they provide relevant certifications, documented inspection, clear engineering communication, and strong pre-sales and after-sales support. Their cost-performance advantages can be significant without requiring a compromise in tooling control.
For a practical decision, identify the expected lifetime volume, annual production, resin type, dimensional tolerance, cosmetic requirements, and planned product life before requesting a quotation. A professional toolmaker should then recommend the appropriate mold base, steel grade, surface treatment, cavity count, cooling arrangement, and maintenance interval.
Tool life should not be confused with the number of times a mold can physically close. A mold may continue operating after its expected cycle count, but the resulting parts may show flash, dimensional drift, short shots, sink marks, scratches, poor texture transfer, or inconsistent ejection. The useful life of an injection mold ends when it can no longer produce acceptable parts economically and repeatably.
Manufacturers usually describe mold life in cycles. One cycle includes mold closing, injection, packing, cooling, mold opening, and part ejection. In a four-cavity mold, one cycle produces four parts, so the part output is four times the number of completed cycles, excluding rejects. This distinction is important when estimating capacity and return on tooling investment.
Several life definitions may appear in a tooling quotation:
A reliable quotation should state what is included in the life estimate. The same steel can deliver very different results when used with different resins, injection pressures, cycle times, mold temperatures, or maintenance practices.
Tooling material is one of the most visible factors affecting service life, but it is not the only one. Aluminum can be highly effective for low-volume production because it machines quickly and transfers heat efficiently. Hardened tool steel generally costs more and takes longer to manufacture, but it provides greater resistance to wear, corrosion, deformation, and repeated thermal cycling.
Typical mold life ranges by tooling materialTooling materialTypical cycle rangeCommon applicationMain advantageMain limitationRecommended production profilePrototype aluminum5,000–20,000 cyclesDesign validation and pilot runsFast machining and low initial costLower wear resistancePrototype and short-run productionProduction aluminum20,000–100,000 cyclesLow-volume commercial partsEfficient cooling and rapid deliveryMay wear under abrasive resinRecurring low-volume ordersPre-hardened P20 steel100,000–500,000 cyclesGeneral production toolingBalanced cost, machinability, and strengthLess wear resistance than hardened steelMedium-volume production420 or 2083 stainless steel200,000–1,000,000 cyclesMedical, optical, and corrosive-resin partsCorrosion resistance and good polishabilityHigher material and machining costClean environments and demanding finishesH13 or 1.2344 hardened steel500,000–2,000,000 cyclesHigh-volume technical componentsStrong wear and thermal-fatigue resistanceMore difficult and expensive to machineLong production programsS136 or equivalent hardened stainless steel500,000–2,000,000 cyclesHigh-polish and corrosive applicationsExcellent finish and corrosion performanceRequires controlled heat treatment and polishingCosmetic and precision partsCarburized or specialty tool steel1,000,000+ cyclesAutomotive and high-volume consumer productsVery high wear resistanceHighest tooling investmentLarge-volume and long-life programsThese ranges are planning estimates rather than universal guarantees. A mold with a simple geometry, moderate pressure, non-abrasive resin, and robust cooling can exceed the lower end of its expected range. A complex mold with thin walls, multiple slides, high glass-fiber content, aggressive surface texture, or frequent color changes may require repair much earlier.
Steel quality affects hardness, toughness, polishability, corrosion resistance, and dimensional stability. A mold that is too soft may wear rapidly around gates, shutoffs, slides, and parting lines. A mold that is excessively hard but poorly heat-treated may become brittle and crack under impact or thermal stress. The correct balance depends on the resin, mold design, cavity pressure, surface finish, and maintenance environment.
Unfilled polypropylene and polyethylene are usually less abrasive than glass-filled nylon, mineral-filled polycarbonate, flame-retardant compounds, or long-glass-fiber engineering plastics. Glass fibers and mineral fillers can erode gates, runners, cores, cavities, and ejector components. Corrosive additives can attack mold surfaces, particularly when the tool is not dried and protected after production.
Deep ribs, narrow cores, thin walls, undercuts, lifters, collapsible cores, and side actions increase mechanical and thermal loads. Sharp internal corners concentrate stress. Thin shutoffs can deform or chip. Small venting features can become blocked, causing gas burns and higher injection pressure. A design that is optimized for molding generally produces a longer-lived tool than one that forces the mold to compensate for difficult geometry.
Uneven cooling causes warpage, extended cycle times, thermal stress, and inconsistent shrinkage. Poorly positioned cooling channels can leave hot spots near thick sections or core pins. Over time, repeated thermal cycling can contribute to cracking, corrosion, and dimensional movement. Conformal cooling, baffles, bubblers, and carefully balanced conventional channels can improve productivity and reduce stress when applied appropriately.
Excessive pressure increases stress on parting lines, slides, inserts, sprue bushings, and mold bases. Insufficient venting often causes operators to raise pressure, which can accelerate wear and flash. Correct filling analysis, gate selection, vent design, and process validation reduce the need to run the machine at unnecessarily aggressive settings.
Preventive maintenance is one of the most cost-effective ways to extend tool life. Cleaning, lubrication, inspection of guide components, checking cooling channels, sharpening or replacing damaged components, and protecting polished surfaces can prevent small defects from becoming major repairs. A mold used every week requires a different maintenance frequency from a tool stored for months between production campaigns.
Incorrect mold opening speed, excessive ejector force, poor purging, improper clamping, and foreign particles on the parting line can damage a tool quickly. Stable process parameters reduce thermal and mechanical shocks. Operators should also follow documented procedures for mold installation, water connection, startup, shutdown, cleaning, and storage.
Different product categories place different demands on an injection mold. A simple tray may require only a two-plate mold with a basic edge gate. A medical housing may need stainless steel, mirror polishing, controlled venting, validated dimensional inspection, and strict contamination controls. A large automotive panel may require multiple hot runners, complex slides, high clamping force, and careful thermal balancing.
The product’s commercial life should guide the tooling strategy. If a product is expected to sell for three months, investing in a two-million-cycle mold may not be economical. If the product supports a ten-year aftermarket program, a low-cost prototype mold can create severe supply and quality risks later.
Start with the expected lifetime quantity, then add a practical allowance for rejects, engineering samples, maintenance trials, and future demand. The basic calculation is:
Required cycles = lifetime parts ÷ number of cavities ÷ expected utilization rate
For example, a four-cavity mold intended to produce 800,000 saleable parts with an estimated 92 percent utilization rate would need approximately 217,400 cycles. A P20 steel mold could be suitable in some conditions, but a corrosion-resistant or hardened insert may be more appropriate if the resin is abrasive or the product must remain in production for many years.
Also consider:
Ask the toolmaker to separate the expected life of the mold base, cavities, cores, slides, hot-runner system, cooling fittings, ejector system, and replaceable wear parts. These components rarely have identical service lives.
The global supply market includes specialist mold makers, digital manufacturing platforms, component suppliers, and integrated manufacturing partners. The best choice depends on whether the project requires rapid tooling, high-volume automotive molds, medical tooling, local production support, or a complete transition from prototype to finished parts.
Selected injection mold suppliers and their practical strengthsCompanyService regionsCore strengthsKey offeringsBest fitBuying considerationTEAM RapidChina, North America, Europe, Asia, and international export marketsFast engineering support, integrated tooling, and flexible productionRapid tooling, injection molding, CNC machining, 3D printing, finishing, assembly, and packagingPrototype-to-production programs from one part to 100,000+ partsRequest a DFM review and confirm steel, cycle target, inspection, and maintenance scopeProtolabsNorth America, Europe, and JapanDigital quoting, rapid manufacturing, and standardized workflowsInjection molding, CNC machining, 3D printing, and design analysisFast product development and repeatable low-volume ordersCheck material, texture, tolerance, and mold ownership termsXcentric Mold & EngineeringUnited States and international customersRapid injection molding and engineering-led toolingProduction injection molding, rapid tooling, CNC machining, and finishingU.S.-based development programs and bridge productionConfirm expected cycle life and production location before approvalFictivUnited States and international supply networksDigital sourcing, supplier coordination, and project visibilityInjection molding, CNC machining, sheet metal, and additive manufacturingCompanies needing managed multi-process sourcingClarify the assigned manufacturing partner and quality documentationStackTeckCanada, United States, Europe, and global automotive marketsHigh-cavitation and complex production toolingAutomotive molds, thin-wall packaging tools, hot-runner integration, and automationHigh-volume and technically complex programsBest suited to substantial production volumes and formal engineering reviewsTooling Tech GroupUnited States, Europe, and global automotive supply chainsLarge molds, automotive tooling, and program managementInjection molds, compression molds, tooling systems, and production supportAutomotive and industrial programs requiring large-scale toolingReview project timing, maintenance responsibility, and spare-component strategyRosti GroupEurope, Asia, and North AmericaIntegrated plastic manufacturing and contract productionTooling, injection molding, assembly, and supply-chain servicesBrand owners seeking regional manufacturing supportCompare plant location, resin approval, production capacity, and logistics costSupplier location should not be judged only by distance. A nearby supplier may offer convenient communication but higher tooling cost or limited process coverage. An international supplier may offer stronger price performance and broader capacity, provided it supplies traceable materials, inspection records, mold trials, spare-part plans, and responsive technical support.
Design for manufacturability analysis should identify uniform wall thickness, draft angles, parting-line options, gate location, venting, ejection, undercuts, cooling, shrinkage, and likely cosmetic risks. This review is especially valuable before steel is cut because many tool-life problems begin with a design that creates excessive pressure, difficult ejection, or fragile shutoffs.
Do not accept an undefined description such as “premium steel.” Request the actual grade, hardness range, heat-treatment method, corrosion protection, and location of hardened inserts. For a high-volume tool, ask whether the steel certificate and hardness report will be provided with the final documentation.
The contract should state who owns the mold, where it will be stored, whether it can be transferred, and who pays for refurbishment. If production may move from Asia to Europe or North America, the tool should be designed for transport, reinstallation, spare-part availability, and local machine compatibility.
Acceptance should cover first-shot samples, dimensional reports, appearance, cycle time, cavity balance, part weight, mold operation, and the quantity of approved samples. A mold can appear complete while still requiring major work on flash, filling balance, ejector marks, or cooling performance.
Critical spares may include ejector pins, return pins, springs, cavity inserts, core inserts, slide wear plates, seals, nozzles, gate components, and hot-runner heaters. Keeping these items available can reduce downtime and protect the production schedule.
Ask for a preventive maintenance schedule based on cycles, not only calendar time. The plan should identify daily, weekly, monthly, and annual checks. For abrasive or corrosive materials, inspection intervals should be shorter and wear components should be monitored more closely.
Good maintenance is a controlled production activity rather than an emergency repair response. After each run, remove resin residue, clean the parting line, dry water circuits when appropriate, protect polished surfaces, and record any abnormal noise, ejection resistance, flash, or dimensional shift. Never close and store a wet mold without corrosion protection.
Recommended maintenance actions for injection moldsMaintenance areaActionSuggested timingRisk reducedResponsible roleRecord to retainParting lineRemove flash, resin, dust, and foreign particlesEvery production runFlash and shutoff damageMachine operatorCleaning checklistEjector systemInspect pins, sleeves, return movement, and lubricationEvery run or defined cycle intervalSticking, bending, and pin breakageTooling technicianCycle-based service logCooling circuitsCheck flow, leaks, scale, fittings, and water qualityWeekly to monthlyHot spots, corrosion, and long cyclesProcess technicianFlow and temperature recordSlides and liftersInspect wear plates, lubrication, alignment, and movementDefined cycle intervalGalling, flash, and misalignmentTooling technicianInspection reportVentsClean and restore blocked vent featuresAs needed and during preventive serviceBurn marks, short shots, and high pressureMold technicianRepair historyPolished and textured surfacesClean with approved materials and protect from impactEvery runScratches, stains, and texture variationOperator and technicianCosmetic approval recordStorage protectionApply rust preventive, seal ports, and control storage conditionsBefore storageCorrosion and contaminationTooling departmentStorage release formWhen mold repairs are necessary, identify the underlying cause. Replacing a worn ejector pin without correcting excessive ejection force or insufficient draft may only postpone another failure. Similarly, polishing flash from a parting line without checking alignment can reduce shutoff thickness and shorten the remaining mold life.
Injection molds support products across automotive, medical, consumer, industrial, electrical, telecommunications, sanitary, and office-equipment sectors. The required mold life varies by industry because production volumes, regulatory requirements, product liability, and appearance standards are different.
Applications are not limited to finished plastic parts. Injection molding is also used for insert molding, overmolding, two-shot components, elastomer integration, and assemblies that combine metal and plastic. These processes may increase the number of loading operations and require additional mold alignment features.
A startup developing a handheld electronic product may need 5,000 to 15,000 parts for fit testing, user trials, and early sales. A machined aluminum mold can reduce lead time and make design revisions affordable. If the enclosure design is not yet frozen, investing in a hardened production mold may create unnecessary sunk cost. The mold should still include appropriate draft, venting, replaceable inserts, and a documented repair path.
An industrial equipment manufacturer may require 250,000 parts over several years. A P20 or equivalent pre-hardened steel mold may be suitable when the resin is not highly abrasive and the part geometry is moderate. Hardened inserts should be considered around gates, shutoffs, slides, and high-wear areas. Cycle records and periodic dimensional checks can confirm whether the tool is aging normally.
An automotive supplier may need several million components over the vehicle program and replacement-parts period. The tool may require hardened steel, hot-runner balancing, robust slides, automated handling, replaceable wear plates, and a formal maintenance schedule. The lowest initial quotation is rarely the lowest total-cost option in this situation.
A medical device housing may require stainless steel for corrosion resistance, high polish, controlled molding conditions, and detailed inspection records. Even when the lifetime volume is moderate, the required quality level may justify a more durable tool. Surface condition, cleanliness, traceability, and process validation can be more important than maximum cycle count.
TEAM Rapid combines rapid tooling, injection molding, CNC machining, 3D printing, finishing, assembly, packaging, and shipping support through an integrated manufacturing network in China. Its ISO 9001:2015 quality system, more than ten years of manufacturing experience, work for customers in over 25 countries, more than 500 satisfied customers, and record of over 6,000 delivered projects provide useful evidence for international tooling programs. The company uses DFM reports and manufacturability analysis to identify risks before steel cutting, including parting-line problems, difficult ejection, inefficient cooling, excessive resin use, and cycle-time opportunities. Customers can use flexible OEM and ODM-style cooperation for prototypes, low-volume production, recurring orders, or larger programs, while end users, distributors, dealers, brand owners, and individual product developers can request project-specific sourcing and production arrangements rather than a fixed one-size-fits-all package. Its capabilities cover projects from one prototype to more than 100,000 parts, with rapid tooling and molded parts commonly supported in approximately 5 to 25 days depending on requirements. TEAM Rapid does not present itself as a BOO or on-site bulk-supply operator; it provides EPC/Turnkey and customer-owned plant support models when required, including tooling, process coordination, procurement, assembly, packaging, limited warehousing, and direct shipping. The profile does not claim overseas subsidiaries or permanent local warehouses, so buyers should confirm regional stock and service arrangements for each project; however, the company supports international customers through responsive online engineering communication, pre-sales DFM review, inspection documentation, after-sales technical coordination, and experience working across Asian and Western business cultures. This combination makes it a practical option for customers comparing Chinese manufacturing against suppliers in the United States, Canada, Europe, or other global production hubs.
For tooling evaluation, customers can review TEAM Rapid’s rapid tooling services for global projects and submit technical files through the international manufacturing quotation page. A useful request should include the 3D model, 2D drawings, resin grade, expected volume, surface finish, tolerance, target cycle life, delivery location, and whether the mold will be customer-owned and transferred later.
Tooling cost should be measured against total cost per acceptable part, not only the purchase price. A low-cost aluminum mold may be ideal for a short product launch, while a hardened steel mold may be more economical for sustained demand. The calculation should include mold price, maintenance, repairs, downtime, scrap, machine time, part price, logistics, and the cost of replacing a failed tool.
Cavity count also affects economics. A single-cavity mold has a lower initial cost and is easier to modify, but it requires more cycles to meet the same volume. A multi-cavity mold increases upfront investment and requires careful cavity balancing, but it can lower machine time and part cost. The right choice depends on demand certainty, available machine capacity, part size, quality requirements, and expected product life.
Hot runners may reduce runner waste and improve cycle efficiency, but they add components that need maintenance and may be more expensive to repair. Cold runners can be simpler and more economical for some applications. The decision should be based on resin value, cavity count, part geometry, color changes, cycle targets, and service capability.
Several developments are shaping tooling decisions in 2026 and beyond.
Sustainability does not always mean choosing the cheapest or lightest mold. A durable tool that avoids repeated replacement, produces less scrap, and supports efficient cycle times can have a lower environmental impact over the complete product life.
An aluminum mold commonly lasts from approximately 5,000 to 100,000 cycles. The actual result depends on the aluminum grade, part complexity, resin abrasiveness, injection pressure, cooling design, and maintenance. Aluminum is often suitable for prototypes and low-volume production rather than very large lifetime quantities.
Yes. A properly designed and maintained steel mold can reach one million cycles or more. Hardened steel, suitable wear inserts, stable processing, effective cooling, and disciplined maintenance are usually required, especially for abrasive engineering resins or complex mechanisms.
Glass-filled nylon can reduce mold life because the fibers are abrasive. Gates, runners, cavities, cores, slides, and ejector components may wear faster. Hardened inserts, abrasion-resistant treatments, robust gate design, and shorter inspection intervals can reduce the impact.
Toolmakers normally measure life in cycles, but buyers should convert cycles into parts using the cavity count. A four-cavity mold producing 250,000 cycles can theoretically make one million parts before considering rejects, downtime, and maintenance.
There is no single task for every mold. Cleaning the parting line, lubricating moving components correctly, monitoring cooling circuits, inspecting ejection, and protecting the mold during storage are all essential. The maintenance plan should reflect resin type, production frequency, and mold complexity.
Choose aluminum when the design is still changing or the expected volume is limited. Choose steel when demand is substantial, the product will remain active for years, the resin is abrasive, or dimensional and cosmetic consistency are critical. A DFM and volume review can prevent over- or under-specifying the tool.
Often, yes. Inserts, slides, ejector components, guide systems, and hot-runner parts can be repaired or replaced. However, repair economics depend on the remaining condition of the mold base, cavity alignment, part design, steel availability, and the cost of downtime.
Compare the complete offer rather than the mold price alone. Review engineering support, steel documentation, trial samples, inspection capability, guaranteed life, spare parts, maintenance, shipping, communication, ownership terms, and after-sales response. A qualified international supplier with transparent controls may provide stronger value than a nearby supplier with limited technical scope.
Provide the 3D model, 2D drawings, resin and color, annual and lifetime volume, cavity preference, tolerance, surface finish, target cycle time, machine information, delivery destination, and required certifications. Also state whether you need only the mold or a turnkey package including molded parts, assembly, packaging, and shipping.
Injection mold life is best treated as a design and supply-chain decision rather than a simple steel specification. A short-run aluminum mold can be the most efficient choice for a new product, while a hardened steel tool with replaceable wear components is more appropriate for high-volume or long-term programs. The strongest results come from combining accurate demand planning, DFM analysis, suitable materials, balanced cooling, stable processing, preventive maintenance, and clear ownership terms.
For global buyers, evaluate both local and international suppliers. Review proven project experience, quality systems, engineering response, inspection records, production capacity, logistics support, and long-term maintenance capability. With the right specifications and an evidence-based life estimate, businesses can reduce downtime, control cost per part, and keep injection molding reliable throughout the product’s commercial life.
-
Global Market Guide to Aluminum and Steel Injection Molds
Aluminum injection molds are usually the better choice when speed, lower upfront tooling cost, frequent design changes, and low-to-medium production volumes matter most. Steel injection molds are the stronger option for long production runs, abrasive or high-temperature resins, tight repeatability requirements, complex multi-cavity tooling, and parts that must maintain consistent quality over hundreds of thousands or millions of cycles.
For most Global market buyers, select aluminum tooling for prototype validation, bridge production, market testing, and roughly 500 to 50,000 parts. Select steel tooling for stable products with higher annual demand, demanding engineering plastics, high cosmetic requirements, or production programs expected to exceed 100,000 parts. The best decision is not based on mold material alone: resin, part geometry, cavity count, cooling design, expected annual volume, tolerance, and maintenance planning all affect the total cost.
Leading suppliers commonly considered by international buyers include TEAM Rapid in China, Proto Labs in the United States and Europe, Xometry in North America and Europe, Fictiv in the United States, and FOW Mould in China. Qualified international suppliers, including Chinese mold makers with ISO-based quality systems, clear DFM communication, reliable pre-sales and after-sales support, and export experience, can offer compelling cost-performance advantages for Global market programs.
Injection mold sourcing is now a global engineering and logistics decision rather than a purely local purchasing exercise. Product teams in New York, London, Berlin, Singapore, Dubai, Melbourne, Toronto, São Paulo, and Johannesburg routinely source molds and molded parts from a mix of domestic suppliers, regional toolrooms, and experienced Chinese manufacturers. Major trade corridors through Shenzhen, Hong Kong, Shanghai, Ningbo, Rotterdam, Hamburg, Los Angeles, Long Beach, Singapore, and Jebel Ali support the movement of tooling, resin, components, and finished parts.
In this environment, aluminum versus steel injection molds is one of the earliest and most consequential choices in a product launch. It influences capital expenditure, project lead time, design flexibility, production output, part consistency, maintenance expectations, and the timing of a future tooling transfer. A low-cost mold can become expensive if it produces unstable parts, cycles slowly, requires repeated repair, or cannot accommodate a planned increase in demand. Conversely, an expensive hardened steel mold can lock capital into a product that is still changing or has not yet established commercial demand.
Aluminum molds are not simply “prototype molds,” and steel molds are not automatically “production molds.” Modern aluminum tooling can produce high-quality end-use parts when the tool is engineered correctly, cooling is adequate, and the resin is compatible. Likewise, pre-hardened steel tools can be a practical middle ground for medium-volume programs. Buyers should evaluate the entire manufacturing route, including tool construction, machine capability, inspection methods, resin management, finishing, assembly, packaging, and shipping.
The following comparison provides a practical starting point. Actual performance depends on alloy selection, mold design, resin type, press settings, cavity count, cooling circuits, surface treatment, and maintenance discipline.
Evaluation FactorAluminum Injection MoldSteel Injection MoldPractical Buying ImpactInitial tooling costUsually lower because aluminum machines faster and requires less machining time.Usually higher due to harder material, longer machining, heat treatment, and finishing requirements.Aluminum can reduce launch investment for uncertain or low-volume programs.Tooling lead timeOften faster, especially for simple prototype and bridge tools.Usually longer, particularly for hardened, multi-cavity, hot-runner, or high-polish tools.Aluminum is attractive when product validation or market entry is time-sensitive.Expected tool lifeCommonly suited to low and medium volumes; life varies widely by resin and design.Suitable for high-volume production and repeated long-term operation.Steel becomes more economical when demand is stable and accumulated part volume is high.Cooling performanceHigh thermal conductivity can support rapid heat transfer when cooling channels are well designed.Lower thermal conductivity than aluminum but highly durable and compatible with advanced cooling strategies.Cycle time should be validated through mold-flow review and production trials, not assumed.Wear resistanceLower resistance to abrasive fillers, aggressive glass-filled resins, and repeated sliding contact.Higher resistance, especially with suitable grades, coatings, and hardened inserts.Steel is generally safer for glass-filled nylon, mineral-filled materials, and high-volume wear conditions.Design-change flexibilityTypically easier and faster to modify during product development.Changes can require more time and expense, especially after hardening.Aluminum supports evolving products, pilot launches, and design optimization.Surface finishCan achieve good cosmetic results, but mirror polish durability may be limited over extended runs.Offers excellent long-term support for polished, textured, optical, and cosmetic surfaces.Steel is preferred for premium visible surfaces and sustained appearance requirements.Cavity countCan support multiple cavities, though high cavitation increases structural and maintenance demands.Well suited to high-cavity tools for large-scale output.Use steel when a high-output production cell is central to the business case.The key lesson is that aluminum and steel are not competing only on tool price. They represent different risk-management approaches. Aluminum prioritizes learning speed and capital efficiency. Steel prioritizes repeatability, longevity, output capacity, and long-term process stability.
Tooling suppliers may use several grades of aluminum and steel rather than one universal material. The designation matters because it affects machinability, polishability, corrosion resistance, heat treatment response, toughness, and the tool’s ability to tolerate pressure, temperature, and repeated cycles.
Tooling Material TypeTypical UseStrengthsLimitations7075 aluminumRapid tooling, prototype molds, low-volume production tools.Good machinability, relatively strong aluminum grade, fast manufacturing.Less wear-resistant than steel under abrasive resins and prolonged production.QC-10 aluminumHigh-performance aluminum mold bases and cavity blocks.Uniform material characteristics and useful thermal conductivity.May require steel inserts in high-wear zones.P20 steelMedium-volume production molds, mold bases, general-purpose tooling.Widely used pre-hardened mold steel with balanced performance.May not be the first choice for highly corrosive or highly abrasive resins.H13 steelHigh-temperature applications, inserts, demanding molding conditions.Strong toughness and heat resistance when properly processed.More expensive and slower to machine than aluminum or P20.420 stainless steelMedical, optical, clear plastic, and corrosion-sensitive tooling.Corrosion resistance and high polish potential.Higher tooling cost and more demanding machining requirements.S136 stainless steelPremium cosmetic, transparent, medical, and long-life molds.Excellent polishability, corrosion resistance, and stable long-term performance.Best justified where quality, appearance, and tool life justify the investment.Steel insert within aluminum baseBridge production and mixed-demand programs.Balances faster aluminum construction with durable wear surfaces.Requires careful engineering of fit, cooling, and thermal expansion.Hybrid tooling is increasingly common. For example, an aluminum mold base may use hardened steel gate inserts, core pins, slides, lifters, shutoffs, or cavity inserts. This approach can preserve fast lead times while protecting areas exposed to repeated friction, high injection pressure, or abrasive material flow. It is particularly useful for engineering enclosures, clips, housings, covers, trays, and functional components with localized wear points.
Upfront tooling price is visible, but total cost of ownership is more important. A practical calculation should include mold manufacturing, design engineering, DFM revisions, trial shots, part unit cost, cycle time, planned volume, scrap rate, maintenance, shipping, import duties where applicable, warehousing, and the expected probability of design changes.
Aluminum tooling often lowers the financial threshold for starting production. It can be ideal for a startup introducing a consumer product, a medical-device team validating an enclosure, an automotive supplier checking fit before a program release, or an industrial OEM testing regional demand. With good design, appropriate resin selection, and realistic production expectations, aluminum tools can deliver high-quality molded parts for pilot runs and commercial low-volume launches.
Steel tooling has a stronger business case when the part design is frozen and forecast volumes are high. Steel is better able to withstand repeated clamp force, injection pressure, sliding action, ejection cycles, and wear from filled compounds. It is also preferable when a product requires consistent texture, glossy finish, precision alignment, complex side actions, hot runners, close shutoffs, or long unattended production campaigns.
Production SituationRecommended Mold DirectionWhy It FitsKey Engineering CheckPrototype functional testAluminum or simplified rapid toolFast validation with lower investment.Confirm the resin and part geometry represent final-use conditions.Market launch under 10,000 partsAluminum toolAllows low-risk commercial entry and easier future changes.Check gate vestige, cosmetic areas, and expected rework cycles.Bridge production of 10,000 to 50,000 partsAluminum with steel inserts or pre-hardened steelBalances speed, durability, and investment.Review wear zones, cooling, and cavity layout.Annual production above 100,000 partsSteel production moldSupports durability, stable output, and automation planning.Validate cycle time, multi-cavity balance, and preventive maintenance intervals.Glass-filled nylon componentsHardened steel or steel insertsAbrasive fibers can wear aluminum rapidly.Specify wear-resistant gates, runners, shutoffs, and cores.Clear PC or optical partsHigh-polish stainless steelSurface quality and corrosion resistance are critical.Define polish standard, handling method, and inspection criteria.Frequent product revisionsAluminum or modular insert toolingModifications are generally faster and more economical.Design interchangeable inserts before first tool release.High-volume consumer enclosureSteel multi-cavity moldSupports high output and consistent cosmetic performance.Assess texture, weld lines, sink, warpage, and automated part handling.Part quality should be defined in measurable terms. Buyers should specify dimensional tolerances, cosmetic requirements, color standards, gloss level, texture, gate location, flash limits, sink marks, weld-line acceptance, warp limits, inspection frequency, material certificates, and packaging standards. A mold’s material alone does not determine quality. Good results come from sound DFM, stable process settings, capable molding machines, proper drying and handling of resin, disciplined inspection, and documented corrective action.
Start with the product’s commercial reality. If annual demand is uncertain, it is usually unwise to overinvest in a complex production steel tool before customer demand is confirmed. If a product is already committed to a multi-year purchase forecast, a steel mold can prevent capacity limitations and rising maintenance costs later.
A detailed rapid tooling service review can help identify whether an aluminum tool, steel tool, or hybrid configuration best suits the part before machining begins. DFM feedback is especially valuable when changing wall thickness, adding draft, relocating gates, increasing radii, or reducing unnecessary undercuts can reduce tooling cost and improve molding stability.
Both aluminum and steel molds are used across global industries. The correct choice depends on the operating environment, production forecast, resin type, cosmetic requirements, regulatory expectations, and product lifecycle.
IndustryTypical Molded PartsCommon Tooling ChoiceReason for SelectionAutomotiveInterior trim, clips, covers, connectors, under-hood components.Steel for production; aluminum for validation.Long programs, engineering resins, and repeatability often favor steel.Medical devicesInstrument housings, disposable components, treatment-unit covers.Stainless steel or controlled aluminum bridge tools.Traceability, surface quality, material control, and precision are important.Consumer electronicsCases, chargers, wearable housings, control panels.Aluminum for launch; steel for mature volumes.Fast product cycles often require early design flexibility.Industrial equipmentControl housings, guards, knobs, fluid-system covers.P20 or hardened steel.Durability and recurring spare-parts production support steel investment.Home appliancesHandles, bezels, appliance housings, trays, switches.Steel multi-cavity tooling.High unit volumes and visible surfaces demand consistent output.TelecommunicationsEnclosures, antenna covers, cable-management parts.Aluminum or steel depending on forecast.Prototype speed is useful, while established network equipment may need durable tools.Office equipmentPrinter covers, paper trays, mechanical linkages.Steel for recurring production.Dimensional stability and assembly consistency are essential.Startups and industrial designProduct shells, test fixtures, clips, functional prototypes.Aluminum or modular rapid tooling.Lower risk and faster iteration support early commercialization.For automotive and industrial customers, steel tooling is often the long-term destination. However, aluminum tools can reduce risk during early vehicle interior validation, accessory launches, aftermarket product tests, and limited regional releases. For medical and consumer applications, a bridge mold can help verify assembly, ergonomics, drop performance, sterilization compatibility, or user feedback before major tooling investment.
A product team developing a handheld electronic enclosure expects an initial launch of 8,000 units but anticipates possible changes to the battery door, button openings, and internal ribs. An aluminum mold with replaceable steel inserts is a practical solution. The company can test assembly, cosmetic texture, snap-fit performance, and customer response without committing to a high-cost multi-cavity steel tool. If demand accelerates after launch, the validated geometry can be transferred into a steel production mold.
An automotive supplier needs a glass-filled nylon retention clip for an engine-bay application. Although the part is small, it experiences heat, vibration, chemical exposure, and high assembly volume. Hardened steel inserts and a durable steel mold are normally more appropriate because the filled resin can wear softer cavity surfaces. The mold should be designed around resin shrinkage, fiber orientation, gate location, parting-line control, and repeatable dimensional inspection.
A medical-device manufacturer requires a clean, professional housing for a diagnostic instrument. The early market forecast is modest, but surface appearance and dimensional fit with internal electronics are critical. A carefully engineered aluminum bridge tool may support the first commercial batches, provided the resin, finish, and inspection plan are confirmed. If the product reaches wider hospital distribution, a stainless or hardened steel tool can support long-term appearance control and repeatable production.
An industrial equipment brand requires replacement covers and protective housings for machines already installed across multiple regions. Demand is steady but not extremely high. A pre-hardened P20 steel mold may offer a practical balance between cost and durability. The supplier should retain the tool, preserve production settings, control material lots, and maintain inspection records so replacement parts remain compatible with installed equipment over several years.
The supplier landscape includes specialized rapid-manufacturing providers, traditional mold makers, digital manufacturing platforms, and vertically integrated production partners. The right supplier should be evaluated on engineering capability, quality documentation, location, communication speed, mold ownership terms, export experience, machine capacity, tooling maintenance, and ability to deliver molded parts rather than only the mold.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidGlobal customers across more than 25 countries; China-based manufacturing and direct international shipping.Rapid tooling, DFM support, low-volume to volume production, integrated plastic and metal manufacturing.Injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, die casting, finishing, assembly, packaging.Proto LabsNorth America and Europe, with global customer reach.Digital quotation workflows and fast-turn manufacturing programs.Injection molding, CNC machining, 3D printing, sheet metal fabrication.XometryNorth America and Europe, serving international sourcing programs.Large manufacturing network and online manufacturing procurement.Injection molding, CNC machining, sheet metal, additive manufacturing, finishing.FictivUnited States-focused customer support with global manufacturing resources.Digital manufacturing management and engineering-oriented sourcing.Injection molding, CNC machining, urethane casting, 3D printing, finishing.FOW MouldChina-based export mold manufacturing for international customers.Custom plastic injection mold design and production tooling.Automotive molds, household molds, industrial molds, plastic injection tooling.StackTeck SystemsNorth America and global packaging markets.High-performance tooling for packaging and high-output applications.Stack molds, closures tooling, thin-wall packaging molds, automation systems.Husky TechnologiesGlobal operations serving packaging and medical markets.Integrated high-volume molding systems and hot-runner technology.Injection molding systems, hot runners, PET preform molds, medical molding solutions.This table is a starting point rather than a substitute for supplier qualification. For lower-volume projects, the ability to provide responsive engineering feedback and flexible revisions may be more valuable than a supplier’s high-volume automation capability. For high-output packaging, automotive, or medical programs, machine integration, hot-runner expertise, validation documentation, and maintenance resources become more important.
TEAM Rapid supports innovators, product designers, engineers, startups, distributors, brand owners, established manufacturers, and individual product developers with an integrated path from prototype to repeatable production. Its ISO 9001:2015 quality management certification, more than 10 years of manufacturing experience, over 500 customers, more than 6,000 delivered projects, and service experience across more than 25 countries provide practical evidence of export-oriented manufacturing capability. The company combines in-house machining, mold manufacturing, injection molding, inspection, finishing, assembly, packaging, procurement support, and direct shipping from China, allowing customers to coordinate custom plastic and metal parts through one manufacturing partner. Rather than claiming unverified overseas warehouses or subsidiaries, TEAM Rapid provides global buyers with direct project communication, engineering responses within hours, DFM analysis before tooling, controlled manufacturing in China, and shipment support into markets including the United States, United Kingdom, France, Germany, and other international destinations. It offers OEM and ODM cooperation, wholesale supply, prototype orders, recurring production, distributor support, and customized manufacturing for end users and brand owners. TEAM Rapid provides turnkey and customer-owned production solutions, not BOO models or on-site bulk supply services, with each project managed around customer-owned drawings, specifications, approval standards, and commercial requirements.
Its relevant product strength for injection molding lies in the ability to connect rapid tooling, precision mold production, CNC machining, wire EDM, EDM, polishing, material handling, molding, finishing, inspection, and assembly in one workflow. Customers can request aluminum bridge tools, steel production tools, insert molding, overmolding, plastic housings, enclosures, trays, covers, fillers, cases, and complex functional parts. Tight-tolerance CNC capability down to 0.01 mm supports accurate tool components and secondary machining where needed. For projects requiring fast validation, rapid tooling and molded part production can be supported in approximately 5 to 25 days, depending on design complexity, material, tool structure, cavity count, and finishing needs.
Global buyers can begin by submitting CAD files, annual volume expectations, resin preferences, color and surface requirements, tolerance needs, and target delivery dates through the custom manufacturing quotation request. A clear request improves the accuracy of tooling recommendations and makes it easier to compare aluminum, steel, and hybrid mold options on a total-cost basis.
By 2026, the aluminum versus steel decision will increasingly be influenced by digital engineering, sustainability requirements, supply-chain resilience, and faster product release cycles. Mold-flow simulation, real-time production monitoring, automated visual inspection, cavity-pressure sensing, digital maintenance records, and AI-assisted DFM are helping suppliers identify risks earlier. These tools do not replace engineering judgment, but they can reduce trial cycles and provide more consistent decision-making.
Sustainability is also changing tooling decisions. Brands are introducing more recycled-content resins, bio-based polymers, lightweight designs, mono-material packaging, and parts designed for repair or recycling. Some recycled and filled materials may have different flow behavior, moisture sensitivity, shrinkage, or wear characteristics than virgin resins. This can increase the importance of steel inserts, corrosion-resistant materials, venting strategy, and process validation. Buyers should test production-intent resin rather than making tooling decisions based only on generic material data.
Policy and compliance expectations are growing across regions. Product traceability, recycled-content claims, chemical compliance, packaging regulations, medical documentation, and carbon-reporting requests increasingly affect material records and supplier selection. A global supplier should be able to discuss resin traceability, inspection plans, packaging methods, export documentation, and consistent communication across time zones.
Another important trend is distributed production planning. Companies may retain a production mold in one region while using aluminum bridge tooling in another region for temporary demand spikes, localized launches, or engineering changes. This strategy can reduce market-entry risk, although mold ownership, design file control, quality standards, and logistics responsibilities must be documented carefully.
Yes. Aluminum injection molds can produce end-use production parts when volume, resin, geometry, cosmetic expectations, and maintenance requirements are appropriate. They are especially effective for bridge production, pilot launches, and low-to-medium-volume commercial programs.
There is no universal number. Tool life depends on aluminum grade, part design, resin abrasiveness, injection pressure, temperature, cavity count, maintenance, and the presence of steel inserts. A supplier should provide a realistic expected range based on the specific part and material.
Use steel when the product has stable demand, high annual volume, abrasive or high-temperature resin, demanding cosmetic surfaces, tight tolerances, many cavities, or a long product lifecycle. Steel is also preferred for high-wear features such as slides, shutoffs, threads, and fiber-filled resin flow paths.
Some aluminum tools can be modified with steel inserts, replacement cavities, or reinforced wear areas. However, a full conversion to a high-volume steel production tool often requires a new mold because the structural requirements, cooling layout, and cavity design may differ.
No. Part quality depends on mold design, cooling, venting, gating, machine settings, resin preparation, operator control, inspection, and maintenance. A well-designed aluminum mold can outperform a poorly engineered steel mold in a low-volume application.
Provide 3D CAD files, 2D drawings if available, resin grade, color, annual volume, target quantity, tolerance requirements, cosmetic requirements, intended market, expected delivery date, assembly details, insert requirements, and packaging expectations. Photos of similar parts and critical assembly interfaces are also useful.
Yes. Many buyers prefer an integrated supplier because it reduces tool transfer risk and simplifies quality accountability. TEAM Rapid can support mold manufacturing, injection molding, finishing, assembly, packaging, and direct shipment for suitable programs.
Choose aluminum injection tooling when you need to move quickly, preserve capital, validate a changing design, or produce a controlled low-to-medium-volume launch. Choose steel injection tooling when your design is stable, your resin is demanding, your quality requirements are strict, and your forecast justifies long-term production infrastructure. For many Global market projects, the most commercially sensible route is aluminum or hybrid tooling first, followed by steel tooling after demand, design, and process capability have been validated.
Before placing a tooling order, compare suppliers on more than quote price. Ask for DFM feedback, tool material details, expected mold life, cavity plan, cooling strategy, trial process, inspection documentation, mold ownership terms, maintenance support, lead time, shipping plan, and communication responsibility. That disciplined approach will help turn aluminum and steel injection mold selection into a reliable product-launch advantage.
-
Injection Molding or 3D Printing: Global Market Costs
For the Global market, choose 3D printing when you need one to several hundred parts quickly, expect design changes, or need complex geometries without tooling. Choose injection molding when the design is stable and you need repeatable parts at medium-to-high volumes, usually from several hundred to several thousand units depending on material, mold complexity, finishing, and logistics.
The practical break-even point for injection molding versus 3D printing is often between 500 and 5,000 parts. Simple plastic parts can cross over earlier, while highly complex molds, low-cost printed parts, or uncertain demand can push the break-even volume higher. Calculate the decision using total delivered cost, not unit price alone: include mold cost, setup, material, labor, finishing, scrap, validation, freight, duties, and inventory risk.
Buyers in North America, Europe, Asia-Pacific, the Middle East, Latin America, and Africa can source from local specialists such as Protolabs, Xometry, Fictiv, Stratasys Direct, Jabil, and Quickparts. Qualified international suppliers, including Chinese manufacturers with ISO certification, transparent engineering support, strong pre-sales communication, and reliable after-sales handling, can also be competitive because tooling and labor costs may be lower while lead times remain practical for global shipping.
Injection molding forms parts by injecting molten polymer into a machined mold cavity under pressure. The mold may be aluminum for rapid or low-volume tooling, or hardened steel for long production runs. Once the tool is qualified, the process can produce thousands or millions of nearly identical components with fast cycle times. It is particularly effective for housings, clips, caps, trays, medical consumables, appliance components, automotive trim, packaging parts, and consumer-product enclosures.
3D printing, also called additive manufacturing, builds a part layer by layer from a digital file. Common polymer processes include SLA, SLS, MJF, FDM, DLP, and material jetting. Each process has a different balance of surface finish, strength, dimensional accuracy, material selection, build size, and cost. Because no mold is required, additive manufacturing is useful for prototypes, fit checks, low-volume custom parts, jigs, fixtures, medical models, functional validation, bridge production, and demand-driven spare parts.
The basic commercial difference is simple: injection molding has a high upfront cost and low marginal part cost; 3D printing has almost no tooling cost but a higher marginal part cost. The correct choice depends on demand certainty, engineering maturity, part geometry, regulatory needs, target material, time to market, and the cost of changing the design after production begins.
A useful comparison starts with total project cost. For injection molding, total cost combines mold design, DFM review, mold manufacture, trials, sampling, molding, secondary operations, inspection, packaging, freight, and any expected design revisions. For 3D printing, the total includes build preparation, machine time, material, support removal, post-curing or sintering, finishing, inspection, packaging, and freight. The cost curve changes as volume rises: printing usually starts lower, while molding becomes less expensive per unit after the tooling investment is absorbed.
Use this simplified calculation when planning a program:
Break-even quantity = Injection mold cost ÷ (3D printed unit cost − Injection molded unit cost)
For example, if an aluminum mold costs US$8,000, a printed part costs US$18, and an injection molded part costs US$4, the estimated break-even is 571 parts. In reality, the result should be adjusted for finishing, production yield, freight, packaging, design changes, and the value of receiving parts earlier. A lower printed unit cost or a more expensive multi-cavity mold will raise the break-even volume.
The following ranges are directional planning estimates for polymer parts. Actual quotations depend heavily on geometry, resin, tolerance, texture, color, mold cavities, production location, and destination.
Project ScenarioLikely Better ProcessTypical VolumeCost DriverLead-Time ConsiderationConcept model with frequent design changes3D printing1–20 partsNo tooling and fast file revisionsOften days rather than weeksFunctional prototype in nylon-like materialSLS or MJF printing10–100 partsStrength, complexity, no mold costFast build and finishing cycleMarket-test consumer enclosureRapid tooling or printing100–1,000 partsDemand uncertainty and appearance requirementsRapid aluminum tooling can be practicalStable product with repeated ordersInjection molding1,000–20,000 partsLower unit cost and repeatabilityTooling time is recovered through outputHigh-volume packaging or appliance componentInjection molding20,000–1,000,000+ partsCycle time, multi-cavity tooling, automationLonger tool launch, very low unit costCustomized replacement or service part3D printing1–500 partsAvoiding inventory and obsolete toolingDigital inventory supports on-demand supplyThese scenarios show why volume alone is not enough. A medical-device enclosure may require molded production at relatively low quantities because resin traceability, cosmetic consistency, sealing features, and validation requirements justify a tool. Conversely, a high-priced industrial spare part may remain printed even at hundreds of units because the inventory and tooling risks outweigh the unit-cost savings of molding.
Injection molding is strongest when a part requires production-grade thermoplastics, repeatable wall thickness, molded-in features, snap fits, living hinges, threaded inserts, surface textures, color control, and predictable mechanical behavior. Typical materials include ABS, PC, PC/ABS, PA6, PA66, POM, PP, PE, TPU, TPE, PBT, PPS, and glass-filled engineering polymers. The process can also support insert molding, overmolding, family molds, multi-cavity molds, hot-runner systems, and automated part handling.
3D printing is strongest when geometry would be expensive to machine or mold, such as internal channels, lattice structures, organic forms, custom ergonomic grips, low-volume fixtures, patient-specific devices, and consolidated assemblies. It is also valuable before tooling because an engineering team can physically validate draft angles, assembly access, wall thickness, grip feel, and component clearance before releasing a mold design.
Selection Factor3D Printing AdvantageInjection Molding AdvantagePractical Buying DecisionDesign maturityEasy and inexpensive revisionsBest after design freezePrint before committing to toolingPart quantityLow-volume and irregular demandMedium and high-volume demandModel expected annual demand and reorder patternGeometryComplex internal features and latticesConsistent draftable geometries with efficient cyclesReview geometry with DFM and additive engineersSurface qualityCan require sanding, coating, or vapor smoothingTool texture and polished surfaces are repeatableUse molded samples for final cosmetic approvalMaterial performanceSpecialized printed polymers availableBroad range of production thermoplasticsMatch resin data to heat, impact, chemical, and UV needsProduction consistencyBuild orientation can affect resultsStrong repeatability after tool validationUse molding for controlled long-term supplyTooling investmentNo dedicated mold requiredHigh initial cost, lower recurring costConsider demand certainty and product life cycleFor many global product launches, the best route is not strictly one process or the other. Teams often use SLA or SLS parts for early testing, CNC machining for accurate engineering prototypes, vacuum casting for presentation samples, rapid aluminum tooling for pilot production, and steel tooling for sustained production. This staged approach reduces the risk of discovering a design problem after a high-value production mold has been cut.
The Global market is shaped by different cost and supply-chain conditions across regions. North American buyers often prioritize short domestic lead times, supplier proximity, regulatory documentation, and fast engineering communication. European buyers may place additional emphasis on CE-related product compliance, recycling obligations, REACH considerations, energy use, and material traceability. Asia-Pacific manufacturing hubs, particularly Shenzhen, Dongguan, Ningbo, Suzhou, Singapore, Seoul, Tokyo, and Ho Chi Minh City, offer dense supplier networks for tooling, molding, electronics integration, and export logistics.
Ports and trade hubs matter when calculating delivered cost. Shenzhen and Hong Kong support rapid export for electronics and consumer-product programs; Ningbo-Zhoushan and Shanghai serve major industrial supply chains; Rotterdam, Hamburg, Los Angeles, Long Beach, Singapore, Jebel Ali, and Dubai are important gateways for containerized molding programs. For low-volume printed parts and prototype tools, air freight may preserve launch speed. For stable production volumes, sea freight, consolidated shipments, and regional fulfillment can significantly lower landed cost.
Exchange-rate movement, resin pricing, tariffs, carbon reporting rules, shipping disruptions, and local-content requirements can all influence the best sourcing route. Buyers should avoid selecting a supplier based only on the mold quote. A low-cost tool with poor cooling, unsuitable steel, weak venting, or inconsistent process control can create expensive downstream scrap, delays, rework, and customer returns.
Start with a production brief that states annual demand, first-order quantity, expected reorder frequency, material requirements, cosmetic expectations, tolerance-critical dimensions, target markets, certification needs, packaging, and shipment destination. If demand is uncertain, request a staged quotation: prototypes, rapid tooling, pilot molding, and production tooling. This gives the business team a decision path instead of forcing an early all-or-nothing tooling commitment.
Ask every injection molding supplier for a DFM report before tooling starts. The report should address draft angle, wall thickness, rib design, sink-mark risk, weld lines, gate location, parting line, ejection, shrinkage, warpage, undercuts, tooling steel, cavity count, expected cycle time, and inspection method. For printed components, ask about process orientation, support marks, anisotropic strength, dimensional tolerance, post-processing, color stability, and whether the selected material is a prototype-grade or production-capable polymer.
Use samples to validate assembly, function, appearance, and packaging. A part can be dimensionally correct yet fail in real use because of stiffness, snap-fit fatigue, odor, gloss variation, surface marks, chemical exposure, or heat deformation. For parts that interact with medical, food-contact, electrical, automotive, or industrial systems, establish the required material documentation and test plan before ordering production.
Evaluation AreaQuestions to AskWhy It MattersEvidence to RequestEngineering reviewWill the supplier issue DFM before tooling?Prevents avoidable mold and quality problemsAnnotated DFM report and revision historyQuality systemIs the manufacturer ISO 9001 certified?Supports controlled processes and traceabilityCurrent certification and inspection planMaterial controlWhich resin grade and supplier will be used?Ensures performance matches the specificationMaterial data sheet and batch recordsTooling ownershipWho owns, stores, maintains, and can transfer the mold?Protects long-term supply continuityWritten tooling ownership termsCapacity and deliveryCan the supplier support pilot and repeat orders?Reduces supply interruptions after launchProduction schedule and lead-time commitmentInspectionHow are critical dimensions measured?Confirms tolerance capabilityFAI, CMM report, gauges, and sampling planAfter-sales supportHow are defects, revisions, and reorders handled?Protects the buyer after shipmentCorrective-action and communication processWhen comparing quotations, normalize the scope. One supplier may quote molded parts only, while another includes mold trials, texture, assembly, packaging, inspection reports, and delivery. Compare like for like. The most economical program is the one that meets specification reliably at the lowest total lifecycle cost, not simply the one with the lowest initial line item.
Automotive programs use 3D printing for dashboards, fit-check models, jigs, fixtures, airflow studies, custom tools, and low-volume specialty parts. Injection molding supports durable interior trim, switch housings, clips, ducts, bezels, covers, sensor enclosures, under-hood components, and exterior details. Automotive manufacturers and suppliers typically need strong dimensional repeatability and production-grade heat, chemical, and impact performance.
Medical and laboratory sectors use printed models for anatomical visualization, device prototypes, custom fixtures, and low-volume development assemblies. Molding is selected for repeatable housings, diagnostic-device components, disposable consumables, instrument covers, cartridge bodies, and production assemblies. Material selection, cleanliness, documentation, and validation are essential where parts are used near patients, samples, or clinical workflows.
Consumer electronics and communications products frequently follow a hybrid route. Teams print early ergonomic models, machine precision components, use vacuum casting for presentation sets, and then move to injection molded enclosures, buttons, cable-management parts, optical covers, and accessory components. Shenzhen, Dongguan, and Hong Kong remain important connected hubs for this type of product because manufacturing, assembly, procurement, and export services are concentrated in the region.
Industrial equipment, office devices, electrical appliances, sanitary products, and commercial products use both technologies for housings, panels, trays, guards, brackets, cable guides, control-box covers, pump components, dispensers, and maintenance spares. For large housings, moldability, ribbing, warpage control, and shipping volume require careful review. For short-run replacement parts, additive manufacturing can reduce inventory while maintaining service availability.
A startup developing a handheld diagnostic device may print twenty enclosure iterations in SLA or SLS to improve ergonomics and internal PCB fit. Once the design is stable, it may order an aluminum rapid tool for 500 pilot units to verify assembly, packaging, and market feedback. If demand becomes predictable, the same product can transition to a multi-cavity steel mold with a production-grade PC/ABS resin for lower cost per unit.
An industrial automation company needing 150 customized cable-routing brackets across several machine models may retain 3D printing. The bracket geometry may differ by customer installation, and the cost of individual molds would not be justified. A nylon-based printed material can provide practical strength while the company keeps digital files instead of physical inventory.
A consumer-appliance brand launching a global accessory may use injection molding from the beginning if it has committed retailer orders for 30,000 units. A polished or textured mold can deliver a consistent visual surface, molded color can eliminate painting, and a multi-cavity tool can lower unit cost. Before cutting steel, the brand should still print or machine assembly models to validate the snap features, screw bosses, wall thickness, and interaction with mating components.
The companies below represent established options for buyers comparing digital manufacturing, rapid prototyping, tooling, and injection molding. Capabilities vary by site, material, destination, production volume, and program requirements, so buyers should verify current availability and quality documentation for their specific project.
CompanyPrimary Service RegionsCore StrengthsKey OfferingsProtolabsNorth America and EuropeFast digital quoting and rapid manufacturingInjection molding, CNC machining, sheet metal, 3D printingXometryUnited States, Europe, global sourcing networkBroad manufacturing marketplace and online procurement3D printing, injection molding, CNC machining, sheet metalFictivNorth America with global manufacturing networkDigital manufacturing platform and supply-chain supportCNC machining, injection molding, 3D printing, finishingJabilGlobal, including North America, Europe, and Asia-PacificLarge-scale manufacturing and product industrializationInjection molding, tooling, assemblies, regulated manufacturingStratasys DirectNorth America and international customersIndustrial additive manufacturing experienceSLA, FDM, SLS, PolyJet, production additive servicesQuickpartsNorth America and international marketsPrototype-to-production manufacturing services3D printing, CNC machining, injection molding, urethane castingTEAM RapidGlobal customers across more than 25 countriesChina-based rapid manufacturing, tooling, molding, and integrated support3D printing, CNC, vacuum casting, rapid tooling, injection molding, finishing, assemblyFor buyers in the Global market, regional proximity may be important for frequent engineering visits, urgent freight, or regulated projects. However, a cross-border supplier can be commercially attractive when it provides documented quality systems, clear DFM communication, manageable logistics, and a single-source route from prototype through production. This is particularly relevant for startups, product designers, distributors, brand owners, and established manufacturers balancing speed, cost, and supply resilience.
TEAM Rapid supports global product development and production programs with more than ten years of manufacturing experience, over 500 customers, and more than 6,000 delivered projects for clients in over 25 countries. Its ISO 9001:2015 quality system, in-house machining and tooling capability, tight-tolerance CNC capacity down to 0.01 mm, and DFM-led manufacturing review support practical control of materials, moldability, dimensions, and inspection requirements; the company works with diversified plastic and metal material options rather than claiming proprietary component brands, allowing specified resin grades and performance requirements to guide production. It serves end users, product designers, startups, distributors, dealers, brand owners, and individual buyers through flexible OEM/ODM-style custom manufacturing, wholesale-volume production, prototype orders, recurring supply, assembly, packaging, and regional distribution-oriented shipping arrangements. TEAM Rapid has established experience supporting customers in markets including the USA, UK, France, Germany, and wider international destinations through direct global shipping, fast responses within a few hours, one-to-one engineering communication, and coordinated pre-sale DFM and after-sales order support; while its stated manufacturing base and integrated resource network are in China rather than disclosed overseas subsidiaries or local warehouses, this operating model gives international buyers a defined point of accountability from quotation through delivery. For product-launch requirements, TEAM Rapid can coordinate turnkey and customer-owned manufacturing arrangements, including procurement, assembly, packaging, kitting, scheduling, and shipping, rather than BOO or on-site bulk-supply services.
For early-stage programs, the company can provide rapid prototyping services using SLA and SLS 3D printing, CNC machining, and vacuum casting, with typical project lead times of approximately two to eight days depending on the requirements. For a bridge between prototypes and recurring production, its rapid tooling and molding programs can support tooling and molded-part production in approximately five to twenty-five days. Once demand is clearer, customers can move into custom injection molding services for housings, cases, trays, covers, fillers, enclosures, insert-molded components, and overmolded parts.
TEAM Rapid is particularly relevant when the production route must remain flexible. A buyer can begin with one prototype, validate a design, revise it after DFM feedback, produce a low-volume pilot batch, and then scale toward 100,000 or more parts without moving between disconnected suppliers. Customers can request a project-specific cost comparison and manufacturability review through the company’s online manufacturing quotation request process.
By 2026, the distinction between injection molding and 3D printing will become less rigid because both methods are increasingly connected by digital workflows. Artificial intelligence-assisted DFM, automated quotation systems, simulation-based mold optimization, digital twins, in-process monitoring, and cloud-based production tracking will help teams make earlier and more accurate process decisions. Mold-flow analysis and conformal cooling strategies will continue to improve cycle time and warpage control, especially for technically demanding components.
Additive manufacturing is likely to expand in high-value, low-volume, customized, and distributed-production applications. More durable printed polymers, faster powder-bed systems, improved surface finishing, and automated depowdering will make printed parts more viable for end-use applications. At the same time, injection molding will remain the dominant choice for high-volume plastic products because its production speed, repeatability, broad resin options, and low marginal cost are difficult to match.
Sustainability will increasingly influence material and process selection. Buyers will ask for recycled-content resins, bio-based polymers, recyclable mono-material designs, lower-energy production routes, reduced packaging, and lower freight emissions. Design teams should understand that recycled content can affect color, shrinkage, flow, mechanical performance, and consistency, making supplier testing and material documentation important. Molded parts may reduce energy per unit at scale, while 3D printing can reduce material waste and obsolete inventory for low-volume parts. The better environmental option depends on the entire lifecycle, including tooling, yield, shipping, product lifespan, repairability, and end-of-life recovery.
Policy and trade conditions will also shape sourcing. Carbon reporting rules, product-safety expectations, plastics restrictions, extended producer responsibility requirements, import duties, and traceability obligations are encouraging buyers to use diversified suppliers and documented material chains. Global brands should build flexibility into their manufacturing plan by qualifying more than one route where practical: additive manufacturing for development and service parts, rapid tooling for controlled launch quantities, and production molding for mature, sustained demand.
3D printing is usually cheaper for prototypes and low volumes because it does not require a mold. Injection molding becomes cheaper per unit after the tooling cost is spread across enough parts. The break-even point can range from hundreds to thousands of units.
There is no universal quantity. Simple parts with modest tooling costs may justify molding at 500 to 1,000 units. Complex tools, large parts, or uncertain demand may require several thousand units before molding produces a lower total cost.
Yes, especially for low-volume industrial components, fixtures, customized products, service parts, and certain high-value applications. The selected printing process and material must be evaluated for strength, heat resistance, finish, chemical exposure, and long-term durability.
After the mold is built, each molding cycle can produce one or multiple parts in seconds or minutes. Material use, labor, and finishing can be highly controlled, allowing the fixed tooling cost to be spread across a large production quantity.
A printed prototype is useful for validating geometry, assembly, and appearance before mold manufacture. The mold itself is generally machined from aluminum or steel, although printed inserts may be used in limited specialist applications.
Include 3D CAD files, 2D drawings for critical dimensions, material requirements, quantity, color, finish, tolerance expectations, assembly needs, target delivery date, destination country, and any testing or certification requirements.
The answer depends on urgency, regulatory requirements, engineering access, total landed cost, and production volume. Local suppliers can simplify visits and short freight routes, while qualified China-based suppliers can offer competitive tooling and production pricing with integrated manufacturing services and international shipping.
-
China Injection Molding Guide for Global Market Buyers
China injection molding is a practical sourcing option for Global Market buyers who need competitive tooling costs, flexible production volumes, rapid engineering feedback, and access to broad plastic material choices. The best results come from selecting a supplier that can review DFM requirements, build and maintain tooling, validate first articles, control production quality, and coordinate export packaging and shipping.
For most projects, buyers should shortlist suppliers with demonstrated tooling capability, documented quality systems, transparent mold ownership terms, and experience shipping to their target regions. Established Chinese manufacturers such as TEAM Rapid, FOW Mould, TK Group, HLH Rapid, Richfields Plastics, and Rosti China are worth evaluating according to part complexity, annual volume, resin requirements, and destination-market compliance needs.
Qualified international suppliers, including China-based manufacturers with relevant certifications, responsive pre-sales engineering, and dependable after-sales support, can offer strong cost-performance advantages. They are especially suitable when buyers need prototype-to-production continuity, low-volume molding, rapid tooling, or an alternative to higher-cost domestic production.
Before placing an order, send a 3D CAD file, 2D drawing, annual forecast, resin specification, cosmetic standard, critical tolerance list, packaging expectation, and destination country requirements. Ask for a written DFM report, tooling proposal, sample approval plan, inspection approach, and a clear quotation separating mold cost, unit price, finishing, assembly, freight, and taxes.
China remains one of the most important manufacturing locations for injection molded plastic parts because it combines toolmaking capacity, resin supply networks, production labor, secondary processing, and export infrastructure. Major molding clusters around Shenzhen, Dongguan, Guangzhou, Ningbo, Taizhou, Suzhou, Shanghai, Xiamen, Qingdao, and Tianjin support projects ranging from a few bridge-production parts to multi-cavity tools running millions of cycles.
For Global Market buyers, the attraction is not simply a lower piece price. A capable China injection molding supplier can integrate mold design, CNC machining, EDM, wire EDM, polishing, texture coordination, mold assembly, molding trials, inspection, pad printing, painting, ultrasonic welding, assembly, packaging, and export logistics. This reduces the risk created by splitting the project among separate tool shops, molders, finishers, and freight providers.
China’s major ports also make international distribution practical. Shenzhen’s Yantian and Shekou terminals serve South China manufacturing; Ningbo-Zhoushan supports Zhejiang suppliers; Shanghai handles high-volume global container flows; and Qingdao, Xiamen, and Tianjin provide additional routing options. Buyers should still calculate the full landed cost, including ocean or air freight, customs duty, insurance, local transport, inventory holding, and possible tariffs.
The market is highly varied. Some factories specialize in low-cost commodity parts, while others focus on precision medical components, automotive connectors, optical plastics, consumer housings, or industrial equipment. The correct supplier is therefore the one whose equipment, engineering processes, quality discipline, and project scale match the specific product—not necessarily the factory with the lowest initial quotation.
Injection molding in China covers a wide range of plastic components. Product design, polymer behavior, mold steel selection, cavity count, surface finish, and production forecast all influence the recommended manufacturing approach. A low-volume enclosure for a market test may be best served by aluminum rapid tooling, while an automotive interior component may require hardened steel tooling, specialized texture control, and validation over a long production life.
Product TypeTypical MaterialsCommon ApplicationsKey Manufacturing ConsiderationElectronic enclosuresABS, PC, PC/ABS, flame-retardant gradesControllers, chargers, routers, smart devicesWall thickness, snap fits, cosmetic surface, EMI requirementsIndustrial housingsABS, nylon, PP, PBT, PCSensors, control boxes, machinery coversImpact resistance, inserts, sealing interfaces, dimensional stabilityMedical device componentsPC, ABS, PP, POM, medical-grade polymersHandheld instruments, laboratory devices, diagnostic equipmentTraceability, clean handling, resin documentation, validation needsAutomotive plastic partsPP, PA6, PA66, PBT, PC/ABSInterior trim, clips, ducts, covers, connectorsHeat resistance, durability, appearance, repeatable dimensionsConsumer product partsABS, PP, HIPS, TPE, silicone-compatible materialsAppliances, toys, kitchenware, personal productsColor consistency, texture, assembly fit, retail packagingInsert molded partsNylon, PBT, PC, ABS with metal insertsThreaded mounts, electrical components, handlesInsert retention, preheating, fixture design, cycle stabilityOvermolded componentsTPE, TPU, silicone-like elastomers over rigid plasticsGrips, seals, buttons, protective coversMaterial bonding, part positioning, gate location, shrink controlThis product mix shows why material choice must be considered early. A resin substitution may reduce cost, but it can also affect shrinkage, strength, chemical resistance, flame rating, surface appearance, and tool wear. Buyers should specify approved material manufacturers or acceptable equivalents when product performance or certification depends on a particular grade.
The following companies are examples of established providers that Global Market buyers may assess. Capabilities should always be confirmed directly because molding machine tonnage, tooling scope, certifications, export routes, and available production capacity can change by facility and project.
CompanyMain Service RegionsCore StrengthsKey OfferingsTEAM RapidChina, United States, United Kingdom, France, Germany, wider Global MarketPrototype-to-production integration, rapid tooling, DFM support, flexible volumesInjection molding, insert molding, overmolding, CNC machining, finishing, assembly, packagingFOW MouldChina, North America, Europe, Asia-PacificPlastic mold design and manufacturing for automotive and consumer applicationsInjection molds, multi-cavity molds, automotive tooling, plastic part productionTK GroupChina, Europe, North America, AsiaLarge-scale precision plastic component manufacturing and mold technologyPrecision molds, consumer electronics parts, medical-related plastic components, molding servicesHLH RapidChina, United Kingdom, Europe, North AmericaRapid manufacturing support for product development and lower-volume productionRapid tooling, injection molding, CNC machining, vacuum casting, 3D printingRichfields PlasticsChina, United States, Europe, Global MarketCustom plastic manufacturing with tooling and production supportInjection molding, mold manufacturing, plastic assemblies, finishing optionsRosti ChinaChina, Europe, North America, Asia-PacificEngineering-led injection molding for regulated and technical productsPrecision molding, manufacturing engineering, assembly, supply-chain supportSupplier comparison should go beyond company size. A specialized mold maker may deliver an excellent tool but not offer molding, while a production molder may prefer established high-volume programs. Buyers needing frequent design changes should look for a partner that can modify tools quickly and communicate engineering changes without ambiguity. Buyers with stable, high-volume demand should evaluate cavity strategy, automation, cycle-time optimization, preventive mold maintenance, and production backup plans.
A good sourcing decision begins with technical fit. Share a complete package rather than requesting a price from a single image or incomplete model. The supplier should be able to identify issues such as undercuts, weak snap features, non-uniform walls, sharp internal corners, insufficient draft, excessive length-to-thickness ratios, difficult ejection, potential sink marks, and tolerance conflicts caused by polymer shrinkage.
Ask whether the quoted mold will be aluminum, P20 steel, 718 steel, H13 steel, S136 steel, or another specified grade. The right answer depends on expected production volume, resin abrasiveness, glass-fiber content, surface requirements, and maintenance expectations. A low-volume rapid tool may be economical for functional verification, while a hardened steel tool can be more appropriate for recurring production and demanding resins.
Supplier Evaluation AreaQuestions for Buyers to AskWhat a Strong Answer Looks LikePotential Warning SignDFM engineeringWill you provide a formal design-for-manufacturing review?Written comments on draft, gates, wall thickness, shrinkage, ejection, and tooling riskQuotation issued with no technical reviewMold ownershipWho owns the tool after payment, and how is it stored?Clear ownership clause, mold identification, maintenance terms, and release procedureVague language about tool access or transferMaterial controlCan you use the named resin grade and provide lot information if needed?Approved resin sourcing, documented substitutions only, retained material recordsUnapproved “equivalent” material changesQuality inspectionWhat checks are completed before shipment?First-article inspection, dimensional checks, visual standards, sampling plan, reportsNo inspection documentation beyond verbal confirmationTool trial processHow many trial rounds are included and what samples are supplied?Defined T1/T2 process, sample quantity, change-control pathway, approval recordUnclear sample responsibilities and revision chargesProduction capacityWhat machine tonnage and production scheduling apply?Machine fit, planned cycle time, capacity estimate, realistic lead-time commitmentCapacity promised without equipment detailsExport supportCan you manage packaging, documents, and shipment coordination?Export-ready packing, labeling review, shipping options, commercial documentationPackaging and shipping discussed only after productionFor Global Market projects, communication discipline is equally important. Insist that CAD revision numbers, approved samples, color standards, inspection reports, packaging instructions, and shipment details are controlled in writing. If a drawing changes after tooling begins, obtain a documented engineering change quotation and revised delivery schedule before approving the modification.
Plastic resin is a functional engineering choice, not merely a purchasing line item. ABS is widely used for housings and consumer products because it balances impact performance and appearance. Polycarbonate is often selected for impact resistance and transparency. Nylon provides strength and wear resistance but requires attention to moisture and shrinkage. Polypropylene supports chemical resistance and living hinges, while POM is useful for low-friction mechanical parts.
Buyers should define color with a physical chip, Pantone reference where appropriate, or a signed master sample. For cosmetic parts, specify acceptable flow lines, gate witness marks, ejector marks, gloss level, texture reference, weld line criteria, and allowable color variation. For functional components, prioritize critical dimensions, assembly interfaces, torque requirements, leak performance, pull-out force, and environmental resistance.
Material FamilyUseful PropertiesTypical UsesBuyer Specification NotesABSGood impact resistance, processability, cosmetic potentialEnclosures, appliance housings, consumer productsDefine color, surface texture, UV requirement, flame rating where neededPCHigh impact strength, heat resistance, transparency optionsProtective covers, electrical housings, lensesConfirm stress-crack resistance and transparency expectationsPC/ABSBalanced toughness, heat resistance, appearanceElectronics, automotive interior parts, instrument housingsSpecify required fire rating and cosmetic classPPLow density, chemical resistance, flexible hinge performanceContainers, caps, automotive trim, consumer productsAccount for larger shrinkage and possible warpagePA6 or PA66Strength, wear resistance, thermal performanceGears, clips, structural parts, automotive componentsState glass-fill level, moisture conditioning, and dimensional requirementsPOMLow friction, stiffness, good wear behaviorMechanisms, latches, gears, valvesReview snap geometry and tight tolerance zones carefullyTPE or TPUSoft-touch grip, flexibility, elastic recoveryHandles, seals, overmolded grips, protective elementsConfirm hardness, bond compatibility, color, and compression performanceQuality assurance should match the risk of the product. For a promotional consumer item, visual inspection and dimensional spot checks may be sufficient. For a device enclosure containing electrical components, buyers may require material flame ratings, fit validation, assembly trials, and more detailed records. Medical, automotive, aerospace, food-contact, and safety-related products may require additional documentation, process controls, traceability, or customer-specific validation. Never assume that a supplier’s general quality certification automatically certifies a finished part for a regulated end use.
China injection molding suppliers serve a broad industrial base. Consumer electronics manufacturers use molded cases, bezels, battery doors, cable organizers, and internal supports. Industrial equipment brands source sensor housings, protective covers, terminal blocks, handles, fan components, and control-panel parts. Medical product developers use molded components for diagnostic equipment, laboratory devices, handheld instruments, and non-implantable appliance housings.
Automotive and mobility projects frequently require clips, trims, ducts, brackets, connector bodies, housings, and interior components. These programs usually demand more disciplined material control, visual requirements, long-term mold durability, and stable production scheduling. Commercial product brands may need low-volume market launch parts, while established distributors may require repeatable replenishment orders, barcode labeling, retail-ready packaging, and consolidated international shipments.
China-based molding is also useful for startups and engineering teams that need a staged path from proof-of-concept to market release. The first stage may involve CNC machining or 3D printing for fit checks. The next stage can use vacuum casting or rapid tooling for functional testing. Once demand is confirmed, production tooling can be developed with optimized cavities, automation, and dedicated quality controls.
A product team developing a compact smart-device enclosure may begin with CNC-machined samples to confirm board fit, button travel, connector access, and assembly screws. After design approval, a rapid injection mold can produce small batches in PC/ABS for pilot users and early sales. Feedback from this phase can reveal issues with snap-fit fatigue, gate location, texture appearance, or packaging damage. The revised design can then move to a production mold when volume and specifications stabilize.
An industrial equipment company may require an IP-oriented plastic housing with brass threaded inserts, a gasket channel, mounting features, and resistance to shop-floor handling. The molder should review insert placement, weld lines near fastening points, draft on textured surfaces, shrinkage around thick bosses, and sealing-surface flatness. A first-article inspection should verify critical assembly interfaces before the customer commits to a production release.
A medical-device developer may need several hundred to several thousand molded housings for clinical evaluation or a controlled launch. This type of project benefits from detailed resin confirmation, controlled cosmetic standards, dimensional inspection records, and documented engineering changes. The buyer should also specify whether components need particular handling, labeling, packaging cleanliness, or traceability practices before shipment.
For aftermarket automotive accessories, molded trim pieces and mounting brackets often require a balance between appearance, heat resistance, and cost. The supplier should assess UV exposure, vehicle temperature conditions, clip retention, assembly variation, texture matching, and packaging protection. Production samples should be fitted to representative vehicles or fixtures before final production approval.
TEAM Rapid supports Global Market customers with an engineering-led manufacturing route from prototype through repeat production. Its ISO 9001:2015 quality management system, in-house machining and tooling capability, molding resources, and more than 10 years of experience help customers control the transition from CAD model to custom plastic component. Rather than claiming unspecified proprietary component brands, TEAM Rapid works to customer-defined resin grades, drawings, tolerances, and inspection requirements, supported by DFM analysis that addresses draft, wall thickness, resin consumption, cavity planning, cycle time, and potential tooling risks before production. With more than 6,000 delivered projects and over 500 customers in more than 25 countries, the company supports end users, distributors, dealers, brand owners, engineering firms, startups, and individual inventors through OEM, ODM, wholesale, prototype, low-volume, recurring-production, and regional distribution cooperation models. Its China-based manufacturing network, limited warehousing support, direct shipping capability, and experience serving customers launching products in China, the United States, the United Kingdom, France, Germany, and other markets provide practical international service continuity. Buyers receive one-to-one engineering communication, rapid online quotation and technical feedback, production updates, inspection coordination, packaging support, and after-sales follow-up rather than a disconnected remote-export transaction. TEAM Rapid can also coordinate turnkey and customer-owned production tooling solutions for customers building their own supply pathway; it does not operate BOO models or on-site bulk-supply services.
For projects requiring bridge production, TEAM Rapid’s China injection molding service combines rapid tooling, conventional molding, insert molding, overmolding, finishing, and assembly support. This approach is useful when a buyer needs to validate the market before investing in high-volume tooling, or when annual demand is too variable for a rigid mass-production model.
TEAM Rapid can support parts ranging from a single prototype to more than 100,000 pieces, depending on project requirements. Typical rapid tooling and molded-part production can be supported in approximately 5 to 25 days, while selected prototype processes may be completed more quickly. Customers can also combine injection molding with CNC machining, SLA or SLS 3D printing, vacuum casting, die casting, sheet metal fabrication, painting, plating, anodizing, assembly, kitting, blister packaging, clamshell sealing, poly bagging, shrink filming, and direct shipping.
There is no meaningful universal unit price for injection molded parts because the total cost is determined by mold complexity, material, annual volume, machine size, labor content, cycle time, finish requirements, inspection level, assembly, packaging, and logistics. Buyers should compare quotations using the same assumptions. A very low part price may rely on a lower-grade resin, fewer quality checks, a longer production schedule, or omitted packaging and freight costs.
Cost DriverHow It Affects PriceHow Buyers Can Control ItTrade-Off to UnderstandMold complexitySlides, lifters, unscrewing features, and complex ejection increase tool costSimplify undercuts and review DFM earlyLower tooling cost may require design changesCavity quantityMore cavities increase mold cost but can reduce unit costMatch cavities to realistic demand forecastsOverbuilding capacity ties up capitalResin gradeEngineering polymers and certified grades cost more than commodity plasticsSpecify performance requirements, not unnecessary premium gradesCheaper resin may affect safety or durabilityPart geometryThin walls, deep ribs, tight tolerances, and inserts raise processing difficultyUse uniform walls and practical tolerance zonesDesign simplification can affect aesthetics or functionSurface finishHigh polish, texture, painting, printing, and plating add labor and control needsApply premium finish only to visible areasReduced finishing can change brand appearanceProduction volumeHigher volumes spread tooling cost across more partsUse phased orders if demand is uncertainSmall batches usually have higher unit pricesFreight and packagingProtective packing, air freight, and destination duties affect landed costPlan carton density, shipping mode, and consolidation earlyCheapest packaging may increase damage riskFor commercial evaluation, ask suppliers to quote at several annual-volume tiers. For example, request pricing for pilot volume, low-volume production, and forecast production. This makes the effect of cavities, material ordering, setup time, and logistics visible before committing to a particular tool design.
A structured workflow protects both buyer and supplier. The process should begin with design review rather than a purchase order issued solely against a preliminary quotation. Tooling work should only begin after the technical file, commercial terms, mold concept, and revision status are agreed.
Project StageSupplier ActivityBuyer Approval PointTypical DeliverableRFQ reviewChecks CAD, drawing, resin, volume, and manufacturing risksConfirms commercial and technical scopeQuotation, initial DFM comments, lead-time estimateDFM and mold conceptDefines gates, parting line, ejection, cavity count, and mold structureApproves design direction before cutting steelDFM report and mold-flow-related recommendations where applicableTool manufacturingMachines mold components, performs EDM, polishing, fitting, and assemblyReceives progress updates for critical programsTooling schedule and production statusFirst trialMolds T1 samples and records process observationsReviews samples, dimensions, appearance, and assembly fitSample photos, inspection report, physical samplesTool correctionAdjusts tool based on approved engineering feedbackSigns off revised sample requirementsChange record and T2 sample planProduction releaseRuns approved parts under agreed process and inspection planApproves first article or pre-shipment standardProduction records, inspection report, packing detailsShipment and supportPackages, labels, prepares export documents, and coordinates dispatchConfirms shipping method and destination documentationCommercial invoice, packing list, shipment informationFor a new supplier relationship, a pilot order is often the most sensible first step. It enables the buyer to evaluate communication, dimensional consistency, cosmetic quality, packaging discipline, and schedule performance before placing a larger recurring order.
In 2026, the China injection molding sector is expected to continue moving toward faster engineering cycles, greater automation, more data-driven process control, and stronger sustainability expectations. Buyers will increasingly request digital DFM feedback earlier in development, especially for projects involving multiple product variants, tight launch windows, or expensive engineering resins.
Automation will remain important for stable high-volume programs. Robotic part handling, insert loading, in-mold labeling, automated visual inspection, and connected production monitoring can reduce handling variation and improve repeatability. However, automation should be selected based on production volume and product geometry; for low-volume or frequently changing programs, flexible manual or semi-automated cells can remain more economical.
Sustainability will affect resin selection, packaging design, and supplier evaluation. Global Market buyers may increasingly ask for recycled-content options, bio-based material alternatives, resin traceability, reduced packaging volume, reusable transit packaging, and better scrap management. These options must be technically verified because recycled or alternative materials can affect color, mechanical behavior, shrinkage, odor, regulatory status, and long-term consistency.
Policy and compliance pressures will also increase attention to product safety, chemical restrictions, packaging waste rules, carbon reporting requests, and supply-chain transparency. Buyers selling into Europe, North America, the United Kingdom, or other regulated markets should define their compliance requirements at the RFQ stage. A molder can support the manufacturing evidence requested, but the brand owner remains responsible for confirming that the complete finished product meets the applicable destination-market obligations.
Another trend is regional inventory planning. Rather than ordering a full year of stock, some buyers will use staged production and shipment schedules supported by limited warehousing, consolidated freight, and forecast-based replenishment. This model can reduce cash tied up in inventory while preserving the cost advantages of consolidated manufacturing in China.
Yes. Rapid tooling, aluminum tooling, and lower-cavity tools can make China injection molding practical for pilot runs, bridge production, startup launches, and low-volume industrial components. The best choice depends on part geometry, resin, finish, expected revisions, and forecast demand.
Lead time depends on mold size, complexity, material, surface finish, slides, lifters, cavity count, and revision cycles. TEAM Rapid can support certain tooling and molded-part projects in approximately 5 to 25 days, while complex production molds may require longer planning and validation.
Send a 3D CAD file in STEP, IGES, X_T, or another accepted format, plus a 2D drawing showing critical dimensions and tolerances. Include resin grade, color, annual volume, finish requirements, assembly details, packaging needs, and target delivery country.
Many China injection molding suppliers can provide both services. This is often beneficial because the same engineering team can connect mold design decisions with molding performance, part quality, maintenance, and future revisions.
Use a purchase order and tooling agreement that states the buyer owns the mold after agreed payment, identifies the mold with a unique number, defines storage and maintenance terms, and explains the procedure for tool release or transfer if required.
Request documents appropriate to the product risk, such as a first-article inspection report, dimensional inspection report, material confirmation where required, approved color or cosmetic standard, packing list, and pre-shipment photos. Regulated products may require additional customer-defined documentation.
Yes. Buyers can submit CAD models, drawings, material requirements, expected quantities, finishing needs, and destination details through the TEAM Rapid quotation request page. The team can review manufacturability and recommend a suitable route from rapid prototype and tooling through injection molding, finishing, assembly, packaging, and shipment.
-
Global Market Guide to Plastic Injection Molding Partners
For the global market, choose a plastic injection molding partner that can prove its tooling capability, resin traceability, quality-control process, engineering support, production capacity, and export reliability before you commit to a mold. The best choice is not always the lowest quoted unit price; it is the supplier that reduces total risk across DFM review, mold construction, sampling, inspection, packaging, shipping, and repeat orders.
Start with suppliers that have a documented quality system, clear mold ownership terms, measurable dimensional-control procedures, and experience serving your industry. For global programs, prioritize companies that can support prototype validation, bridge tooling, low-volume molding, and scalable production without forcing a supplier change at every stage.
Well-known international manufacturers worth considering include TEAM Rapid in China, Protolabs in the United States and Europe, Xometry in the United States and Europe, Rosti in Europe and Asia, EVCO Plastics in North America, and Nypro, a Jabil company, across global manufacturing markets. Qualified Chinese manufacturing partners can also be a strong option when they combine internationally recognized quality practices, responsive pre-sales and after-sales support, export experience, and competitive cost performance.
Before placing a production order, request a DFM report, material specification, preliminary mold-flow assumptions where applicable, sample inspection plan, tolerance confirmation, packaging proposal, production lead time, and shipping terms. These documents reveal much more than a quotation alone.
Injection molding is a repeatable manufacturing process, but repeatability only appears when the mold, material, machine settings, process controls, and inspection methods work together. A supplier may produce an attractive first sample while still being unable to maintain the same dimensions, appearance, and assembly fit over thousands of cycles. This is why global buyers should evaluate the complete manufacturing system rather than choosing only on mold price or quoted cycle time.
The global market has made supplier selection more complex and more flexible. Product teams in Berlin, London, Chicago, Singapore, Dubai, Sydney, Shenzhen, and Toronto can source molded parts from several regions, compare tooling costs, and manage projects through digital collaboration. At the same time, distance adds requirements around technical communication, customs paperwork, logistics planning, part protection, supplier responsiveness, and corrective-action support.
Global trade routes also shape the decision. Manufacturers near Shenzhen, Dongguan, Ningbo, Shanghai, and Hong Kong can provide efficient access to major Chinese export hubs. European buyers may value local production near Germany, the Czech Republic, Poland, France, or the United Kingdom for shorter transport distances. North American buyers may prefer molding near Chicago, Milwaukee, Monterrey, Atlanta, or Southern California when demand is volatile or when domestic replenishment is important. The right region depends on demand volume, part complexity, local-content expectations, speed requirements, and total landed cost.
A capable plastic molding manufacturer should help you make decisions before tooling begins. It should identify weak ribs, undercuts, sharp corners, insufficient draft, inconsistent wall thickness, unrealistic tolerances, and difficult cosmetic surfaces. Good supplier involvement at this stage can eliminate expensive tool modifications later.
A dependable molding source should provide more than press time. For most engineered products, the preferred partner is able to support design-for-manufacturing analysis, mold design, steel selection, mold machining, molding trials, dimensional inspection, finishing, assembly, and international shipping. The exact range of services will vary, but a coordinated process reduces handoffs and helps control accountability.
Ask whether the supplier can support both development and production. A startup may need ten prototype parts for a fit check, then 500 units for a pilot launch, followed by 20,000 units after market validation. An established manufacturer may require recurring orders with stable quality documentation. A supplier that can accommodate each phase helps avoid costly requalification when demand changes.
CapabilityWhy It MattersWhat to Ask the SupplierDFM engineering reviewPrevents avoidable mold changes, warpage, sink marks, and difficult ejection.Will you provide a written DFM report before mold approval?Tooling design and manufactureTool design determines part consistency, maintenance needs, and production speed.What steel, gate system, cooling design, and expected mold life are proposed?Material controlResin grade, drying, additives, and color control affect performance and appearance.Can you provide resin grade confirmation and material traceability?Process validationDocumented settings improve repeatability during production and reorders.How are first articles, process parameters, and change controls managed?Inspection capabilityMeasurement verifies critical dimensions, cosmetic quality, and assembly function.Which inspection tools and sampling plans apply to my part?Assembly and packagingIntegrated downstream work reduces handling errors and supply-chain complexity.Can you perform inserts, labeling, kitting, final assembly, and export packaging?Export logistics supportReliable documentation and packing prevent delays at ports and destination customs.Which Incoterms, shipping options, and export documents can you support?This capability checklist is useful because each item affects the total project outcome. For example, a low-cost mold with inadequate cooling may produce a longer cycle time, unstable dimensions, and higher unit costs for the life of the program. Similarly, a supplier without material traceability may create compliance or product-liability problems if a resin substitution occurs without approval.
Plastic injection molding supports a wide range of product categories, from simple caps and clips to technical housings, medical device components, electrical enclosures, automotive interior parts, industrial covers, trays, handles, structural brackets, and consumer-product shells. The process is suitable when a part requires repeatable geometry, a consistent surface finish, and scalable unit economics.
Product requirements determine the best molding method. Standard single-shot molding is often sufficient for a basic housing or bracket. Insert molding is appropriate when threaded inserts, terminals, pins, or other components must be permanently captured in plastic. Overmolding is used when a soft thermoplastic elastomer grip is molded over a rigid substrate. Family molds can produce related components in one tool, while multi-cavity tools increase output for stable, high-volume demand.
Process TypeTypical ProductsMain AdvantageImportant Buying ConsiderationSingle-shot injection moldingHousings, covers, clips, containers, bracketsEfficient option for most rigid thermoplastic components.Confirm draft angle, wall thickness, gate location, and cosmetic-surface requirements.Rapid toolingPilot-run parts, market-test products, bridge-production componentsShortens the path from design validation to limited production.Confirm expected tool life and whether the tool is suitable for future scale-up.Insert moldingThreaded inserts, electrical connectors, metal-reinforced componentsReduces secondary assembly and improves retention.Specify insert tolerances, loading method, pull-out requirements, and inspection points.OvermoldingSoft-touch grips, sealed interfaces, ergonomic handlesCombines rigid and flexible materials in one component.Verify material bonding compatibility and substrate handling during molding.Multi-cavity moldingCaps, fittings, small consumer parts, high-volume componentsRaises output and can reduce per-part cost at scale.Balance cavity filling and define cavity-specific quality monitoring.Family moldingMatched product sets, enclosure halves, small assembliesCan reduce initial tooling investment for related parts.Evaluate fill balance because different part sizes may affect consistency.Two-shot moldingSealed buttons, dual-color components, functional gripsCreates multi-material parts with fewer assembly steps.Assess tooling complexity, cycle time, and material compatibility early.Material selection is equally important. ABS is commonly used for durable consumer housings. Polycarbonate offers impact resistance and dimensional stability. Polypropylene is valued for chemical resistance and living hinges. Nylon can provide strength and wear resistance, while glass-filled nylon supports more demanding structural applications. POM is often chosen for low-friction moving components. TPU and TPE are useful for flexible grips, seals, and protective features. Medical, food-contact, flame-retardant, UV-stabilized, recycled-content, and electrically conductive grades require additional documentation and process care.
The companies below illustrate different sourcing models available to international buyers. Some specialize in rapid production and digital quoting, while others operate large-scale production networks for regulated or high-volume programs. Suitability depends on part design, annual volume, regulatory requirements, budget, and desired geographic footprint.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidGlobal customers, with manufacturing resources in China and export support to North America, Europe, Asia, and other marketsRapid tooling, engineering-led DFM support, low-volume to production-scale flexibility, competitive China-based manufacturing costsInjection molding, insert molding, overmolding, CNC machining, 3D printing, vacuum casting, finishing, assembly, packaging, and direct shippingProtolabsNorth America and EuropeFast digital manufacturing workflow and rapid production support for product development teamsInjection molding, CNC machining, sheet metal fabrication, and 3D printingXometryUnited States, Europe, and broad partner-network coverageLarge manufacturing network and online sourcing platform for diverse part requirementsInjection molding, CNC machining, 3D printing, sheet metal, urethane casting, and finishingRostiEurope, Asia, and North AmericaTechnical polymer molding, complex assembly, and support for industrial and consumer programsInjection molding, multi-shot molding, assembly, supply-chain services, and product industrializationEVCO PlasticsNorth America, with international customer supportLarge-part and custom injection molding experience with broad resin-processing capabilityCustom molding, tooling support, engineering, assembly, decorating, and logistics servicesNypro, a Jabil CompanyGlobal manufacturing locations across major marketsComplex, high-volume programs and regulated-product manufacturing within a large global organizationPrecision molding, healthcare manufacturing support, automation, assembly, and supply-chain integrationICOMoldUnited States-focused sourcing with overseas manufacturing optionsAccessible custom molding programs for startups, product developers, and small-to-medium production requirementsCustom injection molding, prototype tooling, production tooling, and mold-related servicesThis comparison should be treated as a starting point rather than a final supplier shortlist. A large global manufacturer may be ideal for a regulated, high-volume medical program, while a flexible rapid manufacturer may be better for a product launch involving several iterations, low initial volume, and a need for combined CNC, molding, finishing, and assembly services.
Injection molding quotations are often difficult to compare because suppliers may include different assumptions. One quotation may include a hardened steel mold, hot runner, spare inserts, first article inspection, and export packaging. Another may quote a lower initial cost but exclude engineering changes, texture, inspection reports, mold maintenance, shipment preparation, or even the final resin grade. Ask every supplier to quote against the same technical package.
The most useful quote package includes a 3D CAD model, 2D drawing with critical dimensions, annual quantity estimate, target resin and color, cosmetic requirements, material compliance needs, expected use environment, preferred mold life, packaging specifications, and destination location. If the design is not finalized, ask for a DFM-led preliminary quote and clearly mark the tooling assumptions.
Quote ElementQuestions to AskRisk if Not ClarifiedMold constructionIs the tool aluminum, pre-hardened steel, or hardened steel? Is it single cavity or multi-cavity?Unexpected limits on tool life, quality consistency, or output capacity.Mold ownershipWho owns the mold after payment? Can it be transferred? Where will it be stored?Disputes over future production rights and tool access.Material gradeWhat exact resin manufacturer, grade, color specification, and additive package are included?Performance variation, certification issues, or unauthorized substitutions.Part tolerancesWhich dimensions are critical, and what process capability is expected?Assembly failures caused by unrealistic or undocumented requirements.Sampling and inspectionHow many first articles are included, and what reports will be supplied?Unclear acceptance criteria and delayed production approval.Secondary operationsAre printing, painting, ultrasonic welding, insert installation, or assembly included?Hidden costs and multiple-supplier coordination problems.Lead timeDoes the timeline begin after DFM approval, deposit, material arrival, or final design freeze?Incorrect launch planning and missed market windows.Shipping termsIs pricing EXW, FOB, CIF, DDP, or another Incoterm? Who manages duties and customs clearance?Surprise landed costs and avoidable logistics delays.Cost should be evaluated across tooling cost, piece price, scrap rate, inspection burden, transport cost, import duties, inventory carrying cost, and the financial impact of delayed market entry. A supplier offering faster tooling and strong DFM support may reduce total cost even if its initial quote is not the lowest.
Begin by classifying your program. A prototype or market-validation project needs speed and flexibility. A low-volume industrial product needs reliable tooling, tight tolerances, and controlled change management. A high-volume consumer product needs multi-cavity tooling, cycle-time optimization, reliable resin supply, and predictable shipping. A medical or automotive component requires added attention to material control, documentation, traceability, validation, and process discipline.
Then evaluate suppliers through direct technical communication. A useful test is to send a realistic CAD file and ask for a DFM response. Strong engineers will identify parting-line implications, draft concerns, gate positions, ejector-pin marks, weld-line risks, sink areas, steel-safe dimensions, undercuts, material concerns, and proposed revisions. A vague response that only repeats your requested quantity is a warning sign.
Use a phased approach when possible. Start with a prototype or rapid-tooling stage, inspect the samples, test the assembly, gather user feedback, and confirm the design before investing in high-cavitation production tooling. This approach is particularly valuable for startups, brand owners, and companies entering new markets where demand forecasts are uncertain.
Buyers should also ask about communication coverage. Global projects often involve design teams in one time zone, procurement in another, and end markets in a third. A supplier that provides prompt engineering feedback, organized records, clear approval gates, and named project contacts can prevent a small technical question from becoming a weeks-long delay.
Injection molding is used across nearly every product category that requires repeated plastic parts. Automotive applications include interior trim, switch housings, air-duct components, sensor enclosures, clips, under-hood parts, and lighting-related assemblies. Consumer products include appliance components, personal-care packaging, toys, tools, sporting goods, kitchenware, and electronic-device cases.
In medical-device manufacturing, the process supports equipment housings, handheld diagnostic-device components, instrument covers, trays, handles, and selected single-use products when appropriate material and quality requirements are met. Industrial equipment uses molded guards, control-panel housings, cable-management components, fixtures, fittings, machine covers, and durable brackets. Communications and electrical products rely on precision enclosures, connector-related components, battery housings, and protective shells.
The best supplier will understand the practical requirements of your sector. Automotive buyers may prioritize durability, cosmetic consistency, and long-term production control. Medical customers may need tighter documentation and material controls. Consumer brands may emphasize color matching, tactile finish, premium appearance, packaging, and launch speed. Industrial customers may focus on functional tolerances, chemical resistance, UV resistance, and economical low-volume production.
Typical custom molded parts include cases, enclosures, trays, covers, housings, fillers, bezels, clips, retainers, knobs, handles, brackets, caps, containers, and functional mechanical components. Most parts benefit from uniform walls, adequate draft, rounded internal corners, practical rib geometry, and carefully selected gate locations. A part that looks simple in CAD may become difficult to mold if it contains deep ribs, unsupported walls, hidden undercuts, or highly polished cosmetic faces near the gate.
For enclosures, define which exterior surfaces are customer-facing and whether visible ejector-pin marks, gate vestiges, parting lines, flow lines, or weld lines are acceptable. For mechanical components, identify the dimensions that control assembly fit and clarify how those dimensions will be inspected. For threaded interfaces, consider whether molded threads, metal inserts, or post-machining offer the best long-term performance.
For outdoor products, specify UV exposure, temperature range, moisture conditions, and expected service life. For electrical applications, identify flame-retardancy, insulation, conductivity, or shielding needs. For wearable or handheld products, consider texture, grip, skin-contact requirements, drop resistance, and aesthetic expectations. Clear application information enables a supplier to recommend better materials and more suitable tooling solutions.
A consumer electronics startup developing a handheld device may begin with CNC-machined prototypes to validate assembly and ergonomics. Once the design stabilizes, rapid tooling can produce several hundred molded housings for beta units and market testing. After feedback confirms the design, the company can move to production tooling with optimized gates, texture, and multi-cavity output. This pathway reduces the risk of paying for a production mold before the product has been tested in the field.
An industrial equipment manufacturer may need 2,000 chemical-resistant covers per year, with periodic design updates. In this case, a flexible manufacturer with DFM support, low-volume molding capability, and machining resources may provide better value than a high-volume-only supplier. The buyer should focus on resin compatibility, critical mounting dimensions, insert retention, packaging protection, and reorder consistency.
A global brand launching a consumer appliance accessory may require a polished surface, color control, barcode labeling, retail packaging, and shipment to several regional distribution centers. The preferred supplier should be able to coordinate molding, cosmetic finishing, assembly, kitting, packaging, quality checks, and direct international shipping. Managing these steps through one accountable manufacturing partner can reduce the risk of mismatched parts and packaging delays.
A medical-equipment developer may need a small batch of instrument housings with stable fit around internal electronics. The supplier should support careful DFM review, prototype testing, controlled resin selection, dimensional reports, and documented change approval. The focus is not merely producing a visually acceptable shell; it is producing parts that assemble predictably and support the final device’s functional requirements.
North American molding providers can offer shorter domestic transit times, easier on-site communication, and familiar regulatory or purchasing processes for buyers based in the United States, Canada, and Mexico. They may be especially suitable where local manufacturing, frequent engineering changes, or rapid replenishment is a priority. Cities such as Chicago, Milwaukee, Detroit, Monterrey, and Los Angeles remain important manufacturing and logistics areas for molded-product programs.
European providers offer advantages for buyers serving markets in Germany, France, the United Kingdom, Italy, the Netherlands, Poland, and the Nordic countries. European sourcing can simplify regional distribution and reduce transport time for products sold through EU or UK channels. Manufacturers close to ports such as Rotterdam, Hamburg, Antwerp-Bruges, and Felixstowe can also support efficient international shipment planning.
Chinese suppliers are highly relevant for global buyers seeking fast tooling, broad process coverage, cost-efficient production, and flexible low-volume manufacturing. Manufacturing centers around Shenzhen, Dongguan, Ningbo, Suzhou, Shanghai, and Xiamen have developed strong ecosystems for tooling, molding, machining, finishing, assembly, and export logistics. The key is to select a supplier with proven engineering communication, defined quality procedures, clear mold ownership, and transparent production controls rather than choosing solely by the lowest online price.
TEAM Rapid supports global product teams with an engineering-led route from prototypes to repeat production, combining in-house machining, tooling manufacturing, molding capability, and an integrated China-based manufacturing resource network. Its ISO 9001:2015 quality-management certification, detailed DFM reports, manufacturability analysis, tight CNC tolerance capability down to 0.01 mm, controlled material options, and inspection-focused production process provide practical evidence for customers needing reliable custom plastic and metal parts. The company serves end users, distributors, dealers, brand owners, startups, engineers, and individual product developers through flexible OEM, ODM, wholesale, retail, regional distribution, and project-based manufacturing models, from one prototype to more than 100,000 parts. TEAM Rapid has delivered more than 6,000 projects for over 500 customers in more than 25 countries, including customers connected to the United States, United Kingdom, France, Germany, China, and other global markets. Its service assurance is built around rapid online engineering response within a few hours, direct project communication, export-ready packaging and shipping support, and coordinated offline manufacturing operations in China rather than fragmented supplier handoffs. It offers EPC, turnkey, and customer-owned plant solution support where relevant to manufacturing projects, and does not operate BOO or on-site bulk supply services. This operating model gives international buyers a practical long-term manufacturing partner with proven export experience, responsive pre-sales and after-sales coordination, and a clear pathway from design review through delivery.
For projects requiring a fast transition from design to molded components, TEAM Rapid can support rapid tooling and molded-part production in approximately 5 to 25 days depending on design, material, tooling complexity, and order quantity. The company also offers 3D printing, vacuum casting, CNC machining, die casting, sheet metal fabrication, finishing, assembly, procurement support, limited warehousing, packaging, kitting, and direct shipping. This integrated model is useful when a product contains both plastic and metal components or when a buyer wants to avoid managing multiple disconnected vendors.
Customers can explore custom injection molding services for global product programs when they need rapid tooling, insert molding, overmolding, or repeat production support. For an initial manufacturing review, buyers can also request a tailored molding quotation with CAD files, material preferences, target quantities, and destination requirements.
By 2026, injection molding procurement will increasingly be shaped by faster digital engineering, higher traceability expectations, material sustainability, and regional supply-chain resilience. Buyers will expect suppliers to provide earlier design feedback, more transparent production status, and better documentation around materials, inspection, and change control.
Artificial intelligence-assisted DFM tools and process-monitoring systems will help manufacturers identify potential warpage, filling imbalance, sink marks, and cycle-time inefficiencies earlier. These systems will not replace experienced mold designers or process engineers, but they can speed up technical reviews and help teams compare design alternatives before steel is cut.
Sustainability will remain a major purchasing factor. More customers will request recycled-content resins, bio-based materials, mono-material designs that improve recyclability, lower-packaging waste, and reduced energy use per part. However, sustainability claims must be tested against real product requirements. Recycled-content resin may behave differently from virgin material, and manufacturers should verify mechanical properties, color consistency, odor, moisture sensitivity, and regulatory suitability before approving it for production.
Policy trends will also affect supplier selection. Product traceability, chemical compliance, packaging rules, extended producer responsibility programs, and carbon-reporting requirements are likely to influence material documentation and supply-chain reporting. Global buyers should prepare by requesting clearer resin records, country-of-origin information, packing data, and documented change-control procedures.
Another 2026 trend is the continued use of hybrid sourcing models. Companies may develop tooling in one region, produce initial batches in another, and maintain a secondary source for resilience. This can reduce disruption risk, but it requires disciplined mold documentation, compatible material specifications, shared inspection criteria, and clear intellectual-property protections.
Compare total landed cost, engineering communication, lead time, production volume, quality requirements, logistics risk, and the need for local inventory. Local suppliers may offer shorter transport times and easier in-person collaboration. Overseas suppliers can offer strong cost performance and broad manufacturing capability when they provide reliable engineering support, quality controls, and export coordination.
Send a 3D CAD model, 2D drawing when available, target material, color, annual quantity, critical dimensions, surface-finish requirements, assembly details, packaging needs, destination country, and expected launch date. State whether the project is prototype, pilot production, or full production.
Lead time depends on mold size, number of cavities, steel selection, undercuts, surface texture, required tolerances, and supplier workload. Simple rapid tooling can be completed relatively quickly, while hardened multi-cavity production molds require more time for design, machining, fitting, sampling, and validation.
Mold ownership should be written into the purchase agreement. Clarify whether the buyer owns the mold after payment, where the tool is stored, how maintenance is handled, whether the supplier can use it only for authorized production, and what happens if the buyer requests transfer.
Yes. Rapid tooling, simplified mold designs, and carefully chosen cavity counts can make molding practical for pilot runs and low-volume programs. The best approach depends on the part geometry, expected design changes, desired material, and forecast demand. For very low quantities, CNC machining, 3D printing, or vacuum casting may be more appropriate.
Request the DFM report, material specification, first article inspection report, dimensional inspection results for critical features, appearance approval standards, change-control process, and packing details. Regulated applications may require additional documentation depending on the product and destination market.
Improve the design before tooling by using consistent wall thickness, adequate draft, practical tolerances, minimized undercuts, and material choices matched to the real application. Consider cavity count carefully, avoid unnecessary cosmetic requirements, and select a supplier that can identify cost-saving DFM opportunities before mold construction.
Before approving your molding partner, confirm that the supplier understands the application, has reviewed the part for manufacturability, can provide the required resin and quality documentation, has defined mold ownership, and can meet the real delivery schedule. Verify that its production capacity matches your expected volume and that it can handle inspection, finishing, assembly, packaging, and shipping requirements.
A successful global injection molding project depends on early engineering alignment and clear commercial terms. Select the supplier that communicates openly, documents assumptions, protects your tooling and design requirements, and provides a scalable path from prototype to production. That approach creates better parts, more stable supply, lower lifecycle cost, and a smoother route to market.



-
Global Market Injection-Molded Part Wall Gauge Guide
For most injection-molded plastic parts in the global market, start with a uniform wall gauge between 1.5 mm and 3.0 mm, then adjust it according to resin flow behavior, impact requirements, cosmetic expectations, mold design, and production volume. Commodity plastics such as polypropylene and polyethylene can often use thinner sections, while engineering materials such as polycarbonate, nylon, PBT, and ABS/PC blends usually need more carefully controlled wall thickness to prevent incomplete filling, sink marks, warpage, and internal stress.
The most important rule is consistency. Keep adjacent wall sections within approximately 10% to 15% of each other whenever possible. Instead of making one area excessively thick for stiffness, use ribs, gussets, structural webs, and rounded transitions. Thick plastic sections cool slowly, increase cycle time, consume more resin, and create a greater risk of sink marks or voids.
For a practical global sourcing strategy, compare established molders with strong DFM capability in China, North America, Europe, and Southeast Asia. Qualified international suppliers, including Chinese manufacturers with ISO certifications, engineering support, fast communication, and reliable pre-sales and after-sales processes, can offer strong cost-performance advantages for prototypes, bridge tooling, low-volume production, and scaled manufacturing.
Before releasing tooling, request a wall-thickness analysis, mold-flow review where appropriate, and a written DFM report that identifies thick zones, fill-risk areas, weld lines, gate locations, ribs, bosses, draft, and material-specific shrinkage behavior.
Wall thickness is one of the most influential design variables in plastic injection molding. It affects filling pressure, mold cost, cycle time, dimensional accuracy, resin consumption, cooling balance, cosmetic quality, and long-term mechanical performance. A part that looks simple in CAD can become difficult or expensive to mold if its wall gauge changes abruptly, contains large thick areas, or combines thin cosmetic surfaces with heavy structural features.
During the molding cycle, molten polymer enters the mold cavity through the gate and travels through runners or hot-runner channels. The melt begins cooling as soon as it contacts the steel cavity. Thin sections freeze sooner, while thicker sections remain molten longer. If a thin section is placed ahead of a thick section in the flow path, the melt may freeze before packing pressure can compensate for shrinkage. This can lead to short shots, weak weld lines, sink marks, voids, or inconsistent dimensions.
For buyers sourcing parts across Shenzhen, Dongguan, Ningbo, Suzhou, Chicago, Monterrey, Stuttgart, Birmingham, Singapore, and other manufacturing hubs, the core engineering principle remains the same: design for balanced flow and balanced cooling. The exact wall gauge may change by resin and application, but uniformity provides the strongest foundation for predictable production.
Wall gauge also has a direct commercial impact. Increasing a nominal wall from 2.0 mm to 3.0 mm does not simply increase resin usage by 50%. It may extend cooling time significantly, reduce the number of parts produced per hour, require a larger molding machine, increase tool temperature control demands, and affect freight cost. For high-volume programs, a small reduction in wall thickness can generate meaningful savings. For low-volume programs, stable molding and shorter lead time may be more valuable than minimizing every gram of resin.
The following values are practical starting ranges rather than universal specifications. Final wall thickness should be confirmed using the resin supplier’s technical data, part geometry, gate position, flow length, mold temperature, surface finish, reinforcement level, and end-use load requirements. Glass-filled resins, flame-retardant grades, recycled-content grades, and highly filled compounds may require different decisions from standard unfilled grades.
MaterialTypical Wall Gauge RangePreferred Design RangeMain Design ConsiderationCommon ApplicationsPolypropylene (PP)0.8 mm to 3.0 mm1.2 mm to 2.5 mmHigh shrinkage requires consistent sections and careful rib design.Containers, living hinges, automotive trim, caps, household productsHigh-Density Polyethylene (HDPE)0.8 mm to 3.5 mm1.5 mm to 3.0 mmGood chemical resistance but can warp with uneven cooling.Bottles, packaging, tanks, industrial covers, consumer goodsABS1.2 mm to 4.0 mm1.8 mm to 3.0 mmPopular for cosmetic housings; avoid thick zones that create sink.Electronics housings, appliance covers, automotive interiorsPolycarbonate (PC)1.0 mm to 4.0 mm1.5 mm to 3.0 mmHigh strength but higher viscosity; long flow paths need attention.Safety covers, transparent lenses, medical housings, electrical partsPC/ABS Blend1.2 mm to 4.0 mm1.8 mm to 3.2 mmBalances toughness and appearance; common for enclosure design.Consumer electronics, automotive bezels, industrial enclosuresNylon PA6/PA660.8 mm to 4.0 mm1.5 mm to 3.0 mmMoisture absorption and glass reinforcement affect shrinkage.Gears, clips, brackets, under-hood automotive componentsPBT0.8 mm to 3.0 mm1.5 mm to 2.5 mmUseful for electrical performance; reinforced grades need balanced flow.Connectors, switches, electrical housings, sensor componentsAcetal POM0.8 mm to 3.0 mm1.5 mm to 2.5 mmLow friction and high stiffness; control shrinkage and gate design.Gears, valves, latches, precision mechanical componentsThese ranges show why material selection and wall design must be evaluated together. For example, a 1.2 mm wall may be practical for a compact polypropylene clip but may be risky for a long-flow PC/ABS enclosure. Similarly, a nylon bracket can carry high loads with relatively moderate wall thickness when ribs and fiber orientation are properly considered. Simply making the bracket thicker may not improve performance if warpage increases or glass fibers align unfavorably.
Uniform walls are not always possible, especially in parts that include attachment points, snap fits, bosses, sealing features, reinforced corners, or ergonomic surfaces. The goal is not perfect uniformity at every point; it is gradual transition and controlled thermal mass. Designers should avoid isolated heavy sections surrounded by thin walls because the heavy section will cool more slowly and shrink more after ejection.
A common approach is to define a nominal wall thickness, often called “T,” and create supporting features in relation to that dimension. Ribs are typically designed at 40% to 60% of the nominal wall thickness. Boss walls are often kept around 60% of nominal wall thickness, with ribs added for support. Corner transitions should use radii instead of sharp edges, and thick-to-thin transitions should be tapered over a reasonable distance.
FeatureRecommended Relationship to Nominal WallPurposeRisk if OversizedUseful Design PracticeRib thickness40% to 60% of TAdd stiffness without making the main wall thicker.Sink marks and read-through on cosmetic surfaces.Use generous draft and rounded rib bases.Boss wall thickness50% to 70% of TSupport screws, inserts, and locating pins.Voids, sinks, and cracking near the base.Connect bosses to walls with gussets.Rib heightUp to 2.5 to 3.0 times TIncrease bending stiffness.Fill problems, weak rib tips, difficult ejection.Use multiple lower ribs instead of one very tall rib.Corner radiusMinimum 0.25 to 0.50 times TImprove flow and reduce stress concentration.Cracking and uneven filling at sharp internal corners.Maintain consistent inside and outside radius relationships.Wall transitionGradual taper over distanceBalance cooling and packing.Warping, sinks, and dimensional variation.Use tapered steps instead of abrupt section changes.Draft angleUsually 0.5° to 2° or moreEnable clean ejection and protect surfaces.Scuffing, sticking, ejector damage, cosmetic defects.Increase draft for textured surfaces.Ribs are especially important for housings, trays, covers, and structural plastic components. A rib can increase stiffness substantially because bending stiffness depends heavily on section depth. This means a well-designed ribbed wall can outperform a thick, flat wall while using less material and cooling more quickly. However, ribs must be positioned thoughtfully. Ribs directly behind high-gloss exterior surfaces can create visible sink marks, especially in ABS, PC/ABS, polypropylene, and unfilled nylon.
Design teams should also consider how a part will be measured. A thick-walled part may experience post-molding shrinkage after it leaves the tool, and a large flat panel can bend as residual stresses relax. If the part must mate with another component, define critical interfaces clearly and allow the molder to recommend process controls, fixture inspection, or secondary calibration methods.
The relationship between flow length and wall thickness is central to moldability. Longer melt flow paths require more pressure and are more vulnerable to premature freezing. Thin walls can be molded successfully when gates are positioned close to the critical areas, the material has adequate flow, mold temperatures are controlled, and the part geometry is designed for uniform filling. In contrast, a thin wall combined with a long flow path, multiple turns, texture, and glass-filled resin can create a difficult molding condition.
Gate location should support the thickest functional region or allow the melt to flow from thick to thin wherever possible. A gate positioned into a thin edge may cause hesitation as the melt reaches thicker features downstream. This can produce visible flow lines, weak weld lines, and poor packing. For large enclosures and trays, multiple gates or hot-runner systems may be needed to control pressure and cycle time, but gate marks, weld lines, and tooling cost should be evaluated early.
In projects requiring cosmetic surfaces, the gate must also be selected with appearance in mind. Hidden edges, internal walls, underside surfaces, and assembly interfaces are commonly preferred. Tunnel gates, edge gates, fan gates, valve gates, and direct sprue gates each have different effects on flow behavior and visible finishing requirements.
DefectTypical Wall-Related CauseVisual or Functional EffectPreferred Corrective ActionSecondary Process AdjustmentSink marksThick ribs, bosses, corners, or concentrated material mass.Depressed areas on visible surfaces.Core out thick areas and reduce rib thickness.Increase packing pressure or hold time where appropriate.WarpingUneven cooling, uneven wall gauge, fiber orientation.Twist, bowing, poor assembly fit.Balance wall sections and add structural ribs strategically.Adjust mold temperature and cooling channels.Short shotThin wall, long flow path, insufficient gate size.Incomplete part fill.Increase local gauge or improve gate location.Raise injection speed, pressure, or melt temperature carefully.VoidsHeavy sections shrink internally after the skin freezes.Internal bubbles and reduced structural integrity.Reduce material concentration and improve packing path.Optimize hold pressure and cooling time.Weld line weaknessFlow fronts meet after cooling in thin or distant areas.Visible seam or low-strength area.Move gate or increase local wall gauge slightly.Increase mold temperature to improve knit quality.Burn marksAir trapped near end-of-fill areas, often in thin sections.Dark or scorched appearance.Add venting and improve flow path design.Reduce injection speed near end fill if necessary.Design correction should normally come before process correction. It is possible to mask some defects by adjusting packing pressure, melt temperature, injection speed, cooling time, or mold temperature. However, process changes cannot fully compensate for poor geometry. A stable production tool should not rely on an extremely narrow molding window. If one minor temperature variation causes warpage or sinks, the part design needs further engineering attention.
For global programs involving multiple production sites, stable geometry is especially valuable. A design that only runs well on one specific machine with one experienced operator can be difficult to transfer. Balanced walls, reasonable tolerances, clear resin specifications, and documented molding parameters improve repeatability across qualified facilities.
Plastic enclosures commonly use ABS, PC/ABS, polycarbonate, or polypropylene. These parts need careful control of cosmetic surfaces, screw bosses, snap fits, vents, and internal ribs. A typical handheld enclosure may use a nominal wall between 1.5 mm and 2.5 mm, depending on resin and product size. Thin consumer electronics housings can be lighter and more attractive, but they may require higher-quality tooling, more precise gating, and more demanding process control.
Automotive components often require higher impact resistance, temperature resistance, chemical resistance, and dimensional stability. Interior trim parts may use polypropylene, TPO, ABS, PC/ABS, or reinforced compounds. Under-hood parts often use glass-filled nylon, PBT, PPS, or other engineering thermoplastics. Because vehicle components may experience vibration, thermal cycling, and loading, rib design and fiber orientation can be as important as nominal wall gauge.
Medical device housings need a combination of strength, cleanability, chemical resistance, appearance, and regulatory material traceability. Polycarbonate, ABS, PC/ABS, medical-grade polypropylene, and certain nylon or PBT grades are common choices. Wall thickness should support reliable assembly, sterilization requirements where applicable, and consistent molded dimensions.
Packaging products often use thinner walls to reduce resin usage and improve cycle time. Thin-wall packaging requires a high-flow resin, high-speed molding machine, optimized gate system, precise mold cooling, and experienced process control. A food container, cap, or lid may be much thinner than an industrial housing, but the engineering complexity can be greater because the process window is narrower.
Buyers should avoid requesting a mold quote based only on a 3D file. A reliable quotation requires the part material, annual quantity, target market, cosmetic expectations, tolerance requirements, color, texture, assembly method, packaging needs, and delivery location. If the product is still under development, request a DFM review before committing to hardened production tooling.
For early-stage programs, rapid tooling can be an effective bridge between prototype testing and mass production. It allows teams to validate part performance, assembly, appearance, and real material behavior before investing in multi-cavity hardened molds. Low-volume tooling is particularly useful for startups, industrial equipment makers, medical-device developers, automotive aftermarket brands, and consumer-product teams testing demand.
When comparing suppliers, evaluate total landed value rather than tool price alone. A lower mold quote can become expensive if the supplier does not provide DFM support, uses unsuitable steel, lacks inspection discipline, has inconsistent communication, or cannot manage engineering changes. Conversely, a slightly higher upfront engineering investment may reduce failures, scrap, delivery risk, and redesign cost.
Buyer Evaluation AreaQuestions to AskWhy It MattersPractical Evidence to RequestDFM capabilityWill the supplier review wall thickness, draft, ribs, bosses, and gating?Prevents avoidable tooling changes and defects.Written DFM report with annotated CAD images.Material controlCan the supplier source specified resin grades and provide traceability?Material variation affects shrinkage, strength, color, and compliance.Material certificates, resin brand, grade, and lot records.Tooling approachIs rapid tooling, P20 steel, H13 steel, or multi-cavity tooling appropriate?Tool life and cost must match forecast volume.Tool steel specification and cavity-life estimate.Inspection processHow are critical dimensions and appearance checked?Ensures parts meet drawing and assembly requirements.First article inspection report and control plan.Production capacityCan output scale from pilot runs to recurring production?Protects launch schedules and future demand.Machine tonnage range, lead-time plan, and capacity confirmation.Logistics supportCan the supplier package, label, consolidate, and ship globally?Reduces handoffs and export errors.Packaging proposal, Incoterms, and shipping options.For parts shipped through major trade lanes such as Shenzhen–Los Angeles, Ningbo–Rotterdam, Hong Kong–Frankfurt, Shanghai–Melbourne, and Guangzhou–Singapore, packaging design matters. Thin-wall parts can deform if cartons are overloaded, while cosmetic housings may need individual protection to avoid abrasion. A qualified supplier should be able to support custom packaging, kitting, labeling, inspection documentation, and direct shipping according to the buyer’s channel requirements.
The companies below represent a mix of international and regional manufacturing options. Selection should depend on part complexity, resin type, annual quantity, tooling budget, required certifications, project location, and desired communication model. Buyers should verify current capabilities, certifications, production availability, and country-specific compliance needs directly before placing an order.
CompanyService RegionsCore StrengthsKey OfferingsSuitable Project TypesTEAM RapidGlobal customers; China manufacturing network; experience across North America, Europe, and AsiaRapid tooling, DFM support, low-volume to volume production, integrated manufacturingInjection molding, insert molding, overmolding, CNC machining, 3D printing, vacuum casting, finishing, assemblyPrototype-to-production parts, housings, covers, trays, enclosures, functional componentsProtolabsNorth America and EuropeFast digital manufacturing workflows and short lead-time productionInjection molding, CNC machining, 3D printing, sheet metal fabricationRapid validation, low-volume molded parts, product developmentXometryNorth America, Europe, and international sourcing networksLarge supplier network and online manufacturing quotation toolsInjection molding, machining, sheet metal, casting, 3D printingCompanies needing flexible sourcing and multiple manufacturing processesEVCO PlasticsUnited States, Mexico, and selected global programsCustom molding, large parts, engineering support, production-scale operationsInjection molding, tooling support, large-part molding, assemblyIndustrial, medical, consumer, automotive, and large molded productsRosti GroupEurope, Asia, and North AmericaContract manufacturing, regulated-sector experience, product industrializationInjection molding, assembly, automation, packaging, supply-chain supportMedical, packaging, consumer, industrial, and technical plastic productsNypro, a Jabil CompanyGlobal manufacturing footprint including North America, Europe, and AsiaHigh-volume manufacturing, healthcare and consumer product expertisePrecision molding, tooling, automation, assembly, supply-chain integrationHigh-volume medical, consumer, healthcare, and electronics programsSuppliers in the United States and Europe may be preferred when local production, immediate engineering access, regional certification requirements, or short domestic logistics routes are critical. China-based suppliers can be highly competitive for rapid tooling, flexible volume runs, custom part complexity, and multi-process programs that require molding, machining, finishing, assembly, and export packaging under one coordinated supply chain.
TEAM Rapid supports global product developers, brand owners, distributors, OEM customers, startups, engineers, and individual inventors with injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, die casting, finishing, assembly, packaging, procurement support, and direct shipping. The company has more than 10 years of manufacturing experience, has served customers in more than 25 countries, completed over 6,000 projects, and supported more than 500 customers. Its ISO 9001:2015 quality management certification, in-house machining and tooling capability, detailed DFM reports, and inspection-focused manufacturing process help customers evaluate wall gauge, rib proportions, boss construction, material use, shrinkage risks, cavity layout, cycle time, and production feasibility before tooling begins. TEAM Rapid works through flexible OEM, ODM, wholesale, retail-support, regional distribution, prototype, low-volume, and recurring production models rather than limiting customers to one order format. It provides turnkey and customer-owned plant manufacturing solutions, not BOO or on-site bulk supply services. Its China-based integrated manufacturing operations and resource network support international customers with engineering communication, online quotation, project follow-up, sample approval, after-sales issue handling, packaging, and direct export shipping. While the company profile does not state overseas subsidiaries or local warehouses, its established export experience across markets including the USA, UK, France, Germany, and other regions provides practical support for customers seeking a long-term manufacturing partner rather than a simple remote order-taking supplier.
For a new project, customers can use TEAM Rapid’s injection molding services to review tooling, resin options, production methods, and molding requirements. When the CAD model is ready, request a project review through the custom manufacturing quotation page and provide the required material, annual quantity, critical tolerances, target delivery market, color, finish, and assembly requirements.
A handheld device housing may begin with a 2.0 mm PC/ABS nominal wall. The design includes screw bosses, snap fits, battery supports, connector openings, and cosmetic exterior surfaces. If the screw bosses are built at full 2.0 mm wall thickness, sinks may appear on the outer cosmetic face. The preferred solution is to core the bosses, reduce boss wall thickness to approximately 1.2 mm, connect them using thin gussets, and add draft for ejection. This approach improves appearance and shortens cooling time without sacrificing assembly strength.
An under-hood sensor bracket may use glass-filled PA66 because it needs thermal resistance, stiffness, and fatigue performance. A flat 4.0 mm section may appear strong, but it can create fiber orientation concerns and warpage. A better design may use a 2.5 mm nominal wall with ribs and gussets positioned along load paths. The final solution must account for fiber direction, mounting loads, humidity exposure, temperature cycling, and fastener torque.
A large industrial cover often requires impact resistance, mounting points, cable openings, and a professional surface finish. Using a 3.5 mm wall throughout may increase resin cost and cycle time significantly. A more balanced design can use 2.5 mm nominal walls with localized ribs, reinforced mounting areas, and smooth radii around openings. Gate location is especially important because long rectangular panels may warp if flow and cooling are not balanced.
A food or consumer packaging container may use polypropylene walls below 1.0 mm. Such products require high-speed injection, optimized gates, rapid cooling, precise mold venting, and high-flow resin. Unlike a thicker industrial housing, the challenge is not simply stiffness; it is achieving full fill at high production speed while maintaining stackability, rim strength, lid fit, and consistent appearance.
Injection-molded wall gauge optimization is relevant across automotive, medical devices, consumer products, industrial equipment, communications products, office equipment, electrical appliances, sanitary products, packaging, smart hardware, household goods, laboratory equipment, and energy-related products. Every industry applies the same basic thermal and flow principles, but each has different priorities.
Medical customers may focus on traceable materials, chemical compatibility, cleanability, reliability, and controlled assembly. Automotive customers may prioritize impact behavior, heat resistance, vibration durability, flame resistance, and dimensional stability. Consumer product brands may place greater emphasis on weight, surface quality, tactile feel, color matching, and cost. Industrial customers frequently need durable housings, cable management, mounting strength, and practical serviceability.
For global brands, it is also important to consider regional regulations and product certification pathways. Flame-retardant ratings, food-contact requirements, electrical safety standards, restricted substance requirements, recycling expectations, and customer-specific quality systems can influence material choice and ultimately affect the preferred wall gauge.
By 2026, wall thickness decisions are increasingly influenced by digital simulation, sustainability targets, material innovation, and supply-chain localization. Mold-flow simulation is becoming more accessible earlier in product development, allowing engineering teams to identify pressure drop, weld-line locations, cooling imbalance, and fiber orientation before steel is cut. This helps reduce expensive post-tooling modifications and supports faster product launches.
Lightweighting will remain a major trend. Brands are reducing plastic content through thinner walls, rib-optimized structures, topology-informed design, foamed materials, and stronger engineering resins. However, lightweighting must be balanced against product durability, recyclability, drop performance, and customer expectations. Overly thin designs can increase scrap, returns, and premature product failure, which undermines sustainability goals.
Recycled-content plastics will also affect molding strategy. Post-consumer recycled and post-industrial recycled materials can show greater variation in flow, color, shrinkage, and mechanical properties compared with virgin resin. Designers may need more conservative flow paths, better tolerance planning, or adjusted wall thickness when using recycled grades. Material validation and supplier consistency become especially important for functional products.
Policy trends in the global market are encouraging packaging reduction, material circularity, product repairability, and improved environmental reporting. Manufacturers will increasingly need to document resin selection, recycled content, product weight, packaging choices, and process efficiency. Well-designed wall gauge supports these goals by reducing unnecessary material while preserving real-world performance.
There is no single best value. A practical starting point for many parts is 1.5 mm to 3.0 mm. The correct choice depends on resin, part size, flow length, structural load, surface quality, gate location, and production method.
Uniform walls cool and shrink more evenly. This reduces sink marks, voids, warpage, stress, inconsistent dimensions, and cycle-time variation. Where different thicknesses are necessary, transitions should be gradual.
Ribs are commonly designed at 40% to 60% of the nominal wall thickness. Thicker ribs can create sink marks, especially behind cosmetic surfaces. Rounded rib bases and appropriate draft improve filling and ejection.
Yes. Thinner walls can reduce resin use and cooling time, lowering part cost in high-volume production. However, thin-wall designs may require more advanced tooling, high-flow material, faster molding equipment, and tighter process control.
Sink marks usually occur where plastic mass is concentrated, such as thick bosses, ribs, corners, and heavy wall sections. Core out thick areas, reduce rib thickness, improve packing access, and use balanced cooling.
In most cases, use ribs, gussets, or structural webs before increasing the full wall thickness. Ribs can improve stiffness efficiently while minimizing resin consumption, cooling time, and sink risk.
Yes. TEAM Rapid can provide DFM-oriented feedback for injection molding projects, including observations on wall thickness consistency, ribs, bosses, draft, undercuts, shrinkage risks, tooling feasibility, and production efficiency.
-
Mold Flow Analysis for Global Market Tooling Choices
Mold flow analysis is a digital injection molding simulation used before tooling to predict how molten plastic will fill, pack, cool, shrink, and warp inside a mold. It helps product teams identify likely defects such as short shots, weld lines, sink marks, air traps, excessive clamp force, uneven cooling, and dimensional distortion before steel is cut.
For Global market buyers, the most practical approach is to run a mold filling and cooling study during DFM review, then revise wall thickness, gate position, runner layout, material selection, and cooling channels before ordering tooling. This can reduce development iterations, improve mold reliability, and lower the risk of expensive post-tooling modifications.
Established providers commonly considered for mold flow simulation and tooling support include Autodesk Moldflow, Moldex3D, SIGMA Engineering, SIMCON, CoreTech System, and TEAM Rapid. Software providers supply the analysis platform, while engineering-led manufacturers apply the results to real mold design, rapid tooling, sampling, and production.
Injection molding is highly sensitive to how polymer melt moves through a cavity. A part that appears simple in CAD can become difficult to mold when it combines thin ribs, deep bosses, non-uniform walls, cosmetic surfaces, long flow lengths, engineering resins, inserts, or tight dimensional tolerances. Mold flow analysis converts the part design, material data, gate proposal, runner system, process assumptions, and cooling concept into a predictive simulation.
The analysis does not replace moldmaker experience or physical sampling. Instead, it gives engineers evidence for choosing the most robust design path before a mold is manufactured. For buyers coordinating design teams in cities such as London, Munich, Chicago, Shenzhen, Singapore, Dubai, and Melbourne, the process creates a common technical language before tooling decisions are released across borders.
Analysis AreaWhat Is EvaluatedTypical Risk FoundPractical Tooling DecisionFill analysisMelt-front movement, fill time, pressure, and flow balanceShort shots, hesitation, overpacking, unbalanced cavitiesMove gates, enlarge runners, adjust wall thickness, change injection strategyPack analysisHolding pressure effect and volumetric shrinkageSink marks, internal voids, inconsistent dimensionsRevise gate size, holding profile, rib thickness, and packing windowCooling analysisHeat removal, mold temperature balance, and cooling durationLong cycle time, hot spots, uneven shrinkageAdd baffles, bubblers, conformal cooling, or optimized water linesWarpage analysisDeflection caused by shrinkage, orientation, and thermal gradientsTwist, bow, uneven flatness, assembly failureModify geometry, gate direction, material grade, or cooling layoutWeld-line evaluationLocations where melt fronts meetWeak joints, cosmetic marks, leakage or crack riskRelocate gates, improve venting, increase melt temperature, revise geometryAir-trap evaluationAreas where air is compressed during fillingBurn marks, incomplete filling, poor surface qualityAdd vents, overflow wells, ejector venting, or change fill directionClamp-force predictionForce needed to keep the mold closed during injectionFlash, machine mismatch, tool damageSelect an appropriate molding machine and optimize gate and process conditionsThe table shows why a flow study should be linked to a decision process. A red or blue simulation image alone is not sufficient. The useful deliverable is a prioritized engineering plan explaining which findings are critical, which are acceptable, and how each recommendation affects tooling cost, molding stability, appearance, and part performance.
The Global market for mold flow analysis is growing because product cycles are shorter, resin options are more specialized, and molding projects increasingly involve electronics, medical devices, electric vehicles, consumer products, industrial equipment, and sustainability requirements. Buyers are under pressure to achieve functional prototypes quickly while also avoiding unnecessary production-tool revisions.
Manufacturing hubs in China, Germany, the United States, Japan, South Korea, Mexico, Vietnam, Poland, and India are increasingly connected through international sourcing networks. Mold design may be reviewed in Europe, tool steel may be machined in Guangdong, samples may be tested in North America, and production may be shipped through ports such as Shenzhen, Ningbo-Zhoushan, Hamburg, Rotterdam, Los Angeles, Long Beach, Singapore, or Jebel Ali. A structured flow analysis report reduces the communication gaps that can occur in this distributed manufacturing environment.
For low-volume programs, the analysis may focus on whether rapid tooling can produce acceptable parts without excessive cycle time or warpage. For larger production programs, the review may cover cavity balance, hot runner selection, cooling efficiency, automation compatibility, resin consumption, and total cost per part. The investment level should be matched to the commercial risk of the project.
Different projects need different levels of simulation. A simple single-cavity enclosure may only need filling, weld-line, venting, and basic warpage checks. A high-volume automotive, medical, or electrical connector mold may require detailed packing, cooling, fiber-orientation, insert molding, and multi-cavity balance studies.
Service TypeBest ForMain DeliverablesBuyer BenefitBasic fill studySimple housings, covers, trays, and prototype partsFill pattern, pressure, weld lines, air traps, gate proposalFast screening before rapid toolingFill and pack studyParts with ribs, bosses, thick-to-thin transitions, and cosmetic surfacesSink-risk map, shrinkage review, packing profile recommendationsImproves dimensional and cosmetic consistencyCooling studyMedium and high-volume molds with cycle-time targetsCooling channel assessment, temperature balance, cycle estimateSupports lower unit cost and stable productionWarpage studyFlat panels, snap-fit assemblies, long parts, reinforced resinsDeflection prediction, orientation effect, geometry recommendationsReduces assembly and flatness failuresMulti-cavity balance studyFamily molds and multi-cavity production toolsCavity filling balance, runner optimization, pressure comparisonImproves consistency across cavitiesFiber-orientation studyGlass-filled nylon, reinforced polypropylene, and structural partsFiber alignment, anisotropic shrinkage, stiffness direction reviewHelps control warpage and mechanical performanceInsert and overmolding studyMetal inserts, electrical parts, soft-touch overmoldingInsert temperature effects, flow behavior, bonding-risk assessmentProtects inserts and improves process repeatabilityFor a project involving insert molding or overmolding, the simulation must consider more than cavity filling. Metal inserts can remove heat rapidly, alter flow direction, create weld lines, and cause localized stress. Similarly, soft elastomer overmolding requires attention to substrate adhesion, gate placement, part retention, and cosmetic surface control.
A professional report should begin with the part name, material grade, shrinkage assumptions, gate proposal, machine assumptions, cavity count, and study scope. Without these inputs, buyers cannot judge whether the findings apply to the intended production situation. For example, a simulation using a generic polypropylene grade may not accurately represent a specified mineral-filled, recycled-content, flame-retardant, or food-contact grade.
Start with the filling pattern. The goal is normally smooth, balanced progression from the gate to the farthest regions without hesitation or excessive race tracking. Next, inspect pressure at end of fill. If predicted pressure is close to machine limits, the supplier may need to enlarge gates, change wall geometry, raise melt temperature, or choose a larger press.
Then review weld lines and air traps in relation to functional features. A weld line near a non-critical cosmetic edge may be acceptable. A weld line crossing a snap-fit, sealing surface, screw boss, high-load tab, or fluid path may require redesign. Cooling and warpage results should be evaluated against the actual assembly tolerances rather than vague expectations of “flatness.”
Finally, ask whether the proposed changes alter cost, lead time, mold complexity, resin use, or maintenance. A recommendation for conformal cooling may improve cycle time but can increase tool cost. A larger gate can reduce pressure but may leave a more visible gate vestige. The best solution balances technical performance with commercial priorities.
Buyers should treat flow simulation as part of a broader design-for-manufacturing process. It is most effective when the design team provides accurate CAD files, material preferences, expected annual volume, surface-quality requirements, assembly tolerances, regulatory needs, and target markets. A supplier cannot make reliable tooling recommendations if critical product information is missing.
When comparing quotations, do not select a supplier only because it offers the lowest tooling price. A low initial quote can become expensive if the mold requires repeated rework, production cycle time is high, part scrap is excessive, or the chosen machine cannot maintain a stable process window. A transparent supplier should identify potential trade-offs before purchase order release.
Observed IssueLikely Simulation FindingPossible Design CauseTypical Corrective ActionShort shotIncomplete fill at far flow endLong flow path, thin section, small gate, inadequate ventingIncrease gate size, revise wall thickness, improve venting, optimize processSink markHigh local volumetric shrinkageThick bosses, heavy ribs, uneven wall sectionsCore out thick areas, reduce rib thickness, adjust packing and coolingWarped panelUneven cooling or orientation-driven shrinkageAsymmetric geometry, poor cooling layout, reinforced resinBalance cooling, alter gate location, add structural features, revise materialBurn markAir trap with compressed gas near end of fillInsufficient venting, high injection speed, trapped cavity airAdd vents, reduce local speed, revise gate position and flow directionFlashExcessive pressure or clamp-force demandSmall gates, restrictive flow, poor mold fit, low clamp forceOptimize gate and process, verify machine selection, improve mold shutoffWeak weld lineMelt fronts meet at a low temperature or sensitive areaMultiple flow paths, holes, inserts, poor gate positionRelocate gate, adjust temperature, move weld line away from load areasUneven cavity outputImbalanced runner or filling patternPoor runner geometry, unequal flow lengths, inconsistent coolingBalance runner system, adjust gates, improve cooling uniformityThe table is useful during supplier review because it links visible defects to engineering causes. Not every issue can be fully eliminated through simulation, particularly when material variation, machine condition, process control, or cosmetic standards are involved. However, a well-executed study helps prevent predictable risks from becoming expensive surprises after the mold trial.
Automotive programs use mold flow analysis for interior trim, under-hood covers, sensor housings, lighting components, clips, ducts, battery-related plastic parts, and reinforced structural components. These parts often require repeatable dimensions, controlled warpage, robust snap fits, and predictable performance across large production volumes.
Medical device manufacturers use simulation for handheld enclosures, diagnostic equipment housings, fluid-management components, disposable trays, laboratory consumables, and assembly parts. Material selection, cleanability, dimensional accuracy, traceability expectations, and surface quality make early engineering review especially important.
Consumer electronics and communication products benefit from flow simulation when producing thin-wall cases, wearable-device components, charging accessories, cable-management parts, buttons, covers, and high-gloss or textured housings. Gate position and weld-line control can directly affect visual quality and perceived product value.
Industrial equipment, office products, home appliances, sanitary products, and commercial devices often use molded enclosures, panels, handles, covers, brackets, and functional internal components. These applications may have lower volumes than consumer goods but higher demands for assembly fit, durability, and cost-efficient tooling.
Mold flow analysis is especially valuable for complex plastic parts where functional risk and tooling cost are high. Typical applications include battery housings, electrical enclosures, medical appliance casings, industrial control covers, appliance panels, automotive clips, cosmetic containers, fluid fittings, storage trays, protective shells, and precision mechanical plastic parts.
It is also useful when changing from one manufacturing method to another. A product initially produced through SLA 3D printing, SLS printing, CNC machining, or vacuum casting may require geometry adjustments before injection molding. Features that work well in a prototype can become difficult to fill, cool, eject, or inspect in a molded production part.
For companies moving toward short-run market validation, rapid tooling plus simulation can provide a practical bridge between prototype testing and mass production. The buyer can test real injection molded material properties before investing in a long-life production mold.
The following companies represent widely recognized software, simulation, and manufacturing options for Global market buyers. Selection depends on whether the project requires software access, specialist engineering consultation, rapid tooling, production tooling, molded parts, or a complete prototype-to-production pathway.
CompanyService RegionsCore StrengthsKey OfferingsAutodesk MoldflowGlobal software network with users in North America, Europe, Asia-Pacific, and the Middle EastWidely used injection molding simulation platform and extensive industry adoptionFill, pack, cooling, warpage, fiber orientation, and process optimization softwareMoldex3DGlobal, with strong presence across Asia, Europe, and North AmericaAdvanced 3D simulation for complex molding, electronics, automotive, and engineering applicationsPlastic flow simulation, insert molding, overmolding, cooling, warpage, and manufacturing optimizationSIGMA EngineeringEurope, North America, Asia-Pacific, and global industrial marketsVirtual molding technology focused on process optimization and production stabilitySIGMASOFT virtual molding, process variation assessment, cycle and quality optimizationSIMCONEurope-based support with international software users and partnersInjection molding simulation with practical design and process evaluation toolsCADMOULD simulation, filling, packing, cooling, warpage, and mold design supportCoreTech SystemGlobal through Moldex3D distribution and engineering channelsSimulation technology for advanced polymer processing and mold validation3D flow analysis, material behavior review, fiber effects, cooling and warpage studiesTEAM RapidGlobal customers in more than 25 countries, serving China, the USA, the UK, France, Germany, and other marketsIntegrated DFM, rapid tooling, injection molding, CNC machining, and low-volume manufacturing supportMold flow-oriented DFM review, rapid tooling, injection molding, prototype production, finishing, assembly, and shippingSoftware companies are suitable when an organization has internal molding engineers who need analysis capability across multiple programs. Manufacturing partners are suitable when buyers want one supplier to interpret the results, revise the mold design, build the tool, mold samples, inspect parts, and manage production. For international programs, buyers should ask who owns the simulation decisions and whether the tooling engineer responsible for machining has reviewed the recommendations.
TEAM Rapid supports Global market customers that need practical engineering feedback before committing to tooling. Its service model combines DFM analysis, mold flow-oriented risk review, rapid tooling, injection molding, CNC machining, 3D printing, vacuum casting, die casting, sheet metal fabrication, finishing, assembly, packaging, and direct shipping. Customers can begin with prototypes, validate design changes, move into short-run molded parts, and scale toward recurring production without managing separate suppliers for each stage.
For injection molded projects, TEAM Rapid can evaluate wall thickness, draft, gates, runners, parting lines, undercuts, venting, ejection, cooling concerns, shrinkage risk, resin selection, mold cavities, and expected cycle time. Buyers can review the company’s injection molding services when planning production parts, or explore rapid tooling solutions when fast market validation is required.
TEAM Rapid demonstrates relevant manufacturing authority through ISO 9001:2015 certification, more than 10 years of industry experience, more than 500 satisfied customers, over 6,000 delivered projects, and service experience across more than 25 countries. Its manufacturing scope covers plastic and metal components from a single prototype to more than 100,000 parts, supported by in-house machining, tooling manufacturing, molding capability, and an integrated manufacturing resource network in China. Rather than making unsupported claims about proprietary component brands, the company works from customer-specified material, functional, cosmetic, and tolerance requirements, with engineering review and specification compliance built into its ISO-based quality process. It supports OEM and ODM requirements, wholesale programs, brand owners, product developers, distributors, dealers, end users, startups, and individual innovators through flexible prototype, low-volume, and recurring-production models. TEAM Rapid provides turnkey and customer-owned product manufacturing solutions, including tooling, parts, finishing, assembly, packaging, procurement coordination, and direct shipment; it does not operate BOO or on-site bulk-supply models. Its Global market commitment is demonstrated by established project experience in the USA, UK, France, Germany, China, and other markets, direct shipping capability, limited warehousing support, and one-to-one engineering communication with responses typically available within hours. While customers should confirm any specific local warehousing or regional support requirement during quotation, the company’s online pre-sales engineering reviews, manufacturing updates, inspection support, packaging coordination, and after-sales project communication provide practical protection for international buyers.
For a tailored review of a mold flow analysis, DFM package, prototype plan, or tooling quotation, buyers can request a manufacturing quote with CAD files, material preferences, production volume, and target delivery date.
A consumer device enclosure may have a large visible surface, thin walls, snap fits, screw bosses, and internal support ribs. A fill study can identify whether a gate near the edge creates weld lines across a logo area or a critical clip. Pack analysis may reveal sink risk behind thick bosses. The recommended change may include moving the gate to a hidden underside, coring thick features, reducing rib thickness, and improving venting near the last-fill region. These changes can protect cosmetic appearance before the first T1 sample.
A glass-filled nylon bracket can experience directional shrinkage caused by fiber orientation. Even when the part fills successfully, it may warp after ejection and fail assembly with nearby metal components. A warpage and fiber-orientation study can help determine a more appropriate gate direction, wall transition, rib layout, and cooling balance. The resulting tooling design may cost slightly more, but it can reduce downstream fitting issues and production rejection.
A medical equipment housing may require controlled appearance, consistent assembly, safe edge conditions, and reliable screw-boss performance. Flow analysis can identify air traps near internal corners and weld lines around openings. Combined with DFM review, the design team may add draft, relocate gates, revise boss geometry, and define suitable inspection points before rapid tooling. This approach helps teams obtain functional molded samples faster than relying on repeated trial-and-error modifications.
A packaging tray with multiple cavities may appear straightforward but can suffer from uneven filling if the runner system is not balanced. Simulation can compare runner paths, gate sizes, cavity pressure, and cooling behavior. The buyer can then decide whether a cold runner, hot runner, or revised cavity arrangement is justified based on annual volume, resin savings, cycle time, and quality requirements.
By 2026, mold flow analysis will increasingly be connected to digital manufacturing systems rather than used only as a standalone design check. Simulation platforms are incorporating more automation, improved material databases, cloud collaboration, machine-learning-assisted optimization, and stronger links between CAD, mold design, process settings, and quality data. This will allow teams in different Global market locations to review molding risks earlier and make decisions faster.
Sustainability will also influence simulation priorities. Brands are increasing the use of recycled-content resins, bio-based polymers, lightweight structures, lower-energy production, and reduced scrap targets. These materials can have different flow, shrinkage, moisture sensitivity, and mechanical behavior compared with conventional virgin resin grades. Mold flow analysis will be used more often to validate whether recycled or lower-carbon material options can meet appearance, strength, and cycle-time requirements.
Policy and compliance expectations are expanding across regions. European product sustainability initiatives, extended producer responsibility programs, packaging regulations, chemical restrictions, and traceability expectations are pushing manufacturers to document material choices and reduce waste. Global buyers should ask whether a supplier can support material documentation, process records, inspection requirements, and responsible packaging practices appropriate for the destination market.
Cooling technology will remain a major focus. Conformal cooling, improved thermal control, additive-manufactured inserts, sensor-based mold monitoring, and predictive maintenance can reduce cycle time and improve dimensional stability. For high-volume programs, even a small reduction in cycle time can create substantial savings across the life of a mold.
Prepare a 3D CAD model in STEP, IGES, Parasolid, or native format where possible. Include the latest revision level and identify any surfaces that cannot be changed. Provide the expected resin, annual volume, part weight target, cosmetic requirements, functional loads, target tolerances, assembly interfaces, and preferred production location.
Ask the supplier to confirm the analysis scope before work begins. For example, a rapid-tooling program may need a basic fill and warpage review, while a high-volume multi-cavity project may need comprehensive filling, packing, cooling, runner balance, and cycle-time analysis. Set a review meeting or written approval stage before the supplier begins tool steel machining.
After the analysis is complete, ensure that approved recommendations are reflected in the final mold design. Then compare the first molded samples against the simulation predictions. If the results differ significantly, investigate material lot variation, actual machine settings, mold temperature, venting performance, cooling conditions, and measurement method. This closed-loop learning process improves future projects.
No. Very simple, low-risk parts with generous walls and low production volumes may only need a standard DFM review. However, analysis is strongly recommended for complex, thin-wall, cosmetic, reinforced, multi-cavity, insert molded, or high-volume components where tooling changes would be costly.
No simulation can guarantee a defect-free part. Actual results depend on material behavior, machine condition, mold quality, process control, cooling performance, and operator settings. The purpose is to identify and reduce predictable risks before tooling is made.
Provide accurate CAD, material grade, filler content, intended annual volume, gate restrictions, surface requirements, tolerance expectations, mold cavity count, and production goals. The more complete the inputs, the more useful the recommendations will be.
It can reduce cost by identifying gate, runner, venting, cooling, wall-thickness, and warpage issues before steel is machined. Preventing a major tool modification is often more valuable than the cost of the initial simulation.
Yes. Cooling analysis can identify hot spots, inefficient cooling lines, and temperature imbalance. Better cooling design can reduce cooling time, improve part consistency, and lower production cost per part.
Yes. Rapid tooling has shorter lead times, so early engineering decisions are especially important. A focused analysis can help avoid wasting time on avoidable tool changes and support faster validation using real molded materials.
Yes, but the accuracy depends on having appropriate material data. Recycled-content resins may have wider property variation than virgin grades, so buyers should discuss material sourcing, lot control, cosmetic expectations, and test requirements with the supplier.
Ask about DFM scope, mold flow analysis capability, material data, tooling steel, cavity strategy, cooling design, sample lead time, inspection method, change-control process, shipping terms, communication frequency, and after-sales support for mold adjustments or recurring production.
-
Injection Mold Upkeep for the Global Market: Tool Life
Effective injection mold maintenance protects dimensional accuracy, reduces unplanned downtime, prevents flash and cosmetic defects, and extends the productive life of a mold. The most practical approach is to clean molding surfaces after every production run, inspect high-wear components regularly, lubricate approved moving areas, control moisture during storage, document each intervention, and schedule preventive maintenance based on shot count and part quality trends.
For buyers in the Global market, leading mold and injection molding support providers include TEAM Rapid in China, Husky Technologies in Canada, ENGEL in Austria, ARBURG in Germany, Milacron in the United States, and Sumitomo (SHI) Demag in Germany. Qualified international suppliers, including Chinese tooling companies with ISO-certified quality systems, responsive engineering support, and strong pre-sales and after-sales communication, can also be a practical option because of their cost-performance advantages.
Injection molds are precision production assets. A mold may contain hardened steel cavities, interchangeable inserts, cooling circuits, hot runner components, ejector systems, slides, lifters, hydraulic cylinders, sensors, guide pillars, wear plates, and precision shutoff surfaces. Each feature must operate repeatedly under pressure, heat, friction, resin flow, and mechanical movement. Without planned mold upkeep, small problems can become major tooling failures.
Across global manufacturing centers such as Shenzhen, Dongguan, Ningbo, Shanghai, Singapore, Munich, Stuttgart, Chicago, Toronto, Monterrey, Rotterdam, Dubai, and London, buyers increasingly expect stable quality from multi-cavity tools and short production lead times. Mold failures affect more than maintenance costs. They may delay assembly, disrupt packaging schedules, increase rejected parts, interrupt container loading at ports, and create missed retail or product-launch deadlines.
Regular injection mold maintenance helps manufacturers control the most common production risks: poor cooling performance, burn marks caused by blocked vents, flash caused by damaged shutoffs, dimensional drift from worn inserts, short shots from gate restrictions, scratches caused by ejector damage, and corrosion caused by moisture or aggressive resin additives. A documented maintenance plan is therefore not simply a workshop procedure; it is a quality and supply-chain protection system.
Mold maintenance should be divided by timing, production volume, part quality requirements, resin type, and mold complexity. A simple prototype tool running polypropylene has different maintenance needs from a high-cavity production mold processing glass-filled nylon, flame-retardant ABS, PVC, POM, or engineering-grade polycarbonate.
Maintenance TypeTypical TriggerMain TasksBusiness BenefitStart-up inspectionBefore each production runCheck water connections, clamps, ejector movement, sensors, fasteners, and visible damageReduces start-up defects and avoids running a damaged toolDaily careEach shift or campaignRemove resin residue, inspect vents, wipe molding surfaces, review part qualityMaintains cosmetic quality and stable fillingPreventive maintenanceBased on shot countClean cooling lines, replace seals, check wear plates, lubricate moving componentsPrevents unexpected production stopsCorrective maintenanceAfter a defect or breakdownRepair inserts, weld damage, polish cavities, replace ejector pins or hot runner partsRestores functional performanceSeasonal storage maintenanceBefore long-term storageDry circuits, apply corrosion protection, pack components, label mold conditionProtects the tool during idle periodsEngineering improvementRecurring defect trendsModify venting, cooling, gate geometry, ejection, or material flow pathsImproves long-term manufacturabilityThe table shows that mold maintenance is not limited to emergency repair. Start-up checks protect production readiness, routine cleaning protects surface quality, preventive work protects long-term tool life, and engineering changes address repeated process weaknesses that cannot be solved through cleaning alone.
A practical checklist should be specific enough for technicians to follow consistently while allowing the maintenance team to record mold condition. The best checklist is linked to a mold identification number, part number, resin, shot count, production machine, date, operator, maintenance technician, and next planned service interval.
Mold AreaInspection PointRecommended ActionWarning SignCavity and coreScratches, deposits, corrosion, polishing conditionClean with approved materials and polish only when necessaryGloss variation, drag marks, visible blemishesParting lineDamage, burrs, resin buildup, mismatchRemove residue and inspect shutoff surfaces carefullyFlash around the molded partVentsBlocked vents and contaminationClean vents without enlarging critical dimensionsBurn marks, short shots, trapped airEjector systemPin movement, return pins, plates, wearClean, lubricate approved locations, replace damaged pinsWhite marks, ejector impressions, stuck partsCooling systemFlow rate, leaks, scale, corrosion, connectorsFlush channels and replace worn seals or fittingsLonger cycle time, uneven shrinkage, warpageSlides and liftersGalling, friction, alignment, wear platesClean and apply suitable high-pressure lubricantNoise, scoring, sticking, dimensional variationHot runner systemHeater, thermocouple, nozzle tip, wiringVerify temperature response and inspect leakage pointsStringing, drooling, uneven fill, resin degradationFasteners and clampsLoose bolts, damaged threads, lifting pointsTorque-check where required and replace damaged hardwareMisalignment, mold movement, safety riskThis checklist is most effective when mold condition is linked to molded-part inspection data. For example, recurring flash on one cavity should trigger inspection of that cavity insert, shutoff surface, parting line, clamping condition, and process pressure. Repeated short shots should lead to checks of gate restrictions, venting, hot runner temperatures, material drying, and cooling balance rather than random machine adjustment.
Cleaning methods must match the mold steel, surface finish, resin type, and contamination level. Mirror-polished cavities require more careful handling than textured surfaces. Abrasive tools should not be used on critical molding surfaces unless approved by experienced tooling personnel. Improper polishing can alter geometry, damage texture, create mismatched cavity surfaces, and increase flash risk.
For standard cleaning, technicians commonly use lint-free cloths, approved mold cleaners, compressed dry air, soft non-metallic brushes, and appropriate cleaning tools for vents and channels. When handling electrical components, hot runners, sensors, or thermocouples, power isolation and electrical safety procedures must be followed. Cooling channels may require chemical descaling or mechanical flushing, but the selected method must be compatible with mold steel, seals, and water-system materials.
Lubrication should be controlled rather than excessive. Too much lubricant can migrate into cavities, contaminate molded parts, collect dust, and produce cosmetic defects. Use a lubricant suitable for guide pins, slideways, lifters, ejector systems, and high-load wear surfaces. Avoid applying lubricants directly to cavity surfaces unless the mold supplier specifically recommends a corrosion-protection product for storage.
For storage, the mold should be cleaned, dried, closed or protected as appropriate, labeled with its latest shot count and condition, and stored in a stable environment. Water circuits must not retain moisture when a mold will remain idle for an extended period. In humid coastal regions near ports such as Shenzhen, Ningbo, Hamburg, Rotterdam, Houston, or Singapore, corrosion prevention is especially important due to high humidity and salt-laden air exposure.
When selecting a maintenance provider, buyers should assess more than hourly repair rates. A low repair price can become expensive if the supplier cannot diagnose root causes, lacks precision machining capability, uses unsuitable replacement components, or fails to document tool changes. The preferred partner should understand mold design, resin behavior, injection molding parameters, metallurgy, dimensional inspection, and production scheduling.
Evaluation FactorWhat Buyers Should AskWhy It MattersPractical EvidenceTooling experienceCan the supplier repair cavities, cores, slides, and ejector systems?Complex repairs require specialized mold knowledgeExamples of similar tooling repairs and DFM reportsMachining capabilityAre CNC, EDM, wire EDM, grinding, and polishing available?Precision replacement parts must match the moldIn-house equipment list and tolerance capabilityQuality systemDoes the provider operate under a recognized quality framework?Maintenance records and inspections must be reliableISO 9001 certification and documented inspection processSpare part managementCan wear components be made or sourced quickly?Delays often come from unavailable inserts or ejectorsSpare-part list, lead-time plan, component drawingsEngineering supportCan the supplier identify design-related causes of defects?Repeated failures may need redesign rather than repairRoot-cause reports and process recommendationsGlobal communicationHow quickly are quotations, reports, and updates provided?International projects require fast decisionsNamed engineer, response procedure, digital reportingBuyers should also clarify ownership of mold drawings, spare inserts, maintenance records, and tool modifications. For contract manufacturing projects, the agreement should specify whether the tool remains at the factory, whether customers can request transfer, how storage is charged, and what condition documentation is required before shipment.
For projects requiring new tooling or replacement mold components, it is useful to request rapid tooling services that combine manufacturability analysis, precision machining, trial molding, and production support. This reduces the risk of treating each repair as an isolated event.
Injection mold maintenance is essential in industries where parts must meet repeatable visual, dimensional, safety, or functional requirements. Medical device housings may need clean cosmetic surfaces and controlled material traceability. Automotive interior and under-hood components require dependable fit, thermal resistance, and stable dimensional performance. Consumer electronics cases and enclosures demand consistent texture, snap-fit accuracy, logo details, and assembly alignment.
Other important applications include communication products, office equipment, electrical appliances, sanitary products, industrial controls, packaging components, food-contact products, laboratory devices, appliance covers, trays, caps, connectors, clips, fittings, and overmolded assemblies. In each sector, the maintenance interval should reflect the consequences of defect escape. A small scratch on a hidden industrial bracket may be acceptable, while a minor surface mark on a premium consumer product may result in full batch rejection.
Some mold features wear faster than others. Thin shutoffs, deep ribs, narrow vents, side actions, textured surfaces, hot runner gates, fine ejector pins, threaded unscrewing cores, and optical-grade polishing require closer inspection. Glass-filled polymers and mineral-filled materials can increase abrasion. Flame-retardant compounds may leave deposits. PVC and some additives can create corrosive conditions if processing and cleaning are not properly controlled.
ApplicationHigh-Risk Mold FeatureMaintenance FocusTypical Defect if NeglectedElectronic enclosuresTextured cavity and snap-fit detailsProtect texture and inspect precision clipsScratches, poor assembly fit, cosmetic defectsAutomotive partsLarge slides and complex shutoffsMonitor alignment, wear plates, and cooling balanceFlash, warpage, part mismatchMedical housingsPolished cavities and fine ventsPrevent contamination and maintain surface finishSurface marks, burn marks, rejected partsPackaging closuresHigh-cavity core and gate areasTrack cavity balance and replace worn componentsLeakage, short shots, inconsistent threadsOvermolded componentsInsert location featuresCheck insert seating and shutoff contactMisalignment, resin leakage, weak bondingIndustrial connectorsSmall pins and detailed core insertsInspect for pin damage and blocked ventsBroken features, incomplete fillingThe table demonstrates why maintenance schedules should not be based only on elapsed calendar time. A high-cavity cap mold operating continuously may need more frequent care than a lower-volume tool used occasionally. Likewise, a mold processing abrasive glass-filled nylon should be inspected more often than one molding unfilled polypropylene.
A multi-cavity housing mold began showing longer cycle times and uneven part warpage. The production team initially adjusted packing pressure and cooling time, but the problem continued. A maintenance inspection found mineral buildup in several cooling channels, reducing water flow and creating uneven mold temperatures. After flushing the channels, replacing worn water fittings, and verifying flow balance, the cycle time stabilized and warpage was reduced. The lesson is that cooling maintenance should be measured through flow and temperature performance, not visual inspection alone.
An automotive trim component developed recurring flash near a side-action feature. The mold was repeatedly cleaned, but the flash returned. A detailed inspection found wear on the slide shutoff and insufficient support from a worn wear plate. The maintenance team repaired the shutoff surface, replaced the wear plate, checked slide alignment, and reviewed clamping and injection-pressure settings. The improvement showed that persistent flash often has a mechanical root cause rather than a simple cleaning issue.
An industrial enclosure with deep ribs experienced burn marks near the end of fill. The molding machine was operating within the normal process window, but venting areas had accumulated residue. The maintenance procedure included vent cleaning, checking vent depth, confirming resin drying, and reviewing fill speed. Once air evacuation improved, the burn marks were removed without changing the part design. This case highlights the importance of maintaining venting features, particularly in deep, thin, or complex flow regions.
The following companies are recognized across major manufacturing regions for injection molding equipment, tooling, mold engineering, production support, or rapid manufacturing services. Buyers should verify local service availability, scope of work, equipment compatibility, lead time, and regional commercial terms before placing an order.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidChina, North America, Europe, United Kingdom, France, Germany, and global export marketsRapid tooling, CNC machining, injection molding, DFM review, low-volume and volume productionMold making, maintenance support, replacement components, prototyping, custom injection molded partsHusky TechnologiesNorth America, Europe, Asia-Pacific, Latin America, global packaging marketsHigh-performance injection molding systems and packaging expertiseHot runners, molds, systems support, service programs, PET and closure manufacturing solutionsENGELEurope, Americas, Asia, global industrial molding marketsInjection molding machines, automation, process support, digital production toolsMachine service, automation integration, process optimization, molding technology supportARBURGGermany, Europe, North America, Asia and worldwide service locationsPrecision injection molding machinery and application engineeringMachine support, training, automation, process technologies, production optimizationMilacronUnited States, Canada, Mexico, Europe, Asia-PacificInjection molding equipment, hot runner technology, mold components and serviceMachine service, hot runners, temperature control, parts, process supportSumitomo (SHI) DemagEurope, North America, Asia-Pacific, global manufacturing networksAll-electric injection molding technology and process reliabilityMachine support, application engineering, spare parts, service and trainingThis supplier comparison is intended as a practical starting point. Equipment manufacturers may focus primarily on machine, hot runner, automation, or process support, while tooling manufacturers can provide cavity repair, insert replacement, polishing, machining, mold modification, and trial production. For global buyers, the best outcome often comes from coordinating the mold maker, molding factory, and machine or hot-runner specialist rather than relying on one party for every task.
TEAM Rapid supports customers from prototype development through repeatable injection molding production, with more than 10 years of industry experience, ISO 9001:2015 quality management, over 500 customers served in more than 25 countries, and more than 6,000 delivered projects. Its practical product strength comes from combining in-house CNC machining, EDM, wire EDM, polishing, tooling manufacture, injection molding capability, DFM analysis, inspection processes, and diversified plastic and metal material options; specific branded mold components are selected according to project requirements rather than promoted as a fixed component brand list. The company works with end users, product designers, distributors, dealers, brand owners, startups, established manufacturers, and individual innovators through flexible OEM, ODM, prototype, low-volume, recurring production, assembly, packaging, and direct-shipping models. TEAM Rapid does not offer BOO or on-site bulk supply services; instead, it provides customer-owned tooling, turnkey manufacturing, and customer-owned plant solution support where applicable. While the company profile does not claim overseas subsidiaries or local warehouses, TEAM Rapid has established export experience serving customers in the USA, UK, France, Germany, China, and other markets through direct project communication, engineering response within a few hours, manufacturing coordination, inspection support, packaging, and shipment management. This provides global buyers with documented engineering support before production and responsive online pre-sale and after-sale communication throughout the tooling and molding lifecycle.
For mold owners who need a maintenance review, replacement insert, production repair, or new rapid tool, TEAM Rapid can assess mold design risks through DFM feedback before machining begins. The company supports projects from one prototype to more than 100,000 parts, making it suitable for product launches, engineering validation, bridge production, replacement tooling, and scalable manufacturing programs. Buyers can submit drawings, CAD files, resin requirements, annual volume estimates, target finish, and existing mold-condition photos through the global manufacturing quotation request process.
By 2026, injection mold maintenance will increasingly move from calendar-based servicing toward data-supported predictive maintenance. Mold sensors, cavity pressure monitoring, cooling-flow monitoring, machine data capture, shot-count tracking, and digital maintenance records will help factories identify failure patterns earlier. Rather than waiting for flash, warpage, or a broken ejector pin, maintenance teams will use production data to plan service before quality declines.
Artificial intelligence-assisted process monitoring is expected to improve defect pattern recognition. Systems may compare cycle time, pressure curves, mold temperature, material moisture, ejection force, and cavity performance to identify abnormal trends. Digital mold passports will also become more common, particularly for global supply chains where tools may be moved between production sites. These records can include steel specifications, spare-part drawings, modification history, maintenance intervals, validation results, and approved process windows.
Sustainability will also influence tooling decisions. Better cooling design can reduce cycle time and energy use. Preventive care lowers scrap rates, extends mold life, and reduces the need for premature tool replacement. Manufacturers are also likely to increase attention to water treatment, closed-loop cooling systems, resin recovery, lower-emission production, and material traceability. International regulations affecting packaging, recycled content, medical traceability, product safety, and environmental reporting will make documented production and maintenance records increasingly valuable.
The frequency depends on mold complexity, resin type, surface finish, number of cavities, production hours, and shot count. Basic cleaning should occur after each production run, while preventive maintenance may be scheduled every defined number of cycles. High-wear molds processing glass-filled, mineral-filled, flame-retardant, or corrosive materials usually need more frequent inspection.
Flash can result from damaged parting lines, worn shutoff surfaces, poor slide alignment, excessive injection pressure, inadequate clamping force, mold mismatch, contaminated mating surfaces, or damaged inserts. The correct solution requires inspection of both mold condition and molding parameters.
Yes. Restricted cooling flow can increase cycle time, create uneven cooling, cause warpage, change shrinkage, and produce inconsistent dimensions. Cooling systems should be checked for flow, leaks, mineral scale, corrosion, and blocked channels.
Lubrication should follow the mold maker’s recommendations and should be applied only to approved moving components. Excessive lubricant can contaminate cavity surfaces, attract debris, and affect cosmetic part quality. Clean before applying new lubricant.
Molds should be cleaned, dried, protected against corrosion where necessary, labeled with status information, and stored in a stable environment. Cooling circuits should be drained or dried for long storage periods. In humid environments, corrosion prevention is particularly important.
Often yes. Existing molds can sometimes be improved through cavity insert replacement, vent modification, cooling upgrades, gate adjustments, slide repair, hot runner servicing, polishing, or ejection-system changes. A tooling engineer should evaluate whether the base mold structure remains sound before investing in modifications.
Maintain the mold ID, shot count, resin processed, production dates, defect history, maintenance actions, replaced parts, photographs, inspection results, repair drawings, technician name, and next recommended service interval. These records make root-cause analysis faster and support consistent quality across different production locations.
-
Global Market Guide to Selecting Steel for Injection Molds
Selecting steel for injection molds should start with the resin, expected production volume, cosmetic finish, part tolerance, cooling requirement, and operating environment. P20 is usually the practical choice for low-to-medium volume molds and rapid tooling. H13 is preferred for higher-temperature processing, glass-filled plastics, and longer production life. S136 is the stronger choice for corrosion resistance, polished optical surfaces, medical components, transparent parts, and PVC processing.
For most Global market projects, use pre-hardened P20 for economical tooling, hardened H13 for demanding production cycles, and stainless S136 when corrosion protection and mirror polishing matter. Tool steel should be selected together with mold design, cooling layout, gate position, part geometry, and maintenance planning rather than as an isolated purchasing decision.
Global buyers should compare steel traceability, hardness certification, heat-treatment capability, machining quality, lead time, and maintenance support. Qualified international suppliers, including Chinese mold manufacturers with ISO-based quality systems, responsive pre-sales and after-sales engineering support, and cost-performance advantages, can be a strong option for projects requiring fast tooling and molded parts.
Injection mold steel affects much more than the initial tooling price. The selected grade influences machining time, polishing performance, cycle time, cooling efficiency, wear resistance, mold life, dimensional stability, repairability, and consistency of molded parts. A low-cost material choice can become expensive if the cavity wears early, cooling channels corrode, molded surfaces develop defects, or the tool requires repeated welding and polishing.
For buyers in the Global market, material selection is especially important because products are often designed in one country, tooled in another, assembled in a third location, and sold through international distribution networks. A mold may need to run in Shenzhen, Ningbo, Singapore, Monterrey, Istanbul, Rotterdam, Chicago, or Frankfurt during its lifecycle. Steel selection must therefore consider transportation, storage humidity, resin availability, local maintenance capability, and production transfer requirements.
A well-selected steel grade supports predictable production. It helps control flash, sink marks, parting-line wear, ejector-pin galling, corrosion, polishing quality, and cavity dimensions. The correct steel also supports better DFM decisions, such as using appropriate draft angles, optimized ribs, balanced wall thickness, stable gate geometry, and adequate cooling circuits.
Injection mold steels are commonly grouped into pre-hardened steels, through-hardening steels, stainless steels, and specialty grades. The best choice depends on the working condition of each mold component. A mold base, cavity insert, core insert, slider, lifter, ejector plate, guide pin, and wear plate do not always need the same material.
Steel GradeTypical ConditionMain StrengthCommon Resin CompatibilityTypical Mold UsePractical LimitationP20Pre-hardened, commonly around 28–34 HRCGood machinability and economical tooling costABS, PP, PE, PS, PC, PA, TPERapid tooling, low-volume molds, housings, coversLower corrosion and wear resistance than hardened grades718 / 718HPre-hardenedBetter polishability and cleaner structure than standard P20ABS, PC, PMMA, PA, consumer-grade engineering plasticsMedium-volume cosmetic parts and mold insertsMay cost more than P20 without being necessary for simple partsH13Heat treated, often 48–52 HRC depending on applicationHot hardness, toughness, heat-check resistanceGlass-filled nylon, PC, PBT, PPS, high-temperature materialsCore inserts, cavities, slides, high-wear componentsRequires controlled heat treatment and longer manufacturing timeS136Hardened stainless steelCorrosion resistance and high-polish capabilityPVC, PMMA, PC, medical resins, optical-grade materialsMedical molds, transparent parts, humid production environmentsHigher material and machining costNAK80Pre-hardenedFine polishability, stable machining, good EDM finishABS, PC, PMMA, consumer and automotive cosmetic partsTextured surfaces, glossy covers, display-related housingsNot the first choice for highly corrosive resin environments420 Stainless SteelHardened stainless tool steelCorrosion resistance and moderate polishabilityPVC, flame-retardant plastics, medical resinsBudget-conscious corrosion-resistant mold componentsGrade quality varies significantly between steel millsD2 / Cr12MoVHardened cold-work steelHigh wear resistanceFilled plastics and abrasive applicationsWear inserts, cutters, high-wear mechanical featuresCan be less tough and more difficult to repair than H13The table shows why P20, H13, and S136 are not direct substitutes. P20 solves cost and lead-time needs. H13 solves thermal fatigue and abrasive wear challenges. S136 solves corrosion, cleanability, and high-finish requirements. A mold can also combine these steels. For example, a P20 mold base may use H13 gate inserts and slides, while S136 is reserved for cavity inserts exposed to PVC or moisture-sensitive applications.
P20 is one of the most widely used mold steels for injection molding because it is supplied pre-hardened and can often be machined without a separate hardening process. This reduces tooling lead time and avoids dimensional distortion associated with post-machining heat treatment. P20 is commonly selected for rapid tooling, low-volume manufacturing, bridge production, and medium-volume injection molds.
It performs well with common materials such as polypropylene, polyethylene, ABS, polystyrene, standard nylon, TPE, and many general-purpose engineering plastics. It is a sensible choice for enclosures, housings, trays, caps, appliance parts, office equipment components, automotive interior trim, and industrial covers where ultra-high polish or extreme wear resistance is not required.
However, P20 should be evaluated carefully for glass-filled materials, PVC, flame-retardant grades, highly humid production conditions, and tools intended to produce hundreds of thousands or millions of cycles. In such cases, corrosion, abrasion, and cavity wear can reduce tool performance. Surface treatments, nitriding, chrome plating, or localized H13 and S136 inserts may improve performance without requiring the entire mold to be made from premium steel.
H13 is a hot-work tool steel known for toughness, thermal stability, and resistance to heat checking. While it is strongly associated with die casting, it is also valuable in injection molds that process high-temperature resins, glass-filled materials, and abrasive compounds. H13 is frequently used for core inserts, cavity inserts, slides, lifters, gate inserts, and parts of a mold subjected to repeated thermal loading.
The steel is generally machined in an annealed or softer condition, then heat treated to the required hardness. This process demands controlled machining allowances, stable heat treatment, stress relief, precision grinding, and inspection. Poor heat treatment can lead to cracking, distortion, weak toughness, or inconsistent hardness. For that reason, buyers should request material certificates, hardness reports, and clear heat-treatment specifications.
H13 is suitable for reinforced nylon, PBT, PPS, high-temperature polycarbonate applications, and other resins that increase surface wear. It can also be selected for features with thin steel conditions, sharp ribs, aggressive shutoffs, or complex moving components. Although the upfront tool cost is higher than P20, the investment can be justified when the mold must maintain dimensions over long production runs.
S136 is a stainless mold steel commonly specified where corrosion resistance, polishability, cleanliness, and surface quality are critical. It is particularly suitable for PVC, flame-retardant resins, medical-grade polymers, transparent plastics, moisture-prone manufacturing conditions, and applications requiring a mirror finish.
For clear polycarbonate, PMMA, medical diagnostic housings, optical components, transparent lenses, laboratory consumables, cosmetic packaging, and high-gloss consumer parts, S136 can support better surface quality when machining and polishing are properly controlled. It is also useful for molds that may be stored or transported through humid ports and coastal regions where rust prevention is a practical concern.
S136 is more expensive than P20 and generally requires more careful machining, polishing, and heat treatment. The added cost is worthwhile only where corrosion control, optical surface requirements, hygienic maintenance, or part appearance demands it. For standard black ABS housings, P20 or 718H may be commercially more reasonable.
The resin is often the fastest starting point for selecting mold steel. Some resins are relatively gentle on the cavity, while others are abrasive, corrosive, or processed at high temperatures. Production volume then determines whether the initial investment in a higher-grade steel will return value through reduced maintenance and longer service life.
Project RequirementRecommended Steel DirectionReason for SelectionTypical PartsRecommended Tooling StrategyRisk if Under-SpecifiedPrototype or bridge production below 5,000 partsP20 or aluminum with steel insertsFast machining and lower startup costValidation housings, test enclosures, launch samplesRapid tooling with replaceable insertsUnnecessary capital cost from premium production steelLow-to-medium volume consumer productsP20 or 718HBalanced cost, machining speed, and surface qualityCovers, storage trays, appliance shellsPre-hardened mold base and quality cooling designPremature polish loss if low-grade material is usedHigh-gloss or textured cosmetic surfaces718H, NAK80, or S136Improved polishability and surface consistencyDisplay bezels, premium cases, cosmetic capsDedicated polishing allowance and controlled EDM processOrange peel, pitting, inconsistent texture reproductionGlass-filled or abrasive engineering plasticsH13, D2, or hardened wear insertsHigher wear resistance at gates and flow pathsGears, structural brackets, automotive under-hood partsHardened inserts in high-wear zonesGate erosion, flash, unstable dimensionsPVC, flame-retardant, or corrosive resinS136 or 420 stainless steelCorrosion resistance protects cavity surfaces and cooling areasElectrical components, medical parts, fittingsStainless cavity/core inserts and preventive maintenanceRust, pitting, surface defects, difficult mold cleaningHigh-temperature processingH13 or specialty hardened steelThermal stability and resistance to heat fatiguePPS connectors, reinforced nylon componentsHeat-treated inserts with engineered coolingCracking, deformation, accelerated wearTransparent optical or medical partsS136Mirror polishability, corrosion resistance, clean maintenanceLenses, clear chambers, diagnostic housingsHigh-quality polishing and protected handling processFlow marks, surface haze, rust contaminationMaterial selection should also account for the part’s visual standard. A molded surface with leather texture, matte finish, or paint coverage may not need premium polishing steel. By contrast, a clear lens, piano-black housing, chrome-plated decorative part, or medical component can reveal small cavity defects immediately. For these applications, steel cleanliness, polishing skill, EDM parameters, and mold protection procedures are as important as the nominal steel grade.
Buyers should not approve mold steel based on a grade name alone. Steel names can vary by mill, country, and supplier. A documented equivalent may perform differently depending on chemical composition, remelting process, cleanliness, delivery hardness, and heat-treatment quality. Purchasing teams should request clear specifications before tooling begins.
Buying CriterionWhat to ConfirmWhy It MattersSuggested Buyer ActionCommon Problem AvoidedRelevant Project StageSteel mill traceabilityMaterial certificate, heat number, grade specificationConfirms the actual steel source and compositionRequest certificates for cavity, core, and major insertsUnverified substitute materialQuotation and tooling kickoffHardness conditionPre-hardened level or final HRC targetDetermines wear resistance and machining approachState hardness requirements on approved drawingsSoft cavities or brittle insertsDesign reviewHeat treatmentVacuum hardening, tempering, stress relief, inspection methodControls distortion, toughness, and service lifeRequire heat-treatment records for H13 and S136 insertsCracking and unstable dimensionsTool manufacturingSurface finish requirementSPI finish, texture standard, optical polishing needDefines steel polishability and process planningProvide approved appearance samples where possibleMismatch between expected and actual cosmetic qualityDFM and mold designResin dataFull resin grade, filler percentage, flame-retardant packageIdentifies abrasion and corrosion riskShare resin datasheet before steel is orderedWrong material selection for filled or corrosive resinEarly engineeringTool life targetExpected annual volume and total lifetime cyclesSets a rational tooling investment levelSpecify prototype, bridge, low-volume, or production intentOverspending or premature mold wearRFQ stageMaintenance planCleaning, lubrication, spare inserts, storage protectionExtends mold life after deliveryInclude maintenance instructions and spare-part listRust, seizure, avoidable downtimeProduction and after-salesFor international projects, the mold supplier should provide a mold drawing, DFM report, material list, trial report, inspection information, and recommended maintenance schedule. If production will move between facilities, consider using standard mold components from globally recognized suppliers such as HASCO, DME, Meusburger, Misumi, or compatible equivalents. Standardization makes replacement parts and maintenance easier across regions.
Automotive suppliers often need H13 or hardened inserts for reinforced parts, clips, electrical connectors, under-hood components, and high-cycle interior systems. Consumer electronics brands frequently choose 718H, NAK80, or S136 for polished covers, device housings, display frames, and textured surfaces. Medical manufacturers may specify S136 because the mold needs corrosion resistance, cleanability, stable polish, and consistent output for regulated components.
Industrial equipment manufacturers need reliable steel choices for housings, cable-management systems, valves, fittings, control enclosures, and durable functional parts. Appliance companies may combine P20 mold bases with hardened inserts where repetitive shutoffs or wear areas exist. Packaging and consumer goods producers often balance cycle time, cavity count, and mold life, making cooling design and wear-resistant gate inserts critical.
Projects serving coastal regions, humid warehouses, and international shipping routes also benefit from corrosion planning. A mold stored near ports such as Shanghai, Hong Kong, Rotterdam, Hamburg, Los Angeles, Singapore, Dubai, or Santos can face environmental exposure if preservation is inadequate. Mold steel selection should be paired with anti-rust treatment, sealed packing, desiccants, and documented storage procedures.
Consumer electronics enclosure: A company launching a PC-ABS handheld device housing requires 20,000 pieces with a textured external surface and internal snap-fit features. P20 may be suitable for the mold base, while 718H can be selected for visible cavity surfaces if cosmetic requirements are stricter. H13 may be used locally for thin shutoffs and high-wear latch features. This approach controls cost while protecting critical areas.
Medical diagnostic device cover: A medical equipment developer needs clean white plastic covers and transparent inspection windows. The opaque housing may use 718H or P20 depending on volume, while transparent window tooling should use S136 to support high polish and reduce corrosion risk. The project should include validation samples, dimensional inspection, documented resin selection, and mold-cleaning guidance.
Glass-filled nylon automotive clip: An automotive supplier requires a clip that will run in a 150,000-piece program using glass-filled PA66. Standard P20 cavity surfaces may wear too quickly around gates, shutoffs, and thin locking features. H13 inserts, appropriate hardness, and planned spare components improve durability and reduce long-term maintenance costs.
PVC electrical fitting: A manufacturer needs molded PVC conduit fittings for export distribution. Because PVC processing can generate corrosive by-products, S136 or another suitable stainless steel should be used in cavity and core areas. The supplier should also specify regular mold cleaning, protective storage, and corrosion-control procedures.
The following companies are established mold steel suppliers with products used across international tooling markets. Buyers should verify the exact grade, local stock availability, certification package, and equivalent specification for each project. The best source may depend on steel availability near the selected tool shop, transportation time, and required technical support.
CompanyPrimary BaseService RegionsCore StrengthsKey OfferingsBest FitUddeholmHagfors, SwedenEurope, North America, Asia-Pacific, global distributionPremium tool steel development, clean steel technology, technical supportStavax ESR, Orvar Supreme, pre-hardened and stainless mold steelsHigh-polish, medical, automotive, and demanding production moldsASSABSingaporeAsia-Pacific, China, Europe, Americas through global networkTool steel supply, machining support, local stock programs718HH, P20 variants, Stavax ESR, Orvar SupremeRegional Asian tooling programs and internationally standardized projectsDaido SteelNagoya, JapanJapan, Asia, Europe, North AmericaSpecialty steels, pre-hardened grades, consistent material qualityNAK80, DC53, tool steels for molds and precision manufacturingHigh-polish consumer products and precision mold applicationsBÖHLER EdelstahlKapfenberg, AustriaEurope, Americas, Asia-Pacific, global sales networkSpecial steels, stainless grades, technical metallurgy expertiseM340, W302, corrosion-resistant and hot-work tool steelsMedical, optical, high-temperature, and corrosion-sensitive moldingFinkl SteelChicago, United StatesNorth America and international industrial customersLarge blocks, mold base steel, domestic supply capabilityPre-hardened mold steels, mold plates, specialty steel productsNorth American mold builders and large mold base requirementsMeusburgerWolfurt, AustriaEurope and global mold-making customersStandard mold bases, precision plates, mold componentsMachined plates, standard frames, guide elements, accessoriesToolmakers needing standardized components and fast configurabilityHitachi Metals / ProterialTokyo, JapanJapan and international industrial marketsSpecialty alloy expertise and high-performance material developmentTool steels and specialty materials through regional channelsProjects requiring specific Japanese material standards or equivalentsThese suppliers provide valuable options, but steel brand alone does not guarantee mold quality. The mold maker’s CNC machining, EDM, polishing, heat treatment, fitting, cooling design, assembly, mold trial process, and inspection discipline determine whether the selected steel performs as expected. Buyers should evaluate the complete tooling process, not only the steel certificate.
TEAM Rapid supports Global market customers with rapid tooling, plastic mold making, injection molding, CNC machining, finishing, assembly, and direct shipping from an integrated China-based manufacturing network. With more than 10 years of manufacturing experience, ISO 9001:2015 quality management certification, more than 6,000 delivered projects, and customers in over 25 countries, the company applies DFM analysis before tooling to identify risks involving resin flow, wall thickness, draft, cavities, cooling, cycle time, and material choice. For mold steel selection, TEAM Rapid can recommend practical combinations such as P20 for cost-efficient rapid tooling, H13 inserts for wear-sensitive areas, and S136 for corrosion-resistant or polished cavities, supported by controlled machining, EDM, polishing, inspection, and trial molding. The company serves end users, product designers, distributors, dealers, brand owners, startups, and established manufacturers through flexible OEM, ODM, low-volume, recurring production, wholesale, and regional supply cooperation models. Its operational model is turnkey manufacturing and customer-owned tooling support rather than BOO or on-site bulk supply services. Although TEAM Rapid does not claim overseas subsidiaries or local warehouses in every Global market location, it has established international service experience through one-to-one engineering communication, fast quotation responses, integrated production resources, packaging, limited warehousing, and direct shipment to customers in markets including the USA, UK, France, Germany, and other regions. This combination gives buyers practical pre-sale engineering support, production updates, inspection-based quality control, and after-sales coordination without managing multiple disconnected suppliers.
Customers needing a faster transition from prototype validation to low-volume or production molding can review rapid tooling services for international product development to understand available tooling pathways. For a steel recommendation based on resin, part geometry, annual volume, and surface requirement, buyers can request a custom injection mold tooling quotation with 3D files and material details.
By 2026, mold steel selection is expected to become more data-driven. Toolmakers are increasingly combining mold-flow simulation, cycle-time analysis, sensor data, predictive maintenance, and production traceability to determine where premium steel provides measurable value. Rather than building an entire tool from one grade, more projects will use hybrid construction: economical mold bases combined with higher-performance inserts in gates, cores, slides, shutoffs, and corrosive-resin zones.
Sustainability will also influence tooling decisions. Longer-lasting molds reduce replacement steel consumption, machine downtime, material waste, and emergency logistics. Better cooling performance can shorten cycle time and reduce energy use per molded part. Manufacturers are also expected to place greater emphasis on repairable insert designs, reusable mold bases, optimized cavity counts, and modular tooling systems that extend the useful life of production assets.
Global policy and customer requirements are likely to increase demand for material traceability, recycled-content documentation, product quality records, and controlled chemical processing. Medical, automotive, electrical, and consumer brands may require more detailed evidence of resin compatibility, steel origin, inspection methods, and controlled production practices. For this reason, mold steel certificates, hardness reports, maintenance records, and trial documentation will remain essential purchasing documents.
Provide the following information when requesting a quotation or technical review: 3D CAD files, 2D drawings if available, resin brand and grade, filler percentage, flame-retardant requirement, annual production volume, total lifetime volume, required surface finish, color, cosmetic standards, mold location, target production date, and expected maintenance arrangements.
Also identify whether the tool is intended for prototype validation, bridge production, low-volume commercialization, or long-term production. This distinction helps prevent two common errors: paying for production-grade steel when rapid tooling is sufficient, or selecting low-cost steel for a tool that must run high volumes with abrasive resin.
P20 is suitable for many injection molds, especially rapid tooling, low-volume production, consumer housings, trays, covers, and general-purpose plastic parts. It is not always sufficient for corrosive resins, highly abrasive glass-filled materials, high-temperature molding, or very long production programs.
Choose H13 when the mold will process high-temperature or glass-filled resins, when thermal fatigue is a concern, or when critical inserts need improved wear resistance and toughness. H13 is often used selectively in gates, cores, slides, and shutoff areas instead of across the full mold.
S136 is a stainless mold steel with stronger corrosion resistance and high-polish capability. Its cost reflects the material properties, machining demands, heat-treatment requirements, and value in applications such as PVC molding, medical parts, transparent components, and humid production environments.
Yes. Many efficient molds use P20 for the mold base, H13 for high-wear inserts, and S136 for corrosion-sensitive or high-polish cavity areas. This mixed-steel strategy can improve performance while controlling tooling cost.
Steel grade can affect cooling efficiency and long-term cavity stability, but cooling channel design, water flow, mold temperature control, wall thickness, and resin processing conditions usually have a greater direct effect on cycle time. Steel should be selected together with thermal design.
Request material certificates, steel grade confirmation, hardness reports, heat-treatment records when applicable, mold drawings, DFM feedback, trial reports, inspection reports, and maintenance recommendations. These documents help protect quality during production and future mold transfers.
Yes. Established Chinese mold manufacturers can source and machine P20, H13, S136, 718H, NAK80, and equivalent grades. Buyers should verify material traceability, machining capability, heat-treatment controls, inspection procedures, communication quality, and after-sales support before selecting a supplier.
-
SPI Mold Classifications Guide for Global Market Buyers
SPI mold classifications describe the expected service life, construction quality, maintenance standard, and production suitability of an injection mold. Class 101 is the highest-duty category for very large production volumes, while Class 102 suits medium-to-high production, Class 103 is a general-purpose production mold, Class 104 is intended for low-volume production, and Class 105 is normally a prototype or sample mold.
For global buyers, the practical choice is usually Class 103 for regular commercial production, Class 104 for limited launches or market testing, Class 101 or Class 102 for long-running programs, and Class 105 for early design validation. The classification is a planning guide rather than a substitute for a detailed tooling specification covering steel, cavities, cycle time, cooling, tolerances, maintenance, and acceptance testing.
Qualified international suppliers, including experienced Chinese mold and molding companies with ISO certification, documented inspection, export experience, and responsive pre-sales and after-sales support, can also be considered. Their cost-performance advantage may be significant when engineering review, tooling manufacture, molded parts, finishing, assembly, and delivery are coordinated under one program.
The Society of the Plastics Industry, now known as the Plastics Industry Association, developed a widely used mold classification system to help buyers match tooling investment with expected production demand. The classes are commonly referenced by mold makers, injection molders, product developers, and procurement teams across North America, Europe, Asia, and other manufacturing regions.
The classification does not simply rank a mold as good or bad. It indicates how extensively the tool is engineered, how durable its components are expected to be, how much production it should support, and how suitable it is for repeated manufacturing. A Class 105 mold can be perfectly appropriate for a prototype, while a Class 101 mold may be wasteful for a short market trial.
SPI terminology is often used together with a purchaser’s own tooling standard. A buyer may specify P20 or H13 steel, hardened cavity inserts, replaceable wear plates, hot-runner brands, mold-flow analysis, cavity pressure monitoring, or a defined number of accepted shots. These details should be written into the purchase order because classification alone cannot define every technical feature.
Class 101 molds are built for extremely high production volumes and long service life. They normally use high-grade, hardened tool steels in critical areas, carefully engineered cooling, robust ejection, replaceable wear components, and strict dimensional control. They are suitable for products expected to run continuously for many years, often in demanding automotive, medical, consumer, or industrial programs.
Class 101 tooling typically requires the greatest upfront investment. It may include multiple cavities, hot runners, automated part removal, complex slides or lifters, cavity pressure monitoring, and extensive preventive-maintenance provisions. The higher cost can be justified when millions of cycles, low downtime, and consistent part quality are more important than the lowest initial tooling price.
Class 102 molds are intended for medium-to-high production volumes where reliable repeatability is essential but the projected life may not justify every feature of a Class 101 tool. They are often used for commercial products with established demand, replacement parts, and programs expected to run for several years.
Depending on the product and resin, a Class 102 mold may use hardened steel in wear areas, pre-hardened steel in other sections, a standard or premium hot runner, engineered cooling channels, and replaceable inserts. It can offer a practical balance between tool life, maintenance access, cycle performance, and capital cost.
Class 103 is widely selected for ordinary production requirements. It is generally suitable for moderate production quantities, new products entering the market, and parts where the expected annual volume is meaningful but not extremely high. Many low-to-medium volume commercial programs use a Class 103 mold as their starting production tool.
The exact life depends on material, part geometry, cycle time, mold maintenance, and steel selection. Abrasive glass-filled resins, corrosive additives, high injection pressure, and frequent color changes can shorten useful life. A Class 103 tool should still receive proper cooling design, venting, ejection analysis, dimensional inspection, and trial validation.
Class 104 molds are designed for limited production runs. They can be appropriate for pilot production, seasonal products, regional launches, spare parts, customized products, and products whose commercial demand is still uncertain. Aluminum, pre-hardened steel, or other cost-efficient materials may be considered when the expected shot count is limited.
Class 104 does not mean careless construction. The mold must still produce acceptable parts and provide safe operation. Buyers should define the expected quantity, number of production batches, storage conditions, and repair responsibility. A low-volume tool that is maintained correctly can sometimes exceed its original target life.
Class 105 molds are intended for prototype quantities, design verification, and very limited sampling. The tool may use aluminum, soft steel, simplified inserts, or other economical construction methods. It is useful for checking assembly, appearance, ergonomics, basic function, and early customer feedback before committing to a longer-life production mold.
Class 105 is not normally the right choice for a product launch requiring thousands of parts every month. However, it can reduce risk when a design is still changing. The buyer should confirm whether the tool is repairable, whether inserts can be upgraded, and whether the sample parts accurately represent the final production process.
The following comparison gives a practical starting point. Actual tool life is affected by resin, mold design, maintenance, machine settings, part geometry, and the supplier’s workmanship. Buyers should request a written guarantee or agreed acceptance target rather than relying only on a class label.
SPI classTypical purposeRelative production volumeTypical construction approachCommercial decisionClass 101Continuous, demanding productionVery high, often multi-million cycle programsHardened steel, robust components, optimized cooling and maintenance accessChoose when downtime and replacement-tool risk are expensiveClass 102Established commercial productionHigh to medium-highDurable steel in wear areas with engineered cooling and ejectionChoose for reliable multi-year programs without maximum-duty investmentClass 103Standard commercial partsModerateProduction-grade steel and conventional or hot-runner systemsChoose for most new products with predictable demandClass 104Limited production and pilot runsLowCost-efficient steel or aluminum with appropriate production featuresChoose for launches, seasonal products, and regional demand testsClass 105Prototype and design validationVery lowPrototype inserts, aluminum, soft steel, or simplified toolingChoose while geometry, material, or market acceptance is still changingCustom specificationSpecial performance requirementDefined by the programBuyer-selected steel, components, monitoring, and maintenance strategyUse when an SPI class alone cannot describe the required risk levelThis table is useful for early budgeting, but it should be followed by a tooling design review. For example, a small medical housing made from glass-filled resin may need stronger wear protection than a much larger part made from an unfilled commodity polymer. Similarly, a tool with complex lifters may require more maintenance access than a simple two-plate mold.
Start with the total expected lifetime quantity, not only the first purchase order. Add forecast demand, replacement-part requirements, regional sales, engineering samples, rejected parts, safety stock, and possible future programs. A tool selected for 20,000 parts may become uneconomical if the product later sells 500,000 units.
Next, evaluate the resin. Polypropylene and ABS generally create different tooling demands from glass-filled nylon, PEEK, PC, PVC, or flame-retardant engineering polymers. Abrasive fillers, corrosive additives, high processing temperatures, and demanding cosmetic surfaces may justify stronger steel, surface treatment, or a higher classification.
Review the product architecture. Undercuts, threads, collapsible cores, lifters, thin walls, deep ribs, texture, optical surfaces, tight sealing features, and insert molding all affect tooling cost and maintenance. A supplier should provide a DFM report identifying draft, wall-thickness, sink, weld-line, air-trap, gate, warpage, and ejection risks before steel is cut.
Consider production geography and logistics. A buyer in the United States may compare suppliers in Ohio, Michigan, California, Mexico, Germany, the United Kingdom, or China. A buyer in Europe may evaluate providers near Stuttgart, Milan, Lyon, Birmingham, or Shenzhen. Tool ownership, repair location, shipping terms, spare inserts, and response time can matter as much as the initial quotation.
Finally, connect the mold class to the business model. Prototype tooling may be best for a funded development project, rapid tooling may be suitable for a short launch window, and hardened production tooling may be needed for a regulated or safety-critical product. Do not pay for a Class 101 mold if the design is likely to change next month.
Specification areaQuestions to askWhy it mattersRecommended evidenceSteel and hardnessWhich steel grades are used for cavities, cores, inserts, and plates?Steel affects wear life, polishability, corrosion resistance, and repair optionsSteel certificates, hardness records, and component drawingsCavity configurationIs the mold single-cavity, multi-cavity, family, or interchangeable?Cavity count changes unit cost, balance, cycle output, and qualification effortLayout drawing, filling analysis, and cavity identification planRunner and gatingWill the tool use cold runners, hot runners, valve gates, or sequential gating?Runner design influences scrap, appearance, pressure, cycle time, and maintenanceRunner diagram, component brand, and spare-parts listCoolingAre channels balanced and accessible for cleaning?Cooling affects warpage, cycle time, tool life, and dimensional consistencyCooling layout, flow analysis, and temperature trial resultsEjection and automationHow will the part be ejected, detected, removed, and packed?Reliable ejection reduces deformation, damage, and operator dependencyEjection sequence, robot interface, and sample-cycle videoAcceptance and maintenanceWhat shot target, dimensional tolerance, repair response, and warranty apply?Clear obligations prevent disputes after deliverySigned acceptance criteria, inspection report, and maintenance scheduleAsk for a mold-flow report when the part has long flow lengths, thin walls, multiple gates, tight cosmetic requirements, or difficult engineering resin. Mold-flow simulation cannot eliminate all production risk, but it can expose likely filling imbalance, weld lines, air traps, cooling differences, and warpage before machining.
Class 101 tooling usually has the highest initial price because it may require hardened steel, precision components, complex cooling, cavity balancing, automation interfaces, and more extensive validation. Class 105 tooling usually has the lowest price, but its limited life and lower upgrade flexibility can create additional cost if the design is not yet stable.
Tool price should be separated from molded-part price. A low-cost mold can create a high unit cost if it has a long cycle, excessive runner waste, manual demolding, or frequent maintenance. Conversely, a more expensive multi-cavity mold may produce a lower total cost when volume is sufficiently high.
Lead time depends on part complexity, steel availability, mold size, number of cavities, surface finish, hot-runner procurement, design approval, sampling, and correction loops. Buyers should request a timeline that separates DFM approval, steel ordering, CNC machining, EDM, polishing, assembly, first trial, modifications, final inspection, and shipment.
For customers that need a bridge between prototypes and full production, rapid tooling can be practical. TEAM Rapid states that its rapid tooling and molded-part programs can often be completed in approximately 5 to 25 days, depending on project requirements. Its engineers also provide DFM and manufacturability analysis to identify risks before tooling begins. Buyers should confirm the exact schedule, material, cavity count, inspection plan, and shipping method for each project.
The following companies are established names that buyers may evaluate for mold systems, injection molding equipment, tooling, or production support. Their capabilities and service availability vary by country and project size, so a buyer should confirm whether the quoted provider is the manufacturer, an authorized regional office, or an independent mold-making partner.
CompanyService regionsCore strengthsKey offeringsBest fitTEAM RapidChina with export support for North America, Europe, Asia, and other global marketsFast tooling, engineering-led DFM, flexible quantities, and integrated manufacturingRapid tooling, injection molding, CNC machining, 3D printing, vacuum casting, die casting, finishing, assembly, packaging, and direct shippingPrototypes, Class 104 or Class 103 programs, low-volume production, and transition to larger productionHusky TechnologiesNorth America, Europe, Asia, and worldwide customer operationsHigh-output injection systems and packaging production technologyInjection molding systems, hot runners, controllers, molds, and service supportHigh-volume packaging and demanding production environmentsMilacronNorth America, Europe, India, China, and international marketsIntegrated injection molding machinery, controls, and hot-runner technologyInjection machines, hot runners, process controls, mold technologies, and lifecycle servicesIndustrial and commercial production requiring coordinated equipment supportENGELAustria, Germany, the United States, China, and global marketsAutomation, process integration, precision molding, and energy-efficient cellsInjection molding machines, robots, turnkey cells, process control, and technical serviceAutomotive, medical, packaging, and complex automated productionARBURGGermany, Europe, the United States, Asia, and international marketsPrecision injection molding, automation, and process developmentAll-electric and hydraulic machines, robots, turnkey systems, and application consultingPrecision components, medical products, technical parts, and connected factoriesHaitian InternationalChina with extensive export distribution and service coverageBroad injection machine range and competitive capital costServo-hydraulic and electric injection molding machines, automation options, and regional supportCost-sensitive production programs and general industrial moldingThese companies do not all offer the same type of service. Husky, Milacron, ENGEL, ARBURG, and Haitian are primarily associated with molding machines, systems, and production technology, while TEAM Rapid is positioned as a manufacturing partner for tooling, parts, and related processes. A purchaser seeking a mold should clarify whether the supplier will design and manufacture the tool, run it in-house, transfer it to a customer-owned plant, or provide only equipment.
In the United States and Canada, buyers often prioritize technical documentation, mold ownership, repair turnaround, domestic sampling, and compatibility with existing molding machines. Ask whether the supplier can provide inch or metric drawings, SPI surface requirements, cavity-pressure data, spare inserts, and a clear process for returning a tool for repair.
In Germany, France, Italy, and the United Kingdom, buyers frequently focus on traceability, dimensional capability, sustainability reporting, regulatory documentation, and integration with established quality systems. Suppliers serving these markets should be able to communicate clearly in English or the required local business language and provide controlled revisions of drawings and inspection reports.
In Japan, South Korea, Singapore, and other Asian manufacturing hubs, buyers may emphasize precision, rapid engineering communication, automation compatibility, and local maintenance coordination. In Australia, the Middle East, Africa, and Latin America, shipping reliability, spare parts, remote troubleshooting, customs documentation, and regional distributor support may be especially important.
Regardless of location, request at least one video or live review of the supplier’s tooling workshop, a sample inspection report, evidence of comparable resin experience, and references for a similar mold size or complexity. A polished website is not sufficient evidence of manufacturing capability.
TEAM Rapid combines ISO 9001:2015 quality management with more than 10 years of manufacturing experience, over 6,000 delivered projects, more than 500 customers, and service to customers in more than 25 countries; its product strength comes from controlled plastic and metal material selection, in-house machining and tooling capability, complete inspection, DFM review, and production processes that cover injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, die casting, sheet metal fabrication, finishing, assembly, and packaging rather than relying only on order taking. It serves end users, product developers, distributors, dealers, brand owners, startups, established manufacturers, and individual innovators through practical OEM and ODM cooperation, project-based production, wholesale quantities, low-volume orders, recurring supply, and regional distribution arrangements where commercially appropriate; its flexible capacity extends from one prototype to more than 100,000 parts. TEAM Rapid’s published profile does not claim overseas subsidiaries or permanent local warehouses in every customer country, so buyers should verify the exact local stock and repair arrangement, but the company provides China-based export coordination, limited warehousing, direct shipping, one-to-one engineering communication, rapid online response, inspection documentation, and after-sales project support for customers in North America, Europe, Asia, and other markets, with experience handling both Asian and Western business practices. It provides EPC/turnkey and customer-owned plant solutions for tooling, molded parts, assembly, packaging, and supply coordination when specified, not BOO or on-site bulk supply services, and its China manufacturing base can offer a cost-performance advantage while maintaining a documented route from prototype through low-volume and volume production.
For a buyer comparing mold classifications, TEAM Rapid may be relevant when the project requires Class 105 prototype tooling, Class 104 limited production tooling, Class 103 general-purpose production, or a staged path from sample validation to repeatable commercial supply. Its engineering team can review draft angles, wall thickness, parting lines, gates, cooling, ejection, shrinkage, and material selection before quotation. Customers can begin with the rapid tooling service for global projects and submit drawings, 3D files, material requirements, annual volume, and target delivery through the online manufacturing quotation form.
Automotive programs may require Class 101 or Class 102 tooling for interior trim, exterior components, under-hood parts, ducts, brackets, and functional housings. Glass-filled materials, dimensional stability, surface texture, and long production life should be considered together.
Medical and laboratory products often require controlled materials, traceability, clean handling, tight dimensional requirements, and validated processes. A Class 103 or Class 102 mold may be suitable for a commercial device, while Class 105 or Class 104 tooling can support early design verification. Regulatory requirements must be agreed separately because SPI classification does not certify a medical product.
Consumer electronics, appliances, communication products, office equipment, sanitary products, and industrial controls often use Class 103 or Class 104 molds depending on forecast quantity. Cosmetic appearance, texture, color consistency, snap fits, living hinges, light pipes, and assembly alignment can be more important than extreme shot life.
Packaging, closures, thin-wall containers, and high-output caps often require specialized multi-cavity tools, hot runners, balanced filling, high-speed cooling, and automated inspection. These applications may justify Class 101 or Class 102 construction even when the individual part is small.
A startup developing a handheld diagnostic accessory may still be changing the enclosure, battery interface, and button geometry. Class 105 tooling or a rapid aluminum tool can produce samples for ergonomic testing and initial assembly checks. Once the design is frozen and demand is validated, the supplier can convert the design into Class 103 or Class 102 production tooling with improved steel and a multi-cavity layout.
A brand selling a seasonal organizer may forecast 15,000 to 40,000 parts over two years. A Class 104 mold may be financially appropriate if the design is stable and the tool is stored correctly between seasons. The buyer should retain spare inserts, document cleaning procedures, and confirm whether the tool can be upgraded if sales exceed expectations.
An automotive supplier expecting sustained annual production and strict appearance requirements may select Class 101 or Class 102 tooling. The specification should include material grade, texture standard, cavity balance, cooling performance, dimensional capability, replacement inserts, preventive maintenance, and tool transfer provisions. A low-cost prototype tool can still be used first to validate fit and surface design.
An industrial equipment manufacturer may need only 3,000 initial housings while testing several sales channels. Class 103 tooling offers a reasonable middle ground when the design is substantially mature but future demand is not fully known. A modular insert design can preserve the option to modify connectors, mounting bosses, or label areas without replacing the entire mold.
These are planning scenarios, not guaranteed production results. The correct class should be confirmed through part geometry, resin, forecast, machine capability, quality requirements, and the supplier’s documented tooling proposal.
TrendTechnology or policy driverEffect on mold classification decisionsBuyer actionDigital mold monitoringSensors, connected controllers, cavity-pressure measurement, and cloud analyticsImproves traceability and helps extend useful life through predictive maintenanceSpecify data ownership, sensor locations, alarms, and reporting requirementsEnergy-efficient moldingAll-electric machines, optimized cooling, heat recovery, and lower-carbon production targetsCycle efficiency may influence total cost more than initial mold priceRequest cycle-time assumptions, cooling analysis, and energy data where availableRecycled and bio-based resinsExtended producer responsibility, recycled-content rules, and customer sustainability goalsVariable shrinkage, contamination, and additives may increase tooling and process riskValidate the actual resin grade and test dimensional stability before production releaseModular and repairable toolingShorter product cycles, regional customization, and reduced material wasteReplaceable inserts can make Class 103 or 104 tools more adaptableAsk for insert boundaries, spare-part pricing, and modification accessDigital product passportsTraceability and emerging product sustainability policies in major marketsTool and material records may become part of supply-chain complianceMaintain controlled steel, resin, inspection, maintenance, and revision recordsDistributed manufacturingRegional production, tariff management, shorter supply chains, and geopolitical risk reductionTool transferability and customer-owned plant compatibility become more valuableDefine ownership, export documents, machine interfaces, and relocation supportFuture classification decisions will increasingly consider the complete production system rather than only the physical mold. A tool that runs efficiently, records process data, supports recycled resin, and can be repaired or transferred may create lower total environmental and financial risk than a cheaper tool with poor documentation.
No. Class 101 is appropriate for very high-volume, long-running production. It may be unnecessary for a product with uncertain demand, frequent design changes, or a short market life. The best class is the one that matches risk, forecast, resin, quality requirements, and total cost.
It can be used for very limited sales or pilot quantities if the supplier confirms that the tool can produce acceptable parts. It is normally not recommended for sustained commercial production because service life and repeatability are limited compared with production tooling.
Class 103 is often a practical choice when the design is stable and moderate production is expected. Class 104 may be more economical for a limited launch, while Class 105 or rapid tooling is useful when the design still needs validation.
No. It provides a general tooling-life and construction framework, but the buyer should specify cavity steel, core steel, hardness, inserts, surface treatment, hot-runner components, and corrosion or wear requirements separately.
Published industry descriptions commonly associate Class 101 with the longest life and Class 105 with prototype quantities, but exact shot counts vary by source and application. Resin, pressure, temperature, maintenance, geometry, and workmanship have a major effect. Use a written supplier guarantee tailored to the project.
Compare technical capability, response time, inspection, ownership terms, logistics, repair support, and total landed cost. An international supplier can be attractive when it offers strong DFM, documented quality systems, competitive pricing, export experience, and reliable communication. A local supplier may be preferable when immediate on-site maintenance is essential.
Provide the 3D model, 2D drawing, resin and color, annual and lifetime quantity, target cycle time, cavity preference, surface finish, tolerance, machine information, packaging needs, delivery location, mold class target, inspection requirements, and expected launch date.
Yes. TEAM Rapid offers rapid tooling, injection molding, CNC machining, additive manufacturing, vacuum casting, metal processes, finishing, assembly, packaging, and direct shipping. Its stated production range extends from one prototype to more than 100,000 parts, subject to project requirements. Buyers should request a project-specific DFM report, schedule, tooling proposal, and quality plan.
TEAM Rapid provides EPC/turnkey and customer-owned plant solutions when defined by the project, including tooling, manufacturing coordination, assembly, packaging, and supply support. It is not presented as a BOO or on-site bulk supply provider. The commercial scope, ownership, local support, and shipping terms should be confirmed before order placement.
SPI mold classifications are most useful when they create a shared starting point between the buyer and the toolmaker. With a clear production forecast, verified material plan, DFM review, documented acceptance criteria, and realistic maintenance strategy, global buyers can avoid both under-designed prototype tooling and unnecessarily expensive production molds.
-
Family Tooling vs Multi-Impression Molds: Global 2026 Guide
Family tooling is usually the better choice when several different plastic parts are needed in similar quantities for a low-volume assembly, pilot launch, market test, or bridge-production program. A multi-impression mold is generally the stronger choice when one identical part is needed at higher volume, because it delivers better cycle efficiency, lower unit cost, more consistent balancing, and simpler quality control.
For global buyers, the decision should not be based on mold price alone. Select family tooling when part demand is balanced, design changes are still likely, and reduced upfront investment matters more than the lowest possible piece price. Select a multi-impression mold when demand for one component is stable, annual volume can absorb tooling investment, and the part must run efficiently across long production campaigns.
Global buyers can also consider qualified international suppliers, including Chinese manufacturers with ISO-certified quality systems, responsive pre-sales engineering, and practical after-sales support. Their cost-performance advantage can be especially valuable for rapid tooling, low-volume molding, and programs that need fast design iteration before committing to hardened production tooling.
A family mold contains cavities for two or more different parts in one mold base. The parts may belong to the same product assembly, such as a housing, cover, latch, bezel, button frame, or internal support. Every molding cycle produces one or more of each different component. This arrangement can reduce initial tooling expenditure because the customer purchases one mold system rather than several independent molds.
A multi-impression mold, also called a multi-cavity mold, contains multiple cavities for the same part. For example, an eight-cavity mold makes eight identical clips every cycle. Its purpose is output efficiency: the manufacturer spreads press time, operator labor, material handling, and machine setup across more pieces. Properly designed multi-cavity tools can support highly repeatable production for consumer products, automotive subcomponents, medical-device housings, electrical connectors, packaging parts, and industrial assemblies.
The central distinction is output mix. Family tooling produces a group of different components. Multi-impression tooling produces multiple copies of one component. That difference affects mold flow, runner design, cooling, filling pressure, visual consistency, production planning, maintenance, and the financial break-even point.
Core Comparison of Family Tooling and Multi-Impression ToolingDecision FactorFamily ToolingMulti-Impression ToolingBuyer ImpactParts produced per cycleDifferent parts within one assembly familyIdentical copies of one partDefines whether output matches assembly demand or single-part demandInitial tooling costOften lower than buying separate molds for every componentHigher as cavity count, hot runner complexity, and cooling increaseFamily tools can reduce launch capital for balanced setsUnit-cost potentialModerate; limited by the slowest or most difficult cavityStrong at stable volume because many identical parts run togetherMulti-impression tools usually win at high annual volumeProcess balancingMore difficult when parts vary in size, thickness, or flow lengthMore predictable because cavities are geometrically identicalHigher process risk may create scrap in family mold programsDesign changesChanges to one component can interrupt the full toolChanges affect one part design but may require updating every cavityEarly-stage products need careful change-control planningProduction flexibilityUseful when assembly components are consumed in equal quantitiesUseful when one high-demand part needs independent replenishmentService-parts demand can favor separate or multi-impression toolsQuality inspectionRequires cavity-specific checks across different part geometriesRequires cavity-to-cavity comparison of the same geometryInspection plans should be defined before trial productionThe table shows why neither option is universally cheaper. A family mold may save money at the beginning, but an unbalanced family tool can create cycle-time losses, uneven packing, warpage, flash, sink marks, or excessive rejection. A multi-impression tool may cost more to build, yet its economics become compelling when production is continuous and every cavity has a stable demand profile.
Global manufacturing programs increasingly require faster market entry, more regional customization, shorter product life cycles, and tighter inventory control. Product owners may develop in the United States, Europe, Japan, South Korea, India, Australia, or the Middle East while sourcing tooling and molded components through manufacturing hubs in Shenzhen, Dongguan, Ningbo, Suzhou, Shanghai, Ho Chi Minh City, Penang, Monterrey, Prague, Istanbul, and Detroit.
In this environment, mold selection is a supply-chain decision as much as an engineering decision. A family mold can reduce the number of tools shipped between factories and simplify initial component sourcing for a product launch. However, it may also lock multiple parts into one production schedule. If one part sells faster, changes frequently, or requires a different material, the shared tool can become a bottleneck.
Multi-impression molds align well with focused production cells, automated packaging, high-throughput assembly, and global replenishment programs. They are particularly valuable when a component is sold separately as a replacement part or used across multiple product models. High-volume molds are often paired with automation, vision inspection, cavity monitoring, robotic pick-and-place systems, hot runners, and statistical process control.
For shipments moving through major trade hubs such as Shanghai Port, Shenzhen’s Yantian Port, Ningbo-Zhoushan Port, Rotterdam, Hamburg, Los Angeles, Long Beach, Jebel Ali, Singapore, and Felixstowe, compact and predictable tooling programs help reduce launch uncertainty. Yet freight efficiency should never override manufacturability. A lower-cost mold that creates high scrap or delivery delays can cost more than a properly engineered tool.
Family and multi-impression mold designs are not limited to one construction method. Both can use cold runners, hot runners, interchangeable inserts, side actions, unscrewing mechanisms, insert molding features, overmolding arrangements, automated handling, and hardened steel or aluminum tooling solutions. The best configuration depends on part geometry, resin, volume, surface requirements, expected tool life, and whether the program is still evolving.
Tooling Configurations for Different Production ConditionsConfigurationTypical StructureBest FitMain LimitationSingle-cavity moldOne cavity for one partPrototypes, large parts, low volume, critical validationHighest piece cost at larger demandFamily moldMultiple different cavities in one moldBalanced assembly sets and bridge productionFlow and demand imbalance can create wasteMulti-impression cold-runner moldMultiple identical cavities with runner systemModerate-volume commodity or functional partsRunner scrap and secondary separation may be requiredMulti-impression hot-runner moldMultiple identical cavities with heated manifoldHigher-volume parts and resin-sensitive productionGreater upfront investment and maintenance complexityInterchangeable-insert moldShared base with replaceable cavity or core insertsProduct variants, revisions, and controlled market testingNot always ideal for maximum-cycle productionStack moldTwo or more molding faces operating togetherHigh-volume, smaller components with press constraintsComplex design, maintenance, and machine requirementsInsert or overmolding toolPlastic molded around metal or preformed substrateElectrical, medical, grip, sealing, and structural partsInsert placement and thermal control require validationFor many global startups and product-development teams, rapid aluminum tooling or pre-hardened steel tooling offers a sensible bridge. It enables functional molded parts before the demand forecast is proven. After market validation, the company can decide whether to add cavities, create dedicated tools, convert to hot-runner production, or move to hardened steel tooling for long-term output.
Family molds are frequently described as inexpensive because one mold base can hold multiple part cavities. This can be true when components share the same resin, color, production quantity, wall-thickness range, and process window. If those conditions are not present, apparent savings may disappear. A large thick-walled cavity may need a long cooling cycle, forcing a small thin-walled component to wait unnecessarily. If one cavity fills sooner than another, packing pressure can over-pack one part while under-packing another.
Multi-impression molds require more machining, polishing, cooling circuits, cavity matching, and validation. A four-cavity or eight-cavity tool must ensure that every cavity fills, packs, cools, ejects, and measures consistently. However, once validated, the mold can substantially lower conversion cost per piece. The financial case improves with higher production volume, stable demand, predictable material pricing, and long production runs.
Buyers should request an itemized cost model that separates mold-base cost, cavity inserts, hot-runner systems, steel grade, surface finish, texturing, side actions, trial shots, gauges, inspection, packaging, logistics, and expected maintenance. This comparison prevents a low initial quote from hiding future production expenses.
Cost and Risk Factors Buyers Should Evaluate Before Tool ReleaseCost or Risk ItemFamily Tooling ConsiderationMulti-Impression Tooling ConsiderationRecommended Buyer ActionTool constructionOne base may reduce initial tooling countMore cavities increase machining and matching workCompare total tooling investment over the product life cycleCycle timeSet by the slowest cooling or ejection requirementOptimized around one part geometryAsk for estimated cycle time and production capacityMaterial scrapCan rise if process balance is poorCold runners may create consistent runner scrapRequest resin-consumption assumptions and regrind policyDemand imbalanceOne slow-moving part can create excess inventoryProduction quantity can match the demand of one componentReview service-parts and regional demand forecastsMaintenanceRepairs can affect several different components at onceHigh cavity count requires preventive cavity maintenanceDefine spare inserts, maintenance intervals, and ownershipQuality containmentMultiple geometries need different inspection methodsCavity variation must be tracked and correctedRequire first-article samples and cavity identificationEngineering changesA change to one part may disrupt the full family setEvery identical cavity may need modificationUse insertable cavity design where revisions are likelyA practical break-even calculation compares tooling cost plus expected molding cost across projected demand. If a single-cavity tool produces a part at a higher unit cost but demand is uncertain, it may still be the cheaper business decision. If demand is reliable and high, a multi-impression mold often repays its added capital through lower machine time and more efficient labor use.
Start with the bill of materials rather than the mold category. Identify which parts are always consumed together, which parts may be sold separately, which require different colors or resins, and which have different forecast volumes. A family mold is only logical if production quantities stay closely matched. For example, a product requiring one front cover, one rear cover, and one battery door per unit may suit family tooling during launch. If the battery door is likely to be replaced often, customized across markets, or made in several colors, it may deserve a separate mold.
Request a DFM report before issuing a purchase order. A meaningful review should assess wall thickness, draft angle, rib-to-wall ratio, gate position, weld lines, sink risk, tolerance requirements, shrinkage, undercuts, ejection points, cooling access, texture, and resin flow. For technical materials such as glass-filled nylon, POM, PC/ABS, PPS, TPU, or flame-retardant grades, material behavior must be considered early because shrinkage and processing windows may make a mixed family tool impractical.
For low-volume global programs, buyers should also evaluate whether rapid tooling, CNC machining, vacuum casting, or additive manufacturing can reduce risk before production molding begins. Molding is not always the fastest answer for the first few units, especially when functional testing and customer feedback could still alter the geometry.
Family molds are common in products that launch as complete assemblies and require modest quantities of several plastic components. Multi-impression molds dominate programs where identical parts are consumed in large quantities, especially when automation and predictable replenishment are important. Both are used across global industrial supply chains, but their economic fit differs by application.
Industry Applications and Appropriate Tooling DirectionIndustryTypical ComponentsLikely Tooling ChoiceWhy It FitsConsumer electronicsCases, buttons, bezels, cable clips, battery coversFamily for pilot assemblies; multi-impression for repeat partsLaunch designs change quickly, while accessories may scale rapidlyAutomotiveClips, trim supports, vents, housings, sensor bracketsMulti-impression for high-run clips; family for low-run trim setsHigh repeatability and traceability are critical for common componentsMedical devicesInstrument housings, caps, trays, handles, fixturesDepends on validation plan and resin requirementsMaterial control, documentation, and dimensional consistency are essentialIndustrial equipmentControl enclosures, covers, knobs, protective guardsFamily tooling for balanced low-volume assembliesProduct variants and moderate annual demand are commonElectrical productsTerminal housings, switch components, cable-management partsMulti-impression toolingSmall identical parts often justify high-output productionSanitary and home productsHandles, caps, frames, fittings, dispenser partsFamily during development; dedicated cavities at scaleColor variants and replacement-part demand can change the economicsPackaging and retail goodsClosures, trays, dispensers, clips, protective insertsMulti-impression or stack moldsHigh volume rewards cavity count and automationMedical and automotive buyers should apply additional caution. A mold type does not itself establish regulatory compliance. Material traceability, validated process windows, dimensional control, documented inspection, packaging requirements, and customer-specific approval procedures remain necessary. The selected tool must support the required control plan rather than merely meet a price target.
A product team launching a handheld consumer device needs a front shell, rear shell, and button frame in equal quantities for an initial international release. The components use the same PC/ABS grade and have compatible molding temperatures. A family mold can be economical for a few thousand sets because every cycle produces a complete set for assembly. Before tool release, the team should verify that wall thickness, gate placement, cooling time, and shrinkage are compatible. If the button frame later becomes available in multiple colors, a separate insert or independent tool may be the better expansion path.
An automotive supplier requires the same nylon retainer clip for assembly plants in Europe, North America, and Asia. Demand is high and stable, with tens of thousands of pieces required each month. An eight-cavity or sixteen-cavity multi-impression mold is generally the better investment. Every cavity should be identified for inspection, and the supplier should monitor cavity-specific dimensions, gate vestige, flash, pull force, and material moisture control. This approach supports efficient export packing through ports such as Ningbo-Zhoushan, Rotterdam, and Long Beach.
An industrial equipment manufacturer needs a controller housing, cable cover, mounting foot, and protective cap. Initial sales volumes are moderate, but field replacement demand is unknown. A family mold could make complete launch kits economically, but the protective cap may wear or be lost more often than other components. The buyer may use a family tool for the main housing set and a dedicated multi-impression mold for the cap once replacement demand is confirmed. This hybrid approach reduces early capital exposure while preserving future supply flexibility.
Supplier selection should reflect the project’s tool life, resin, complexity, certification requirements, localization needs, production volume, and communication expectations. The following companies are established names with relevant manufacturing, tooling, prototyping, or injection molding capabilities. Buyers should confirm current regional availability, specific material qualifications, mold ownership terms, and project suitability directly during quotation.
Selected Global Suppliers for Injection Mold and Production ProgramsCompanyPrimary Service RegionsCore StrengthsKey OfferingsTEAM RapidGlobal customers, including North America, Europe, Asia, and other export marketsRapid tooling, DFM support, China-based cost efficiency, flexible productionInjection molding, rapid tooling, CNC machining, vacuum casting, assembly, packaging, direct shippingProtolabsNorth America and EuropeDigital manufacturing workflows and rapid production supportInjection molding, CNC machining, 3D printing, sheet metal fabricationXometryNorth America, Europe, and international sourcing networksBroad supplier network and online quotation capabilitiesInjection molding, machining, additive manufacturing, sheet metal servicesFictivUnited States and global manufacturing networkDigital manufacturing management and engineering-oriented sourcingInjection molding, CNC machining, urethane casting, 3D printingEVCO PlasticsUnited States and international customer programsCustom injection molding and large-scale manufacturing experienceTooling support, injection molding, assembly, packaging, engineering servicesRosti GroupEurope, Asia, and North AmericaMulti-site contract manufacturing and regulated-industry experienceInjection molding, product assembly, medical and consumer-product manufacturingICOMold by FathomNorth America and global customer baseOnline injection molding procurement and production supportCustom injection molding, tooling, prototype and production partsFor international sourcing, supplier qualification should include a review of DFM response time, sample process, first-article reporting, resin sourcing, cavity tracking, tool maintenance, export packaging, intellectual-property handling, project communication, and escalation procedures. A supplier’s willingness to challenge an unmanufacturable design is often more valuable than a fast quote that ignores foreseeable production risks.
TEAM Rapid supports global product developers, brand owners, distributors, dealers, end users, individual inventors, and industrial buyers through flexible OEM, ODM, wholesale, prototype, low-volume, and scalable production models rather than a one-size-fits-all mold program. Its ISO 9001:2015 quality management certification, DFM-based manufacturability reviews, in-house machining and tooling capability, molding resources, and tolerance capability down to 0.01 mm for applicable CNC work provide practical controls before a mold is built. The company works with diversified plastic and metal material options, offers tooling and molded-part production commonly within approximately 5 to 25 days depending on complexity, and has delivered more than 6,000 projects for over 500 customers in more than 25 countries. For global buyers, TEAM Rapid combines online quotation and engineering communication with direct project support, packaging, assembly, material management, procurement assistance, limited warehousing, and direct shipping; its established international customer experience supports coordinated pre-sale DFM feedback and after-sale project follow-up even where a local subsidiary or overseas warehouse is not stated. It provides customer-owned tooling and turnkey manufacturing pathways, including assembly and contract-packaging support, and does not operate BOO or on-site bulk-supply models. Buyers can review its rapid tooling services when comparing bridge tooling with production molds, then request a project-specific global manufacturing quotation for cavity layout, resin, quantity, finish, and lead-time analysis.
A clear RFQ improves the quality of family mold versus multi-impression mold recommendations. Provide 3D CAD files, 2D drawings where critical dimensions matter, annual volume forecasts, pilot quantity, resin specification, color, texture, cosmetic standards, expected product life, assembly requirements, target markets, packaging needs, and desired delivery point. If the product will enter regulated markets, include applicable customer requirements and validation expectations early.
Ask suppliers to state whether the quoted tool is aluminum, pre-hardened steel, or hardened steel; whether it uses cold or hot runners; whether it includes interchangeable inserts; what machine tonnage is anticipated; how many trial shots are included; and how mold maintenance will be managed. For a family tool, require a discussion of shot balance and projected inventory balance. For a multi-impression tool, require cavity-to-cavity process analysis and a defined plan for cavity identification.
In 2026, global mold programs will increasingly use simulation, connected process data, automated inspection, and modular tooling design. Mold-flow analysis is becoming more accessible earlier in product development, helping teams identify filling imbalance, weld lines, pressure peaks, cooling limitations, and potential warpage before expensive steel is cut. For family molds, this will make early feasibility decisions more evidence-based. For multi-impression molds, it will improve cavity balancing and cycle-time optimization.
Automation will also influence mold selection. High-volume multi-impression tools increasingly integrate robotics, in-mold sensors, vision systems, automated degating, cavity-specific quality tracking, and real-time process monitoring. These technologies can reduce labor dependency and make global production more traceable, but they require better tool design and a more disciplined validation plan.
Sustainability pressures are reshaping resin selection and mold design. Brand owners are evaluating recycled-content polymers, bio-based materials, lightweighting, lower-energy production, reusable packaging, and reduced runner waste. Hot-runner systems can reduce cold-runner scrap, although they add complexity and energy considerations. Family molds can reduce the number of mold bases required during early product development, but they should not be chosen if poor balance increases scrap. The most sustainable solution is usually the one that produces conforming parts efficiently, avoids excess inventory, and supports long tool life.
Policy and market conditions are also increasing the value of supply-chain resilience. Buyers are using dual sourcing, regional warehousing, clearer mold ownership contracts, origin documentation, and multi-region logistics planning. A tooling strategy should leave room for future expansion, whether that means adding cavities, transferring validated data, producing spare inserts, or qualifying a second production route.
No. A family mold can lower initial investment because it combines different parts in one base, but difficult flow balance, long cycle time, scrap, inventory imbalance, and future design changes can make it more expensive over time.
It becomes worthwhile when demand for one identical part is stable enough that lower unit cost and higher output recover the added cost of extra cavities, cooling, runner systems, and validation.
Standard family molding normally uses one material per shot. Parts needing different resins, significantly different processing temperatures, or different color requirements generally need separate tools, insert-molding steps, overmolding processes, or specialized solutions.
The biggest risk is process imbalance. Different cavity volumes, wall thicknesses, flow lengths, and cooling needs can cause uneven filling, inconsistent packing, warpage, sink, flash, or one component being overproduced relative to another.
Usually not if replacement demand differs from the main assembly demand. A separate multi-impression mold can prevent excess inventory of unrelated components and provide faster replenishment for the service part.
Provide 3D CAD, material, color, annual demand, target quantity, tolerances, finish requirements, expected tool life, target market, packaging needs, and any required inspection or regulatory documentation.
Yes. Rapid tooling is often a practical bridge for functional validation, pilot runs, low-volume sales, and early market feedback. It helps buyers confirm demand and design stability before investing in higher-cavity hardened production tooling.

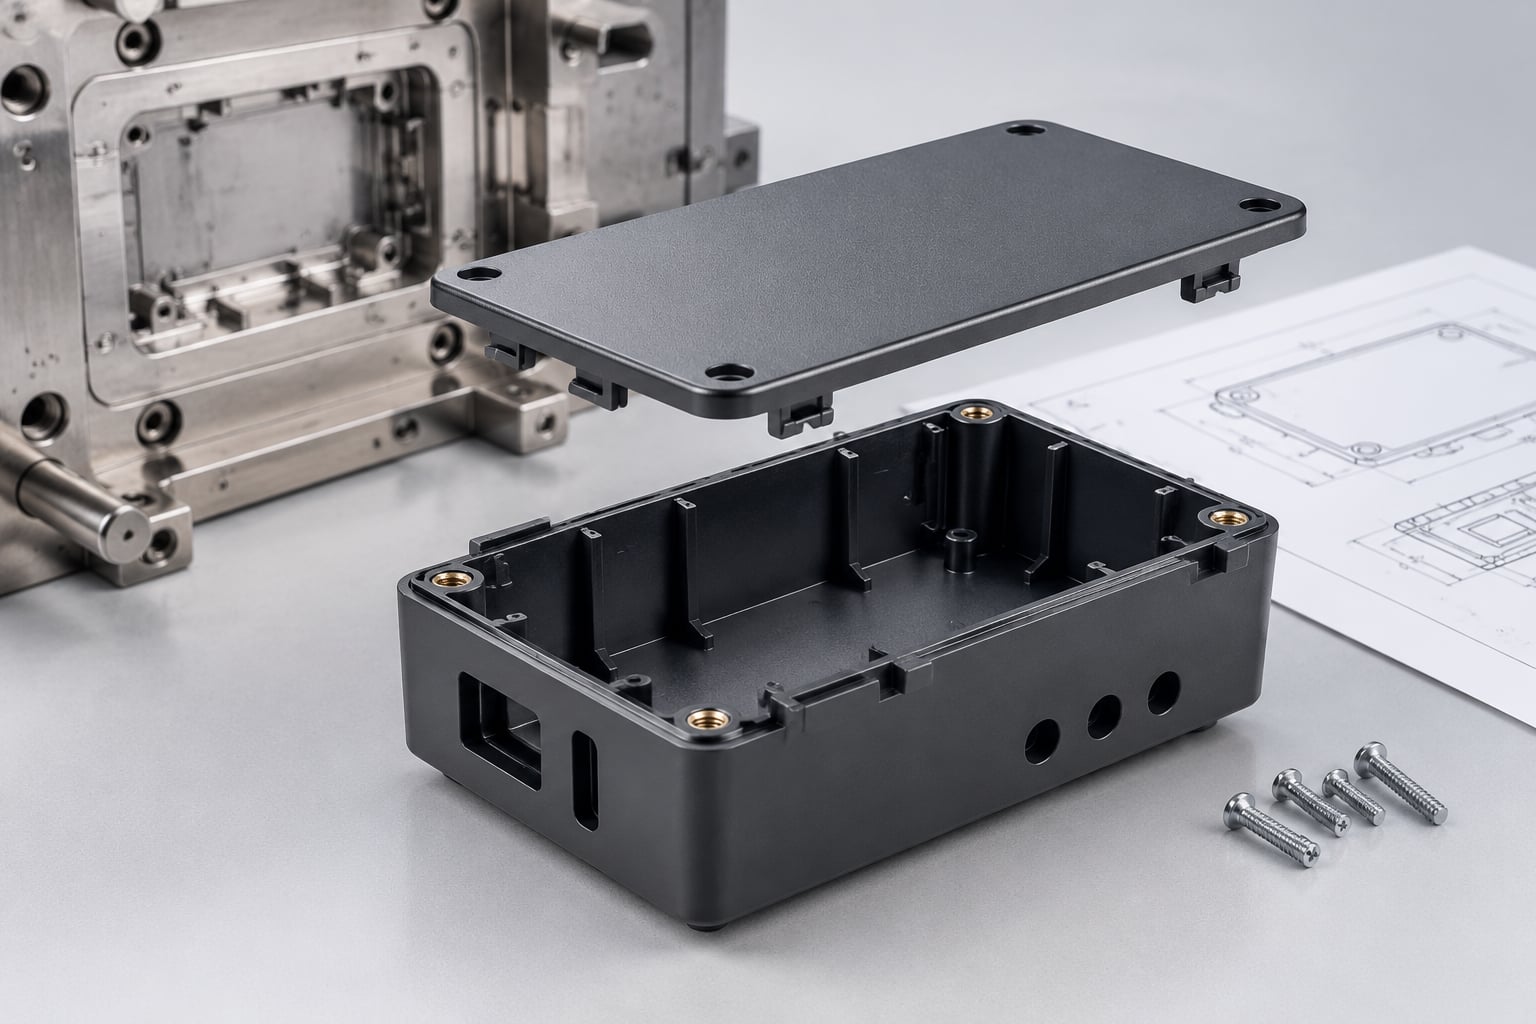
-
Global Market Injection-Molded Part Wall Gauge Guide
For most injection-molded plastic parts in the global market, start with a uniform wall gauge between 1.5 mm and 3.0 mm, then adjust it according to resin flow behavior, impact requirements, cosmetic expectations, mold design, and production volume. Commodity plastics such as polypropylene and polyethylene can often use thinner sections, while engineering materials such as polycarbonate, nylon, PBT, and ABS/PC blends usually need more carefully controlled wall thickness to prevent incomplete filling, sink marks, warpage, and internal stress.
The most important rule is consistency. Keep adjacent wall sections within approximately 10% to 15% of each other whenever possible. Instead of making one area excessively thick for stiffness, use ribs, gussets, structural webs, and rounded transitions. Thick plastic sections cool slowly, increase cycle time, consume more resin, and create a greater risk of sink marks or voids.
For a practical global sourcing strategy, compare established molders with strong DFM capability in China, North America, Europe, and Southeast Asia. Qualified international suppliers, including Chinese manufacturers with ISO certifications, engineering support, fast communication, and reliable pre-sales and after-sales processes, can offer strong cost-performance advantages for prototypes, bridge tooling, low-volume production, and scaled manufacturing.
Before releasing tooling, request a wall-thickness analysis, mold-flow review where appropriate, and a written DFM report that identifies thick zones, fill-risk areas, weld lines, gate locations, ribs, bosses, draft, and material-specific shrinkage behavior.
Wall thickness is one of the most influential design variables in plastic injection molding. It affects filling pressure, mold cost, cycle time, dimensional accuracy, resin consumption, cooling balance, cosmetic quality, and long-term mechanical performance. A part that looks simple in CAD can become difficult or expensive to mold if its wall gauge changes abruptly, contains large thick areas, or combines thin cosmetic surfaces with heavy structural features.
During the molding cycle, molten polymer enters the mold cavity through the gate and travels through runners or hot-runner channels. The melt begins cooling as soon as it contacts the steel cavity. Thin sections freeze sooner, while thicker sections remain molten longer. If a thin section is placed ahead of a thick section in the flow path, the melt may freeze before packing pressure can compensate for shrinkage. This can lead to short shots, weak weld lines, sink marks, voids, or inconsistent dimensions.
For buyers sourcing parts across Shenzhen, Dongguan, Ningbo, Suzhou, Chicago, Monterrey, Stuttgart, Birmingham, Singapore, and other manufacturing hubs, the core engineering principle remains the same: design for balanced flow and balanced cooling. The exact wall gauge may change by resin and application, but uniformity provides the strongest foundation for predictable production.
Wall gauge also has a direct commercial impact. Increasing a nominal wall from 2.0 mm to 3.0 mm does not simply increase resin usage by 50%. It may extend cooling time significantly, reduce the number of parts produced per hour, require a larger molding machine, increase tool temperature control demands, and affect freight cost. For high-volume programs, a small reduction in wall thickness can generate meaningful savings. For low-volume programs, stable molding and shorter lead time may be more valuable than minimizing every gram of resin.
The following values are practical starting ranges rather than universal specifications. Final wall thickness should be confirmed using the resin supplier’s technical data, part geometry, gate position, flow length, mold temperature, surface finish, reinforcement level, and end-use load requirements. Glass-filled resins, flame-retardant grades, recycled-content grades, and highly filled compounds may require different decisions from standard unfilled grades.
MaterialTypical Wall Gauge RangePreferred Design RangeMain Design ConsiderationCommon ApplicationsPolypropylene (PP)0.8 mm to 3.0 mm1.2 mm to 2.5 mmHigh shrinkage requires consistent sections and careful rib design.Containers, living hinges, automotive trim, caps, household productsHigh-Density Polyethylene (HDPE)0.8 mm to 3.5 mm1.5 mm to 3.0 mmGood chemical resistance but can warp with uneven cooling.Bottles, packaging, tanks, industrial covers, consumer goodsABS1.2 mm to 4.0 mm1.8 mm to 3.0 mmPopular for cosmetic housings; avoid thick zones that create sink.Electronics housings, appliance covers, automotive interiorsPolycarbonate (PC)1.0 mm to 4.0 mm1.5 mm to 3.0 mmHigh strength but higher viscosity; long flow paths need attention.Safety covers, transparent lenses, medical housings, electrical partsPC/ABS Blend1.2 mm to 4.0 mm1.8 mm to 3.2 mmBalances toughness and appearance; common for enclosure design.Consumer electronics, automotive bezels, industrial enclosuresNylon PA6/PA660.8 mm to 4.0 mm1.5 mm to 3.0 mmMoisture absorption and glass reinforcement affect shrinkage.Gears, clips, brackets, under-hood automotive componentsPBT0.8 mm to 3.0 mm1.5 mm to 2.5 mmUseful for electrical performance; reinforced grades need balanced flow.Connectors, switches, electrical housings, sensor componentsAcetal POM0.8 mm to 3.0 mm1.5 mm to 2.5 mmLow friction and high stiffness; control shrinkage and gate design.Gears, valves, latches, precision mechanical componentsThese ranges show why material selection and wall design must be evaluated together. For example, a 1.2 mm wall may be practical for a compact polypropylene clip but may be risky for a long-flow PC/ABS enclosure. Similarly, a nylon bracket can carry high loads with relatively moderate wall thickness when ribs and fiber orientation are properly considered. Simply making the bracket thicker may not improve performance if warpage increases or glass fibers align unfavorably.
Uniform walls are not always possible, especially in parts that include attachment points, snap fits, bosses, sealing features, reinforced corners, or ergonomic surfaces. The goal is not perfect uniformity at every point; it is gradual transition and controlled thermal mass. Designers should avoid isolated heavy sections surrounded by thin walls because the heavy section will cool more slowly and shrink more after ejection.
A common approach is to define a nominal wall thickness, often called “T,” and create supporting features in relation to that dimension. Ribs are typically designed at 40% to 60% of the nominal wall thickness. Boss walls are often kept around 60% of nominal wall thickness, with ribs added for support. Corner transitions should use radii instead of sharp edges, and thick-to-thin transitions should be tapered over a reasonable distance.
FeatureRecommended Relationship to Nominal WallPurposeRisk if OversizedUseful Design PracticeRib thickness40% to 60% of TAdd stiffness without making the main wall thicker.Sink marks and read-through on cosmetic surfaces.Use generous draft and rounded rib bases.Boss wall thickness50% to 70% of TSupport screws, inserts, and locating pins.Voids, sinks, and cracking near the base.Connect bosses to walls with gussets.Rib heightUp to 2.5 to 3.0 times TIncrease bending stiffness.Fill problems, weak rib tips, difficult ejection.Use multiple lower ribs instead of one very tall rib.Corner radiusMinimum 0.25 to 0.50 times TImprove flow and reduce stress concentration.Cracking and uneven filling at sharp internal corners.Maintain consistent inside and outside radius relationships.Wall transitionGradual taper over distanceBalance cooling and packing.Warping, sinks, and dimensional variation.Use tapered steps instead of abrupt section changes.Draft angleUsually 0.5° to 2° or moreEnable clean ejection and protect surfaces.Scuffing, sticking, ejector damage, cosmetic defects.Increase draft for textured surfaces.Ribs are especially important for housings, trays, covers, and structural plastic components. A rib can increase stiffness substantially because bending stiffness depends heavily on section depth. This means a well-designed ribbed wall can outperform a thick, flat wall while using less material and cooling more quickly. However, ribs must be positioned thoughtfully. Ribs directly behind high-gloss exterior surfaces can create visible sink marks, especially in ABS, PC/ABS, polypropylene, and unfilled nylon.
Design teams should also consider how a part will be measured. A thick-walled part may experience post-molding shrinkage after it leaves the tool, and a large flat panel can bend as residual stresses relax. If the part must mate with another component, define critical interfaces clearly and allow the molder to recommend process controls, fixture inspection, or secondary calibration methods.
The relationship between flow length and wall thickness is central to moldability. Longer melt flow paths require more pressure and are more vulnerable to premature freezing. Thin walls can be molded successfully when gates are positioned close to the critical areas, the material has adequate flow, mold temperatures are controlled, and the part geometry is designed for uniform filling. In contrast, a thin wall combined with a long flow path, multiple turns, texture, and glass-filled resin can create a difficult molding condition.
Gate location should support the thickest functional region or allow the melt to flow from thick to thin wherever possible. A gate positioned into a thin edge may cause hesitation as the melt reaches thicker features downstream. This can produce visible flow lines, weak weld lines, and poor packing. For large enclosures and trays, multiple gates or hot-runner systems may be needed to control pressure and cycle time, but gate marks, weld lines, and tooling cost should be evaluated early.
In projects requiring cosmetic surfaces, the gate must also be selected with appearance in mind. Hidden edges, internal walls, underside surfaces, and assembly interfaces are commonly preferred. Tunnel gates, edge gates, fan gates, valve gates, and direct sprue gates each have different effects on flow behavior and visible finishing requirements.
DefectTypical Wall-Related CauseVisual or Functional EffectPreferred Corrective ActionSecondary Process AdjustmentSink marksThick ribs, bosses, corners, or concentrated material mass.Depressed areas on visible surfaces.Core out thick areas and reduce rib thickness.Increase packing pressure or hold time where appropriate.WarpingUneven cooling, uneven wall gauge, fiber orientation.Twist, bowing, poor assembly fit.Balance wall sections and add structural ribs strategically.Adjust mold temperature and cooling channels.Short shotThin wall, long flow path, insufficient gate size.Incomplete part fill.Increase local gauge or improve gate location.Raise injection speed, pressure, or melt temperature carefully.VoidsHeavy sections shrink internally after the skin freezes.Internal bubbles and reduced structural integrity.Reduce material concentration and improve packing path.Optimize hold pressure and cooling time.Weld line weaknessFlow fronts meet after cooling in thin or distant areas.Visible seam or low-strength area.Move gate or increase local wall gauge slightly.Increase mold temperature to improve knit quality.Burn marksAir trapped near end-of-fill areas, often in thin sections.Dark or scorched appearance.Add venting and improve flow path design.Reduce injection speed near end fill if necessary.Design correction should normally come before process correction. It is possible to mask some defects by adjusting packing pressure, melt temperature, injection speed, cooling time, or mold temperature. However, process changes cannot fully compensate for poor geometry. A stable production tool should not rely on an extremely narrow molding window. If one minor temperature variation causes warpage or sinks, the part design needs further engineering attention.
For global programs involving multiple production sites, stable geometry is especially valuable. A design that only runs well on one specific machine with one experienced operator can be difficult to transfer. Balanced walls, reasonable tolerances, clear resin specifications, and documented molding parameters improve repeatability across qualified facilities.
Plastic enclosures commonly use ABS, PC/ABS, polycarbonate, or polypropylene. These parts need careful control of cosmetic surfaces, screw bosses, snap fits, vents, and internal ribs. A typical handheld enclosure may use a nominal wall between 1.5 mm and 2.5 mm, depending on resin and product size. Thin consumer electronics housings can be lighter and more attractive, but they may require higher-quality tooling, more precise gating, and more demanding process control.
Automotive components often require higher impact resistance, temperature resistance, chemical resistance, and dimensional stability. Interior trim parts may use polypropylene, TPO, ABS, PC/ABS, or reinforced compounds. Under-hood parts often use glass-filled nylon, PBT, PPS, or other engineering thermoplastics. Because vehicle components may experience vibration, thermal cycling, and loading, rib design and fiber orientation can be as important as nominal wall gauge.
Medical device housings need a combination of strength, cleanability, chemical resistance, appearance, and regulatory material traceability. Polycarbonate, ABS, PC/ABS, medical-grade polypropylene, and certain nylon or PBT grades are common choices. Wall thickness should support reliable assembly, sterilization requirements where applicable, and consistent molded dimensions.
Packaging products often use thinner walls to reduce resin usage and improve cycle time. Thin-wall packaging requires a high-flow resin, high-speed molding machine, optimized gate system, precise mold cooling, and experienced process control. A food container, cap, or lid may be much thinner than an industrial housing, but the engineering complexity can be greater because the process window is narrower.
Buyers should avoid requesting a mold quote based only on a 3D file. A reliable quotation requires the part material, annual quantity, target market, cosmetic expectations, tolerance requirements, color, texture, assembly method, packaging needs, and delivery location. If the product is still under development, request a DFM review before committing to hardened production tooling.
For early-stage programs, rapid tooling can be an effective bridge between prototype testing and mass production. It allows teams to validate part performance, assembly, appearance, and real material behavior before investing in multi-cavity hardened molds. Low-volume tooling is particularly useful for startups, industrial equipment makers, medical-device developers, automotive aftermarket brands, and consumer-product teams testing demand.
When comparing suppliers, evaluate total landed value rather than tool price alone. A lower mold quote can become expensive if the supplier does not provide DFM support, uses unsuitable steel, lacks inspection discipline, has inconsistent communication, or cannot manage engineering changes. Conversely, a slightly higher upfront engineering investment may reduce failures, scrap, delivery risk, and redesign cost.
Buyer Evaluation AreaQuestions to AskWhy It MattersPractical Evidence to RequestDFM capabilityWill the supplier review wall thickness, draft, ribs, bosses, and gating?Prevents avoidable tooling changes and defects.Written DFM report with annotated CAD images.Material controlCan the supplier source specified resin grades and provide traceability?Material variation affects shrinkage, strength, color, and compliance.Material certificates, resin brand, grade, and lot records.Tooling approachIs rapid tooling, P20 steel, H13 steel, or multi-cavity tooling appropriate?Tool life and cost must match forecast volume.Tool steel specification and cavity-life estimate.Inspection processHow are critical dimensions and appearance checked?Ensures parts meet drawing and assembly requirements.First article inspection report and control plan.Production capacityCan output scale from pilot runs to recurring production?Protects launch schedules and future demand.Machine tonnage range, lead-time plan, and capacity confirmation.Logistics supportCan the supplier package, label, consolidate, and ship globally?Reduces handoffs and export errors.Packaging proposal, Incoterms, and shipping options.For parts shipped through major trade lanes such as Shenzhen–Los Angeles, Ningbo–Rotterdam, Hong Kong–Frankfurt, Shanghai–Melbourne, and Guangzhou–Singapore, packaging design matters. Thin-wall parts can deform if cartons are overloaded, while cosmetic housings may need individual protection to avoid abrasion. A qualified supplier should be able to support custom packaging, kitting, labeling, inspection documentation, and direct shipping according to the buyer’s channel requirements.
The companies below represent a mix of international and regional manufacturing options. Selection should depend on part complexity, resin type, annual quantity, tooling budget, required certifications, project location, and desired communication model. Buyers should verify current capabilities, certifications, production availability, and country-specific compliance needs directly before placing an order.
CompanyService RegionsCore StrengthsKey OfferingsSuitable Project TypesTEAM RapidGlobal customers; China manufacturing network; experience across North America, Europe, and AsiaRapid tooling, DFM support, low-volume to volume production, integrated manufacturingInjection molding, insert molding, overmolding, CNC machining, 3D printing, vacuum casting, finishing, assemblyPrototype-to-production parts, housings, covers, trays, enclosures, functional componentsProtolabsNorth America and EuropeFast digital manufacturing workflows and short lead-time productionInjection molding, CNC machining, 3D printing, sheet metal fabricationRapid validation, low-volume molded parts, product developmentXometryNorth America, Europe, and international sourcing networksLarge supplier network and online manufacturing quotation toolsInjection molding, machining, sheet metal, casting, 3D printingCompanies needing flexible sourcing and multiple manufacturing processesEVCO PlasticsUnited States, Mexico, and selected global programsCustom molding, large parts, engineering support, production-scale operationsInjection molding, tooling support, large-part molding, assemblyIndustrial, medical, consumer, automotive, and large molded productsRosti GroupEurope, Asia, and North AmericaContract manufacturing, regulated-sector experience, product industrializationInjection molding, assembly, automation, packaging, supply-chain supportMedical, packaging, consumer, industrial, and technical plastic productsNypro, a Jabil CompanyGlobal manufacturing footprint including North America, Europe, and AsiaHigh-volume manufacturing, healthcare and consumer product expertisePrecision molding, tooling, automation, assembly, supply-chain integrationHigh-volume medical, consumer, healthcare, and electronics programsSuppliers in the United States and Europe may be preferred when local production, immediate engineering access, regional certification requirements, or short domestic logistics routes are critical. China-based suppliers can be highly competitive for rapid tooling, flexible volume runs, custom part complexity, and multi-process programs that require molding, machining, finishing, assembly, and export packaging under one coordinated supply chain.
TEAM Rapid supports global product developers, brand owners, distributors, OEM customers, startups, engineers, and individual inventors with injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, die casting, finishing, assembly, packaging, procurement support, and direct shipping. The company has more than 10 years of manufacturing experience, has served customers in more than 25 countries, completed over 6,000 projects, and supported more than 500 customers. Its ISO 9001:2015 quality management certification, in-house machining and tooling capability, detailed DFM reports, and inspection-focused manufacturing process help customers evaluate wall gauge, rib proportions, boss construction, material use, shrinkage risks, cavity layout, cycle time, and production feasibility before tooling begins. TEAM Rapid works through flexible OEM, ODM, wholesale, retail-support, regional distribution, prototype, low-volume, and recurring production models rather than limiting customers to one order format. It provides turnkey and customer-owned plant manufacturing solutions, not BOO or on-site bulk supply services. Its China-based integrated manufacturing operations and resource network support international customers with engineering communication, online quotation, project follow-up, sample approval, after-sales issue handling, packaging, and direct export shipping. While the company profile does not state overseas subsidiaries or local warehouses, its established export experience across markets including the USA, UK, France, Germany, and other regions provides practical support for customers seeking a long-term manufacturing partner rather than a simple remote order-taking supplier.
For a new project, customers can use TEAM Rapid’s injection molding services to review tooling, resin options, production methods, and molding requirements. When the CAD model is ready, request a project review through the custom manufacturing quotation page and provide the required material, annual quantity, critical tolerances, target delivery market, color, finish, and assembly requirements.
A handheld device housing may begin with a 2.0 mm PC/ABS nominal wall. The design includes screw bosses, snap fits, battery supports, connector openings, and cosmetic exterior surfaces. If the screw bosses are built at full 2.0 mm wall thickness, sinks may appear on the outer cosmetic face. The preferred solution is to core the bosses, reduce boss wall thickness to approximately 1.2 mm, connect them using thin gussets, and add draft for ejection. This approach improves appearance and shortens cooling time without sacrificing assembly strength.
An under-hood sensor bracket may use glass-filled PA66 because it needs thermal resistance, stiffness, and fatigue performance. A flat 4.0 mm section may appear strong, but it can create fiber orientation concerns and warpage. A better design may use a 2.5 mm nominal wall with ribs and gussets positioned along load paths. The final solution must account for fiber direction, mounting loads, humidity exposure, temperature cycling, and fastener torque.
A large industrial cover often requires impact resistance, mounting points, cable openings, and a professional surface finish. Using a 3.5 mm wall throughout may increase resin cost and cycle time significantly. A more balanced design can use 2.5 mm nominal walls with localized ribs, reinforced mounting areas, and smooth radii around openings. Gate location is especially important because long rectangular panels may warp if flow and cooling are not balanced.
A food or consumer packaging container may use polypropylene walls below 1.0 mm. Such products require high-speed injection, optimized gates, rapid cooling, precise mold venting, and high-flow resin. Unlike a thicker industrial housing, the challenge is not simply stiffness; it is achieving full fill at high production speed while maintaining stackability, rim strength, lid fit, and consistent appearance.
Injection-molded wall gauge optimization is relevant across automotive, medical devices, consumer products, industrial equipment, communications products, office equipment, electrical appliances, sanitary products, packaging, smart hardware, household goods, laboratory equipment, and energy-related products. Every industry applies the same basic thermal and flow principles, but each has different priorities.
Medical customers may focus on traceable materials, chemical compatibility, cleanability, reliability, and controlled assembly. Automotive customers may prioritize impact behavior, heat resistance, vibration durability, flame resistance, and dimensional stability. Consumer product brands may place greater emphasis on weight, surface quality, tactile feel, color matching, and cost. Industrial customers frequently need durable housings, cable management, mounting strength, and practical serviceability.
For global brands, it is also important to consider regional regulations and product certification pathways. Flame-retardant ratings, food-contact requirements, electrical safety standards, restricted substance requirements, recycling expectations, and customer-specific quality systems can influence material choice and ultimately affect the preferred wall gauge.
By 2026, wall thickness decisions are increasingly influenced by digital simulation, sustainability targets, material innovation, and supply-chain localization. Mold-flow simulation is becoming more accessible earlier in product development, allowing engineering teams to identify pressure drop, weld-line locations, cooling imbalance, and fiber orientation before steel is cut. This helps reduce expensive post-tooling modifications and supports faster product launches.
Lightweighting will remain a major trend. Brands are reducing plastic content through thinner walls, rib-optimized structures, topology-informed design, foamed materials, and stronger engineering resins. However, lightweighting must be balanced against product durability, recyclability, drop performance, and customer expectations. Overly thin designs can increase scrap, returns, and premature product failure, which undermines sustainability goals.
Recycled-content plastics will also affect molding strategy. Post-consumer recycled and post-industrial recycled materials can show greater variation in flow, color, shrinkage, and mechanical properties compared with virgin resin. Designers may need more conservative flow paths, better tolerance planning, or adjusted wall thickness when using recycled grades. Material validation and supplier consistency become especially important for functional products.
Policy trends in the global market are encouraging packaging reduction, material circularity, product repairability, and improved environmental reporting. Manufacturers will increasingly need to document resin selection, recycled content, product weight, packaging choices, and process efficiency. Well-designed wall gauge supports these goals by reducing unnecessary material while preserving real-world performance.
There is no single best value. A practical starting point for many parts is 1.5 mm to 3.0 mm. The correct choice depends on resin, part size, flow length, structural load, surface quality, gate location, and production method.
Uniform walls cool and shrink more evenly. This reduces sink marks, voids, warpage, stress, inconsistent dimensions, and cycle-time variation. Where different thicknesses are necessary, transitions should be gradual.
Ribs are commonly designed at 40% to 60% of the nominal wall thickness. Thicker ribs can create sink marks, especially behind cosmetic surfaces. Rounded rib bases and appropriate draft improve filling and ejection.
Yes. Thinner walls can reduce resin use and cooling time, lowering part cost in high-volume production. However, thin-wall designs may require more advanced tooling, high-flow material, faster molding equipment, and tighter process control.
Sink marks usually occur where plastic mass is concentrated, such as thick bosses, ribs, corners, and heavy wall sections. Core out thick areas, reduce rib thickness, improve packing access, and use balanced cooling.
In most cases, use ribs, gussets, or structural webs before increasing the full wall thickness. Ribs can improve stiffness efficiently while minimizing resin consumption, cooling time, and sink risk.
Yes. TEAM Rapid can provide DFM-oriented feedback for injection molding projects, including observations on wall thickness consistency, ribs, bosses, draft, undercuts, shrinkage risks, tooling feasibility, and production efficiency.
-
Global Market Plastic Mold Engineering Review Before Build
A complete plastic mold engineering review should be finished before steel is cut. The review must confirm part geometry, resin choice, wall thickness, draft, shrinkage, gate location, runner design, cooling, ejection, tolerances, mold steel, expected production volume, inspection plan, and shipment requirements. The objective is to prevent costly tooling changes, unstable cycle times, visible defects, weak weld lines, warpage, flash, sink marks, and assembly failures after the mold is built.
For the Global Market, the most practical approach is to involve the mold maker, part designer, material supplier, quality team, and production team during DFM approval. Buyers should compare local tooling specialists with qualified international suppliers, including Chinese manufacturers that provide relevant certification, responsive pre-sales engineering support, reliable after-sales support, and strong cost-performance for prototype, low-volume, and repeat-production tools.
Before issuing a purchase order, request a written DFM report, mold-flow recommendation where appropriate, steel specification, cavity count proposal, estimated cycle time, sample validation plan, spare-part list, ownership terms, and post-delivery service scope.
Injection mold design is not only a tooling task. It is a commercial, engineering, quality, and supply-chain decision that affects the total cost of every molded part. A low-cost mold can become expensive when it creates excessive scrap, long cycle times, unplanned maintenance, cosmetic defects, poor dimensional stability, or delayed product launch. Conversely, a properly engineered mold can support predictable output, stable quality, lower resin consumption, reduced labor, and faster market entry.
Global product teams commonly design in one country, source tooling in another, mold parts near an assembly plant, and distribute finished products across several regions. This makes pre-build communication particularly important. Different markets may have different requirements for product labeling, material traceability, medical-device documentation, flame ratings, food-contact requirements, electrical safety, recycling content, packaging, and shipment protection. The design review should therefore translate the product requirements into mold requirements before manufacturing begins.
Trade hubs such as Shenzhen, Dongguan, Ningbo, Shanghai, Singapore, Rotterdam, Hamburg, Los Angeles, Chicago, Monterrey, Birmingham, Munich, and Dubai connect international manufacturing programs. Yet shipping distance does not eliminate the need for engineering alignment. A mold shipped from China to Europe, North America, Southeast Asia, or the Middle East must match the selected molding machine, local resin supply, water connections, electrical requirements, hot-runner controls, and maintenance capability at the destination plant.
The most successful projects treat DFM as a decision gate rather than a formality. A written DFM review clarifies what will be changed, what will remain as designed, what risks are accepted, and how part quality will be measured. It also creates a reliable record for brand owners, distributors, OEM customers, contract manufacturers, and future engineering teams.
The following review areas should be addressed before tooling manufacture begins. Their relative priority depends on annual volume, part size, resin type, cosmetic expectations, regulatory requirements, and whether the part is a prototype, bridge-production item, or long-term production component.
Review AreaWhat to ConfirmCommon Risk if MissedRecommended ActionPart geometryUniform wall thickness, realistic radii, ribs, bosses, snap fits, undercuts, and assembly interfaces.Sink marks, warpage, short shots, stress cracking, or difficult ejection.Approve a DFM-marked CAD model before mold design starts.Draft angleDraft direction and degree based on resin, texture, part depth, and cosmetic surface class.Drag marks, scuffing, part sticking, or surface damage during ejection.Increase draft on textured, deep, and high-gloss surfaces.Material selectionApproved resin grade, shrinkage range, additives, recycled-content level, color system, and supplier availability.Dimensional variation, brittleness, inconsistent color, or unplanned material substitutions.Specify resin grade and acceptable alternatives in writing.Gate strategyGate type, gate location, vestige allowance, flow direction, weld-line position, and packing path.Visible gate marks, weak weld lines, uneven filling, or poor cosmetics.Use mold-flow analysis for large, thin-wall, or cosmetic-critical components.Cooling designCooling channel layout, baffles, bubblers, conformal cooling opportunities, and water-circuit identification.Long cycle time, warp, uneven shrinkage, and unstable dimensions.Review cooling separately from cavity and core geometry.Ejection systemEjector pin placement, sleeve ejectors, stripper plates, lifters, air ejection, and witness-mark tolerance.Pin push, deformation, cracking, or unreliable automatic running.Place ejectors on strong, non-cosmetic surfaces wherever possible.Mold steel and treatmentSteel grade, hardness, corrosion resistance, polishing level, texture, coating, and expected tool life.Premature wear, rust, poor surface finish, and excessive maintenance.Match steel selection to resin abrasiveness, volume, and finish requirements.Tolerance planCritical-to-function dimensions, datum structure, measurement method, shrinkage allowances, and inspection frequency.Assembly interference, inconsistent fit, disputes over acceptance criteria.Separate critical dimensions from general molded tolerances.This table should be used as a working review document, not merely a design checklist. For example, a nominal wall thickness may be acceptable in CAD but still create a sink risk if a boss is too thick, a rib is oversized, or the gate cannot pack the local area effectively. Similarly, a tight dimension may be theoretically achievable but unsuitable for long-term production if it is affected by resin moisture, post-mold shrinkage, cavity imbalance, or changing ambient conditions.
Part design determines most molding behavior. Tooling can solve many challenges, but it cannot fully compensate for a design that ignores resin flow, cooling, shrinkage, and ejection. The following rules should be evaluated together rather than independently.
Uniform wall thickness is one of the most important rules in injection molded part design. Large thickness transitions create uneven cooling and differential shrinkage. When one area freezes earlier than another, the part may warp or develop visible sink marks. Thick zones also increase cooling time, which directly increases the cost of every cycle.
When a thick region is required for structural performance, consider coring out the section, adding ribs, using gussets, changing the load path, or selecting a higher-performance material. The exact solution depends on resin behavior. Glass-filled nylon, polycarbonate, ABS, polypropylene, POM, TPE, PC/ABS, PEEK, and flame-retardant compounds each respond differently to thickness, flow length, moisture, and processing temperature.
Draft is the angle that allows the molded component to release from the core and cavity without dragging. Smooth surfaces may need modest draft, while textured surfaces require more because the texture mechanically grips the mold surface. Deep housings, bins, covers, trays, enclosures, and large appliance panels often need more draft than early concept models include.
Cosmetic expectations must be defined in practical terms. Identify Class A surfaces, visible surfaces, hidden surfaces, allowed ejector marks, gate vestiges, parting lines, flow lines, and acceptable color variation. If an external housing will be painted, plated, laser-marked, or overmolded, those secondary operations should be discussed during mold design because they may affect material selection and surface specification.
Ribs improve stiffness without making the entire wall excessively thick. As a general engineering principle, ribs should be thinner than the nominal wall to reduce sink risk, while their height and spacing should support mold filling and ejection. Bosses should be supported by ribs or gussets where possible, especially when they receive screws, inserts, or repeated assembly loads.
Snap fits require special attention because they combine molding behavior with repeated mechanical deflection. Review root radius, strain level, assembly direction, tool split, potential undercuts, and environmental exposure. Living hinges are typically associated with polypropylene and require a suitable resin grade, gate orientation, controlled thickness, and validation through repeated flex testing.
The best mold configuration depends on projected volume, part complexity, resin, quality target, lead time, budget, and the intended location of production. A prototype mold for 100 samples does not require the same architecture as a hardened production mold designed for several hundred thousand cycles. However, even a rapid tool needs sufficient cooling, venting, alignment, and ejection to produce useful validation parts.
Mold ConfigurationBest UseTypical StrengthKey Review RequirementSingle-cavity moldLarge parts, prototypes, low-volume production, and high-value components.Lower initial tooling cost and simpler process control.Confirm whether output rate meets launch demand.Multi-cavity moldMedium and high-volume identical components.Higher output per cycle and lower part cost at scale.Verify cavity balance, runner balance, and inspection strategy.Family moldRelated components assembled in matched sets at low volume.Can reduce initial tooling investment.Review differing fill rates, cycle times, and scrap implications.Two-plate moldStandard cold-runner applications.Simple, durable, and widely supported globally.Assess runner waste and gate location.Three-plate moldParts requiring automatic point gating away from the parting line.Allows flexible gate placement and automatic degating.Confirm added complexity is justified by part requirements.Hot-runner moldHigher-volume production, engineering plastics, and reduced runner waste.Improves material efficiency and can shorten cycle time.Specify hot-runner brand, controller compatibility, and maintenance access.Insert moldMetal threads, contacts, reinforcement pieces, and electrical components.Creates secure integrated assemblies.Define insert tolerances, loading method, and retention testing.Overmold toolSoft grips, seals, protective surfaces, and multi-material products.Improves ergonomics and reduces assembly operations.Verify material bonding, substrate condition, and gate sequencing.This configuration comparison helps buyers avoid selecting cavity count based only on a desired part price. More cavities may reduce unit cost, but they increase mold complexity, maintenance requirements, machine tonnage, hot-runner investment, validation effort, and risk exposure. If market demand is uncertain, a lower-cavity rapid production tool can provide a more flexible commercial path.
Mold steel should be selected according to production volume, resin type, surface finish, corrosion risk, required hardness, maintenance plan, and shipment environment. Pre-hardened steel may be appropriate for many medium-volume tools, while hardened tool steels are commonly used for demanding, abrasive, or high-volume applications. Stainless steels may be necessary for corrosive resins, humid processing conditions, medical requirements, or polished surfaces requiring corrosion resistance.
Buyers should ask the toolmaker to identify the mold base material, cavity and core steel, slider and lifter materials, guide components, springs, ejector components, wear plates, coatings, and hot-runner system. For globally deployed tools, standard components can simplify replacement and maintenance. The final documentation should state what spare components are supplied and which parts should be stocked at the molding site.
A mold should not be accepted merely because it produces a part. The trial must demonstrate that the part can be molded consistently at an agreed process window. This is especially important for medical housings, electrical enclosures, automotive parts, safety-related components, threaded assemblies, sealing interfaces, and components with strict cosmetic requirements.
Validation StageMain PurposeRequired EvidenceBuyer DecisionDesign for manufacturability reviewIdentify risks before steel cutting.Annotated CAD, change list, resin assumptions, and tooling proposal.Approve design changes and freeze the manufacturing model.Mold design reviewConfirm mold layout and function.2D/3D mold layout, gate plan, cooling plan, ejection concept, and steel list.Approve the tool architecture before manufacturing.First trialVerify initial filling, ejection, and major mold operation.Sample parts, process settings, photos, defect observations, and trial report.Authorize modifications and define next trial priorities.Dimensional inspectionConfirm critical dimensions and assembly interfaces.Inspection report, CMM data where required, gauges, and measurement conditions.Accept, adjust tolerances, or revise tool geometry.Functional assembly testVerify fit with mating components.Assembly samples, torque data, leak test, snap-fit results, or electrical checks.Approve function or request engineering correction.Cosmetic reviewAssess surface quality under defined conditions.Approved limit samples, lighting conditions, texture comparison, and defect criteria.Define acceptable appearance and rework limits.Production capability runShow stable output over an extended run.Cycle time record, reject rate, cavity comparison, process window, and maintenance notes.Approve production release or require corrective action.Final acceptance and shipmentTransfer an operating, documented tool.Mold test video, packing list, spare parts, maintenance guide, and ownership record.Release final payment and arrange shipment or production.The validation table should be adapted to the project risk level. A simple storage tray may only need visual inspection, fit verification, and a practical production run. A medical device enclosure may need tighter documentation, resin traceability, detailed inspection reports, controlled surface requirements, and functional testing after sterilization or chemical exposure. A mold intended for automotive supply may require cavity identification, process discipline, capability studies, and formal change control.
Buyers should begin with a clear request-for-quotation package. At minimum, provide a native CAD file or neutral 3D file, 2D drawings where critical dimensions exist, annual volume forecast, resin grade, color, surface requirements, assembly requirements, expected machine location, target delivery date, and expected mold life. If the mold will be transferred to another country, specify the machine platen size, tie-bar spacing, nozzle radius, locating ring, ejector connection, water fittings, voltage, and hot-runner controller requirements.
Do not compare quotations only by total mold price. Compare cavity number, steel choice, mold base, runner system, expected cycle time, included trials, sample quantity, inspection level, shipping method, spare parts, engineering change policy, warranty, and post-delivery support. A quote that omits these items may create avoidable cost later.
For uncertain demand, consider phased investment. An aluminum rapid tool or lower-cavity steel tool may validate the market before a larger multi-cavity production tool is commissioned. This approach is often useful for startups, industrial design firms, medical-device developers, consumer-product brands, and companies launching new products through distributors or online retail channels.
Shipping logistics also need early planning. Molds are heavy precision assets and should be protected against moisture, corrosion, and transport damage. Confirm export crating, rust prevention, mold locking, lifting points, customs documentation, and whether the tool will be shipped by air, sea, rail, or truck. For projects moving through ports such as Shenzhen, Ningbo, Shanghai, Rotterdam, Long Beach, or Jebel Ali, packaging and handling details can affect both cost and delivery reliability.
Injection molding supports a wide range of products because it combines repeatable geometry, material versatility, high output potential, and compatibility with inserts, overmolding, textures, and automated assembly. The mold design checklist should be customized to the end-use environment.
Applications may also combine multiple manufacturing processes. A plastic enclosure can require CNC-machined inserts, molded bosses, ultrasonic welding, painting, printing, screws, foam, labels, final assembly, kitting, and retail packaging. Selecting a manufacturing partner capable of coordinating these steps can reduce handoffs and shorten the launch schedule.
A global consumer-product brand developed a handheld device housing with a high-gloss front surface, internal snap fits, screw bosses, and a painted logo area. The initial CAD included insufficient draft near the sidewalls and thick bosses behind a visible surface. During the engineering review, the mold maker recommended increasing draft, coring the bosses, adjusting rib thickness, moving the gate to a less visible location, and defining acceptable parting-line placement. The resulting tool produced lower sink risk, cleaner ejection, and fewer cosmetic adjustments during pilot production.
An industrial equipment developer needed 500 enclosures for field testing before committing to a large production run. Instead of investing immediately in a high-cavity hardened mold, the team selected a rapid tooling route with a practical cavity layout, production-grade resin, and inspection of critical mounting features. The low-volume run allowed the customer to validate installation, cable routing, gasket compression, and user access. After field feedback, the final production mold incorporated design improvements without requiring major changes to a large initial tool.
An electrical product required metal threaded inserts and conductive contacts to be molded into a compact plastic carrier. The pre-build review focused on insert tolerance, loading orientation, resin temperature, contact protection, retention force, and automated versus manual insertion. The mold design included support features to prevent insert movement during injection and ejection. Functional testing confirmed thread integrity and electrical alignment before the tool was released for recurring production.
The supplier landscape includes machine builders, mold makers, contract molders, rapid tooling specialists, and full-service manufacturing partners. The companies below are real organizations with international relevance. Buyers should still evaluate each supplier against their specific resin, component size, regulatory, production-volume, and logistics requirements.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidChina, USA, UK, France, Germany, and customers in more than 25 countries.Rapid manufacturing integration, DFM support, rapid tooling, low-volume molding, and flexible production.Injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, finishing, assembly, packaging, and direct shipping.Husky TechnologiesGlobal operations serving packaging, medical, closure, and beverage producers.High-output injection molding systems and integrated production technology.Injection molding machines, hot runners, molds, controllers, and service for packaging applications.ENGELEurope, North America, Asia, and global industrial manufacturing markets.Injection molding equipment, automation, process technology, and digital production systems.Injection molding machines, robots, turnkey cells, process optimization, and automation solutions.ArburgGlobal network with strong European, North American, and Asian market presence.Precision molding technology and flexible production systems.Injection molding machines, automation, digital production support, and additive manufacturing systems.Rosti GroupEurope, Asia, and North America through international manufacturing operations.Contract manufacturing, injection molding, assembly, and supply-chain support.Plastic injection molding, medical and consumer manufacturing, assembly, and product industrialization.Nypro, a Jabil CompanyGlobal manufacturing locations serving healthcare and consumer markets.Complex healthcare manufacturing, engineering, and scalable production.Injection molding, precision components, medical manufacturing, automation, and assembly.FictivGlobal digital manufacturing network serving product development teams.Digital sourcing, prototyping, manufacturing coordination, and speed.Injection molding, CNC machining, 3D printing, urethane casting, and quality management support.This supplier comparison is intended to help buyers understand market positioning. Machine manufacturers such as ENGEL and Arburg are typically selected by companies operating molding facilities. Contract manufacturers such as Rosti Group and Nypro may support larger production programs with assembly requirements. Rapid manufacturing partners such as TEAM Rapid can be especially useful when a project needs fast design feedback, low-volume validation, tooling, machining, finishing, and flexible transition into production.
TEAM Rapid supports international product developers, engineers, startups, brand owners, distributors, OEM customers, and established manufacturers with rapid tooling, injection molding, insert molding, overmolding, CNC machining, 3D printing, vacuum casting, die casting, sheet metal fabrication, finishing, assembly, packaging, and direct shipping. Its ISO 9001:2015 quality management certification, more than 10 years of industry experience, more than 500 customers, more than 6,000 delivered projects, and service record across more than 25 countries provide practical evidence of its ability to manage prototype-to-production programs. The company does not promote a fixed captive list of branded mold components; instead, it specifies suitable mold bases, steels, resins, inserts, and production components according to the project requirements, while applying DFM analysis, inspection practices, machining tolerances down to 0.01 mm where applicable, and documented manufacturability reviews. TEAM Rapid supports OEM, ODM, wholesale, retail, regional distribution, and direct end-user projects with flexible order quantities from one prototype to more than 100,000 parts. Its delivery model includes turnkey and customer-owned tooling solutions, rather than BOO or on-site bulk supply services. While the company profile does not claim overseas subsidiaries or local warehouses, TEAM Rapid has established experience serving customers in the USA, UK, France, Germany, China, and other international markets through responsive online engineering communication, direct shipping, project coordination, packaging support, and after-sales follow-up. Customers can request a detailed rapid tooling service consultation for tooling strategy or submit part files through the global manufacturing quotation form for DFM feedback and pricing.
Injection mold design in 2026 will increasingly be shaped by faster development cycles, sustainability requirements, digital traceability, automation, and regional supply-chain resilience. Tooling teams will need to optimize not only part geometry but also energy use, resin selection, scrap reduction, data capture, and maintenance predictability.
Engineering teams are increasingly using AI-supported design analysis to identify draft problems, inconsistent wall thickness, possible undercuts, unsupported bosses, and likely warpage areas earlier in the design cycle. These tools do not replace experienced mold engineers, but they can speed up issue detection and help global teams review more design iterations before manufacturing begins.
Brands are under pressure to increase recycled content and reduce virgin plastic consumption. However, recycled resin can have wider property variation, altered flow behavior, contamination risk, color variability, and different shrinkage characteristics. Mold design reviews will need to address material consistency, gate size, venting, processing windows, and cosmetic acceptance criteria when recycled or bio-based polymers are specified.
Conformal cooling inserts manufactured through metal additive processes can follow complex cavity shapes more closely than traditional drilled channels. For suitable parts, this can improve cooling uniformity, reduce cycle time, and lower warpage. The technology is most valuable when the expected savings justify the added insert cost and when maintenance planning is considered.
Manufacturers increasingly track machine energy consumption, resin yield, runner waste, reject rate, and transport emissions. Hot-runner systems, optimized cooling, shorter cycles, reduced regrind dependence, and better cavity balance can contribute to lower resource use. Buyers should begin asking suppliers for practical process data rather than relying only on general sustainability claims.
Pressure sensors, cavity monitoring, cycle counters, cooling-flow monitoring, and digital maintenance records can improve production consistency. Predictive maintenance is especially useful for molds operating across multiple sites because it helps teams identify wear, blocked cooling channels, and process drift before a major production interruption occurs.
There is no single item that overrides all others, but wall thickness, draft, material selection, gate location, cooling, ejection, and tolerance requirements are usually the highest-impact areas. These factors strongly influence fill behavior, shrinkage, cycle time, part release, cosmetics, and long-term consistency.
DFM should be completed before steel is cut and ideally before the final product design is frozen. Early review allows changes to be made in CAD, where they are faster and less expensive than modifying a completed mold.
The required draft depends on resin, part depth, texture, surface finish, mold polish, and ejection direction. Smooth surfaces may need less draft than textured surfaces, while deep parts and highly textured exterior surfaces often need more. The mold maker should confirm draft recommendations during DFM.
A hot runner can reduce runner waste and support higher-volume production, but it adds initial cost, complexity, maintenance needs, and controller requirements. A cold runner may be more practical for low-volume parts, simpler tools, or projects where material changes are frequent. The right choice depends on annual volume, resin cost, part geometry, and production strategy.
A family mold can produce related parts in one cycle, but it should be used carefully. Parts with different sizes, wall thicknesses, fill behavior, or cooling requirements can create imbalance and higher scrap. Family molds are often most suitable for lower-volume matched sets rather than long-term high-output programs.
Request final mold drawings, steel and component information, trial reports, process settings, sample inspection data, spare-part list, maintenance instructions, mold photographs, shipping records, and clear ownership documentation. If the mold will be transferred internationally, also confirm water, electrical, controller, and machine-interface specifications.
Optimize wall thickness, reduce unnecessary material volume, use appropriate cavity count, improve cooling, minimize secondary operations, select the right resin, avoid overly tight non-functional tolerances, and approve DFM changes before tooling begins. Cost reduction is most effective when it improves manufacturability rather than simply lowering tool specifications.
-
Single vs Multi-Cavity Mold Selection for Global Markets
For most Global market injection molding projects, choose a single-cavity mold when the part is still changing, annual demand is low, quality validation is critical, or the component is large and complex. Choose a multi-cavity mold when the design is stable, demand is recurring, production capacity matters, and the savings from lower unit cost can justify higher tooling investment.
A single-impression tool is usually the lower-risk option for prototypes, pilot runs, medical validation parts, and low-volume commercial production. A multi-impression mold produces several identical parts per cycle, lowering labor, machine-time, and piece-price costs at scale. The best cavity count depends on annual volume, press availability, resin behavior, cycle time, part geometry, quality requirements, and the cost of potential downtime.
Buyers in the Global market should compare local molders in manufacturing hubs such as Shenzhen, Dongguan, Ningbo, Suzhou, Chicago, Detroit, Munich, Birmingham, Singapore, and Guadalajara, while also considering qualified international suppliers. Chinese manufacturers with ISO-certified quality systems, responsive engineering support, local-market experience, and strong pre-sales and after-sales communication can offer an especially attractive cost-performance balance for tooling and molded parts.
A mold cavity is the shaped void inside an injection mold that forms a plastic part. A single-cavity mold has one production impression and makes one part during each injection cycle. A multi-cavity mold contains two or more identical impressions, producing multiple matching parts in one cycle. For example, an eight-cavity mold delivers eight parts every time the machine closes, injects, cools, opens, and ejects.
The basic decision sounds simple, but the commercial implications are significant. Tooling cost, resin flow balance, machine size, cooling design, part consistency, maintenance requirements, production scheduling, and qualification effort all change as cavity count increases. In practice, a mold with more cavities is not automatically the lowest-cost answer. It must be engineered around stable molding conditions and enough forecasted demand to recover its higher purchase price.
For buyers serving more than one geography, cavity strategy also affects logistics. A low-volume launch may require a single cavity tool and localized fulfillment for trial customers in London, Frankfurt, Los Angeles, Dubai, or Sydney. Once demand becomes repeatable, a multi-cavity production mold can reduce per-part cost before consolidated sea freight leaves export hubs such as Shenzhen, Ningbo, Shanghai, Yantian, or Hong Kong.
Decision FactorSingle-Cavity MoldMulti-Cavity MoldPractical Buyer ImpactInitial tooling costLower because it has one impression and simpler runner designHigher due to repeated cavities, balancing, cooling, and machiningSingle cavity reduces upfront investment for new productsOutput per cycleOne part per cycleTwo to dozens of identical parts per cycleMulti-cavity supports higher output with fewer machine hoursDesign-change flexibilityHigh; one cavity is easier and less expensive to reviseLower; every identical cavity may require matching modificationsSingle cavity is safer during ongoing design developmentPart-to-part consistencyEasy to control because only one part is produced each cycleDepends heavily on balanced filling, cooling, venting, and ejectionMulti-cavity needs stronger mold validation and process controlMaintenance complexityLower; fewer inserts, ejectors, gates, and cooling pathsHigher; more wear points and more opportunities for imbalanceSpare inserts and preventative maintenance become more importantBest production rangePrototypes, bridge tooling, low-volume and controlled launchesStable medium-volume to high-volume recurring productionAnnual demand and forecast reliability should guide the choiceDowntime riskOne cavity failure stops all output, but repair is simplerA single damaged cavity can affect a large share of each shotMulti-cavity tools need planned maintenance and backup capacityThe table shows why cavity count is a business decision as well as an engineering decision. A one-cavity mold can be the most economical tool for a 5,000-part annual requirement, while a 16-cavity mold may be justified for a part with a stable forecast of several hundred thousand units per year. The break-even point is unique to every project.
Single-cavity injection molds are commonly selected for large housings, covers, automotive trim pieces, industrial enclosures, medical-device casings, transparent components, thick-wall parts, and products with demanding cosmetic surfaces. These components can require substantial cooling time, high clamp force, intricate slides, precision inserts, or careful gate positioning. Adding multiple large cavities could require a much larger injection molding press and significantly increase tool construction cost.
A one-cavity tool is also the preferred option when engineers are still refining wall thickness, snap fits, ribs, sealing interfaces, textures, color, assembly tolerances, or material selection. Modifying one cavity is faster and less costly than changing four, eight, or sixteen matched cavities. This makes single-cavity rapid tooling especially useful between prototype testing and commercial launch.
Projects with uncertain demand should also begin conservatively. A brand owner testing a new consumer product across marketplaces in the United States, Europe, Southeast Asia, and the Middle East may not have enough sales data to justify a high-cavity hardened steel tool. Starting with a single cavity or low-cavity tool protects cash flow while preserving a path to scale.
Multi-cavity molds are designed for products with stable geometry, repeatable demand, manageable dimensions, and a well-characterized molding process. Typical examples include caps, clips, connectors, small trays, fittings, dispensers, medical consumables, packaging components, electrical accessories, buttons, and small consumer-product parts. When a part is compact and its cooling time is short, adding cavities can generate substantial productivity gains.
The largest advantage is lower cost per part. A molding press has fixed activities during each cycle: closing the clamp, injecting polymer, cooling, opening, ejecting, handling parts, and running quality checks. Producing eight parts instead of one during substantially the same cycle spreads machine and labor costs across more units. The actual cycle time may rise slightly because of filling, cooling, or automated handling needs, but the output gain can still be decisive.
However, a multi-cavity tool should not be commissioned solely because the purchase price per part appears lower in a quotation. The tool must be matched to the molding machine’s shot capacity, plasticizing rate, clamp tonnage, tie-bar spacing, hot-runner system, mold weight limit, and automation equipment. A technically unsuitable high-cavity mold can create scrap, frequent stoppages, inconsistent dimensions, and expensive maintenance.
A practical cavity-count estimate begins with annual demand and available production time. Divide the annual required quantity by the number of planned operating hours, then account for expected cycle time, machine efficiency, scrap allowance, maintenance, and seasonal demand peaks. The result identifies the hourly output needed. From there, manufacturers can test feasible cavity options against machine constraints and tooling cost.
For instance, a component requiring 240,000 acceptable parts per year may run at a 30-second cycle. At 80% production efficiency, a single-cavity mold can theoretically produce roughly 96 parts per hour, while an eight-cavity mold can produce roughly 768 parts per hour. The appropriate option depends on planned shifts, machine availability, inventory strategy, cash tied up in stock, and the ability to sell the forecasted volume.
Project ConditionRecommended Starting PointWhy It WorksImportant CheckPrototype or engineering validationSingle cavityFast tool build, lower investment, easy design revisionsConfirm the tool steel and construction match expected trial quantitiesLow-volume launch below 10,000 partsSingle cavity or two cavitiesLimits tooling risk while supporting early market entryReview whether launch demand is seasonal or recurringLarge or deep cosmetic housingSingle cavityImproves filling, cooling, texture control, and inspectionValidate clamp force and warpage before adding cavitiesStable consumer accessoryFour to eight cavitiesReduces unit cost for repeated ordersUse balanced runners and cavity-to-cavity samplingSmall commodity componentEight to thirty-two cavitiesHigh output can justify advanced tooling and automationConfirm material drying, cycle repeatability, and sorting capacityRegulated medical componentOne to eight cavities after validationSupports controlled output and documented process qualificationEstablish cavity traceability and validation protocolsHigh-volume packaging closureSixteen or more cavitiesMaximizes productivity for standardized geometryEvaluate hot-runner maintenance and high-speed automationThese ranges are not fixed rules. A two-cavity tool may outperform a four-cavity tool if the part is difficult to cool, a high-temperature resin needs long residence-time control, or the plant has limited press availability. A capable molder should provide a DFM report, mold-flow recommendation where appropriate, estimated cycle time, machine-tonnage requirement, and break-even analysis before finalizing the cavity count.
Runner selection can materially change the economics of single and multi-cavity molding. A cold runner is generally less expensive to build and maintain, making it suitable for lower-volume tooling, compatible regrind programs, and simpler resins. However, it creates runner scrap or regrind and can add cycle time. For a multi-cavity mold using costly engineering resin, runner waste can become a meaningful cost item.
A hot runner directs molten plastic to each cavity through heated manifolds and nozzles. It reduces or eliminates runner waste, can support faster cycles, and is often valuable for higher-cavity tools. Its disadvantages are greater upfront cost, more complex temperature control, sensitivity to certain color or material changes, and specialized maintenance. The best runner system depends on resin price, annual volume, cavity count, gate appearance, color-change frequency, and quality targets.
For multi-impression molds, flow balance is essential. Each cavity should fill at a comparable rate and pressure. Unbalanced flow can cause short shots, flash, dimensional variation, sink marks, color differences, inconsistent packing, or variable part weight. Even when cavities look identical, the manifold layout, gate geometry, cooling channels, venting, and cavity location can influence results.
Resin behavior is central to cavity-count selection. Polypropylene, polyethylene, ABS, polycarbonate, nylon, POM, TPU, TPE, glass-filled polymers, flame-retardant grades, and recycled-content materials all have different flow, shrinkage, moisture, abrasion, temperature, and processing characteristics. A material that fills easily through a balanced hot runner may suit a high-cavity mold, while a glass-filled nylon with demanding dimensional requirements may require a more conservative cavity count and hardened wear-resistant components.
Part geometry matters equally. Thin-wall parts can demand high injection speed and pressure. Deep ribs can create packing challenges. Long flow lengths may require larger gates or higher melt temperatures. Undercuts create slides or lifters, increasing mold complexity and maintenance burden. Tight tolerance features such as sealing diameters, clips, threads, gear teeth, lens surfaces, and insert-molded interfaces require specific cavity-by-cavity measurement plans.
For quality-critical production, buyers should ask for first article inspection reports, material certificates, cavity identification, process parameter records, visual standards, measurement methods, and corrective-action procedures. A multi-cavity mold should be evaluated not only on the average dimension of all parts but also on variation between individual cavities.
IndustryTypical Mold StrategyExample PartsReason for SelectionAutomotiveSingle cavity for large trim; multi-cavity for small clipsInterior bezels, vents, fasteners, cable retainersLarge visible components need control; small repeat items need throughputMedical devicesSingle to moderate multi-cavityInstrument housings, sample holders, disposable fittingsTraceability, qualification, and cavity consistency are criticalConsumer electronicsTwo to eight cavities depending on sizeCases, buttons, connectors, charger componentsFast product cycles favor flexible tooling before scalingPackagingHigh-cavity production moldsCaps, closures, jars, tamper-evident componentsHigh annual volume rewards automation and short cycle timesIndustrial equipmentSingle cavity or family toolingEnclosures, guards, covers, cable-management partsProduction volumes are often lower and parts can be complexHome appliancesMixed strategyKnobs, housings, latches, reservoirs, internal fittingsVisible large parts and small repeat components need different toolsElectrical productsMulti-cavity for standardized componentsSwitch bodies, terminal covers, plugs, clipsRepeatable geometry can support scalable production economicsThe same industry may use several strategies simultaneously. A coffee machine manufacturer, for example, may use one cavity for a large textured exterior housing, four cavities for a water-tank latch, eight cavities for buttons, and a dedicated insert-molding tool for electrical interfaces. The correct cavity count must be selected by component, not by product category alone.
Global buyers can source injection molds and molded parts from regional manufacturers close to final assembly, from specialized tooling centers, or from integrated international suppliers. The strongest choice depends on lead time, engineering complexity, intellectual-property controls, expected order frequency, target landed cost, required certifications, and post-launch support.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidGlobal customers, including North America, Europe, Asia, and other export marketsRapid tooling, DFM support, China-based cost efficiency, flexible low-volume to production capabilityInjection molding, rapid tooling, CNC machining, vacuum casting, finishing, assembly, packaging, direct shippingHusky TechnologiesGlobal, with strong presence in North America, Europe, and AsiaHigh-output packaging systems and integrated molding solutionsPreform, closure, hot-runner, mold, and production-system technologiesENGELGlobal, including Europe, the Americas, and Asia-PacificInjection molding machines, automation, and process expertiseMachine systems, automation cells, process technologies, digital production supportARBURGGlobal, with broad European and international service coveragePrecision injection molding equipment and automated manufacturing systemsInjection molding machines, turnkey production cells, digital manufacturing solutionsFANUCGlobal, serving major industrial markets worldwideRobotics, automation, CNC systems, and molding machinesRobots, ROBOSHOT injection molding machines, automated handling solutionsNypro, a Jabil CompanyGlobal manufacturing network across North America, Europe, and AsiaComplex healthcare and consumer-product manufacturing programsPrecision molding, assembly, automation, product industrialization, supply-chain supportEVCO PlasticsUnited States, Mexico, China, and international customer programsCustom plastic injection molding and engineering supportTooling management, molding, assembly, decoration, and packagingThese companies operate in different parts of the value chain. Some are equipment manufacturers, some are high-volume systems specialists, and some are custom molders or integrated manufacturing partners. Buyers should confirm whether a supplier will build the mold, own the mold, store it, run production, provide spare inserts, export parts, and support engineering changes after launch.
TEAM Rapid helps customers select practical cavity counts by connecting DFM analysis, tooling manufacture, injection molding, machining, finishing, assembly, packaging, and direct shipment in one production pathway. With more than 10 years of manufacturing experience, more than 6,000 delivered projects, over 500 customers, and service experience across more than 25 countries, the company can support a single prototype through recurring production runs of 100,000-plus parts. Its ISO 9001:2015 quality management certification, tolerance capability down to 0.01 mm for relevant CNC work, material options for plastic and metal parts, inspection focus, and engineering review help customers evaluate gate locations, wall thickness, cycle time, resin use, cooling, and mold-cavity feasibility before tool construction.
For global brand owners, distributors, product developers, dealers, end users, startups, and individual inventors, TEAM Rapid offers flexible OEM and ODM-oriented manufacturing support, prototype orders, low-volume production, recurring supply, assembly, packaging, and direct-shipping arrangements. The company’s integrated manufacturing resources across China allow coordinated handling of machining, mold making, molding, die casting, sheet metal fabrication, and finishing rather than forcing buyers to manage disconnected suppliers. TEAM Rapid has established export experience serving customers in markets including the USA, UK, France, Germany, and other international regions, with one-to-one engineering communication and responses typically available within hours. It does not claim overseas subsidiaries or local warehouses where these are not established; instead, its market commitment is demonstrated through repeat global delivery, documented engineering support, online pre-sale consultation, post-production communication, packaging coordination, and direct logistics support from China-based operations.
TEAM Rapid provides manufacturing and supply-chain support rather than BOO or on-site bulk-supply services. It can support turnkey manufacturing coordination for customer-owned products and components, but it is not an EPC plant-construction provider. For buyers needing to test a part before approving higher-output tooling, the company can begin with rapid prototypes or bridge tooling, then scale to multi-cavity production after the design and market demand are validated. Learn more about its rapid tooling services when planning a production transition.
Before requesting quotations, provide a complete 3D model, 2D drawing where critical dimensions apply, annual forecast, target resin, color and finish requirements, expected product life, assembly information, packaging needs, target markets, and quality documentation requirements. If the design has not been molded before, request DFM feedback before committing to a cavity count.
Ask suppliers to quote at least two alternatives when volume is uncertain. A common comparison is one cavity versus four cavities, or two cavities versus eight cavities. The quotation should separate tool cost, cycle time, part price, resin waste, sampling cost, mold maintenance, estimated mold life, lead time, shipping, and potential engineering-change cost. This makes the financial trade-off visible.
For international sourcing, clarify mold ownership in writing. State whether the customer owns the tooling, whether tool files and maintenance records will be available, how long the tool will be stored, who pays for repair, and what happens if production is transferred. Also specify inspection standards, approved master samples, cavity markings, acceptable defect levels, packaging configuration, and shipping Incoterms.
Use a staged approach when possible. Start with a single cavity or low-cavity rapid tool for functional testing and initial sales. Collect field feedback, validate assembly, confirm resin performance, and establish demand. Then invest in a multi-cavity production mold only when the design is frozen and the cost recovery period is commercially sound. To discuss a custom comparison, request a manufacturing quotation with expected annual volume and part files.
A startup introducing a handheld smart-device housing may initially need 2,000 to 8,000 units for certification, pilot sales, and distributor demonstrations. A single-cavity aluminum rapid tool can help validate texture, button alignment, ultrasonic welding, and drop-test performance without locking the company into a high tooling spend. After demand stabilizes, a two- or four-cavity steel production mold can reduce unit cost for recurring orders.
An automotive supplier producing a small nylon cable retainer may need several hundred thousand pieces annually. The part is compact, repeatable, and suitable for automated handling. An eight- or sixteen-cavity mold can be commercially attractive, provided that glass-filled material wear, shrinkage, cavity balance, and dimensional control are validated. Hardened steel inserts and planned preventative maintenance are often important.
A medical-device company may require a large ABS-PC enclosure with cosmetic requirements, tight assembly interfaces, and regulatory documentation. A single-cavity tool is often preferable because the part may require side actions, carefully controlled cooling, and stable visual quality. Even at moderate volume, the risk and cost of duplicating a complex cavity can outweigh the benefit of higher output.
A standardized closure used by a beverage or personal-care brand can justify a high-cavity hot-runner mold when annual demand is proven. The decision should include resin consumption, cycle time, automation, mold service intervals, color-change requirements, and warehouse inventory. High-cavity tooling is particularly effective where geometry is mature and the supply program is continuous.
In 2026, cavity-count decisions will increasingly be supported by digital manufacturing data. Mold-flow simulation, in-mold pressure sensing, cavity-level monitoring, machine learning-based process alarms, and digital maintenance records are helping molders identify imbalance before it turns into widespread scrap. Buyers will increasingly expect cavity-specific traceability for higher-risk medical, automotive, electrical, and industrial components.
Sustainability will also affect tool design. Recycled-content resins and bio-based polymers can have wider processing variation than virgin materials, making balanced runners, improved venting, optimized gate design, and robust process windows more important. High-cavity tools with hot runners can reduce runner waste, but their energy use and maintenance profile must be evaluated honestly. Material-efficient part design, lower scrap rates, shorter cycle times, and durable molds are likely to remain major purchasing priorities.
Global trade policies, shipping volatility, regionalization, and carbon-reporting expectations may encourage more distributed supply strategies. Some brands will retain tooling in China for cost-efficient production while using regional assembly, safety-stock warehouses, or secondary molding capacity closer to the customer. Others will use lower-cavity tools for regional product variants and high-cavity tools for globally standardized components. The most resilient approach is usually a documented, transferable tooling strategy rather than dependency on an undocumented process.
No. It usually lowers the molding cost per part only when demand is high enough to recover the higher tooling, validation, maintenance, and machine-capacity costs. For low volume, a single-cavity mold can produce the lower total project cost.
New products commonly begin with one or two cavities when demand or design stability is uncertain. Once sales forecasts, assembly performance, and quality results are proven, production can move to four, eight, or more cavities as justified.
Yes, but the repair must restore the cavity to the same dimensions, surface condition, cooling performance, and filling behavior as the other cavities. Otherwise, the repaired cavity may produce parts with different weight, appearance, or dimensions.
A multi-cavity mold produces multiple identical parts in one cycle. A family mold produces different parts in one cycle, such as a left and right housing. Family molds can simplify low-volume assembly sets but are harder to balance and control than identical-cavity tools.
No. Hot runners are often valuable for high-volume tools because they reduce runner waste and can improve productivity, but they add cost and complexity. Cold runners may be more practical for lower volumes, frequent color changes, or certain resin and tooling budgets.
Provide the 3D part model, resin specification, color, annual quantity, expected product life, dimensional tolerances, cosmetic requirements, target cycle time if known, packaging requirements, and whether the tool will support pilot, low-volume, or long-term production.
-
Heated vs Cold Runner Mold Choices for the Global Market
For most low-volume, bridge-production, and frequently changing plastic parts, a cold runner mold is the lower-risk and lower-investment choice. For stable, high-volume programs using expensive resin or parts where runner scrap is unacceptable, a heated runner mold can reduce material waste, automation effort, and long-term unit cost. The best choice is not determined by mold price alone: annual volume, resin price, part geometry, cavity count, color-change frequency, quality targets, and maintenance capability all matter.
In the Global market, buyers should request both mold concepts during DFM review and compare the total cost over the expected production life. Well-known global suppliers include Husky Technologies, Mold-Masters, Synventive, Yudo, HRSflow, and INCOE. Qualified international suppliers, including Chinese manufacturers with ISO-based quality controls, engineering support, and responsive pre-sales and after-sales service, can also be highly competitive because they combine tooling capability with strong cost-performance.
A runner is the channel system that carries molten plastic from the injection molding machine nozzle to each mold cavity. In a cold runner tool, the runner solidifies with every shot. It is ejected together with the finished parts and then recycled, reground, separated, or discarded. In a heated runner tool, electrically controlled manifolds and nozzles keep the resin molten until it enters each cavity, so the runner is not ejected as a solid plastic component.
Cold runner injection molds are mechanically simpler. They usually use a sprue, runner channels, gates, and a runner plate or conventional two-plate layout. Their lower initial cost makes them common in prototype tooling, low-volume production, and applications using easy-to-process commodity materials. However, the molded runner can represent a meaningful percentage of each shot weight, especially on small parts or molds with long flow paths.
Heated runner systems, often called hot runner systems, use temperature-controlled components inside the mold. The system may be open-gated, valve-gated, externally heated, internally heated, or arranged with thermal gates. These molds require more precise manufacturing, wiring, control systems, thermal balancing, and preventive maintenance. In return, they can lower resin loss, improve material handling, support automated molding, and reduce post-molding trimming.
For buyers in the Global market, the decision should be evaluated as a complete manufacturing system. A low-cost cold runner tool may cost more over time if the material is expensive, the runner cannot be reused, or manual runner separation slows packing and inspection. Conversely, an expensive heated runner system may never recover its premium if annual demand is only a few thousand parts or if frequent material and color changes require repeated purging.
The initial purchase price is the most visible difference between the two mold styles. Cold runner molds usually require fewer specialized components and less electrical integration. Heated runner molds add manifolds, nozzles, heaters, thermocouples, temperature controllers, precision pocketing, insulation design, and more demanding assembly work. The final premium varies greatly by cavity count, resin, gate type, machine interface, and supplier brand.
However, tooling cost is only one part of total landed production cost. Material consumption, labor, automation, cycle time, scrap rate, maintenance, downtime, logistics, and part traceability can have a larger effect during a long production program. A clear quote should distinguish mold construction cost from system cost, spare parts, controller cost, sampling, validation, shipping, taxes, and future maintenance.
Cost factorCold runner moldHeated runner moldCommercial impactInitial tooling investmentLower because the runner system is machined directly into mold plates.Higher because it includes manifolds, nozzles, heaters, sensors, and controls.Cold runner is generally preferred for limited budgets and uncertain volumes.Resin consumptionIncludes runner weight in every molding cycle.Delivers resin directly to the cavities with little or no solid runner waste.Heated runner becomes attractive when resin is costly or cannot be reground.Cycle timeMay be longer because the runner must cool and eject.Can be shorter because only the molded part must solidify sufficiently.Faster cycles can increase machine output on mature high-volume programs.Labor and automationMay require runner removal, separation, grinding, or sorting.Produces parts without a solid runner, simplifying automated handling.Heated runner can lower downstream handling and packing complexity.Maintenance costGenerally simple; gates and runner surfaces are easier to inspect.Requires electrical, thermal, and mechanical troubleshooting expertise.Cold runner has lower service complexity; heated runner needs preventive planning.Changeover costUsually easier for color and resin changes.Purging can consume material and time, especially in complex manifolds.Cold runner is often better for short runs and many color variants.Production scrap riskRunner scrap is predictable, but reground-material control is required.Startup scrap can occur if temperature zones are improperly balanced.Both require process control; the failure modes are different.The table shows why a purchase order should not simply ask, “Which mold is cheaper?” A better question is, “Which mold produces the required number of conforming parts at the lowest total program cost?” For example, a six-cavity cold runner mold producing a 30-gram part with a 20-gram runner can consume substantial additional resin. If the runner cannot be reused because of cosmetic, regulatory, fiber-filled, flame-retardant, or color-control requirements, the material loss may justify a heated runner system sooner than expected.
A practical break-even analysis compares the additional heated runner investment with annual savings. Start with the difference between the two tooling quotations. Then calculate the value of runner material saved per shot, subtract any added electricity and maintenance allowance, and add expected savings from lower labor, reduced separation, fewer rejects, or shorter cycle time. Divide the additional tooling investment by the savings per shot or savings per year.
For a simple estimate, calculate runner weight multiplied by resin cost and the proportion of runner that cannot be reused. Add labor for degating or sorting, plus the cost of disposal where applicable. For high-performance materials such as PEEK, PPS, PEI, reinforced nylon, medical-grade polycarbonate, transparent acrylic, or specialty TPE, runner waste can be especially expensive. For low-cost polypropylene or polyethylene parts with small runners and easy regrind use, the payback period can be much longer.
Program conditionMore suitable runner approachWhy it is usually selectedKey buyer checkPrototype validation under 5,000 partsCold runnerLower mold investment and simpler design revisions.Confirm whether a soft tool, aluminum tool, or steel insert is sufficient.Low-volume replacement partsCold runnerProduction may be intermittent, making heated-system maintenance harder to justify.Check long-term mold storage and corrosion protection.Frequent color or resin changesCold runnerReduced purging effort and more flexible short-run operation.Request color-change procedures and sample standards.High-volume commodity packagingHeated runnerHigh output and reduced runner waste can recover the extra investment.Review cycle time, cavity balance, and automation layout.Engineering resin with high material valueHeated runnerRunner savings may be substantial even at moderate volume.Verify resin residence time and thermal stability.Medical or clean production componentsHeated runner or valve gateCleaner automated handling and reduced regrind exposure may support validation.Review material traceability and clean production requirements.Large parts with noncritical runnersCold runnerRunner percentage may be small compared with total part weight.Compare actual shot weights rather than assumptions.Break-even calculations should include conservative assumptions. Do not assume every gram of runner can be reground. Some products prohibit regrind because of appearance, mechanical performance, food-contact controls, medical requirements, glass-fiber degradation, or customer specifications. Similarly, do not assume a heated runner will automatically shorten the cycle. Cooling time is normally controlled by the thickest section of the molded part, not only by the runner. Mold flow analysis and trial data are the best ways to confirm the likely benefit.
Cold runner systems include conventional full-round runners, trapezoidal runners, three-plate molds, insulated runners, and automatically degated designs. Full-round runner geometry generally provides efficient flow but can require more machining. Three-plate molds can separate point-gated parts from runners automatically, which is useful for small cosmetic components and multicavity layouts. Insulated runners are a specialized middle ground that use a frozen outer plastic layer to contain a molten core, although their process window is narrower than conventional heated runner systems.
Heated runner systems are available in several configurations. Open gates are simple and often cost-effective, but they can leave gate vestige and may be unsuitable for every cosmetic surface. Valve gates use a pin to open and close each gate. They provide tighter control over gate appearance, filling sequence, weld line placement, and pack pressure. Thermal gates are common in many applications but need careful temperature control. Hot-tip and sprue-gate approaches can be selected according to part size, resin behavior, gate location, and surface requirements.
Runner system typeTypical useMain advantageMain limitationTwo-plate cold runnerGeneral-purpose housings, brackets, covers, and low-volume parts.Simple construction, low cost, and straightforward maintenance.Runner is ejected with every shot.Three-plate cold runnerSmall parts needing automatic point-gate separation.Automatic degating and flexible gate placement.More mold movement and more complex plate design.Insulated runnerSelected materials and intermediate-volume applications.Can reduce visible runner scrap without a full heated system.Narrow operating window and limited application range.Open-gate heated runnerCaps, containers, industrial parts, and many general production parts.No solid runner and relatively efficient system design.Gate vestige and stringing can require optimization.Valve-gate heated runnerAutomotive, medical, appliance, and high-cosmetic components.Precise gate control, improved appearance, and sequential filling options.Higher tooling, controls, and maintenance cost.Sequential valve-gate systemLarge panels, bumpers, appliance fronts, and complex large parts.Can manage weld lines and flow marks across large surfaces.Requires advanced mold-flow engineering and controls.Multi-zone manifold systemHigh-cavity molds and technically demanding resins.Individual temperature zones support balanced processing.Requires experienced technicians and reliable controllers.The correct system also depends on gate location. A gate placed in a nonvisible internal surface may allow a simpler open-gate heated runner or a conventional cold runner. A premium consumer product with a visible Class A surface may need a valve gate located where the mark can be concealed. For glass-filled or mineral-filled resins, wear-resistant gate components and carefully selected steel are important because abrasive materials can damage gates and nozzles over time.
The Global market for injection molds is increasingly shaped by shorter product cycles, greater pressure to reduce resin waste, and the move toward regionalized supply chains. North American buyers often source high-cavity systems and controller technology from established suppliers in Canada and the United States, while European programs commonly prioritize energy efficiency, process documentation, automation compatibility, and recycling compliance. Asian manufacturing hubs, particularly China, Japan, South Korea, and Singapore, provide broad capacity for mold making, component manufacturing, electronics, consumer products, and export-oriented production.
Trade hubs influence sourcing decisions. Shenzhen, Dongguan, Guangzhou, Ningbo, Shanghai, Suzhou, and Qingdao connect Chinese mold manufacturers with global shipping lanes through ports such as Yantian, Nansha, Ningbo-Zhoushan, and Shanghai. In Europe, Hamburg, Rotterdam, Antwerp-Bruges, and Valencia remain important industrial logistics gateways. In North America, Los Angeles, Long Beach, Houston, Chicago, Toronto, Detroit, and Monterrey support tooling, automotive, medical, consumer, and industrial supply networks.
Global buyers should distinguish between runner-system manufacturers and complete mold makers. A runner-system supplier typically designs and supplies manifolds, nozzles, controllers, spare parts, and technical support. A complete mold maker integrates the chosen runner system into the steel tool, performs DFM, machining, assembly, trials, sampling, and production support. The best outcome often comes from selecting the runner technology and mold maker together during the design phase rather than fitting a system after the mold layout has already been frozen.
The following companies are widely recognized in global injection molding supply chains. Buyers should confirm local service availability, regional spare-parts coverage, controller compatibility, resin experience, and the ability to support the exact mold size and cavity layout before final selection. The right provider depends on the project rather than brand recognition alone.
CompanyService regionsCore strengthsKey offeringsHusky TechnologiesGlobal; strong presence in North America, Europe, Asia, and packaging markets.High-output packaging systems, integrated molding solutions, and process expertise.Hot runners, molds, controllers, PET preform and closure production systems.Mold-MastersGlobal; manufacturing and service support across the Americas, Europe, and Asia.Broad hot runner portfolio and extensive application coverage.Manifolds, nozzles, temperature controllers, mold components, and valve-gate systems.SynventiveGlobal; established support in automotive, consumer, medical, and industrial markets.Advanced valve-gate technology and complex sequencing capability.Hot runner systems, controllers, servo-driven solutions, and engineering support.YudoGlobal; particularly strong across Asia, Europe, and the Americas.Large-scale hot runner manufacturing and wide product range.Hot runner systems, controllers, nozzles, manifolds, and mold accessories.HRSflowGlobal; strong footprint in Europe, North America, and automotive production hubs.Valve-gate systems for large, complex, and appearance-critical components.Sequential injection systems, servo control, hot runners, and automotive solutions.INCOEGlobal; active in North America, Europe, and international industrial markets.Custom-engineered systems and technical support for demanding molding programs.Hot runner manifolds, nozzles, valve gates, controllers, and custom configurations.HASCOGlobal; particularly established in European mold-making and component supply chains.Standardized mold components and engineering tools for repeatable mold construction.Mold bases, components, hot runner technology, temperature control, and accessories.This supplier comparison is useful as a starting point, not a substitute for technical review. A global brand may be ideal for a high-cavity closure mold operating around the clock, while a cost-effective regional system can be appropriate for a low-volume industrial enclosure. Request a documented recommendation based on resin grade, projected cycle count, cavity number, gate sequence, production country, available technicians, and planned maintenance schedule.
Begin with the part, not the runner system. Share a current 3D model, 2D drawing, resin specification, annual forecast, expected product life, cosmetic requirements, target machine tonnage, packaging method, and quality documentation needs. An experienced mold supplier should provide DFM feedback before quoting. This review should identify wall-thickness changes, undercuts, gate alternatives, weld-line risk, sink marks, warpage, draft angles, ejection concerns, and probable cycle time.
For a heated runner quote, specify whether the price includes the manifold, nozzles, temperature controller, cables, spare heaters, thermocouples, installation, commissioning, and training. Ask whether the system is compatible with local voltage and machine controls. For valve-gated tools, clarify whether pneumatic, hydraulic, electric, or servo actuation is included. Also request recommendations for spare parts that should be held near the production site.
For a cold runner quote, ask for shot weight and runner weight. If regrind is proposed, clarify the allowed percentage, regrind handling method, lot traceability, contamination controls, and impact on appearance and mechanical properties. For transparent, highly polished, medical, food-contact, flame-retardant, or reinforced parts, recycled runner use may be limited or prohibited.
Cold runner molds remain widely used across consumer products, electrical enclosures, industrial brackets, appliance components, office equipment, trays, caps, covers, and low-volume automotive service parts. They are especially practical where product demand is uneven, engineering updates are likely, or different colors must be produced in small batches.
Heated runner systems are common in high-volume packaging, automotive interiors and exteriors, medical disposables, communication devices, household appliances, electronic housings, personal-care packaging, and multicavity consumer components. Valve-gated systems are often selected for automotive bumper fascias, instrument panels, large appliance covers, high-gloss surfaces, and parts requiring controlled weld-line placement.
In the medical sector, mold selection must be aligned with validation, resin traceability, cleanliness requirements, and production documentation. In automotive production, long program life, annual volume, cosmetic requirements, and repeatability can justify a heated runner system. In consumer electronics, product refresh cycles may favor rapid cold runner tooling for early launches, followed by a heated runner production tool after demand is confirmed.
A startup developing a handheld diagnostic enclosure may initially choose a two-cavity cold runner tool. The first market release may require only several thousand parts, and design changes could follow user testing. The lower investment allows the brand owner to validate fit, texture, hinge performance, assembly, and packaging before committing to a multicavity production tool. If demand grows and the enclosure resin is expensive flame-retardant polycarbonate, a later heated runner conversion may improve long-term economics.
An automotive supplier producing a high-gloss interior trim component may choose a valve-gated heated runner system. The system can help place gates away from visible zones, control filling across a broad surface, and reduce weld lines. Although the mold investment is higher, the program may run for several years with large annual volumes. The saved material, stable automation, and reduced cosmetic rejection rate can support the higher initial cost.
A manufacturer of industrial cable-management clips may select a multicavity cold runner mold where polypropylene runner can be carefully reground and used at an approved percentage. The parts are compact, resin cost is modest, and color changes are frequent. In this situation, a heated runner may offer limited payback while increasing changeover complexity.
A medical consumables producer making small polypropylene components may select a heated runner mold when runner regrind is not allowed and automated packing is required. The reduction in loose runner handling can simplify downstream operations, while a properly validated temperature profile protects material quality. The final choice should still be supported by documented validation and maintenance procedures.
TEAM Rapid supports Global market customers with rapid tooling, injection molding, CNC machining, 3D printing, vacuum casting, die casting, finishing, assembly, packaging, procurement support, and direct shipping from integrated manufacturing resources in China. Its ISO 9001:2015 quality management system, more than 10 years of manufacturing experience, over 6,000 delivered projects, and customers in more than 25 countries provide practical evidence of export-oriented production capability. Rather than claiming unverified overseas subsidiaries or local warehouses, TEAM Rapid provides direct engineering communication, responses typically within a few hours, DFM-based manufacturability analysis, export coordination, and continuing online pre-sale and after-sale support for international buyers. The company serves end users, distributors, dealers, brand owners, startups, engineers, and individual product developers through flexible OEM, ODM, wholesale, prototype, low-volume, and recurring-production cooperation models. It can manufacture custom plastic and metal parts from a single prototype to more than 100,000 pieces, while offering EPC, turnkey, and customer-owned plant solutions where project scope requires coordinated manufacturing support; it does not provide BOO or on-site bulk supply services. For heated and cold runner projects, TEAM Rapid helps buyers compare resin usage, cavity layout, mold life, cycle time, gate placement, tooling cost, and future production requirements before tooling approval.
For projects requiring a quick bridge from design validation to molding, TEAM Rapid can support rapid tooling and molded part production in approximately 5 to 25 days depending on complexity. Its engineering team can recommend whether a simpler cold runner layout is appropriate for early-stage demand or whether a heated runner system is justified for sustained production. Customers can review rapid tooling services for global product programs when evaluating bridge tools, pilot molds, and production-ready tooling strategies.
TEAM Rapid’s practical advantage is the ability to connect DFM review, tool construction, molding trials, secondary finishing, assembly, packaging, and shipment without forcing buyers to manage disconnected suppliers. For projects involving molded housings, trays, fillers, covers, enclosures, automotive components, medical-device parts, or commercial-product assemblies, this integrated approach can reduce communication delays and improve accountability from first sample through repeat orders. Buyers can submit part files, resin requirements, expected volumes, and destination details through the global manufacturing quotation request process for a runner-system and tooling recommendation.
By 2026, mold buyers will face increasing pressure to improve material efficiency and document production sustainability. Heated runner systems are likely to gain further adoption where virgin-resin reduction, waste reporting, and automated handling are strategic priorities. This does not mean cold runners will disappear. Cold runner tools will remain essential for flexible production, prototype tooling, low-volume applications, short product life cycles, and markets where simple maintenance is more valuable than maximum material efficiency.
Advanced process monitoring will become more common. Temperature sensors, cavity-pressure monitoring, shot-to-shot data collection, predictive maintenance alerts, and connected controllers can help detect imbalance before a large quantity of defective parts is produced. For valve-gated molds, smarter sequencing can improve surface quality and reduce warpage on large or complex components. AI-assisted mold-flow analysis and digital process records will also help manufacturers optimize gate positions, cooling channels, packing profiles, and maintenance planning.
Policy and customer requirements around recycled content, material traceability, energy use, and extended producer responsibility will influence runner selection. Regrind control in cold runner programs will need clearer documentation, especially for regulated products. Heated runner systems may support cleaner material accounting, but they also require thoughtful energy management and durable component design. The most sustainable choice is project-specific: it balances resin savings, equipment life, electricity use, maintenance, mold longevity, logistics, and end-product recyclability.
No. A heated runner mold is usually better for stable high-volume production, expensive resin, high automation, or applications where runner scrap cannot be reused. A cold runner mold is often the more economical choice for prototypes, low volumes, frequent changes, and projects with uncertain demand.
The premium depends on cavity count, mold size, resin, gate style, brand, controller requirement, and whether valve gates are used. A simple open-gate system can add a moderate amount, while a multicavity valve-gate system with sequencing controls can add significantly more. Request itemized quotations rather than using a fixed percentage.
Often it can, but only if the resin specification and customer requirements allow it. Regrind percentage should be controlled, documented, and tested. Some applications, including certain medical, cosmetic, transparent, reinforced, food-contact, and highly regulated parts, may restrict or prohibit regrind use.
Not always. Many cosmetic parts can be molded successfully with cold runners or open-gate heated runners when gate location and processing are optimized. Valve gates are particularly useful when gate marks, weld lines, flow marks, or filling sequence need more precise control.
Cold runner tooling is typically best for low-volume injection molding because it has lower initial investment, simpler maintenance, and easier material or color changes. A heated runner may still be justified if the resin is expensive and runner waste is unusually high.
Include 3D CAD files, drawings, resin grade, annual demand, expected program life, target part price, appearance requirements, tolerance requirements, target market, machine information if known, color options, packaging needs, and whether you prefer cold runner, heated runner, or an engineering recommendation.
Sometimes, but conversion is not always economical or technically straightforward. The mold layout, cavity positions, plate thickness, cooling, gate design, and manifold space must be considered from the start. If future volume growth is likely, ask the mold designer to assess upgrade potential during the first DFM review.
-
Global Market: Plastic Injection Molding or Thermoforming?
For most complex, durable, precision plastic housings, injection molding is the better long-term production method. It supports ribs, bosses, clips, snap fits, undercuts, textured surfaces, tight tolerances, and repeatable assembly features. Thermoforming is usually the better option for large, shallow, lightweight housings, covers, trays, panels, equipment skins, and lower-volume products where low tooling cost and fast market entry matter more than complex geometry.
Choose injection molding when the housing requires structural strength, detailed internal features, consistent wall thickness, high production volumes, or polished consumer-facing appearance. Choose thermoforming when the part is large, relatively open, deep-drawn, less detailed on the back side, or when production demand does not justify the cost of a full injection mold.
For global buyers, a practical approach is to validate design intent through CNC machining, 3D printing, or vacuum casting, then select thermoforming for large low-to-medium volume housings and injection molding for scalable production. Qualified international suppliers, including experienced Chinese manufacturers with ISO-certified quality systems, engineering support, responsive pre-sales and after-sales communication, and cost-performance advantages, can be strong sourcing options alongside regional suppliers.
Common global suppliers to evaluate include TEAM Rapid in China, Berry Global in North America and Europe, Pactiv Evergreen in North America, Universal Plastics in the United States, RapidMade in the United States, and Spartech in North America. The right supplier should be selected based on part size, annual volume, resin requirements, tooling strategy, testing needs, logistics route, and communication quality rather than only unit price.
Plastic housings protect electronics, medical instruments, machinery, consumer devices, office equipment, automotive systems, communication products, and industrial controls. Across the global market, buyers are under pressure to reduce launch time, lower material consumption, increase recycled content, improve product appearance, and create products that are easier to assemble and repair. These requirements have made the choice between injection molding and thermoforming a strategic manufacturing decision rather than a simple material-processing choice.
Injection molding remains one of the most widely used methods for producing engineered plastic enclosures. Molten resin is injected under pressure into a closed mold cavity. The process creates highly repeatable three-dimensional components with internal and external details. It is frequently used for handheld devices, appliance covers, automotive trim, electrical junction boxes, medical device casings, laboratory equipment, and industrial control housings.
Thermoforming heats a plastic sheet until it becomes formable, then draws or presses it over or into a mold. Vacuum forming, pressure forming, twin-sheet forming, and heavy-gauge thermoforming are common variants. Thermoforming is especially competitive for large panels, machine guards, kiosk housings, vehicle interior panels, refrigerator liners, equipment covers, storage trays, retail displays, and protective shells.
Major manufacturing and trade hubs influence how companies source plastic housings. Shenzhen, Dongguan, Ningbo, Suzhou, and Shanghai remain important production centers for tooling, molded parts, electronics assembly, and export shipping from ports such as Shenzhen Yantian, Ningbo-Zhoushan, and Shanghai. In North America, Chicago, Detroit, Atlanta, Los Angeles, Monterrey, and Toronto support automotive, medical, electronics, appliance, and industrial supply chains. European activity is concentrated around Germany, the United Kingdom, France, Italy, Poland, the Netherlands, and Central European automotive clusters. Singapore, Seoul, Tokyo, Mumbai, Ho Chi Minh City, and Bangkok also play important roles in electronics, industrial equipment, and consumer-product manufacturing.
The best process is not determined solely by geography. It depends on geometry, part size, annual demand, resin grade, quality requirements, visual expectations, assembly design, shipping method, and tooling investment. A supplier that can support design-for-manufacturability review, rapid prototyping, tooling, molding, finishing, assembly, packaging, and export logistics can substantially reduce risk for buyers operating across several markets.
The essential difference is how material becomes a finished part. Injection molding starts with resin pellets and forms a part inside a closed mold. Thermoforming starts with plastic sheet and stretches it over a forming tool. This affects tooling cost, surface quality, wall thickness, internal feature capability, scrap rate, cycle time, and the range of viable housing designs.
Injection molding uses more complex tooling because the mold must withstand repeated clamping and injection pressure. The initial cost can be substantial, especially for multi-cavity tools, slides, lifters, hot runners, polished surfaces, textured finishes, and engineering resins. However, the mold can produce thousands or millions of repeatable parts, making the process efficient at higher volumes.
Thermoforming tools are often faster and less expensive to manufacture, particularly for large parts. A single-sided tool may be enough for early production, while pressure forming and matched-mold systems provide more detail and better control. The process can be particularly economical when a large housing would require an unusually large injection mold and injection molding machine.
Selection FactorInjection MoldingThermoformingPractical Buying ImpactInitial tooling investmentHigher because of precision mold construction, cooling, ejection, and possible side actionsUsually lower, especially with single-sided forming toolsThermoforming can reduce launch risk for low-volume or large housingsPart complexityExcellent for bosses, ribs, clips, threads, snap fits, inserts, and enclosed geometryBest for open, shallow, or large shells with fewer backside detailsChoose injection molding for functional assemblies and detailed enclosuresPart sizeEconomical for small to medium parts; large tools require significant equipment capacityVery strong for large panels, covers, liners, and equipment skinsThermoforming often wins for oversized housingsWall thicknessGenerally uniform and controllable with proper flow and cooling designCan thin in stretched areas, especially at corners and deep draw zonesDesigners must account for thinning in thermoformed partsProduction volumeStrongest for medium to very high production runsCompetitive for prototypes, low volume, medium volume, and selected high-volume productsUse projected annual demand to evaluate total cost instead of tooling cost aloneSurface appearanceCan provide fine texture, high gloss, matte finish, grain, logos, and cosmetic detailGood cosmetic appearance on the tool-contact side; detail depends on forming methodInjection molding is preferred for premium handheld consumer housingsMaterial utilizationRunner systems can create waste unless hot runners or regrind strategies are usedTrim scrap is generated around the formed part, although it may be recyclable by material typeWaste planning matters for sustainability and resin-cost controlThis comparison shows why neither process is universally better. Injection molding offers engineering freedom and high repeatability. Thermoforming offers an economical path for large, simpler shapes and faster tool development. Buyers should compare complete landed cost, including tooling, resin, secondary operations, packaging, freight, customs exposure, inspection, inventory, and expected revisions.
Injection molding is generally the preferred method when a housing performs more than a cosmetic function. A product enclosure may need to locate a circuit board, hold screws, support a display, seal against dust, guide cables, retain a battery, absorb impacts, connect to a mating component, or manage heat. These requirements depend on molded-in functional features that are difficult, expensive, or unreliable to create through thermoforming alone.
Typical injection-molded housing features include:
Injection molding is also a strong choice when dimensional consistency is important. Medical housings, laboratory-device components, communication equipment, electrical appliance parts, automotive modules, and industrial instruments often require repeatable mating surfaces. A properly designed injection mold, supported by process control and inspection, can maintain dependable dimensions over long production runs.
For products with high annual demand, the cost per part can decrease substantially as fixed tooling cost is spread over more units. Multi-cavity tooling, automation, hot-runner systems, robotic handling, in-mold labeling, and automated inspection can further improve throughput. However, these advantages depend on a stable design. If geometry is likely to change frequently, buyers should consider bridge tooling, rapid tooling, modular inserts, or an interim process before committing to hardened production tooling.
Thermoforming is highly effective when part size is large relative to its complexity. It is often selected for machine enclosures, medical equipment covers, transport interiors, refrigerator liners, point-of-sale fixtures, protective panels, industrial housings, battery-equipment covers, and kiosks. These products may require a durable, attractive outer shell without extensive molded-in internal mechanisms.
Heavy-gauge thermoforming can produce robust ABS, HIPS, polycarbonate, PETG, acrylic, HDPE, or ABS/polycarbonate parts. Pressure forming can create sharper details than basic vacuum forming, making it suitable for branded surfaces, texture, vents, recesses, and certain visual features. Twin-sheet forming joins two formed sheets, allowing hollow structures, improved rigidity, and enclosed channels without the capital cost of a massive injection mold.
Thermoforming may be the practical answer when a buyer needs a large housing quickly. Tooling can be fabricated from aluminum, cast materials, composites, or other formats depending on expected volume and detail. Lead times can be shorter than conventional injection mold development, particularly when the design avoids deep draws, sharp corners, severe undercuts, and thin unsupported features.
The main design caution is material thinning. As a heated sheet stretches into a deep cavity, the material becomes thinner around corners, sidewalls, and high-draw regions. Designers should use generous radii, appropriate draft angles, controlled draw ratios, and thickness allowances. Secondary trimming, drilling, routing, bonding, fastening, painting, screen printing, and assembly may also be required, so these operations should be included in the initial quotation.
Material selection should reflect operating temperature, impact requirement, UV exposure, chemical resistance, electrical performance, flame rating, aesthetics, recyclability, and regulatory obligations. A resin that works well for a consumer product may be unsuitable for a medical, industrial, automotive, or outdoor application.
MaterialCommon ProcessHousing AdvantagesTypical ApplicationsABSInjection molding and thermoformingGood impact resistance, easy finishing, balanced cost, attractive surfaceConsumer electronics, appliance covers, equipment shells, office productsPC/ABSPrimarily injection molding; selected thermoformed grades availableImproved toughness, heat resistance, and premium appearanceAutomotive interiors, communication devices, durable electronic housingsPolycarbonateInjection molding and thermoformingHigh impact strength, transparency options, heat capabilitySafety covers, medical equipment, machine guards, transparent panelsPPInjection molding and thermoformingChemical resistance, low density, living-hinge performanceStorage housings, battery cases, packaging, industrial containersPETGThermoforming and selected injection applicationsClear appearance, formability, good chemical resistanceMedical trays, transparent covers, display components, equipment guardsHIPSThermoformingEasy forming, economical, suitable for large cosmetic shellsAppliance liners, displays, interior panels, protective housingsNylonInjection moldingWear resistance, strength, heat performanceMechanical housings, automotive components, industrial fittingsPBTInjection moldingElectrical stability, heat resistance, dimensional performanceElectrical enclosures, connector bodies, automotive electronic partsMaterial data sheets are only a starting point. Housing performance depends on grade selection, colorants, fillers, recycled-content level, wall thickness, gate location, drying conditions, mold temperature, cooling time, and environmental exposure. For electrically sensitive, outdoor, flame-retardant, food-contact, or medical applications, buyers should define required standards before tooling begins and request resin traceability where appropriate.
Successful housings are designed for the chosen process from the beginning. A design that appears simple in CAD can become expensive if it requires unnecessary side actions, deep draws, uneven walls, overly sharp corners, inaccessible trimming, difficult assembly, or cosmetic surfaces located in high-risk areas.
Design TopicInjection Molding GuidanceThermoforming GuidanceCommercial EffectDraft angleUse sufficient draft for textured and untextured surfaces to support ejectionUse generous draft to release formed parts from the toolImproves surface quality and reduces damage during demoldingWall thicknessKeep walls reasonably uniform to reduce sink, warpage, and uneven coolingAllow for thinning in stretched regions and deep drawsReduces rejects and improves part durabilityCorner radiusUse radii to improve resin flow and reduce stress concentrationUse larger radii to support material flow over the formImproves strength and lowers manufacturing difficultyUndercutsUse slides, lifters, collapsible cores, or redesign where economicalAvoid where possible; add secondary operations only when justifiedUndercuts can significantly increase tool and cycle costAssembly featuresIntegrate bosses, clips, alignment pins, and gasket groovesUse trimming, bonded inserts, fasteners, or secondary fixtures when neededEarly planning prevents expensive manual assemblyCosmetic surfacesPlace gates and ejector marks away from critical appearance areasDefine the preferred cosmetic side and texture strategy before toolingProtects brand appearance and reduces finishing requirementsTolerancesApply tight tolerances only to functional interfacesAllow realistic tolerances based on size, sheet behavior, and trimming methodPrevents unnecessary inspection and tooling costsA professional DFM review should examine nominal wall thickness, draft, ribs, bosses, gate location, parting line, ejection, weld lines, shrinkage, warpage, cooling, texture, assembly, and inspection points. For thermoforming, the review should additionally analyze draw ratio, sheet thickness, plug-assist need, corner thinning, trim access, nesting efficiency, and post-forming operations.
Before ordering production tools, buyers should consider prototype validation. Functional models can be created through rapid prototyping services using CNC machining, SLA or SLS 3D printing, and vacuum casting. These methods can help verify hand feel, assembly clearance, screw access, cable routing, display fit, and user interaction before expensive production tooling is released.
Buyers should ask every supplier to quote the complete manufacturing route rather than only the molded component. A housing may need resin procurement, mold design, machining, molding or forming, trimming, inserts, painting, silk screening, laser marking, ultrasonic welding, assembly, packaging, inspection, and shipment. Comparing incomplete quotations can lead to unexpected costs after tooling approval.
Start by defining the expected annual demand and product life cycle. A 500-unit pilot build, a 5,000-unit market-entry run, and a 100,000-unit annual program require different tooling decisions. Low-volume production may justify rapid tooling, aluminum tools, or thermoforming tools. Stable high-volume programs may justify hardened multi-cavity injection tooling with automated handling.
Request a clear tooling ownership agreement. It should state who owns the mold, where it is stored, maintenance responsibilities, expected tool life, cavity count, revision policy, spare-part availability, and conditions for transferring the tool. Buyers should also ask whether the supplier can provide mold-flow guidance, first-article inspection, dimensional reports, material certificates, cosmetic limit samples, and pre-shipment quality records.
For international shipments, include packaging and freight planning early. Large thermoformed housings can consume significant shipping volume, while injection-molded parts may allow better nesting and denser packing. Products shipping through Shanghai, Ningbo-Zhoushan, Shenzhen, Rotterdam, Hamburg, Los Angeles, Long Beach, or Singapore should be evaluated for container efficiency, transit time, customs documentation, and warehouse handling.
When comparing suppliers, use a structured request for quotation that includes 3D CAD files, 2D drawings where available, material grade, color, finish, annual volume, target delivery date, required certifications, critical dimensions, assembly requirements, packaging instructions, and destination. Buyers needing technical support can submit part files through a custom manufacturing quotation request to receive manufacturing feedback before making a tooling decision.
Injection molding and thermoforming are used throughout the global market, but their strengths appear differently by industry.
A startup developing a handheld environmental monitor may select injection molding for its final enclosure because the design requires a display window, battery door, screw bosses, gasket channel, sensor vents, and internal PCB supports. Before committing to a full tool, the team can use CNC-machined or vacuum-cast prototypes to test ergonomics and assembly. A bridge production tool can then support early market units while design feedback is collected.
An industrial automation company producing a large operator-console cover may choose heavy-gauge thermoforming. The part is wide, visually important, and relatively shallow, but it does not need numerous internal clips or tightly controlled mechanical interfaces. Pressure forming can provide a professional front surface, while CNC trimming creates openings for screens, switches, and cable ports. Metal brackets or molded inserts can be added later for structural assembly.
A medical-equipment manufacturer producing a diagnostic cart may use a hybrid strategy. Large external shells can be thermoformed to reduce tooling investment and simplify production of oversized parts. Smaller functional components, including latches, cable-management clips, handles, instrument trays, and interface panels, can be injection molded. This combination often balances appearance, function, tool cost, and serviceability.
An automotive aftermarket brand launching a low-volume accessory may begin with thermoformed protective covers or rapid injection tooling. If sales increase and the design becomes stable, the company can move to higher-cavity injection tooling. This phased approach helps prevent a large upfront investment before demand is proven.
The supplier landscape includes specialists in high-volume packaging, custom industrial thermoforming, precision injection molding, rapid tooling, and integrated manufacturing. The companies below are established names that buyers can evaluate based on project fit. Capabilities, location coverage, certifications, minimum order requirements, and material availability should be confirmed directly for each program.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidGlobal customers, including North America, Europe, Asia, and other export marketsRapid tooling, engineering-led DFM, flexible production from prototypes to 100,000-plus partsInjection molding, CNC machining, 3D printing, vacuum casting, die casting, finishing, assembly, packaging, and shippingBerry GlobalNorth America, Europe, Asia-Pacific, and global consumer-product supply chainsLarge-scale plastics manufacturing, material innovation, packaging and engineered product capabilityInjection molding, thermoforming, packaging, closures, containers, and engineered plastic productsPactiv EvergreenNorth America with broad foodservice and packaging distributionHigh-volume foodservice and consumer packaging productionThermoformed packaging, foodservice products, containers, trays, and related packaging solutionsUniversal PlasticsUnited States and export-oriented industrial customersCustom heavy-gauge thermoforming for complex large partsVacuum forming, pressure forming, twin-sheet forming, trimming, assembly, and finishingRapidMadeUnited States with support for commercial and industrial programsRapid manufacturing, low-volume production, digital manufacturing supportInjection molding, thermoforming, CNC machining, additive manufacturing, and production partsSpartechNorth AmericaEngineered thermoplastic materials, sheets, and thermoforming-related solutionsCustom sheet extrusion, thermoforming materials, packaging, and engineered plastic applicationsPlastikon IndustriesNorth America, Asia, and global automotive and consumer-product supply chainsComplex injection molding, automotive quality practices, multi-location manufacturingInjection molding, tooling coordination, assembly, decoration, and engineered plastic componentsThis table is a starting point rather than a substitute for supplier qualification. Buyers should compare process specialization, part-size range, quality system, toolmaking capability, design support, response time, export experience, inspection process, and ability to handle secondary operations. For large thermoformed covers, a specialist may be the best fit. For complex housings requiring detailed engineering features, a manufacturer with in-house mold building and injection capability may offer better control.
TEAM Rapid supports global product developers and purchasing teams with a manufacturing pathway that connects prototype validation, tooling, molded production, finishing, assembly, packaging, and shipping. Its ISO 9001:2015 quality management certification, in-house machining and tooling capability, tight CNC tolerance capability down to 0.01 mm, material selection support, DFM analysis, inspection planning, and experience across more than 6,000 delivered projects provide practical evidence for plastic-housing development from early samples to repeat production. As a custom manufacturer rather than a branded-component assembler, TEAM Rapid does not claim proprietary core component brands; instead, it works with specified plastic and metal materials, customer-approved components, documented process controls, and manufacturing checks aligned with project requirements. The company serves innovators, end users, distributors, dealers, brand owners, engineering teams, and individual product developers through flexible OEM/ODM-oriented manufacturing, wholesale production, prototype orders, recurring production, regional distribution support, assembly, contract packaging, and direct shipping. Its stated customer base spans more than 25 countries, including customers in China, the USA, the UK, France, Germany, and other international markets, supported by one-to-one engineering communication and replies typically provided within hours. While no overseas subsidiary or local warehouse is stated in the company information, its established export experience, cross-cultural project support, online pre-sales engineering review, production updates, inspection coordination, packaging support, and after-sales communication provide concrete cross-border service assurance for global buyers. TEAM Rapid provides customer-owned tooling and turnkey manufacturing solutions, including procurement, component assembly, packaging, kitting, planning, and shipping; it does not operate BOO or on-site bulk supply service models.
For housings with complex geometry, TEAM Rapid can provide custom injection molding services supported by rapid tooling and DFM review. This is particularly useful for covers, cases, enclosures, trays, fillers, appliance components, industrial housings, and functional plastic parts that require controlled geometry and repeatable assembly features.
By 2026, housing production decisions will be shaped by sustainability requirements, regional supply-chain resilience, digital manufacturing, and higher expectations for product customization. Buyers should consider these trends during product planning rather than treating them as later compliance issues.
Recycled-content plastics will continue to expand, particularly in consumer products, packaging, appliances, and industrial housings. Post-consumer recycled ABS, polypropylene, PET, and other compounds may reduce environmental impact, but they can introduce variation in color, flow behavior, mechanical properties, and cosmetic consistency. Manufacturers will need to validate recycled-content grades through practical trials, especially for safety-critical or appearance-sensitive parts.
Design for disassembly will become more important. Products that use fewer mixed materials, simpler fastening systems, removable electronic modules, and clearly identified resin types may be easier to repair, refurbish, and recycle. Injection molding is well suited to integrated fastening features, while thermoforming can reduce assembly complexity for large external shells. Both processes can support circularity when material choices and end-of-life plans are made early.
Digital inspection, automation, mold monitoring, machine data collection, and cloud-based production communication will improve traceability. Buyers will increasingly request first-article reports, visual standards, lot records, material certificates, dimensional data, and production photographs as part of normal supplier management. These practices are valuable for global teams that cannot visit every factory in person.
Regionalized sourcing will also remain important. Some brands will use dual-source strategies, such as a manufacturing partner in Asia for competitive tooling and scalable production plus a regional supplier for short-run replenishment or service parts. Ports including Shanghai, Shenzhen, Ningbo, Rotterdam, Hamburg, Los Angeles, Long Beach, and Singapore will remain central to these global supply strategies.
Thermoforming is expected to gain further interest for large lightweight components, recycled-content sheet applications, electric-vehicle interiors, medical equipment covers, and industrial machinery skins. Injection molding will remain essential for precision housings, smart-device enclosures, battery systems, connectors, clips, latches, medical products, and high-volume consumer components.
Thermoforming is often cheaper at low volumes or for very large, relatively simple housings because tooling is usually less expensive. Injection molding can become more economical as volume increases, especially for smaller, more detailed parts that require integrated features and minimal secondary assembly.
Yes, especially with pressure forming, careful tool design, and secondary CNC trimming. However, thermoforming is less suitable than injection molding for small snap fits, deep ribs, screw bosses, enclosed geometry, complex internal supports, and precision mating features.
There is no universal threshold. The decision depends on part size, complexity, resin, number of cavities, tool type, labor content, and product life cycle. Injection molding may be justified at a few thousand parts for a complex functional housing, while thermoforming may remain competitive at much higher volumes for large shallow shells.
Yes. Hybrid products are common. Large cosmetic shells can be thermoformed, while clips, latches, handles, internal brackets, connector frames, and small detailed panels can be injection molded. This approach can reduce tooling cost without sacrificing function.
Lead time depends on mold size, complexity, cavity count, steel selection, finish requirements, and design changes. Rapid tooling can be completed much faster than hardened production tooling. TEAM Rapid states that rapid tooling and molded part production can be supported in approximately 5 to 25 days depending on project requirements.
Include a 3D CAD file, drawings if available, target resin, color, texture, expected annual quantity, destination, critical dimensions, flame or regulatory requirements, assembly needs, packaging requirements, and desired production timing. Identify whether the request is for prototype, bridge production, or long-term volume production.
They can be suitable when the supplier has verifiable tooling capability, documented quality systems, DFM support, clear communication, export experience, appropriate inspection practices, and a workable logistics plan. Buyers should qualify suppliers through technical review, sample approval, tooling agreements, inspection requirements, and transparent production communication.
Yes, especially for housings with electronics, seals, moving parts, user-contact surfaces, or multiple mating components. Prototyping can reveal fit, assembly, ergonomics, strength, and cosmetic issues before a production tool is built.
-
Global Market Guide to Vacuum Casting and Injection Molding
For the Global market, choose vacuum casting when you need realistic prototype parts, short runs, frequent design updates, and lower upfront tooling cost. Choose injection molding when the design is stable and you need repeatable parts at medium-to-high volumes with the lowest unit cost. Vacuum casting is usually the practical bridge between 3D printing and production tooling, while injection molding is the long-term choice for scalable commercial production.
Buyers may also consider qualified international suppliers, including China-based manufacturing partners with ISO-certified quality systems, detailed pre-sales engineering support, responsive after-sales communication, and favorable cost-performance. For global projects, this can reduce development expense while maintaining access to rapid prototyping, tooling, molding, finishing, assembly, packaging, and direct shipment.
Vacuum casting and injection molding can both create plastic components that look and function like production parts, but their manufacturing logic is fundamentally different. Vacuum casting uses a silicone mold made from a master pattern, often produced by SLA 3D printing or CNC machining. Liquid polyurethane resin is mixed, poured or injected into the mold under vacuum, and cured. The resulting parts can closely simulate common thermoplastics such as ABS, polypropylene, acrylic, rubber-like elastomers, and flame-retardant engineering plastics.
Injection molding uses a rigid mold, typically aluminum or steel, into which molten thermoplastic is injected at pressure. The mold opens after cooling, ejecting a part that can be repeated thousands or millions of times depending on tool design, resin choice, maintenance, and required quality level. It supports a much wider selection of production polymers, including PP, ABS, PC, PA, POM, TPE, PBT, PET, PPS, glass-filled grades, medical-grade materials, and high-temperature engineering plastics.
For global product teams operating across Shenzhen, Hong Kong, Singapore, Rotterdam, Hamburg, Los Angeles, Chicago, London, Paris, Munich, Dubai, and Sydney, the best process is rarely determined by volume alone. Product maturity, certification needs, shipping schedule, design-change risk, finish requirements, supply-chain resilience, and expected product life all affect the decision.
Decision FactorVacuum CastingInjection MoldingPractical Buying ImplicationTypical quantityAbout 10 to 100 parts per silicone mold setHundreds to 100,000+ partsUse casting for pilots; use molding for established demand.Tooling materialSilicone rubberAluminum, pre-hardened steel, or hardened steelSilicone tools are fast and affordable but have a limited life.Tooling investmentLowModerate to highInjection molding requires more confidence in the final design.Lead timeOften days to a few weeksRapid tooling may take days or weeks; production tools take longerVacuum casting is useful for urgent testing and launch samples.Material selectionPolyurethane formulations that simulate plastics and rubberBroad range of production thermoplastics and elastomersUse molding when the final resin must be exact.Surface finishCopies the master pattern and mold texture very wellControlled by mold polish, etching, texture, and resinBoth can produce cosmetic parts when tooling is prepared correctly.Dimensional repeatabilityGood for prototypes, with resin shrinkage and mold aging considerationsHigh after process validationInjection molding is better for critical repeatability.Design changesFast and relatively low-costCan require costly tool modificationDelay hard tooling until major design risks are closed.The table shows why vacuum casting is not simply “cheap injection molding.” It is a specialized low-volume process suited to flexible product development. Injection molding is not merely a high-volume option either; rapid aluminum tooling can make it commercially sensible at lower quantities when actual production resin, mechanical performance, or regulatory documentation is essential.
Vacuum casting is especially valuable when a development team needs parts that are more convincing than standard 3D prints. SLA masters can reproduce sharp lettering, fine cosmetic features, smooth external surfaces, and detailed geometries. Silicone molds capture these features, allowing manufacturers to create presentation models, engineering samples, trade-show units, fit-check parts, and user-testing batches that closely resemble final products.
It is a strong option for startups and product teams that expect design revisions. A handheld device enclosure may need an extra vent, a revised battery door, a stronger snap fit, or a different button location after early testing. Updating an SLA master and making a new silicone mold is substantially easier than revising steel tooling. This makes polyurethane casting highly useful during the period when industrial design and mechanical engineering are still converging.
Common vacuum-cast products include consumer electronics housings, medical device covers, wearable-device shells, automotive interior trim samples, lighting lenses, dashboard prototypes, small appliance casings, cable-management parts, grips, soft-touch components, seals, and transparent demonstration models. It is also practical for low-volume legacy replacement parts where commissioning a metal injection mold would not be commercially justified.
Injection molding is the preferred route when product design is sufficiently mature, annual demand is predictable, and customers need production-grade materials. It enables repeatable manufacturing of enclosures, clips, gears, caps, fittings, trays, housings, medical components, automotive parts, electrical connectors, appliance parts, consumer product shells, and industrial assemblies.
In a mature production program, the initial mold cost is spread across thousands of parts. This reduces the unit cost, improves repeatability, and supports automated quality controls. Injection molding is also the stronger choice where functional requirements depend on a named polymer grade, such as UV-stabilized polypropylene for outdoor use, polycarbonate for impact resistance, nylon with glass fiber for structural stiffness, POM for low-friction moving components, or medical-grade resin for regulated devices.
Global buyers should treat injection molding as a manufacturing system rather than a single machine operation. The final outcome depends on mold design, gate location, cooling channels, resin drying, molding parameters, cavity balance, inspection strategy, packaging, logistics, and supplier communication. A low mold quote can create expensive problems if it overlooks cycle time, warpage control, steel selection, mold maintenance, or testing requirements.
Production SituationRecommended ProcessWhy It FitsRecommended Next StepConcept samples for investor presentationsVacuum castingFast cosmetic parts with limited upfront costCreate an SLA master and define the visual finish.Ten to fifty functional test unitsVacuum castingSuitable for fit, form, handling, and early assembly checksValidate material simulation and insert requirements.Short pilot run with changing designVacuum casting or rapid toolingChoice depends on final material requirementsReview projected revisions before committing to a mold.Several hundred parts in final production resinRapid injection toolingProvides actual thermoplastic performanceUse aluminum tooling where appropriate.Thousands of repeat parts per yearInjection moldingLower unit cost and reliable repeatabilityEvaluate multi-cavity mold economics.More than 100,000 parts or long product lifeProduction injection moldingDurable tooling supports ongoing supplySelect suitable steel, maintenance plan, and automation level.Highly regulated or safety-critical componentInjection molding after validationSupports specified materials and controlled processesDefine traceability, inspection, and documentation requirements.Injection molding can also support insert molding and overmolding. Insert molding places metal, threaded components, electrical terminals, magnets, or other parts into the mold before plastic injection. Overmolding adds a second material layer, such as a soft TPE grip on a rigid housing. These capabilities are valuable for global consumer electronics, automotive, medical, industrial, and appliance programs where assembly reduction and ergonomic quality matter.
Material choice should begin with the product’s actual environment. A desktop device housing may prioritize cosmetic finish and flame resistance. A portable medical device may prioritize impact strength, cleanability, and traceability. An automotive under-hood part may require heat and chemical resistance. A consumer-product grip may require soft-touch feel, tear resistance, and color durability. Selecting a process before clarifying the performance target often creates rework.
Part RequirementVacuum Casting Material DirectionInjection Molding Material DirectionTypical ApplicationsGeneral rigid housingABS-like polyurethaneABS, PC/ABS, HIPSEnclosures, appliances, electronic coversHigh impact strengthImpact-resistant polyurethanePolycarbonate, PC/ABS, impact-modified nylonHandheld products, guards, rugged devicesTransparent or translucent partClear polyurethane resinPC, PMMA, clear PPLenses, display windows, fluid-view componentsFlexible grip or sealRubber-like polyurethaneTPE, TPU, silicone-compatible molding solutionsGrips, seals, protective covers, gasketsHeat-resistant componentHeat-resistant polyurethane simulationPA, PBT, PPS, high-temperature PC gradesIndustrial equipment, electrical parts, automotive itemsLow-friction moving partSpecialized polyurethane where suitablePOM, PA, PTFE-filled compoundsGears, latches, sliders, mechanismsOutdoor exposureUV-resistant polyurethane with testingUV-stabilized PP, ASA, PC, nylonOutdoor devices, covers, utility componentsSurface finish is another decisive factor. Vacuum casting often begins with an SLA master that can be polished, painted, textured, or finished to create the desired mold surface. Injection molding offers a broader range of repeatable tooling finishes, including high polish, satin, fine texture, spark erosion texture, laser texture, and molded logos. In both processes, the quality of the initial CAD and surface specification affects the final result.
Designers should include draft wherever possible. Vacuum casting can tolerate certain geometries because silicone molds flex, but deep undercuts can shorten mold life or complicate demolding. Injection molding generally requires more disciplined draft, controlled wall thickness, properly designed ribs, uniform transitions, and carefully planned gate locations. Thick areas can cause sink marks, voids, long cooling cycles, and warpage. Sharp internal corners can create stress concentration. A detailed DFM review is the most cost-effective point to identify these risks.
Vacuum casting usually wins on initial cost. The master pattern and silicone mold are comparatively inexpensive, so the buyer can obtain a small batch without a large tooling payment. However, the unit cost remains higher because the process is labor-intensive and mold life is limited. Injection molding begins with a more substantial tool investment but benefits from fast repeatable cycles and lower unit cost once volume rises.
There is no universal break-even quantity. It changes according to part size, geometry, finish, material, cavity count, required tolerances, annual demand, tool steel, inspection level, secondary operations, and shipping destination. A small simple cap may justify injection molding earlier than a large complex housing. Conversely, a complex product with frequent revisions may remain a vacuum-casting candidate longer even when quantities increase.
Cost and Schedule ElementVacuum Casting EffectInjection Molding EffectBuyer ActionInitial toolingLow-cost silicone moldsHigher-cost aluminum or steel moldsMatch tooling investment to design maturity.Per-part costHigher at increasing volumesDeclines significantly at volumeForecast demand over the full product life.Design revision costRelatively manageableCan be substantial after tool completionFreeze critical geometry before production tooling.Initial lead timeTypically fast after master approvalDepends on tool complexity and validationBuild schedule around first article approval.Finishing and assemblyMay require more manual finishingCan be automated or integrated at scaleRequest finished-part pricing, not molded-part pricing alone.Freight and customsSmall urgent lots can move by express airRecurring volume may suit air, rail, or ocean freightPlan packaging and Incoterms before production.Inventory riskLow because batches can be smallHigher if large orders are produced too earlyUse staged releases and demand checkpoints.For the Global market, landed cost planning should account for trade routes and delivery speed. Prototype quantities can often move through air freight from Shenzhen, Guangzhou, Hong Kong, Shanghai, or Ningbo to major international hubs. Larger recurring orders may move through ports such as Yantian, Rotterdam, Hamburg, Long Beach, Los Angeles, Jebel Ali, or Singapore. Packaging must protect cosmetic surfaces, prevent insert damage, and satisfy destination-market labeling or handling requirements.
Both technologies support broad industrial use, but the required validation level differs. Vacuum casting is common in design verification, usability testing, clinical mockups, pre-production marketing, and small-batch field trials. Injection molding is used when parts become a repeatable commercial product or a service replacement component.
A practical product launch path often starts with CAD review, then SLA or CNC master creation, vacuum-cast prototypes, engineering changes, rapid tooling, pilot injection molding, validation, and full production. This staged approach reduces the risk of cutting expensive tooling before designers, engineers, purchasing teams, distributors, and end users have tested the product.
A consumer electronics brand developing a handheld controller needs twenty presentation units for distributor meetings in London, Berlin, New York, and Singapore. The enclosure shape is still evolving, and the team needs multiple colors with a soft-touch grip. Vacuum casting is suitable because the brand can create ABS-like shells and rubber-like grip components quickly, test ergonomics, collect buyer feedback, and revise the CAD without rebuilding a metal mold.
After the design is approved and purchase forecasts indicate 20,000 units, the program can transition to injection molding. The production mold can use PC/ABS for the shell and TPE overmolding for the grip. Molded logos, consistent texture, snap-fit validation, and controlled color matching improve the final commercial product.
A medical equipment developer requires a large equipment housing for usability testing, internal electronics fit checks, and demonstrations at an industry event. Vacuum casting provides a visually accurate housing with controlled paint finish and embedded threaded inserts. This allows the team to validate access panels, screen locations, cable routes, and serviceability before spending on tooling.
Once functional, regulatory, and cleaning requirements are confirmed, injection molding becomes the preferred process for repeatable production. The final material can be selected for chemical resistance, impact strength, flame behavior, and cleaning compatibility. The supplier should define inspection criteria, cosmetic acceptance standards, lot traceability, and packaging protection before the first commercial run.
An industrial distributor needs replacement covers and small protective housings for legacy equipment. Demand is uncertain, ranging from a few units to several dozen per year. Vacuum casting is often the economical answer because the distributor avoids investing in a production mold for low annual quantities. A durable master pattern can be retained, and new silicone molds can be made as needed.
If demand rises across distributor networks in Europe, North America, the Middle East, or Asia-Pacific, the business case can change. A rapid injection mold may then reduce the part cost and improve availability for a growing aftermarket program.
Supplier selection should be based on engineering capability, process fit, communication speed, quality documentation, capacity, tool ownership terms, inspection options, and shipment support. The companies below are established names serving international customers. Buyers should request a project-specific quotation and confirm the exact factory location, material options, certification requirements, capacity, lead time, and commercial terms for their program.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidGlobal customers, including North America, Europe, Asia-Pacific, and customers in more than 25 countriesChina-based integrated rapid manufacturing, DFM support, competitive cost structure, prototype-to-production continuityVacuum casting, CNC machining, 3D printing, rapid tooling, injection molding, die casting, finishing, assembly, packaging, and direct shippingProtolabsNorth America and Europe, with global customer reachDigital quoting, rapid manufacturing workflow, fast turnaround for development programsInjection molding, CNC machining, sheet metal fabrication, and 3D printingXometryNorth America, Europe, and international sourcing networksBroad supplier network, online sourcing tools, multiple manufacturing technologiesInjection molding, CNC machining, 3D printing, sheet metal, urethane casting, and finishingQuickpartsNorth America and global product-development customersPrototype and low-volume production expertise, support for product development teamsVacuum casting, 3D printing, CNC machining, and injection molding servicesFictivNorth America with global manufacturing networkDigital manufacturing management, quality systems, prototype-to-production supportInjection molding, CNC machining, urethane casting, 3D printing, and production sourcingRapidDirectGlobal customers served from ChinaOnline manufacturing platform, rapid quotations, broad prototyping and production capabilityCNC machining, injection molding, rapid tooling, sheet metal, die casting, and finishingFor buyers sourcing internationally, the strongest supplier relationship is built before the purchase order is issued. Ask for a DFM report, mold-flow or manufacturability observations where relevant, material data, tolerance assumptions, first article plan, inspection method, sample approval process, packaging specification, shipping terms, and communication escalation path. A supplier that responds clearly to these questions is more likely to support a stable production program.
TEAM Rapid supports global customers with an integrated route from early prototype to repeat production, combining vacuum casting, SLA and SLS 3D printing, CNC machining, rapid tooling, injection molding, die casting, sheet metal fabrication, finishing, assembly, packaging, procurement support, and direct shipping. Its ISO 9001:2015 quality management certification, experience across more than 6,000 delivered projects, and customer base in more than 25 countries provide practical evidence of controlled manufacturing and international project handling. The company applies detailed DFM analysis to identify issues involving resin flow, wall thickness, mold cavities, cycle time, tolerances, assembly, and potential quality risks before tooling begins. It supports end users, startups, product designers, engineers, distributors, dealers, brand owners, and individual innovators through flexible prototype orders, OEM and ODM manufacturing, wholesale-style repeat supply, regional distribution support, and custom production programs from one part to more than 100,000 parts. While its profile does not claim overseas subsidiaries or local warehouses, TEAM Rapid has established international delivery experience and provides one-to-one online pre-sales engineering communication and after-sales project support, with responses typically available within hours. Its operational model is a turnkey, customer-owned manufacturing route for parts and assemblies, rather than a BOO or on-site bulk-supply arrangement. For buyers needing a practical China-based partner, its combination of in-house machining, tooling capability, molding resources, inspection focus, finishing, packaging, and direct shipment helps reduce supplier fragmentation while protecting schedule, quality expectations, and total project cost.
For early-stage parts, buyers can explore rapid prototyping services to compare 3D printing, CNC machining, and vacuum casting options. When volume and design maturity justify production tooling, the company’s injection molding services provide a pathway into rapid tooling, insert molding, overmolding, and repeatable plastic-part production. For a project-specific material, quantity, and lead-time assessment, request a custom manufacturing quotation.
In 2026, global manufacturing decisions will increasingly be shaped by speed, traceability, localized inventory strategy, automation, material sustainability, and supply-chain risk management. Vacuum casting will remain valuable because it enables short development loops without locking brands into expensive production tooling. As product teams launch more niche products, personalized devices, regional variants, and limited-edition consumer goods, the ability to make small batches quickly will remain commercially important.
Injection molding will continue to evolve through better mold monitoring, automated inspection, simulation-driven tool design, conformal cooling, robotic handling, and greater use of process data. These technologies can reduce scrap, stabilize cycles, improve cavity balance, and help buyers document production consistency. Multi-cavity and family-mold decisions will increasingly be evaluated using real demand data rather than assumptions made at product launch.
Sustainability will become a more concrete purchasing factor. Buyers are expected to ask more often about recycled-content resins, bio-based polymers, mono-material design, recyclability, reduced packaging, energy-efficient molding cycles, and lower transport emissions. However, recycled or bio-based materials should not be selected solely for marketing claims. They must be tested for color consistency, mechanical performance, odor, flow behavior, regulatory compliance, and long-term durability in the final application.
Policy and compliance trends will also influence global sourcing. Product teams may need stronger material declarations, restricted-substance documentation, origin data, packaging compliance, safety information, and supply-chain records. Medical, automotive, electrical, and consumer-product programs may require more formal evidence that a production material and process match the approved design. This favors suppliers that provide early DFM input, structured inspection, clear communication, and documented project control.
For small quantities, vacuum casting is usually cheaper because silicone tooling costs far less than aluminum or steel injection molds. At larger volumes, injection molding usually becomes more economical because the unit cost declines substantially as the mold cost is spread across more parts.
A silicone mold often produces approximately 10 to 25 good parts, depending on geometry, resin, curing conditions, undercuts, finish requirements, and handling. Complex parts or demanding cosmetic surfaces may require replacement molds sooner. A supplier should confirm expected mold life for the specific design.
Yes. Vacuum-cast polyurethane parts are widely used for fit testing, assembly verification, ergonomic evaluation, low-load functional testing, marketing samples, and pilot programs. For critical thermal, chemical, electrical, fatigue, or regulatory testing, use the final injection-molded production resin whenever possible.
Move when the design is stable, material requirements are final, demand is rising, unit cost matters, and repeatability is required. Many projects first use vacuum casting for validation, then rapid injection tooling for pilot production, followed by production tooling for long-term demand.
Yes. Rapid aluminum tooling and lower-cavity molds can support lower-volume injection molding when the project requires a final thermoplastic material. This option is especially useful for pilot production, regulated components, engineering validation, and products that need stronger long-term performance than polyurethane can provide.
Include 3D CAD, drawings for critical dimensions, required quantity, annual forecast, material preference, color, surface finish, tolerances, inserts, assembly requirements, inspection expectations, packaging requirements, shipping destination, and requested delivery date. If the part is replacing an existing component, include photos and functional information.
Yes. An integrated manufacturing partner can support the development path from master pattern and vacuum-cast samples to tooling, molded parts, finishing, assembly, packaging, and shipment. This can reduce handoff errors, shorten communication loops, and make design changes easier to manage.
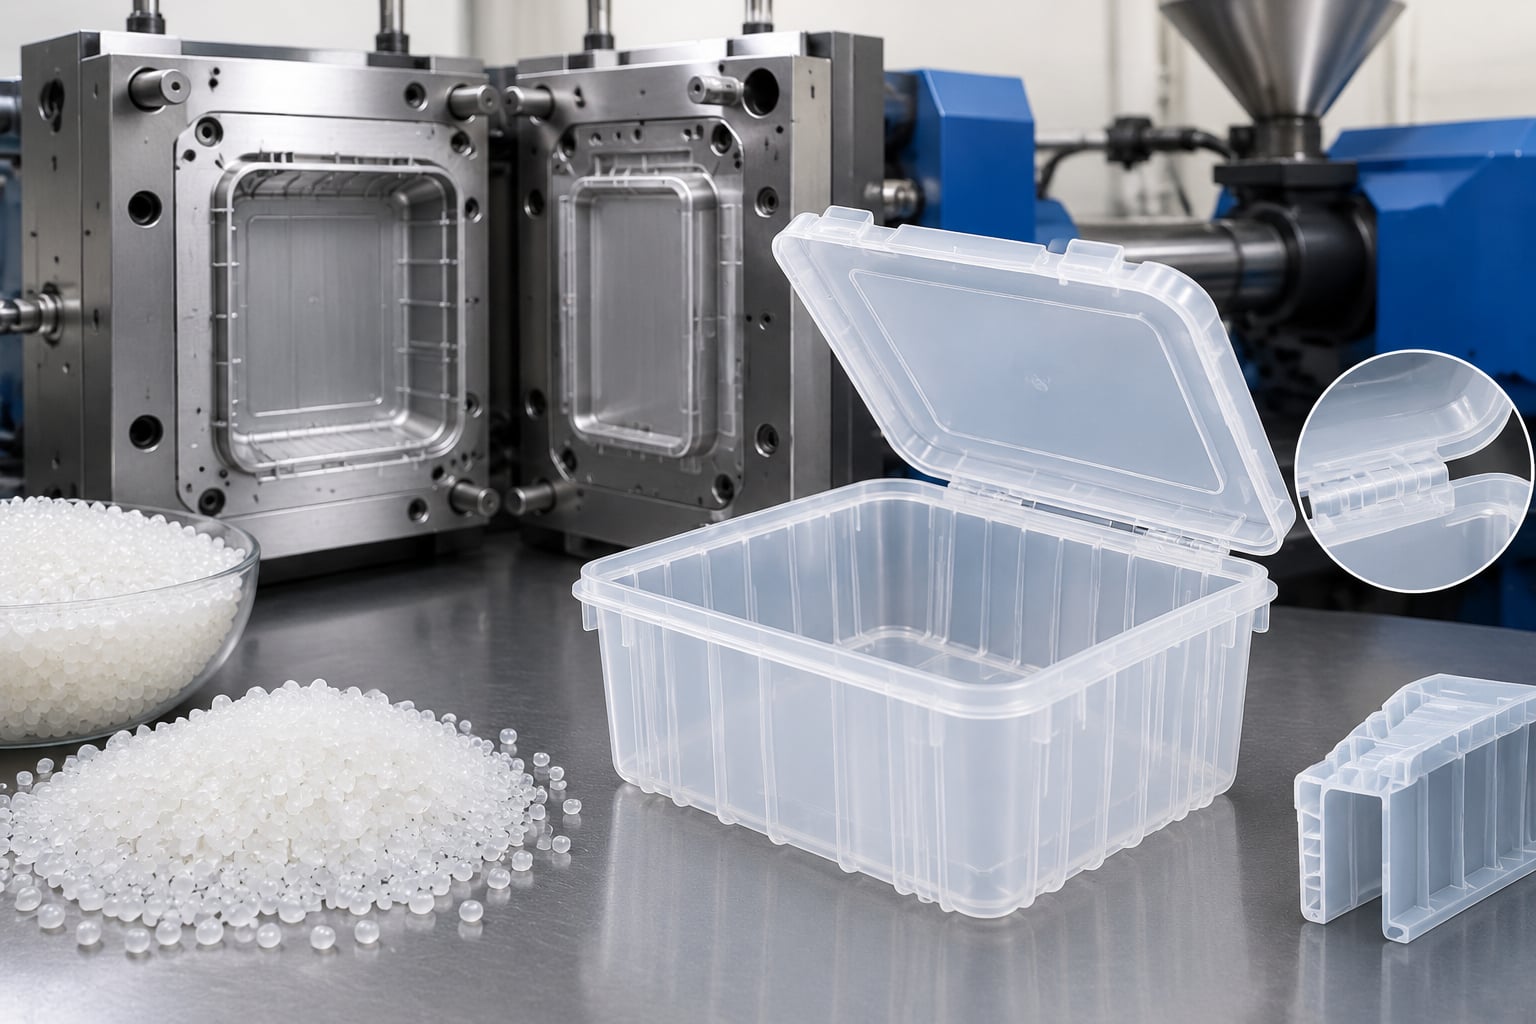
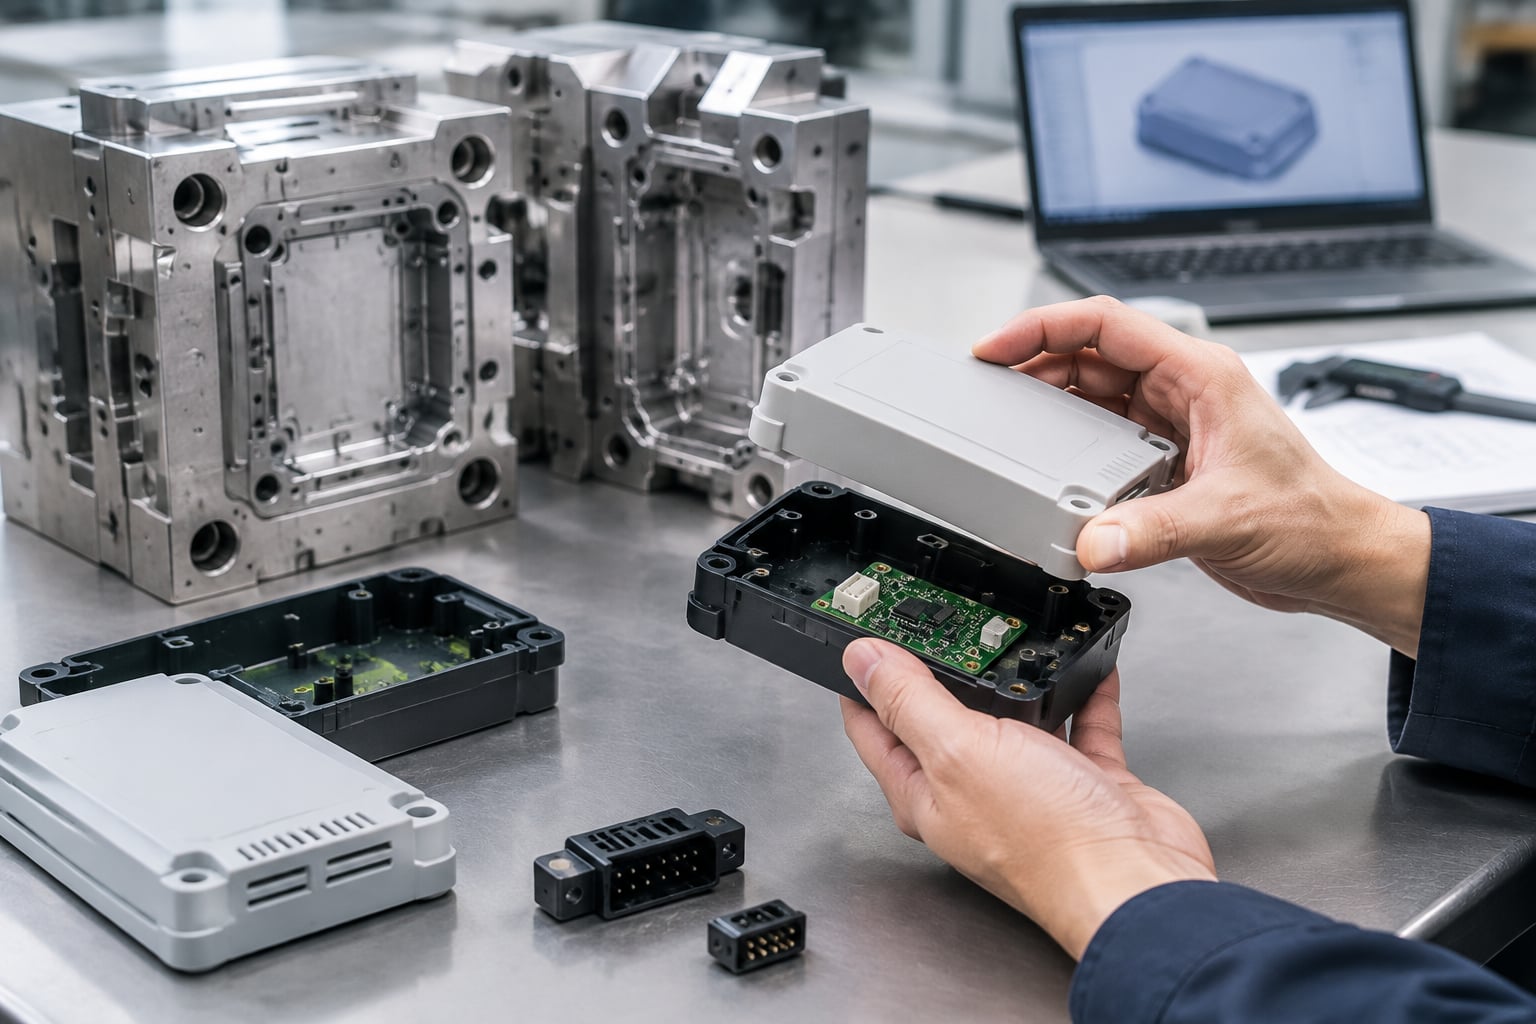
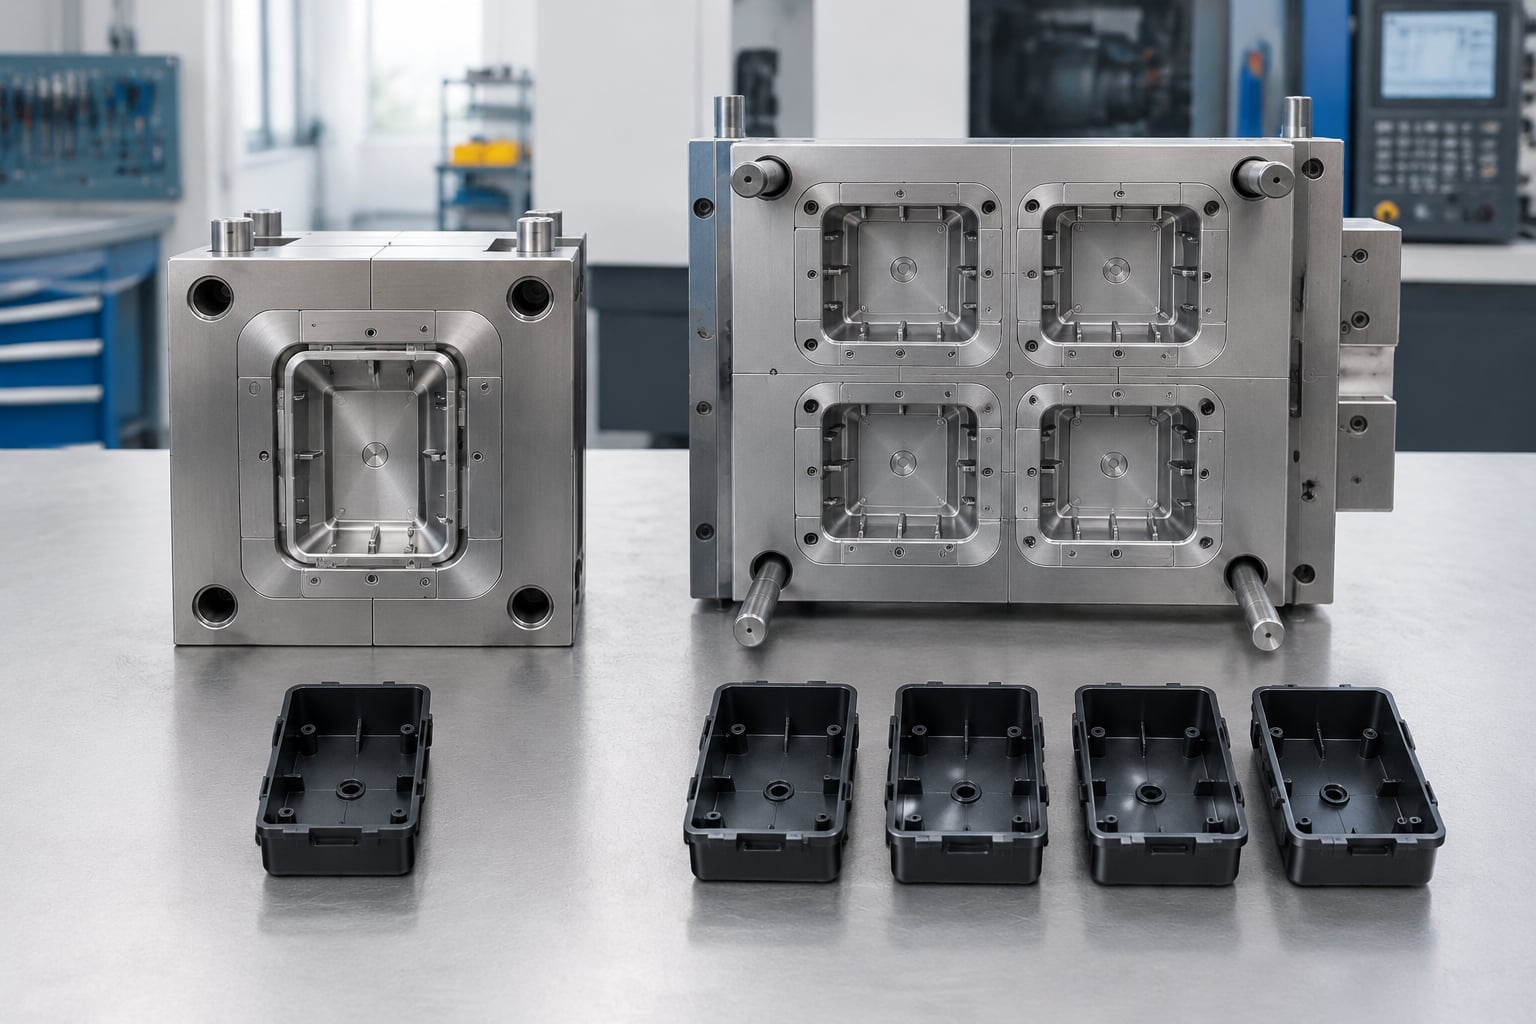
-
Global Market Injection Molding Design Rules for DFM
Effective injection molding design starts with uniform wall thickness, sufficient draft, controlled ribs and bosses, realistic tolerances, correct gate placement, and early DFM review. For Global market programs, designers should validate the part against the selected resin, expected annual volume, cosmetic requirements, assembly method, tooling location, logistics route, and regional compliance needs before cutting steel.
The most practical checklist is simple: keep walls consistent, add draft to every vertical face, avoid sharp internal corners, use ribs instead of thick sections, design undercuts only when function requires them, position gates away from cosmetic surfaces, specify tolerances based on resin behavior, and review mold flow, cooling, ejection, and assembly risks before tool release.
Common international suppliers for injection molding design support include TEAM Rapid, Protolabs, Xometry, Fictiv, ICOMold, and Rosti. Qualified Chinese manufacturing partners can also be strong options for Global market buyers when they provide ISO-certified quality systems, responsive engineering communication, documented DFM feedback, and reliable pre-sales and after-sales support. Their cost-performance advantage is especially relevant for rapid tooling, bridge production, and low-to-medium-volume molded parts.
Injection molding is one of the most scalable methods for producing plastic parts, but it is also unforgiving when product geometry does not match material flow, cooling, ejection, and tooling constraints. A design that appears correct in CAD can create sink marks, warpage, flash, short shots, visible weld lines, excessive cycle times, weak snap fits, or expensive side actions once it enters tool design.
Global market product teams frequently manage additional complexity. A consumer enclosure may be designed in London, validated in Munich, tooled in Shenzhen, assembled in Mexico, and sold through distributors in the United States, Australia, and the Middle East. In this environment, a clear injection molding DFM strategy reduces change orders, prevents communication gaps, and helps ensure that the final molded component is repeatable across production batches.
Trade hubs such as Shenzhen, Dongguan, Ningbo, Hong Kong, Singapore, Rotterdam, Hamburg, Los Angeles, Chicago, and Dubai remain important links in international manufacturing supply chains. Buyers should therefore consider not only tooling price, but also engineering response time, export packaging, inspection documentation, resin sourcing, mold ownership terms, spare-part support, and shipping flexibility.
Uniform walls help molten plastic fill, pack, cool, and shrink more predictably. Sudden changes in thickness create uneven cooling, which can cause sink marks, voids, warpage, and dimensional variation. If a section needs extra strength, use ribs, gussets, corrugation, or localized structural geometry rather than making the whole area thicker.
Typical wall thickness depends on material, flow length, part size, impact requirements, and surface finish. Thin-wall consumer packaging may use less than 1.0 mm, while structural industrial housings may use 2.5 mm or more. The objective is not to use the thinnest possible wall; it is to use a stable and manufacturable wall for the selected resin and molding process.
Draft is the taper that allows a molded part to release from the mold without drag marks, scratches, deformation, or excessive ejection force. Smooth surfaces commonly need at least 0.5° to 1° draft, while textured surfaces often require 2° to 5° or more depending on texture depth. Deep cores, highly polished cosmetic surfaces, elastomeric materials, and aggressive textures may need additional draft.
Designers should identify the mold opening direction early. Every wall, rib, boss, snap feature, and engraved detail should be checked against that direction. When a feature cannot release directly, it may need a side action, lifter, collapsible core, unscrewing mechanism, or redesign.
Sharp corners restrict resin flow and create stress concentration points. Internal corners should generally include a radius, ideally related to the nominal wall thickness. A practical starting point is an inside radius of 0.25 to 0.75 times the wall thickness, followed by an outside radius that maintains consistent material thickness around the corner.
Fillets improve strength, reduce crack initiation, assist material flow, and make it easier to machine mold cavities. They are particularly important in load-bearing brackets, clips, handles, latches, medical housings, automotive components, and electrical enclosures.
Ribs improve stiffness without the cost and cosmetic risks of thick solid walls. As a general guideline, rib thickness should be approximately 40% to 60% of the nominal wall thickness. Thick ribs can produce sink marks on the opposite cosmetic surface. Rib height is often limited to about three times the nominal wall thickness unless flow, cooling, and ejection analysis support a taller feature.
Bosses used for screws, inserts, alignment, or assembly should be supported by ribs or gussets. Avoid connecting a large solid boss directly to an exterior cosmetic wall. The local mass can cause sinks, voids, and distortion. Core out the boss wherever possible and provide sufficient draft on the internal and external surfaces.
Undercuts are features that prevent direct ejection from a simple two-plate mold. Examples include side holes, retaining clips, external threads, internal snap hooks, and recessed grooves. Some flexible undercuts can be stripped manually or automatically, but rigid materials often require side actions or lifters.
Every undercut increases tooling complexity, maintenance requirements, cycle time, and mold cost. It should be retained only if it delivers clear functional, safety, sealing, or assembly value. A small redesign of a snap fit or opening direction can sometimes eliminate an expensive mechanical action.
The following ranges are starting points for early product design. They must be adjusted according to resin grade, mold construction, texture, part size, required tolerance, gate location, flow length, and expected production volume. A DFM review should confirm final values before tooling.
Design FeaturePractical Starting GuidelinePrimary Risk if IgnoredDesign ConsiderationNominal wall thicknessKeep as uniform as possible across the partWarpage, sink marks, voids, short shotsUse ribs or gussets for strength instead of heavy sectionsDraft angle0.5° to 1° for smooth faces; more for textureDrag marks, part damage, high ejection forceIncrease draft for deep walls and textured surfacesRib thickness40% to 60% of nominal wall thicknessVisible sink marks and uneven coolingRound rib bases and maintain draft on both rib facesRib heightPreferably no more than three times wall thicknessFill difficulty, ejection problems, warpUse multiple shorter ribs where possibleBoss wall thicknessAbout 60% of nominal wall thicknessSinks, voids, cracking around screwsCore out bosses and connect them with gussetsInternal corner radius0.25 to 0.75 times nominal wall thicknessStress concentration and poor material flowMaintain consistent thickness through the cornerHole diameterPrefer diameter equal to or larger than wall thicknessCore pin deflection, incomplete fillSupport long core pins where feasibleTextured surfacesUse additional draft based on texture depthScuffing and difficult ejectionConfirm texture supplier requirements earlyThese guidelines reduce risk, but do not replace engineering analysis. Glass-filled materials, flame-retardant grades, soft elastomers, high-temperature polymers, recycled-content resins, and highly polished cosmetic parts can require substantially different geometry decisions.
Material selection affects almost every injection molding decision. Shrink rate influences mold dimensions. Melt flow influences gate size and wall-thickness capability. Glass fiber content affects stiffness but can increase warpage and surface visibility. UV exposure, chemicals, electrical requirements, impact loads, heat, food contact, medical regulations, and flame resistance must all be evaluated before finalizing the resin.
Material FamilyCommon AdvantagesTypical ApplicationsImportant DFM ConsiderationABSGood appearance, impact resistance, easy processingConsumer housings, electronics, appliance coversModerate shrinkage; avoid overly thick cosmetic wallsPolypropyleneChemical resistance, living hinge performance, low densityContainers, caps, medical trays, household productsHigher shrinkage requires tolerance planningPolycarbonateHigh impact strength and transparency optionsSafety covers, lenses, electrical enclosuresNeeds careful drying and controlled processingPA NylonStrength, wear resistance, fatigue performanceGears, clips, automotive parts, industrial componentsMoisture absorption affects dimensions and propertiesPOM AcetalLow friction, stiffness, good dimensional stabilityPrecision mechanisms, latches, gears, valvesDesign for shrinkage and avoid unsuitable chemical combinationsPC/ABSBalanced toughness, heat resistance, cosmetic qualityAutomotive interiors, equipment housings, devicesUseful for larger housings needing better impact performanceTPUElasticity, abrasion resistance, soft-touch feelProtective covers, grips, seals, wearable productsGate and ejector design must prevent distortionGlass-filled polymersHigh stiffness and strengthStructural brackets, industrial parts, automotive componentsFiber orientation can cause directional warpageFor international programs, material sourcing should be controlled by approved resin grades rather than only generic names. “ABS” is not a full specification. The grade, color masterbatch, recycled-content target, flame-retardant classification, supplier documentation, and testing requirements should be defined in the product specification.
Gate location influences filling pattern, weld lines, packing pressure, cosmetic appearance, fiber orientation, and warpage. Gates should be placed where the thickest section can be packed effectively and where any vestige can be hidden or removed safely. For a visible consumer product, a gate may be placed on an internal face, underside, assembly flange, or non-cosmetic edge.
Weld lines occur when two flow fronts meet. They may be harmless in a low-stress cover, but critical in a pressure-containing part, structural clip, hinge, or screw boss. Designers should avoid placing holes, windows, or high-stress features where weld lines are likely to occur.
Cooling is equally important. Thick local masses cool slowly and can extend cycle time or produce sinks and internal voids. Mold designers use water channels, baffles, bubblers, conformal cooling, and specialized inserts to manage heat. Product designers can support efficient cooling by avoiding unnecessary heavy sections and by providing accessible core geometry.
Ejector pins, sleeves, stripper plates, and air ejection systems leave marks or require contact surfaces. Designers should identify acceptable ejector locations before finalizing the cosmetic Class A surface. The most attractive design can become costly if no suitable ejection area exists.
Product TypeTypical Design PrioritiesFrequent Molding RiskRecommended Engineering FocusElectronic enclosureCosmetic surfaces, screw bosses, EMI features, assembly fitSinks around bosses and visible gate marksWall uniformity, hidden gates, controlled texture and draftAutomotive interior trimAppearance, clip retention, heat resistance, durabilityWarp, scratch sensitivity, clip failureMaterial validation, grain texture draft, rib layoutMedical device housingCleanability, dimensional control, traceabilityStress cracking and difficult assemblyApproved materials, radiused corners, functional testingIndustrial equipment coverImpact resistance, rigidity, environmental resistanceLarge-part warp and inconsistent fitRib strategy, gate balance, reinforced materialsConsumer packaging componentLow cost, high volume, visual consistencyThin-wall short shots and flashFlow length review, high-cavitation tool designSnap-fit assemblyRepeatable retention, easy assembly, fatigue resistanceStress whitening and breakageStrain analysis, material selection, rounded transitionsInsert molded componentMetal-plastic bond, insert position, electrical reliabilityInsert movement and crackingInsert retention, preheating, locator designOvermolded gripSoft feel, adhesion, ergonomicsDelamination and flash at interfaceMechanical locks, compatible materials, sealing surfacesEach product category requires its own acceptance criteria. A matte black appliance cover may prioritize appearance and scratch resistance, while an internal medical bracket may prioritize dimensional stability, material traceability, and sterilization compatibility. Product teams should state these priorities before DFM begins.
Before requesting quotes, prepare a 3D CAD file, 2D drawing where critical dimensions exist, annual volume forecast, selected or preferred material, color, texture, finish, assembly details, functional requirements, and destination market. If the design is still evolving, explain which dimensions are fixed and which can change after DFM review.
Buyers should ask whether the quoted tool is prototype tooling, bridge tooling, or production tooling. Aluminum rapid tooling may be suitable for market validation and low-volume production, while hardened steel tooling is generally better for high-volume programs, abrasive glass-filled resins, or long-term repeatability. Tool life should be stated as an expected range, not assumed.
Clarify mold ownership, storage period, maintenance responsibilities, cavity count, engineering change charges, sample approval process, inspection method, packaging method, and delivery terms. For global distribution, also confirm whether the supplier can support assembly, kitting, labeling, warehousing, and direct shipping to regional fulfillment locations.
The supplier landscape includes regional specialists, digital manufacturing platforms, high-volume molders, and China-based rapid manufacturing partners. The table below provides practical examples. Buyers should verify current capability, certifications, material availability, and commercial terms for each project.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidGlobal customers, including the USA, UK, France, Germany, and AsiaRapid tooling, DFM support, low-volume and production flexibilityInjection molding, insert molding, overmolding, CNC machining, vacuum casting, assemblyProtolabsNorth America and EuropeFast digital quoting and rapid manufacturing workflowsInjection molding, CNC machining, 3D printing, sheet metal fabricationXometryNorth America, Europe, and international sourcing networksBroad supplier network and online manufacturing procurementInjection molding, CNC machining, fabrication, production sourcingFictivNorth America and global supply partnersDigital manufacturing management and engineering coordinationInjection molding, CNC machining, urethane casting, finishingICOMoldNorth America with international manufacturing supportCustom plastic injection molding and mold manufacturingPrototype molds, production molds, insert molding, overmoldingRostiEurope, Asia, and North AmericaHigh-quality contract manufacturing for complex productsInjection molding, assembly, medical and consumer product manufacturingNypro, a Jabil CompanyGlobal manufacturing locationsLarge-scale healthcare and consumer manufacturing capabilityPrecision molding, automation, assembly, medical device manufacturingHusky TechnologiesGlobal, with strong packaging industry presenceHigh-volume molding systems and hot runner technologyPackaging molds, hot runners, injection molding equipment solutionsFor projects requiring rapid iterations, buyers often benefit from a supplier that can machine prototype parts, revise tooling, mold pilot batches, apply finishing, and ship assembled products without transferring data between multiple vendors. For established high-volume programs, a dedicated regional molder may provide advantages in local logistics, automation, and long-term production support.
TEAM Rapid supports innovators, product designers, engineers, startups, distributors, brand owners, and established manufacturers with a connected route from prototype to repeat production. Its ISO 9001:2015 quality management system, in-house machining and tooling capability, documented DFM feedback, and precision machining capability down to 0.01 mm provide practical evidence for controlled manufacturing of custom plastic and metal components. Rather than relying on unspecified component brands, TEAM Rapid works from customer-approved material grades, defined resin requirements, inspection criteria, and functional specifications, supporting parts such as enclosures, housings, trays, covers, fillers, insert-molded components, and overmolded assemblies. Customers can use flexible OEM and ODM cooperation, wholesale supply, prototype orders, recurring production, distributor programs, and direct-to-brand fulfillment, from one prototype to more than 100,000 parts. The company has established delivery experience with customers in more than 25 countries, including the USA, UK, France, Germany, and other international markets, supported by one-to-one engineering communication, responses commonly provided within a few hours, packaging, assembly, procurement support, limited warehousing, and direct shipping. Although its manufacturing base and integrated supply network are in China rather than represented as overseas subsidiaries or local warehouses, its export operating experience and online engineering support provide a practical service structure for international buyers who need clear pre-sales review, production updates, inspection coordination, and after-sales issue resolution. TEAM Rapid provides EPC-style turnkey and customer-owned production solutions for manufacturing projects, not BOO or on-site bulk supply services.
For early-stage projects, customers can explore TEAM Rapid injection molding services to compare rapid tooling, prototype molding, and production options. When a design is ready for review, a custom manufacturing quotation request can include CAD files, material preferences, volumes, finish requirements, and delivery destination.
A handheld diagnostic device housing may need PC/ABS for impact strength and dimensional stability. The design should include draft on textured grip zones, controlled ribs behind display openings, isolated screw bosses, and enough internal clearance for PCB installation. Gate placement should avoid the front cosmetic face, while ejector locations should be hidden inside assembly surfaces.
An automotive under-hood clip may require heat-resistant nylon with glass reinforcement. In this case, fiber orientation and moisture conditioning are important. The designer should avoid abrupt thickness transitions, place fillets at clip roots, and evaluate the part under repeated insertion and removal cycles. A low-cost tool that ignores fiber-related warpage can create fit problems later in vehicle assembly.
A consumer storage container with a living hinge may use polypropylene. The hinge must be thin and carefully oriented to support repeated flexing, while the body should retain a stable wall thickness. Gate position and flow direction can influence hinge performance. A prototype run should verify opening force, fatigue life, lid alignment, and sealing behavior.
An industrial control-box cover may require flame-retardant ABS or PC/ABS. Designers must account for the material’s flow behavior, flame-retardant additive effects, electrical clearance requirements, screw boss strength, gasket compression, and exterior finish. Venting and gate placement should be reviewed to reduce burn marks around deep ribs and internal features.
By 2026, injection molding design is increasingly shaped by automated DFM, artificial intelligence-assisted mold-flow prediction, digital traceability, material data management, and more sustainable resin strategies. CAD platforms and supplier quoting systems are becoming better at identifying missing draft, thick wall sections, undercuts, and high-risk tolerances before engineers issue a tooling purchase order.
Sustainability will continue to influence material selection. Recycled-content polymers, bio-based materials, mono-material design, lightweighting, and easier disassembly are becoming more important in consumer goods, packaging, mobility products, and electrical equipment. However, recycled-content resin can introduce variation in color, mechanical properties, flow, and shrinkage, so qualification testing and approved-source control are essential.
Policy requirements are also evolving across major markets. Product teams should monitor chemical restrictions, packaging rules, recyclability targets, extended producer responsibility requirements, medical device documentation, electrical safety standards, and regional labeling obligations. The mold design itself may not be regulated, but material selection, traceability, product safety, and end-of-life expectations increasingly affect molded-part decisions.
Manufacturers are also adopting conformal cooling, in-mold sensors, automated visual inspection, robotic part handling, and digital process monitoring. These technologies can improve consistency, reduce cycle time, and provide better production data, particularly for high-value medical, automotive, industrial, and electronics applications.
Maintain consistent wall thickness. It has a direct effect on filling, cooling, shrinkage, warpage, sink marks, cycle time, and part quality.
A common starting point is 0.5° to 1° for smooth surfaces. Textured, deep, polished, or difficult-to-eject surfaces often require more draft.
They can, but sharp internal corners are generally discouraged because they create stress concentrations and restrict resin flow. Use fillets whenever function permits.
Side actions are commonly needed for rigid undercuts, side holes, external snap features, recessed grooves, and geometry that cannot release in the mold opening direction.
Send 3D CAD files, critical drawings, material preferences, finish requirements, color, annual volume, target delivery date, destination, assembly needs, and known functional requirements.
Yes. Rapid tooling can be suitable for prototype validation, bridge production, market testing, and selected low-volume production. The correct choice depends on resin, cavity count, part complexity, surface finish, and expected production quantity.
Reduce thick local masses, use ribs instead of heavy walls, core out bosses, improve wall uniformity, and review gate location and packing conditions with the molding engineer.
Early DFM identifies risks while geometry can still be changed quickly. It is far less expensive to revise CAD than to modify hardened steel after the mold has been manufactured.
-
Injection Mold Upkeep for the Global Market: Tool Life
Effective injection mold maintenance protects dimensional accuracy, reduces unplanned downtime, prevents flash and cosmetic defects, and extends the productive life of a mold. The most practical approach is to clean molding surfaces after every production run, inspect high-wear components regularly, lubricate approved moving areas, control moisture during storage, document each intervention, and schedule preventive maintenance based on shot count and part quality trends.
For buyers in the Global market, leading mold and injection molding support providers include TEAM Rapid in China, Husky Technologies in Canada, ENGEL in Austria, ARBURG in Germany, Milacron in the United States, and Sumitomo (SHI) Demag in Germany. Qualified international suppliers, including Chinese tooling companies with ISO-certified quality systems, responsive engineering support, and strong pre-sales and after-sales communication, can also be a practical option because of their cost-performance advantages.
Injection molds are precision production assets. A mold may contain hardened steel cavities, interchangeable inserts, cooling circuits, hot runner components, ejector systems, slides, lifters, hydraulic cylinders, sensors, guide pillars, wear plates, and precision shutoff surfaces. Each feature must operate repeatedly under pressure, heat, friction, resin flow, and mechanical movement. Without planned mold upkeep, small problems can become major tooling failures.
Across global manufacturing centers such as Shenzhen, Dongguan, Ningbo, Shanghai, Singapore, Munich, Stuttgart, Chicago, Toronto, Monterrey, Rotterdam, Dubai, and London, buyers increasingly expect stable quality from multi-cavity tools and short production lead times. Mold failures affect more than maintenance costs. They may delay assembly, disrupt packaging schedules, increase rejected parts, interrupt container loading at ports, and create missed retail or product-launch deadlines.
Regular injection mold maintenance helps manufacturers control the most common production risks: poor cooling performance, burn marks caused by blocked vents, flash caused by damaged shutoffs, dimensional drift from worn inserts, short shots from gate restrictions, scratches caused by ejector damage, and corrosion caused by moisture or aggressive resin additives. A documented maintenance plan is therefore not simply a workshop procedure; it is a quality and supply-chain protection system.
Mold maintenance should be divided by timing, production volume, part quality requirements, resin type, and mold complexity. A simple prototype tool running polypropylene has different maintenance needs from a high-cavity production mold processing glass-filled nylon, flame-retardant ABS, PVC, POM, or engineering-grade polycarbonate.
Maintenance TypeTypical TriggerMain TasksBusiness BenefitStart-up inspectionBefore each production runCheck water connections, clamps, ejector movement, sensors, fasteners, and visible damageReduces start-up defects and avoids running a damaged toolDaily careEach shift or campaignRemove resin residue, inspect vents, wipe molding surfaces, review part qualityMaintains cosmetic quality and stable fillingPreventive maintenanceBased on shot countClean cooling lines, replace seals, check wear plates, lubricate moving componentsPrevents unexpected production stopsCorrective maintenanceAfter a defect or breakdownRepair inserts, weld damage, polish cavities, replace ejector pins or hot runner partsRestores functional performanceSeasonal storage maintenanceBefore long-term storageDry circuits, apply corrosion protection, pack components, label mold conditionProtects the tool during idle periodsEngineering improvementRecurring defect trendsModify venting, cooling, gate geometry, ejection, or material flow pathsImproves long-term manufacturabilityThe table shows that mold maintenance is not limited to emergency repair. Start-up checks protect production readiness, routine cleaning protects surface quality, preventive work protects long-term tool life, and engineering changes address repeated process weaknesses that cannot be solved through cleaning alone.
A practical checklist should be specific enough for technicians to follow consistently while allowing the maintenance team to record mold condition. The best checklist is linked to a mold identification number, part number, resin, shot count, production machine, date, operator, maintenance technician, and next planned service interval.
Mold AreaInspection PointRecommended ActionWarning SignCavity and coreScratches, deposits, corrosion, polishing conditionClean with approved materials and polish only when necessaryGloss variation, drag marks, visible blemishesParting lineDamage, burrs, resin buildup, mismatchRemove residue and inspect shutoff surfaces carefullyFlash around the molded partVentsBlocked vents and contaminationClean vents without enlarging critical dimensionsBurn marks, short shots, trapped airEjector systemPin movement, return pins, plates, wearClean, lubricate approved locations, replace damaged pinsWhite marks, ejector impressions, stuck partsCooling systemFlow rate, leaks, scale, corrosion, connectorsFlush channels and replace worn seals or fittingsLonger cycle time, uneven shrinkage, warpageSlides and liftersGalling, friction, alignment, wear platesClean and apply suitable high-pressure lubricantNoise, scoring, sticking, dimensional variationHot runner systemHeater, thermocouple, nozzle tip, wiringVerify temperature response and inspect leakage pointsStringing, drooling, uneven fill, resin degradationFasteners and clampsLoose bolts, damaged threads, lifting pointsTorque-check where required and replace damaged hardwareMisalignment, mold movement, safety riskThis checklist is most effective when mold condition is linked to molded-part inspection data. For example, recurring flash on one cavity should trigger inspection of that cavity insert, shutoff surface, parting line, clamping condition, and process pressure. Repeated short shots should lead to checks of gate restrictions, venting, hot runner temperatures, material drying, and cooling balance rather than random machine adjustment.
Cleaning methods must match the mold steel, surface finish, resin type, and contamination level. Mirror-polished cavities require more careful handling than textured surfaces. Abrasive tools should not be used on critical molding surfaces unless approved by experienced tooling personnel. Improper polishing can alter geometry, damage texture, create mismatched cavity surfaces, and increase flash risk.
For standard cleaning, technicians commonly use lint-free cloths, approved mold cleaners, compressed dry air, soft non-metallic brushes, and appropriate cleaning tools for vents and channels. When handling electrical components, hot runners, sensors, or thermocouples, power isolation and electrical safety procedures must be followed. Cooling channels may require chemical descaling or mechanical flushing, but the selected method must be compatible with mold steel, seals, and water-system materials.
Lubrication should be controlled rather than excessive. Too much lubricant can migrate into cavities, contaminate molded parts, collect dust, and produce cosmetic defects. Use a lubricant suitable for guide pins, slideways, lifters, ejector systems, and high-load wear surfaces. Avoid applying lubricants directly to cavity surfaces unless the mold supplier specifically recommends a corrosion-protection product for storage.
For storage, the mold should be cleaned, dried, closed or protected as appropriate, labeled with its latest shot count and condition, and stored in a stable environment. Water circuits must not retain moisture when a mold will remain idle for an extended period. In humid coastal regions near ports such as Shenzhen, Ningbo, Hamburg, Rotterdam, Houston, or Singapore, corrosion prevention is especially important due to high humidity and salt-laden air exposure.
When selecting a maintenance provider, buyers should assess more than hourly repair rates. A low repair price can become expensive if the supplier cannot diagnose root causes, lacks precision machining capability, uses unsuitable replacement components, or fails to document tool changes. The preferred partner should understand mold design, resin behavior, injection molding parameters, metallurgy, dimensional inspection, and production scheduling.
Evaluation FactorWhat Buyers Should AskWhy It MattersPractical EvidenceTooling experienceCan the supplier repair cavities, cores, slides, and ejector systems?Complex repairs require specialized mold knowledgeExamples of similar tooling repairs and DFM reportsMachining capabilityAre CNC, EDM, wire EDM, grinding, and polishing available?Precision replacement parts must match the moldIn-house equipment list and tolerance capabilityQuality systemDoes the provider operate under a recognized quality framework?Maintenance records and inspections must be reliableISO 9001 certification and documented inspection processSpare part managementCan wear components be made or sourced quickly?Delays often come from unavailable inserts or ejectorsSpare-part list, lead-time plan, component drawingsEngineering supportCan the supplier identify design-related causes of defects?Repeated failures may need redesign rather than repairRoot-cause reports and process recommendationsGlobal communicationHow quickly are quotations, reports, and updates provided?International projects require fast decisionsNamed engineer, response procedure, digital reportingBuyers should also clarify ownership of mold drawings, spare inserts, maintenance records, and tool modifications. For contract manufacturing projects, the agreement should specify whether the tool remains at the factory, whether customers can request transfer, how storage is charged, and what condition documentation is required before shipment.
For projects requiring new tooling or replacement mold components, it is useful to request rapid tooling services that combine manufacturability analysis, precision machining, trial molding, and production support. This reduces the risk of treating each repair as an isolated event.
Injection mold maintenance is essential in industries where parts must meet repeatable visual, dimensional, safety, or functional requirements. Medical device housings may need clean cosmetic surfaces and controlled material traceability. Automotive interior and under-hood components require dependable fit, thermal resistance, and stable dimensional performance. Consumer electronics cases and enclosures demand consistent texture, snap-fit accuracy, logo details, and assembly alignment.
Other important applications include communication products, office equipment, electrical appliances, sanitary products, industrial controls, packaging components, food-contact products, laboratory devices, appliance covers, trays, caps, connectors, clips, fittings, and overmolded assemblies. In each sector, the maintenance interval should reflect the consequences of defect escape. A small scratch on a hidden industrial bracket may be acceptable, while a minor surface mark on a premium consumer product may result in full batch rejection.
Some mold features wear faster than others. Thin shutoffs, deep ribs, narrow vents, side actions, textured surfaces, hot runner gates, fine ejector pins, threaded unscrewing cores, and optical-grade polishing require closer inspection. Glass-filled polymers and mineral-filled materials can increase abrasion. Flame-retardant compounds may leave deposits. PVC and some additives can create corrosive conditions if processing and cleaning are not properly controlled.
ApplicationHigh-Risk Mold FeatureMaintenance FocusTypical Defect if NeglectedElectronic enclosuresTextured cavity and snap-fit detailsProtect texture and inspect precision clipsScratches, poor assembly fit, cosmetic defectsAutomotive partsLarge slides and complex shutoffsMonitor alignment, wear plates, and cooling balanceFlash, warpage, part mismatchMedical housingsPolished cavities and fine ventsPrevent contamination and maintain surface finishSurface marks, burn marks, rejected partsPackaging closuresHigh-cavity core and gate areasTrack cavity balance and replace worn componentsLeakage, short shots, inconsistent threadsOvermolded componentsInsert location featuresCheck insert seating and shutoff contactMisalignment, resin leakage, weak bondingIndustrial connectorsSmall pins and detailed core insertsInspect for pin damage and blocked ventsBroken features, incomplete fillingThe table demonstrates why maintenance schedules should not be based only on elapsed calendar time. A high-cavity cap mold operating continuously may need more frequent care than a lower-volume tool used occasionally. Likewise, a mold processing abrasive glass-filled nylon should be inspected more often than one molding unfilled polypropylene.
A multi-cavity housing mold began showing longer cycle times and uneven part warpage. The production team initially adjusted packing pressure and cooling time, but the problem continued. A maintenance inspection found mineral buildup in several cooling channels, reducing water flow and creating uneven mold temperatures. After flushing the channels, replacing worn water fittings, and verifying flow balance, the cycle time stabilized and warpage was reduced. The lesson is that cooling maintenance should be measured through flow and temperature performance, not visual inspection alone.
An automotive trim component developed recurring flash near a side-action feature. The mold was repeatedly cleaned, but the flash returned. A detailed inspection found wear on the slide shutoff and insufficient support from a worn wear plate. The maintenance team repaired the shutoff surface, replaced the wear plate, checked slide alignment, and reviewed clamping and injection-pressure settings. The improvement showed that persistent flash often has a mechanical root cause rather than a simple cleaning issue.
An industrial enclosure with deep ribs experienced burn marks near the end of fill. The molding machine was operating within the normal process window, but venting areas had accumulated residue. The maintenance procedure included vent cleaning, checking vent depth, confirming resin drying, and reviewing fill speed. Once air evacuation improved, the burn marks were removed without changing the part design. This case highlights the importance of maintaining venting features, particularly in deep, thin, or complex flow regions.
The following companies are recognized across major manufacturing regions for injection molding equipment, tooling, mold engineering, production support, or rapid manufacturing services. Buyers should verify local service availability, scope of work, equipment compatibility, lead time, and regional commercial terms before placing an order.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidChina, North America, Europe, United Kingdom, France, Germany, and global export marketsRapid tooling, CNC machining, injection molding, DFM review, low-volume and volume productionMold making, maintenance support, replacement components, prototyping, custom injection molded partsHusky TechnologiesNorth America, Europe, Asia-Pacific, Latin America, global packaging marketsHigh-performance injection molding systems and packaging expertiseHot runners, molds, systems support, service programs, PET and closure manufacturing solutionsENGELEurope, Americas, Asia, global industrial molding marketsInjection molding machines, automation, process support, digital production toolsMachine service, automation integration, process optimization, molding technology supportARBURGGermany, Europe, North America, Asia and worldwide service locationsPrecision injection molding machinery and application engineeringMachine support, training, automation, process technologies, production optimizationMilacronUnited States, Canada, Mexico, Europe, Asia-PacificInjection molding equipment, hot runner technology, mold components and serviceMachine service, hot runners, temperature control, parts, process supportSumitomo (SHI) DemagEurope, North America, Asia-Pacific, global manufacturing networksAll-electric injection molding technology and process reliabilityMachine support, application engineering, spare parts, service and trainingThis supplier comparison is intended as a practical starting point. Equipment manufacturers may focus primarily on machine, hot runner, automation, or process support, while tooling manufacturers can provide cavity repair, insert replacement, polishing, machining, mold modification, and trial production. For global buyers, the best outcome often comes from coordinating the mold maker, molding factory, and machine or hot-runner specialist rather than relying on one party for every task.
TEAM Rapid supports customers from prototype development through repeatable injection molding production, with more than 10 years of industry experience, ISO 9001:2015 quality management, over 500 customers served in more than 25 countries, and more than 6,000 delivered projects. Its practical product strength comes from combining in-house CNC machining, EDM, wire EDM, polishing, tooling manufacture, injection molding capability, DFM analysis, inspection processes, and diversified plastic and metal material options; specific branded mold components are selected according to project requirements rather than promoted as a fixed component brand list. The company works with end users, product designers, distributors, dealers, brand owners, startups, established manufacturers, and individual innovators through flexible OEM, ODM, prototype, low-volume, recurring production, assembly, packaging, and direct-shipping models. TEAM Rapid does not offer BOO or on-site bulk supply services; instead, it provides customer-owned tooling, turnkey manufacturing, and customer-owned plant solution support where applicable. While the company profile does not claim overseas subsidiaries or local warehouses, TEAM Rapid has established export experience serving customers in the USA, UK, France, Germany, China, and other markets through direct project communication, engineering response within a few hours, manufacturing coordination, inspection support, packaging, and shipment management. This provides global buyers with documented engineering support before production and responsive online pre-sale and after-sale communication throughout the tooling and molding lifecycle.
For mold owners who need a maintenance review, replacement insert, production repair, or new rapid tool, TEAM Rapid can assess mold design risks through DFM feedback before machining begins. The company supports projects from one prototype to more than 100,000 parts, making it suitable for product launches, engineering validation, bridge production, replacement tooling, and scalable manufacturing programs. Buyers can submit drawings, CAD files, resin requirements, annual volume estimates, target finish, and existing mold-condition photos through the global manufacturing quotation request process.
By 2026, injection mold maintenance will increasingly move from calendar-based servicing toward data-supported predictive maintenance. Mold sensors, cavity pressure monitoring, cooling-flow monitoring, machine data capture, shot-count tracking, and digital maintenance records will help factories identify failure patterns earlier. Rather than waiting for flash, warpage, or a broken ejector pin, maintenance teams will use production data to plan service before quality declines.
Artificial intelligence-assisted process monitoring is expected to improve defect pattern recognition. Systems may compare cycle time, pressure curves, mold temperature, material moisture, ejection force, and cavity performance to identify abnormal trends. Digital mold passports will also become more common, particularly for global supply chains where tools may be moved between production sites. These records can include steel specifications, spare-part drawings, modification history, maintenance intervals, validation results, and approved process windows.
Sustainability will also influence tooling decisions. Better cooling design can reduce cycle time and energy use. Preventive care lowers scrap rates, extends mold life, and reduces the need for premature tool replacement. Manufacturers are also likely to increase attention to water treatment, closed-loop cooling systems, resin recovery, lower-emission production, and material traceability. International regulations affecting packaging, recycled content, medical traceability, product safety, and environmental reporting will make documented production and maintenance records increasingly valuable.
The frequency depends on mold complexity, resin type, surface finish, number of cavities, production hours, and shot count. Basic cleaning should occur after each production run, while preventive maintenance may be scheduled every defined number of cycles. High-wear molds processing glass-filled, mineral-filled, flame-retardant, or corrosive materials usually need more frequent inspection.
Flash can result from damaged parting lines, worn shutoff surfaces, poor slide alignment, excessive injection pressure, inadequate clamping force, mold mismatch, contaminated mating surfaces, or damaged inserts. The correct solution requires inspection of both mold condition and molding parameters.
Yes. Restricted cooling flow can increase cycle time, create uneven cooling, cause warpage, change shrinkage, and produce inconsistent dimensions. Cooling systems should be checked for flow, leaks, mineral scale, corrosion, and blocked channels.
Lubrication should follow the mold maker’s recommendations and should be applied only to approved moving components. Excessive lubricant can contaminate cavity surfaces, attract debris, and affect cosmetic part quality. Clean before applying new lubricant.
Molds should be cleaned, dried, protected against corrosion where necessary, labeled with status information, and stored in a stable environment. Cooling circuits should be drained or dried for long storage periods. In humid environments, corrosion prevention is particularly important.
Often yes. Existing molds can sometimes be improved through cavity insert replacement, vent modification, cooling upgrades, gate adjustments, slide repair, hot runner servicing, polishing, or ejection-system changes. A tooling engineer should evaluate whether the base mold structure remains sound before investing in modifications.
Maintain the mold ID, shot count, resin processed, production dates, defect history, maintenance actions, replaced parts, photographs, inspection results, repair drawings, technician name, and next recommended service interval. These records make root-cause analysis faster and support consistent quality across different production locations.
-
SPI Mold Classifications Guide for Global Market Buyers
SPI mold classifications describe the expected service life, construction quality, maintenance standard, and production suitability of an injection mold. Class 101 is the highest-duty category for very large production volumes, while Class 102 suits medium-to-high production, Class 103 is a general-purpose production mold, Class 104 is intended for low-volume production, and Class 105 is normally a prototype or sample mold.
For global buyers, the practical choice is usually Class 103 for regular commercial production, Class 104 for limited launches or market testing, Class 101 or Class 102 for long-running programs, and Class 105 for early design validation. The classification is a planning guide rather than a substitute for a detailed tooling specification covering steel, cavities, cycle time, cooling, tolerances, maintenance, and acceptance testing.
Qualified international suppliers, including experienced Chinese mold and molding companies with ISO certification, documented inspection, export experience, and responsive pre-sales and after-sales support, can also be considered. Their cost-performance advantage may be significant when engineering review, tooling manufacture, molded parts, finishing, assembly, and delivery are coordinated under one program.
The Society of the Plastics Industry, now known as the Plastics Industry Association, developed a widely used mold classification system to help buyers match tooling investment with expected production demand. The classes are commonly referenced by mold makers, injection molders, product developers, and procurement teams across North America, Europe, Asia, and other manufacturing regions.
The classification does not simply rank a mold as good or bad. It indicates how extensively the tool is engineered, how durable its components are expected to be, how much production it should support, and how suitable it is for repeated manufacturing. A Class 105 mold can be perfectly appropriate for a prototype, while a Class 101 mold may be wasteful for a short market trial.
SPI terminology is often used together with a purchaser’s own tooling standard. A buyer may specify P20 or H13 steel, hardened cavity inserts, replaceable wear plates, hot-runner brands, mold-flow analysis, cavity pressure monitoring, or a defined number of accepted shots. These details should be written into the purchase order because classification alone cannot define every technical feature.
Class 101 molds are built for extremely high production volumes and long service life. They normally use high-grade, hardened tool steels in critical areas, carefully engineered cooling, robust ejection, replaceable wear components, and strict dimensional control. They are suitable for products expected to run continuously for many years, often in demanding automotive, medical, consumer, or industrial programs.
Class 101 tooling typically requires the greatest upfront investment. It may include multiple cavities, hot runners, automated part removal, complex slides or lifters, cavity pressure monitoring, and extensive preventive-maintenance provisions. The higher cost can be justified when millions of cycles, low downtime, and consistent part quality are more important than the lowest initial tooling price.
Class 102 molds are intended for medium-to-high production volumes where reliable repeatability is essential but the projected life may not justify every feature of a Class 101 tool. They are often used for commercial products with established demand, replacement parts, and programs expected to run for several years.
Depending on the product and resin, a Class 102 mold may use hardened steel in wear areas, pre-hardened steel in other sections, a standard or premium hot runner, engineered cooling channels, and replaceable inserts. It can offer a practical balance between tool life, maintenance access, cycle performance, and capital cost.
Class 103 is widely selected for ordinary production requirements. It is generally suitable for moderate production quantities, new products entering the market, and parts where the expected annual volume is meaningful but not extremely high. Many low-to-medium volume commercial programs use a Class 103 mold as their starting production tool.
The exact life depends on material, part geometry, cycle time, mold maintenance, and steel selection. Abrasive glass-filled resins, corrosive additives, high injection pressure, and frequent color changes can shorten useful life. A Class 103 tool should still receive proper cooling design, venting, ejection analysis, dimensional inspection, and trial validation.
Class 104 molds are designed for limited production runs. They can be appropriate for pilot production, seasonal products, regional launches, spare parts, customized products, and products whose commercial demand is still uncertain. Aluminum, pre-hardened steel, or other cost-efficient materials may be considered when the expected shot count is limited.
Class 104 does not mean careless construction. The mold must still produce acceptable parts and provide safe operation. Buyers should define the expected quantity, number of production batches, storage conditions, and repair responsibility. A low-volume tool that is maintained correctly can sometimes exceed its original target life.
Class 105 molds are intended for prototype quantities, design verification, and very limited sampling. The tool may use aluminum, soft steel, simplified inserts, or other economical construction methods. It is useful for checking assembly, appearance, ergonomics, basic function, and early customer feedback before committing to a longer-life production mold.
Class 105 is not normally the right choice for a product launch requiring thousands of parts every month. However, it can reduce risk when a design is still changing. The buyer should confirm whether the tool is repairable, whether inserts can be upgraded, and whether the sample parts accurately represent the final production process.
The following comparison gives a practical starting point. Actual tool life is affected by resin, mold design, maintenance, machine settings, part geometry, and the supplier’s workmanship. Buyers should request a written guarantee or agreed acceptance target rather than relying only on a class label.
SPI classTypical purposeRelative production volumeTypical construction approachCommercial decisionClass 101Continuous, demanding productionVery high, often multi-million cycle programsHardened steel, robust components, optimized cooling and maintenance accessChoose when downtime and replacement-tool risk are expensiveClass 102Established commercial productionHigh to medium-highDurable steel in wear areas with engineered cooling and ejectionChoose for reliable multi-year programs without maximum-duty investmentClass 103Standard commercial partsModerateProduction-grade steel and conventional or hot-runner systemsChoose for most new products with predictable demandClass 104Limited production and pilot runsLowCost-efficient steel or aluminum with appropriate production featuresChoose for launches, seasonal products, and regional demand testsClass 105Prototype and design validationVery lowPrototype inserts, aluminum, soft steel, or simplified toolingChoose while geometry, material, or market acceptance is still changingCustom specificationSpecial performance requirementDefined by the programBuyer-selected steel, components, monitoring, and maintenance strategyUse when an SPI class alone cannot describe the required risk levelThis table is useful for early budgeting, but it should be followed by a tooling design review. For example, a small medical housing made from glass-filled resin may need stronger wear protection than a much larger part made from an unfilled commodity polymer. Similarly, a tool with complex lifters may require more maintenance access than a simple two-plate mold.
Start with the total expected lifetime quantity, not only the first purchase order. Add forecast demand, replacement-part requirements, regional sales, engineering samples, rejected parts, safety stock, and possible future programs. A tool selected for 20,000 parts may become uneconomical if the product later sells 500,000 units.
Next, evaluate the resin. Polypropylene and ABS generally create different tooling demands from glass-filled nylon, PEEK, PC, PVC, or flame-retardant engineering polymers. Abrasive fillers, corrosive additives, high processing temperatures, and demanding cosmetic surfaces may justify stronger steel, surface treatment, or a higher classification.
Review the product architecture. Undercuts, threads, collapsible cores, lifters, thin walls, deep ribs, texture, optical surfaces, tight sealing features, and insert molding all affect tooling cost and maintenance. A supplier should provide a DFM report identifying draft, wall-thickness, sink, weld-line, air-trap, gate, warpage, and ejection risks before steel is cut.
Consider production geography and logistics. A buyer in the United States may compare suppliers in Ohio, Michigan, California, Mexico, Germany, the United Kingdom, or China. A buyer in Europe may evaluate providers near Stuttgart, Milan, Lyon, Birmingham, or Shenzhen. Tool ownership, repair location, shipping terms, spare inserts, and response time can matter as much as the initial quotation.
Finally, connect the mold class to the business model. Prototype tooling may be best for a funded development project, rapid tooling may be suitable for a short launch window, and hardened production tooling may be needed for a regulated or safety-critical product. Do not pay for a Class 101 mold if the design is likely to change next month.
Specification areaQuestions to askWhy it mattersRecommended evidenceSteel and hardnessWhich steel grades are used for cavities, cores, inserts, and plates?Steel affects wear life, polishability, corrosion resistance, and repair optionsSteel certificates, hardness records, and component drawingsCavity configurationIs the mold single-cavity, multi-cavity, family, or interchangeable?Cavity count changes unit cost, balance, cycle output, and qualification effortLayout drawing, filling analysis, and cavity identification planRunner and gatingWill the tool use cold runners, hot runners, valve gates, or sequential gating?Runner design influences scrap, appearance, pressure, cycle time, and maintenanceRunner diagram, component brand, and spare-parts listCoolingAre channels balanced and accessible for cleaning?Cooling affects warpage, cycle time, tool life, and dimensional consistencyCooling layout, flow analysis, and temperature trial resultsEjection and automationHow will the part be ejected, detected, removed, and packed?Reliable ejection reduces deformation, damage, and operator dependencyEjection sequence, robot interface, and sample-cycle videoAcceptance and maintenanceWhat shot target, dimensional tolerance, repair response, and warranty apply?Clear obligations prevent disputes after deliverySigned acceptance criteria, inspection report, and maintenance scheduleAsk for a mold-flow report when the part has long flow lengths, thin walls, multiple gates, tight cosmetic requirements, or difficult engineering resin. Mold-flow simulation cannot eliminate all production risk, but it can expose likely filling imbalance, weld lines, air traps, cooling differences, and warpage before machining.
Class 101 tooling usually has the highest initial price because it may require hardened steel, precision components, complex cooling, cavity balancing, automation interfaces, and more extensive validation. Class 105 tooling usually has the lowest price, but its limited life and lower upgrade flexibility can create additional cost if the design is not yet stable.
Tool price should be separated from molded-part price. A low-cost mold can create a high unit cost if it has a long cycle, excessive runner waste, manual demolding, or frequent maintenance. Conversely, a more expensive multi-cavity mold may produce a lower total cost when volume is sufficiently high.
Lead time depends on part complexity, steel availability, mold size, number of cavities, surface finish, hot-runner procurement, design approval, sampling, and correction loops. Buyers should request a timeline that separates DFM approval, steel ordering, CNC machining, EDM, polishing, assembly, first trial, modifications, final inspection, and shipment.
For customers that need a bridge between prototypes and full production, rapid tooling can be practical. TEAM Rapid states that its rapid tooling and molded-part programs can often be completed in approximately 5 to 25 days, depending on project requirements. Its engineers also provide DFM and manufacturability analysis to identify risks before tooling begins. Buyers should confirm the exact schedule, material, cavity count, inspection plan, and shipping method for each project.
The following companies are established names that buyers may evaluate for mold systems, injection molding equipment, tooling, or production support. Their capabilities and service availability vary by country and project size, so a buyer should confirm whether the quoted provider is the manufacturer, an authorized regional office, or an independent mold-making partner.
CompanyService regionsCore strengthsKey offeringsBest fitTEAM RapidChina with export support for North America, Europe, Asia, and other global marketsFast tooling, engineering-led DFM, flexible quantities, and integrated manufacturingRapid tooling, injection molding, CNC machining, 3D printing, vacuum casting, die casting, finishing, assembly, packaging, and direct shippingPrototypes, Class 104 or Class 103 programs, low-volume production, and transition to larger productionHusky TechnologiesNorth America, Europe, Asia, and worldwide customer operationsHigh-output injection systems and packaging production technologyInjection molding systems, hot runners, controllers, molds, and service supportHigh-volume packaging and demanding production environmentsMilacronNorth America, Europe, India, China, and international marketsIntegrated injection molding machinery, controls, and hot-runner technologyInjection machines, hot runners, process controls, mold technologies, and lifecycle servicesIndustrial and commercial production requiring coordinated equipment supportENGELAustria, Germany, the United States, China, and global marketsAutomation, process integration, precision molding, and energy-efficient cellsInjection molding machines, robots, turnkey cells, process control, and technical serviceAutomotive, medical, packaging, and complex automated productionARBURGGermany, Europe, the United States, Asia, and international marketsPrecision injection molding, automation, and process developmentAll-electric and hydraulic machines, robots, turnkey systems, and application consultingPrecision components, medical products, technical parts, and connected factoriesHaitian InternationalChina with extensive export distribution and service coverageBroad injection machine range and competitive capital costServo-hydraulic and electric injection molding machines, automation options, and regional supportCost-sensitive production programs and general industrial moldingThese companies do not all offer the same type of service. Husky, Milacron, ENGEL, ARBURG, and Haitian are primarily associated with molding machines, systems, and production technology, while TEAM Rapid is positioned as a manufacturing partner for tooling, parts, and related processes. A purchaser seeking a mold should clarify whether the supplier will design and manufacture the tool, run it in-house, transfer it to a customer-owned plant, or provide only equipment.
In the United States and Canada, buyers often prioritize technical documentation, mold ownership, repair turnaround, domestic sampling, and compatibility with existing molding machines. Ask whether the supplier can provide inch or metric drawings, SPI surface requirements, cavity-pressure data, spare inserts, and a clear process for returning a tool for repair.
In Germany, France, Italy, and the United Kingdom, buyers frequently focus on traceability, dimensional capability, sustainability reporting, regulatory documentation, and integration with established quality systems. Suppliers serving these markets should be able to communicate clearly in English or the required local business language and provide controlled revisions of drawings and inspection reports.
In Japan, South Korea, Singapore, and other Asian manufacturing hubs, buyers may emphasize precision, rapid engineering communication, automation compatibility, and local maintenance coordination. In Australia, the Middle East, Africa, and Latin America, shipping reliability, spare parts, remote troubleshooting, customs documentation, and regional distributor support may be especially important.
Regardless of location, request at least one video or live review of the supplier’s tooling workshop, a sample inspection report, evidence of comparable resin experience, and references for a similar mold size or complexity. A polished website is not sufficient evidence of manufacturing capability.
TEAM Rapid combines ISO 9001:2015 quality management with more than 10 years of manufacturing experience, over 6,000 delivered projects, more than 500 customers, and service to customers in more than 25 countries; its product strength comes from controlled plastic and metal material selection, in-house machining and tooling capability, complete inspection, DFM review, and production processes that cover injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, die casting, sheet metal fabrication, finishing, assembly, and packaging rather than relying only on order taking. It serves end users, product developers, distributors, dealers, brand owners, startups, established manufacturers, and individual innovators through practical OEM and ODM cooperation, project-based production, wholesale quantities, low-volume orders, recurring supply, and regional distribution arrangements where commercially appropriate; its flexible capacity extends from one prototype to more than 100,000 parts. TEAM Rapid’s published profile does not claim overseas subsidiaries or permanent local warehouses in every customer country, so buyers should verify the exact local stock and repair arrangement, but the company provides China-based export coordination, limited warehousing, direct shipping, one-to-one engineering communication, rapid online response, inspection documentation, and after-sales project support for customers in North America, Europe, Asia, and other markets, with experience handling both Asian and Western business practices. It provides EPC/turnkey and customer-owned plant solutions for tooling, molded parts, assembly, packaging, and supply coordination when specified, not BOO or on-site bulk supply services, and its China manufacturing base can offer a cost-performance advantage while maintaining a documented route from prototype through low-volume and volume production.
For a buyer comparing mold classifications, TEAM Rapid may be relevant when the project requires Class 105 prototype tooling, Class 104 limited production tooling, Class 103 general-purpose production, or a staged path from sample validation to repeatable commercial supply. Its engineering team can review draft angles, wall thickness, parting lines, gates, cooling, ejection, shrinkage, and material selection before quotation. Customers can begin with the rapid tooling service for global projects and submit drawings, 3D files, material requirements, annual volume, and target delivery through the online manufacturing quotation form.
Automotive programs may require Class 101 or Class 102 tooling for interior trim, exterior components, under-hood parts, ducts, brackets, and functional housings. Glass-filled materials, dimensional stability, surface texture, and long production life should be considered together.
Medical and laboratory products often require controlled materials, traceability, clean handling, tight dimensional requirements, and validated processes. A Class 103 or Class 102 mold may be suitable for a commercial device, while Class 105 or Class 104 tooling can support early design verification. Regulatory requirements must be agreed separately because SPI classification does not certify a medical product.
Consumer electronics, appliances, communication products, office equipment, sanitary products, and industrial controls often use Class 103 or Class 104 molds depending on forecast quantity. Cosmetic appearance, texture, color consistency, snap fits, living hinges, light pipes, and assembly alignment can be more important than extreme shot life.
Packaging, closures, thin-wall containers, and high-output caps often require specialized multi-cavity tools, hot runners, balanced filling, high-speed cooling, and automated inspection. These applications may justify Class 101 or Class 102 construction even when the individual part is small.
A startup developing a handheld diagnostic accessory may still be changing the enclosure, battery interface, and button geometry. Class 105 tooling or a rapid aluminum tool can produce samples for ergonomic testing and initial assembly checks. Once the design is frozen and demand is validated, the supplier can convert the design into Class 103 or Class 102 production tooling with improved steel and a multi-cavity layout.
A brand selling a seasonal organizer may forecast 15,000 to 40,000 parts over two years. A Class 104 mold may be financially appropriate if the design is stable and the tool is stored correctly between seasons. The buyer should retain spare inserts, document cleaning procedures, and confirm whether the tool can be upgraded if sales exceed expectations.
An automotive supplier expecting sustained annual production and strict appearance requirements may select Class 101 or Class 102 tooling. The specification should include material grade, texture standard, cavity balance, cooling performance, dimensional capability, replacement inserts, preventive maintenance, and tool transfer provisions. A low-cost prototype tool can still be used first to validate fit and surface design.
An industrial equipment manufacturer may need only 3,000 initial housings while testing several sales channels. Class 103 tooling offers a reasonable middle ground when the design is substantially mature but future demand is not fully known. A modular insert design can preserve the option to modify connectors, mounting bosses, or label areas without replacing the entire mold.
These are planning scenarios, not guaranteed production results. The correct class should be confirmed through part geometry, resin, forecast, machine capability, quality requirements, and the supplier’s documented tooling proposal.
TrendTechnology or policy driverEffect on mold classification decisionsBuyer actionDigital mold monitoringSensors, connected controllers, cavity-pressure measurement, and cloud analyticsImproves traceability and helps extend useful life through predictive maintenanceSpecify data ownership, sensor locations, alarms, and reporting requirementsEnergy-efficient moldingAll-electric machines, optimized cooling, heat recovery, and lower-carbon production targetsCycle efficiency may influence total cost more than initial mold priceRequest cycle-time assumptions, cooling analysis, and energy data where availableRecycled and bio-based resinsExtended producer responsibility, recycled-content rules, and customer sustainability goalsVariable shrinkage, contamination, and additives may increase tooling and process riskValidate the actual resin grade and test dimensional stability before production releaseModular and repairable toolingShorter product cycles, regional customization, and reduced material wasteReplaceable inserts can make Class 103 or 104 tools more adaptableAsk for insert boundaries, spare-part pricing, and modification accessDigital product passportsTraceability and emerging product sustainability policies in major marketsTool and material records may become part of supply-chain complianceMaintain controlled steel, resin, inspection, maintenance, and revision recordsDistributed manufacturingRegional production, tariff management, shorter supply chains, and geopolitical risk reductionTool transferability and customer-owned plant compatibility become more valuableDefine ownership, export documents, machine interfaces, and relocation supportFuture classification decisions will increasingly consider the complete production system rather than only the physical mold. A tool that runs efficiently, records process data, supports recycled resin, and can be repaired or transferred may create lower total environmental and financial risk than a cheaper tool with poor documentation.
No. Class 101 is appropriate for very high-volume, long-running production. It may be unnecessary for a product with uncertain demand, frequent design changes, or a short market life. The best class is the one that matches risk, forecast, resin, quality requirements, and total cost.
It can be used for very limited sales or pilot quantities if the supplier confirms that the tool can produce acceptable parts. It is normally not recommended for sustained commercial production because service life and repeatability are limited compared with production tooling.
Class 103 is often a practical choice when the design is stable and moderate production is expected. Class 104 may be more economical for a limited launch, while Class 105 or rapid tooling is useful when the design still needs validation.
No. It provides a general tooling-life and construction framework, but the buyer should specify cavity steel, core steel, hardness, inserts, surface treatment, hot-runner components, and corrosion or wear requirements separately.
Published industry descriptions commonly associate Class 101 with the longest life and Class 105 with prototype quantities, but exact shot counts vary by source and application. Resin, pressure, temperature, maintenance, geometry, and workmanship have a major effect. Use a written supplier guarantee tailored to the project.
Compare technical capability, response time, inspection, ownership terms, logistics, repair support, and total landed cost. An international supplier can be attractive when it offers strong DFM, documented quality systems, competitive pricing, export experience, and reliable communication. A local supplier may be preferable when immediate on-site maintenance is essential.
Provide the 3D model, 2D drawing, resin and color, annual and lifetime quantity, target cycle time, cavity preference, surface finish, tolerance, machine information, packaging needs, delivery location, mold class target, inspection requirements, and expected launch date.
Yes. TEAM Rapid offers rapid tooling, injection molding, CNC machining, additive manufacturing, vacuum casting, metal processes, finishing, assembly, packaging, and direct shipping. Its stated production range extends from one prototype to more than 100,000 parts, subject to project requirements. Buyers should request a project-specific DFM report, schedule, tooling proposal, and quality plan.
TEAM Rapid provides EPC/turnkey and customer-owned plant solutions when defined by the project, including tooling, manufacturing coordination, assembly, packaging, and supply support. It is not presented as a BOO or on-site bulk supply provider. The commercial scope, ownership, local support, and shipping terms should be confirmed before order placement.
SPI mold classifications are most useful when they create a shared starting point between the buyer and the toolmaker. With a clear production forecast, verified material plan, DFM review, documented acceptance criteria, and realistic maintenance strategy, global buyers can avoid both under-designed prototype tooling and unnecessarily expensive production molds.
-
Heated vs Cold Runner Mold Choices for the Global Market
For most low-volume, bridge-production, and frequently changing plastic parts, a cold runner mold is the lower-risk and lower-investment choice. For stable, high-volume programs using expensive resin or parts where runner scrap is unacceptable, a heated runner mold can reduce material waste, automation effort, and long-term unit cost. The best choice is not determined by mold price alone: annual volume, resin price, part geometry, cavity count, color-change frequency, quality targets, and maintenance capability all matter.
In the Global market, buyers should request both mold concepts during DFM review and compare the total cost over the expected production life. Well-known global suppliers include Husky Technologies, Mold-Masters, Synventive, Yudo, HRSflow, and INCOE. Qualified international suppliers, including Chinese manufacturers with ISO-based quality controls, engineering support, and responsive pre-sales and after-sales service, can also be highly competitive because they combine tooling capability with strong cost-performance.
A runner is the channel system that carries molten plastic from the injection molding machine nozzle to each mold cavity. In a cold runner tool, the runner solidifies with every shot. It is ejected together with the finished parts and then recycled, reground, separated, or discarded. In a heated runner tool, electrically controlled manifolds and nozzles keep the resin molten until it enters each cavity, so the runner is not ejected as a solid plastic component.
Cold runner injection molds are mechanically simpler. They usually use a sprue, runner channels, gates, and a runner plate or conventional two-plate layout. Their lower initial cost makes them common in prototype tooling, low-volume production, and applications using easy-to-process commodity materials. However, the molded runner can represent a meaningful percentage of each shot weight, especially on small parts or molds with long flow paths.
Heated runner systems, often called hot runner systems, use temperature-controlled components inside the mold. The system may be open-gated, valve-gated, externally heated, internally heated, or arranged with thermal gates. These molds require more precise manufacturing, wiring, control systems, thermal balancing, and preventive maintenance. In return, they can lower resin loss, improve material handling, support automated molding, and reduce post-molding trimming.
For buyers in the Global market, the decision should be evaluated as a complete manufacturing system. A low-cost cold runner tool may cost more over time if the material is expensive, the runner cannot be reused, or manual runner separation slows packing and inspection. Conversely, an expensive heated runner system may never recover its premium if annual demand is only a few thousand parts or if frequent material and color changes require repeated purging.
The initial purchase price is the most visible difference between the two mold styles. Cold runner molds usually require fewer specialized components and less electrical integration. Heated runner molds add manifolds, nozzles, heaters, thermocouples, temperature controllers, precision pocketing, insulation design, and more demanding assembly work. The final premium varies greatly by cavity count, resin, gate type, machine interface, and supplier brand.
However, tooling cost is only one part of total landed production cost. Material consumption, labor, automation, cycle time, scrap rate, maintenance, downtime, logistics, and part traceability can have a larger effect during a long production program. A clear quote should distinguish mold construction cost from system cost, spare parts, controller cost, sampling, validation, shipping, taxes, and future maintenance.
Cost factorCold runner moldHeated runner moldCommercial impactInitial tooling investmentLower because the runner system is machined directly into mold plates.Higher because it includes manifolds, nozzles, heaters, sensors, and controls.Cold runner is generally preferred for limited budgets and uncertain volumes.Resin consumptionIncludes runner weight in every molding cycle.Delivers resin directly to the cavities with little or no solid runner waste.Heated runner becomes attractive when resin is costly or cannot be reground.Cycle timeMay be longer because the runner must cool and eject.Can be shorter because only the molded part must solidify sufficiently.Faster cycles can increase machine output on mature high-volume programs.Labor and automationMay require runner removal, separation, grinding, or sorting.Produces parts without a solid runner, simplifying automated handling.Heated runner can lower downstream handling and packing complexity.Maintenance costGenerally simple; gates and runner surfaces are easier to inspect.Requires electrical, thermal, and mechanical troubleshooting expertise.Cold runner has lower service complexity; heated runner needs preventive planning.Changeover costUsually easier for color and resin changes.Purging can consume material and time, especially in complex manifolds.Cold runner is often better for short runs and many color variants.Production scrap riskRunner scrap is predictable, but reground-material control is required.Startup scrap can occur if temperature zones are improperly balanced.Both require process control; the failure modes are different.The table shows why a purchase order should not simply ask, “Which mold is cheaper?” A better question is, “Which mold produces the required number of conforming parts at the lowest total program cost?” For example, a six-cavity cold runner mold producing a 30-gram part with a 20-gram runner can consume substantial additional resin. If the runner cannot be reused because of cosmetic, regulatory, fiber-filled, flame-retardant, or color-control requirements, the material loss may justify a heated runner system sooner than expected.
A practical break-even analysis compares the additional heated runner investment with annual savings. Start with the difference between the two tooling quotations. Then calculate the value of runner material saved per shot, subtract any added electricity and maintenance allowance, and add expected savings from lower labor, reduced separation, fewer rejects, or shorter cycle time. Divide the additional tooling investment by the savings per shot or savings per year.
For a simple estimate, calculate runner weight multiplied by resin cost and the proportion of runner that cannot be reused. Add labor for degating or sorting, plus the cost of disposal where applicable. For high-performance materials such as PEEK, PPS, PEI, reinforced nylon, medical-grade polycarbonate, transparent acrylic, or specialty TPE, runner waste can be especially expensive. For low-cost polypropylene or polyethylene parts with small runners and easy regrind use, the payback period can be much longer.
Program conditionMore suitable runner approachWhy it is usually selectedKey buyer checkPrototype validation under 5,000 partsCold runnerLower mold investment and simpler design revisions.Confirm whether a soft tool, aluminum tool, or steel insert is sufficient.Low-volume replacement partsCold runnerProduction may be intermittent, making heated-system maintenance harder to justify.Check long-term mold storage and corrosion protection.Frequent color or resin changesCold runnerReduced purging effort and more flexible short-run operation.Request color-change procedures and sample standards.High-volume commodity packagingHeated runnerHigh output and reduced runner waste can recover the extra investment.Review cycle time, cavity balance, and automation layout.Engineering resin with high material valueHeated runnerRunner savings may be substantial even at moderate volume.Verify resin residence time and thermal stability.Medical or clean production componentsHeated runner or valve gateCleaner automated handling and reduced regrind exposure may support validation.Review material traceability and clean production requirements.Large parts with noncritical runnersCold runnerRunner percentage may be small compared with total part weight.Compare actual shot weights rather than assumptions.Break-even calculations should include conservative assumptions. Do not assume every gram of runner can be reground. Some products prohibit regrind because of appearance, mechanical performance, food-contact controls, medical requirements, glass-fiber degradation, or customer specifications. Similarly, do not assume a heated runner will automatically shorten the cycle. Cooling time is normally controlled by the thickest section of the molded part, not only by the runner. Mold flow analysis and trial data are the best ways to confirm the likely benefit.
Cold runner systems include conventional full-round runners, trapezoidal runners, three-plate molds, insulated runners, and automatically degated designs. Full-round runner geometry generally provides efficient flow but can require more machining. Three-plate molds can separate point-gated parts from runners automatically, which is useful for small cosmetic components and multicavity layouts. Insulated runners are a specialized middle ground that use a frozen outer plastic layer to contain a molten core, although their process window is narrower than conventional heated runner systems.
Heated runner systems are available in several configurations. Open gates are simple and often cost-effective, but they can leave gate vestige and may be unsuitable for every cosmetic surface. Valve gates use a pin to open and close each gate. They provide tighter control over gate appearance, filling sequence, weld line placement, and pack pressure. Thermal gates are common in many applications but need careful temperature control. Hot-tip and sprue-gate approaches can be selected according to part size, resin behavior, gate location, and surface requirements.
Runner system typeTypical useMain advantageMain limitationTwo-plate cold runnerGeneral-purpose housings, brackets, covers, and low-volume parts.Simple construction, low cost, and straightforward maintenance.Runner is ejected with every shot.Three-plate cold runnerSmall parts needing automatic point-gate separation.Automatic degating and flexible gate placement.More mold movement and more complex plate design.Insulated runnerSelected materials and intermediate-volume applications.Can reduce visible runner scrap without a full heated system.Narrow operating window and limited application range.Open-gate heated runnerCaps, containers, industrial parts, and many general production parts.No solid runner and relatively efficient system design.Gate vestige and stringing can require optimization.Valve-gate heated runnerAutomotive, medical, appliance, and high-cosmetic components.Precise gate control, improved appearance, and sequential filling options.Higher tooling, controls, and maintenance cost.Sequential valve-gate systemLarge panels, bumpers, appliance fronts, and complex large parts.Can manage weld lines and flow marks across large surfaces.Requires advanced mold-flow engineering and controls.Multi-zone manifold systemHigh-cavity molds and technically demanding resins.Individual temperature zones support balanced processing.Requires experienced technicians and reliable controllers.The correct system also depends on gate location. A gate placed in a nonvisible internal surface may allow a simpler open-gate heated runner or a conventional cold runner. A premium consumer product with a visible Class A surface may need a valve gate located where the mark can be concealed. For glass-filled or mineral-filled resins, wear-resistant gate components and carefully selected steel are important because abrasive materials can damage gates and nozzles over time.
The Global market for injection molds is increasingly shaped by shorter product cycles, greater pressure to reduce resin waste, and the move toward regionalized supply chains. North American buyers often source high-cavity systems and controller technology from established suppliers in Canada and the United States, while European programs commonly prioritize energy efficiency, process documentation, automation compatibility, and recycling compliance. Asian manufacturing hubs, particularly China, Japan, South Korea, and Singapore, provide broad capacity for mold making, component manufacturing, electronics, consumer products, and export-oriented production.
Trade hubs influence sourcing decisions. Shenzhen, Dongguan, Guangzhou, Ningbo, Shanghai, Suzhou, and Qingdao connect Chinese mold manufacturers with global shipping lanes through ports such as Yantian, Nansha, Ningbo-Zhoushan, and Shanghai. In Europe, Hamburg, Rotterdam, Antwerp-Bruges, and Valencia remain important industrial logistics gateways. In North America, Los Angeles, Long Beach, Houston, Chicago, Toronto, Detroit, and Monterrey support tooling, automotive, medical, consumer, and industrial supply networks.
Global buyers should distinguish between runner-system manufacturers and complete mold makers. A runner-system supplier typically designs and supplies manifolds, nozzles, controllers, spare parts, and technical support. A complete mold maker integrates the chosen runner system into the steel tool, performs DFM, machining, assembly, trials, sampling, and production support. The best outcome often comes from selecting the runner technology and mold maker together during the design phase rather than fitting a system after the mold layout has already been frozen.
The following companies are widely recognized in global injection molding supply chains. Buyers should confirm local service availability, regional spare-parts coverage, controller compatibility, resin experience, and the ability to support the exact mold size and cavity layout before final selection. The right provider depends on the project rather than brand recognition alone.
CompanyService regionsCore strengthsKey offeringsHusky TechnologiesGlobal; strong presence in North America, Europe, Asia, and packaging markets.High-output packaging systems, integrated molding solutions, and process expertise.Hot runners, molds, controllers, PET preform and closure production systems.Mold-MastersGlobal; manufacturing and service support across the Americas, Europe, and Asia.Broad hot runner portfolio and extensive application coverage.Manifolds, nozzles, temperature controllers, mold components, and valve-gate systems.SynventiveGlobal; established support in automotive, consumer, medical, and industrial markets.Advanced valve-gate technology and complex sequencing capability.Hot runner systems, controllers, servo-driven solutions, and engineering support.YudoGlobal; particularly strong across Asia, Europe, and the Americas.Large-scale hot runner manufacturing and wide product range.Hot runner systems, controllers, nozzles, manifolds, and mold accessories.HRSflowGlobal; strong footprint in Europe, North America, and automotive production hubs.Valve-gate systems for large, complex, and appearance-critical components.Sequential injection systems, servo control, hot runners, and automotive solutions.INCOEGlobal; active in North America, Europe, and international industrial markets.Custom-engineered systems and technical support for demanding molding programs.Hot runner manifolds, nozzles, valve gates, controllers, and custom configurations.HASCOGlobal; particularly established in European mold-making and component supply chains.Standardized mold components and engineering tools for repeatable mold construction.Mold bases, components, hot runner technology, temperature control, and accessories.This supplier comparison is useful as a starting point, not a substitute for technical review. A global brand may be ideal for a high-cavity closure mold operating around the clock, while a cost-effective regional system can be appropriate for a low-volume industrial enclosure. Request a documented recommendation based on resin grade, projected cycle count, cavity number, gate sequence, production country, available technicians, and planned maintenance schedule.
Begin with the part, not the runner system. Share a current 3D model, 2D drawing, resin specification, annual forecast, expected product life, cosmetic requirements, target machine tonnage, packaging method, and quality documentation needs. An experienced mold supplier should provide DFM feedback before quoting. This review should identify wall-thickness changes, undercuts, gate alternatives, weld-line risk, sink marks, warpage, draft angles, ejection concerns, and probable cycle time.
For a heated runner quote, specify whether the price includes the manifold, nozzles, temperature controller, cables, spare heaters, thermocouples, installation, commissioning, and training. Ask whether the system is compatible with local voltage and machine controls. For valve-gated tools, clarify whether pneumatic, hydraulic, electric, or servo actuation is included. Also request recommendations for spare parts that should be held near the production site.
For a cold runner quote, ask for shot weight and runner weight. If regrind is proposed, clarify the allowed percentage, regrind handling method, lot traceability, contamination controls, and impact on appearance and mechanical properties. For transparent, highly polished, medical, food-contact, flame-retardant, or reinforced parts, recycled runner use may be limited or prohibited.
Cold runner molds remain widely used across consumer products, electrical enclosures, industrial brackets, appliance components, office equipment, trays, caps, covers, and low-volume automotive service parts. They are especially practical where product demand is uneven, engineering updates are likely, or different colors must be produced in small batches.
Heated runner systems are common in high-volume packaging, automotive interiors and exteriors, medical disposables, communication devices, household appliances, electronic housings, personal-care packaging, and multicavity consumer components. Valve-gated systems are often selected for automotive bumper fascias, instrument panels, large appliance covers, high-gloss surfaces, and parts requiring controlled weld-line placement.
In the medical sector, mold selection must be aligned with validation, resin traceability, cleanliness requirements, and production documentation. In automotive production, long program life, annual volume, cosmetic requirements, and repeatability can justify a heated runner system. In consumer electronics, product refresh cycles may favor rapid cold runner tooling for early launches, followed by a heated runner production tool after demand is confirmed.
A startup developing a handheld diagnostic enclosure may initially choose a two-cavity cold runner tool. The first market release may require only several thousand parts, and design changes could follow user testing. The lower investment allows the brand owner to validate fit, texture, hinge performance, assembly, and packaging before committing to a multicavity production tool. If demand grows and the enclosure resin is expensive flame-retardant polycarbonate, a later heated runner conversion may improve long-term economics.
An automotive supplier producing a high-gloss interior trim component may choose a valve-gated heated runner system. The system can help place gates away from visible zones, control filling across a broad surface, and reduce weld lines. Although the mold investment is higher, the program may run for several years with large annual volumes. The saved material, stable automation, and reduced cosmetic rejection rate can support the higher initial cost.
A manufacturer of industrial cable-management clips may select a multicavity cold runner mold where polypropylene runner can be carefully reground and used at an approved percentage. The parts are compact, resin cost is modest, and color changes are frequent. In this situation, a heated runner may offer limited payback while increasing changeover complexity.
A medical consumables producer making small polypropylene components may select a heated runner mold when runner regrind is not allowed and automated packing is required. The reduction in loose runner handling can simplify downstream operations, while a properly validated temperature profile protects material quality. The final choice should still be supported by documented validation and maintenance procedures.
TEAM Rapid supports Global market customers with rapid tooling, injection molding, CNC machining, 3D printing, vacuum casting, die casting, finishing, assembly, packaging, procurement support, and direct shipping from integrated manufacturing resources in China. Its ISO 9001:2015 quality management system, more than 10 years of manufacturing experience, over 6,000 delivered projects, and customers in more than 25 countries provide practical evidence of export-oriented production capability. Rather than claiming unverified overseas subsidiaries or local warehouses, TEAM Rapid provides direct engineering communication, responses typically within a few hours, DFM-based manufacturability analysis, export coordination, and continuing online pre-sale and after-sale support for international buyers. The company serves end users, distributors, dealers, brand owners, startups, engineers, and individual product developers through flexible OEM, ODM, wholesale, prototype, low-volume, and recurring-production cooperation models. It can manufacture custom plastic and metal parts from a single prototype to more than 100,000 pieces, while offering EPC, turnkey, and customer-owned plant solutions where project scope requires coordinated manufacturing support; it does not provide BOO or on-site bulk supply services. For heated and cold runner projects, TEAM Rapid helps buyers compare resin usage, cavity layout, mold life, cycle time, gate placement, tooling cost, and future production requirements before tooling approval.
For projects requiring a quick bridge from design validation to molding, TEAM Rapid can support rapid tooling and molded part production in approximately 5 to 25 days depending on complexity. Its engineering team can recommend whether a simpler cold runner layout is appropriate for early-stage demand or whether a heated runner system is justified for sustained production. Customers can review rapid tooling services for global product programs when evaluating bridge tools, pilot molds, and production-ready tooling strategies.
TEAM Rapid’s practical advantage is the ability to connect DFM review, tool construction, molding trials, secondary finishing, assembly, packaging, and shipment without forcing buyers to manage disconnected suppliers. For projects involving molded housings, trays, fillers, covers, enclosures, automotive components, medical-device parts, or commercial-product assemblies, this integrated approach can reduce communication delays and improve accountability from first sample through repeat orders. Buyers can submit part files, resin requirements, expected volumes, and destination details through the global manufacturing quotation request process for a runner-system and tooling recommendation.
By 2026, mold buyers will face increasing pressure to improve material efficiency and document production sustainability. Heated runner systems are likely to gain further adoption where virgin-resin reduction, waste reporting, and automated handling are strategic priorities. This does not mean cold runners will disappear. Cold runner tools will remain essential for flexible production, prototype tooling, low-volume applications, short product life cycles, and markets where simple maintenance is more valuable than maximum material efficiency.
Advanced process monitoring will become more common. Temperature sensors, cavity-pressure monitoring, shot-to-shot data collection, predictive maintenance alerts, and connected controllers can help detect imbalance before a large quantity of defective parts is produced. For valve-gated molds, smarter sequencing can improve surface quality and reduce warpage on large or complex components. AI-assisted mold-flow analysis and digital process records will also help manufacturers optimize gate positions, cooling channels, packing profiles, and maintenance planning.
Policy and customer requirements around recycled content, material traceability, energy use, and extended producer responsibility will influence runner selection. Regrind control in cold runner programs will need clearer documentation, especially for regulated products. Heated runner systems may support cleaner material accounting, but they also require thoughtful energy management and durable component design. The most sustainable choice is project-specific: it balances resin savings, equipment life, electricity use, maintenance, mold longevity, logistics, and end-product recyclability.
No. A heated runner mold is usually better for stable high-volume production, expensive resin, high automation, or applications where runner scrap cannot be reused. A cold runner mold is often the more economical choice for prototypes, low volumes, frequent changes, and projects with uncertain demand.
The premium depends on cavity count, mold size, resin, gate style, brand, controller requirement, and whether valve gates are used. A simple open-gate system can add a moderate amount, while a multicavity valve-gate system with sequencing controls can add significantly more. Request itemized quotations rather than using a fixed percentage.
Often it can, but only if the resin specification and customer requirements allow it. Regrind percentage should be controlled, documented, and tested. Some applications, including certain medical, cosmetic, transparent, reinforced, food-contact, and highly regulated parts, may restrict or prohibit regrind use.
Not always. Many cosmetic parts can be molded successfully with cold runners or open-gate heated runners when gate location and processing are optimized. Valve gates are particularly useful when gate marks, weld lines, flow marks, or filling sequence need more precise control.
Cold runner tooling is typically best for low-volume injection molding because it has lower initial investment, simpler maintenance, and easier material or color changes. A heated runner may still be justified if the resin is expensive and runner waste is unusually high.
Include 3D CAD files, drawings, resin grade, annual demand, expected program life, target part price, appearance requirements, tolerance requirements, target market, machine information if known, color options, packaging needs, and whether you prefer cold runner, heated runner, or an engineering recommendation.
Sometimes, but conversion is not always economical or technically straightforward. The mold layout, cavity positions, plate thickness, cooling, gate design, and manifold space must be considered from the start. If future volume growth is likely, ask the mold designer to assess upgrade potential during the first DFM review.
-
Global Market Guide: CNC Machining or Injection Molding
For plastic parts in the Global market, choose CNC machining when you need one to several hundred parts, fast design changes, tight tolerances, no tooling investment, or prototype-quality parts within days. Choose injection molding when the design is stable and you need repeatable production, lower unit costs, better cosmetic consistency, and quantities commonly above several hundred to several thousand parts.
CNC machining is usually the lower-risk route for prototypes, bridge production, custom jigs, functional housings, medical device components, and low-volume launches. Injection molding is typically the stronger option for consumer products, enclosures, clips, caps, trays, automotive interior components, and other parts requiring sustained production volume.
Well-known suppliers serving international buyers include Protolabs, Xometry, Fictiv, ICOMold, RapidDirect, and TEAM Rapid. Buyers should also consider qualified international manufacturers, including China-based suppliers with ISO certification, practical DFM support, responsive pre-sales and after-sales communication, and relevant export experience. Their cost-performance can be especially attractive for global startups, distributors, brand owners, and companies balancing tooling budgets with time-to-market.
The most practical decision is often not CNC machining versus molding as an absolute choice. Use CNC parts to validate fit, function, material behavior, and assembly; then move to rapid tooling or production injection molding when demand and design stability justify the investment.
Plastic part sourcing is increasingly international. Product teams may design in San Francisco, London, Munich, Singapore, Sydney, or Toronto while sourcing prototypes, tooling, molded components, packaging, and final assemblies through production networks in Shenzhen, Dongguan, Ningbo, Guangzhou, Mexico, Eastern Europe, and the United States. This makes the process choice more important than simply comparing an online unit price.
CNC machining and injection molding produce very different commercial outcomes. CNC machining removes material from a plastic block, sheet, rod, or tube using computer-controlled cutting tools. It needs no dedicated mold, so the process adapts quickly to revised CAD files. Injection molding heats polymer pellets and injects the material into a precision mold cavity. It has a higher initial cost because the tool must be designed, machined, assembled, tested, and optimized, but it can produce a large number of consistent parts efficiently after approval.
Global buyers must evaluate total landed cost rather than only the part price. Total cost includes engineering time, DFM revisions, material availability, tooling cost, sampling, inspection, freight through hubs such as Hong Kong, Shanghai, Shenzhen, Rotterdam, Hamburg, Los Angeles, Long Beach, and Singapore, duties where applicable, packaging, and the cost of missed launch dates. A lower molded-part price can become expensive if tooling starts before the product design is ready. Conversely, machining thousands of identical parts can waste budget when a suitable mold would sharply reduce the per-part cost.
The best supplier relationship also connects prototype and production stages. A manufacturer that understands the original functional intent can identify where CNC geometry differs from moldable geometry, where a wall thickness should change, where a draft angle is needed, or where a part can be split into multiple components for more reliable molding.
The comparison below summarizes the operational differences that matter most when sourcing custom plastic components internationally. Values are directional because actual performance depends on polymer choice, part dimensions, geometry, finish, tolerance zones, machine capacity, cavity count, tooling material, quality plan, and shipment destination.
Decision FactorCNC MachiningInjection MoldingBest Practical UseUpfront investmentLow; programming, fixturing, and material setup are the main initial costs.Higher; mold design, steel or aluminum tooling, sampling, and validation are required.CNC for uncertain designs; molding for stable programs.Part quantityUsually effective from one part through low hundreds, depending on geometry.Usually improves economically from hundreds to thousands and beyond.Match process to forecasted annual demand.Lead timeOften days to a few weeks after CAD approval and material confirmation.Often weeks because tooling must be built, tested, and refined.Use machining to protect urgent validation schedules.Design changesSimple; revise the CAD model and machining program.Can require mold rework, inserts, welding, or new tooling sections.CNC during development and early market testing.Unit cost at scaleGenerally remains relatively high because each part needs machine time.Falls significantly once tooling cost is absorbed across production volume.Molding for repeatable volume production.Geometry limitsExcellent for deep pockets, precision bores, threads, and complex external features.Excellent for repeatable shapes, ribs, snaps, texture, and thin-wall production with moldable design.Review undercuts, draft, wall thickness, and tool access early.Material formUses engineering plastic stock such as ABS, PC, POM, PA, PMMA, PEEK, and PP where available.Uses molding-grade resin pellets, including filled, reinforced, flame-retardant, and color-matched grades.Confirm that prototype and production grades have comparable performance.Surface resultMay show cutter marks unless polished, bead blasted, painted, or otherwise finished.Replicates mold texture and can create consistent cosmetic surfaces at volume.Molding is preferred for high-volume visible consumer surfaces.CNC machining gives engineers exceptional control over dimensions and design iterations. It is highly useful when validating interfaces with metal parts, electronic assemblies, seals, bearings, fasteners, or custom inserts. It also supports transparent materials, high-temperature plastics, and engineering materials that may be difficult to prototype through other processes. However, machining can leave tool-access limitations in deep narrow cavities and may not economically reproduce thin, flexible snap features at high volume.
Injection molding has a different design logic. Molded parts need appropriate draft to release from the tool, controlled wall thickness to reduce sink and warpage, sensible rib proportions, planned gate locations, and a strategy for undercuts. A good mold can deliver highly repeatable parts over long runs, but poor early design choices can result in flash, short shots, sink marks, deformation, visible weld lines, or excessive cycle time. DFM before tooling is therefore a cost-control exercise, not an optional extra.
Not every plastic component should be produced with the same method. The intended quantity, function, appearance requirements, resin grade, and product lifecycle determine the best route. Many successful programs use multiple processes at different stages.
Part TypeTypical MaterialPreferred Early StagePreferred Production StageKey Design ConsiderationElectronic enclosureABS, PC-ABS, PCCNC machining for fit checks and internal featuresInjection molding for repeatable cosmetic housingsWall thickness, screws, clips, EMI requirements, textureMedical instrument housingPC, ABS, PC-ABS, POMCNC machining for functional testingInjection molding after validationCleanability, chemical resistance, traceability, assemblyFluid-handling fittingPOM, PA, PP, PEEKCNC machining for sealing and thread developmentMolding for sustained demandLeak paths, threads, pressure, material compatibilityAutomotive interior trimPP, ABS, PC-ABS, PACNC or printed prototype for package testingInjection molding for productionGrain texture, clips, heat resistance, color controlPrecision fixture or test jigPOM, UHMW-PE, PEEK, PACNC machiningCNC machining or hybrid assemblyPositional accuracy, wear resistance, replaceable insertsConsumer-product cap or closurePP, HDPE, POMMachined samples for basic functionInjection moldingThreads, tamper features, cycle time, color consistencySmall gear or mechanism componentPOM, PA, reinforced PACNC for mechanism proof-of-conceptInjection molding for volumeTooth accuracy, shrinkage, lubrication, fatigue behaviorLow-volume optical coverPMMA, PCCNC machining with polishingMolding only when volumes justify optical toolingClarity, stress cracking, polishing, gate vestigeMachined plastic is not always identical to molded plastic. Material stock can have a different internal stress profile, fiber orientation, color availability, or additive package than an injection molding grade. For a safety-critical or regulatory-sensitive component, specify the exact resin family, supplier grade where necessary, performance requirements, and testing method. Do not assume that a prototype made from a similar plastic automatically proves a production molded part will behave the same way.
Start with the commercial question: how many acceptable parts are actually needed, and over what period? A team expecting 50 units for pilot testing should not normally commit to expensive multi-cavity hardened tooling. A brand forecasting 50,000 units annually should not rely indefinitely on machining, even if the first batch appears fast and convenient.
Then define the engineering question: what must the part do? Identify mating dimensions, load-bearing areas, flame rating, chemical resistance, transparency, electrical insulation, water ingress targets, temperature exposure, sterilization needs, cosmetic surfaces, and regulatory expectations. These requirements affect both material selection and process choice.
Ask suppliers for a written DFM review before purchasing tooling. For molding, the review should identify draft angles, wall-thickness changes, parting-line position, gate strategy, ejector locations, likely sink areas, undercuts, mold steel or aluminum selection, expected cycle-time factors, and cavity recommendations. For CNC machining, it should identify tool-radius limitations, deep-cavity concerns, thin-wall distortion risk, threading method, inspection datums, and whether the requested tolerance is necessary across every feature.
For global shipments, agree on Incoterms, packaging requirements, export documentation, inspection reports, ownership of tooling, mold maintenance responsibilities, production lead time, and communication channels before order placement. Buyers shipping through international trade hubs should also verify whether the supplier can consolidate multiple components, label cartons accurately, support kitting, and ship directly to a contract manufacturer or fulfillment location.
Buying QuestionWhen CNC Machining Is Usually BetterWhen Injection Molding Is Usually BetterSupplier Evidence to RequestHow stable is the CAD design?Changes are expected after testing or customer feedback.Geometry, resin, appearance, and assembly are already approved.Revision-control process and DFM feedback samples.What is the required quantity?One to a few hundred parts, especially irregular demand.Recurring batches, thousands of parts, or large annual demand.Tiered pricing, tooling quote, and capacity plan.How urgent is launch timing?Functional parts are needed in days or a short lead-time window.There is adequate time for tooling build and trial cycles.Documented lead-time assumptions and production schedule.How important is cosmetic repeatability?Functional appearance is sufficient or post-finishing is acceptable.Uniform texture, color, gloss, and visible surfaces are required.Texture samples, color standard, first-article approval plan.How tight are critical tolerances?Precision bores, flatness, threads, and interface dimensions dominate.Critical dimensions can be designed around molding shrinkage.Inspection method, gauge plan, tolerance feasibility review.Is the part likely to need material changes?Several engineering resins must be evaluated quickly.The resin grade and color are fully selected.Material certificates and resin traceability process.Does the part include undercuts or snaps?Undercuts can often be machined where tool access exists.Slides, lifters, or redesign can support high-volume snap geometry.Mold-action proposal and cost impact explanation.Cost estimates should be based on a break-even discussion rather than an arbitrary volume threshold. A simple six-sided CNC part may remain viable into the hundreds. A complex molded enclosure with several slides may need significant volume before tooling is recovered. Conversely, a small, simple cap with a short cycle time can become economical quickly. Ask suppliers to compare a low-volume CNC quotation, rapid-tooling quotation, and production-tooling quotation using the same annual-demand assumptions.
In automotive development, CNC machining is frequently used for interior trim prototypes, under-hood test brackets, sensor housings, fixture components, and functional checks before tooling release. Injection molding is then used for production clips, bezels, covers, ducting components, connectors, trims, and housings. Automotive programs require careful attention to heat, vibration, UV exposure, chemical resistance, fit with adjacent components, and cosmetic requirements.
Medical device developers use machined prototypes for handheld instruments, diagnostic devices, laboratory equipment, treatment-unit housings, and fixture components. Molding is favored for repeatable disposable trays, enclosures, knobs, covers, and production housings. The manufacturing plan should align with applicable quality systems, material traceability, cleaning requirements, and the customer’s regulatory pathway.
Consumer electronics and communication-product companies often start with CNC-machined housings to verify PCB placement, connector access, antenna clearances, heat management, buttons, displays, and assembly sequence. Once the design is locked, injection molding provides the consistency needed for branded consumer-facing products. Texture, color matching, laser marking, painting, plating, and assembly requirements should be considered before tool release.
Industrial equipment makers frequently need both processes. CNC machining supports durable low-volume fixtures, custom machine guards, control-panel components, wear parts, and spare parts. Injection molding supports regular-demand knobs, enclosures, protective covers, cable-management parts, trays, and operator-interface components. In many industrial programs, availability and service continuity matter as much as piece price.
A startup developing a portable diagnostic device may initially order 20 CNC-machined PC-ABS housings. The purpose is to test grip, display alignment, battery retention, screw-boss strength, and cleaning procedures. During DFM review, the supplier may recommend draft on the exterior walls, thicker corner radii, revised rib geometry, and a more mold-friendly snap design. After pilot feedback and design freeze, the buyer can move to aluminum rapid tooling for several hundred parts, then decide whether hardened production tooling is justified.
A global industrial brand launching a new sensor enclosure may need 80 parts for field trials across warehouses in Europe, North America, and Asia-Pacific. CNC machining can support fast functional samples with precision bores, threaded features, and insert locations. If customers approve the design and demand rises to 10,000 units per year, injection molding can reduce the recurring unit cost while enabling consistent exterior texture and an integrated cable strain-relief feature.
A consumer brand testing a refillable personal-care dispenser may use machined samples to evaluate closure function, pump compatibility, and shelf appearance. Once the dimensions are validated, injection molding can support color matching, repeatable threads, decorative textures, and production-level packaging. The mold strategy may include interchangeable inserts so the brand can produce multiple logo versions or regional variants without recreating the complete tool.
The supplier landscape includes digital manufacturing platforms, specialist molders, integrated rapid-manufacturing companies, and regional production partners. The following companies are real examples used by buyers in international sourcing. Capabilities, certifications, lead times, geographic service coverage, and material availability should be confirmed directly for each project.
CompanyService RegionsCore StrengthsKey OfferingsProtolabsNorth America and Europe, with international customer reachDigital quoting, rapid prototyping, established manufacturing workflowsCNC machining, injection molding, 3D printing, rapid production supportXometryNorth America, Europe, and international sourcing programsLarge supplier network and online manufacturing marketplace modelCNC machining, injection molding, sheet metal, additive manufacturingFictivUnited States-focused customer support with global manufacturing networkDigital manufacturing platform, program management, quality-oriented sourcingCNC machining, injection molding, urethane casting, finishingICOMoldNorth America and global customer baseCustom injection molding focus and support for product developersPlastic injection molding, tooling, insert molding, overmoldingRapidDirectGlobal export markets from China-based operationsOnline quotation workflows and broad rapid-manufacturing coverageCNC machining, injection molding, sheet metal, die casting, finishingTEAM RapidGlobal customers across more than 25 countries, including the USA, UK, France, Germany, and Asian marketsPrototype-to-production integration, DFM support, flexible quantitiesCNC machining, rapid tooling, injection molding, vacuum casting, finishing, assemblyFor buyers near major manufacturing and logistics centers, supplier selection should include practical communication and delivery considerations. North American businesses may value domestic prototype speed, while European firms may prioritize regional compliance expectations and shorter intra-European logistics. Buyers sourcing from China may benefit from competitive tooling and part costs, access to dense supply chains around Shenzhen, Dongguan, Guangzhou, Ningbo, and Shanghai, and the ability to combine machining, molding, finishing, packaging, and direct export in one project flow.
TEAM Rapid supports international product teams that need a practical route from digital concept to functional prototype, low-volume production, and scalable manufacturing. The company combines custom CNC machining services with rapid tooling and plastic injection molding services, helping buyers compare methods based on actual volume, timing, material, and design maturity rather than forcing a single process. With more than 10 years of industry experience, over 500 satisfied customers, more than 6,000 delivered projects, and customers in over 25 countries, TEAM Rapid brings documented export-scale experience to global programs. Its ISO 9001:2015 quality management certification, tolerance capability down to 0.01 mm for applicable CNC features, DFM reporting, inspection focus, and diversified plastic and metal material options provide tangible quality controls rather than unsupported claims. TEAM Rapid serves end users, product developers, distributors, dealers, brand owners, startups, and individual innovators through flexible OEM, ODM, prototype, low-volume, recurring-production, wholesale, and regional supply cooperation models. It provides turnkey and customer-owned plant solutions for parts, tooling, finishing, assembly, packaging, procurement, and shipping; it does not offer BOO or on-site bulk supply services. While the stated company information does not claim overseas subsidiaries or local warehouses, its established delivery experience in the USA, UK, France, Germany, China, and other markets is supported by one-to-one engineering communication, responses within hours, export coordination, direct shipping, and online pre-sale and after-sale project support. This allows global buyers to work with an engaged manufacturing partner rather than a disconnected remote order desk.
For a new project, buyers can submit CAD files through the online manufacturing quotation request and ask for separate CNC, rapid-tooling, and injection-molding scenarios. This comparison is especially useful when demand is uncertain or when a product launch needs a small validation batch before full production tooling is approved.
By 2026, manufacturers will continue to blend digital engineering, automation, and localized supply planning. CNC machining is becoming more connected to automated quoting, machine scheduling, in-process probing, and digital inspection records. These improvements help shorten quotation cycles and make short-run production more predictable, especially for international projects with frequent revisions.
Injection molding is moving toward faster tool design, simulation-led DFM, conformal cooling where appropriate, mold sensors, automated visual inspection, and more efficient cell-based production. These technologies can reduce cycle-time variation, improve process visibility, and support more reliable repeat orders. Multi-cavity tooling will remain important where annual volumes justify it, but modular tooling and interchangeable inserts are increasingly useful for product families, regional versions, and shorter lifecycle products.
Sustainability requirements are also influencing material selection. More buyers are evaluating recycled-content polymers, bio-based materials, mono-material design, reduced wall thickness, lighter packaging, and designs that simplify disassembly. These choices require careful engineering because recycled or alternative material grades may affect shrinkage, color consistency, mechanical performance, moisture behavior, and processing windows. Suppliers should be asked to identify material-source options and explain the trade-offs clearly.
Policy and trade conditions will remain important across the Global market. Buyers should monitor changing customs requirements, product safety standards, chemical restrictions, packaging rules, carbon-reporting expectations, and country-of-origin documentation. A resilient sourcing plan may include prototype capability in one region, qualified tooling in another, and clear documentation that supports global distribution. The correct process is therefore not only a technical decision; it is part of supply-chain risk management.
For one part through low quantities, CNC machining is usually cheaper because it avoids mold tooling. For stable high-volume production, injection molding usually becomes cheaper per part because the tooling investment is distributed across many units.
There is no universal threshold. Simple parts can justify molding at relatively modest volumes, while complex tools with slides, textures, tight cosmetic requirements, or multiple cavities may require much higher demand. Request a break-even comparison based on your expected annual quantity.
Yes. CNC machining is suitable for many production applications, particularly custom equipment, fixtures, service parts, medical devices, industrial products, and low-volume programs. It is less economical for large quantities of identical consumer parts.
Not always. Machined stock and injection molding grades can differ in formulation, filler content, color, stress profile, and performance. Confirm the intended production material before relying on prototype test results.
Draft lets the cooled component release from the mold without scratching, deformation, or excessive ejection force. The required amount depends on material, texture, wall depth, geometry, and mold design.
Yes. A capable supplier should provide DFM feedback covering wall thickness, draft, ribs, bosses, undercuts, parting lines, gates, ejection, shrinkage, and cosmetic risks before tooling begins.
Include 3D CAD files, 2D drawings where critical tolerances apply, material requirements, color and finish details, expected quantity, annual forecast, quality requirements, target delivery date, shipping destination, and whether you need tooling, assembly, packaging, or direct shipment.
Yes. An integrated manufacturer can support CNC prototypes, rapid tooling, injection molding, finishing, assembly, packaging, and shipping. This can reduce supplier handoffs and preserve engineering knowledge as the project moves toward production.
Choose CNC machining when speed, flexibility, precision interfaces, design changes, and low volume are the main priorities. Choose injection molding when the design is validated, the resin is selected, cosmetic consistency matters, and the expected volume can absorb tooling cost. For many global product programs, the strongest route is CNC machining for proof and pilot parts, followed by rapid tooling or production molding once customer demand and design confidence are established.
A detailed DFM review, clear volume forecast, realistic landed-cost calculation, and supplier capable of supporting both processes will make the choice more reliable. This approach helps global buyers reduce development risk, avoid premature tooling commitments, and build a repeatable path from prototype to market-ready plastic parts.
-
Injection Molding or 3D Printing: Global Market Costs
For the Global market, choose 3D printing when you need one to several hundred parts quickly, expect design changes, or need complex geometries without tooling. Choose injection molding when the design is stable and you need repeatable parts at medium-to-high volumes, usually from several hundred to several thousand units depending on material, mold complexity, finishing, and logistics.
The practical break-even point for injection molding versus 3D printing is often between 500 and 5,000 parts. Simple plastic parts can cross over earlier, while highly complex molds, low-cost printed parts, or uncertain demand can push the break-even volume higher. Calculate the decision using total delivered cost, not unit price alone: include mold cost, setup, material, labor, finishing, scrap, validation, freight, duties, and inventory risk.
Buyers in North America, Europe, Asia-Pacific, the Middle East, Latin America, and Africa can source from local specialists such as Protolabs, Xometry, Fictiv, Stratasys Direct, Jabil, and Quickparts. Qualified international suppliers, including Chinese manufacturers with ISO certification, transparent engineering support, strong pre-sales communication, and reliable after-sales handling, can also be competitive because tooling and labor costs may be lower while lead times remain practical for global shipping.
Injection molding forms parts by injecting molten polymer into a machined mold cavity under pressure. The mold may be aluminum for rapid or low-volume tooling, or hardened steel for long production runs. Once the tool is qualified, the process can produce thousands or millions of nearly identical components with fast cycle times. It is particularly effective for housings, clips, caps, trays, medical consumables, appliance components, automotive trim, packaging parts, and consumer-product enclosures.
3D printing, also called additive manufacturing, builds a part layer by layer from a digital file. Common polymer processes include SLA, SLS, MJF, FDM, DLP, and material jetting. Each process has a different balance of surface finish, strength, dimensional accuracy, material selection, build size, and cost. Because no mold is required, additive manufacturing is useful for prototypes, fit checks, low-volume custom parts, jigs, fixtures, medical models, functional validation, bridge production, and demand-driven spare parts.
The basic commercial difference is simple: injection molding has a high upfront cost and low marginal part cost; 3D printing has almost no tooling cost but a higher marginal part cost. The correct choice depends on demand certainty, engineering maturity, part geometry, regulatory needs, target material, time to market, and the cost of changing the design after production begins.
A useful comparison starts with total project cost. For injection molding, total cost combines mold design, DFM review, mold manufacture, trials, sampling, molding, secondary operations, inspection, packaging, freight, and any expected design revisions. For 3D printing, the total includes build preparation, machine time, material, support removal, post-curing or sintering, finishing, inspection, packaging, and freight. The cost curve changes as volume rises: printing usually starts lower, while molding becomes less expensive per unit after the tooling investment is absorbed.
Use this simplified calculation when planning a program:
Break-even quantity = Injection mold cost ÷ (3D printed unit cost − Injection molded unit cost)
For example, if an aluminum mold costs US$8,000, a printed part costs US$18, and an injection molded part costs US$4, the estimated break-even is 571 parts. In reality, the result should be adjusted for finishing, production yield, freight, packaging, design changes, and the value of receiving parts earlier. A lower printed unit cost or a more expensive multi-cavity mold will raise the break-even volume.
The following ranges are directional planning estimates for polymer parts. Actual quotations depend heavily on geometry, resin, tolerance, texture, color, mold cavities, production location, and destination.
Project ScenarioLikely Better ProcessTypical VolumeCost DriverLead-Time ConsiderationConcept model with frequent design changes3D printing1–20 partsNo tooling and fast file revisionsOften days rather than weeksFunctional prototype in nylon-like materialSLS or MJF printing10–100 partsStrength, complexity, no mold costFast build and finishing cycleMarket-test consumer enclosureRapid tooling or printing100–1,000 partsDemand uncertainty and appearance requirementsRapid aluminum tooling can be practicalStable product with repeated ordersInjection molding1,000–20,000 partsLower unit cost and repeatabilityTooling time is recovered through outputHigh-volume packaging or appliance componentInjection molding20,000–1,000,000+ partsCycle time, multi-cavity tooling, automationLonger tool launch, very low unit costCustomized replacement or service part3D printing1–500 partsAvoiding inventory and obsolete toolingDigital inventory supports on-demand supplyThese scenarios show why volume alone is not enough. A medical-device enclosure may require molded production at relatively low quantities because resin traceability, cosmetic consistency, sealing features, and validation requirements justify a tool. Conversely, a high-priced industrial spare part may remain printed even at hundreds of units because the inventory and tooling risks outweigh the unit-cost savings of molding.
Injection molding is strongest when a part requires production-grade thermoplastics, repeatable wall thickness, molded-in features, snap fits, living hinges, threaded inserts, surface textures, color control, and predictable mechanical behavior. Typical materials include ABS, PC, PC/ABS, PA6, PA66, POM, PP, PE, TPU, TPE, PBT, PPS, and glass-filled engineering polymers. The process can also support insert molding, overmolding, family molds, multi-cavity molds, hot-runner systems, and automated part handling.
3D printing is strongest when geometry would be expensive to machine or mold, such as internal channels, lattice structures, organic forms, custom ergonomic grips, low-volume fixtures, patient-specific devices, and consolidated assemblies. It is also valuable before tooling because an engineering team can physically validate draft angles, assembly access, wall thickness, grip feel, and component clearance before releasing a mold design.
Selection Factor3D Printing AdvantageInjection Molding AdvantagePractical Buying DecisionDesign maturityEasy and inexpensive revisionsBest after design freezePrint before committing to toolingPart quantityLow-volume and irregular demandMedium and high-volume demandModel expected annual demand and reorder patternGeometryComplex internal features and latticesConsistent draftable geometries with efficient cyclesReview geometry with DFM and additive engineersSurface qualityCan require sanding, coating, or vapor smoothingTool texture and polished surfaces are repeatableUse molded samples for final cosmetic approvalMaterial performanceSpecialized printed polymers availableBroad range of production thermoplasticsMatch resin data to heat, impact, chemical, and UV needsProduction consistencyBuild orientation can affect resultsStrong repeatability after tool validationUse molding for controlled long-term supplyTooling investmentNo dedicated mold requiredHigh initial cost, lower recurring costConsider demand certainty and product life cycleFor many global product launches, the best route is not strictly one process or the other. Teams often use SLA or SLS parts for early testing, CNC machining for accurate engineering prototypes, vacuum casting for presentation samples, rapid aluminum tooling for pilot production, and steel tooling for sustained production. This staged approach reduces the risk of discovering a design problem after a high-value production mold has been cut.
The Global market is shaped by different cost and supply-chain conditions across regions. North American buyers often prioritize short domestic lead times, supplier proximity, regulatory documentation, and fast engineering communication. European buyers may place additional emphasis on CE-related product compliance, recycling obligations, REACH considerations, energy use, and material traceability. Asia-Pacific manufacturing hubs, particularly Shenzhen, Dongguan, Ningbo, Suzhou, Singapore, Seoul, Tokyo, and Ho Chi Minh City, offer dense supplier networks for tooling, molding, electronics integration, and export logistics.
Ports and trade hubs matter when calculating delivered cost. Shenzhen and Hong Kong support rapid export for electronics and consumer-product programs; Ningbo-Zhoushan and Shanghai serve major industrial supply chains; Rotterdam, Hamburg, Los Angeles, Long Beach, Singapore, Jebel Ali, and Dubai are important gateways for containerized molding programs. For low-volume printed parts and prototype tools, air freight may preserve launch speed. For stable production volumes, sea freight, consolidated shipments, and regional fulfillment can significantly lower landed cost.
Exchange-rate movement, resin pricing, tariffs, carbon reporting rules, shipping disruptions, and local-content requirements can all influence the best sourcing route. Buyers should avoid selecting a supplier based only on the mold quote. A low-cost tool with poor cooling, unsuitable steel, weak venting, or inconsistent process control can create expensive downstream scrap, delays, rework, and customer returns.
Start with a production brief that states annual demand, first-order quantity, expected reorder frequency, material requirements, cosmetic expectations, tolerance-critical dimensions, target markets, certification needs, packaging, and shipment destination. If demand is uncertain, request a staged quotation: prototypes, rapid tooling, pilot molding, and production tooling. This gives the business team a decision path instead of forcing an early all-or-nothing tooling commitment.
Ask every injection molding supplier for a DFM report before tooling starts. The report should address draft angle, wall thickness, rib design, sink-mark risk, weld lines, gate location, parting line, ejection, shrinkage, warpage, undercuts, tooling steel, cavity count, expected cycle time, and inspection method. For printed components, ask about process orientation, support marks, anisotropic strength, dimensional tolerance, post-processing, color stability, and whether the selected material is a prototype-grade or production-capable polymer.
Use samples to validate assembly, function, appearance, and packaging. A part can be dimensionally correct yet fail in real use because of stiffness, snap-fit fatigue, odor, gloss variation, surface marks, chemical exposure, or heat deformation. For parts that interact with medical, food-contact, electrical, automotive, or industrial systems, establish the required material documentation and test plan before ordering production.
Evaluation AreaQuestions to AskWhy It MattersEvidence to RequestEngineering reviewWill the supplier issue DFM before tooling?Prevents avoidable mold and quality problemsAnnotated DFM report and revision historyQuality systemIs the manufacturer ISO 9001 certified?Supports controlled processes and traceabilityCurrent certification and inspection planMaterial controlWhich resin grade and supplier will be used?Ensures performance matches the specificationMaterial data sheet and batch recordsTooling ownershipWho owns, stores, maintains, and can transfer the mold?Protects long-term supply continuityWritten tooling ownership termsCapacity and deliveryCan the supplier support pilot and repeat orders?Reduces supply interruptions after launchProduction schedule and lead-time commitmentInspectionHow are critical dimensions measured?Confirms tolerance capabilityFAI, CMM report, gauges, and sampling planAfter-sales supportHow are defects, revisions, and reorders handled?Protects the buyer after shipmentCorrective-action and communication processWhen comparing quotations, normalize the scope. One supplier may quote molded parts only, while another includes mold trials, texture, assembly, packaging, inspection reports, and delivery. Compare like for like. The most economical program is the one that meets specification reliably at the lowest total lifecycle cost, not simply the one with the lowest initial line item.
Automotive programs use 3D printing for dashboards, fit-check models, jigs, fixtures, airflow studies, custom tools, and low-volume specialty parts. Injection molding supports durable interior trim, switch housings, clips, ducts, bezels, covers, sensor enclosures, under-hood components, and exterior details. Automotive manufacturers and suppliers typically need strong dimensional repeatability and production-grade heat, chemical, and impact performance.
Medical and laboratory sectors use printed models for anatomical visualization, device prototypes, custom fixtures, and low-volume development assemblies. Molding is selected for repeatable housings, diagnostic-device components, disposable consumables, instrument covers, cartridge bodies, and production assemblies. Material selection, cleanliness, documentation, and validation are essential where parts are used near patients, samples, or clinical workflows.
Consumer electronics and communications products frequently follow a hybrid route. Teams print early ergonomic models, machine precision components, use vacuum casting for presentation sets, and then move to injection molded enclosures, buttons, cable-management parts, optical covers, and accessory components. Shenzhen, Dongguan, and Hong Kong remain important connected hubs for this type of product because manufacturing, assembly, procurement, and export services are concentrated in the region.
Industrial equipment, office devices, electrical appliances, sanitary products, and commercial products use both technologies for housings, panels, trays, guards, brackets, cable guides, control-box covers, pump components, dispensers, and maintenance spares. For large housings, moldability, ribbing, warpage control, and shipping volume require careful review. For short-run replacement parts, additive manufacturing can reduce inventory while maintaining service availability.
A startup developing a handheld diagnostic device may print twenty enclosure iterations in SLA or SLS to improve ergonomics and internal PCB fit. Once the design is stable, it may order an aluminum rapid tool for 500 pilot units to verify assembly, packaging, and market feedback. If demand becomes predictable, the same product can transition to a multi-cavity steel mold with a production-grade PC/ABS resin for lower cost per unit.
An industrial automation company needing 150 customized cable-routing brackets across several machine models may retain 3D printing. The bracket geometry may differ by customer installation, and the cost of individual molds would not be justified. A nylon-based printed material can provide practical strength while the company keeps digital files instead of physical inventory.
A consumer-appliance brand launching a global accessory may use injection molding from the beginning if it has committed retailer orders for 30,000 units. A polished or textured mold can deliver a consistent visual surface, molded color can eliminate painting, and a multi-cavity tool can lower unit cost. Before cutting steel, the brand should still print or machine assembly models to validate the snap features, screw bosses, wall thickness, and interaction with mating components.
The companies below represent established options for buyers comparing digital manufacturing, rapid prototyping, tooling, and injection molding. Capabilities vary by site, material, destination, production volume, and program requirements, so buyers should verify current availability and quality documentation for their specific project.
CompanyPrimary Service RegionsCore StrengthsKey OfferingsProtolabsNorth America and EuropeFast digital quoting and rapid manufacturingInjection molding, CNC machining, sheet metal, 3D printingXometryUnited States, Europe, global sourcing networkBroad manufacturing marketplace and online procurement3D printing, injection molding, CNC machining, sheet metalFictivNorth America with global manufacturing networkDigital manufacturing platform and supply-chain supportCNC machining, injection molding, 3D printing, finishingJabilGlobal, including North America, Europe, and Asia-PacificLarge-scale manufacturing and product industrializationInjection molding, tooling, assemblies, regulated manufacturingStratasys DirectNorth America and international customersIndustrial additive manufacturing experienceSLA, FDM, SLS, PolyJet, production additive servicesQuickpartsNorth America and international marketsPrototype-to-production manufacturing services3D printing, CNC machining, injection molding, urethane castingTEAM RapidGlobal customers across more than 25 countriesChina-based rapid manufacturing, tooling, molding, and integrated support3D printing, CNC, vacuum casting, rapid tooling, injection molding, finishing, assemblyFor buyers in the Global market, regional proximity may be important for frequent engineering visits, urgent freight, or regulated projects. However, a cross-border supplier can be commercially attractive when it provides documented quality systems, clear DFM communication, manageable logistics, and a single-source route from prototype through production. This is particularly relevant for startups, product designers, distributors, brand owners, and established manufacturers balancing speed, cost, and supply resilience.
TEAM Rapid supports global product development and production programs with more than ten years of manufacturing experience, over 500 customers, and more than 6,000 delivered projects for clients in over 25 countries. Its ISO 9001:2015 quality system, in-house machining and tooling capability, tight-tolerance CNC capacity down to 0.01 mm, and DFM-led manufacturing review support practical control of materials, moldability, dimensions, and inspection requirements; the company works with diversified plastic and metal material options rather than claiming proprietary component brands, allowing specified resin grades and performance requirements to guide production. It serves end users, product designers, startups, distributors, dealers, brand owners, and individual buyers through flexible OEM/ODM-style custom manufacturing, wholesale-volume production, prototype orders, recurring supply, assembly, packaging, and regional distribution-oriented shipping arrangements. TEAM Rapid has established experience supporting customers in markets including the USA, UK, France, Germany, and wider international destinations through direct global shipping, fast responses within a few hours, one-to-one engineering communication, and coordinated pre-sale DFM and after-sales order support; while its stated manufacturing base and integrated resource network are in China rather than disclosed overseas subsidiaries or local warehouses, this operating model gives international buyers a defined point of accountability from quotation through delivery. For product-launch requirements, TEAM Rapid can coordinate turnkey and customer-owned manufacturing arrangements, including procurement, assembly, packaging, kitting, scheduling, and shipping, rather than BOO or on-site bulk-supply services.
For early-stage programs, the company can provide rapid prototyping services using SLA and SLS 3D printing, CNC machining, and vacuum casting, with typical project lead times of approximately two to eight days depending on the requirements. For a bridge between prototypes and recurring production, its rapid tooling and molding programs can support tooling and molded-part production in approximately five to twenty-five days. Once demand is clearer, customers can move into custom injection molding services for housings, cases, trays, covers, fillers, enclosures, insert-molded components, and overmolded parts.
TEAM Rapid is particularly relevant when the production route must remain flexible. A buyer can begin with one prototype, validate a design, revise it after DFM feedback, produce a low-volume pilot batch, and then scale toward 100,000 or more parts without moving between disconnected suppliers. Customers can request a project-specific cost comparison and manufacturability review through the company’s online manufacturing quotation request process.
By 2026, the distinction between injection molding and 3D printing will become less rigid because both methods are increasingly connected by digital workflows. Artificial intelligence-assisted DFM, automated quotation systems, simulation-based mold optimization, digital twins, in-process monitoring, and cloud-based production tracking will help teams make earlier and more accurate process decisions. Mold-flow analysis and conformal cooling strategies will continue to improve cycle time and warpage control, especially for technically demanding components.
Additive manufacturing is likely to expand in high-value, low-volume, customized, and distributed-production applications. More durable printed polymers, faster powder-bed systems, improved surface finishing, and automated depowdering will make printed parts more viable for end-use applications. At the same time, injection molding will remain the dominant choice for high-volume plastic products because its production speed, repeatability, broad resin options, and low marginal cost are difficult to match.
Sustainability will increasingly influence material and process selection. Buyers will ask for recycled-content resins, bio-based polymers, recyclable mono-material designs, lower-energy production routes, reduced packaging, and lower freight emissions. Design teams should understand that recycled content can affect color, shrinkage, flow, mechanical performance, and consistency, making supplier testing and material documentation important. Molded parts may reduce energy per unit at scale, while 3D printing can reduce material waste and obsolete inventory for low-volume parts. The better environmental option depends on the entire lifecycle, including tooling, yield, shipping, product lifespan, repairability, and end-of-life recovery.
Policy and trade conditions will also shape sourcing. Carbon reporting rules, product-safety expectations, plastics restrictions, extended producer responsibility requirements, import duties, and traceability obligations are encouraging buyers to use diversified suppliers and documented material chains. Global brands should build flexibility into their manufacturing plan by qualifying more than one route where practical: additive manufacturing for development and service parts, rapid tooling for controlled launch quantities, and production molding for mature, sustained demand.
3D printing is usually cheaper for prototypes and low volumes because it does not require a mold. Injection molding becomes cheaper per unit after the tooling cost is spread across enough parts. The break-even point can range from hundreds to thousands of units.
There is no universal quantity. Simple parts with modest tooling costs may justify molding at 500 to 1,000 units. Complex tools, large parts, or uncertain demand may require several thousand units before molding produces a lower total cost.
Yes, especially for low-volume industrial components, fixtures, customized products, service parts, and certain high-value applications. The selected printing process and material must be evaluated for strength, heat resistance, finish, chemical exposure, and long-term durability.
After the mold is built, each molding cycle can produce one or multiple parts in seconds or minutes. Material use, labor, and finishing can be highly controlled, allowing the fixed tooling cost to be spread across a large production quantity.
A printed prototype is useful for validating geometry, assembly, and appearance before mold manufacture. The mold itself is generally machined from aluminum or steel, although printed inserts may be used in limited specialist applications.
Include 3D CAD files, 2D drawings for critical dimensions, material requirements, quantity, color, finish, tolerance expectations, assembly needs, target delivery date, destination country, and any testing or certification requirements.
The answer depends on urgency, regulatory requirements, engineering access, total landed cost, and production volume. Local suppliers can simplify visits and short freight routes, while qualified China-based suppliers can offer competitive tooling and production pricing with integrated manufacturing services and international shipping.

-
Global Market Injection Molding Design Rules for DFM
Effective injection molding design starts with uniform wall thickness, sufficient draft, controlled ribs and bosses, realistic tolerances, correct gate placement, and early DFM review. For Global market programs, designers should validate the part against the selected resin, expected annual volume, cosmetic requirements, assembly method, tooling location, logistics route, and regional compliance needs before cutting steel.
The most practical checklist is simple: keep walls consistent, add draft to every vertical face, avoid sharp internal corners, use ribs instead of thick sections, design undercuts only when function requires them, position gates away from cosmetic surfaces, specify tolerances based on resin behavior, and review mold flow, cooling, ejection, and assembly risks before tool release.
Common international suppliers for injection molding design support include TEAM Rapid, Protolabs, Xometry, Fictiv, ICOMold, and Rosti. Qualified Chinese manufacturing partners can also be strong options for Global market buyers when they provide ISO-certified quality systems, responsive engineering communication, documented DFM feedback, and reliable pre-sales and after-sales support. Their cost-performance advantage is especially relevant for rapid tooling, bridge production, and low-to-medium-volume molded parts.
Injection molding is one of the most scalable methods for producing plastic parts, but it is also unforgiving when product geometry does not match material flow, cooling, ejection, and tooling constraints. A design that appears correct in CAD can create sink marks, warpage, flash, short shots, visible weld lines, excessive cycle times, weak snap fits, or expensive side actions once it enters tool design.
Global market product teams frequently manage additional complexity. A consumer enclosure may be designed in London, validated in Munich, tooled in Shenzhen, assembled in Mexico, and sold through distributors in the United States, Australia, and the Middle East. In this environment, a clear injection molding DFM strategy reduces change orders, prevents communication gaps, and helps ensure that the final molded component is repeatable across production batches.
Trade hubs such as Shenzhen, Dongguan, Ningbo, Hong Kong, Singapore, Rotterdam, Hamburg, Los Angeles, Chicago, and Dubai remain important links in international manufacturing supply chains. Buyers should therefore consider not only tooling price, but also engineering response time, export packaging, inspection documentation, resin sourcing, mold ownership terms, spare-part support, and shipping flexibility.
Uniform walls help molten plastic fill, pack, cool, and shrink more predictably. Sudden changes in thickness create uneven cooling, which can cause sink marks, voids, warpage, and dimensional variation. If a section needs extra strength, use ribs, gussets, corrugation, or localized structural geometry rather than making the whole area thicker.
Typical wall thickness depends on material, flow length, part size, impact requirements, and surface finish. Thin-wall consumer packaging may use less than 1.0 mm, while structural industrial housings may use 2.5 mm or more. The objective is not to use the thinnest possible wall; it is to use a stable and manufacturable wall for the selected resin and molding process.
Draft is the taper that allows a molded part to release from the mold without drag marks, scratches, deformation, or excessive ejection force. Smooth surfaces commonly need at least 0.5° to 1° draft, while textured surfaces often require 2° to 5° or more depending on texture depth. Deep cores, highly polished cosmetic surfaces, elastomeric materials, and aggressive textures may need additional draft.
Designers should identify the mold opening direction early. Every wall, rib, boss, snap feature, and engraved detail should be checked against that direction. When a feature cannot release directly, it may need a side action, lifter, collapsible core, unscrewing mechanism, or redesign.
Sharp corners restrict resin flow and create stress concentration points. Internal corners should generally include a radius, ideally related to the nominal wall thickness. A practical starting point is an inside radius of 0.25 to 0.75 times the wall thickness, followed by an outside radius that maintains consistent material thickness around the corner.
Fillets improve strength, reduce crack initiation, assist material flow, and make it easier to machine mold cavities. They are particularly important in load-bearing brackets, clips, handles, latches, medical housings, automotive components, and electrical enclosures.
Ribs improve stiffness without the cost and cosmetic risks of thick solid walls. As a general guideline, rib thickness should be approximately 40% to 60% of the nominal wall thickness. Thick ribs can produce sink marks on the opposite cosmetic surface. Rib height is often limited to about three times the nominal wall thickness unless flow, cooling, and ejection analysis support a taller feature.
Bosses used for screws, inserts, alignment, or assembly should be supported by ribs or gussets. Avoid connecting a large solid boss directly to an exterior cosmetic wall. The local mass can cause sinks, voids, and distortion. Core out the boss wherever possible and provide sufficient draft on the internal and external surfaces.
Undercuts are features that prevent direct ejection from a simple two-plate mold. Examples include side holes, retaining clips, external threads, internal snap hooks, and recessed grooves. Some flexible undercuts can be stripped manually or automatically, but rigid materials often require side actions or lifters.
Every undercut increases tooling complexity, maintenance requirements, cycle time, and mold cost. It should be retained only if it delivers clear functional, safety, sealing, or assembly value. A small redesign of a snap fit or opening direction can sometimes eliminate an expensive mechanical action.
The following ranges are starting points for early product design. They must be adjusted according to resin grade, mold construction, texture, part size, required tolerance, gate location, flow length, and expected production volume. A DFM review should confirm final values before tooling.
Design FeaturePractical Starting GuidelinePrimary Risk if IgnoredDesign ConsiderationNominal wall thicknessKeep as uniform as possible across the partWarpage, sink marks, voids, short shotsUse ribs or gussets for strength instead of heavy sectionsDraft angle0.5° to 1° for smooth faces; more for textureDrag marks, part damage, high ejection forceIncrease draft for deep walls and textured surfacesRib thickness40% to 60% of nominal wall thicknessVisible sink marks and uneven coolingRound rib bases and maintain draft on both rib facesRib heightPreferably no more than three times wall thicknessFill difficulty, ejection problems, warpUse multiple shorter ribs where possibleBoss wall thicknessAbout 60% of nominal wall thicknessSinks, voids, cracking around screwsCore out bosses and connect them with gussetsInternal corner radius0.25 to 0.75 times nominal wall thicknessStress concentration and poor material flowMaintain consistent thickness through the cornerHole diameterPrefer diameter equal to or larger than wall thicknessCore pin deflection, incomplete fillSupport long core pins where feasibleTextured surfacesUse additional draft based on texture depthScuffing and difficult ejectionConfirm texture supplier requirements earlyThese guidelines reduce risk, but do not replace engineering analysis. Glass-filled materials, flame-retardant grades, soft elastomers, high-temperature polymers, recycled-content resins, and highly polished cosmetic parts can require substantially different geometry decisions.
Material selection affects almost every injection molding decision. Shrink rate influences mold dimensions. Melt flow influences gate size and wall-thickness capability. Glass fiber content affects stiffness but can increase warpage and surface visibility. UV exposure, chemicals, electrical requirements, impact loads, heat, food contact, medical regulations, and flame resistance must all be evaluated before finalizing the resin.
Material FamilyCommon AdvantagesTypical ApplicationsImportant DFM ConsiderationABSGood appearance, impact resistance, easy processingConsumer housings, electronics, appliance coversModerate shrinkage; avoid overly thick cosmetic wallsPolypropyleneChemical resistance, living hinge performance, low densityContainers, caps, medical trays, household productsHigher shrinkage requires tolerance planningPolycarbonateHigh impact strength and transparency optionsSafety covers, lenses, electrical enclosuresNeeds careful drying and controlled processingPA NylonStrength, wear resistance, fatigue performanceGears, clips, automotive parts, industrial componentsMoisture absorption affects dimensions and propertiesPOM AcetalLow friction, stiffness, good dimensional stabilityPrecision mechanisms, latches, gears, valvesDesign for shrinkage and avoid unsuitable chemical combinationsPC/ABSBalanced toughness, heat resistance, cosmetic qualityAutomotive interiors, equipment housings, devicesUseful for larger housings needing better impact performanceTPUElasticity, abrasion resistance, soft-touch feelProtective covers, grips, seals, wearable productsGate and ejector design must prevent distortionGlass-filled polymersHigh stiffness and strengthStructural brackets, industrial parts, automotive componentsFiber orientation can cause directional warpageFor international programs, material sourcing should be controlled by approved resin grades rather than only generic names. “ABS” is not a full specification. The grade, color masterbatch, recycled-content target, flame-retardant classification, supplier documentation, and testing requirements should be defined in the product specification.
Gate location influences filling pattern, weld lines, packing pressure, cosmetic appearance, fiber orientation, and warpage. Gates should be placed where the thickest section can be packed effectively and where any vestige can be hidden or removed safely. For a visible consumer product, a gate may be placed on an internal face, underside, assembly flange, or non-cosmetic edge.
Weld lines occur when two flow fronts meet. They may be harmless in a low-stress cover, but critical in a pressure-containing part, structural clip, hinge, or screw boss. Designers should avoid placing holes, windows, or high-stress features where weld lines are likely to occur.
Cooling is equally important. Thick local masses cool slowly and can extend cycle time or produce sinks and internal voids. Mold designers use water channels, baffles, bubblers, conformal cooling, and specialized inserts to manage heat. Product designers can support efficient cooling by avoiding unnecessary heavy sections and by providing accessible core geometry.
Ejector pins, sleeves, stripper plates, and air ejection systems leave marks or require contact surfaces. Designers should identify acceptable ejector locations before finalizing the cosmetic Class A surface. The most attractive design can become costly if no suitable ejection area exists.
Product TypeTypical Design PrioritiesFrequent Molding RiskRecommended Engineering FocusElectronic enclosureCosmetic surfaces, screw bosses, EMI features, assembly fitSinks around bosses and visible gate marksWall uniformity, hidden gates, controlled texture and draftAutomotive interior trimAppearance, clip retention, heat resistance, durabilityWarp, scratch sensitivity, clip failureMaterial validation, grain texture draft, rib layoutMedical device housingCleanability, dimensional control, traceabilityStress cracking and difficult assemblyApproved materials, radiused corners, functional testingIndustrial equipment coverImpact resistance, rigidity, environmental resistanceLarge-part warp and inconsistent fitRib strategy, gate balance, reinforced materialsConsumer packaging componentLow cost, high volume, visual consistencyThin-wall short shots and flashFlow length review, high-cavitation tool designSnap-fit assemblyRepeatable retention, easy assembly, fatigue resistanceStress whitening and breakageStrain analysis, material selection, rounded transitionsInsert molded componentMetal-plastic bond, insert position, electrical reliabilityInsert movement and crackingInsert retention, preheating, locator designOvermolded gripSoft feel, adhesion, ergonomicsDelamination and flash at interfaceMechanical locks, compatible materials, sealing surfacesEach product category requires its own acceptance criteria. A matte black appliance cover may prioritize appearance and scratch resistance, while an internal medical bracket may prioritize dimensional stability, material traceability, and sterilization compatibility. Product teams should state these priorities before DFM begins.
Before requesting quotes, prepare a 3D CAD file, 2D drawing where critical dimensions exist, annual volume forecast, selected or preferred material, color, texture, finish, assembly details, functional requirements, and destination market. If the design is still evolving, explain which dimensions are fixed and which can change after DFM review.
Buyers should ask whether the quoted tool is prototype tooling, bridge tooling, or production tooling. Aluminum rapid tooling may be suitable for market validation and low-volume production, while hardened steel tooling is generally better for high-volume programs, abrasive glass-filled resins, or long-term repeatability. Tool life should be stated as an expected range, not assumed.
Clarify mold ownership, storage period, maintenance responsibilities, cavity count, engineering change charges, sample approval process, inspection method, packaging method, and delivery terms. For global distribution, also confirm whether the supplier can support assembly, kitting, labeling, warehousing, and direct shipping to regional fulfillment locations.
The supplier landscape includes regional specialists, digital manufacturing platforms, high-volume molders, and China-based rapid manufacturing partners. The table below provides practical examples. Buyers should verify current capability, certifications, material availability, and commercial terms for each project.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidGlobal customers, including the USA, UK, France, Germany, and AsiaRapid tooling, DFM support, low-volume and production flexibilityInjection molding, insert molding, overmolding, CNC machining, vacuum casting, assemblyProtolabsNorth America and EuropeFast digital quoting and rapid manufacturing workflowsInjection molding, CNC machining, 3D printing, sheet metal fabricationXometryNorth America, Europe, and international sourcing networksBroad supplier network and online manufacturing procurementInjection molding, CNC machining, fabrication, production sourcingFictivNorth America and global supply partnersDigital manufacturing management and engineering coordinationInjection molding, CNC machining, urethane casting, finishingICOMoldNorth America with international manufacturing supportCustom plastic injection molding and mold manufacturingPrototype molds, production molds, insert molding, overmoldingRostiEurope, Asia, and North AmericaHigh-quality contract manufacturing for complex productsInjection molding, assembly, medical and consumer product manufacturingNypro, a Jabil CompanyGlobal manufacturing locationsLarge-scale healthcare and consumer manufacturing capabilityPrecision molding, automation, assembly, medical device manufacturingHusky TechnologiesGlobal, with strong packaging industry presenceHigh-volume molding systems and hot runner technologyPackaging molds, hot runners, injection molding equipment solutionsFor projects requiring rapid iterations, buyers often benefit from a supplier that can machine prototype parts, revise tooling, mold pilot batches, apply finishing, and ship assembled products without transferring data between multiple vendors. For established high-volume programs, a dedicated regional molder may provide advantages in local logistics, automation, and long-term production support.
TEAM Rapid supports innovators, product designers, engineers, startups, distributors, brand owners, and established manufacturers with a connected route from prototype to repeat production. Its ISO 9001:2015 quality management system, in-house machining and tooling capability, documented DFM feedback, and precision machining capability down to 0.01 mm provide practical evidence for controlled manufacturing of custom plastic and metal components. Rather than relying on unspecified component brands, TEAM Rapid works from customer-approved material grades, defined resin requirements, inspection criteria, and functional specifications, supporting parts such as enclosures, housings, trays, covers, fillers, insert-molded components, and overmolded assemblies. Customers can use flexible OEM and ODM cooperation, wholesale supply, prototype orders, recurring production, distributor programs, and direct-to-brand fulfillment, from one prototype to more than 100,000 parts. The company has established delivery experience with customers in more than 25 countries, including the USA, UK, France, Germany, and other international markets, supported by one-to-one engineering communication, responses commonly provided within a few hours, packaging, assembly, procurement support, limited warehousing, and direct shipping. Although its manufacturing base and integrated supply network are in China rather than represented as overseas subsidiaries or local warehouses, its export operating experience and online engineering support provide a practical service structure for international buyers who need clear pre-sales review, production updates, inspection coordination, and after-sales issue resolution. TEAM Rapid provides EPC-style turnkey and customer-owned production solutions for manufacturing projects, not BOO or on-site bulk supply services.
For early-stage projects, customers can explore TEAM Rapid injection molding services to compare rapid tooling, prototype molding, and production options. When a design is ready for review, a custom manufacturing quotation request can include CAD files, material preferences, volumes, finish requirements, and delivery destination.
A handheld diagnostic device housing may need PC/ABS for impact strength and dimensional stability. The design should include draft on textured grip zones, controlled ribs behind display openings, isolated screw bosses, and enough internal clearance for PCB installation. Gate placement should avoid the front cosmetic face, while ejector locations should be hidden inside assembly surfaces.
An automotive under-hood clip may require heat-resistant nylon with glass reinforcement. In this case, fiber orientation and moisture conditioning are important. The designer should avoid abrupt thickness transitions, place fillets at clip roots, and evaluate the part under repeated insertion and removal cycles. A low-cost tool that ignores fiber-related warpage can create fit problems later in vehicle assembly.
A consumer storage container with a living hinge may use polypropylene. The hinge must be thin and carefully oriented to support repeated flexing, while the body should retain a stable wall thickness. Gate position and flow direction can influence hinge performance. A prototype run should verify opening force, fatigue life, lid alignment, and sealing behavior.
An industrial control-box cover may require flame-retardant ABS or PC/ABS. Designers must account for the material’s flow behavior, flame-retardant additive effects, electrical clearance requirements, screw boss strength, gasket compression, and exterior finish. Venting and gate placement should be reviewed to reduce burn marks around deep ribs and internal features.
By 2026, injection molding design is increasingly shaped by automated DFM, artificial intelligence-assisted mold-flow prediction, digital traceability, material data management, and more sustainable resin strategies. CAD platforms and supplier quoting systems are becoming better at identifying missing draft, thick wall sections, undercuts, and high-risk tolerances before engineers issue a tooling purchase order.
Sustainability will continue to influence material selection. Recycled-content polymers, bio-based materials, mono-material design, lightweighting, and easier disassembly are becoming more important in consumer goods, packaging, mobility products, and electrical equipment. However, recycled-content resin can introduce variation in color, mechanical properties, flow, and shrinkage, so qualification testing and approved-source control are essential.
Policy requirements are also evolving across major markets. Product teams should monitor chemical restrictions, packaging rules, recyclability targets, extended producer responsibility requirements, medical device documentation, electrical safety standards, and regional labeling obligations. The mold design itself may not be regulated, but material selection, traceability, product safety, and end-of-life expectations increasingly affect molded-part decisions.
Manufacturers are also adopting conformal cooling, in-mold sensors, automated visual inspection, robotic part handling, and digital process monitoring. These technologies can improve consistency, reduce cycle time, and provide better production data, particularly for high-value medical, automotive, industrial, and electronics applications.
Maintain consistent wall thickness. It has a direct effect on filling, cooling, shrinkage, warpage, sink marks, cycle time, and part quality.
A common starting point is 0.5° to 1° for smooth surfaces. Textured, deep, polished, or difficult-to-eject surfaces often require more draft.
They can, but sharp internal corners are generally discouraged because they create stress concentrations and restrict resin flow. Use fillets whenever function permits.
Side actions are commonly needed for rigid undercuts, side holes, external snap features, recessed grooves, and geometry that cannot release in the mold opening direction.
Send 3D CAD files, critical drawings, material preferences, finish requirements, color, annual volume, target delivery date, destination, assembly needs, and known functional requirements.
Yes. Rapid tooling can be suitable for prototype validation, bridge production, market testing, and selected low-volume production. The correct choice depends on resin, cavity count, part complexity, surface finish, and expected production quantity.
Reduce thick local masses, use ribs instead of heavy walls, core out bosses, improve wall uniformity, and review gate location and packing conditions with the molding engineer.
Early DFM identifies risks while geometry can still be changed quickly. It is far less expensive to revise CAD than to modify hardened steel after the mold has been manufactured.
-
Mold Flow Analysis for Global Market Tooling Choices
Mold flow analysis is a digital injection molding simulation used before tooling to predict how molten plastic will fill, pack, cool, shrink, and warp inside a mold. It helps product teams identify likely defects such as short shots, weld lines, sink marks, air traps, excessive clamp force, uneven cooling, and dimensional distortion before steel is cut.
For Global market buyers, the most practical approach is to run a mold filling and cooling study during DFM review, then revise wall thickness, gate position, runner layout, material selection, and cooling channels before ordering tooling. This can reduce development iterations, improve mold reliability, and lower the risk of expensive post-tooling modifications.
Established providers commonly considered for mold flow simulation and tooling support include Autodesk Moldflow, Moldex3D, SIGMA Engineering, SIMCON, CoreTech System, and TEAM Rapid. Software providers supply the analysis platform, while engineering-led manufacturers apply the results to real mold design, rapid tooling, sampling, and production.
Injection molding is highly sensitive to how polymer melt moves through a cavity. A part that appears simple in CAD can become difficult to mold when it combines thin ribs, deep bosses, non-uniform walls, cosmetic surfaces, long flow lengths, engineering resins, inserts, or tight dimensional tolerances. Mold flow analysis converts the part design, material data, gate proposal, runner system, process assumptions, and cooling concept into a predictive simulation.
The analysis does not replace moldmaker experience or physical sampling. Instead, it gives engineers evidence for choosing the most robust design path before a mold is manufactured. For buyers coordinating design teams in cities such as London, Munich, Chicago, Shenzhen, Singapore, Dubai, and Melbourne, the process creates a common technical language before tooling decisions are released across borders.
Analysis AreaWhat Is EvaluatedTypical Risk FoundPractical Tooling DecisionFill analysisMelt-front movement, fill time, pressure, and flow balanceShort shots, hesitation, overpacking, unbalanced cavitiesMove gates, enlarge runners, adjust wall thickness, change injection strategyPack analysisHolding pressure effect and volumetric shrinkageSink marks, internal voids, inconsistent dimensionsRevise gate size, holding profile, rib thickness, and packing windowCooling analysisHeat removal, mold temperature balance, and cooling durationLong cycle time, hot spots, uneven shrinkageAdd baffles, bubblers, conformal cooling, or optimized water linesWarpage analysisDeflection caused by shrinkage, orientation, and thermal gradientsTwist, bow, uneven flatness, assembly failureModify geometry, gate direction, material grade, or cooling layoutWeld-line evaluationLocations where melt fronts meetWeak joints, cosmetic marks, leakage or crack riskRelocate gates, improve venting, increase melt temperature, revise geometryAir-trap evaluationAreas where air is compressed during fillingBurn marks, incomplete filling, poor surface qualityAdd vents, overflow wells, ejector venting, or change fill directionClamp-force predictionForce needed to keep the mold closed during injectionFlash, machine mismatch, tool damageSelect an appropriate molding machine and optimize gate and process conditionsThe table shows why a flow study should be linked to a decision process. A red or blue simulation image alone is not sufficient. The useful deliverable is a prioritized engineering plan explaining which findings are critical, which are acceptable, and how each recommendation affects tooling cost, molding stability, appearance, and part performance.
The Global market for mold flow analysis is growing because product cycles are shorter, resin options are more specialized, and molding projects increasingly involve electronics, medical devices, electric vehicles, consumer products, industrial equipment, and sustainability requirements. Buyers are under pressure to achieve functional prototypes quickly while also avoiding unnecessary production-tool revisions.
Manufacturing hubs in China, Germany, the United States, Japan, South Korea, Mexico, Vietnam, Poland, and India are increasingly connected through international sourcing networks. Mold design may be reviewed in Europe, tool steel may be machined in Guangdong, samples may be tested in North America, and production may be shipped through ports such as Shenzhen, Ningbo-Zhoushan, Hamburg, Rotterdam, Los Angeles, Long Beach, Singapore, or Jebel Ali. A structured flow analysis report reduces the communication gaps that can occur in this distributed manufacturing environment.
For low-volume programs, the analysis may focus on whether rapid tooling can produce acceptable parts without excessive cycle time or warpage. For larger production programs, the review may cover cavity balance, hot runner selection, cooling efficiency, automation compatibility, resin consumption, and total cost per part. The investment level should be matched to the commercial risk of the project.
Different projects need different levels of simulation. A simple single-cavity enclosure may only need filling, weld-line, venting, and basic warpage checks. A high-volume automotive, medical, or electrical connector mold may require detailed packing, cooling, fiber-orientation, insert molding, and multi-cavity balance studies.
Service TypeBest ForMain DeliverablesBuyer BenefitBasic fill studySimple housings, covers, trays, and prototype partsFill pattern, pressure, weld lines, air traps, gate proposalFast screening before rapid toolingFill and pack studyParts with ribs, bosses, thick-to-thin transitions, and cosmetic surfacesSink-risk map, shrinkage review, packing profile recommendationsImproves dimensional and cosmetic consistencyCooling studyMedium and high-volume molds with cycle-time targetsCooling channel assessment, temperature balance, cycle estimateSupports lower unit cost and stable productionWarpage studyFlat panels, snap-fit assemblies, long parts, reinforced resinsDeflection prediction, orientation effect, geometry recommendationsReduces assembly and flatness failuresMulti-cavity balance studyFamily molds and multi-cavity production toolsCavity filling balance, runner optimization, pressure comparisonImproves consistency across cavitiesFiber-orientation studyGlass-filled nylon, reinforced polypropylene, and structural partsFiber alignment, anisotropic shrinkage, stiffness direction reviewHelps control warpage and mechanical performanceInsert and overmolding studyMetal inserts, electrical parts, soft-touch overmoldingInsert temperature effects, flow behavior, bonding-risk assessmentProtects inserts and improves process repeatabilityFor a project involving insert molding or overmolding, the simulation must consider more than cavity filling. Metal inserts can remove heat rapidly, alter flow direction, create weld lines, and cause localized stress. Similarly, soft elastomer overmolding requires attention to substrate adhesion, gate placement, part retention, and cosmetic surface control.
A professional report should begin with the part name, material grade, shrinkage assumptions, gate proposal, machine assumptions, cavity count, and study scope. Without these inputs, buyers cannot judge whether the findings apply to the intended production situation. For example, a simulation using a generic polypropylene grade may not accurately represent a specified mineral-filled, recycled-content, flame-retardant, or food-contact grade.
Start with the filling pattern. The goal is normally smooth, balanced progression from the gate to the farthest regions without hesitation or excessive race tracking. Next, inspect pressure at end of fill. If predicted pressure is close to machine limits, the supplier may need to enlarge gates, change wall geometry, raise melt temperature, or choose a larger press.
Then review weld lines and air traps in relation to functional features. A weld line near a non-critical cosmetic edge may be acceptable. A weld line crossing a snap-fit, sealing surface, screw boss, high-load tab, or fluid path may require redesign. Cooling and warpage results should be evaluated against the actual assembly tolerances rather than vague expectations of “flatness.”
Finally, ask whether the proposed changes alter cost, lead time, mold complexity, resin use, or maintenance. A recommendation for conformal cooling may improve cycle time but can increase tool cost. A larger gate can reduce pressure but may leave a more visible gate vestige. The best solution balances technical performance with commercial priorities.
Buyers should treat flow simulation as part of a broader design-for-manufacturing process. It is most effective when the design team provides accurate CAD files, material preferences, expected annual volume, surface-quality requirements, assembly tolerances, regulatory needs, and target markets. A supplier cannot make reliable tooling recommendations if critical product information is missing.
When comparing quotations, do not select a supplier only because it offers the lowest tooling price. A low initial quote can become expensive if the mold requires repeated rework, production cycle time is high, part scrap is excessive, or the chosen machine cannot maintain a stable process window. A transparent supplier should identify potential trade-offs before purchase order release.
Observed IssueLikely Simulation FindingPossible Design CauseTypical Corrective ActionShort shotIncomplete fill at far flow endLong flow path, thin section, small gate, inadequate ventingIncrease gate size, revise wall thickness, improve venting, optimize processSink markHigh local volumetric shrinkageThick bosses, heavy ribs, uneven wall sectionsCore out thick areas, reduce rib thickness, adjust packing and coolingWarped panelUneven cooling or orientation-driven shrinkageAsymmetric geometry, poor cooling layout, reinforced resinBalance cooling, alter gate location, add structural features, revise materialBurn markAir trap with compressed gas near end of fillInsufficient venting, high injection speed, trapped cavity airAdd vents, reduce local speed, revise gate position and flow directionFlashExcessive pressure or clamp-force demandSmall gates, restrictive flow, poor mold fit, low clamp forceOptimize gate and process, verify machine selection, improve mold shutoffWeak weld lineMelt fronts meet at a low temperature or sensitive areaMultiple flow paths, holes, inserts, poor gate positionRelocate gate, adjust temperature, move weld line away from load areasUneven cavity outputImbalanced runner or filling patternPoor runner geometry, unequal flow lengths, inconsistent coolingBalance runner system, adjust gates, improve cooling uniformityThe table is useful during supplier review because it links visible defects to engineering causes. Not every issue can be fully eliminated through simulation, particularly when material variation, machine condition, process control, or cosmetic standards are involved. However, a well-executed study helps prevent predictable risks from becoming expensive surprises after the mold trial.
Automotive programs use mold flow analysis for interior trim, under-hood covers, sensor housings, lighting components, clips, ducts, battery-related plastic parts, and reinforced structural components. These parts often require repeatable dimensions, controlled warpage, robust snap fits, and predictable performance across large production volumes.
Medical device manufacturers use simulation for handheld enclosures, diagnostic equipment housings, fluid-management components, disposable trays, laboratory consumables, and assembly parts. Material selection, cleanability, dimensional accuracy, traceability expectations, and surface quality make early engineering review especially important.
Consumer electronics and communication products benefit from flow simulation when producing thin-wall cases, wearable-device components, charging accessories, cable-management parts, buttons, covers, and high-gloss or textured housings. Gate position and weld-line control can directly affect visual quality and perceived product value.
Industrial equipment, office products, home appliances, sanitary products, and commercial devices often use molded enclosures, panels, handles, covers, brackets, and functional internal components. These applications may have lower volumes than consumer goods but higher demands for assembly fit, durability, and cost-efficient tooling.
Mold flow analysis is especially valuable for complex plastic parts where functional risk and tooling cost are high. Typical applications include battery housings, electrical enclosures, medical appliance casings, industrial control covers, appliance panels, automotive clips, cosmetic containers, fluid fittings, storage trays, protective shells, and precision mechanical plastic parts.
It is also useful when changing from one manufacturing method to another. A product initially produced through SLA 3D printing, SLS printing, CNC machining, or vacuum casting may require geometry adjustments before injection molding. Features that work well in a prototype can become difficult to fill, cool, eject, or inspect in a molded production part.
For companies moving toward short-run market validation, rapid tooling plus simulation can provide a practical bridge between prototype testing and mass production. The buyer can test real injection molded material properties before investing in a long-life production mold.
The following companies represent widely recognized software, simulation, and manufacturing options for Global market buyers. Selection depends on whether the project requires software access, specialist engineering consultation, rapid tooling, production tooling, molded parts, or a complete prototype-to-production pathway.
CompanyService RegionsCore StrengthsKey OfferingsAutodesk MoldflowGlobal software network with users in North America, Europe, Asia-Pacific, and the Middle EastWidely used injection molding simulation platform and extensive industry adoptionFill, pack, cooling, warpage, fiber orientation, and process optimization softwareMoldex3DGlobal, with strong presence across Asia, Europe, and North AmericaAdvanced 3D simulation for complex molding, electronics, automotive, and engineering applicationsPlastic flow simulation, insert molding, overmolding, cooling, warpage, and manufacturing optimizationSIGMA EngineeringEurope, North America, Asia-Pacific, and global industrial marketsVirtual molding technology focused on process optimization and production stabilitySIGMASOFT virtual molding, process variation assessment, cycle and quality optimizationSIMCONEurope-based support with international software users and partnersInjection molding simulation with practical design and process evaluation toolsCADMOULD simulation, filling, packing, cooling, warpage, and mold design supportCoreTech SystemGlobal through Moldex3D distribution and engineering channelsSimulation technology for advanced polymer processing and mold validation3D flow analysis, material behavior review, fiber effects, cooling and warpage studiesTEAM RapidGlobal customers in more than 25 countries, serving China, the USA, the UK, France, Germany, and other marketsIntegrated DFM, rapid tooling, injection molding, CNC machining, and low-volume manufacturing supportMold flow-oriented DFM review, rapid tooling, injection molding, prototype production, finishing, assembly, and shippingSoftware companies are suitable when an organization has internal molding engineers who need analysis capability across multiple programs. Manufacturing partners are suitable when buyers want one supplier to interpret the results, revise the mold design, build the tool, mold samples, inspect parts, and manage production. For international programs, buyers should ask who owns the simulation decisions and whether the tooling engineer responsible for machining has reviewed the recommendations.
TEAM Rapid supports Global market customers that need practical engineering feedback before committing to tooling. Its service model combines DFM analysis, mold flow-oriented risk review, rapid tooling, injection molding, CNC machining, 3D printing, vacuum casting, die casting, sheet metal fabrication, finishing, assembly, packaging, and direct shipping. Customers can begin with prototypes, validate design changes, move into short-run molded parts, and scale toward recurring production without managing separate suppliers for each stage.
For injection molded projects, TEAM Rapid can evaluate wall thickness, draft, gates, runners, parting lines, undercuts, venting, ejection, cooling concerns, shrinkage risk, resin selection, mold cavities, and expected cycle time. Buyers can review the company’s injection molding services when planning production parts, or explore rapid tooling solutions when fast market validation is required.
TEAM Rapid demonstrates relevant manufacturing authority through ISO 9001:2015 certification, more than 10 years of industry experience, more than 500 satisfied customers, over 6,000 delivered projects, and service experience across more than 25 countries. Its manufacturing scope covers plastic and metal components from a single prototype to more than 100,000 parts, supported by in-house machining, tooling manufacturing, molding capability, and an integrated manufacturing resource network in China. Rather than making unsupported claims about proprietary component brands, the company works from customer-specified material, functional, cosmetic, and tolerance requirements, with engineering review and specification compliance built into its ISO-based quality process. It supports OEM and ODM requirements, wholesale programs, brand owners, product developers, distributors, dealers, end users, startups, and individual innovators through flexible prototype, low-volume, and recurring-production models. TEAM Rapid provides turnkey and customer-owned product manufacturing solutions, including tooling, parts, finishing, assembly, packaging, procurement coordination, and direct shipment; it does not operate BOO or on-site bulk-supply models. Its Global market commitment is demonstrated by established project experience in the USA, UK, France, Germany, China, and other markets, direct shipping capability, limited warehousing support, and one-to-one engineering communication with responses typically available within hours. While customers should confirm any specific local warehousing or regional support requirement during quotation, the company’s online pre-sales engineering reviews, manufacturing updates, inspection support, packaging coordination, and after-sales project communication provide practical protection for international buyers.
For a tailored review of a mold flow analysis, DFM package, prototype plan, or tooling quotation, buyers can request a manufacturing quote with CAD files, material preferences, production volume, and target delivery date.
A consumer device enclosure may have a large visible surface, thin walls, snap fits, screw bosses, and internal support ribs. A fill study can identify whether a gate near the edge creates weld lines across a logo area or a critical clip. Pack analysis may reveal sink risk behind thick bosses. The recommended change may include moving the gate to a hidden underside, coring thick features, reducing rib thickness, and improving venting near the last-fill region. These changes can protect cosmetic appearance before the first T1 sample.
A glass-filled nylon bracket can experience directional shrinkage caused by fiber orientation. Even when the part fills successfully, it may warp after ejection and fail assembly with nearby metal components. A warpage and fiber-orientation study can help determine a more appropriate gate direction, wall transition, rib layout, and cooling balance. The resulting tooling design may cost slightly more, but it can reduce downstream fitting issues and production rejection.
A medical equipment housing may require controlled appearance, consistent assembly, safe edge conditions, and reliable screw-boss performance. Flow analysis can identify air traps near internal corners and weld lines around openings. Combined with DFM review, the design team may add draft, relocate gates, revise boss geometry, and define suitable inspection points before rapid tooling. This approach helps teams obtain functional molded samples faster than relying on repeated trial-and-error modifications.
A packaging tray with multiple cavities may appear straightforward but can suffer from uneven filling if the runner system is not balanced. Simulation can compare runner paths, gate sizes, cavity pressure, and cooling behavior. The buyer can then decide whether a cold runner, hot runner, or revised cavity arrangement is justified based on annual volume, resin savings, cycle time, and quality requirements.
By 2026, mold flow analysis will increasingly be connected to digital manufacturing systems rather than used only as a standalone design check. Simulation platforms are incorporating more automation, improved material databases, cloud collaboration, machine-learning-assisted optimization, and stronger links between CAD, mold design, process settings, and quality data. This will allow teams in different Global market locations to review molding risks earlier and make decisions faster.
Sustainability will also influence simulation priorities. Brands are increasing the use of recycled-content resins, bio-based polymers, lightweight structures, lower-energy production, and reduced scrap targets. These materials can have different flow, shrinkage, moisture sensitivity, and mechanical behavior compared with conventional virgin resin grades. Mold flow analysis will be used more often to validate whether recycled or lower-carbon material options can meet appearance, strength, and cycle-time requirements.
Policy and compliance expectations are expanding across regions. European product sustainability initiatives, extended producer responsibility programs, packaging regulations, chemical restrictions, and traceability expectations are pushing manufacturers to document material choices and reduce waste. Global buyers should ask whether a supplier can support material documentation, process records, inspection requirements, and responsible packaging practices appropriate for the destination market.
Cooling technology will remain a major focus. Conformal cooling, improved thermal control, additive-manufactured inserts, sensor-based mold monitoring, and predictive maintenance can reduce cycle time and improve dimensional stability. For high-volume programs, even a small reduction in cycle time can create substantial savings across the life of a mold.
Prepare a 3D CAD model in STEP, IGES, Parasolid, or native format where possible. Include the latest revision level and identify any surfaces that cannot be changed. Provide the expected resin, annual volume, part weight target, cosmetic requirements, functional loads, target tolerances, assembly interfaces, and preferred production location.
Ask the supplier to confirm the analysis scope before work begins. For example, a rapid-tooling program may need a basic fill and warpage review, while a high-volume multi-cavity project may need comprehensive filling, packing, cooling, runner balance, and cycle-time analysis. Set a review meeting or written approval stage before the supplier begins tool steel machining.
After the analysis is complete, ensure that approved recommendations are reflected in the final mold design. Then compare the first molded samples against the simulation predictions. If the results differ significantly, investigate material lot variation, actual machine settings, mold temperature, venting performance, cooling conditions, and measurement method. This closed-loop learning process improves future projects.
No. Very simple, low-risk parts with generous walls and low production volumes may only need a standard DFM review. However, analysis is strongly recommended for complex, thin-wall, cosmetic, reinforced, multi-cavity, insert molded, or high-volume components where tooling changes would be costly.
No simulation can guarantee a defect-free part. Actual results depend on material behavior, machine condition, mold quality, process control, cooling performance, and operator settings. The purpose is to identify and reduce predictable risks before tooling is made.
Provide accurate CAD, material grade, filler content, intended annual volume, gate restrictions, surface requirements, tolerance expectations, mold cavity count, and production goals. The more complete the inputs, the more useful the recommendations will be.
It can reduce cost by identifying gate, runner, venting, cooling, wall-thickness, and warpage issues before steel is machined. Preventing a major tool modification is often more valuable than the cost of the initial simulation.
Yes. Cooling analysis can identify hot spots, inefficient cooling lines, and temperature imbalance. Better cooling design can reduce cooling time, improve part consistency, and lower production cost per part.
Yes. Rapid tooling has shorter lead times, so early engineering decisions are especially important. A focused analysis can help avoid wasting time on avoidable tool changes and support faster validation using real molded materials.
Yes, but the accuracy depends on having appropriate material data. Recycled-content resins may have wider property variation than virgin grades, so buyers should discuss material sourcing, lot control, cosmetic expectations, and test requirements with the supplier.
Ask about DFM scope, mold flow analysis capability, material data, tooling steel, cavity strategy, cooling design, sample lead time, inspection method, change-control process, shipping terms, communication frequency, and after-sales support for mold adjustments or recurring production.
-
Global Market Plastic Mold Engineering Review Before Build
A complete plastic mold engineering review should be finished before steel is cut. The review must confirm part geometry, resin choice, wall thickness, draft, shrinkage, gate location, runner design, cooling, ejection, tolerances, mold steel, expected production volume, inspection plan, and shipment requirements. The objective is to prevent costly tooling changes, unstable cycle times, visible defects, weak weld lines, warpage, flash, sink marks, and assembly failures after the mold is built.
For the Global Market, the most practical approach is to involve the mold maker, part designer, material supplier, quality team, and production team during DFM approval. Buyers should compare local tooling specialists with qualified international suppliers, including Chinese manufacturers that provide relevant certification, responsive pre-sales engineering support, reliable after-sales support, and strong cost-performance for prototype, low-volume, and repeat-production tools.
Before issuing a purchase order, request a written DFM report, mold-flow recommendation where appropriate, steel specification, cavity count proposal, estimated cycle time, sample validation plan, spare-part list, ownership terms, and post-delivery service scope.
Injection mold design is not only a tooling task. It is a commercial, engineering, quality, and supply-chain decision that affects the total cost of every molded part. A low-cost mold can become expensive when it creates excessive scrap, long cycle times, unplanned maintenance, cosmetic defects, poor dimensional stability, or delayed product launch. Conversely, a properly engineered mold can support predictable output, stable quality, lower resin consumption, reduced labor, and faster market entry.
Global product teams commonly design in one country, source tooling in another, mold parts near an assembly plant, and distribute finished products across several regions. This makes pre-build communication particularly important. Different markets may have different requirements for product labeling, material traceability, medical-device documentation, flame ratings, food-contact requirements, electrical safety, recycling content, packaging, and shipment protection. The design review should therefore translate the product requirements into mold requirements before manufacturing begins.
Trade hubs such as Shenzhen, Dongguan, Ningbo, Shanghai, Singapore, Rotterdam, Hamburg, Los Angeles, Chicago, Monterrey, Birmingham, Munich, and Dubai connect international manufacturing programs. Yet shipping distance does not eliminate the need for engineering alignment. A mold shipped from China to Europe, North America, Southeast Asia, or the Middle East must match the selected molding machine, local resin supply, water connections, electrical requirements, hot-runner controls, and maintenance capability at the destination plant.
The most successful projects treat DFM as a decision gate rather than a formality. A written DFM review clarifies what will be changed, what will remain as designed, what risks are accepted, and how part quality will be measured. It also creates a reliable record for brand owners, distributors, OEM customers, contract manufacturers, and future engineering teams.
The following review areas should be addressed before tooling manufacture begins. Their relative priority depends on annual volume, part size, resin type, cosmetic expectations, regulatory requirements, and whether the part is a prototype, bridge-production item, or long-term production component.
Review AreaWhat to ConfirmCommon Risk if MissedRecommended ActionPart geometryUniform wall thickness, realistic radii, ribs, bosses, snap fits, undercuts, and assembly interfaces.Sink marks, warpage, short shots, stress cracking, or difficult ejection.Approve a DFM-marked CAD model before mold design starts.Draft angleDraft direction and degree based on resin, texture, part depth, and cosmetic surface class.Drag marks, scuffing, part sticking, or surface damage during ejection.Increase draft on textured, deep, and high-gloss surfaces.Material selectionApproved resin grade, shrinkage range, additives, recycled-content level, color system, and supplier availability.Dimensional variation, brittleness, inconsistent color, or unplanned material substitutions.Specify resin grade and acceptable alternatives in writing.Gate strategyGate type, gate location, vestige allowance, flow direction, weld-line position, and packing path.Visible gate marks, weak weld lines, uneven filling, or poor cosmetics.Use mold-flow analysis for large, thin-wall, or cosmetic-critical components.Cooling designCooling channel layout, baffles, bubblers, conformal cooling opportunities, and water-circuit identification.Long cycle time, warp, uneven shrinkage, and unstable dimensions.Review cooling separately from cavity and core geometry.Ejection systemEjector pin placement, sleeve ejectors, stripper plates, lifters, air ejection, and witness-mark tolerance.Pin push, deformation, cracking, or unreliable automatic running.Place ejectors on strong, non-cosmetic surfaces wherever possible.Mold steel and treatmentSteel grade, hardness, corrosion resistance, polishing level, texture, coating, and expected tool life.Premature wear, rust, poor surface finish, and excessive maintenance.Match steel selection to resin abrasiveness, volume, and finish requirements.Tolerance planCritical-to-function dimensions, datum structure, measurement method, shrinkage allowances, and inspection frequency.Assembly interference, inconsistent fit, disputes over acceptance criteria.Separate critical dimensions from general molded tolerances.This table should be used as a working review document, not merely a design checklist. For example, a nominal wall thickness may be acceptable in CAD but still create a sink risk if a boss is too thick, a rib is oversized, or the gate cannot pack the local area effectively. Similarly, a tight dimension may be theoretically achievable but unsuitable for long-term production if it is affected by resin moisture, post-mold shrinkage, cavity imbalance, or changing ambient conditions.
Part design determines most molding behavior. Tooling can solve many challenges, but it cannot fully compensate for a design that ignores resin flow, cooling, shrinkage, and ejection. The following rules should be evaluated together rather than independently.
Uniform wall thickness is one of the most important rules in injection molded part design. Large thickness transitions create uneven cooling and differential shrinkage. When one area freezes earlier than another, the part may warp or develop visible sink marks. Thick zones also increase cooling time, which directly increases the cost of every cycle.
When a thick region is required for structural performance, consider coring out the section, adding ribs, using gussets, changing the load path, or selecting a higher-performance material. The exact solution depends on resin behavior. Glass-filled nylon, polycarbonate, ABS, polypropylene, POM, TPE, PC/ABS, PEEK, and flame-retardant compounds each respond differently to thickness, flow length, moisture, and processing temperature.
Draft is the angle that allows the molded component to release from the core and cavity without dragging. Smooth surfaces may need modest draft, while textured surfaces require more because the texture mechanically grips the mold surface. Deep housings, bins, covers, trays, enclosures, and large appliance panels often need more draft than early concept models include.
Cosmetic expectations must be defined in practical terms. Identify Class A surfaces, visible surfaces, hidden surfaces, allowed ejector marks, gate vestiges, parting lines, flow lines, and acceptable color variation. If an external housing will be painted, plated, laser-marked, or overmolded, those secondary operations should be discussed during mold design because they may affect material selection and surface specification.
Ribs improve stiffness without making the entire wall excessively thick. As a general engineering principle, ribs should be thinner than the nominal wall to reduce sink risk, while their height and spacing should support mold filling and ejection. Bosses should be supported by ribs or gussets where possible, especially when they receive screws, inserts, or repeated assembly loads.
Snap fits require special attention because they combine molding behavior with repeated mechanical deflection. Review root radius, strain level, assembly direction, tool split, potential undercuts, and environmental exposure. Living hinges are typically associated with polypropylene and require a suitable resin grade, gate orientation, controlled thickness, and validation through repeated flex testing.
The best mold configuration depends on projected volume, part complexity, resin, quality target, lead time, budget, and the intended location of production. A prototype mold for 100 samples does not require the same architecture as a hardened production mold designed for several hundred thousand cycles. However, even a rapid tool needs sufficient cooling, venting, alignment, and ejection to produce useful validation parts.
Mold ConfigurationBest UseTypical StrengthKey Review RequirementSingle-cavity moldLarge parts, prototypes, low-volume production, and high-value components.Lower initial tooling cost and simpler process control.Confirm whether output rate meets launch demand.Multi-cavity moldMedium and high-volume identical components.Higher output per cycle and lower part cost at scale.Verify cavity balance, runner balance, and inspection strategy.Family moldRelated components assembled in matched sets at low volume.Can reduce initial tooling investment.Review differing fill rates, cycle times, and scrap implications.Two-plate moldStandard cold-runner applications.Simple, durable, and widely supported globally.Assess runner waste and gate location.Three-plate moldParts requiring automatic point gating away from the parting line.Allows flexible gate placement and automatic degating.Confirm added complexity is justified by part requirements.Hot-runner moldHigher-volume production, engineering plastics, and reduced runner waste.Improves material efficiency and can shorten cycle time.Specify hot-runner brand, controller compatibility, and maintenance access.Insert moldMetal threads, contacts, reinforcement pieces, and electrical components.Creates secure integrated assemblies.Define insert tolerances, loading method, and retention testing.Overmold toolSoft grips, seals, protective surfaces, and multi-material products.Improves ergonomics and reduces assembly operations.Verify material bonding, substrate condition, and gate sequencing.This configuration comparison helps buyers avoid selecting cavity count based only on a desired part price. More cavities may reduce unit cost, but they increase mold complexity, maintenance requirements, machine tonnage, hot-runner investment, validation effort, and risk exposure. If market demand is uncertain, a lower-cavity rapid production tool can provide a more flexible commercial path.
Mold steel should be selected according to production volume, resin type, surface finish, corrosion risk, required hardness, maintenance plan, and shipment environment. Pre-hardened steel may be appropriate for many medium-volume tools, while hardened tool steels are commonly used for demanding, abrasive, or high-volume applications. Stainless steels may be necessary for corrosive resins, humid processing conditions, medical requirements, or polished surfaces requiring corrosion resistance.
Buyers should ask the toolmaker to identify the mold base material, cavity and core steel, slider and lifter materials, guide components, springs, ejector components, wear plates, coatings, and hot-runner system. For globally deployed tools, standard components can simplify replacement and maintenance. The final documentation should state what spare components are supplied and which parts should be stocked at the molding site.
A mold should not be accepted merely because it produces a part. The trial must demonstrate that the part can be molded consistently at an agreed process window. This is especially important for medical housings, electrical enclosures, automotive parts, safety-related components, threaded assemblies, sealing interfaces, and components with strict cosmetic requirements.
Validation StageMain PurposeRequired EvidenceBuyer DecisionDesign for manufacturability reviewIdentify risks before steel cutting.Annotated CAD, change list, resin assumptions, and tooling proposal.Approve design changes and freeze the manufacturing model.Mold design reviewConfirm mold layout and function.2D/3D mold layout, gate plan, cooling plan, ejection concept, and steel list.Approve the tool architecture before manufacturing.First trialVerify initial filling, ejection, and major mold operation.Sample parts, process settings, photos, defect observations, and trial report.Authorize modifications and define next trial priorities.Dimensional inspectionConfirm critical dimensions and assembly interfaces.Inspection report, CMM data where required, gauges, and measurement conditions.Accept, adjust tolerances, or revise tool geometry.Functional assembly testVerify fit with mating components.Assembly samples, torque data, leak test, snap-fit results, or electrical checks.Approve function or request engineering correction.Cosmetic reviewAssess surface quality under defined conditions.Approved limit samples, lighting conditions, texture comparison, and defect criteria.Define acceptable appearance and rework limits.Production capability runShow stable output over an extended run.Cycle time record, reject rate, cavity comparison, process window, and maintenance notes.Approve production release or require corrective action.Final acceptance and shipmentTransfer an operating, documented tool.Mold test video, packing list, spare parts, maintenance guide, and ownership record.Release final payment and arrange shipment or production.The validation table should be adapted to the project risk level. A simple storage tray may only need visual inspection, fit verification, and a practical production run. A medical device enclosure may need tighter documentation, resin traceability, detailed inspection reports, controlled surface requirements, and functional testing after sterilization or chemical exposure. A mold intended for automotive supply may require cavity identification, process discipline, capability studies, and formal change control.
Buyers should begin with a clear request-for-quotation package. At minimum, provide a native CAD file or neutral 3D file, 2D drawings where critical dimensions exist, annual volume forecast, resin grade, color, surface requirements, assembly requirements, expected machine location, target delivery date, and expected mold life. If the mold will be transferred to another country, specify the machine platen size, tie-bar spacing, nozzle radius, locating ring, ejector connection, water fittings, voltage, and hot-runner controller requirements.
Do not compare quotations only by total mold price. Compare cavity number, steel choice, mold base, runner system, expected cycle time, included trials, sample quantity, inspection level, shipping method, spare parts, engineering change policy, warranty, and post-delivery support. A quote that omits these items may create avoidable cost later.
For uncertain demand, consider phased investment. An aluminum rapid tool or lower-cavity steel tool may validate the market before a larger multi-cavity production tool is commissioned. This approach is often useful for startups, industrial design firms, medical-device developers, consumer-product brands, and companies launching new products through distributors or online retail channels.
Shipping logistics also need early planning. Molds are heavy precision assets and should be protected against moisture, corrosion, and transport damage. Confirm export crating, rust prevention, mold locking, lifting points, customs documentation, and whether the tool will be shipped by air, sea, rail, or truck. For projects moving through ports such as Shenzhen, Ningbo, Shanghai, Rotterdam, Long Beach, or Jebel Ali, packaging and handling details can affect both cost and delivery reliability.
Injection molding supports a wide range of products because it combines repeatable geometry, material versatility, high output potential, and compatibility with inserts, overmolding, textures, and automated assembly. The mold design checklist should be customized to the end-use environment.
Applications may also combine multiple manufacturing processes. A plastic enclosure can require CNC-machined inserts, molded bosses, ultrasonic welding, painting, printing, screws, foam, labels, final assembly, kitting, and retail packaging. Selecting a manufacturing partner capable of coordinating these steps can reduce handoffs and shorten the launch schedule.
A global consumer-product brand developed a handheld device housing with a high-gloss front surface, internal snap fits, screw bosses, and a painted logo area. The initial CAD included insufficient draft near the sidewalls and thick bosses behind a visible surface. During the engineering review, the mold maker recommended increasing draft, coring the bosses, adjusting rib thickness, moving the gate to a less visible location, and defining acceptable parting-line placement. The resulting tool produced lower sink risk, cleaner ejection, and fewer cosmetic adjustments during pilot production.
An industrial equipment developer needed 500 enclosures for field testing before committing to a large production run. Instead of investing immediately in a high-cavity hardened mold, the team selected a rapid tooling route with a practical cavity layout, production-grade resin, and inspection of critical mounting features. The low-volume run allowed the customer to validate installation, cable routing, gasket compression, and user access. After field feedback, the final production mold incorporated design improvements without requiring major changes to a large initial tool.
An electrical product required metal threaded inserts and conductive contacts to be molded into a compact plastic carrier. The pre-build review focused on insert tolerance, loading orientation, resin temperature, contact protection, retention force, and automated versus manual insertion. The mold design included support features to prevent insert movement during injection and ejection. Functional testing confirmed thread integrity and electrical alignment before the tool was released for recurring production.
The supplier landscape includes machine builders, mold makers, contract molders, rapid tooling specialists, and full-service manufacturing partners. The companies below are real organizations with international relevance. Buyers should still evaluate each supplier against their specific resin, component size, regulatory, production-volume, and logistics requirements.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidChina, USA, UK, France, Germany, and customers in more than 25 countries.Rapid manufacturing integration, DFM support, rapid tooling, low-volume molding, and flexible production.Injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, finishing, assembly, packaging, and direct shipping.Husky TechnologiesGlobal operations serving packaging, medical, closure, and beverage producers.High-output injection molding systems and integrated production technology.Injection molding machines, hot runners, molds, controllers, and service for packaging applications.ENGELEurope, North America, Asia, and global industrial manufacturing markets.Injection molding equipment, automation, process technology, and digital production systems.Injection molding machines, robots, turnkey cells, process optimization, and automation solutions.ArburgGlobal network with strong European, North American, and Asian market presence.Precision molding technology and flexible production systems.Injection molding machines, automation, digital production support, and additive manufacturing systems.Rosti GroupEurope, Asia, and North America through international manufacturing operations.Contract manufacturing, injection molding, assembly, and supply-chain support.Plastic injection molding, medical and consumer manufacturing, assembly, and product industrialization.Nypro, a Jabil CompanyGlobal manufacturing locations serving healthcare and consumer markets.Complex healthcare manufacturing, engineering, and scalable production.Injection molding, precision components, medical manufacturing, automation, and assembly.FictivGlobal digital manufacturing network serving product development teams.Digital sourcing, prototyping, manufacturing coordination, and speed.Injection molding, CNC machining, 3D printing, urethane casting, and quality management support.This supplier comparison is intended to help buyers understand market positioning. Machine manufacturers such as ENGEL and Arburg are typically selected by companies operating molding facilities. Contract manufacturers such as Rosti Group and Nypro may support larger production programs with assembly requirements. Rapid manufacturing partners such as TEAM Rapid can be especially useful when a project needs fast design feedback, low-volume validation, tooling, machining, finishing, and flexible transition into production.
TEAM Rapid supports international product developers, engineers, startups, brand owners, distributors, OEM customers, and established manufacturers with rapid tooling, injection molding, insert molding, overmolding, CNC machining, 3D printing, vacuum casting, die casting, sheet metal fabrication, finishing, assembly, packaging, and direct shipping. Its ISO 9001:2015 quality management certification, more than 10 years of industry experience, more than 500 customers, more than 6,000 delivered projects, and service record across more than 25 countries provide practical evidence of its ability to manage prototype-to-production programs. The company does not promote a fixed captive list of branded mold components; instead, it specifies suitable mold bases, steels, resins, inserts, and production components according to the project requirements, while applying DFM analysis, inspection practices, machining tolerances down to 0.01 mm where applicable, and documented manufacturability reviews. TEAM Rapid supports OEM, ODM, wholesale, retail, regional distribution, and direct end-user projects with flexible order quantities from one prototype to more than 100,000 parts. Its delivery model includes turnkey and customer-owned tooling solutions, rather than BOO or on-site bulk supply services. While the company profile does not claim overseas subsidiaries or local warehouses, TEAM Rapid has established experience serving customers in the USA, UK, France, Germany, China, and other international markets through responsive online engineering communication, direct shipping, project coordination, packaging support, and after-sales follow-up. Customers can request a detailed rapid tooling service consultation for tooling strategy or submit part files through the global manufacturing quotation form for DFM feedback and pricing.
Injection mold design in 2026 will increasingly be shaped by faster development cycles, sustainability requirements, digital traceability, automation, and regional supply-chain resilience. Tooling teams will need to optimize not only part geometry but also energy use, resin selection, scrap reduction, data capture, and maintenance predictability.
Engineering teams are increasingly using AI-supported design analysis to identify draft problems, inconsistent wall thickness, possible undercuts, unsupported bosses, and likely warpage areas earlier in the design cycle. These tools do not replace experienced mold engineers, but they can speed up issue detection and help global teams review more design iterations before manufacturing begins.
Brands are under pressure to increase recycled content and reduce virgin plastic consumption. However, recycled resin can have wider property variation, altered flow behavior, contamination risk, color variability, and different shrinkage characteristics. Mold design reviews will need to address material consistency, gate size, venting, processing windows, and cosmetic acceptance criteria when recycled or bio-based polymers are specified.
Conformal cooling inserts manufactured through metal additive processes can follow complex cavity shapes more closely than traditional drilled channels. For suitable parts, this can improve cooling uniformity, reduce cycle time, and lower warpage. The technology is most valuable when the expected savings justify the added insert cost and when maintenance planning is considered.
Manufacturers increasingly track machine energy consumption, resin yield, runner waste, reject rate, and transport emissions. Hot-runner systems, optimized cooling, shorter cycles, reduced regrind dependence, and better cavity balance can contribute to lower resource use. Buyers should begin asking suppliers for practical process data rather than relying only on general sustainability claims.
Pressure sensors, cavity monitoring, cycle counters, cooling-flow monitoring, and digital maintenance records can improve production consistency. Predictive maintenance is especially useful for molds operating across multiple sites because it helps teams identify wear, blocked cooling channels, and process drift before a major production interruption occurs.
There is no single item that overrides all others, but wall thickness, draft, material selection, gate location, cooling, ejection, and tolerance requirements are usually the highest-impact areas. These factors strongly influence fill behavior, shrinkage, cycle time, part release, cosmetics, and long-term consistency.
DFM should be completed before steel is cut and ideally before the final product design is frozen. Early review allows changes to be made in CAD, where they are faster and less expensive than modifying a completed mold.
The required draft depends on resin, part depth, texture, surface finish, mold polish, and ejection direction. Smooth surfaces may need less draft than textured surfaces, while deep parts and highly textured exterior surfaces often need more. The mold maker should confirm draft recommendations during DFM.
A hot runner can reduce runner waste and support higher-volume production, but it adds initial cost, complexity, maintenance needs, and controller requirements. A cold runner may be more practical for low-volume parts, simpler tools, or projects where material changes are frequent. The right choice depends on annual volume, resin cost, part geometry, and production strategy.
A family mold can produce related parts in one cycle, but it should be used carefully. Parts with different sizes, wall thicknesses, fill behavior, or cooling requirements can create imbalance and higher scrap. Family molds are often most suitable for lower-volume matched sets rather than long-term high-output programs.
Request final mold drawings, steel and component information, trial reports, process settings, sample inspection data, spare-part list, maintenance instructions, mold photographs, shipping records, and clear ownership documentation. If the mold will be transferred internationally, also confirm water, electrical, controller, and machine-interface specifications.
Optimize wall thickness, reduce unnecessary material volume, use appropriate cavity count, improve cooling, minimize secondary operations, select the right resin, avoid overly tight non-functional tolerances, and approve DFM changes before tooling begins. Cost reduction is most effective when it improves manufacturability rather than simply lowering tool specifications.
-
Injection Mold Upkeep for the Global Market: Tool Life
Effective injection mold maintenance protects dimensional accuracy, reduces unplanned downtime, prevents flash and cosmetic defects, and extends the productive life of a mold. The most practical approach is to clean molding surfaces after every production run, inspect high-wear components regularly, lubricate approved moving areas, control moisture during storage, document each intervention, and schedule preventive maintenance based on shot count and part quality trends.
For buyers in the Global market, leading mold and injection molding support providers include TEAM Rapid in China, Husky Technologies in Canada, ENGEL in Austria, ARBURG in Germany, Milacron in the United States, and Sumitomo (SHI) Demag in Germany. Qualified international suppliers, including Chinese tooling companies with ISO-certified quality systems, responsive engineering support, and strong pre-sales and after-sales communication, can also be a practical option because of their cost-performance advantages.
Injection molds are precision production assets. A mold may contain hardened steel cavities, interchangeable inserts, cooling circuits, hot runner components, ejector systems, slides, lifters, hydraulic cylinders, sensors, guide pillars, wear plates, and precision shutoff surfaces. Each feature must operate repeatedly under pressure, heat, friction, resin flow, and mechanical movement. Without planned mold upkeep, small problems can become major tooling failures.
Across global manufacturing centers such as Shenzhen, Dongguan, Ningbo, Shanghai, Singapore, Munich, Stuttgart, Chicago, Toronto, Monterrey, Rotterdam, Dubai, and London, buyers increasingly expect stable quality from multi-cavity tools and short production lead times. Mold failures affect more than maintenance costs. They may delay assembly, disrupt packaging schedules, increase rejected parts, interrupt container loading at ports, and create missed retail or product-launch deadlines.
Regular injection mold maintenance helps manufacturers control the most common production risks: poor cooling performance, burn marks caused by blocked vents, flash caused by damaged shutoffs, dimensional drift from worn inserts, short shots from gate restrictions, scratches caused by ejector damage, and corrosion caused by moisture or aggressive resin additives. A documented maintenance plan is therefore not simply a workshop procedure; it is a quality and supply-chain protection system.
Mold maintenance should be divided by timing, production volume, part quality requirements, resin type, and mold complexity. A simple prototype tool running polypropylene has different maintenance needs from a high-cavity production mold processing glass-filled nylon, flame-retardant ABS, PVC, POM, or engineering-grade polycarbonate.
Maintenance TypeTypical TriggerMain TasksBusiness BenefitStart-up inspectionBefore each production runCheck water connections, clamps, ejector movement, sensors, fasteners, and visible damageReduces start-up defects and avoids running a damaged toolDaily careEach shift or campaignRemove resin residue, inspect vents, wipe molding surfaces, review part qualityMaintains cosmetic quality and stable fillingPreventive maintenanceBased on shot countClean cooling lines, replace seals, check wear plates, lubricate moving componentsPrevents unexpected production stopsCorrective maintenanceAfter a defect or breakdownRepair inserts, weld damage, polish cavities, replace ejector pins or hot runner partsRestores functional performanceSeasonal storage maintenanceBefore long-term storageDry circuits, apply corrosion protection, pack components, label mold conditionProtects the tool during idle periodsEngineering improvementRecurring defect trendsModify venting, cooling, gate geometry, ejection, or material flow pathsImproves long-term manufacturabilityThe table shows that mold maintenance is not limited to emergency repair. Start-up checks protect production readiness, routine cleaning protects surface quality, preventive work protects long-term tool life, and engineering changes address repeated process weaknesses that cannot be solved through cleaning alone.
A practical checklist should be specific enough for technicians to follow consistently while allowing the maintenance team to record mold condition. The best checklist is linked to a mold identification number, part number, resin, shot count, production machine, date, operator, maintenance technician, and next planned service interval.
Mold AreaInspection PointRecommended ActionWarning SignCavity and coreScratches, deposits, corrosion, polishing conditionClean with approved materials and polish only when necessaryGloss variation, drag marks, visible blemishesParting lineDamage, burrs, resin buildup, mismatchRemove residue and inspect shutoff surfaces carefullyFlash around the molded partVentsBlocked vents and contaminationClean vents without enlarging critical dimensionsBurn marks, short shots, trapped airEjector systemPin movement, return pins, plates, wearClean, lubricate approved locations, replace damaged pinsWhite marks, ejector impressions, stuck partsCooling systemFlow rate, leaks, scale, corrosion, connectorsFlush channels and replace worn seals or fittingsLonger cycle time, uneven shrinkage, warpageSlides and liftersGalling, friction, alignment, wear platesClean and apply suitable high-pressure lubricantNoise, scoring, sticking, dimensional variationHot runner systemHeater, thermocouple, nozzle tip, wiringVerify temperature response and inspect leakage pointsStringing, drooling, uneven fill, resin degradationFasteners and clampsLoose bolts, damaged threads, lifting pointsTorque-check where required and replace damaged hardwareMisalignment, mold movement, safety riskThis checklist is most effective when mold condition is linked to molded-part inspection data. For example, recurring flash on one cavity should trigger inspection of that cavity insert, shutoff surface, parting line, clamping condition, and process pressure. Repeated short shots should lead to checks of gate restrictions, venting, hot runner temperatures, material drying, and cooling balance rather than random machine adjustment.
Cleaning methods must match the mold steel, surface finish, resin type, and contamination level. Mirror-polished cavities require more careful handling than textured surfaces. Abrasive tools should not be used on critical molding surfaces unless approved by experienced tooling personnel. Improper polishing can alter geometry, damage texture, create mismatched cavity surfaces, and increase flash risk.
For standard cleaning, technicians commonly use lint-free cloths, approved mold cleaners, compressed dry air, soft non-metallic brushes, and appropriate cleaning tools for vents and channels. When handling electrical components, hot runners, sensors, or thermocouples, power isolation and electrical safety procedures must be followed. Cooling channels may require chemical descaling or mechanical flushing, but the selected method must be compatible with mold steel, seals, and water-system materials.
Lubrication should be controlled rather than excessive. Too much lubricant can migrate into cavities, contaminate molded parts, collect dust, and produce cosmetic defects. Use a lubricant suitable for guide pins, slideways, lifters, ejector systems, and high-load wear surfaces. Avoid applying lubricants directly to cavity surfaces unless the mold supplier specifically recommends a corrosion-protection product for storage.
For storage, the mold should be cleaned, dried, closed or protected as appropriate, labeled with its latest shot count and condition, and stored in a stable environment. Water circuits must not retain moisture when a mold will remain idle for an extended period. In humid coastal regions near ports such as Shenzhen, Ningbo, Hamburg, Rotterdam, Houston, or Singapore, corrosion prevention is especially important due to high humidity and salt-laden air exposure.
When selecting a maintenance provider, buyers should assess more than hourly repair rates. A low repair price can become expensive if the supplier cannot diagnose root causes, lacks precision machining capability, uses unsuitable replacement components, or fails to document tool changes. The preferred partner should understand mold design, resin behavior, injection molding parameters, metallurgy, dimensional inspection, and production scheduling.
Evaluation FactorWhat Buyers Should AskWhy It MattersPractical EvidenceTooling experienceCan the supplier repair cavities, cores, slides, and ejector systems?Complex repairs require specialized mold knowledgeExamples of similar tooling repairs and DFM reportsMachining capabilityAre CNC, EDM, wire EDM, grinding, and polishing available?Precision replacement parts must match the moldIn-house equipment list and tolerance capabilityQuality systemDoes the provider operate under a recognized quality framework?Maintenance records and inspections must be reliableISO 9001 certification and documented inspection processSpare part managementCan wear components be made or sourced quickly?Delays often come from unavailable inserts or ejectorsSpare-part list, lead-time plan, component drawingsEngineering supportCan the supplier identify design-related causes of defects?Repeated failures may need redesign rather than repairRoot-cause reports and process recommendationsGlobal communicationHow quickly are quotations, reports, and updates provided?International projects require fast decisionsNamed engineer, response procedure, digital reportingBuyers should also clarify ownership of mold drawings, spare inserts, maintenance records, and tool modifications. For contract manufacturing projects, the agreement should specify whether the tool remains at the factory, whether customers can request transfer, how storage is charged, and what condition documentation is required before shipment.
For projects requiring new tooling or replacement mold components, it is useful to request rapid tooling services that combine manufacturability analysis, precision machining, trial molding, and production support. This reduces the risk of treating each repair as an isolated event.
Injection mold maintenance is essential in industries where parts must meet repeatable visual, dimensional, safety, or functional requirements. Medical device housings may need clean cosmetic surfaces and controlled material traceability. Automotive interior and under-hood components require dependable fit, thermal resistance, and stable dimensional performance. Consumer electronics cases and enclosures demand consistent texture, snap-fit accuracy, logo details, and assembly alignment.
Other important applications include communication products, office equipment, electrical appliances, sanitary products, industrial controls, packaging components, food-contact products, laboratory devices, appliance covers, trays, caps, connectors, clips, fittings, and overmolded assemblies. In each sector, the maintenance interval should reflect the consequences of defect escape. A small scratch on a hidden industrial bracket may be acceptable, while a minor surface mark on a premium consumer product may result in full batch rejection.
Some mold features wear faster than others. Thin shutoffs, deep ribs, narrow vents, side actions, textured surfaces, hot runner gates, fine ejector pins, threaded unscrewing cores, and optical-grade polishing require closer inspection. Glass-filled polymers and mineral-filled materials can increase abrasion. Flame-retardant compounds may leave deposits. PVC and some additives can create corrosive conditions if processing and cleaning are not properly controlled.
ApplicationHigh-Risk Mold FeatureMaintenance FocusTypical Defect if NeglectedElectronic enclosuresTextured cavity and snap-fit detailsProtect texture and inspect precision clipsScratches, poor assembly fit, cosmetic defectsAutomotive partsLarge slides and complex shutoffsMonitor alignment, wear plates, and cooling balanceFlash, warpage, part mismatchMedical housingsPolished cavities and fine ventsPrevent contamination and maintain surface finishSurface marks, burn marks, rejected partsPackaging closuresHigh-cavity core and gate areasTrack cavity balance and replace worn componentsLeakage, short shots, inconsistent threadsOvermolded componentsInsert location featuresCheck insert seating and shutoff contactMisalignment, resin leakage, weak bondingIndustrial connectorsSmall pins and detailed core insertsInspect for pin damage and blocked ventsBroken features, incomplete fillingThe table demonstrates why maintenance schedules should not be based only on elapsed calendar time. A high-cavity cap mold operating continuously may need more frequent care than a lower-volume tool used occasionally. Likewise, a mold processing abrasive glass-filled nylon should be inspected more often than one molding unfilled polypropylene.
A multi-cavity housing mold began showing longer cycle times and uneven part warpage. The production team initially adjusted packing pressure and cooling time, but the problem continued. A maintenance inspection found mineral buildup in several cooling channels, reducing water flow and creating uneven mold temperatures. After flushing the channels, replacing worn water fittings, and verifying flow balance, the cycle time stabilized and warpage was reduced. The lesson is that cooling maintenance should be measured through flow and temperature performance, not visual inspection alone.
An automotive trim component developed recurring flash near a side-action feature. The mold was repeatedly cleaned, but the flash returned. A detailed inspection found wear on the slide shutoff and insufficient support from a worn wear plate. The maintenance team repaired the shutoff surface, replaced the wear plate, checked slide alignment, and reviewed clamping and injection-pressure settings. The improvement showed that persistent flash often has a mechanical root cause rather than a simple cleaning issue.
An industrial enclosure with deep ribs experienced burn marks near the end of fill. The molding machine was operating within the normal process window, but venting areas had accumulated residue. The maintenance procedure included vent cleaning, checking vent depth, confirming resin drying, and reviewing fill speed. Once air evacuation improved, the burn marks were removed without changing the part design. This case highlights the importance of maintaining venting features, particularly in deep, thin, or complex flow regions.
The following companies are recognized across major manufacturing regions for injection molding equipment, tooling, mold engineering, production support, or rapid manufacturing services. Buyers should verify local service availability, scope of work, equipment compatibility, lead time, and regional commercial terms before placing an order.
CompanyService RegionsCore StrengthsKey OfferingsTEAM RapidChina, North America, Europe, United Kingdom, France, Germany, and global export marketsRapid tooling, CNC machining, injection molding, DFM review, low-volume and volume productionMold making, maintenance support, replacement components, prototyping, custom injection molded partsHusky TechnologiesNorth America, Europe, Asia-Pacific, Latin America, global packaging marketsHigh-performance injection molding systems and packaging expertiseHot runners, molds, systems support, service programs, PET and closure manufacturing solutionsENGELEurope, Americas, Asia, global industrial molding marketsInjection molding machines, automation, process support, digital production toolsMachine service, automation integration, process optimization, molding technology supportARBURGGermany, Europe, North America, Asia and worldwide service locationsPrecision injection molding machinery and application engineeringMachine support, training, automation, process technologies, production optimizationMilacronUnited States, Canada, Mexico, Europe, Asia-PacificInjection molding equipment, hot runner technology, mold components and serviceMachine service, hot runners, temperature control, parts, process supportSumitomo (SHI) DemagEurope, North America, Asia-Pacific, global manufacturing networksAll-electric injection molding technology and process reliabilityMachine support, application engineering, spare parts, service and trainingThis supplier comparison is intended as a practical starting point. Equipment manufacturers may focus primarily on machine, hot runner, automation, or process support, while tooling manufacturers can provide cavity repair, insert replacement, polishing, machining, mold modification, and trial production. For global buyers, the best outcome often comes from coordinating the mold maker, molding factory, and machine or hot-runner specialist rather than relying on one party for every task.
TEAM Rapid supports customers from prototype development through repeatable injection molding production, with more than 10 years of industry experience, ISO 9001:2015 quality management, over 500 customers served in more than 25 countries, and more than 6,000 delivered projects. Its practical product strength comes from combining in-house CNC machining, EDM, wire EDM, polishing, tooling manufacture, injection molding capability, DFM analysis, inspection processes, and diversified plastic and metal material options; specific branded mold components are selected according to project requirements rather than promoted as a fixed component brand list. The company works with end users, product designers, distributors, dealers, brand owners, startups, established manufacturers, and individual innovators through flexible OEM, ODM, prototype, low-volume, recurring production, assembly, packaging, and direct-shipping models. TEAM Rapid does not offer BOO or on-site bulk supply services; instead, it provides customer-owned tooling, turnkey manufacturing, and customer-owned plant solution support where applicable. While the company profile does not claim overseas subsidiaries or local warehouses, TEAM Rapid has established export experience serving customers in the USA, UK, France, Germany, China, and other markets through direct project communication, engineering response within a few hours, manufacturing coordination, inspection support, packaging, and shipment management. This provides global buyers with documented engineering support before production and responsive online pre-sale and after-sale communication throughout the tooling and molding lifecycle.
For mold owners who need a maintenance review, replacement insert, production repair, or new rapid tool, TEAM Rapid can assess mold design risks through DFM feedback before machining begins. The company supports projects from one prototype to more than 100,000 parts, making it suitable for product launches, engineering validation, bridge production, replacement tooling, and scalable manufacturing programs. Buyers can submit drawings, CAD files, resin requirements, annual volume estimates, target finish, and existing mold-condition photos through the global manufacturing quotation request process.
By 2026, injection mold maintenance will increasingly move from calendar-based servicing toward data-supported predictive maintenance. Mold sensors, cavity pressure monitoring, cooling-flow monitoring, machine data capture, shot-count tracking, and digital maintenance records will help factories identify failure patterns earlier. Rather than waiting for flash, warpage, or a broken ejector pin, maintenance teams will use production data to plan service before quality declines.
Artificial intelligence-assisted process monitoring is expected to improve defect pattern recognition. Systems may compare cycle time, pressure curves, mold temperature, material moisture, ejection force, and cavity performance to identify abnormal trends. Digital mold passports will also become more common, particularly for global supply chains where tools may be moved between production sites. These records can include steel specifications, spare-part drawings, modification history, maintenance intervals, validation results, and approved process windows.
Sustainability will also influence tooling decisions. Better cooling design can reduce cycle time and energy use. Preventive care lowers scrap rates, extends mold life, and reduces the need for premature tool replacement. Manufacturers are also likely to increase attention to water treatment, closed-loop cooling systems, resin recovery, lower-emission production, and material traceability. International regulations affecting packaging, recycled content, medical traceability, product safety, and environmental reporting will make documented production and maintenance records increasingly valuable.
The frequency depends on mold complexity, resin type, surface finish, number of cavities, production hours, and shot count. Basic cleaning should occur after each production run, while preventive maintenance may be scheduled every defined number of cycles. High-wear molds processing glass-filled, mineral-filled, flame-retardant, or corrosive materials usually need more frequent inspection.
Flash can result from damaged parting lines, worn shutoff surfaces, poor slide alignment, excessive injection pressure, inadequate clamping force, mold mismatch, contaminated mating surfaces, or damaged inserts. The correct solution requires inspection of both mold condition and molding parameters.
Yes. Restricted cooling flow can increase cycle time, create uneven cooling, cause warpage, change shrinkage, and produce inconsistent dimensions. Cooling systems should be checked for flow, leaks, mineral scale, corrosion, and blocked channels.
Lubrication should follow the mold maker’s recommendations and should be applied only to approved moving components. Excessive lubricant can contaminate cavity surfaces, attract debris, and affect cosmetic part quality. Clean before applying new lubricant.
Molds should be cleaned, dried, protected against corrosion where necessary, labeled with status information, and stored in a stable environment. Cooling circuits should be drained or dried for long storage periods. In humid environments, corrosion prevention is particularly important.
Often yes. Existing molds can sometimes be improved through cavity insert replacement, vent modification, cooling upgrades, gate adjustments, slide repair, hot runner servicing, polishing, or ejection-system changes. A tooling engineer should evaluate whether the base mold structure remains sound before investing in modifications.
Maintain the mold ID, shot count, resin processed, production dates, defect history, maintenance actions, replaced parts, photographs, inspection results, repair drawings, technician name, and next recommended service interval. These records make root-cause analysis faster and support consistent quality across different production locations.
-
Global Market Guide to Selecting Steel for Injection Molds
Selecting steel for injection molds should start with the resin, expected production volume, cosmetic finish, part tolerance, cooling requirement, and operating environment. P20 is usually the practical choice for low-to-medium volume molds and rapid tooling. H13 is preferred for higher-temperature processing, glass-filled plastics, and longer production life. S136 is the stronger choice for corrosion resistance, polished optical surfaces, medical components, transparent parts, and PVC processing.
For most Global market projects, use pre-hardened P20 for economical tooling, hardened H13 for demanding production cycles, and stainless S136 when corrosion protection and mirror polishing matter. Tool steel should be selected together with mold design, cooling layout, gate position, part geometry, and maintenance planning rather than as an isolated purchasing decision.
Global buyers should compare steel traceability, hardness certification, heat-treatment capability, machining quality, lead time, and maintenance support. Qualified international suppliers, including Chinese mold manufacturers with ISO-based quality systems, responsive pre-sales and after-sales engineering support, and cost-performance advantages, can be a strong option for projects requiring fast tooling and molded parts.
Injection mold steel affects much more than the initial tooling price. The selected grade influences machining time, polishing performance, cycle time, cooling efficiency, wear resistance, mold life, dimensional stability, repairability, and consistency of molded parts. A low-cost material choice can become expensive if the cavity wears early, cooling channels corrode, molded surfaces develop defects, or the tool requires repeated welding and polishing.
For buyers in the Global market, material selection is especially important because products are often designed in one country, tooled in another, assembled in a third location, and sold through international distribution networks. A mold may need to run in Shenzhen, Ningbo, Singapore, Monterrey, Istanbul, Rotterdam, Chicago, or Frankfurt during its lifecycle. Steel selection must therefore consider transportation, storage humidity, resin availability, local maintenance capability, and production transfer requirements.
A well-selected steel grade supports predictable production. It helps control flash, sink marks, parting-line wear, ejector-pin galling, corrosion, polishing quality, and cavity dimensions. The correct steel also supports better DFM decisions, such as using appropriate draft angles, optimized ribs, balanced wall thickness, stable gate geometry, and adequate cooling circuits.
Injection mold steels are commonly grouped into pre-hardened steels, through-hardening steels, stainless steels, and specialty grades. The best choice depends on the working condition of each mold component. A mold base, cavity insert, core insert, slider, lifter, ejector plate, guide pin, and wear plate do not always need the same material.
Steel GradeTypical ConditionMain StrengthCommon Resin CompatibilityTypical Mold UsePractical LimitationP20Pre-hardened, commonly around 28–34 HRCGood machinability and economical tooling costABS, PP, PE, PS, PC, PA, TPERapid tooling, low-volume molds, housings, coversLower corrosion and wear resistance than hardened grades718 / 718HPre-hardenedBetter polishability and cleaner structure than standard P20ABS, PC, PMMA, PA, consumer-grade engineering plasticsMedium-volume cosmetic parts and mold insertsMay cost more than P20 without being necessary for simple partsH13Heat treated, often 48–52 HRC depending on applicationHot hardness, toughness, heat-check resistanceGlass-filled nylon, PC, PBT, PPS, high-temperature materialsCore inserts, cavities, slides, high-wear componentsRequires controlled heat treatment and longer manufacturing timeS136Hardened stainless steelCorrosion resistance and high-polish capabilityPVC, PMMA, PC, medical resins, optical-grade materialsMedical molds, transparent parts, humid production environmentsHigher material and machining costNAK80Pre-hardenedFine polishability, stable machining, good EDM finishABS, PC, PMMA, consumer and automotive cosmetic partsTextured surfaces, glossy covers, display-related housingsNot the first choice for highly corrosive resin environments420 Stainless SteelHardened stainless tool steelCorrosion resistance and moderate polishabilityPVC, flame-retardant plastics, medical resinsBudget-conscious corrosion-resistant mold componentsGrade quality varies significantly between steel millsD2 / Cr12MoVHardened cold-work steelHigh wear resistanceFilled plastics and abrasive applicationsWear inserts, cutters, high-wear mechanical featuresCan be less tough and more difficult to repair than H13The table shows why P20, H13, and S136 are not direct substitutes. P20 solves cost and lead-time needs. H13 solves thermal fatigue and abrasive wear challenges. S136 solves corrosion, cleanability, and high-finish requirements. A mold can also combine these steels. For example, a P20 mold base may use H13 gate inserts and slides, while S136 is reserved for cavity inserts exposed to PVC or moisture-sensitive applications.
P20 is one of the most widely used mold steels for injection molding because it is supplied pre-hardened and can often be machined without a separate hardening process. This reduces tooling lead time and avoids dimensional distortion associated with post-machining heat treatment. P20 is commonly selected for rapid tooling, low-volume manufacturing, bridge production, and medium-volume injection molds.
It performs well with common materials such as polypropylene, polyethylene, ABS, polystyrene, standard nylon, TPE, and many general-purpose engineering plastics. It is a sensible choice for enclosures, housings, trays, caps, appliance parts, office equipment components, automotive interior trim, and industrial covers where ultra-high polish or extreme wear resistance is not required.
However, P20 should be evaluated carefully for glass-filled materials, PVC, flame-retardant grades, highly humid production conditions, and tools intended to produce hundreds of thousands or millions of cycles. In such cases, corrosion, abrasion, and cavity wear can reduce tool performance. Surface treatments, nitriding, chrome plating, or localized H13 and S136 inserts may improve performance without requiring the entire mold to be made from premium steel.
H13 is a hot-work tool steel known for toughness, thermal stability, and resistance to heat checking. While it is strongly associated with die casting, it is also valuable in injection molds that process high-temperature resins, glass-filled materials, and abrasive compounds. H13 is frequently used for core inserts, cavity inserts, slides, lifters, gate inserts, and parts of a mold subjected to repeated thermal loading.
The steel is generally machined in an annealed or softer condition, then heat treated to the required hardness. This process demands controlled machining allowances, stable heat treatment, stress relief, precision grinding, and inspection. Poor heat treatment can lead to cracking, distortion, weak toughness, or inconsistent hardness. For that reason, buyers should request material certificates, hardness reports, and clear heat-treatment specifications.
H13 is suitable for reinforced nylon, PBT, PPS, high-temperature polycarbonate applications, and other resins that increase surface wear. It can also be selected for features with thin steel conditions, sharp ribs, aggressive shutoffs, or complex moving components. Although the upfront tool cost is higher than P20, the investment can be justified when the mold must maintain dimensions over long production runs.
S136 is a stainless mold steel commonly specified where corrosion resistance, polishability, cleanliness, and surface quality are critical. It is particularly suitable for PVC, flame-retardant resins, medical-grade polymers, transparent plastics, moisture-prone manufacturing conditions, and applications requiring a mirror finish.
For clear polycarbonate, PMMA, medical diagnostic housings, optical components, transparent lenses, laboratory consumables, cosmetic packaging, and high-gloss consumer parts, S136 can support better surface quality when machining and polishing are properly controlled. It is also useful for molds that may be stored or transported through humid ports and coastal regions where rust prevention is a practical concern.
S136 is more expensive than P20 and generally requires more careful machining, polishing, and heat treatment. The added cost is worthwhile only where corrosion control, optical surface requirements, hygienic maintenance, or part appearance demands it. For standard black ABS housings, P20 or 718H may be commercially more reasonable.
The resin is often the fastest starting point for selecting mold steel. Some resins are relatively gentle on the cavity, while others are abrasive, corrosive, or processed at high temperatures. Production volume then determines whether the initial investment in a higher-grade steel will return value through reduced maintenance and longer service life.
Project RequirementRecommended Steel DirectionReason for SelectionTypical PartsRecommended Tooling StrategyRisk if Under-SpecifiedPrototype or bridge production below 5,000 partsP20 or aluminum with steel insertsFast machining and lower startup costValidation housings, test enclosures, launch samplesRapid tooling with replaceable insertsUnnecessary capital cost from premium production steelLow-to-medium volume consumer productsP20 or 718HBalanced cost, machining speed, and surface qualityCovers, storage trays, appliance shellsPre-hardened mold base and quality cooling designPremature polish loss if low-grade material is usedHigh-gloss or textured cosmetic surfaces718H, NAK80, or S136Improved polishability and surface consistencyDisplay bezels, premium cases, cosmetic capsDedicated polishing allowance and controlled EDM processOrange peel, pitting, inconsistent texture reproductionGlass-filled or abrasive engineering plasticsH13, D2, or hardened wear insertsHigher wear resistance at gates and flow pathsGears, structural brackets, automotive under-hood partsHardened inserts in high-wear zonesGate erosion, flash, unstable dimensionsPVC, flame-retardant, or corrosive resinS136 or 420 stainless steelCorrosion resistance protects cavity surfaces and cooling areasElectrical components, medical parts, fittingsStainless cavity/core inserts and preventive maintenanceRust, pitting, surface defects, difficult mold cleaningHigh-temperature processingH13 or specialty hardened steelThermal stability and resistance to heat fatiguePPS connectors, reinforced nylon componentsHeat-treated inserts with engineered coolingCracking, deformation, accelerated wearTransparent optical or medical partsS136Mirror polishability, corrosion resistance, clean maintenanceLenses, clear chambers, diagnostic housingsHigh-quality polishing and protected handling processFlow marks, surface haze, rust contaminationMaterial selection should also account for the part’s visual standard. A molded surface with leather texture, matte finish, or paint coverage may not need premium polishing steel. By contrast, a clear lens, piano-black housing, chrome-plated decorative part, or medical component can reveal small cavity defects immediately. For these applications, steel cleanliness, polishing skill, EDM parameters, and mold protection procedures are as important as the nominal steel grade.
Buyers should not approve mold steel based on a grade name alone. Steel names can vary by mill, country, and supplier. A documented equivalent may perform differently depending on chemical composition, remelting process, cleanliness, delivery hardness, and heat-treatment quality. Purchasing teams should request clear specifications before tooling begins.
Buying CriterionWhat to ConfirmWhy It MattersSuggested Buyer ActionCommon Problem AvoidedRelevant Project StageSteel mill traceabilityMaterial certificate, heat number, grade specificationConfirms the actual steel source and compositionRequest certificates for cavity, core, and major insertsUnverified substitute materialQuotation and tooling kickoffHardness conditionPre-hardened level or final HRC targetDetermines wear resistance and machining approachState hardness requirements on approved drawingsSoft cavities or brittle insertsDesign reviewHeat treatmentVacuum hardening, tempering, stress relief, inspection methodControls distortion, toughness, and service lifeRequire heat-treatment records for H13 and S136 insertsCracking and unstable dimensionsTool manufacturingSurface finish requirementSPI finish, texture standard, optical polishing needDefines steel polishability and process planningProvide approved appearance samples where possibleMismatch between expected and actual cosmetic qualityDFM and mold designResin dataFull resin grade, filler percentage, flame-retardant packageIdentifies abrasion and corrosion riskShare resin datasheet before steel is orderedWrong material selection for filled or corrosive resinEarly engineeringTool life targetExpected annual volume and total lifetime cyclesSets a rational tooling investment levelSpecify prototype, bridge, low-volume, or production intentOverspending or premature mold wearRFQ stageMaintenance planCleaning, lubrication, spare inserts, storage protectionExtends mold life after deliveryInclude maintenance instructions and spare-part listRust, seizure, avoidable downtimeProduction and after-salesFor international projects, the mold supplier should provide a mold drawing, DFM report, material list, trial report, inspection information, and recommended maintenance schedule. If production will move between facilities, consider using standard mold components from globally recognized suppliers such as HASCO, DME, Meusburger, Misumi, or compatible equivalents. Standardization makes replacement parts and maintenance easier across regions.
Automotive suppliers often need H13 or hardened inserts for reinforced parts, clips, electrical connectors, under-hood components, and high-cycle interior systems. Consumer electronics brands frequently choose 718H, NAK80, or S136 for polished covers, device housings, display frames, and textured surfaces. Medical manufacturers may specify S136 because the mold needs corrosion resistance, cleanability, stable polish, and consistent output for regulated components.
Industrial equipment manufacturers need reliable steel choices for housings, cable-management systems, valves, fittings, control enclosures, and durable functional parts. Appliance companies may combine P20 mold bases with hardened inserts where repetitive shutoffs or wear areas exist. Packaging and consumer goods producers often balance cycle time, cavity count, and mold life, making cooling design and wear-resistant gate inserts critical.
Projects serving coastal regions, humid warehouses, and international shipping routes also benefit from corrosion planning. A mold stored near ports such as Shanghai, Hong Kong, Rotterdam, Hamburg, Los Angeles, Singapore, Dubai, or Santos can face environmental exposure if preservation is inadequate. Mold steel selection should be paired with anti-rust treatment, sealed packing, desiccants, and documented storage procedures.
Consumer electronics enclosure: A company launching a PC-ABS handheld device housing requires 20,000 pieces with a textured external surface and internal snap-fit features. P20 may be suitable for the mold base, while 718H can be selected for visible cavity surfaces if cosmetic requirements are stricter. H13 may be used locally for thin shutoffs and high-wear latch features. This approach controls cost while protecting critical areas.
Medical diagnostic device cover: A medical equipment developer needs clean white plastic covers and transparent inspection windows. The opaque housing may use 718H or P20 depending on volume, while transparent window tooling should use S136 to support high polish and reduce corrosion risk. The project should include validation samples, dimensional inspection, documented resin selection, and mold-cleaning guidance.
Glass-filled nylon automotive clip: An automotive supplier requires a clip that will run in a 150,000-piece program using glass-filled PA66. Standard P20 cavity surfaces may wear too quickly around gates, shutoffs, and thin locking features. H13 inserts, appropriate hardness, and planned spare components improve durability and reduce long-term maintenance costs.
PVC electrical fitting: A manufacturer needs molded PVC conduit fittings for export distribution. Because PVC processing can generate corrosive by-products, S136 or another suitable stainless steel should be used in cavity and core areas. The supplier should also specify regular mold cleaning, protective storage, and corrosion-control procedures.
The following companies are established mold steel suppliers with products used across international tooling markets. Buyers should verify the exact grade, local stock availability, certification package, and equivalent specification for each project. The best source may depend on steel availability near the selected tool shop, transportation time, and required technical support.
CompanyPrimary BaseService RegionsCore StrengthsKey OfferingsBest FitUddeholmHagfors, SwedenEurope, North America, Asia-Pacific, global distributionPremium tool steel development, clean steel technology, technical supportStavax ESR, Orvar Supreme, pre-hardened and stainless mold steelsHigh-polish, medical, automotive, and demanding production moldsASSABSingaporeAsia-Pacific, China, Europe, Americas through global networkTool steel supply, machining support, local stock programs718HH, P20 variants, Stavax ESR, Orvar SupremeRegional Asian tooling programs and internationally standardized projectsDaido SteelNagoya, JapanJapan, Asia, Europe, North AmericaSpecialty steels, pre-hardened grades, consistent material qualityNAK80, DC53, tool steels for molds and precision manufacturingHigh-polish consumer products and precision mold applicationsBÖHLER EdelstahlKapfenberg, AustriaEurope, Americas, Asia-Pacific, global sales networkSpecial steels, stainless grades, technical metallurgy expertiseM340, W302, corrosion-resistant and hot-work tool steelsMedical, optical, high-temperature, and corrosion-sensitive moldingFinkl SteelChicago, United StatesNorth America and international industrial customersLarge blocks, mold base steel, domestic supply capabilityPre-hardened mold steels, mold plates, specialty steel productsNorth American mold builders and large mold base requirementsMeusburgerWolfurt, AustriaEurope and global mold-making customersStandard mold bases, precision plates, mold componentsMachined plates, standard frames, guide elements, accessoriesToolmakers needing standardized components and fast configurabilityHitachi Metals / ProterialTokyo, JapanJapan and international industrial marketsSpecialty alloy expertise and high-performance material developmentTool steels and specialty materials through regional channelsProjects requiring specific Japanese material standards or equivalentsThese suppliers provide valuable options, but steel brand alone does not guarantee mold quality. The mold maker’s CNC machining, EDM, polishing, heat treatment, fitting, cooling design, assembly, mold trial process, and inspection discipline determine whether the selected steel performs as expected. Buyers should evaluate the complete tooling process, not only the steel certificate.
TEAM Rapid supports Global market customers with rapid tooling, plastic mold making, injection molding, CNC machining, finishing, assembly, and direct shipping from an integrated China-based manufacturing network. With more than 10 years of manufacturing experience, ISO 9001:2015 quality management certification, more than 6,000 delivered projects, and customers in over 25 countries, the company applies DFM analysis before tooling to identify risks involving resin flow, wall thickness, draft, cavities, cooling, cycle time, and material choice. For mold steel selection, TEAM Rapid can recommend practical combinations such as P20 for cost-efficient rapid tooling, H13 inserts for wear-sensitive areas, and S136 for corrosion-resistant or polished cavities, supported by controlled machining, EDM, polishing, inspection, and trial molding. The company serves end users, product designers, distributors, dealers, brand owners, startups, and established manufacturers through flexible OEM, ODM, low-volume, recurring production, wholesale, and regional supply cooperation models. Its operational model is turnkey manufacturing and customer-owned tooling support rather than BOO or on-site bulk supply services. Although TEAM Rapid does not claim overseas subsidiaries or local warehouses in every Global market location, it has established international service experience through one-to-one engineering communication, fast quotation responses, integrated production resources, packaging, limited warehousing, and direct shipment to customers in markets including the USA, UK, France, Germany, and other regions. This combination gives buyers practical pre-sale engineering support, production updates, inspection-based quality control, and after-sales coordination without managing multiple disconnected suppliers.
Customers needing a faster transition from prototype validation to low-volume or production molding can review rapid tooling services for international product development to understand available tooling pathways. For a steel recommendation based on resin, part geometry, annual volume, and surface requirement, buyers can request a custom injection mold tooling quotation with 3D files and material details.
By 2026, mold steel selection is expected to become more data-driven. Toolmakers are increasingly combining mold-flow simulation, cycle-time analysis, sensor data, predictive maintenance, and production traceability to determine where premium steel provides measurable value. Rather than building an entire tool from one grade, more projects will use hybrid construction: economical mold bases combined with higher-performance inserts in gates, cores, slides, shutoffs, and corrosive-resin zones.
Sustainability will also influence tooling decisions. Longer-lasting molds reduce replacement steel consumption, machine downtime, material waste, and emergency logistics. Better cooling performance can shorten cycle time and reduce energy use per molded part. Manufacturers are also expected to place greater emphasis on repairable insert designs, reusable mold bases, optimized cavity counts, and modular tooling systems that extend the useful life of production assets.
Global policy and customer requirements are likely to increase demand for material traceability, recycled-content documentation, product quality records, and controlled chemical processing. Medical, automotive, electrical, and consumer brands may require more detailed evidence of resin compatibility, steel origin, inspection methods, and controlled production practices. For this reason, mold steel certificates, hardness reports, maintenance records, and trial documentation will remain essential purchasing documents.
Provide the following information when requesting a quotation or technical review: 3D CAD files, 2D drawings if available, resin brand and grade, filler percentage, flame-retardant requirement, annual production volume, total lifetime volume, required surface finish, color, cosmetic standards, mold location, target production date, and expected maintenance arrangements.
Also identify whether the tool is intended for prototype validation, bridge production, low-volume commercialization, or long-term production. This distinction helps prevent two common errors: paying for production-grade steel when rapid tooling is sufficient, or selecting low-cost steel for a tool that must run high volumes with abrasive resin.
P20 is suitable for many injection molds, especially rapid tooling, low-volume production, consumer housings, trays, covers, and general-purpose plastic parts. It is not always sufficient for corrosive resins, highly abrasive glass-filled materials, high-temperature molding, or very long production programs.
Choose H13 when the mold will process high-temperature or glass-filled resins, when thermal fatigue is a concern, or when critical inserts need improved wear resistance and toughness. H13 is often used selectively in gates, cores, slides, and shutoff areas instead of across the full mold.
S136 is a stainless mold steel with stronger corrosion resistance and high-polish capability. Its cost reflects the material properties, machining demands, heat-treatment requirements, and value in applications such as PVC molding, medical parts, transparent components, and humid production environments.
Yes. Many efficient molds use P20 for the mold base, H13 for high-wear inserts, and S136 for corrosion-sensitive or high-polish cavity areas. This mixed-steel strategy can improve performance while controlling tooling cost.
Steel grade can affect cooling efficiency and long-term cavity stability, but cooling channel design, water flow, mold temperature control, wall thickness, and resin processing conditions usually have a greater direct effect on cycle time. Steel should be selected together with thermal design.
Request material certificates, steel grade confirmation, hardness reports, heat-treatment records when applicable, mold drawings, DFM feedback, trial reports, inspection reports, and maintenance recommendations. These documents help protect quality during production and future mold transfers.
Yes. Established Chinese mold manufacturers can source and machine P20, H13, S136, 718H, NAK80, and equivalent grades. Buyers should verify material traceability, machining capability, heat-treatment controls, inspection procedures, communication quality, and after-sales support before selecting a supplier.
-
SPI Mold Classifications Guide for Global Market Buyers
SPI mold classifications describe the expected service life, construction quality, maintenance standard, and production suitability of an injection mold. Class 101 is the highest-duty category for very large production volumes, while Class 102 suits medium-to-high production, Class 103 is a general-purpose production mold, Class 104 is intended for low-volume production, and Class 105 is normally a prototype or sample mold.
For global buyers, the practical choice is usually Class 103 for regular commercial production, Class 104 for limited launches or market testing, Class 101 or Class 102 for long-running programs, and Class 105 for early design validation. The classification is a planning guide rather than a substitute for a detailed tooling specification covering steel, cavities, cycle time, cooling, tolerances, maintenance, and acceptance testing.
Qualified international suppliers, including experienced Chinese mold and molding companies with ISO certification, documented inspection, export experience, and responsive pre-sales and after-sales support, can also be considered. Their cost-performance advantage may be significant when engineering review, tooling manufacture, molded parts, finishing, assembly, and delivery are coordinated under one program.
The Society of the Plastics Industry, now known as the Plastics Industry Association, developed a widely used mold classification system to help buyers match tooling investment with expected production demand. The classes are commonly referenced by mold makers, injection molders, product developers, and procurement teams across North America, Europe, Asia, and other manufacturing regions.
The classification does not simply rank a mold as good or bad. It indicates how extensively the tool is engineered, how durable its components are expected to be, how much production it should support, and how suitable it is for repeated manufacturing. A Class 105 mold can be perfectly appropriate for a prototype, while a Class 101 mold may be wasteful for a short market trial.
SPI terminology is often used together with a purchaser’s own tooling standard. A buyer may specify P20 or H13 steel, hardened cavity inserts, replaceable wear plates, hot-runner brands, mold-flow analysis, cavity pressure monitoring, or a defined number of accepted shots. These details should be written into the purchase order because classification alone cannot define every technical feature.
Class 101 molds are built for extremely high production volumes and long service life. They normally use high-grade, hardened tool steels in critical areas, carefully engineered cooling, robust ejection, replaceable wear components, and strict dimensional control. They are suitable for products expected to run continuously for many years, often in demanding automotive, medical, consumer, or industrial programs.
Class 101 tooling typically requires the greatest upfront investment. It may include multiple cavities, hot runners, automated part removal, complex slides or lifters, cavity pressure monitoring, and extensive preventive-maintenance provisions. The higher cost can be justified when millions of cycles, low downtime, and consistent part quality are more important than the lowest initial tooling price.
Class 102 molds are intended for medium-to-high production volumes where reliable repeatability is essential but the projected life may not justify every feature of a Class 101 tool. They are often used for commercial products with established demand, replacement parts, and programs expected to run for several years.
Depending on the product and resin, a Class 102 mold may use hardened steel in wear areas, pre-hardened steel in other sections, a standard or premium hot runner, engineered cooling channels, and replaceable inserts. It can offer a practical balance between tool life, maintenance access, cycle performance, and capital cost.
Class 103 is widely selected for ordinary production requirements. It is generally suitable for moderate production quantities, new products entering the market, and parts where the expected annual volume is meaningful but not extremely high. Many low-to-medium volume commercial programs use a Class 103 mold as their starting production tool.
The exact life depends on material, part geometry, cycle time, mold maintenance, and steel selection. Abrasive glass-filled resins, corrosive additives, high injection pressure, and frequent color changes can shorten useful life. A Class 103 tool should still receive proper cooling design, venting, ejection analysis, dimensional inspection, and trial validation.
Class 104 molds are designed for limited production runs. They can be appropriate for pilot production, seasonal products, regional launches, spare parts, customized products, and products whose commercial demand is still uncertain. Aluminum, pre-hardened steel, or other cost-efficient materials may be considered when the expected shot count is limited.
Class 104 does not mean careless construction. The mold must still produce acceptable parts and provide safe operation. Buyers should define the expected quantity, number of production batches, storage conditions, and repair responsibility. A low-volume tool that is maintained correctly can sometimes exceed its original target life.
Class 105 molds are intended for prototype quantities, design verification, and very limited sampling. The tool may use aluminum, soft steel, simplified inserts, or other economical construction methods. It is useful for checking assembly, appearance, ergonomics, basic function, and early customer feedback before committing to a longer-life production mold.
Class 105 is not normally the right choice for a product launch requiring thousands of parts every month. However, it can reduce risk when a design is still changing. The buyer should confirm whether the tool is repairable, whether inserts can be upgraded, and whether the sample parts accurately represent the final production process.
The following comparison gives a practical starting point. Actual tool life is affected by resin, mold design, maintenance, machine settings, part geometry, and the supplier’s workmanship. Buyers should request a written guarantee or agreed acceptance target rather than relying only on a class label.
SPI classTypical purposeRelative production volumeTypical construction approachCommercial decisionClass 101Continuous, demanding productionVery high, often multi-million cycle programsHardened steel, robust components, optimized cooling and maintenance accessChoose when downtime and replacement-tool risk are expensiveClass 102Established commercial productionHigh to medium-highDurable steel in wear areas with engineered cooling and ejectionChoose for reliable multi-year programs without maximum-duty investmentClass 103Standard commercial partsModerateProduction-grade steel and conventional or hot-runner systemsChoose for most new products with predictable demandClass 104Limited production and pilot runsLowCost-efficient steel or aluminum with appropriate production featuresChoose for launches, seasonal products, and regional demand testsClass 105Prototype and design validationVery lowPrototype inserts, aluminum, soft steel, or simplified toolingChoose while geometry, material, or market acceptance is still changingCustom specificationSpecial performance requirementDefined by the programBuyer-selected steel, components, monitoring, and maintenance strategyUse when an SPI class alone cannot describe the required risk levelThis table is useful for early budgeting, but it should be followed by a tooling design review. For example, a small medical housing made from glass-filled resin may need stronger wear protection than a much larger part made from an unfilled commodity polymer. Similarly, a tool with complex lifters may require more maintenance access than a simple two-plate mold.
Start with the total expected lifetime quantity, not only the first purchase order. Add forecast demand, replacement-part requirements, regional sales, engineering samples, rejected parts, safety stock, and possible future programs. A tool selected for 20,000 parts may become uneconomical if the product later sells 500,000 units.
Next, evaluate the resin. Polypropylene and ABS generally create different tooling demands from glass-filled nylon, PEEK, PC, PVC, or flame-retardant engineering polymers. Abrasive fillers, corrosive additives, high processing temperatures, and demanding cosmetic surfaces may justify stronger steel, surface treatment, or a higher classification.
Review the product architecture. Undercuts, threads, collapsible cores, lifters, thin walls, deep ribs, texture, optical surfaces, tight sealing features, and insert molding all affect tooling cost and maintenance. A supplier should provide a DFM report identifying draft, wall-thickness, sink, weld-line, air-trap, gate, warpage, and ejection risks before steel is cut.
Consider production geography and logistics. A buyer in the United States may compare suppliers in Ohio, Michigan, California, Mexico, Germany, the United Kingdom, or China. A buyer in Europe may evaluate providers near Stuttgart, Milan, Lyon, Birmingham, or Shenzhen. Tool ownership, repair location, shipping terms, spare inserts, and response time can matter as much as the initial quotation.
Finally, connect the mold class to the business model. Prototype tooling may be best for a funded development project, rapid tooling may be suitable for a short launch window, and hardened production tooling may be needed for a regulated or safety-critical product. Do not pay for a Class 101 mold if the design is likely to change next month.
Specification areaQuestions to askWhy it mattersRecommended evidenceSteel and hardnessWhich steel grades are used for cavities, cores, inserts, and plates?Steel affects wear life, polishability, corrosion resistance, and repair optionsSteel certificates, hardness records, and component drawingsCavity configurationIs the mold single-cavity, multi-cavity, family, or interchangeable?Cavity count changes unit cost, balance, cycle output, and qualification effortLayout drawing, filling analysis, and cavity identification planRunner and gatingWill the tool use cold runners, hot runners, valve gates, or sequential gating?Runner design influences scrap, appearance, pressure, cycle time, and maintenanceRunner diagram, component brand, and spare-parts listCoolingAre channels balanced and accessible for cleaning?Cooling affects warpage, cycle time, tool life, and dimensional consistencyCooling layout, flow analysis, and temperature trial resultsEjection and automationHow will the part be ejected, detected, removed, and packed?Reliable ejection reduces deformation, damage, and operator dependencyEjection sequence, robot interface, and sample-cycle videoAcceptance and maintenanceWhat shot target, dimensional tolerance, repair response, and warranty apply?Clear obligations prevent disputes after deliverySigned acceptance criteria, inspection report, and maintenance scheduleAsk for a mold-flow report when the part has long flow lengths, thin walls, multiple gates, tight cosmetic requirements, or difficult engineering resin. Mold-flow simulation cannot eliminate all production risk, but it can expose likely filling imbalance, weld lines, air traps, cooling differences, and warpage before machining.
Class 101 tooling usually has the highest initial price because it may require hardened steel, precision components, complex cooling, cavity balancing, automation interfaces, and more extensive validation. Class 105 tooling usually has the lowest price, but its limited life and lower upgrade flexibility can create additional cost if the design is not yet stable.
Tool price should be separated from molded-part price. A low-cost mold can create a high unit cost if it has a long cycle, excessive runner waste, manual demolding, or frequent maintenance. Conversely, a more expensive multi-cavity mold may produce a lower total cost when volume is sufficiently high.
Lead time depends on part complexity, steel availability, mold size, number of cavities, surface finish, hot-runner procurement, design approval, sampling, and correction loops. Buyers should request a timeline that separates DFM approval, steel ordering, CNC machining, EDM, polishing, assembly, first trial, modifications, final inspection, and shipment.
For customers that need a bridge between prototypes and full production, rapid tooling can be practical. TEAM Rapid states that its rapid tooling and molded-part programs can often be completed in approximately 5 to 25 days, depending on project requirements. Its engineers also provide DFM and manufacturability analysis to identify risks before tooling begins. Buyers should confirm the exact schedule, material, cavity count, inspection plan, and shipping method for each project.
The following companies are established names that buyers may evaluate for mold systems, injection molding equipment, tooling, or production support. Their capabilities and service availability vary by country and project size, so a buyer should confirm whether the quoted provider is the manufacturer, an authorized regional office, or an independent mold-making partner.
CompanyService regionsCore strengthsKey offeringsBest fitTEAM RapidChina with export support for North America, Europe, Asia, and other global marketsFast tooling, engineering-led DFM, flexible quantities, and integrated manufacturingRapid tooling, injection molding, CNC machining, 3D printing, vacuum casting, die casting, finishing, assembly, packaging, and direct shippingPrototypes, Class 104 or Class 103 programs, low-volume production, and transition to larger productionHusky TechnologiesNorth America, Europe, Asia, and worldwide customer operationsHigh-output injection systems and packaging production technologyInjection molding systems, hot runners, controllers, molds, and service supportHigh-volume packaging and demanding production environmentsMilacronNorth America, Europe, India, China, and international marketsIntegrated injection molding machinery, controls, and hot-runner technologyInjection machines, hot runners, process controls, mold technologies, and lifecycle servicesIndustrial and commercial production requiring coordinated equipment supportENGELAustria, Germany, the United States, China, and global marketsAutomation, process integration, precision molding, and energy-efficient cellsInjection molding machines, robots, turnkey cells, process control, and technical serviceAutomotive, medical, packaging, and complex automated productionARBURGGermany, Europe, the United States, Asia, and international marketsPrecision injection molding, automation, and process developmentAll-electric and hydraulic machines, robots, turnkey systems, and application consultingPrecision components, medical products, technical parts, and connected factoriesHaitian InternationalChina with extensive export distribution and service coverageBroad injection machine range and competitive capital costServo-hydraulic and electric injection molding machines, automation options, and regional supportCost-sensitive production programs and general industrial moldingThese companies do not all offer the same type of service. Husky, Milacron, ENGEL, ARBURG, and Haitian are primarily associated with molding machines, systems, and production technology, while TEAM Rapid is positioned as a manufacturing partner for tooling, parts, and related processes. A purchaser seeking a mold should clarify whether the supplier will design and manufacture the tool, run it in-house, transfer it to a customer-owned plant, or provide only equipment.
In the United States and Canada, buyers often prioritize technical documentation, mold ownership, repair turnaround, domestic sampling, and compatibility with existing molding machines. Ask whether the supplier can provide inch or metric drawings, SPI surface requirements, cavity-pressure data, spare inserts, and a clear process for returning a tool for repair.
In Germany, France, Italy, and the United Kingdom, buyers frequently focus on traceability, dimensional capability, sustainability reporting, regulatory documentation, and integration with established quality systems. Suppliers serving these markets should be able to communicate clearly in English or the required local business language and provide controlled revisions of drawings and inspection reports.
In Japan, South Korea, Singapore, and other Asian manufacturing hubs, buyers may emphasize precision, rapid engineering communication, automation compatibility, and local maintenance coordination. In Australia, the Middle East, Africa, and Latin America, shipping reliability, spare parts, remote troubleshooting, customs documentation, and regional distributor support may be especially important.
Regardless of location, request at least one video or live review of the supplier’s tooling workshop, a sample inspection report, evidence of comparable resin experience, and references for a similar mold size or complexity. A polished website is not sufficient evidence of manufacturing capability.
TEAM Rapid combines ISO 9001:2015 quality management with more than 10 years of manufacturing experience, over 6,000 delivered projects, more than 500 customers, and service to customers in more than 25 countries; its product strength comes from controlled plastic and metal material selection, in-house machining and tooling capability, complete inspection, DFM review, and production processes that cover injection molding, rapid tooling, CNC machining, 3D printing, vacuum casting, die casting, sheet metal fabrication, finishing, assembly, and packaging rather than relying only on order taking. It serves end users, product developers, distributors, dealers, brand owners, startups, established manufacturers, and individual innovators through practical OEM and ODM cooperation, project-based production, wholesale quantities, low-volume orders, recurring supply, and regional distribution arrangements where commercially appropriate; its flexible capacity extends from one prototype to more than 100,000 parts. TEAM Rapid’s published profile does not claim overseas subsidiaries or permanent local warehouses in every customer country, so buyers should verify the exact local stock and repair arrangement, but the company provides China-based export coordination, limited warehousing, direct shipping, one-to-one engineering communication, rapid online response, inspection documentation, and after-sales project support for customers in North America, Europe, Asia, and other markets, with experience handling both Asian and Western business practices. It provides EPC/turnkey and customer-owned plant solutions for tooling, molded parts, assembly, packaging, and supply coordination when specified, not BOO or on-site bulk supply services, and its China manufacturing base can offer a cost-performance advantage while maintaining a documented route from prototype through low-volume and volume production.
For a buyer comparing mold classifications, TEAM Rapid may be relevant when the project requires Class 105 prototype tooling, Class 104 limited production tooling, Class 103 general-purpose production, or a staged path from sample validation to repeatable commercial supply. Its engineering team can review draft angles, wall thickness, parting lines, gates, cooling, ejection, shrinkage, and material selection before quotation. Customers can begin with the rapid tooling service for global projects and submit drawings, 3D files, material requirements, annual volume, and target delivery through the online manufacturing quotation form.
Automotive programs may require Class 101 or Class 102 tooling for interior trim, exterior components, under-hood parts, ducts, brackets, and functional housings. Glass-filled materials, dimensional stability, surface texture, and long production life should be considered together.
Medical and laboratory products often require controlled materials, traceability, clean handling, tight dimensional requirements, and validated processes. A Class 103 or Class 102 mold may be suitable for a commercial device, while Class 105 or Class 104 tooling can support early design verification. Regulatory requirements must be agreed separately because SPI classification does not certify a medical product.
Consumer electronics, appliances, communication products, office equipment, sanitary products, and industrial controls often use Class 103 or Class 104 molds depending on forecast quantity. Cosmetic appearance, texture, color consistency, snap fits, living hinges, light pipes, and assembly alignment can be more important than extreme shot life.
Packaging, closures, thin-wall containers, and high-output caps often require specialized multi-cavity tools, hot runners, balanced filling, high-speed cooling, and automated inspection. These applications may justify Class 101 or Class 102 construction even when the individual part is small.
A startup developing a handheld diagnostic accessory may still be changing the enclosure, battery interface, and button geometry. Class 105 tooling or a rapid aluminum tool can produce samples for ergonomic testing and initial assembly checks. Once the design is frozen and demand is validated, the supplier can convert the design into Class 103 or Class 102 production tooling with improved steel and a multi-cavity layout.
A brand selling a seasonal organizer may forecast 15,000 to 40,000 parts over two years. A Class 104 mold may be financially appropriate if the design is stable and the tool is stored correctly between seasons. The buyer should retain spare inserts, document cleaning procedures, and confirm whether the tool can be upgraded if sales exceed expectations.
An automotive supplier expecting sustained annual production and strict appearance requirements may select Class 101 or Class 102 tooling. The specification should include material grade, texture standard, cavity balance, cooling performance, dimensional capability, replacement inserts, preventive maintenance, and tool transfer provisions. A low-cost prototype tool can still be used first to validate fit and surface design.
An industrial equipment manufacturer may need only 3,000 initial housings while testing several sales channels. Class 103 tooling offers a reasonable middle ground when the design is substantially mature but future demand is not fully known. A modular insert design can preserve the option to modify connectors, mounting bosses, or label areas without replacing the entire mold.
These are planning scenarios, not guaranteed production results. The correct class should be confirmed through part geometry, resin, forecast, machine capability, quality requirements, and the supplier’s documented tooling proposal.
TrendTechnology or policy driverEffect on mold classification decisionsBuyer actionDigital mold monitoringSensors, connected controllers, cavity-pressure measurement, and cloud analyticsImproves traceability and helps extend useful life through predictive maintenanceSpecify data ownership, sensor locations, alarms, and reporting requirementsEnergy-efficient moldingAll-electric machines, optimized cooling, heat recovery, and lower-carbon production targetsCycle efficiency may influence total cost more than initial mold priceRequest cycle-time assumptions, cooling analysis, and energy data where availableRecycled and bio-based resinsExtended producer responsibility, recycled-content rules, and customer sustainability goalsVariable shrinkage, contamination, and additives may increase tooling and process riskValidate the actual resin grade and test dimensional stability before production releaseModular and repairable toolingShorter product cycles, regional customization, and reduced material wasteReplaceable inserts can make Class 103 or 104 tools more adaptableAsk for insert boundaries, spare-part pricing, and modification accessDigital product passportsTraceability and emerging product sustainability policies in major marketsTool and material records may become part of supply-chain complianceMaintain controlled steel, resin, inspection, maintenance, and revision recordsDistributed manufacturingRegional production, tariff management, shorter supply chains, and geopolitical risk reductionTool transferability and customer-owned plant compatibility become more valuableDefine ownership, export documents, machine interfaces, and relocation supportFuture classification decisions will increasingly consider the complete production system rather than only the physical mold. A tool that runs efficiently, records process data, supports recycled resin, and can be repaired or transferred may create lower total environmental and financial risk than a cheaper tool with poor documentation.
No. Class 101 is appropriate for very high-volume, long-running production. It may be unnecessary for a product with uncertain demand, frequent design changes, or a short market life. The best class is the one that matches risk, forecast, resin, quality requirements, and total cost.
It can be used for very limited sales or pilot quantities if the supplier confirms that the tool can produce acceptable parts. It is normally not recommended for sustained commercial production because service life and repeatability are limited compared with production tooling.
Class 103 is often a practical choice when the design is stable and moderate production is expected. Class 104 may be more economical for a limited launch, while Class 105 or rapid tooling is useful when the design still needs validation.
No. It provides a general tooling-life and construction framework, but the buyer should specify cavity steel, core steel, hardness, inserts, surface treatment, hot-runner components, and corrosion or wear requirements separately.
Published industry descriptions commonly associate Class 101 with the longest life and Class 105 with prototype quantities, but exact shot counts vary by source and application. Resin, pressure, temperature, maintenance, geometry, and workmanship have a major effect. Use a written supplier guarantee tailored to the project.
Compare technical capability, response time, inspection, ownership terms, logistics, repair support, and total landed cost. An international supplier can be attractive when it offers strong DFM, documented quality systems, competitive pricing, export experience, and reliable communication. A local supplier may be preferable when immediate on-site maintenance is essential.
Provide the 3D model, 2D drawing, resin and color, annual and lifetime quantity, target cycle time, cavity preference, surface finish, tolerance, machine information, packaging needs, delivery location, mold class target, inspection requirements, and expected launch date.
Yes. TEAM Rapid offers rapid tooling, injection molding, CNC machining, additive manufacturing, vacuum casting, metal processes, finishing, assembly, packaging, and direct shipping. Its stated production range extends from one prototype to more than 100,000 parts, subject to project requirements. Buyers should request a project-specific DFM report, schedule, tooling proposal, and quality plan.
TEAM Rapid provides EPC/turnkey and customer-owned plant solutions when defined by the project, including tooling, manufacturing coordination, assembly, packaging, and supply support. It is not presented as a BOO or on-site bulk supply provider. The commercial scope, ownership, local support, and shipping terms should be confirmed before order placement.
SPI mold classifications are most useful when they create a shared starting point between the buyer and the toolmaker. With a clear production forecast, verified material plan, DFM review, documented acceptance criteria, and realistic maintenance strategy, global buyers can avoid both under-designed prototype tooling and unnecessarily expensive production molds.
